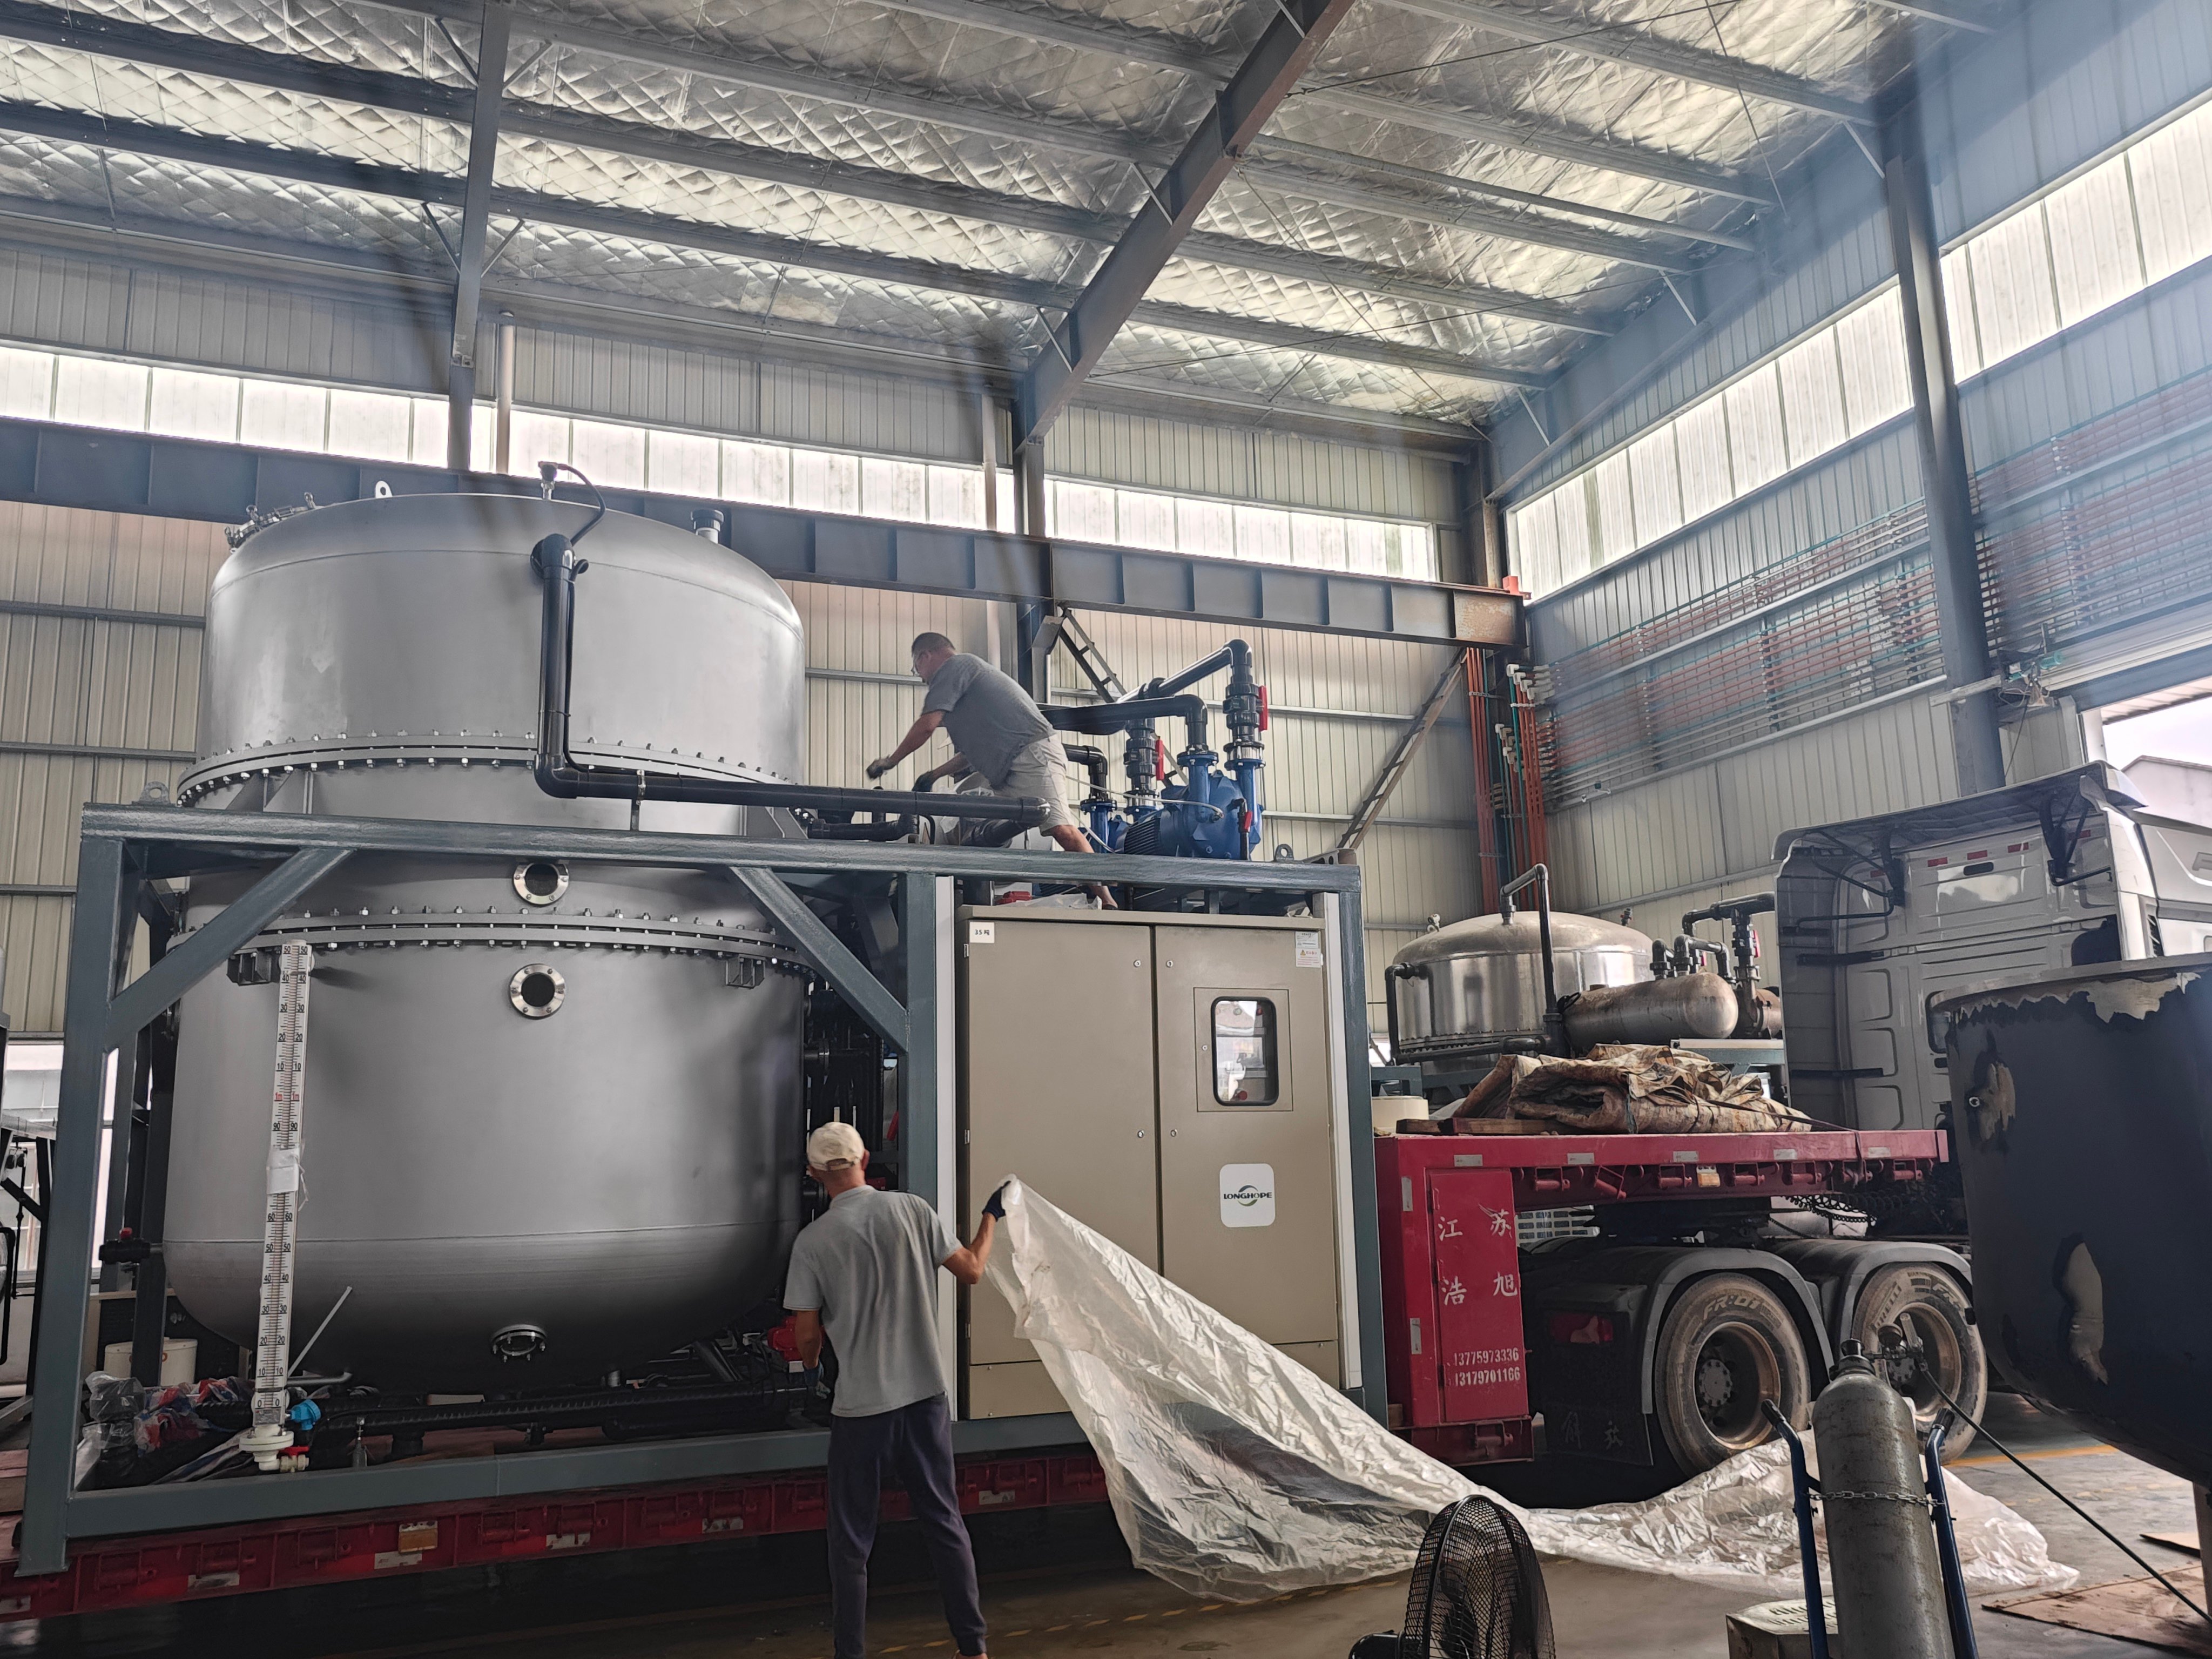
ZLD Treatment System Manufacturer

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

ZLD treatment system manufacturer

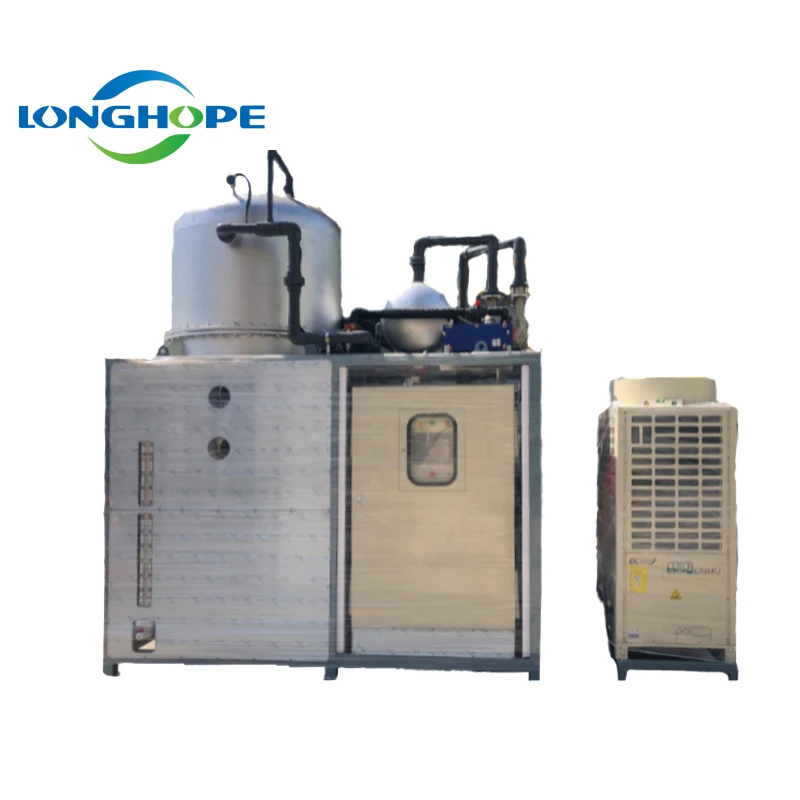
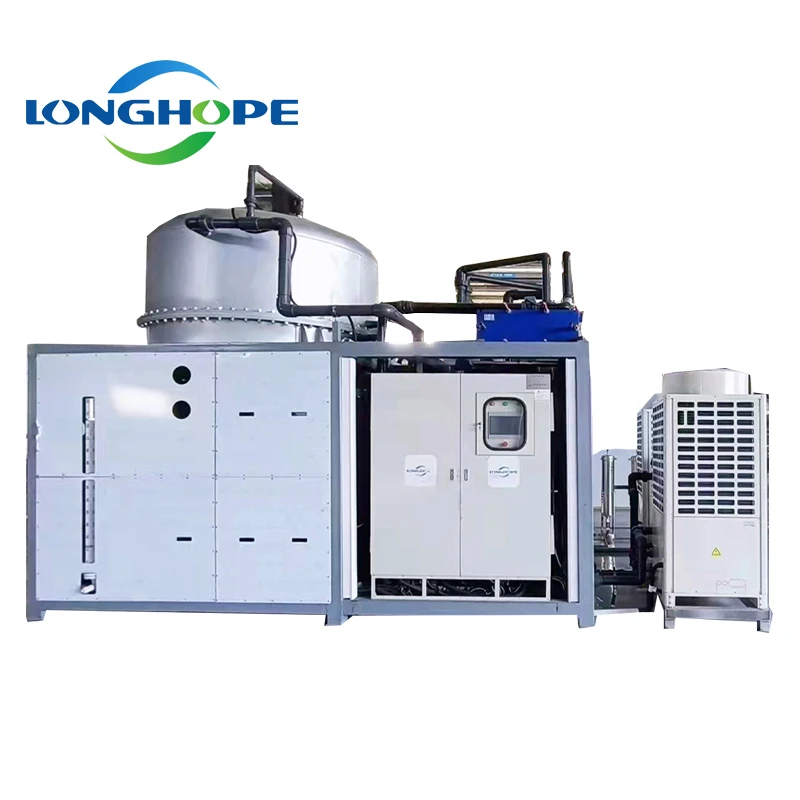
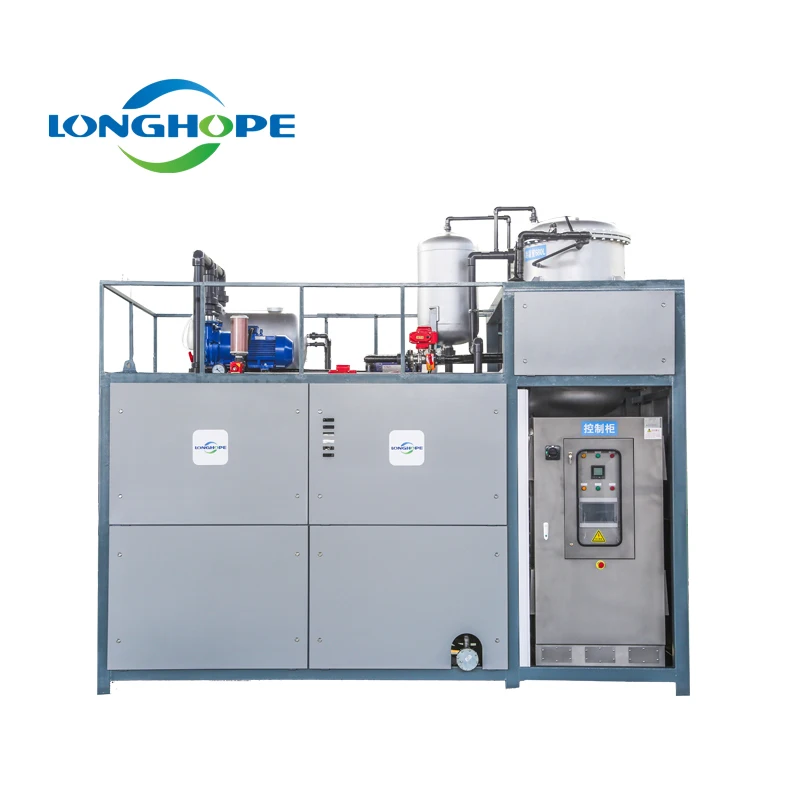
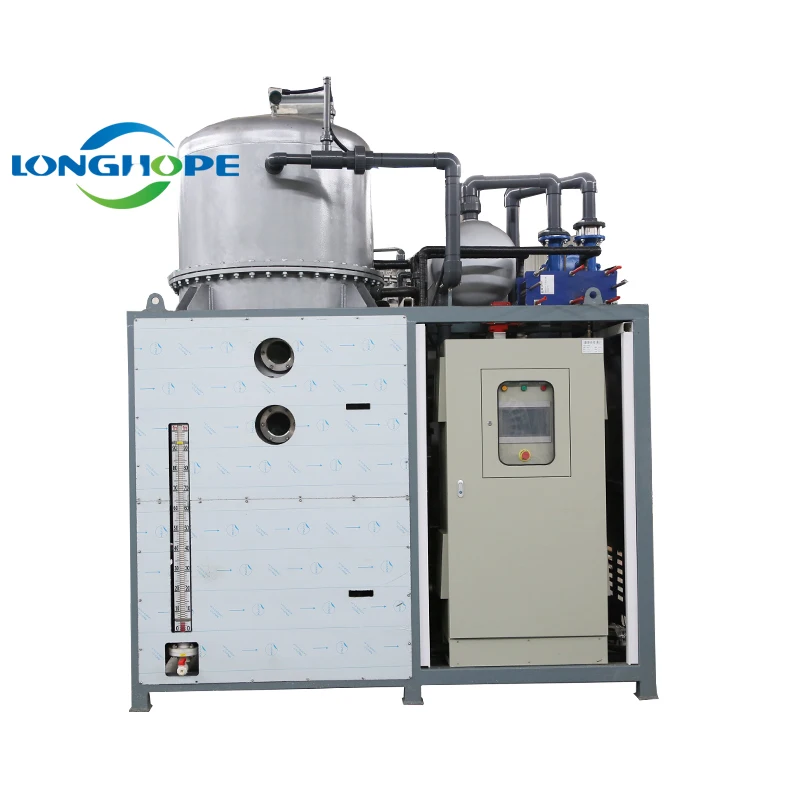
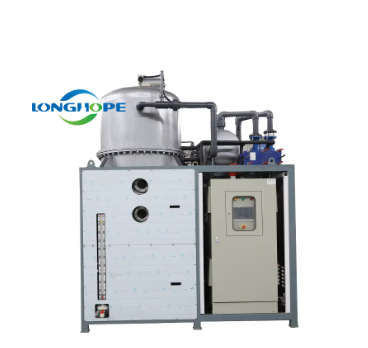
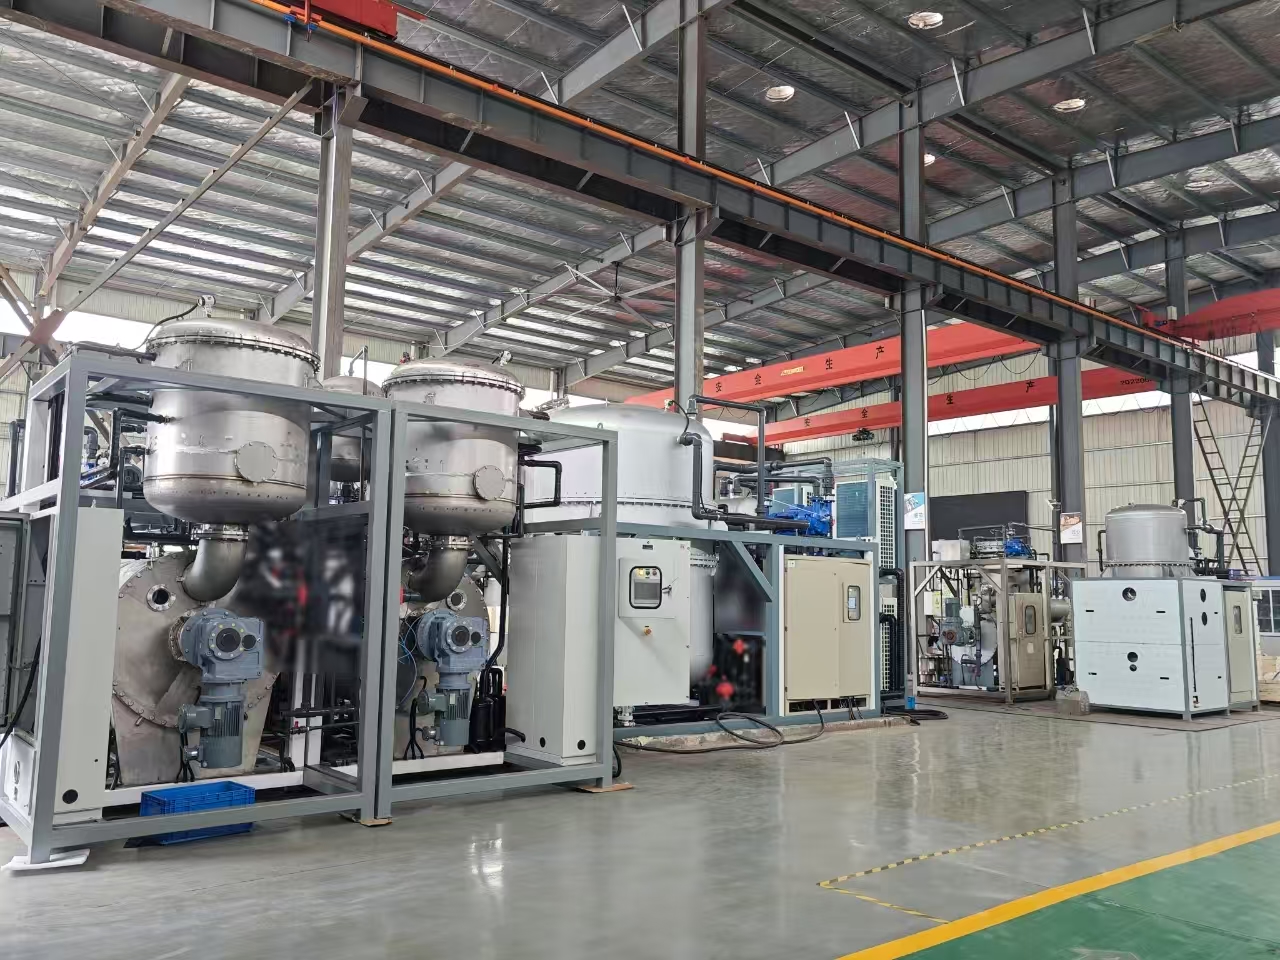
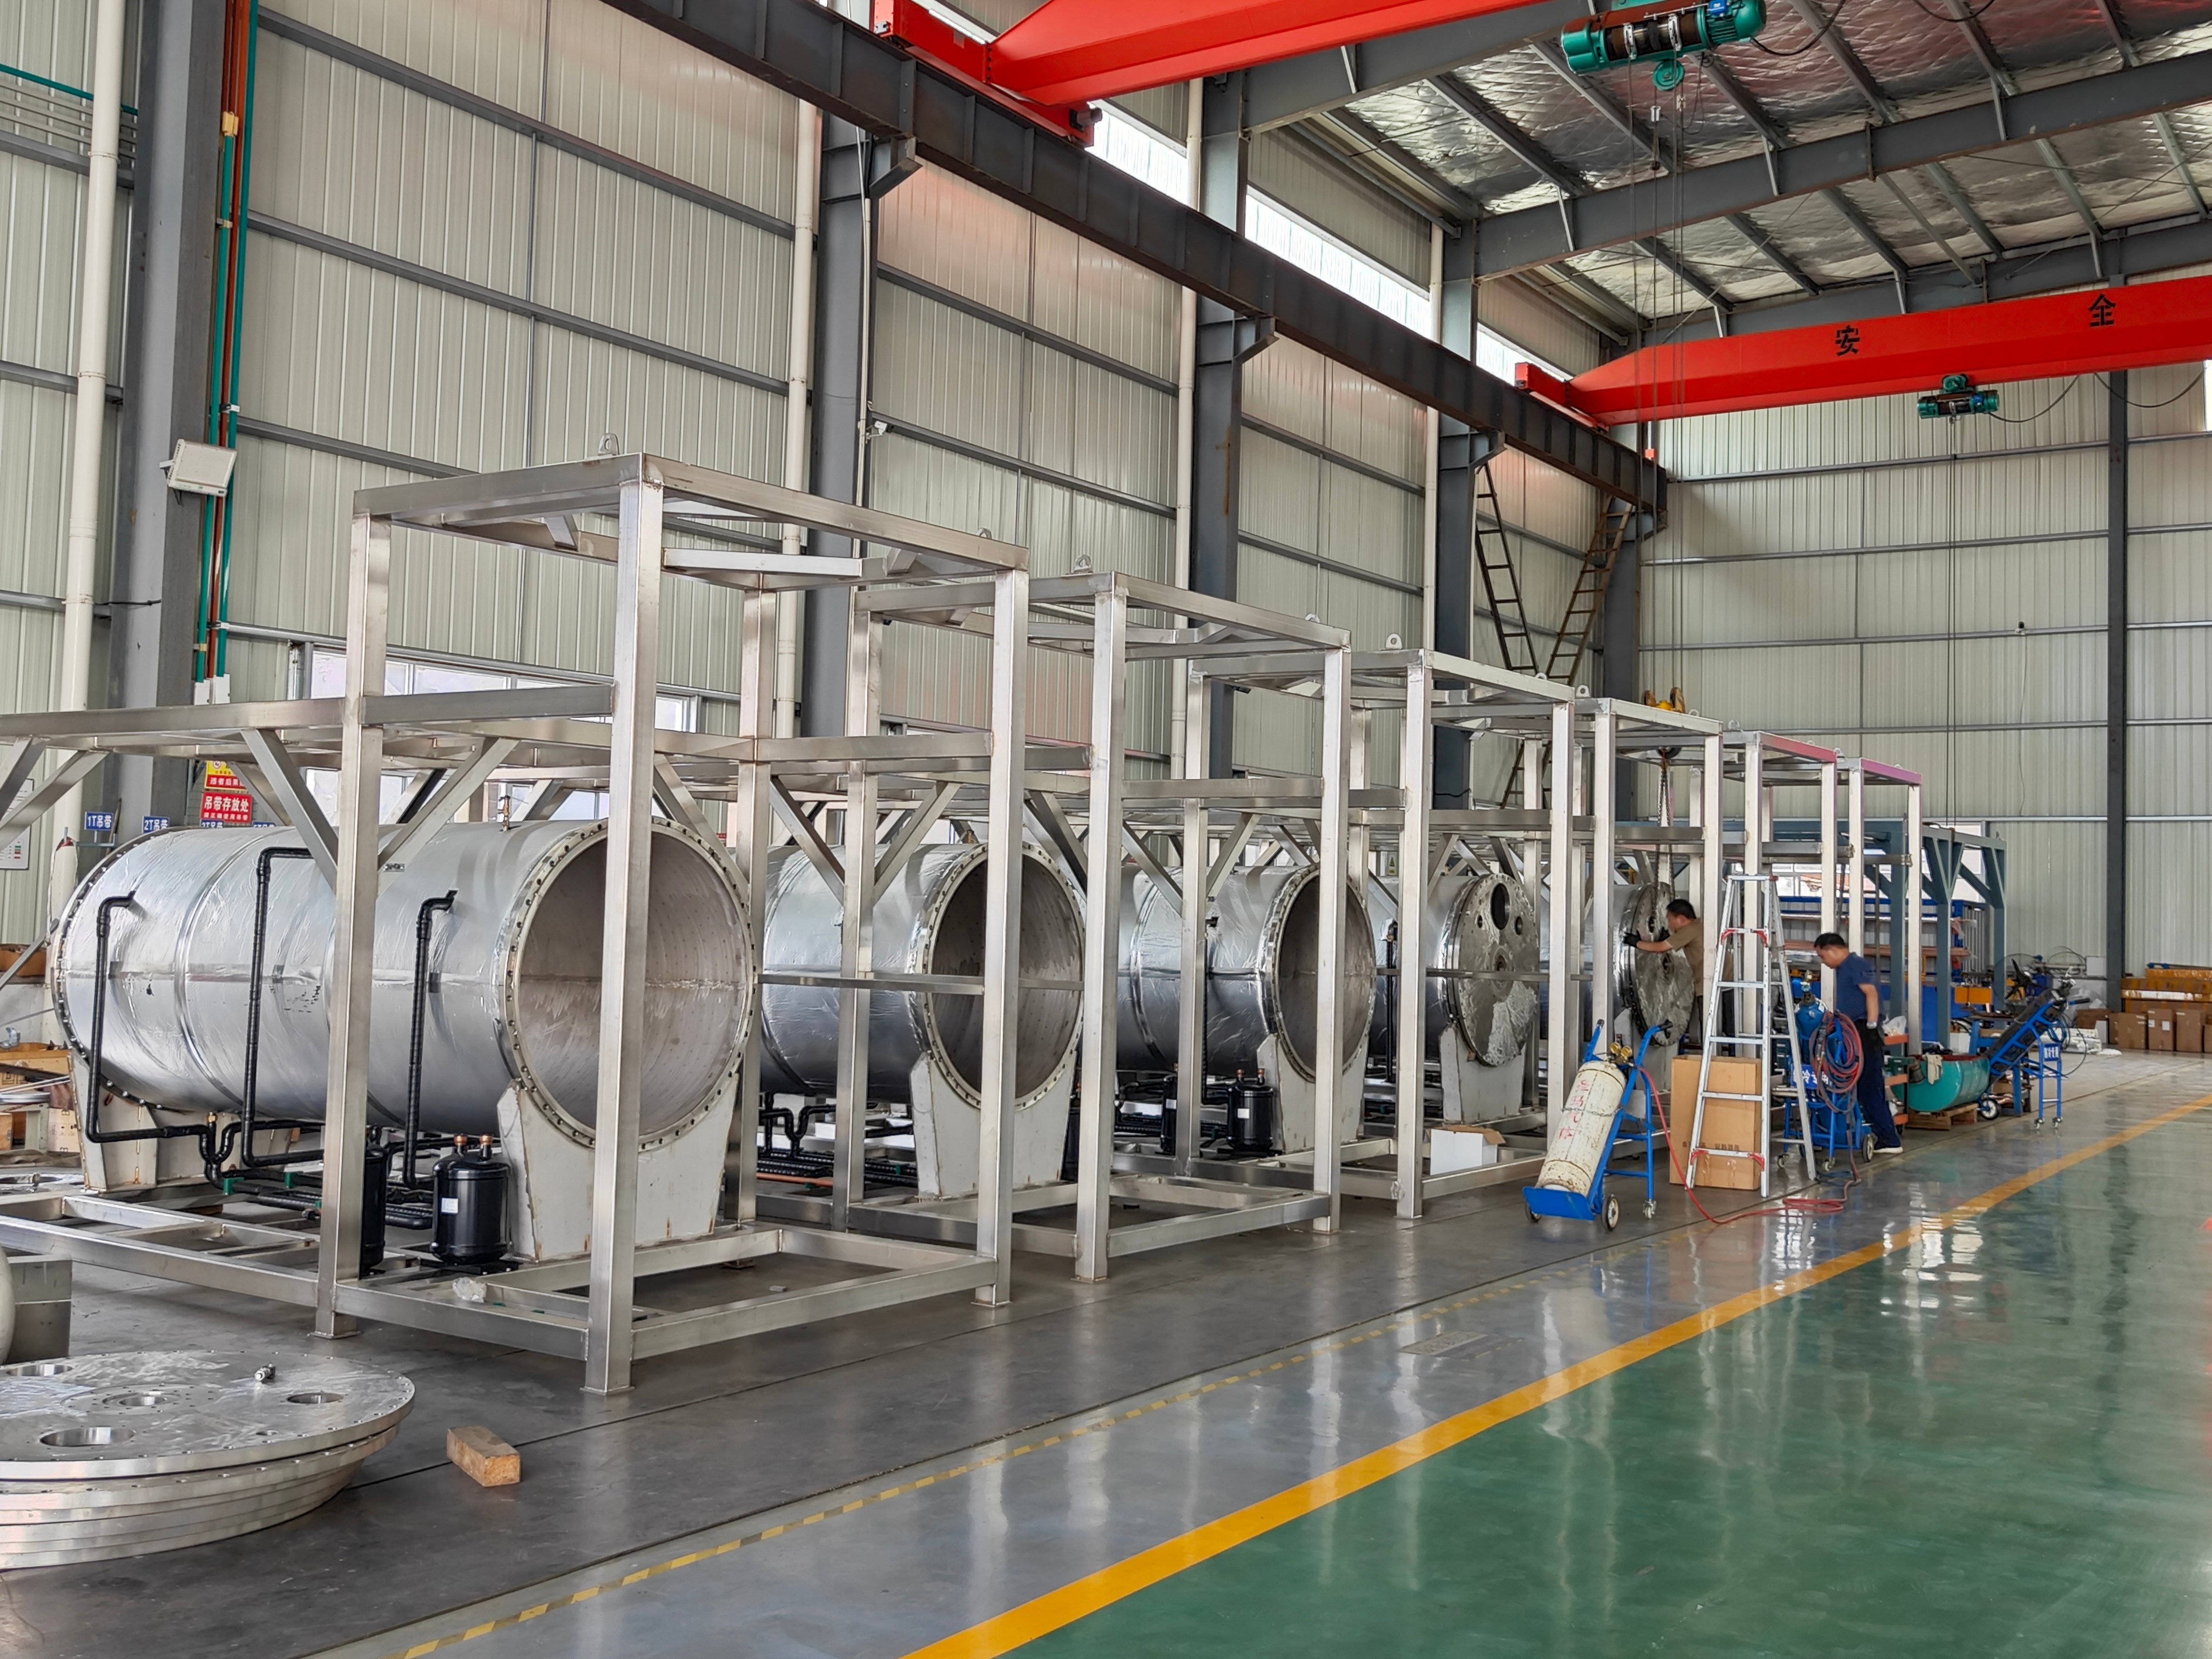
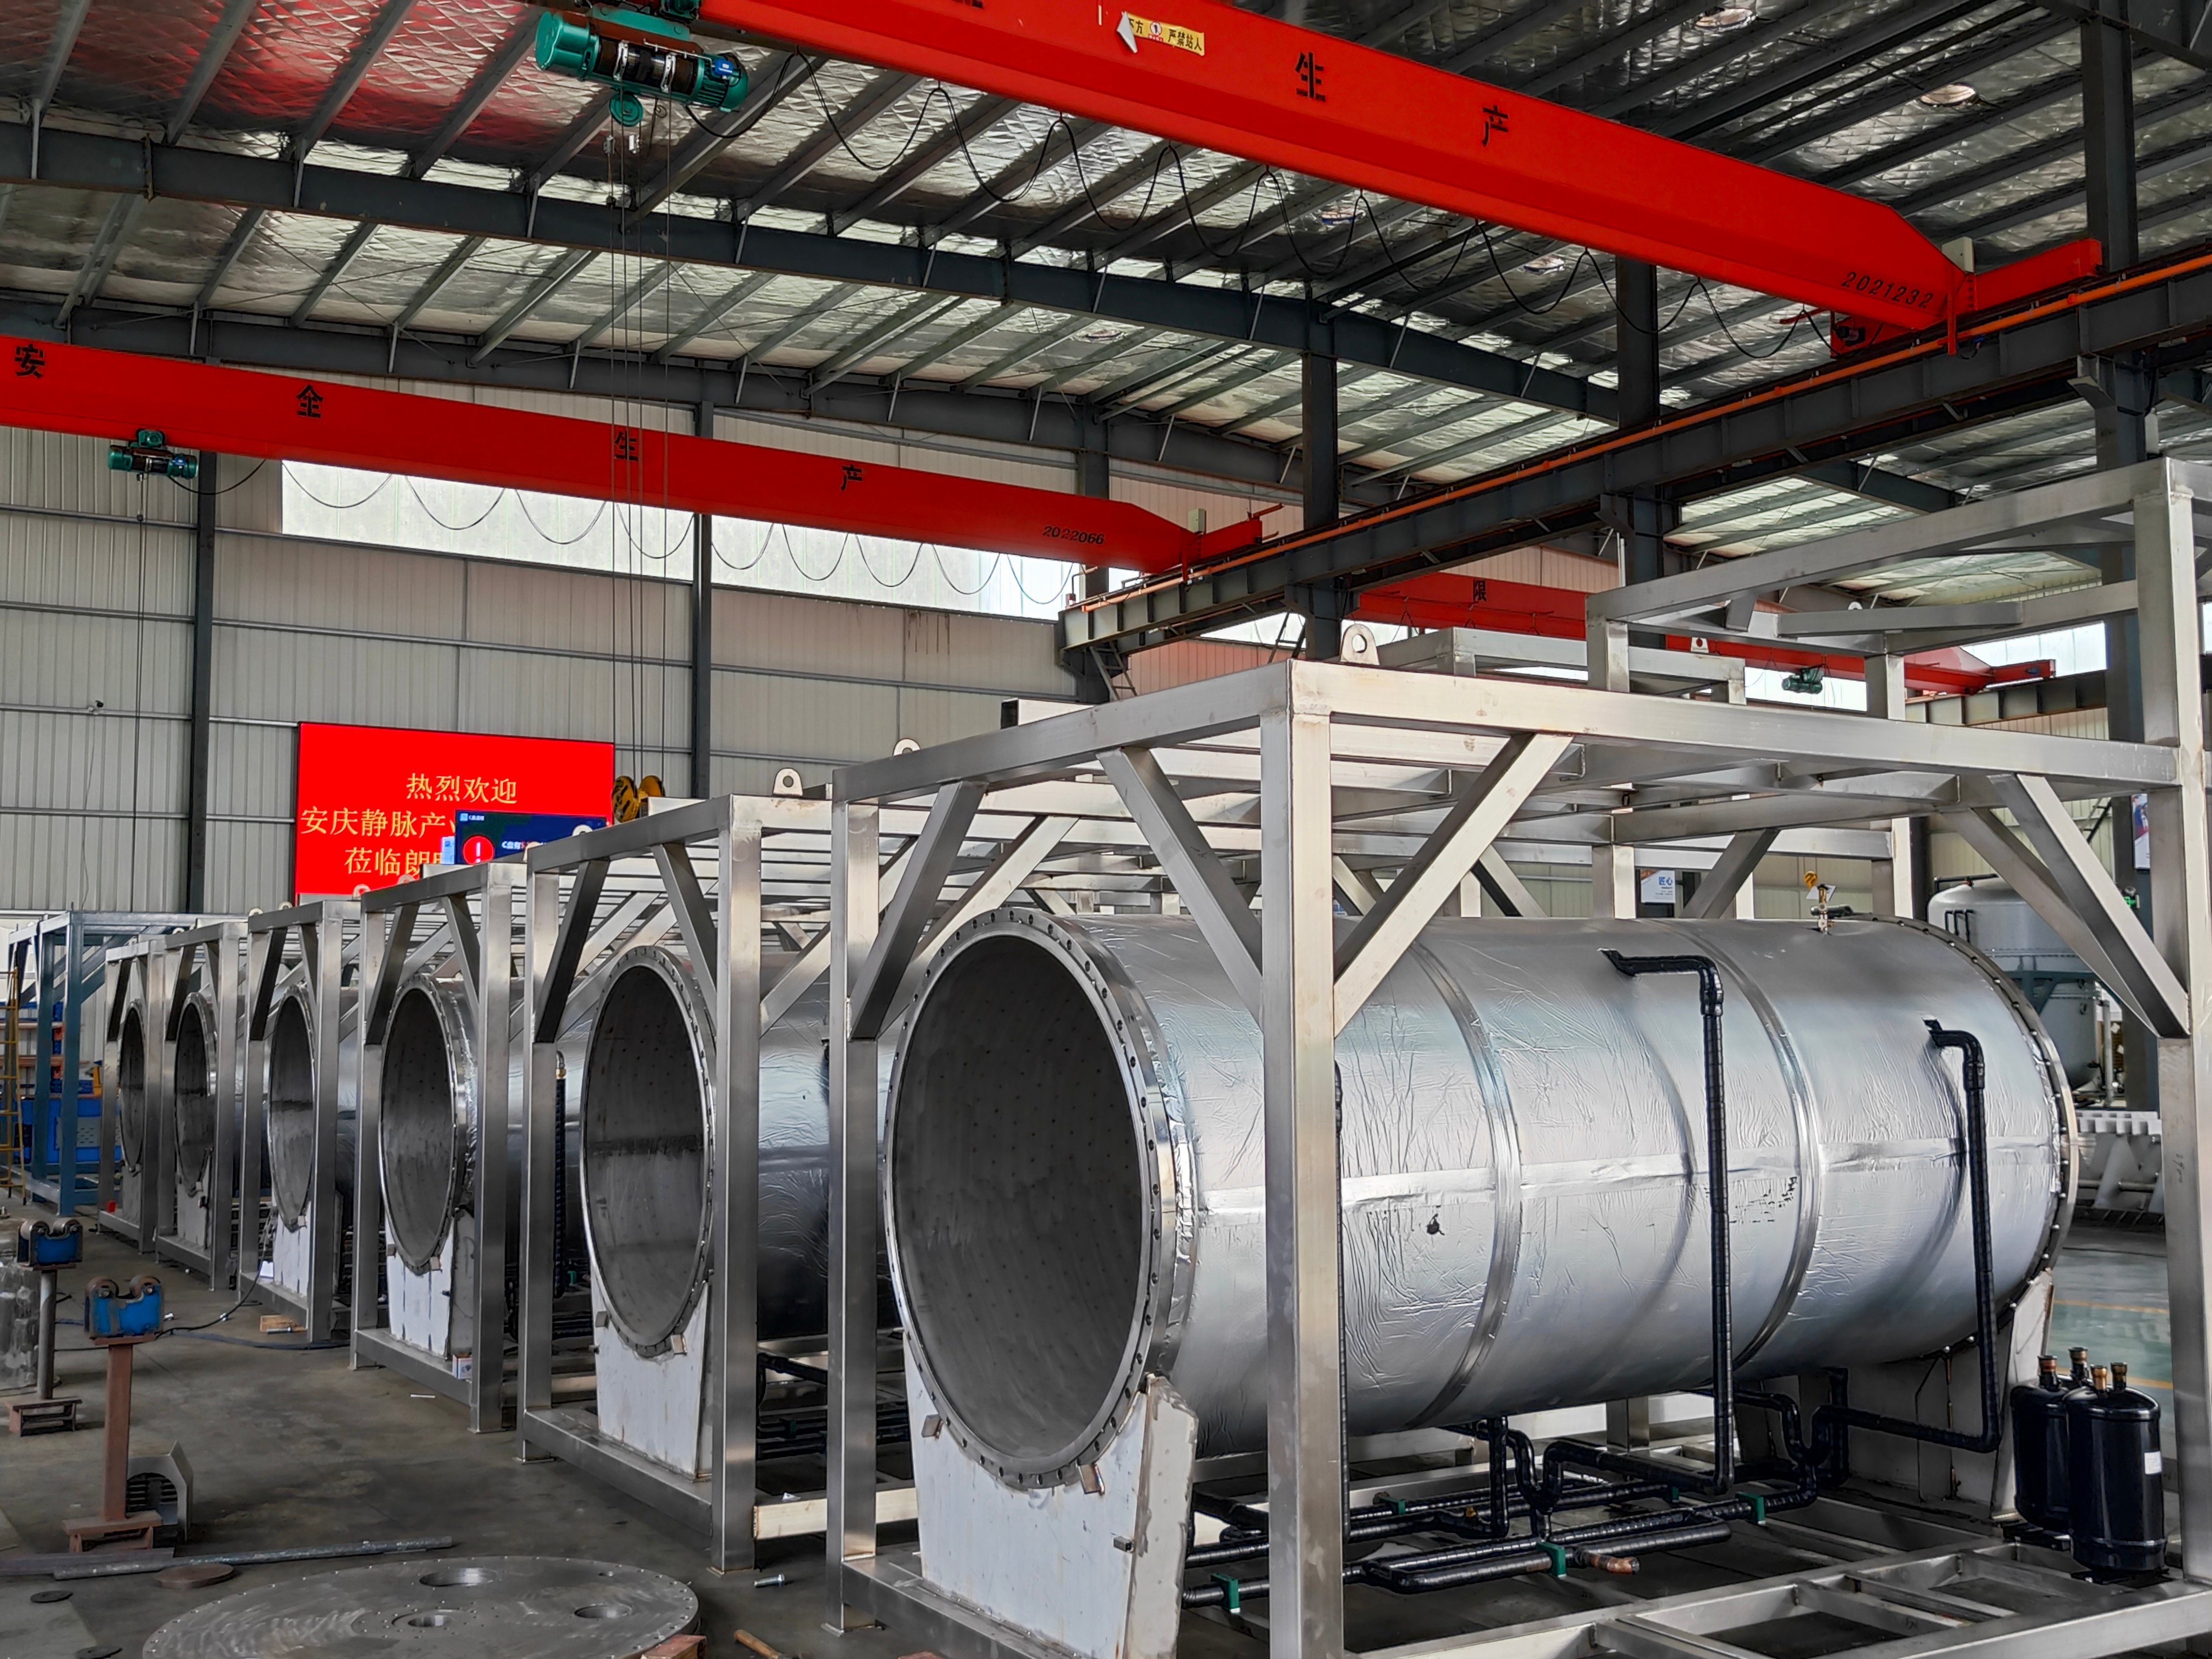
A ZLD treatment system manufacturer specializes in designing and producing Zero Liquid Discharge solutions that eliminate wastewater completely from industrial operations. This advanced technology represents a comprehensive approach to environmental responsibility and resource optimization. A professional ZLD treatment system manufacturer creates customized systems that recover valuable materials while treating contaminated water, reducing environmental impact significantly. The core function of equipment from a ZLD treatment system manufacturer involves multiple treatment stages working together seamlessly. These systems combine physical separation, chemical treatment, thermal processing, and advanced filtration technologies. The ZLD treatment system manufacturer incorporates evaporation, crystallization, and membrane technologies to achieve complete liquid elimination. Advanced monitoring systems track water quality throughout treatment, ensuring consistent performance. Technological features distinguish leading ZLD treatment system manufacturer offerings in the market. High-efficiency evaporation units reduce energy consumption substantially compared to traditional methods. Multi-stage filtration removes suspended solids, oils, and dissolved contaminants effectively. Real-time analytics help operators optimize performance and reduce operational costs continuously. Applications for systems from a ZLD treatment system manufacturer span numerous industries. Mining operations use these solutions to handle mineral-laden wastewater. Chemical manufacturing facilities benefit from resource recovery capabilities. Textile producers eliminate dye-containing effluent responsibly. Power plants treat cooling tower blowdown water efficiently. Each ZLD treatment system manufacturer tailors solutions to specific industry requirements, ensuring optimal performance and regulatory compliance across diverse operational environments.

New Products

Choosing the right ZLD treatment system manufacturer delivers transformative benefits for industrial operations seeking sustainable water management solutions. The most significant advantage involves complete wastewater elimination, which removes environmental liability and protects local water resources permanently. By partnering with an experienced ZLD treatment system manufacturer, companies achieve zero discharge status, gaining regulatory compliance and environmental certification simultaneously. Operational benefits extend far beyond basic compliance requirements. A capable ZLD treatment system manufacturer designs systems that recover valuable resources from wastewater streams. Industries recover salts, minerals, and other marketable materials, creating revenue opportunities while treating waste. This dual-benefit approach improves profitability while advancing environmental goals. Energy efficiency represents another crucial advantage offered by modern ZLD treatment system manufacturer solutions. Advanced thermal management reduces operational costs substantially, enhancing return on investment over system lifetime. Application suitability across industries makes selecting the right ZLD treatment system manufacturer essential for diverse sectors. Mining companies benefit from specialized mineral recovery features. Chemical manufacturers appreciate customizable treatment stages addressing specific contaminants. Textile facilities eliminate environmental concerns associated with dye disposal. Power generation stations solve cooling tower challenges efficiently. Food processing operations maintain product quality while meeting stringent environmental standards. Decision-useful context shows that investing in technology from a reputable ZLD treatment system manufacturer strengthens corporate sustainability credentials. Stakeholders increasingly demand environmental responsibility, and zero discharge status provides competitive advantage. Enhanced brand reputation attracts environmentally conscious customers and investors. Reduced water consumption supports corporate sustainability targets. Long-term operational savings offset capital investment, delivering measurable financial benefits alongside environmental stewardship that modern industries increasingly value.

Tips And Tricks

Industrial Water Treatment Technologies for 2026

02

Sep

Industrial Water Treatment Technologies for 2026

Industrial water treatment remains one of the most critical operational priorities across manufacturing, chemical processing, food production, and energy sectors. As facilities face increasingly stringent environmental regulations, rising operational...
View More
Low Temperature Heat Pump Evaporator: Energy Saving Guide

24

Jul

Low Temperature Heat Pump Evaporator: Energy Saving Guide

Industrial facilities continuously seek ways to reduce operational costs while maintaining peak performance. A low temperature heat pump evaporator represents one of the most effective technologies for achieving significant energy savings in thermal ...
View More
Vacuum Distillation: Key Benefits for Industrial Use

24

Jul

Vacuum Distillation: Key Benefits for Industrial Use

Vacuum distillation has become an essential separation technology across numerous industrial sectors, offering superior performance compared to conventional atmospheric distillation methods. By operating under reduced pressure conditions, vacuum dist...
View More
Benefits of a Modern Evaporator System for Wastewater

24

Jul

Benefits of a Modern Evaporator System for Wastewater

Modern industrial facilities face mounting pressure to reduce wastewater disposal costs while meeting strict environmental regulations. An evaporator systems for wastewater represents a transformative solution that addresses both operational expenses...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

ZLD treatment system manufacturer

Complete Resource Recovery Capability

Complete Resource Recovery Capability

Leading ZLD treatment system manufacturer solutions excel at converting waste into valuable resources through sophisticated recovery processes. Unlike conventional treatment approaches that simply dispose of contaminants, advanced systems capture minerals, salts, and dissolved solids for reuse or sale. This unique capability transforms wastewater from a disposal liability into a profit center. Industries recover marketable byproducts while simultaneously achieving zero discharge status. A professional ZLD treatment system manufacturer designs recovery mechanisms customized to each industry's specific waste composition. Mining operations recover mineral concentrates. Chemical plants recover salts and specialty compounds. Textile mills capture dye components. This comprehensive resource extraction maximizes value recovery while eliminating environmental impact. Companies partnering with an innovative ZLD treatment system manufacturer experience dual benefits simultaneously: complete environmental compliance and significant revenue generation from recovered materials that previously represented pure waste and operational expense.
Energy-Efficient Advanced Treatment Technology

Energy-Efficient Advanced Treatment Technology

Modern ZLD treatment system manufacturer innovations focus on minimizing energy consumption without compromising treatment effectiveness or system reliability. Integrated thermal management systems optimize heat recovery and recycling throughout treatment processes, substantially reducing energy requirements. Efficient evaporation units employ advanced heat exchange technology, cutting energy usage compared to traditional methods significantly. A forward-thinking ZLD treatment system manufacturer incorporates automation and real-time monitoring, enabling continuous performance optimization and rapid adjustment to changing conditions. Variable frequency drives reduce motor energy consumption dynamically. Membrane technologies consume minimal electricity while achieving superior separation. These technological advantages translate directly into operational cost reduction, improving the financial viability of zero discharge compliance. Companies selecting an efficient ZLD treatment system manufacturer experience lower utility bills, reduced carbon footprint, and enhanced operational profitability. Long-term energy savings often surpass initial capital investment, making sustainability economically attractive simultaneously.
Customizable Solutions for Diverse Industrial Applications

Customizable Solutions for Diverse Industrial Applications

Experienced ZLD treatment system manufacturer experts understand that different industries face unique wastewater challenges requiring specialized treatment approaches. Rather than offering generic solutions, professional manufacturers develop customized systems addressing specific contaminant profiles, water volumes, and operational requirements. Mining operations need specialized mineral recovery capabilities. Chemical manufacturers require flexible treatment stages accommodating variable chemistry. Textile producers need advanced dye removal technology. Power plants require high-capacity cooling tower treatment. Food processors need gentle treatment protecting product quality. A responsive ZLD treatment system manufacturer conducts thorough site assessments, analyzing waste characteristics and operational constraints before designing solutions. This customization ensures optimal performance, minimum energy consumption, and maximum resource recovery. Tailored systems integrate seamlessly with existing infrastructure, minimizing disruption during installation. By choosing a ZLD treatment system manufacturer offering comprehensive customization, industries receive purpose-built solutions maximizing efficiency, compliance, and profitability across diverse operational environments and complex wastewater compositions.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000