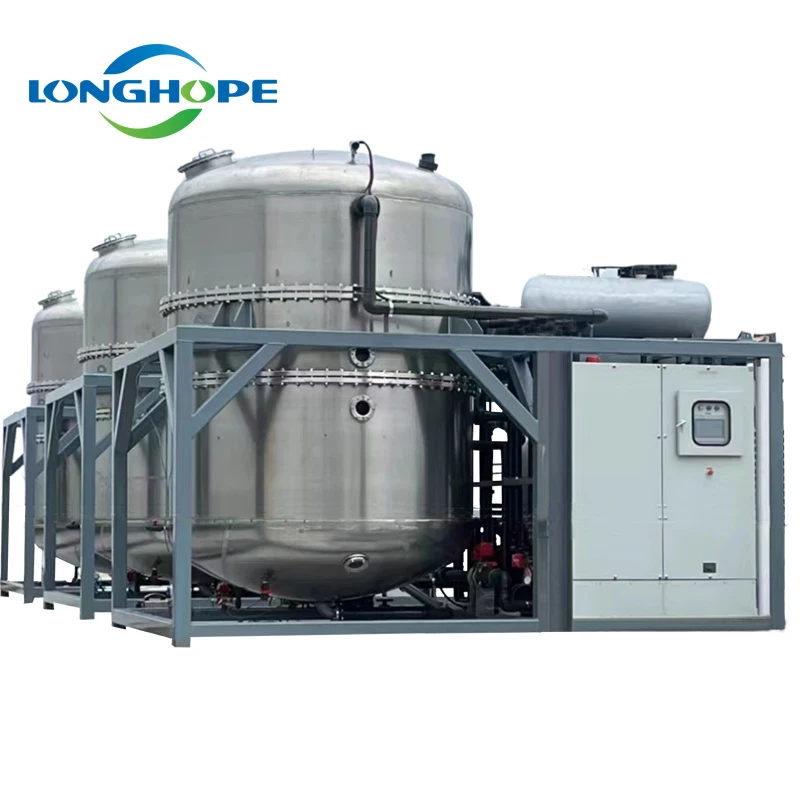
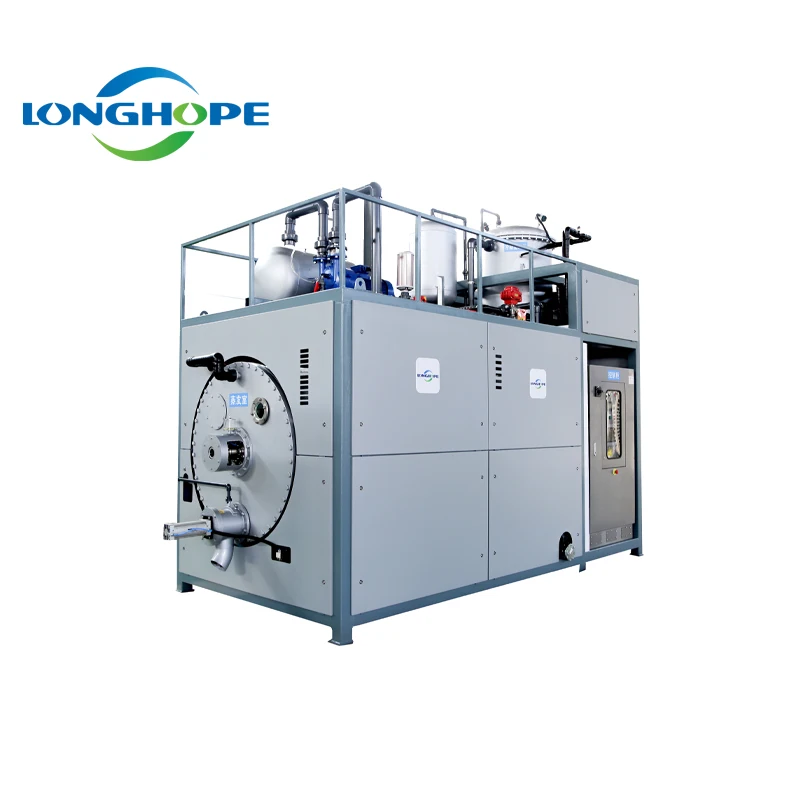
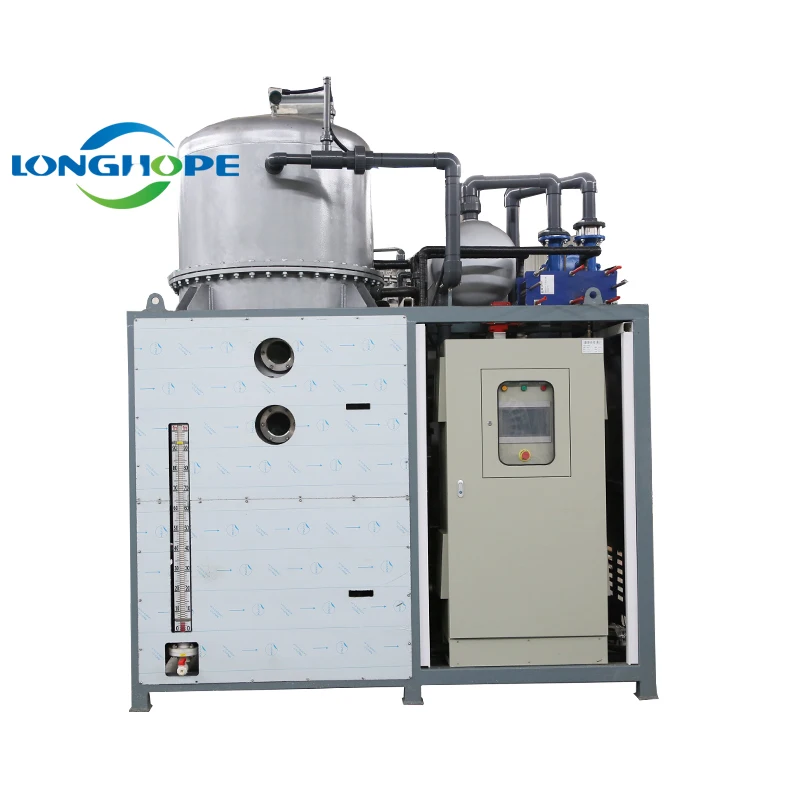
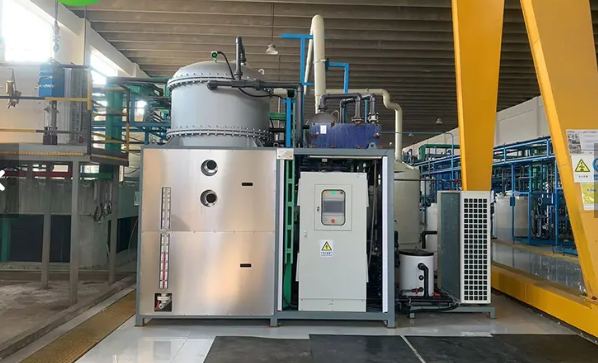
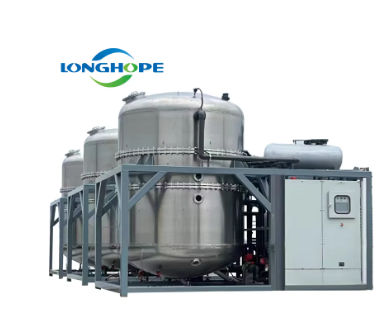
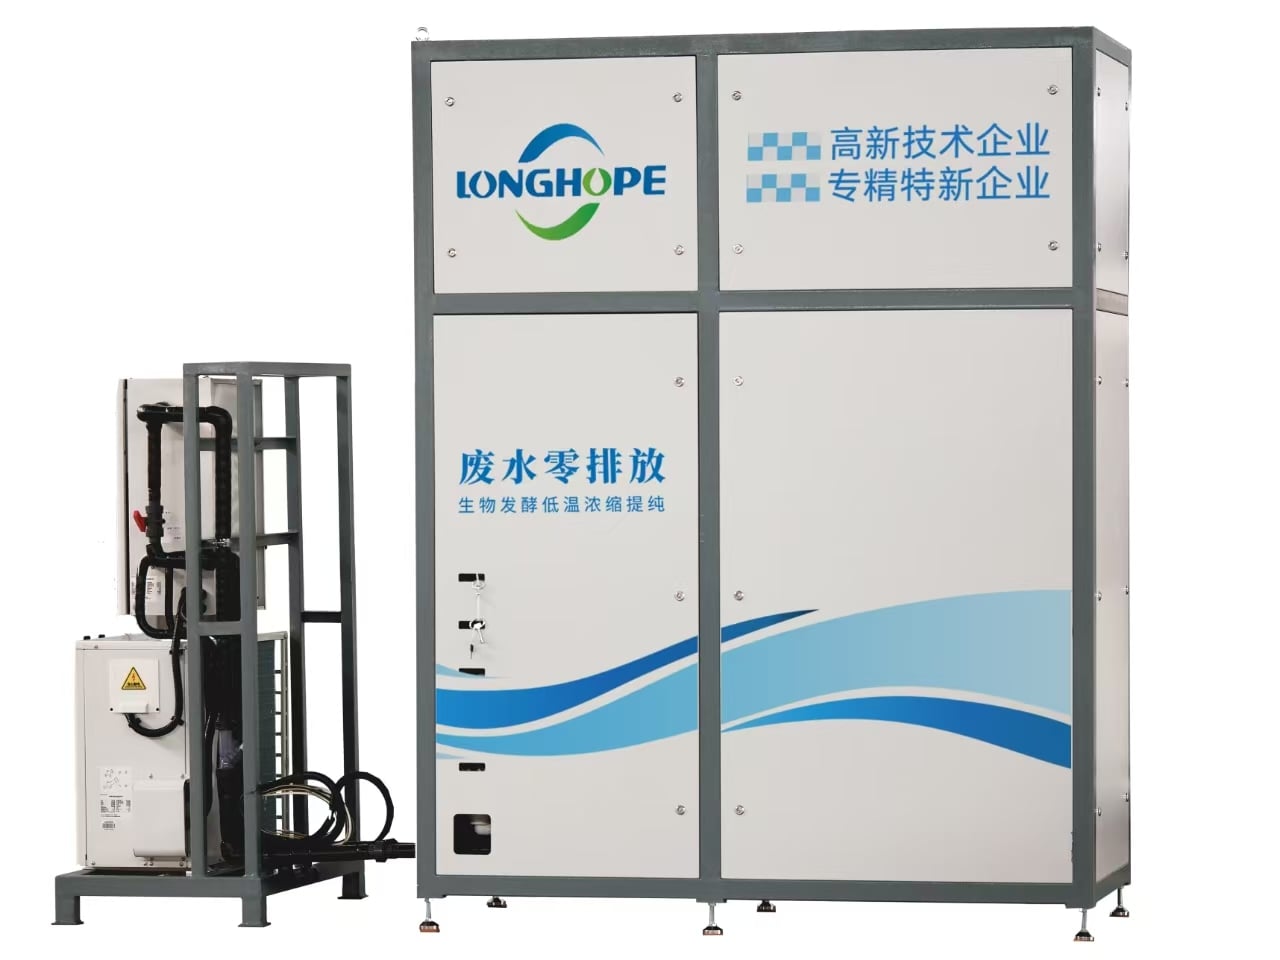
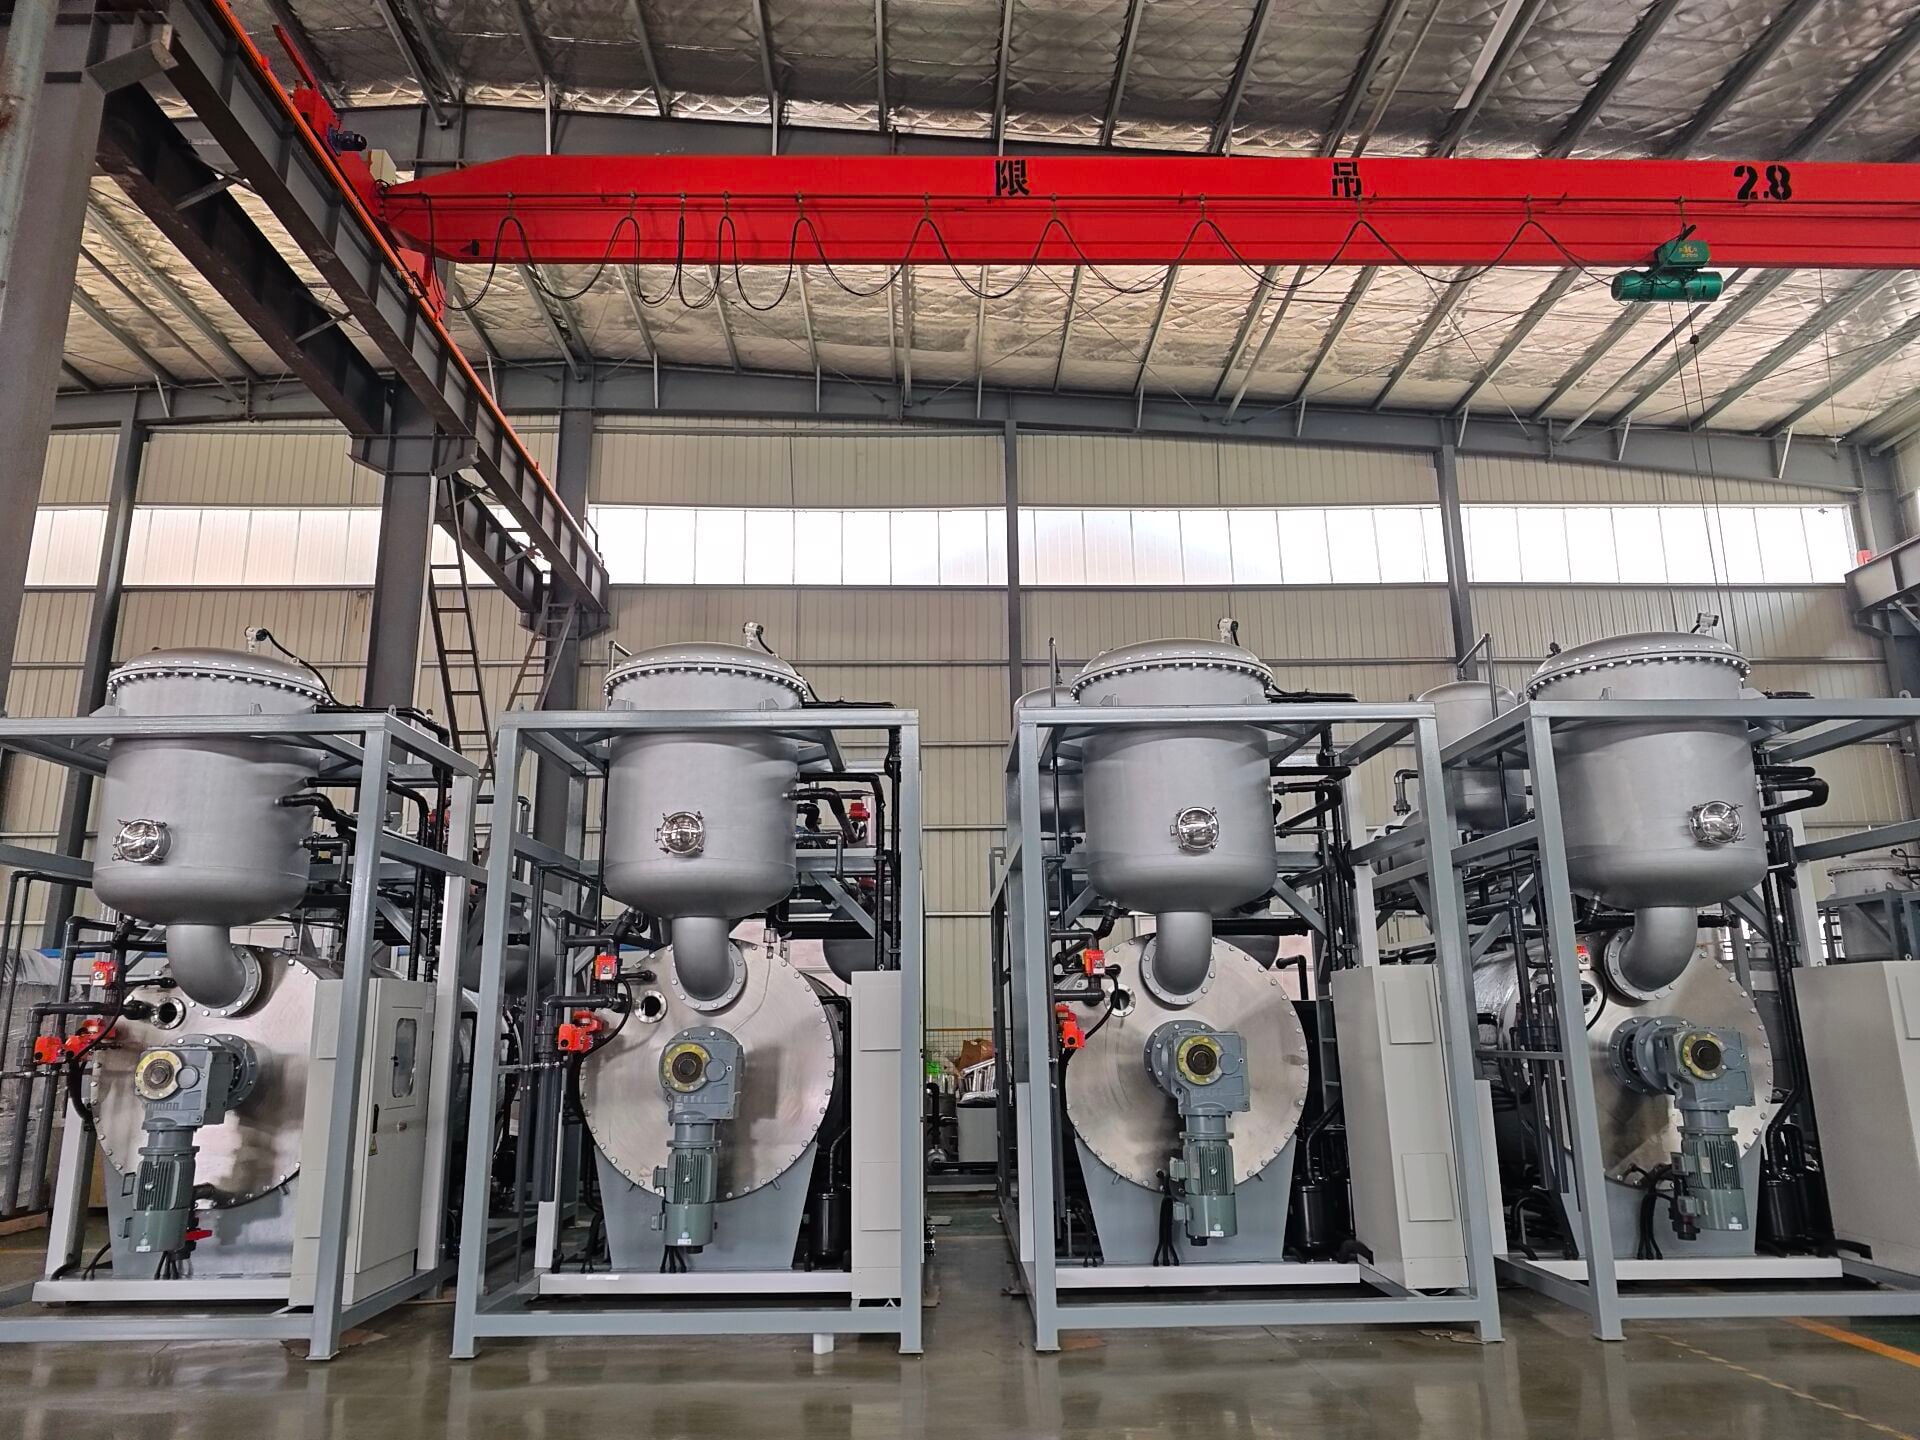
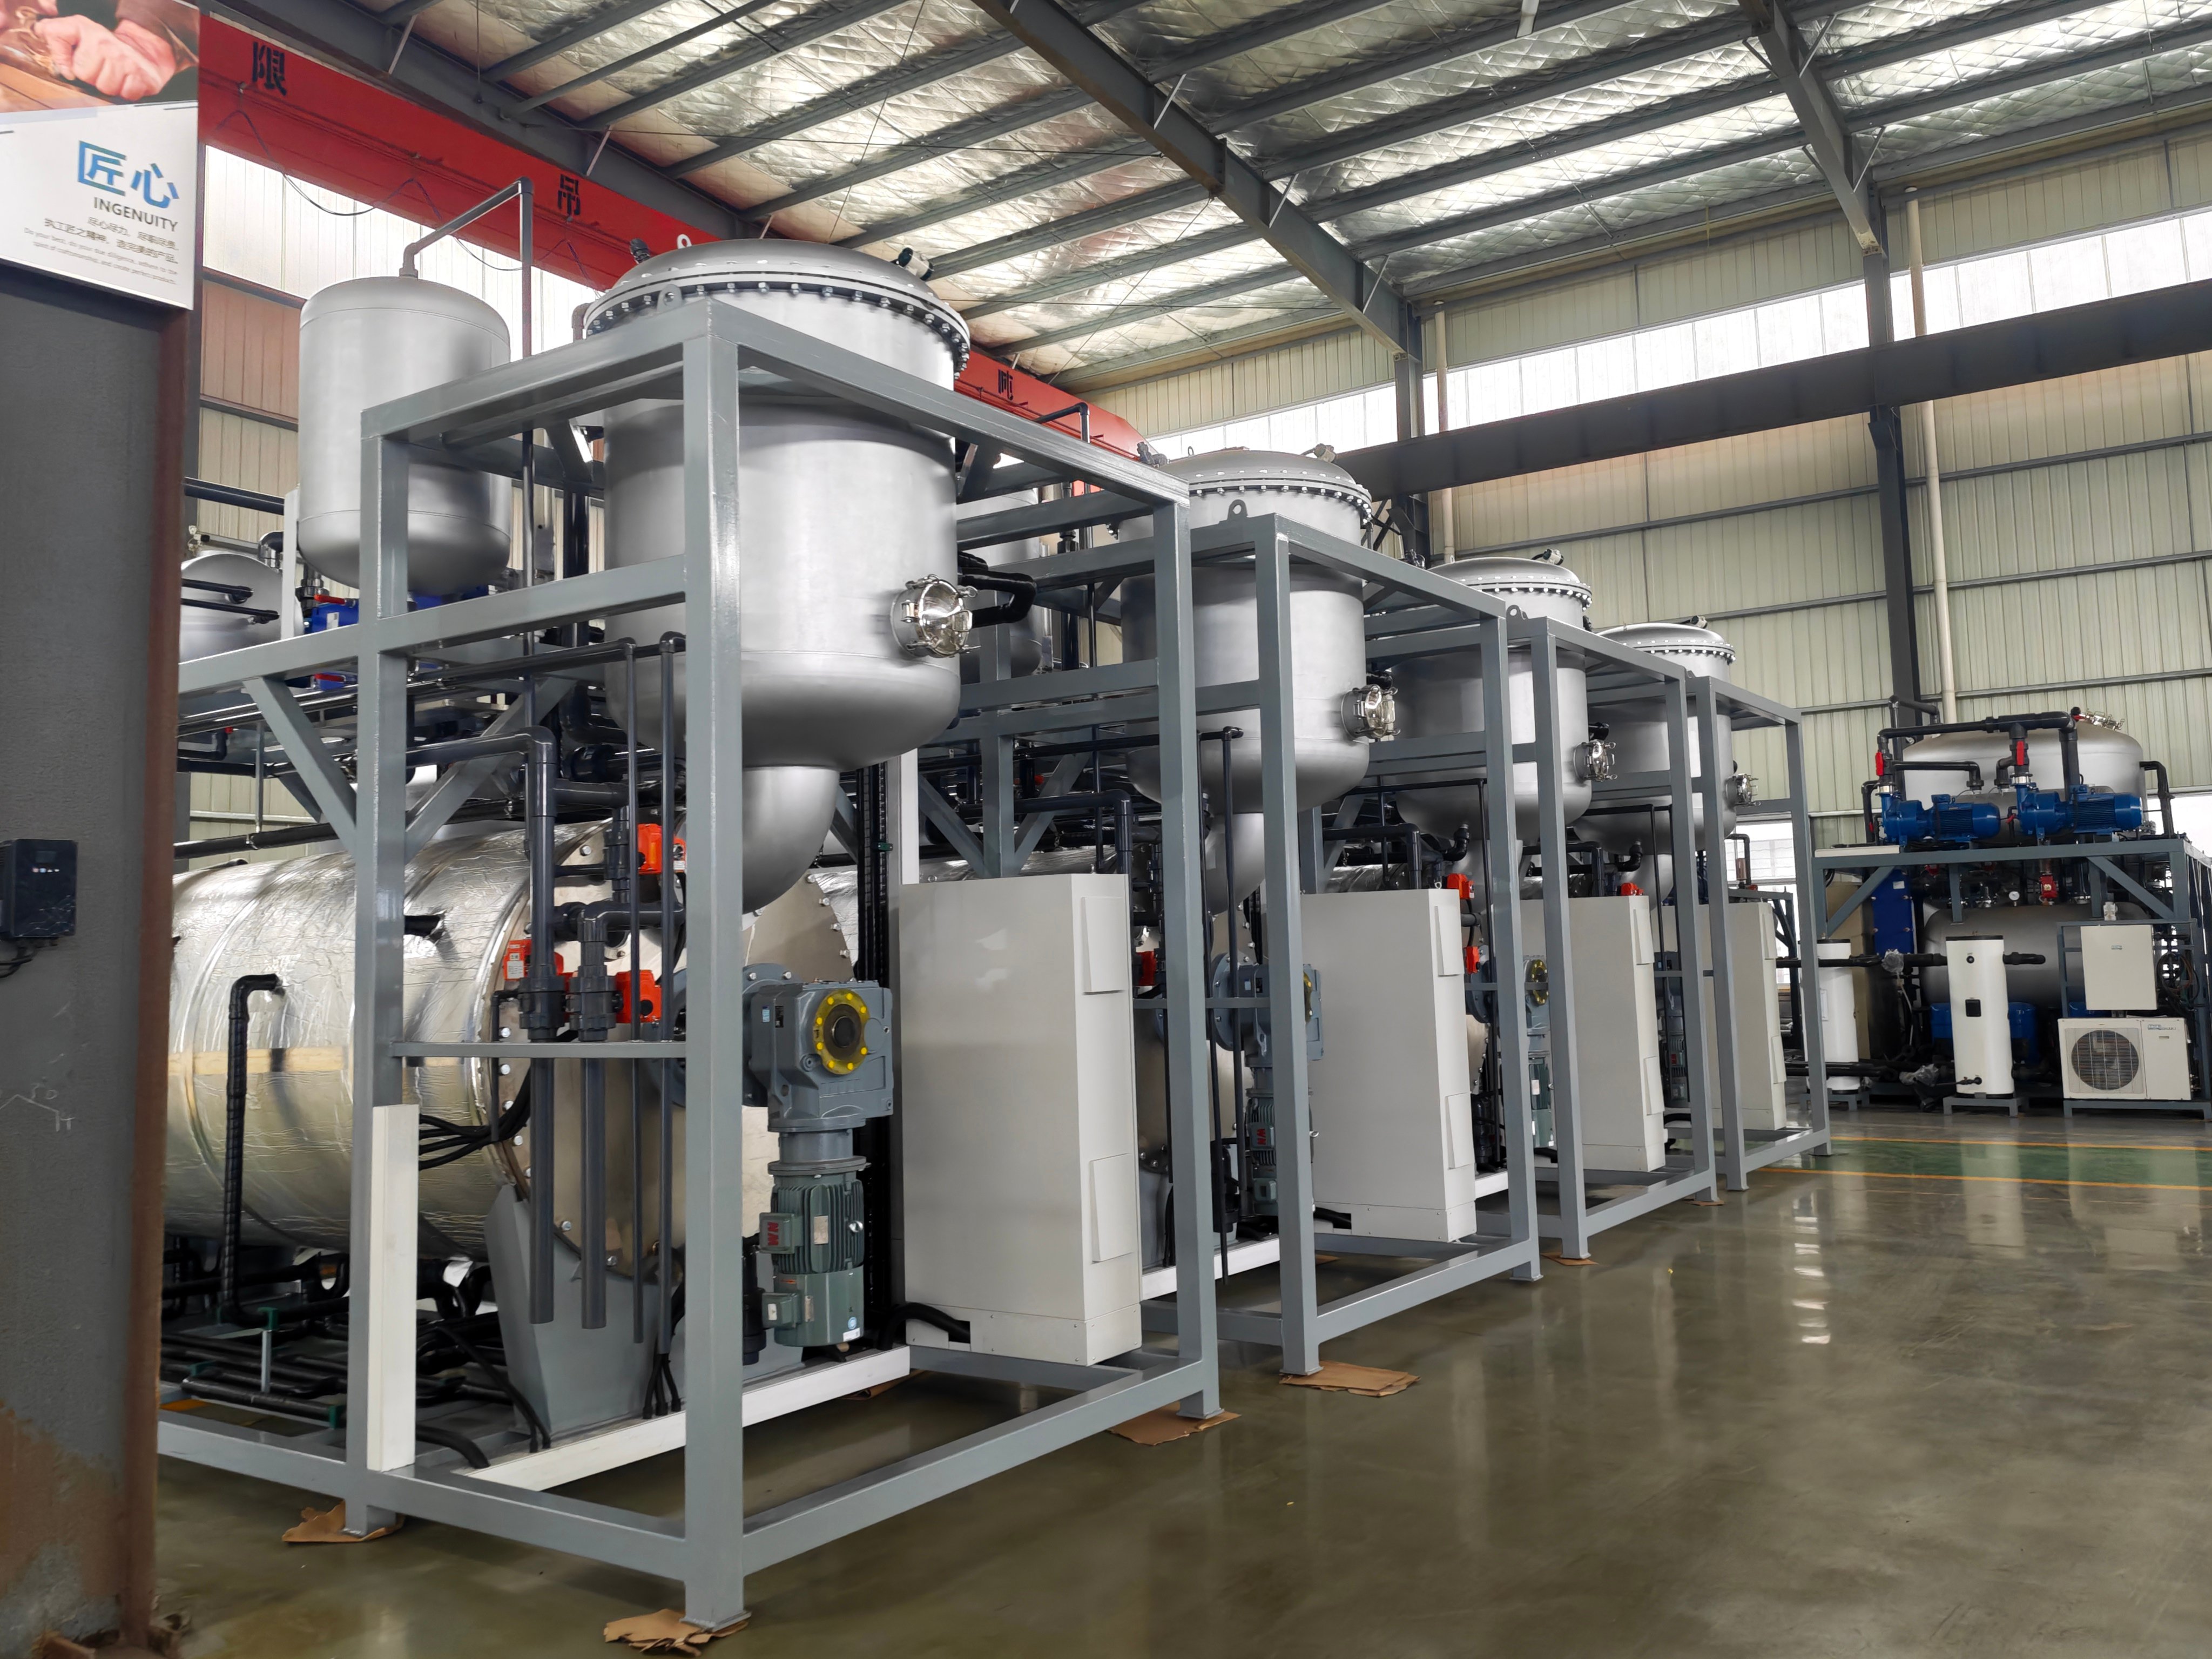
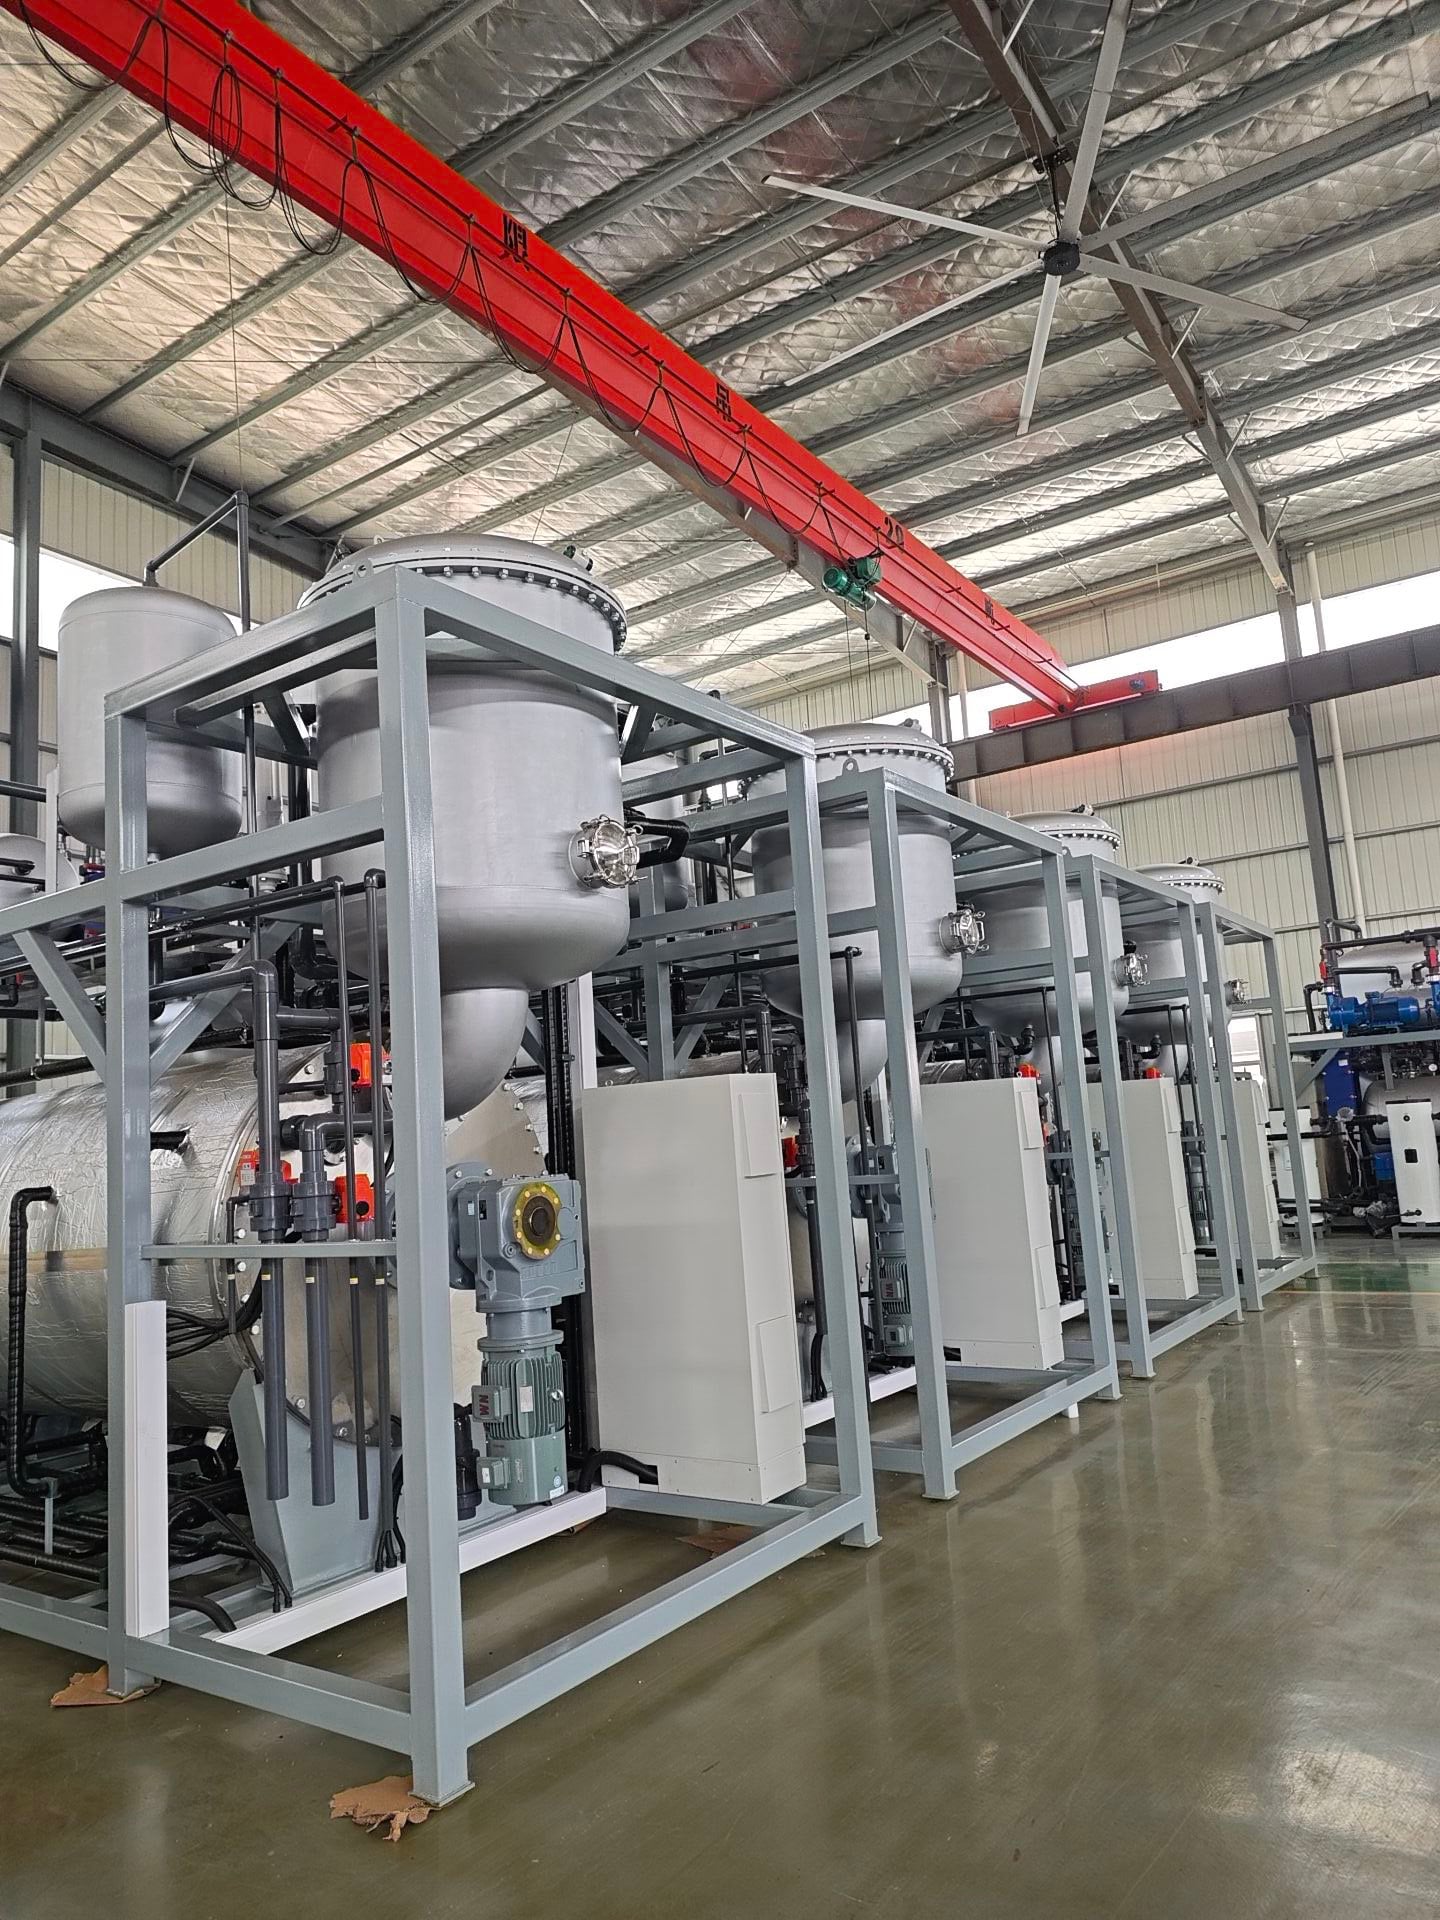
industrial crystallizer factory
An industrial crystallizer factory represents a specialized manufacturing facility dedicated to producing high-quality crystalline products through advanced separation and purification technologies. The industrial crystallizer factory employs sophisticated equipment and processes to extract, refine, and crystallize various chemical compounds, minerals, and organic substances. These facilities serve critical roles across multiple industries by converting liquid solutions into solid crystal structures with precise specifications.
The primary function of an industrial crystallizer factory involves controlling temperature, pressure, and solution concentration to initiate and manage crystallization processes. Modern industrial crystallizer factory operations utilize cooling crystallization, evaporative crystallization, and reactive crystallization methods depending on the target product requirements. Technological features include automated temperature control systems, continuous monitoring equipment, and quality assurance protocols that ensure consistent product purity and crystal size distribution.
Applications for an industrial crystallizer factory extend across pharmaceuticals, chemicals, food processing, and materials manufacturing sectors. These facilities produce essential components including pharmaceutical active ingredients, specialty chemicals, salt compounds, sugar products, and mineral extracts. The industrial crystallizer factory technology enables manufacturers to achieve superior product quality while optimizing production efficiency and reducing waste. Advanced automation within modern facilities minimizes human intervention and enhances safety standards throughout the crystallization cycle, making these operations increasingly vital to contemporary industrial production demands.

 EN