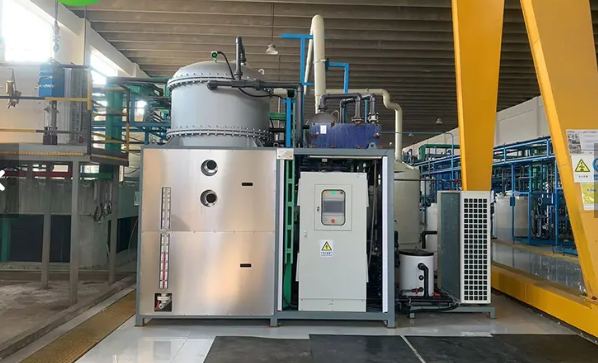
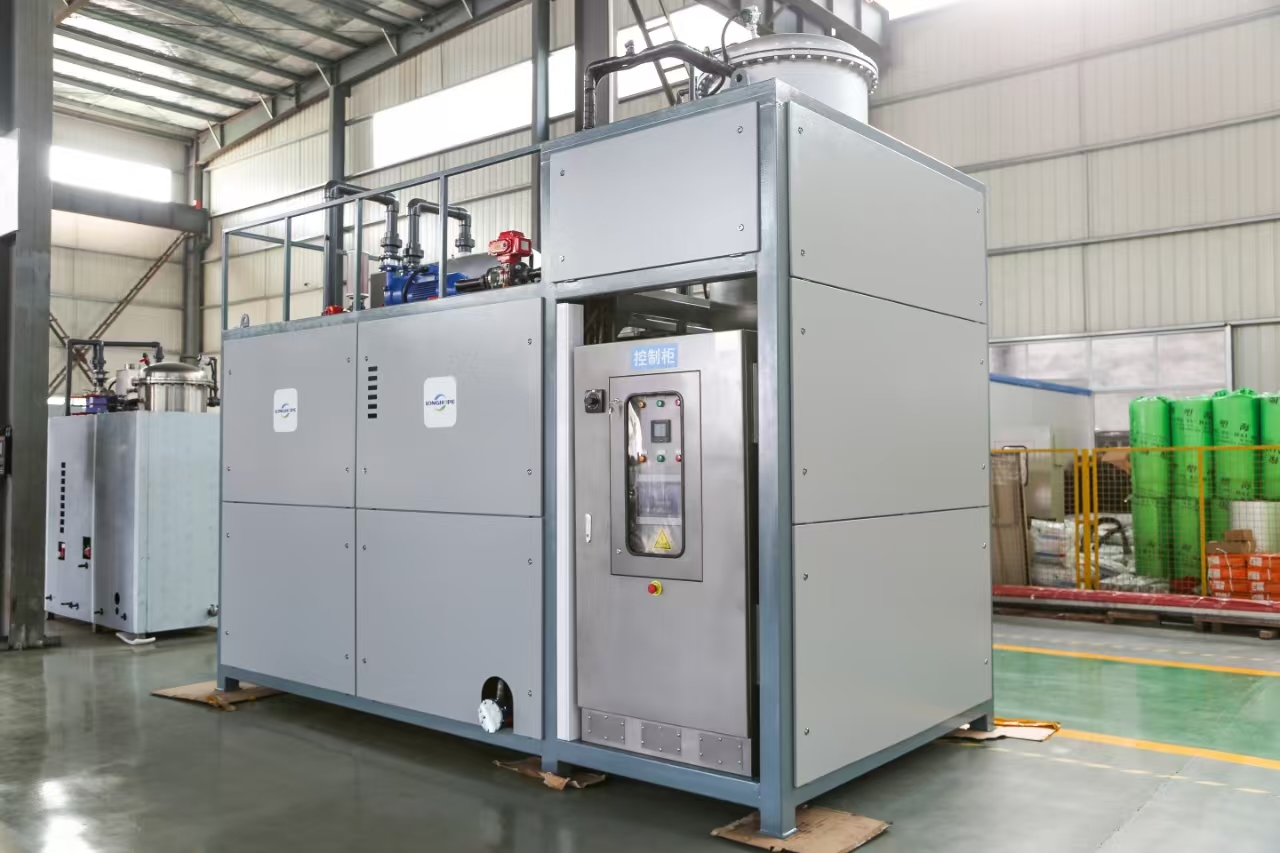
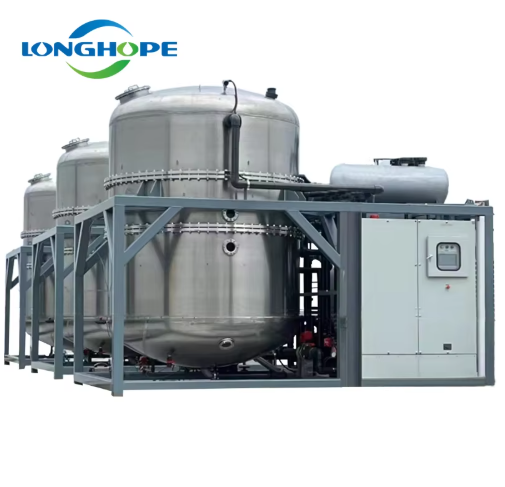
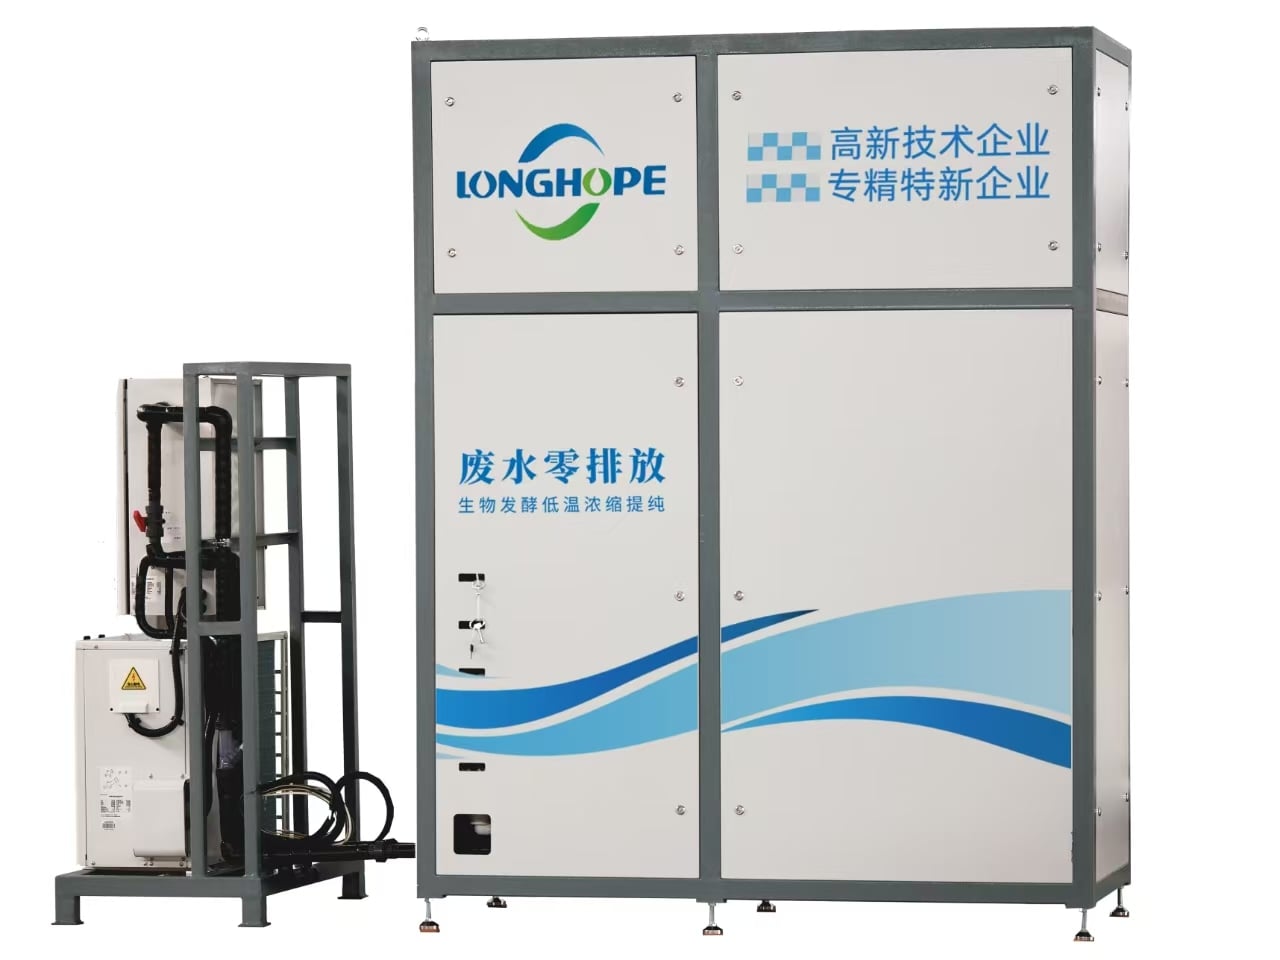
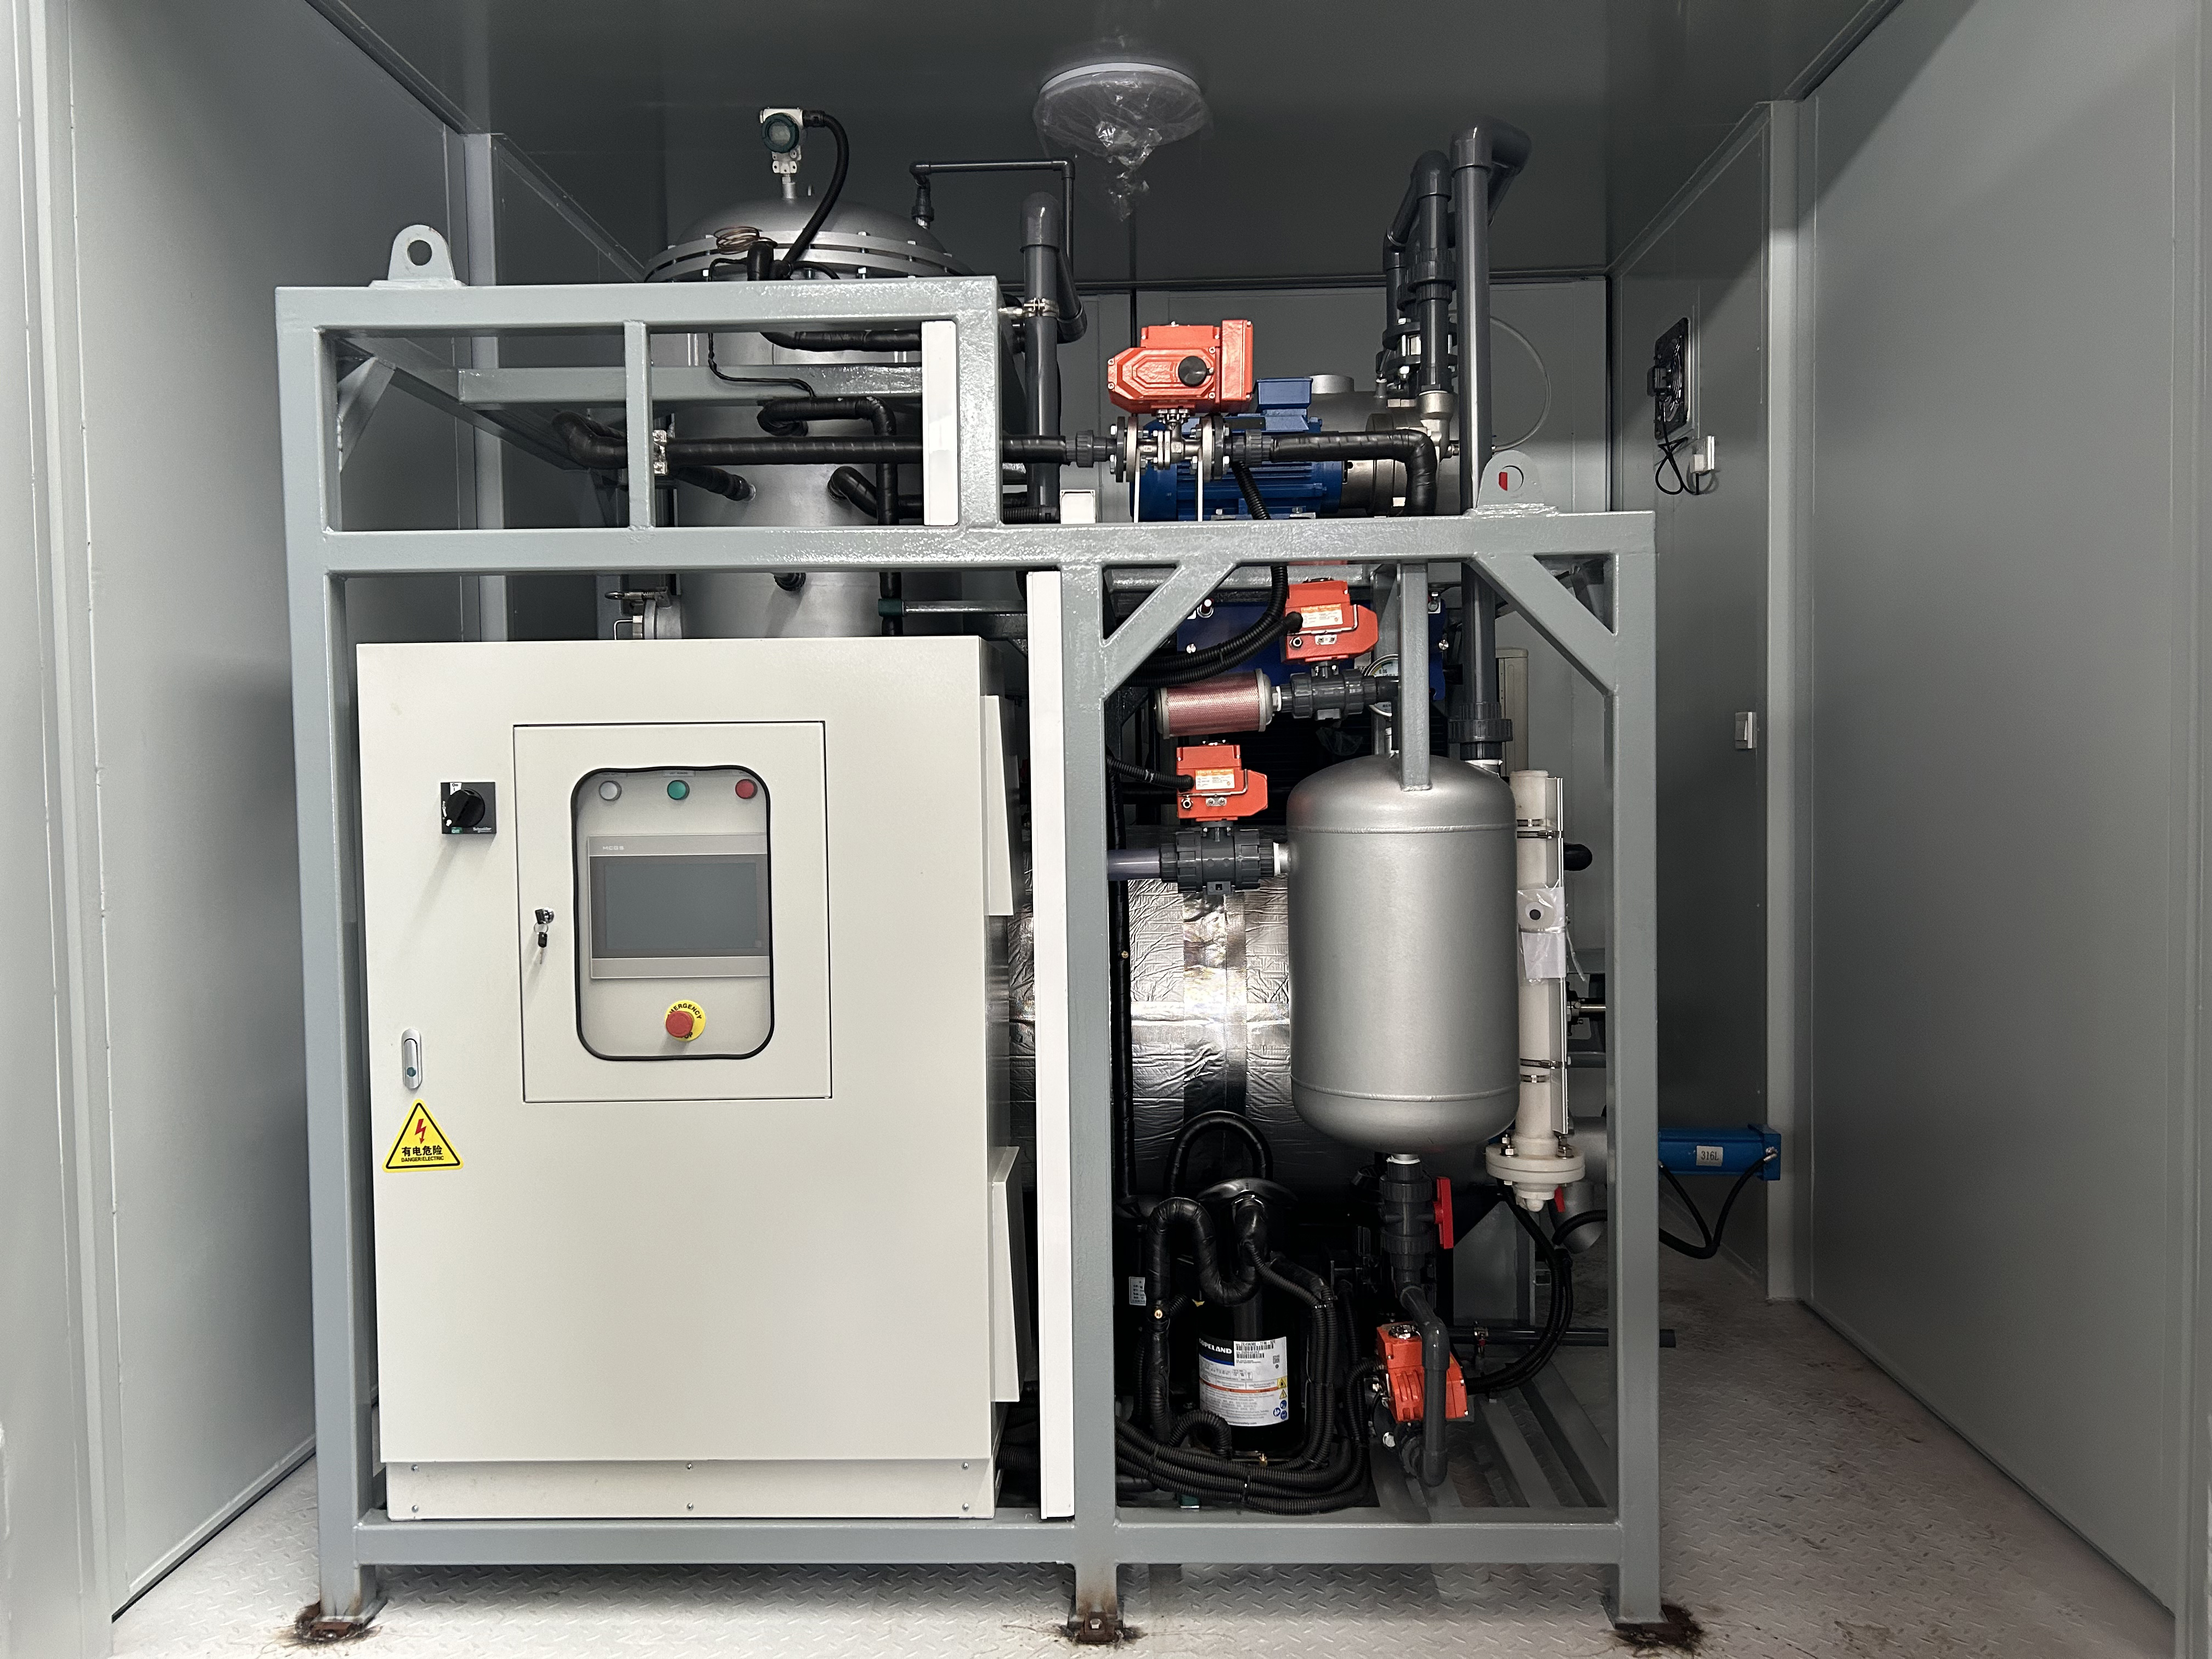
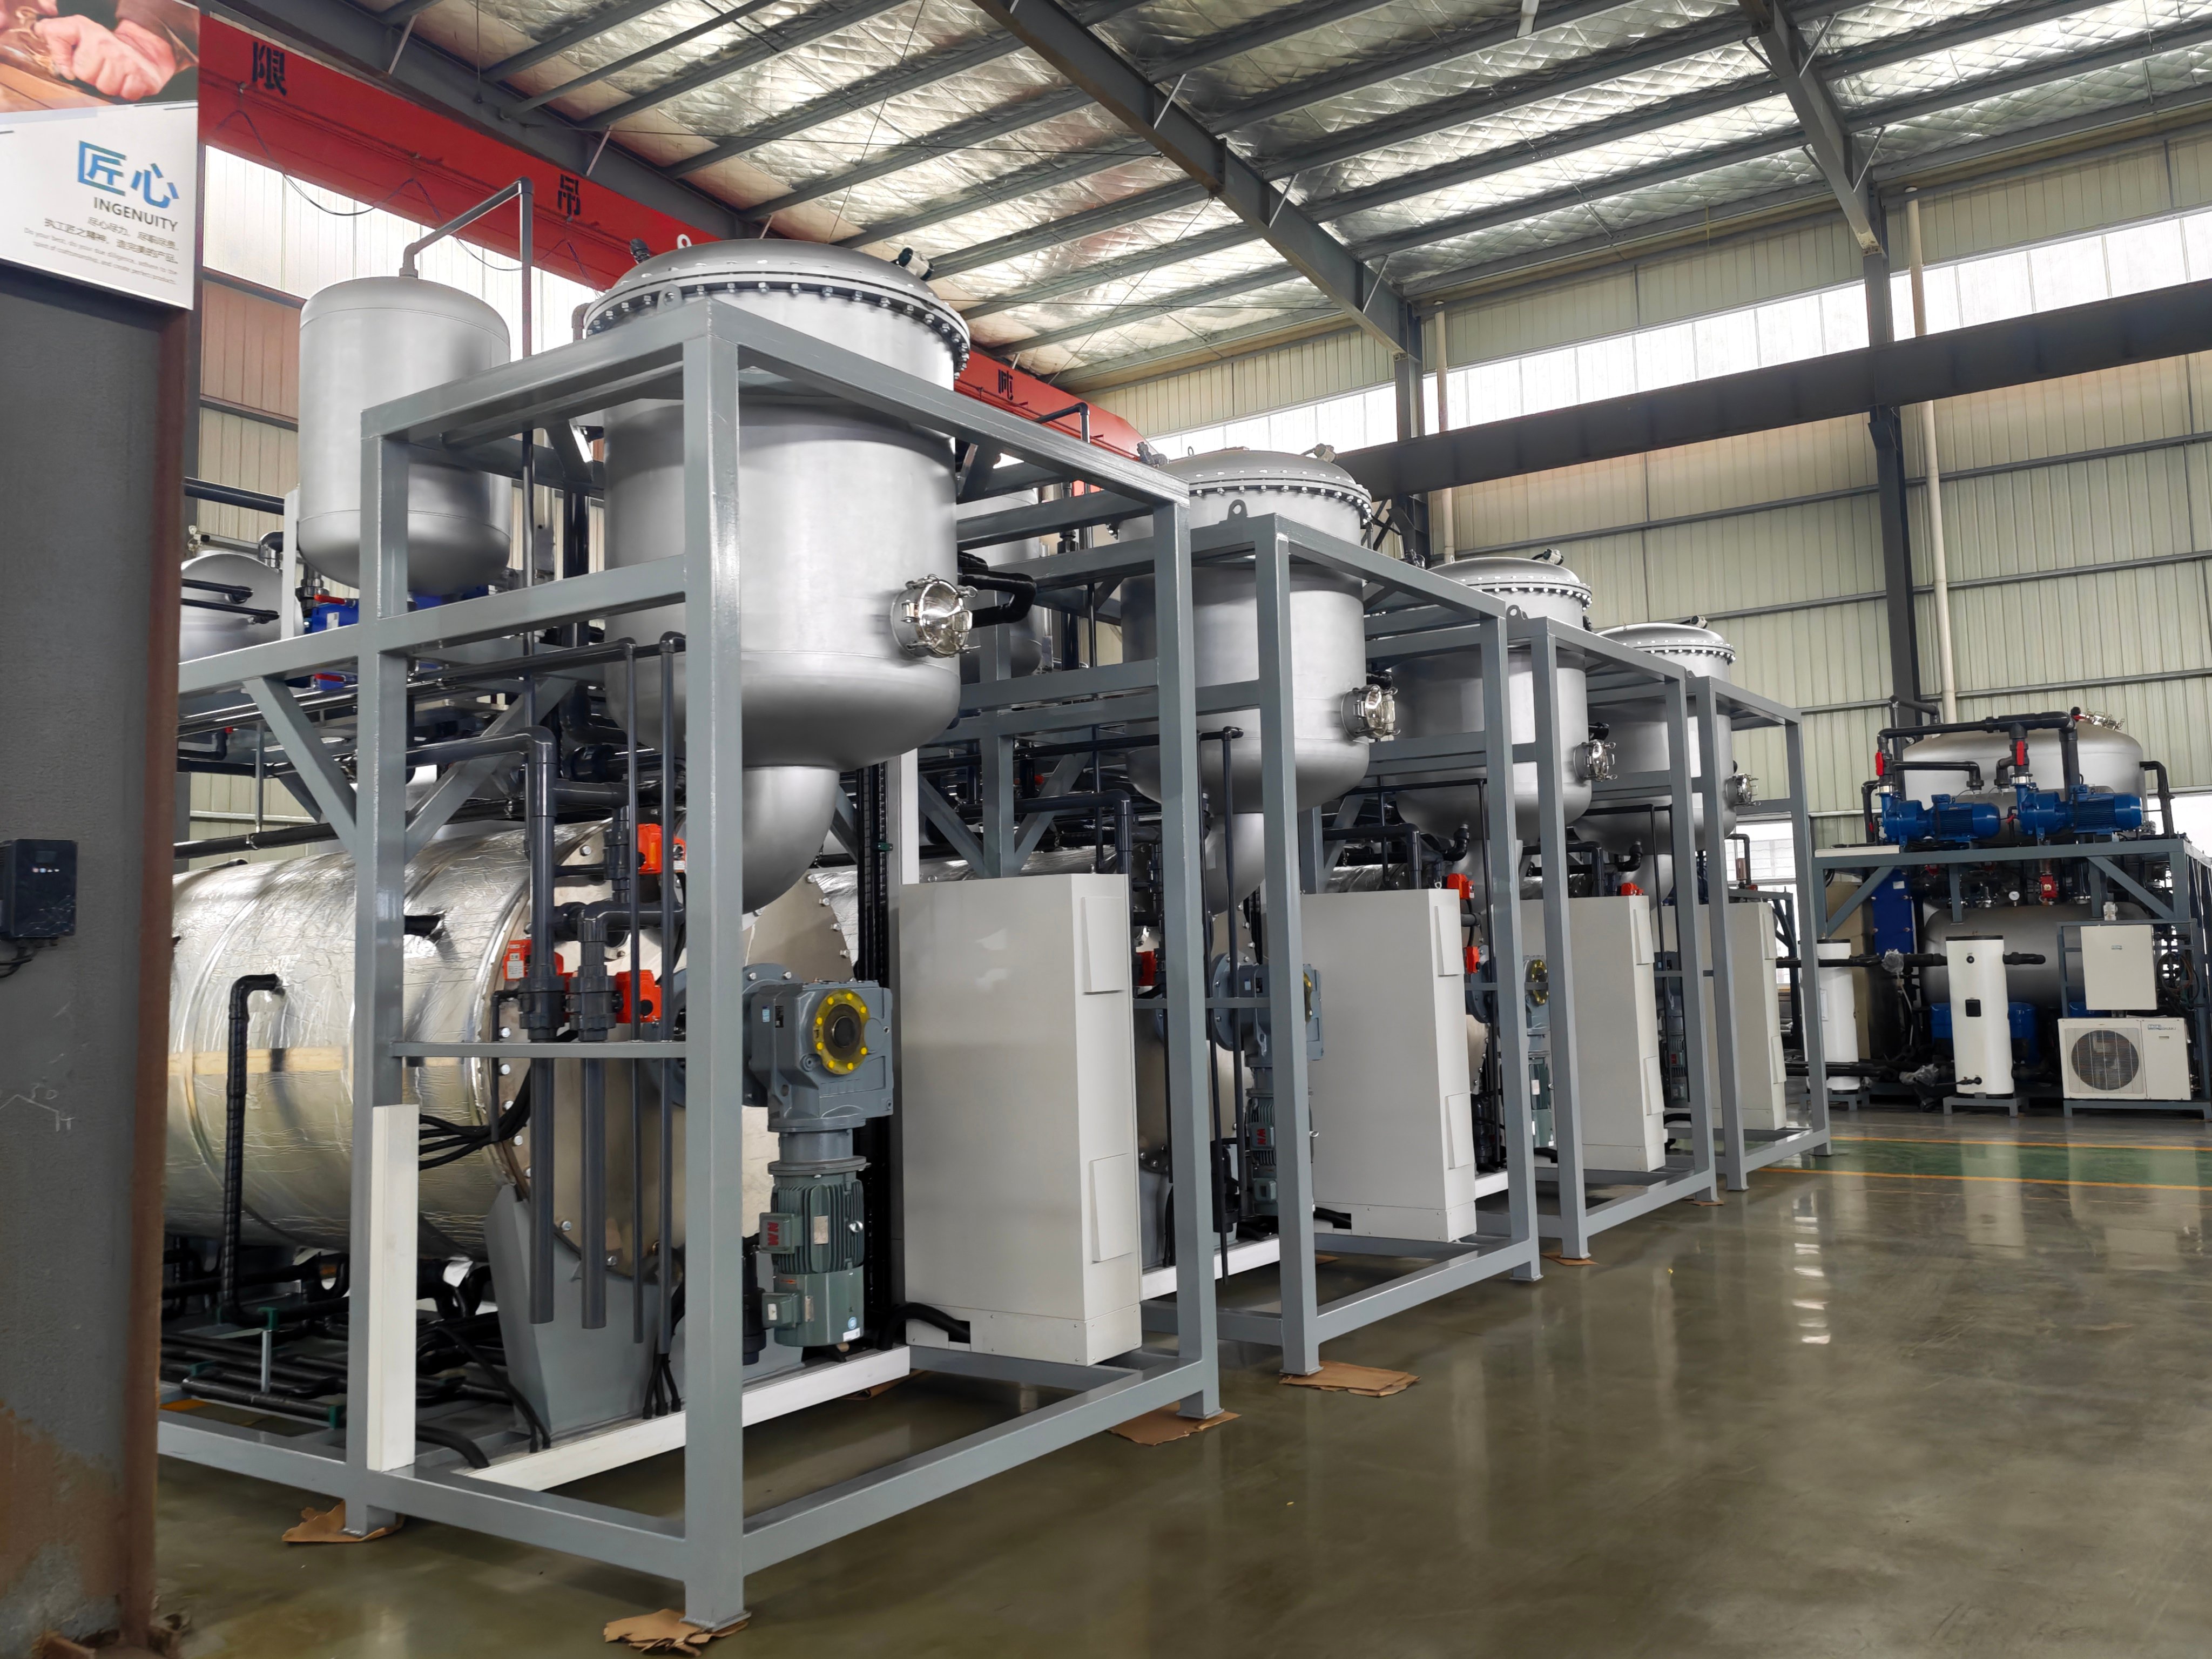
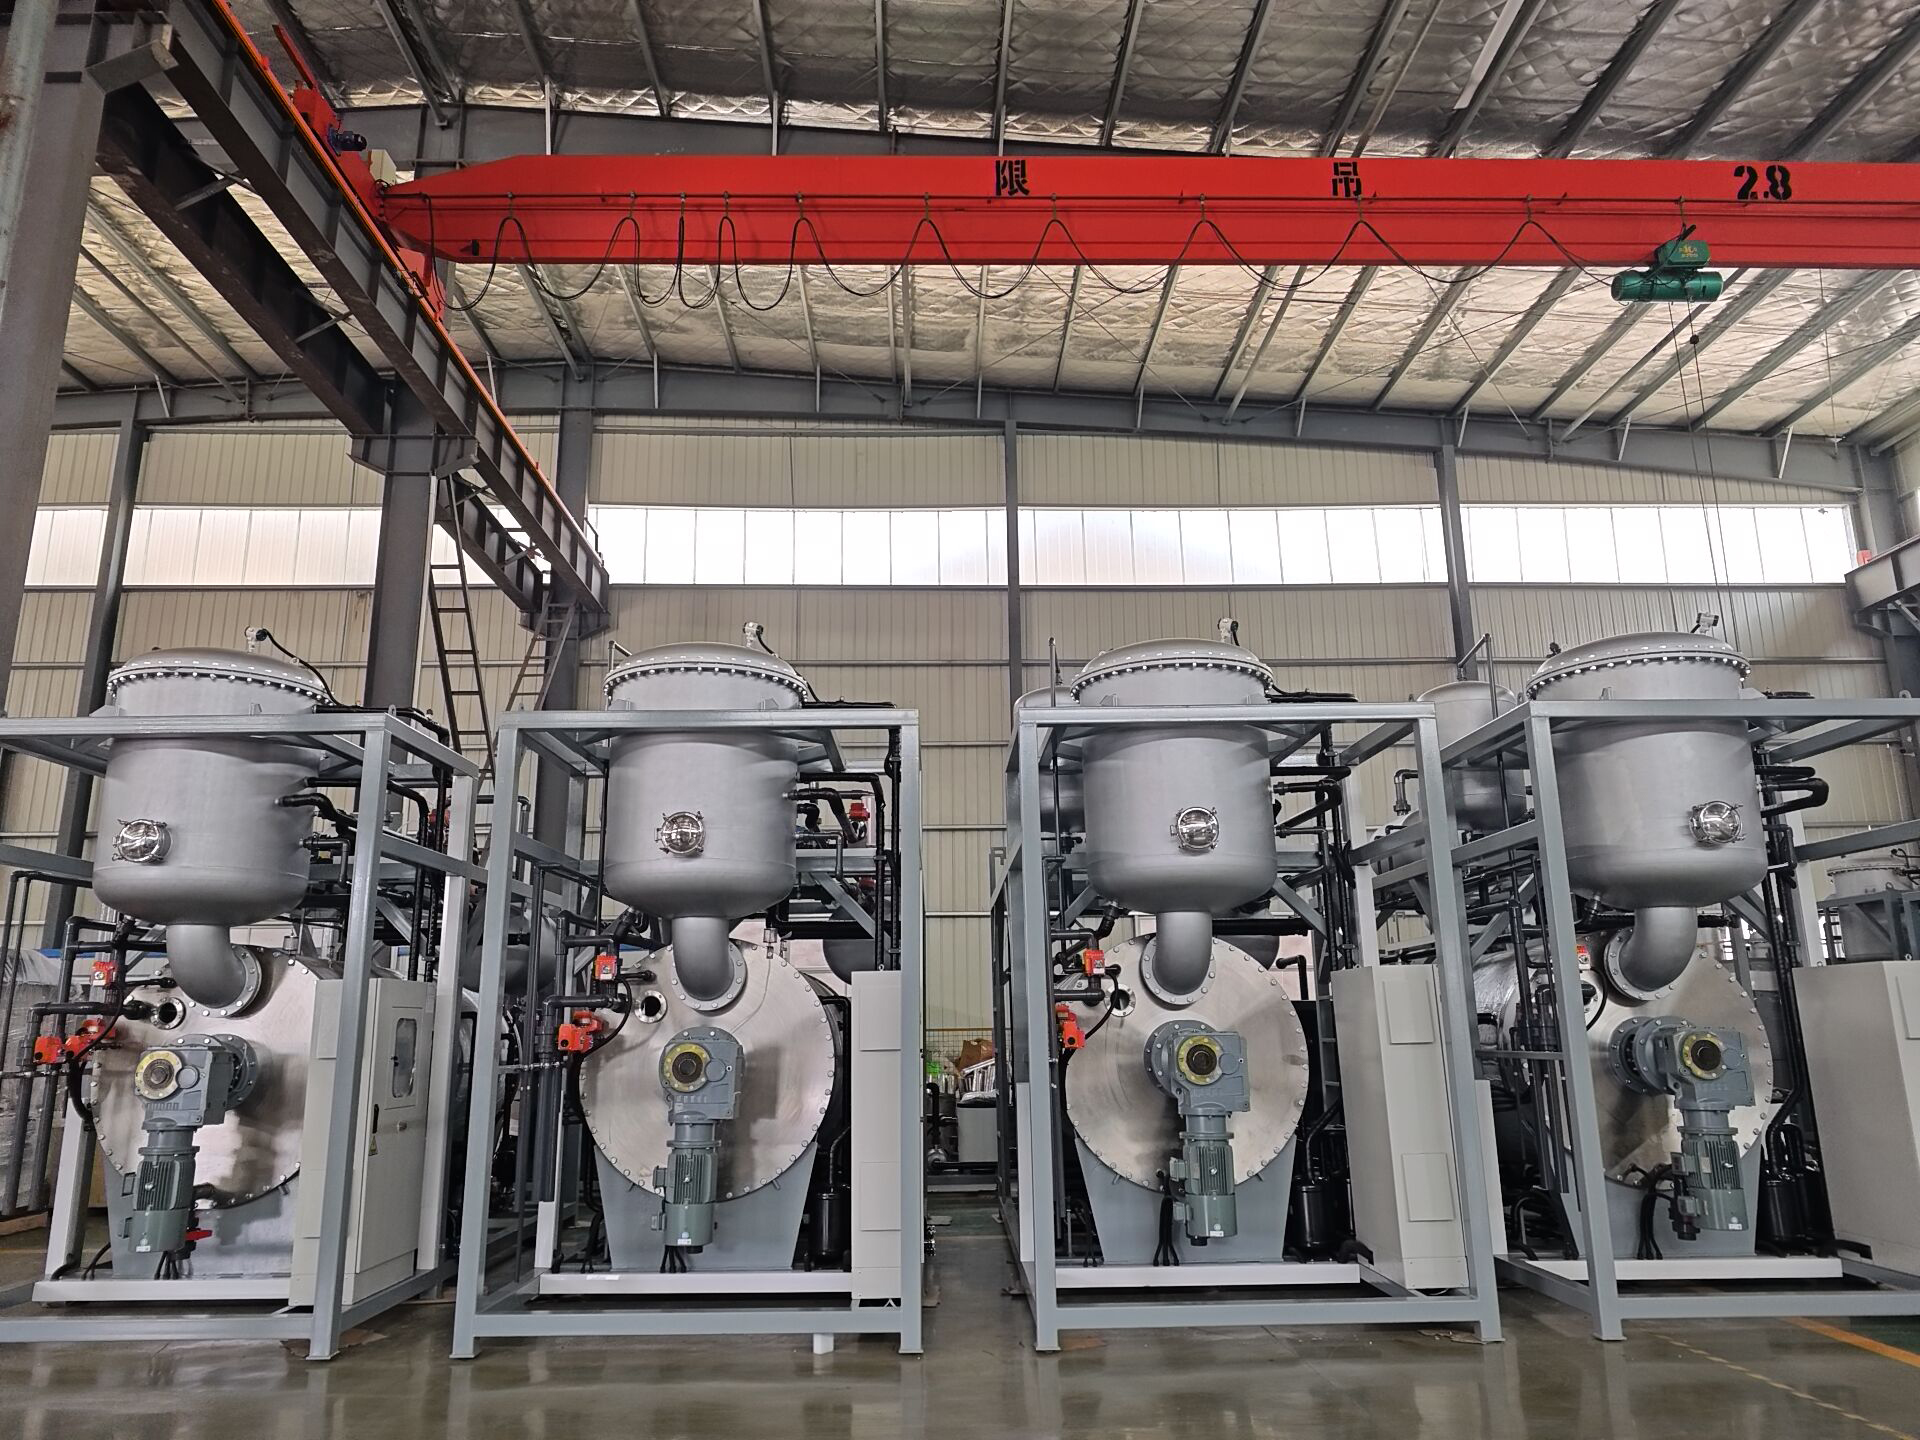
industrial crystallizer system
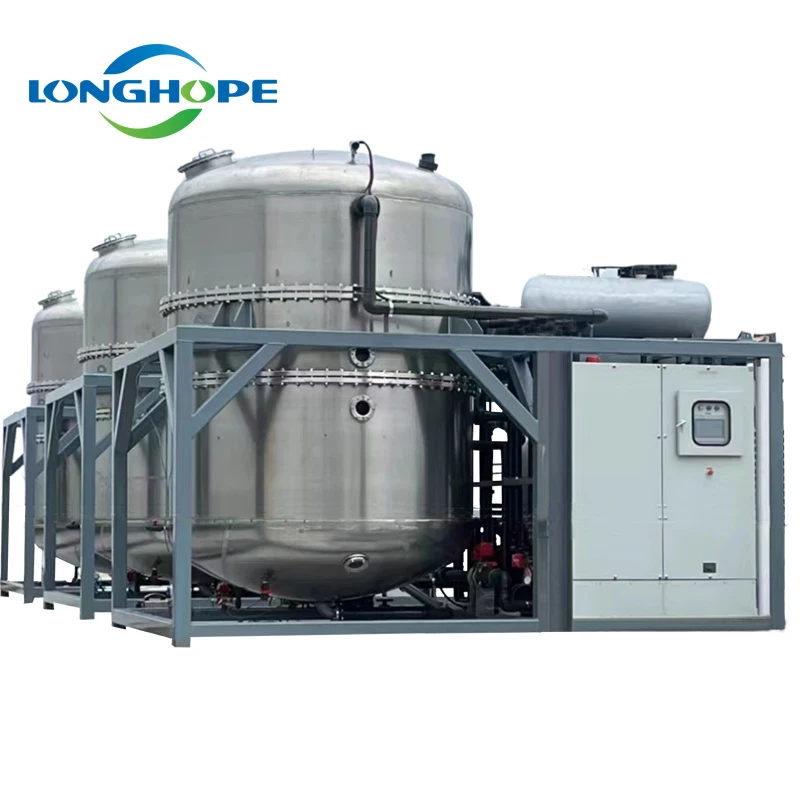
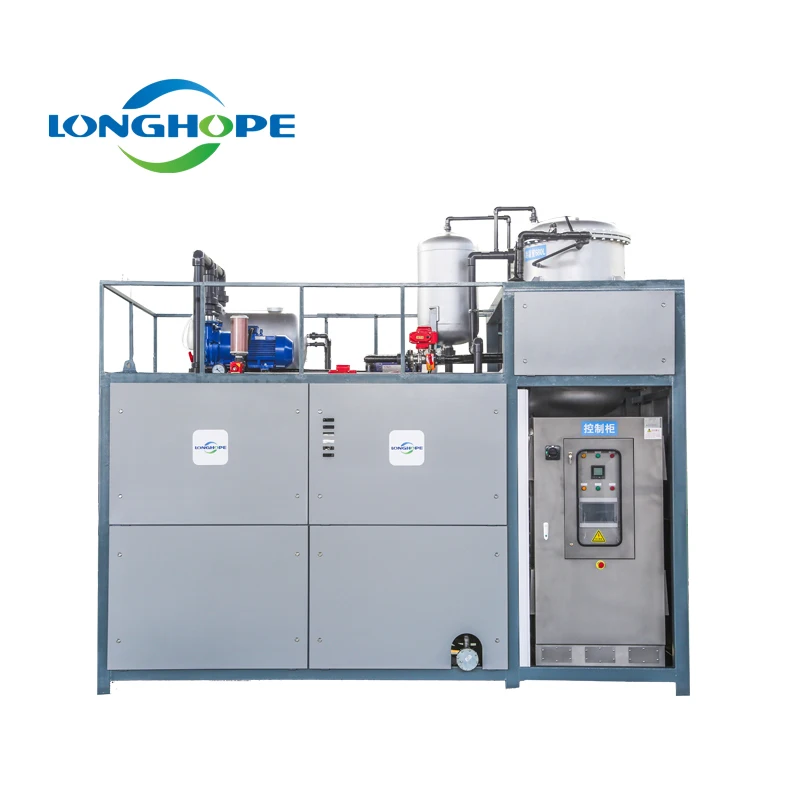
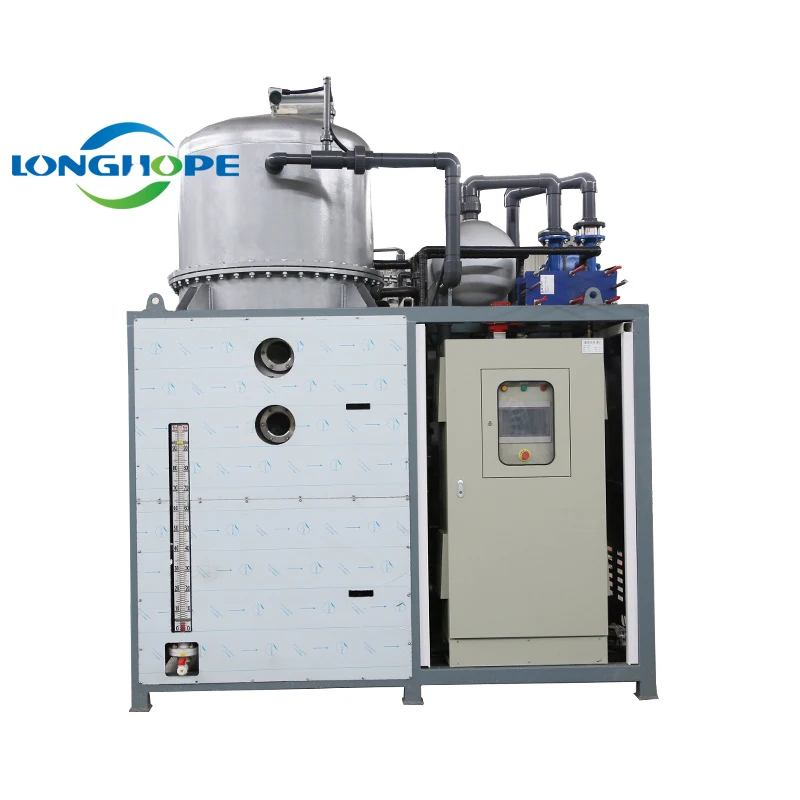
An industrial crystallizer system represents a critical piece of equipment designed to separate and purify dissolved solids from liquid solutions through controlled crystallization processes. This industrial crystallizer system operates by carefully managing temperature, pressure, and agitation to encourage crystal formation and growth. The primary function of an industrial crystallizer system involves transforming supersaturated solutions into solid crystals with uniform size and high purity levels.
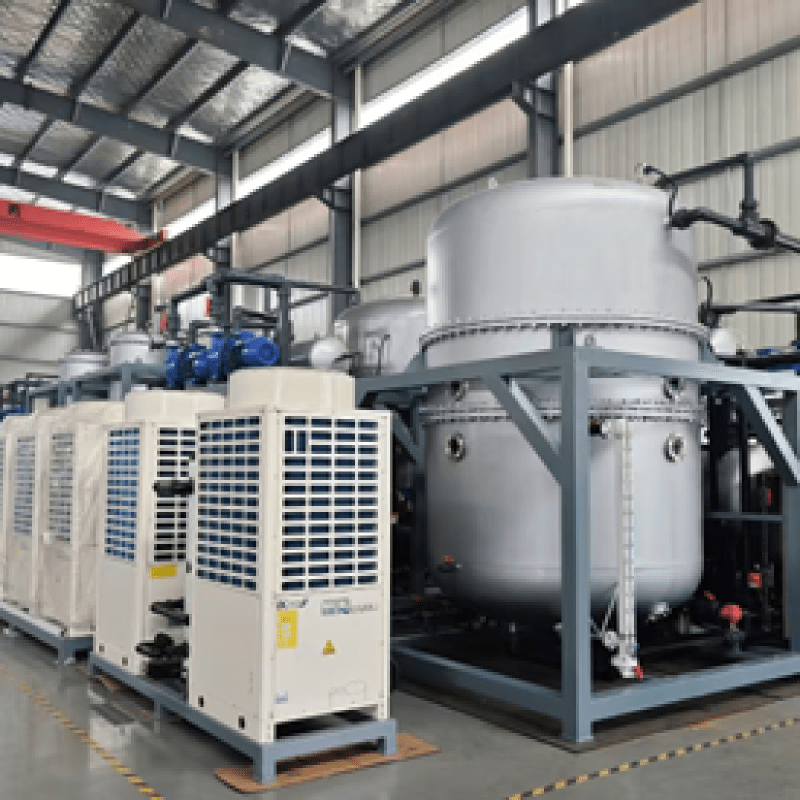
The technological features of an industrial crystallizer system include advanced temperature control mechanisms, automated monitoring systems, and specialized vessel designs that promote optimal crystal nucleation. Modern industrial crystallizer system designs incorporate energy-efficient cooling methods and real-time process monitoring capabilities. These systems maintain precise operational parameters to ensure consistent product quality.
An industrial crystallizer system finds extensive applications across multiple industries including pharmaceuticals, chemicals, food processing, and materials manufacturing. The system excels in producing high-purity crystals for active pharmaceutical ingredients, fine chemicals, and specialty materials. Operators utilize an industrial crystallizer system to achieve precise particle size distribution and crystal morphology specifications.
The versatility of industrial crystallizer system technology enables customization for various crystallization methods such as cooling crystallization, evaporative crystallization, and reactive crystallization. Industrial crystallizer system performance directly impacts product yield, purity, and production efficiency. Organizations implementing an industrial crystallizer system benefit from improved process control and reduced material waste throughout their manufacturing operations.

 EN