Industrial Crystallizer Manufacturer Solutions

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

industrial crystallizer manufacturer

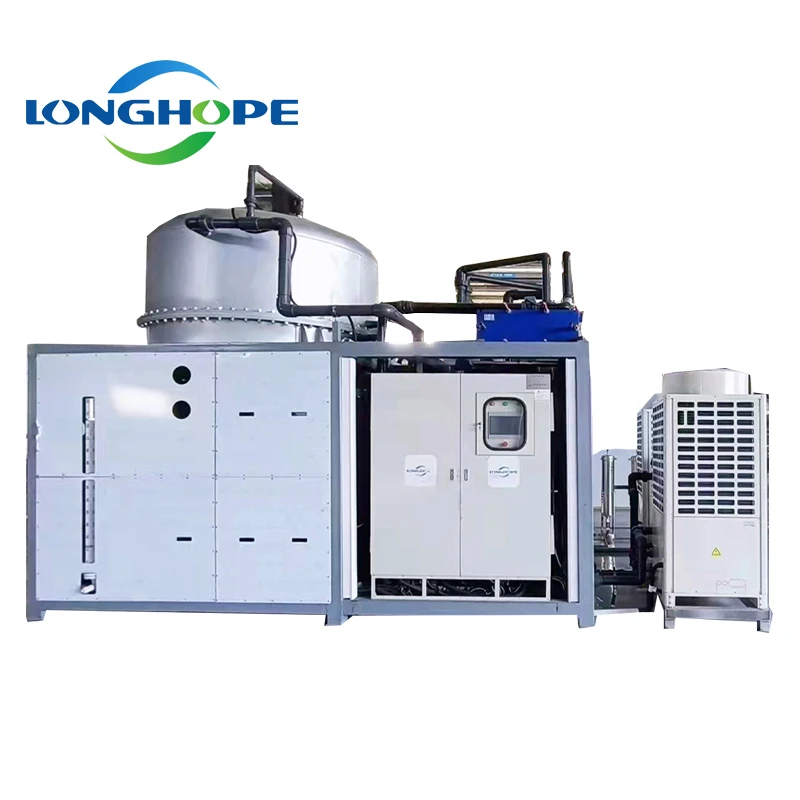
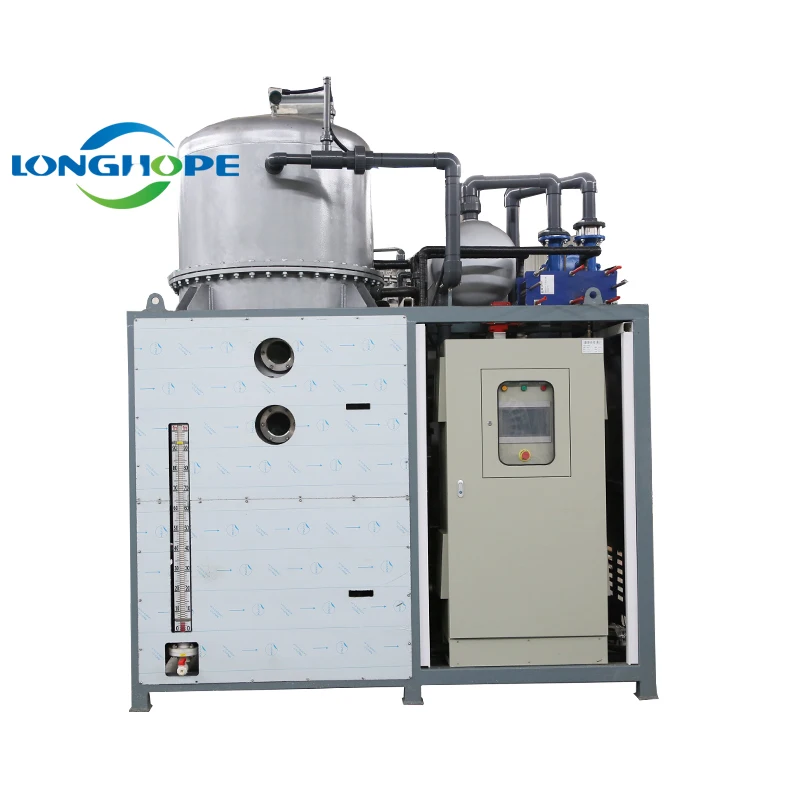
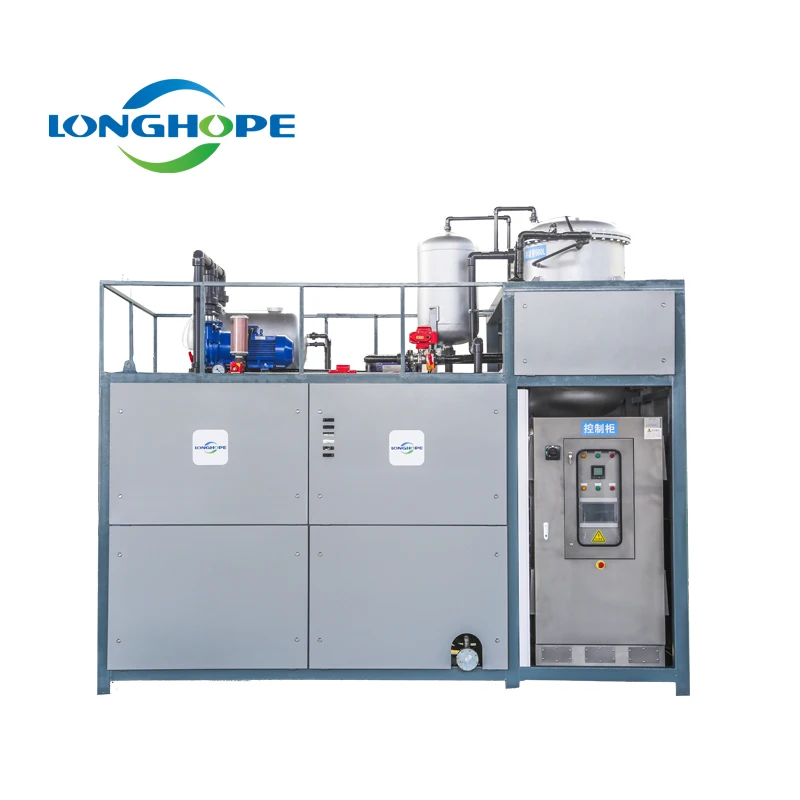
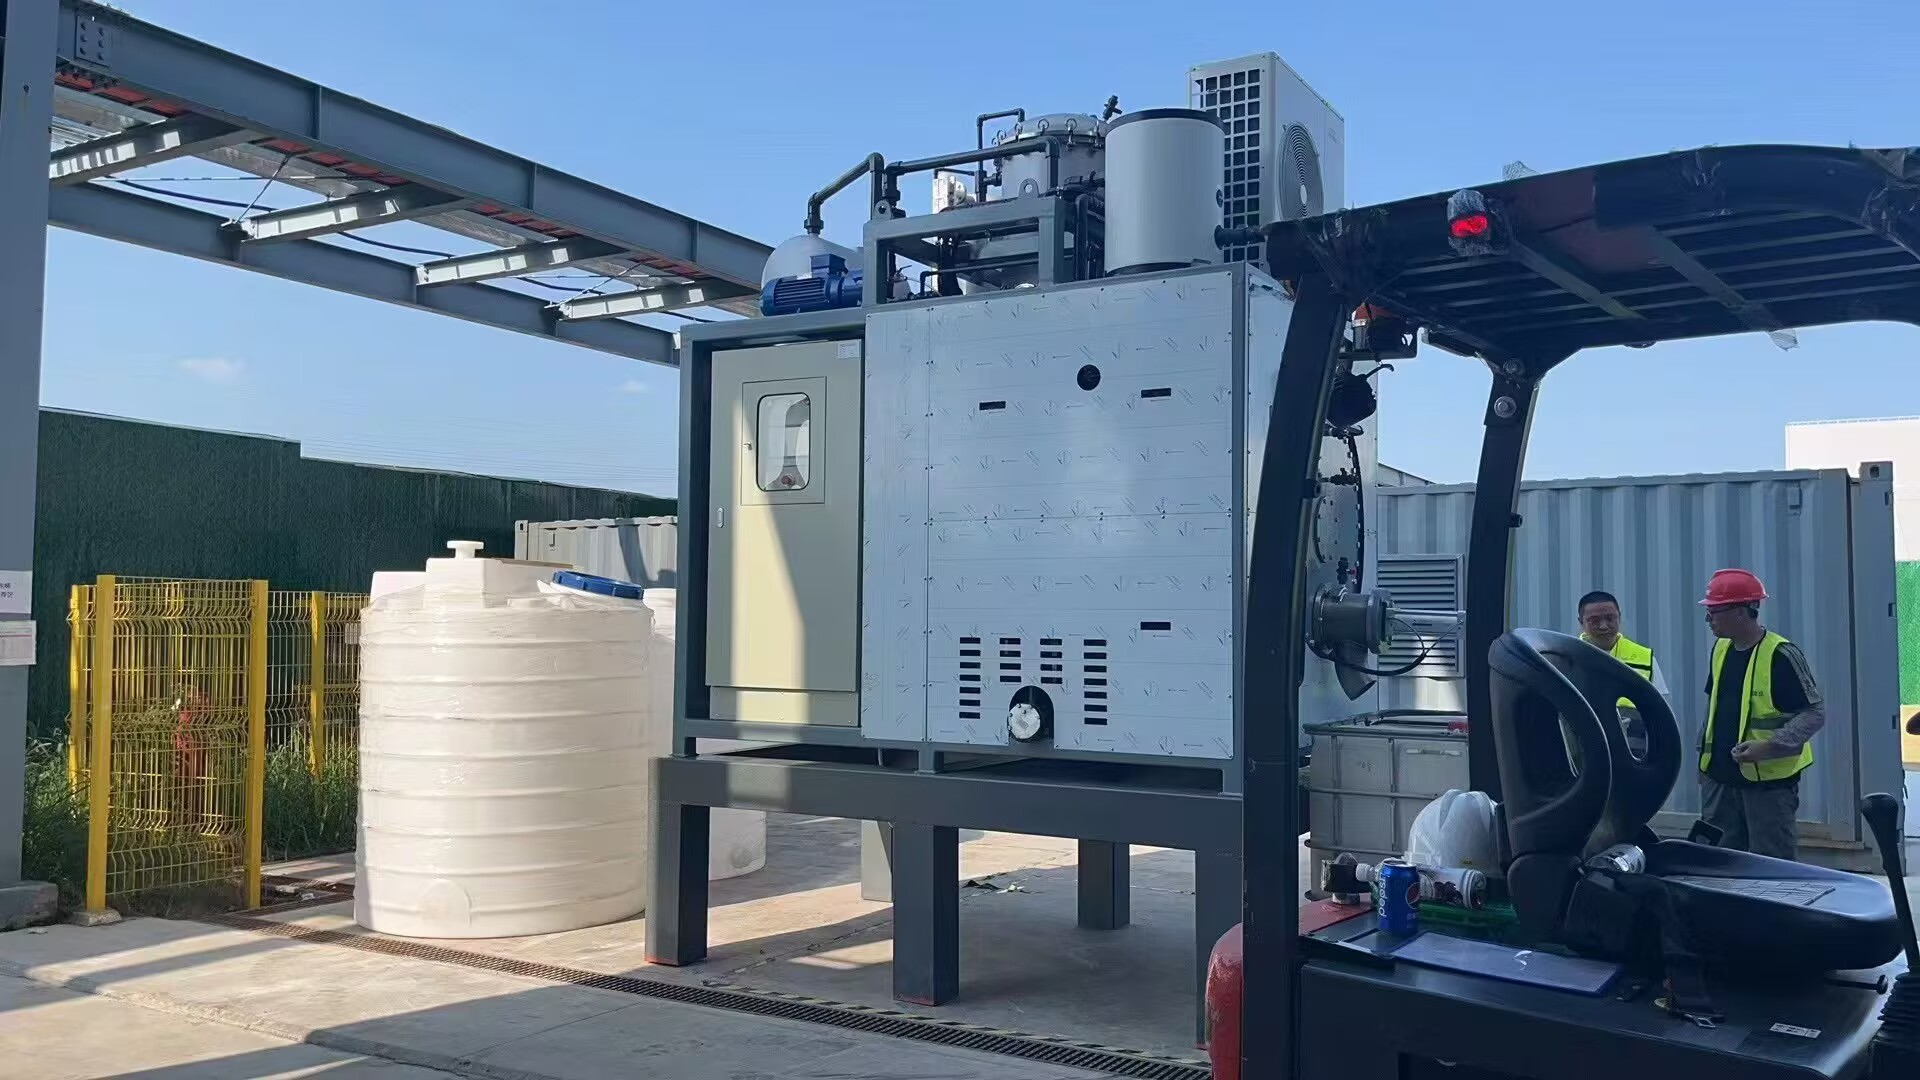
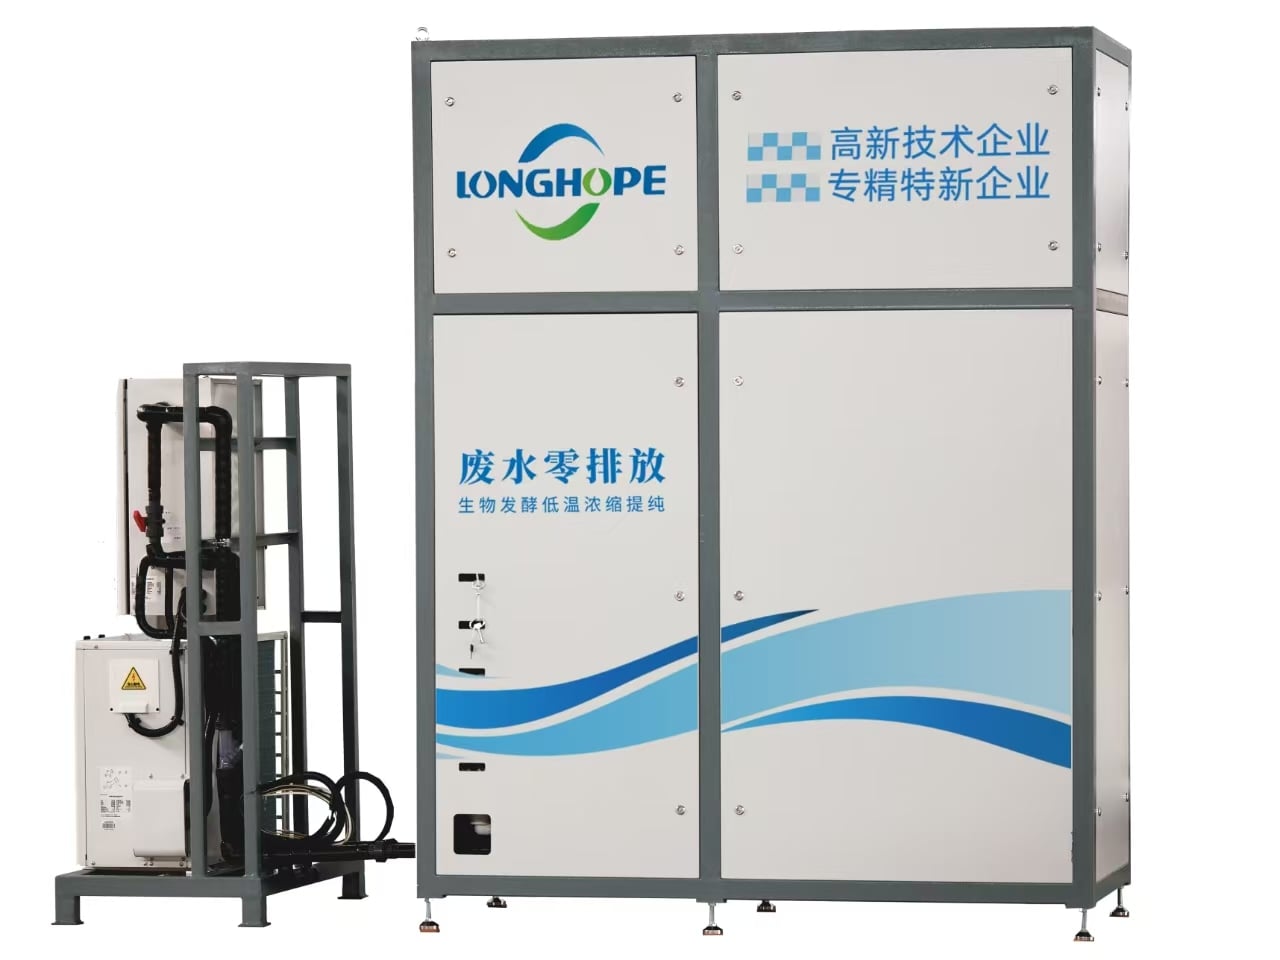
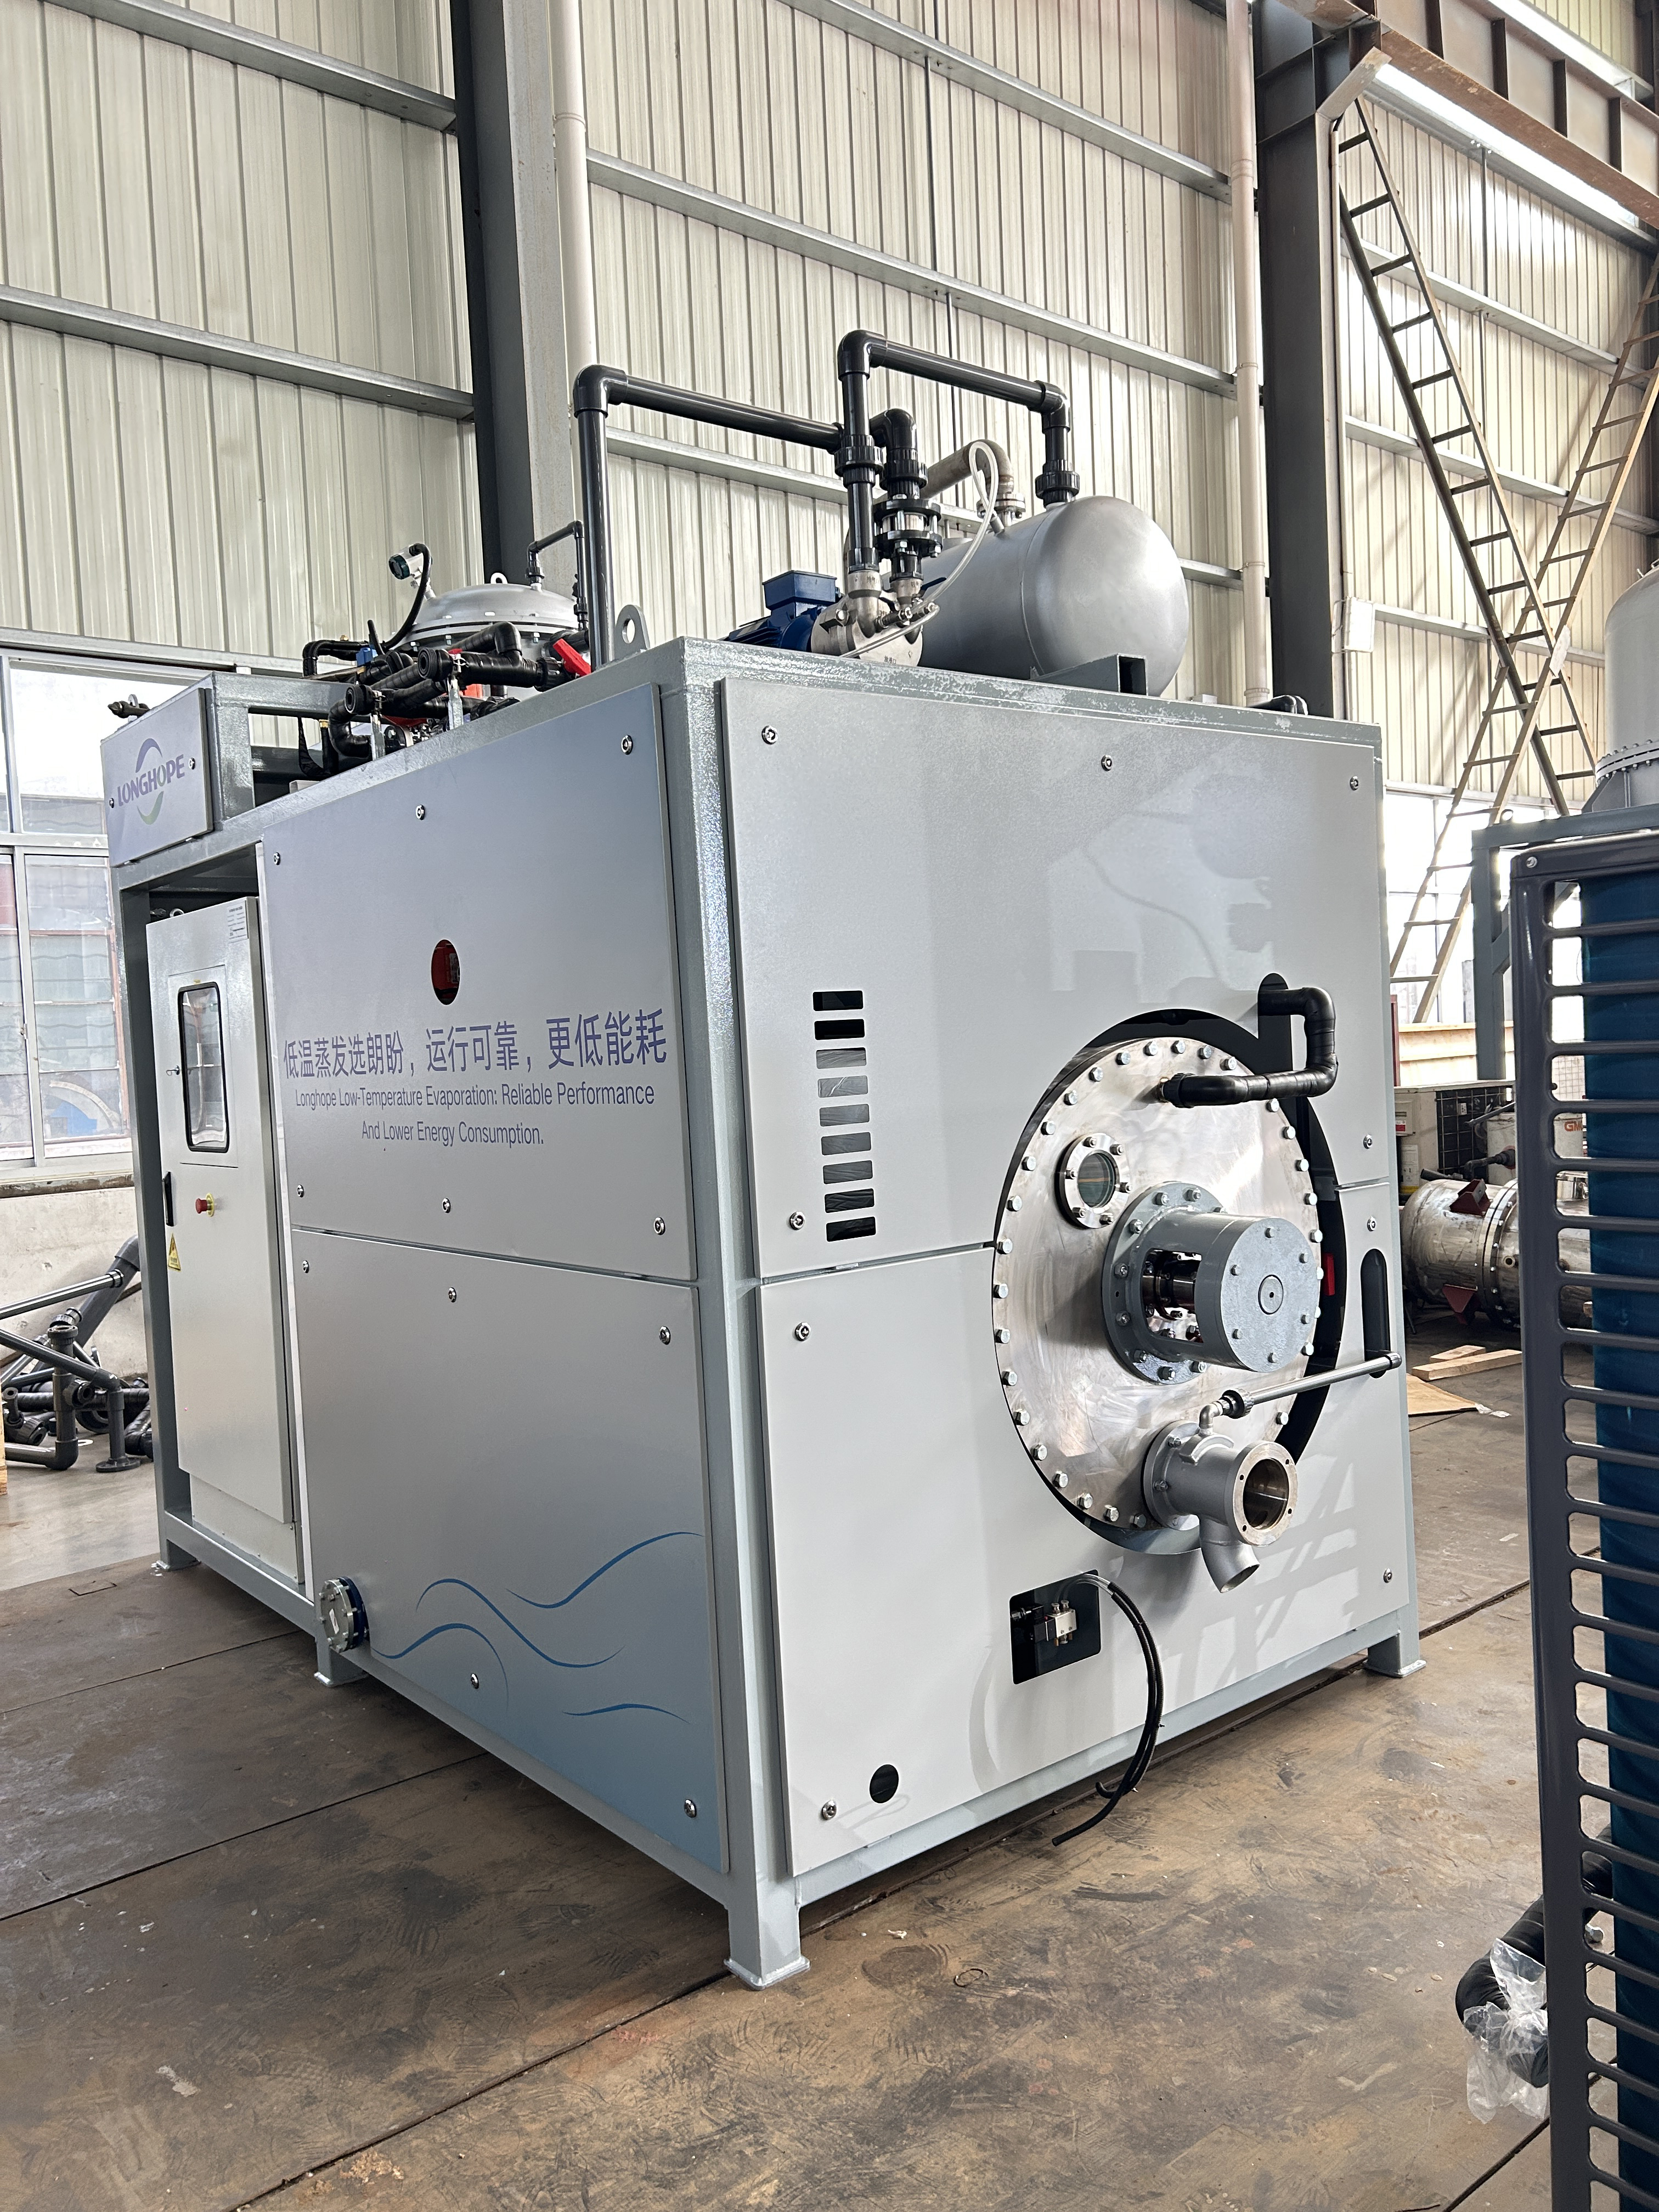
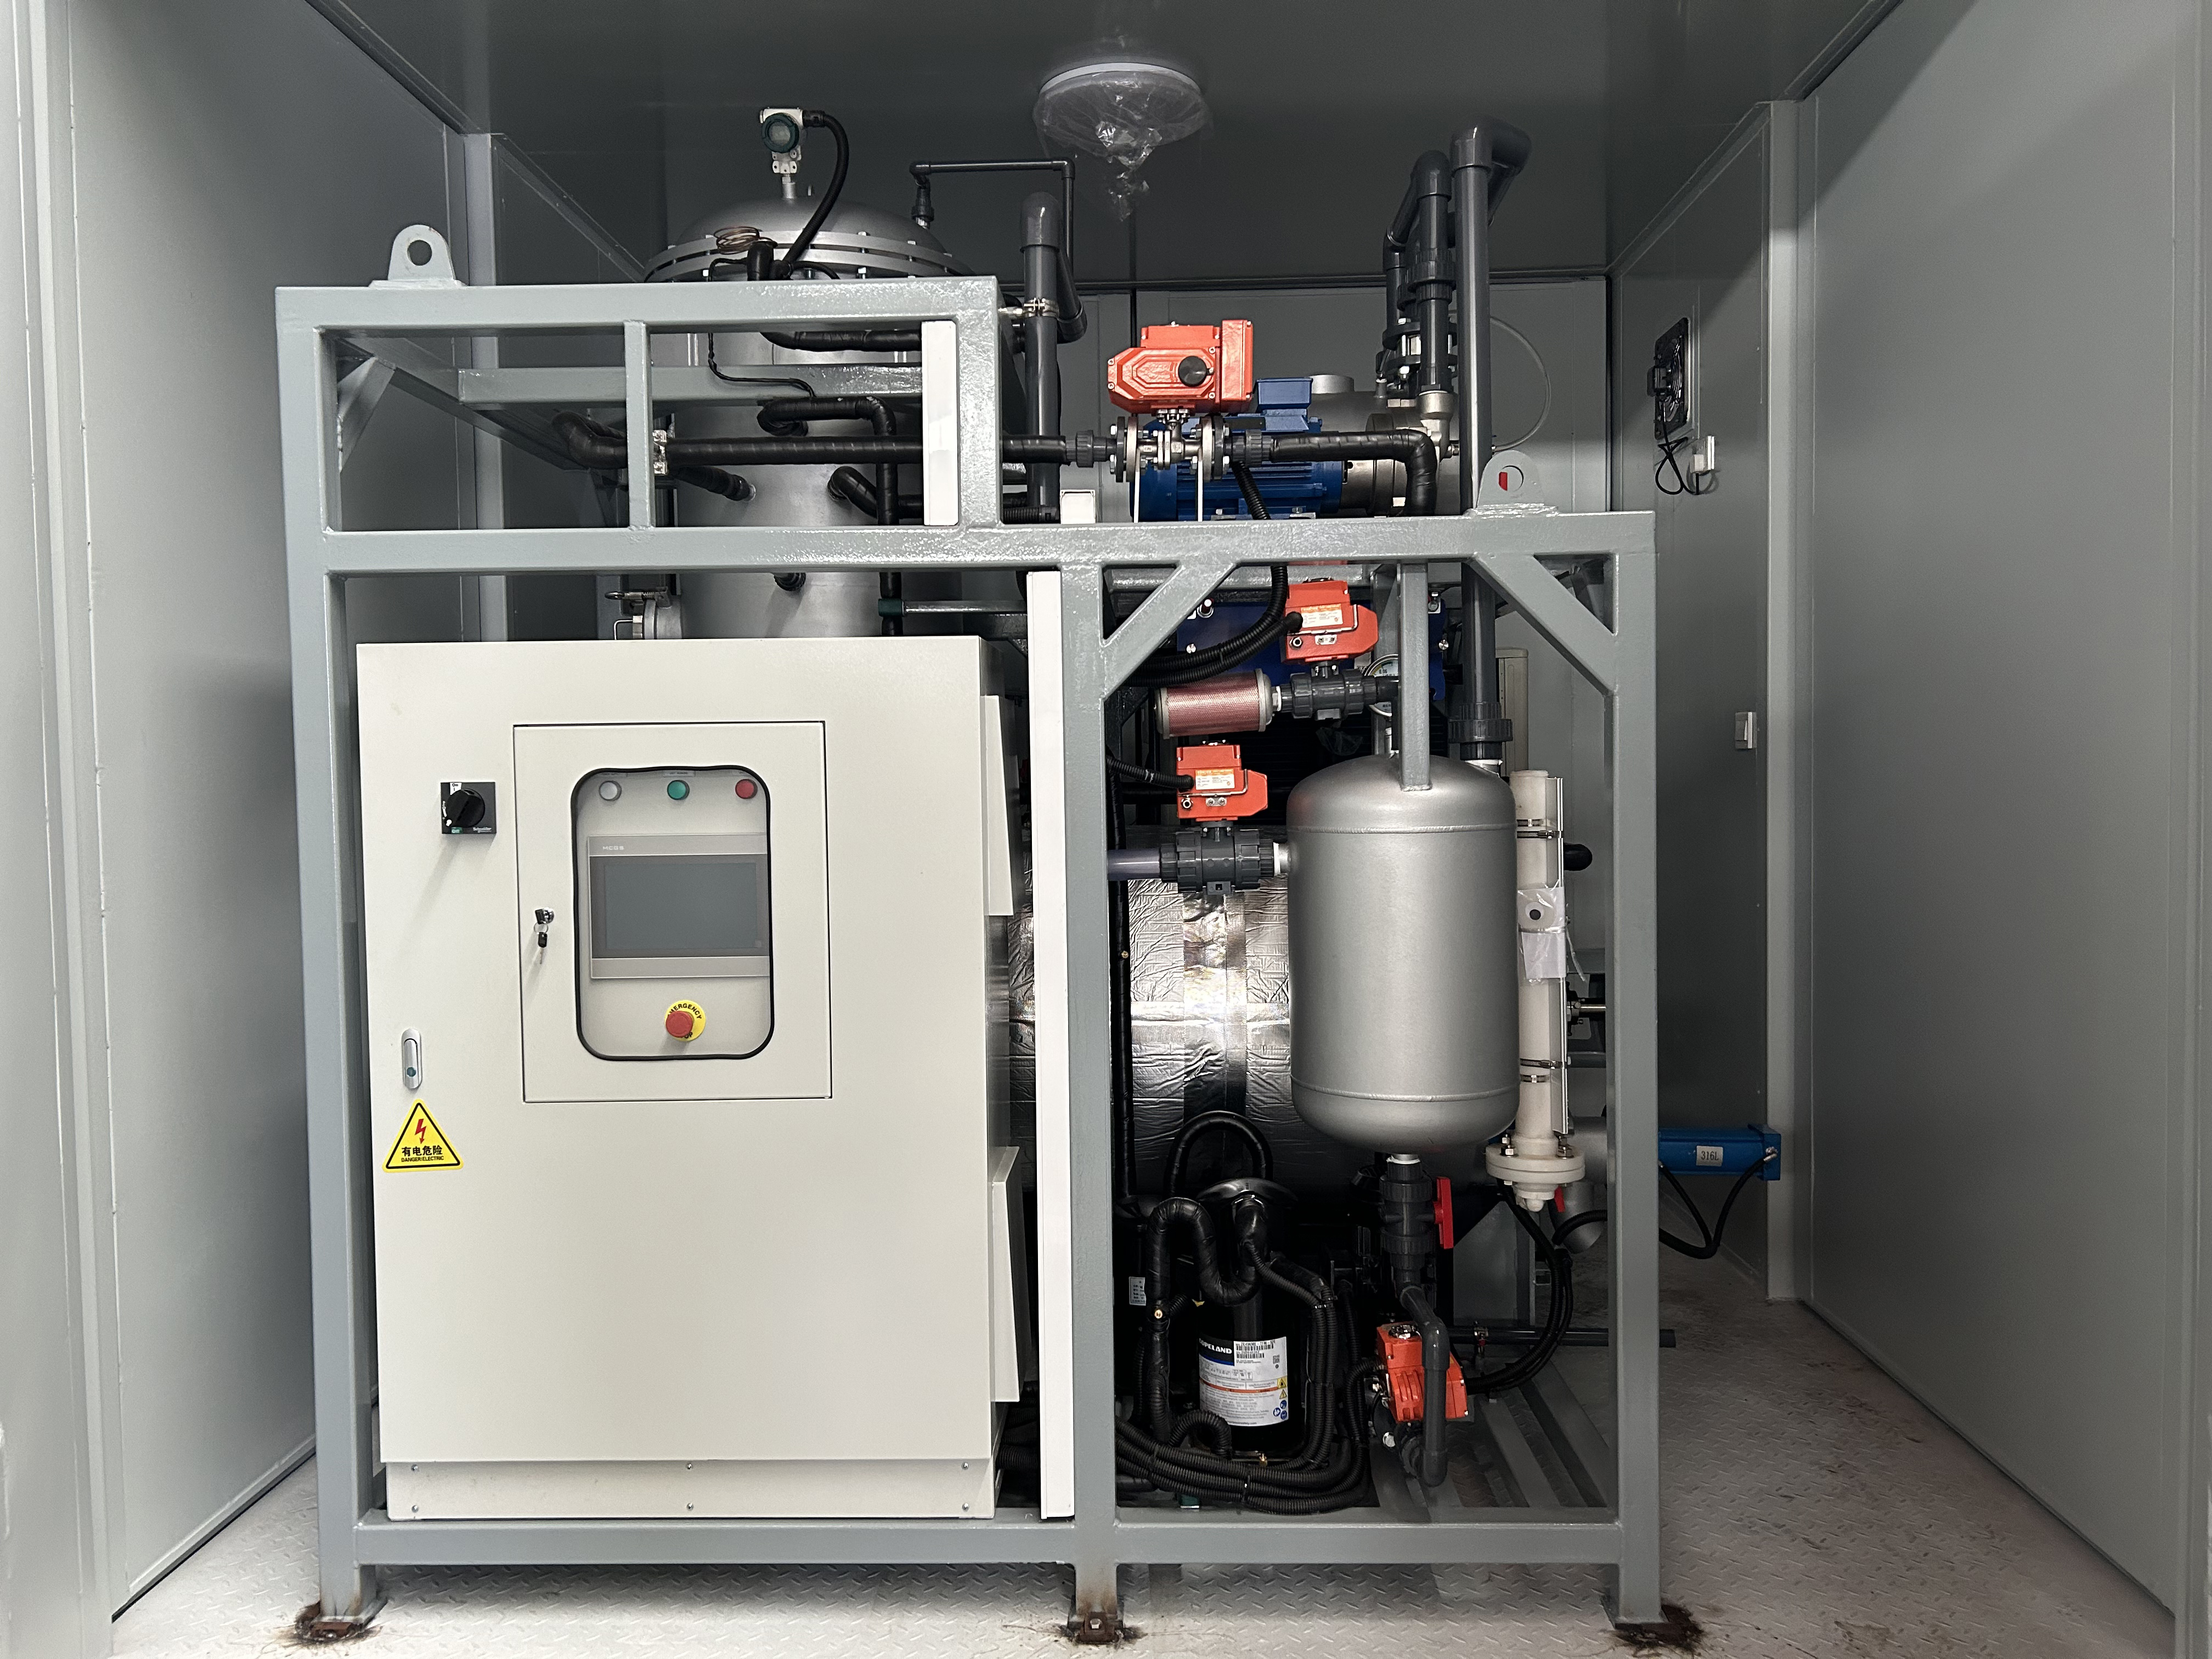
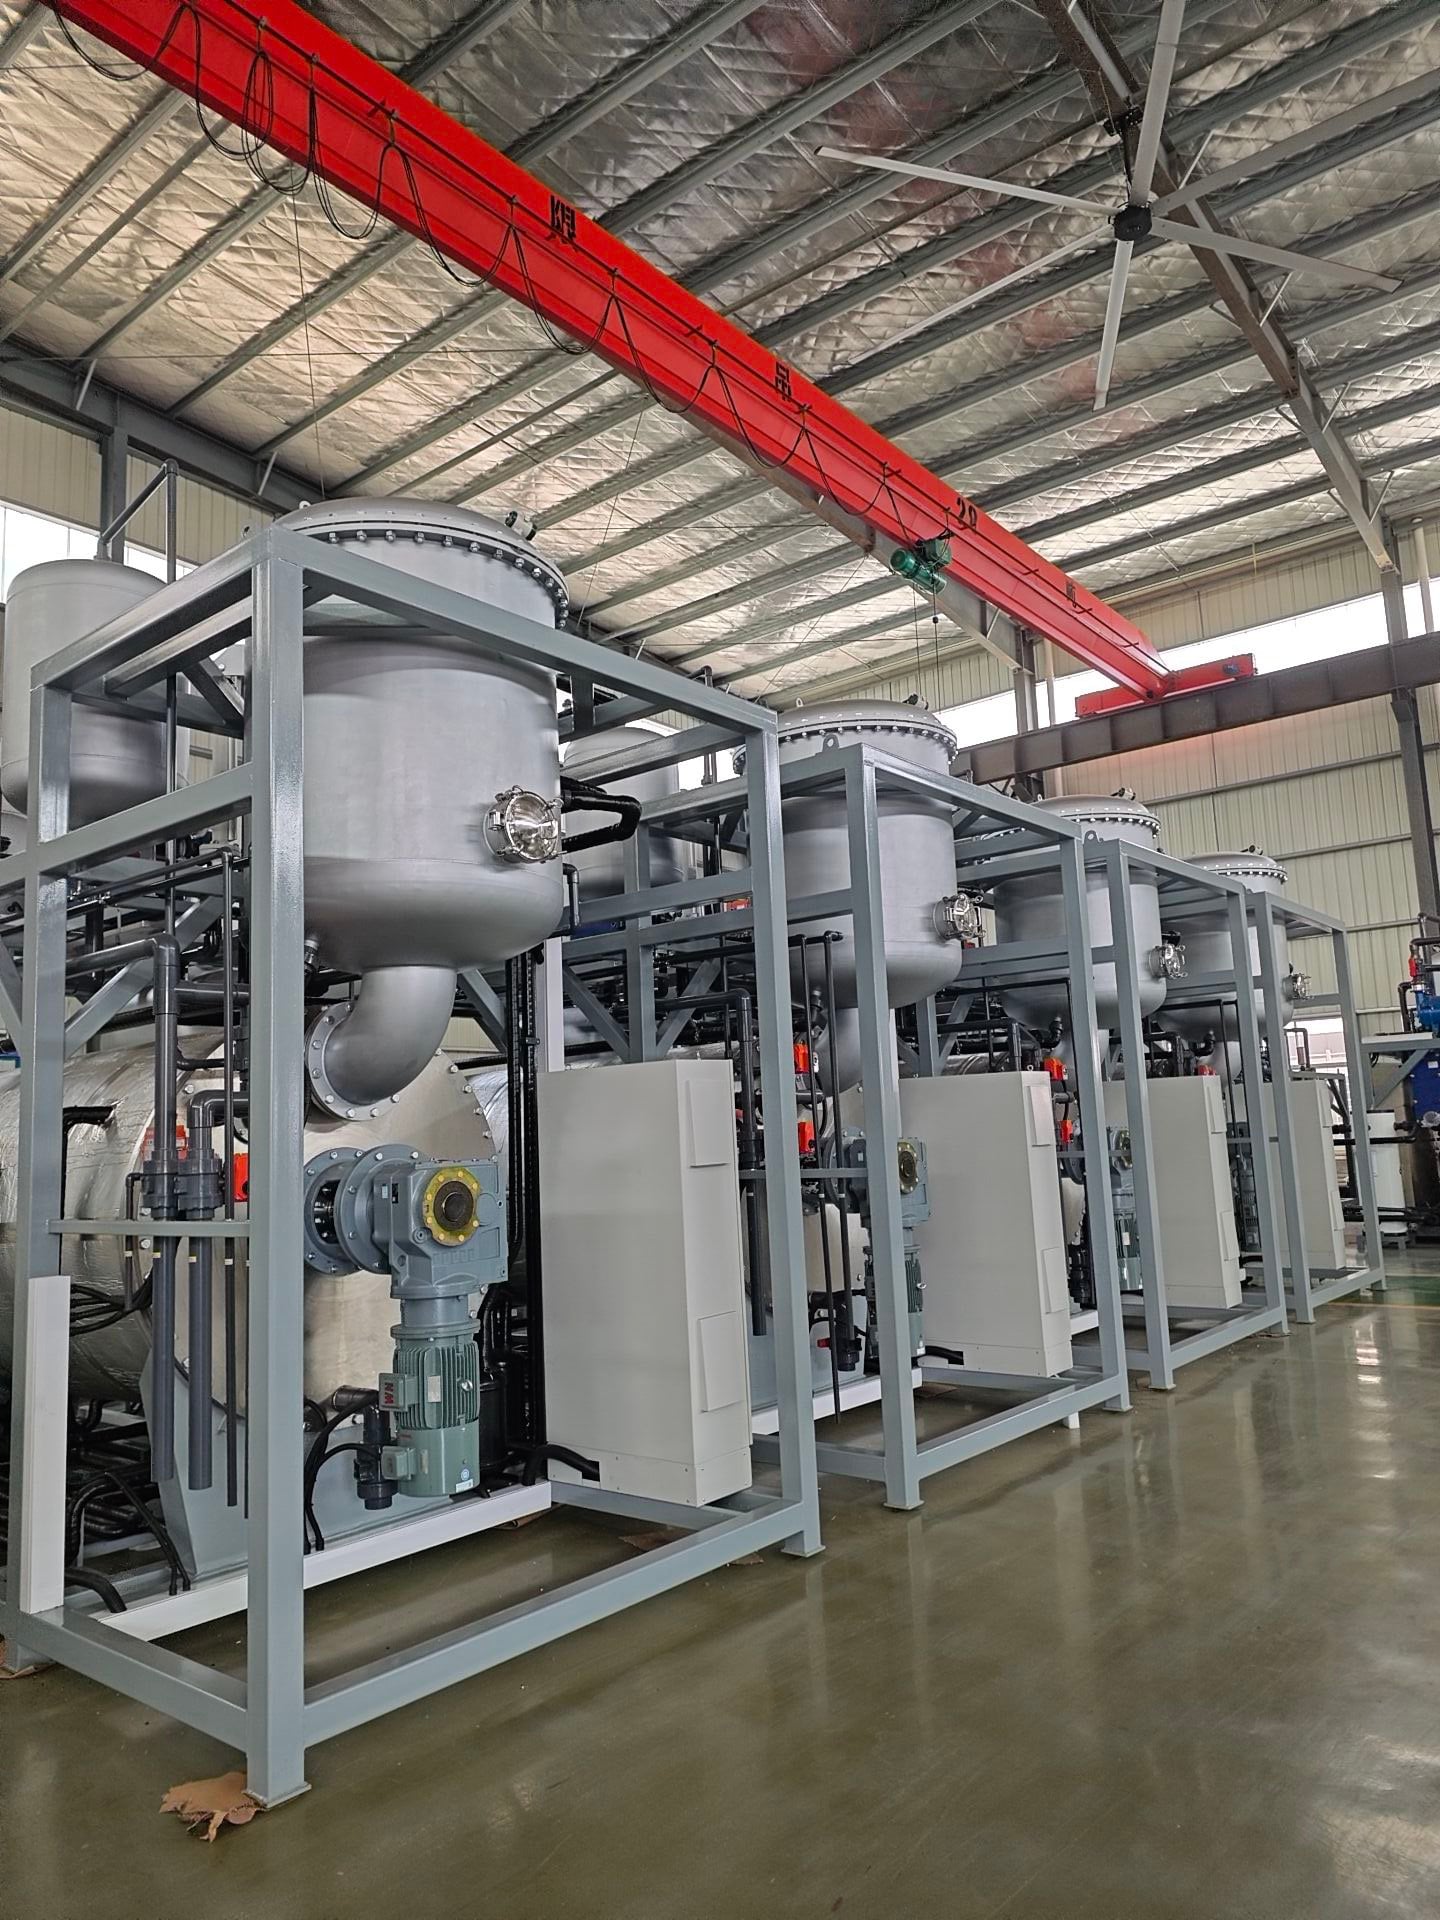
An industrial crystallizer manufacturer specializes in designing and producing advanced crystallization equipment that separates dissolved solids from liquid solutions through controlled cooling, evaporation, or precipitation processes. These systems are essential in chemical, pharmaceutical, food processing, and mining industries where pure crystal production is critical for product quality and operational efficiency. The industrial crystallizer manufacturer develops multiple crystallizer types, including batch crystallizers, continuous crystallizers, and vacuum crystallizers, each tailored to specific production requirements. These devices employ sophisticated temperature control, agitation mechanisms, and crystallization chambers to achieve optimal crystal formation and separation. Modern designs incorporate automated monitoring systems that track crystal growth, solution concentration, and temperature fluctuations in real time. Technological features of an industrial crystallizer manufacturer's equipment include precision heat exchangers, programmable logic controllers, and advanced filtration systems. These components work together to maximize crystal yield while minimizing impurities and energy consumption. The equipment handles various substances, from sodium chloride to pharmaceutical compounds, demonstrating remarkable versatility. Applications span numerous industries: pharmaceutical manufacturers use these crystallizers to purify active ingredients, chemical producers rely on them for salt crystallization, and food processors employ them for sugar refinement. Mining operations utilize crystallization technology for mineral extraction and purification. An industrial crystallizer manufacturer provides customizable solutions that adapt to different production scales, from laboratory testing to large-scale industrial operations, ensuring consistent, high-quality crystal products across diverse applications and manufacturing environments.

New Product Releases

Choosing an industrial crystallizer manufacturer offers substantial operational and economic benefits that directly impact your production capabilities and profitability. These manufacturers deliver equipment that significantly increases crystal purity and yield, reducing waste and improving your bottom line through enhanced product quality and reduced material loss. The primary advantage involves superior energy efficiency. An industrial crystallizer manufacturer designs systems that minimize energy consumption through optimized temperature management and innovative cooling technologies. This translates to lower operational costs and reduced environmental impact, making your facility more sustainable and cost-effective. Operational reliability represents another critical benefit. Equipment from an industrial crystallizer manufacturer undergoes rigorous testing and incorporates redundant safety systems, ensuring consistent performance and minimal downtime. This reliability protects your production schedule and maintains customer satisfaction through dependable delivery timelines. Customization capabilities distinguish reputable manufacturers. An industrial crystallizer manufacturer tailors equipment to your specific material properties, production volume, and quality standards. This personalized approach ensures optimal performance for your unique application rather than forcing your process into generic equipment. Technical support and maintenance services provided by an industrial crystallizer manufacturer extend equipment lifespan and prevent costly interruptions. Expert technicians offer training, spare parts availability, and troubleshooting assistance, maximizing your return on investment. Scalability is particularly valuable for growing operations. An industrial crystallizer manufacturer can design systems that expand with your business, allowing you to increase production capacity without complete equipment replacement. This flexibility supports long-term business growth and strategic planning, making equipment investments more sustainable and financially prudent for evolving enterprises.

Tips And Tricks

How to Optimize Your Evaporator System for Efficiency

24

Jul

How to Optimize Your Evaporator System for Efficiency

An evaporator system efficiency directly impacts your operational costs, production capacity, and environmental footprint in industrial processing. Whether you operate in chemical manufacturing, food processing, pharmaceutical production, or waste ma...
View More
How Industrial Water Treatment Saves Costs and Resources

24

Jul

How Industrial Water Treatment Saves Costs and Resources

Industrial water treatment represents one of the most significant opportunities for manufacturing facilities to reduce operational expenses while protecting environmental resources. Organizations across industries face mounting pressure to minimize w...
View More
Choosing the Right Evaporator System for Your Plant

24

Jul

Choosing the Right Evaporator System for Your Plant

Selecting an evaporator system for your industrial plant is one of the most critical decisions you will make in your facility's operational strategy. An evaporator system directly impacts energy consumption, product quality, waste management efficien...
View More
Vacuum Distillation Setup Maintenance for Longevity

02

Sep

Vacuum Distillation Setup Maintenance for Longevity

A vacuum distillation setup represents a significant investment in industrial separation technology, and protecting that investment requires a structured maintenance approach. Whether your vacuum distillation setup operates in a pharmaceutical labora...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

industrial crystallizer manufacturer

Precision Crystal Quality Control

Precision Crystal Quality Control

An industrial crystallizer manufacturer implements advanced monitoring and control systems that ensure exceptional crystal quality and consistency. Real-time sensors measure solution temperature, concentration, and crystal size distribution, enabling automatic adjustments that optimize crystallization conditions. This precision eliminates batch variations and produces uniform, high-purity crystals that meet strict pharmaceutical, chemical, and food industry standards. The technology significantly reduces defective products and rework requirements, directly improving your manufacturing efficiency. By maintaining optimal crystallization parameters, the industrial crystallizer manufacturer's equipment guarantees reproducible results, essential for regulated industries where quality consistency determines market competitiveness and regulatory compliance success.
Energy-Efficient Innovation and Sustainability

Energy-Efficient Innovation and Sustainability

Modern industrial crystallizer manufacturer technology incorporates energy-saving innovations that substantially reduce operational expenses while supporting environmental responsibility. Advanced heat recovery systems, efficient cooling mechanisms, and intelligent temperature management minimize power consumption without compromising crystallization performance. These systems often reduce energy usage by thirty to forty percent compared to conventional equipment. An industrial crystallizer manufacturer focuses on sustainability by designing equipment that decreases carbon footprint and operational costs simultaneously. Lower energy requirements translate directly to reduced facility expenses, improved profit margins, and enhanced corporate sustainability credentials. This combination of economic and environmental benefits makes modern crystallizers attractive investments for companies pursuing cost optimization and environmental stewardship goals.
Comprehensive Customization and Technical Support

Comprehensive Customization and Technical Support

An industrial crystallizer manufacturer provides tailored solutions specifically engineered for your production requirements, material characteristics, and operational constraints. Rather than purchasing standardized equipment, the manufacturer designs systems addressing your unique challenges and objectives. This customization includes selecting appropriate crystallizer types, sizing components for your production volume, and integrating specialized features for specific substances. Beyond equipment delivery, an industrial crystallizer manufacturer offers extensive technical support, including installation assistance, operator training, maintenance protocols, and troubleshooting services. This comprehensive support ensures smooth operation, maximizes equipment lifespan, and enables your team to achieve optimal performance. Long-term partnerships with manufacturers provide valuable expertise and rapid problem-solving capabilities essential for maintaining production continuity.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000