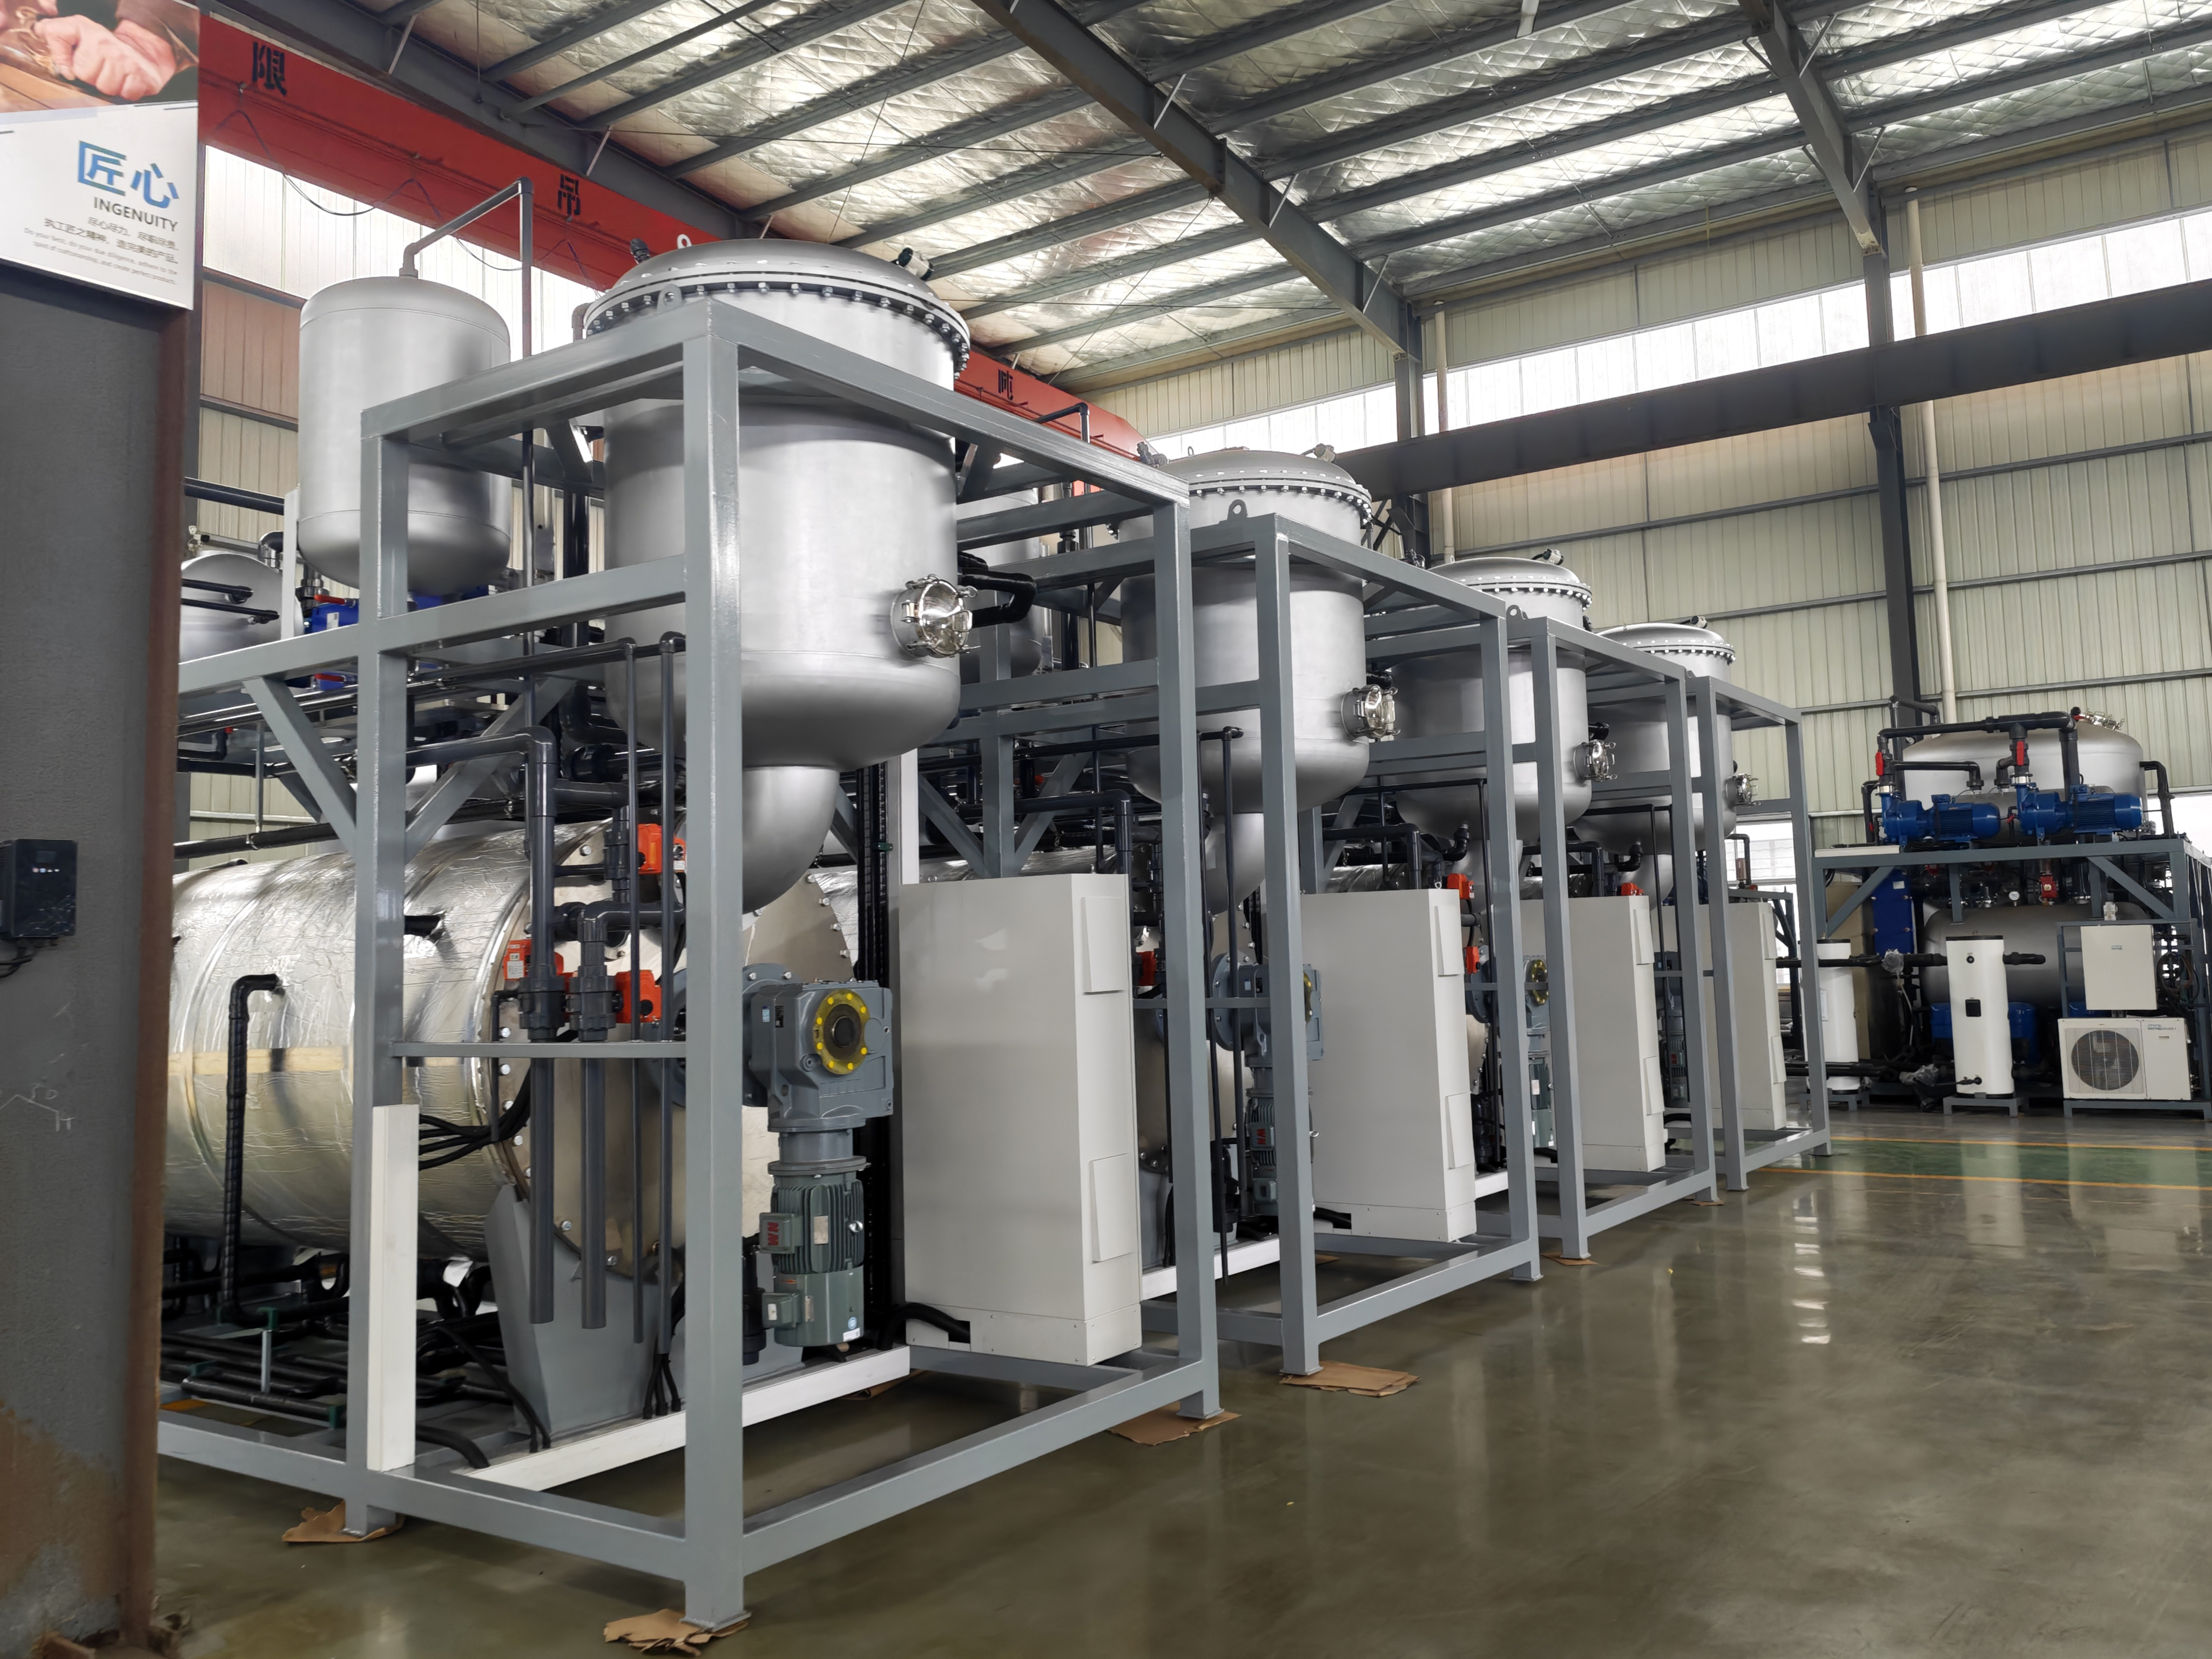
Low Temperature Evaporation Equipment

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

low temperature evaporation equipment

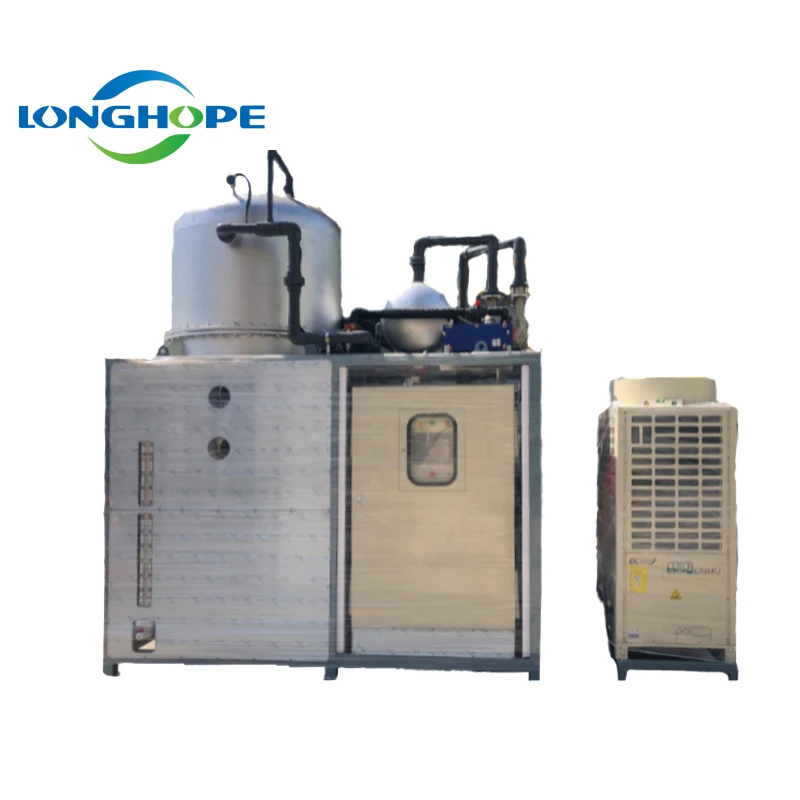
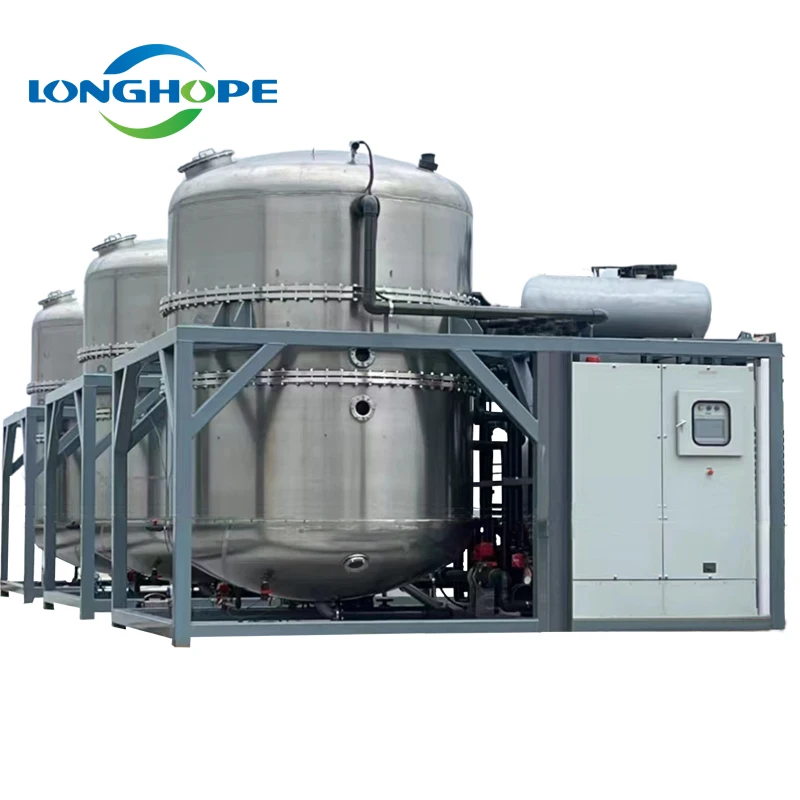
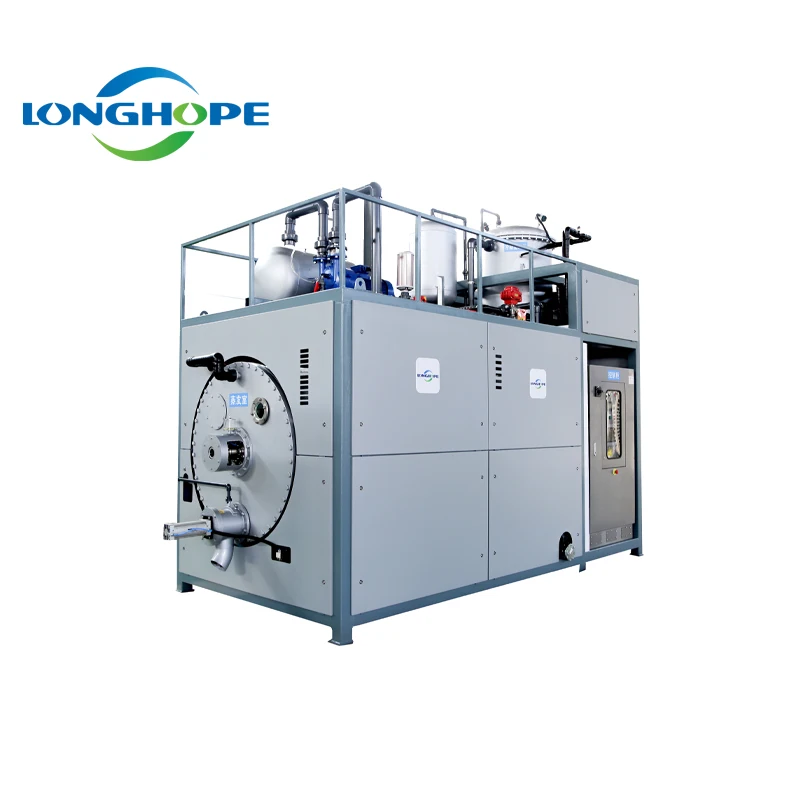
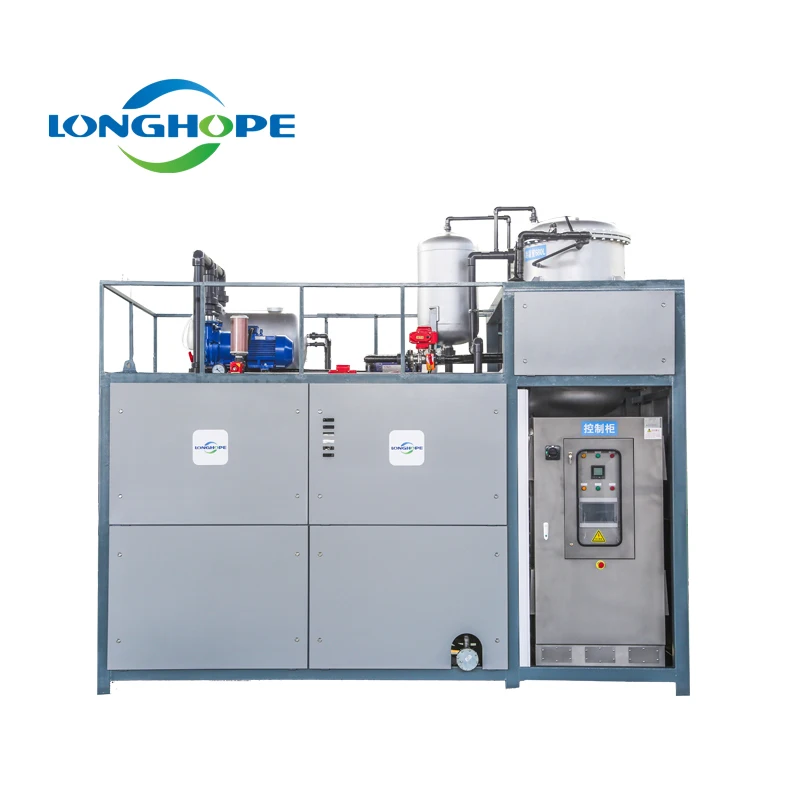
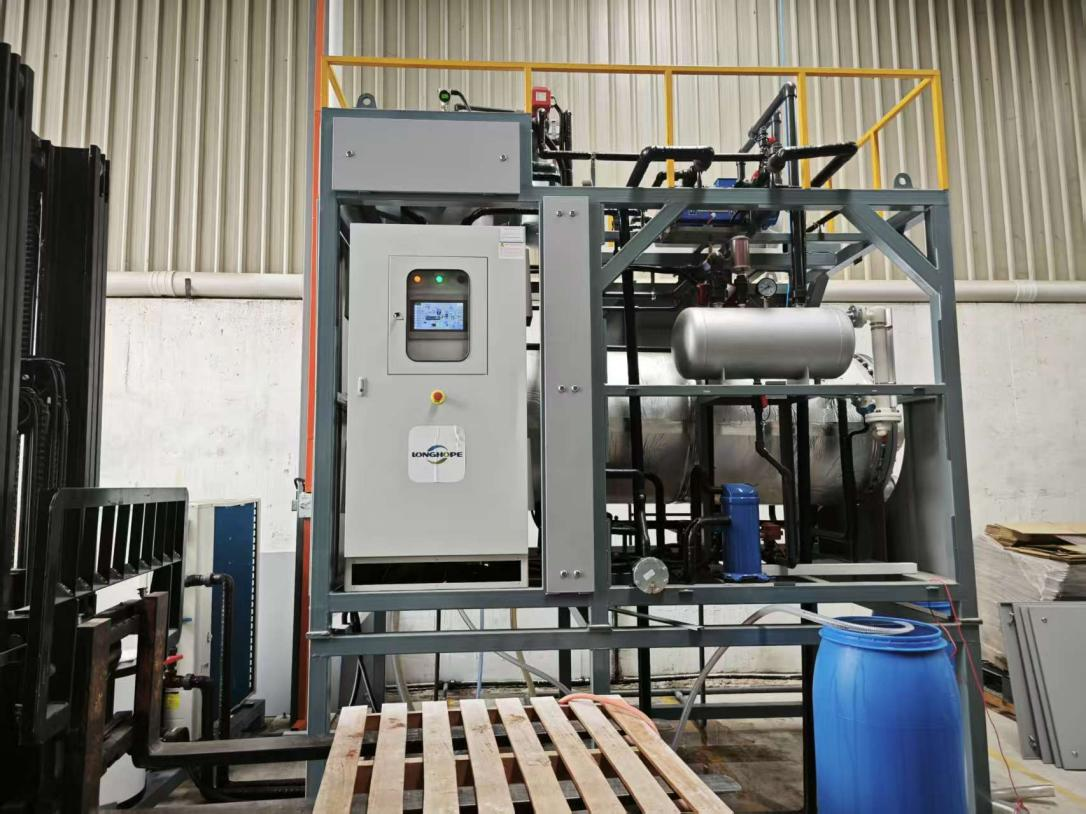
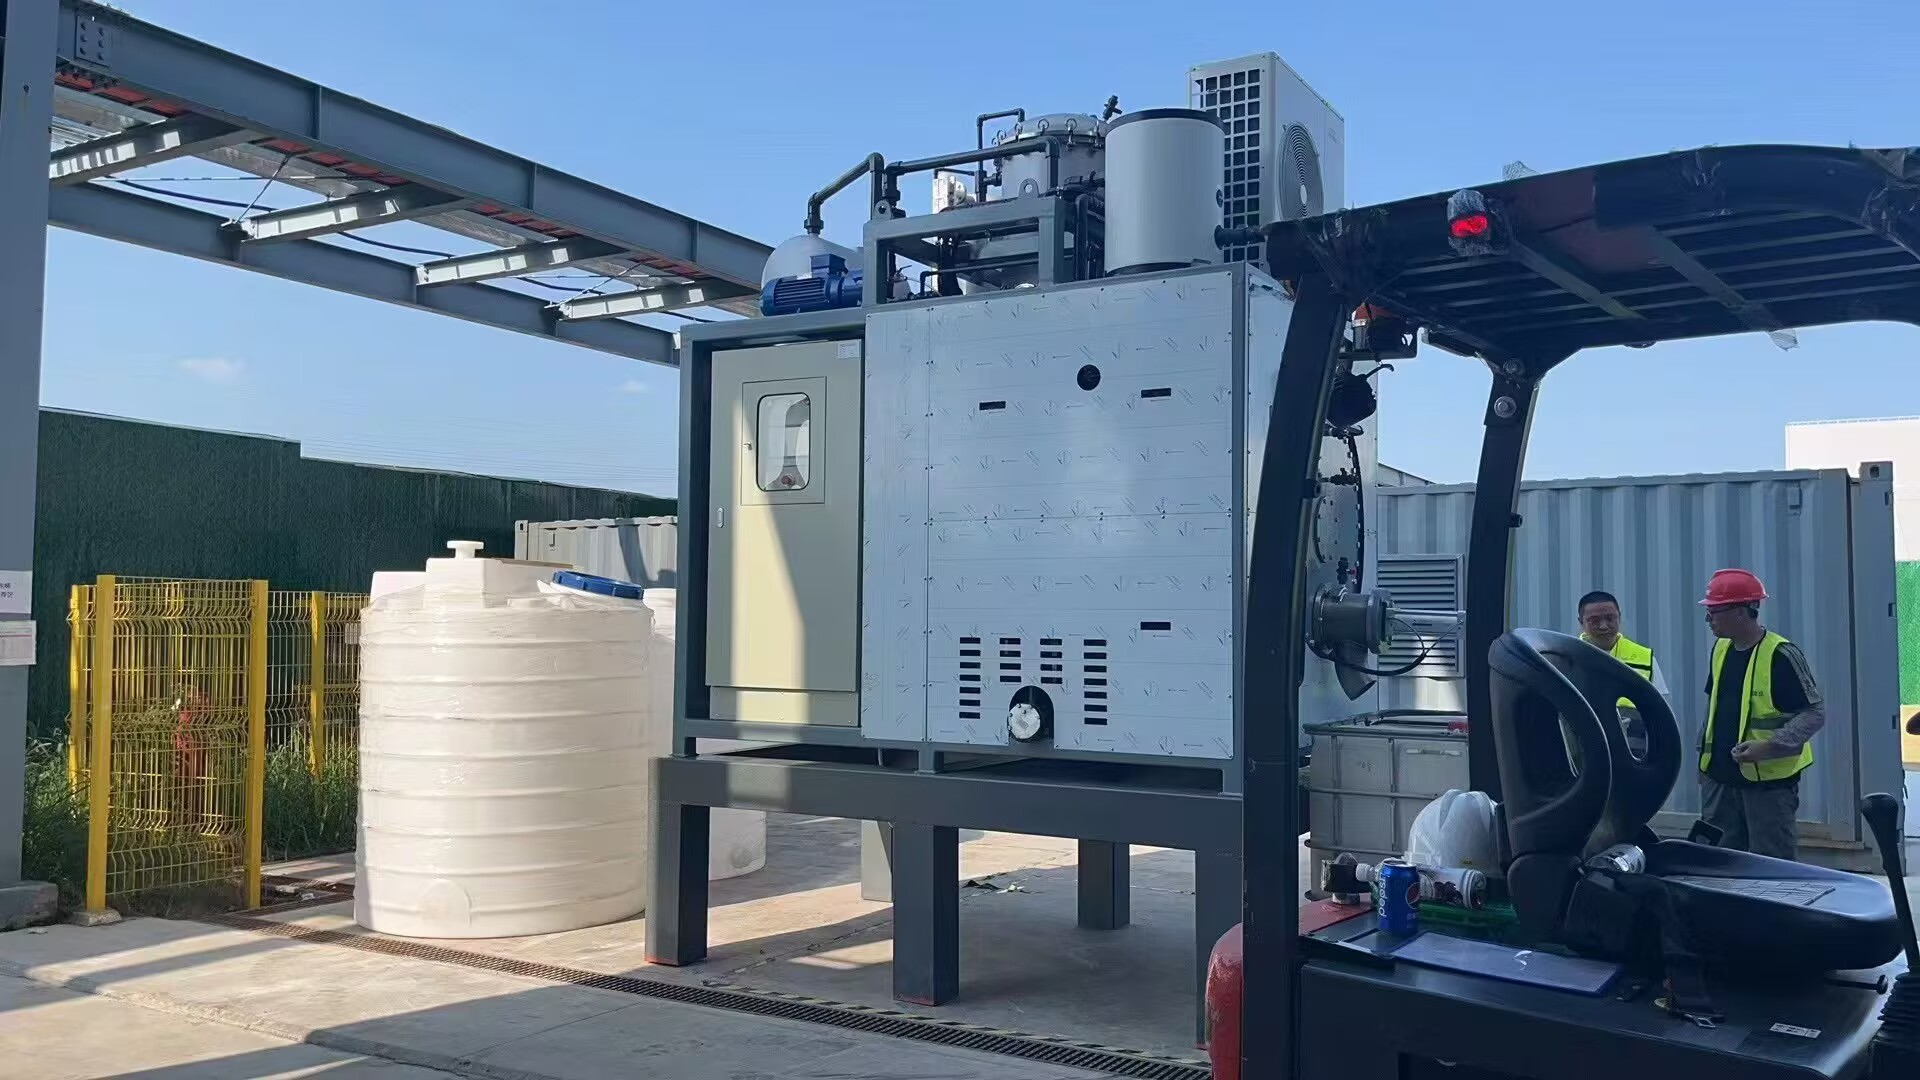
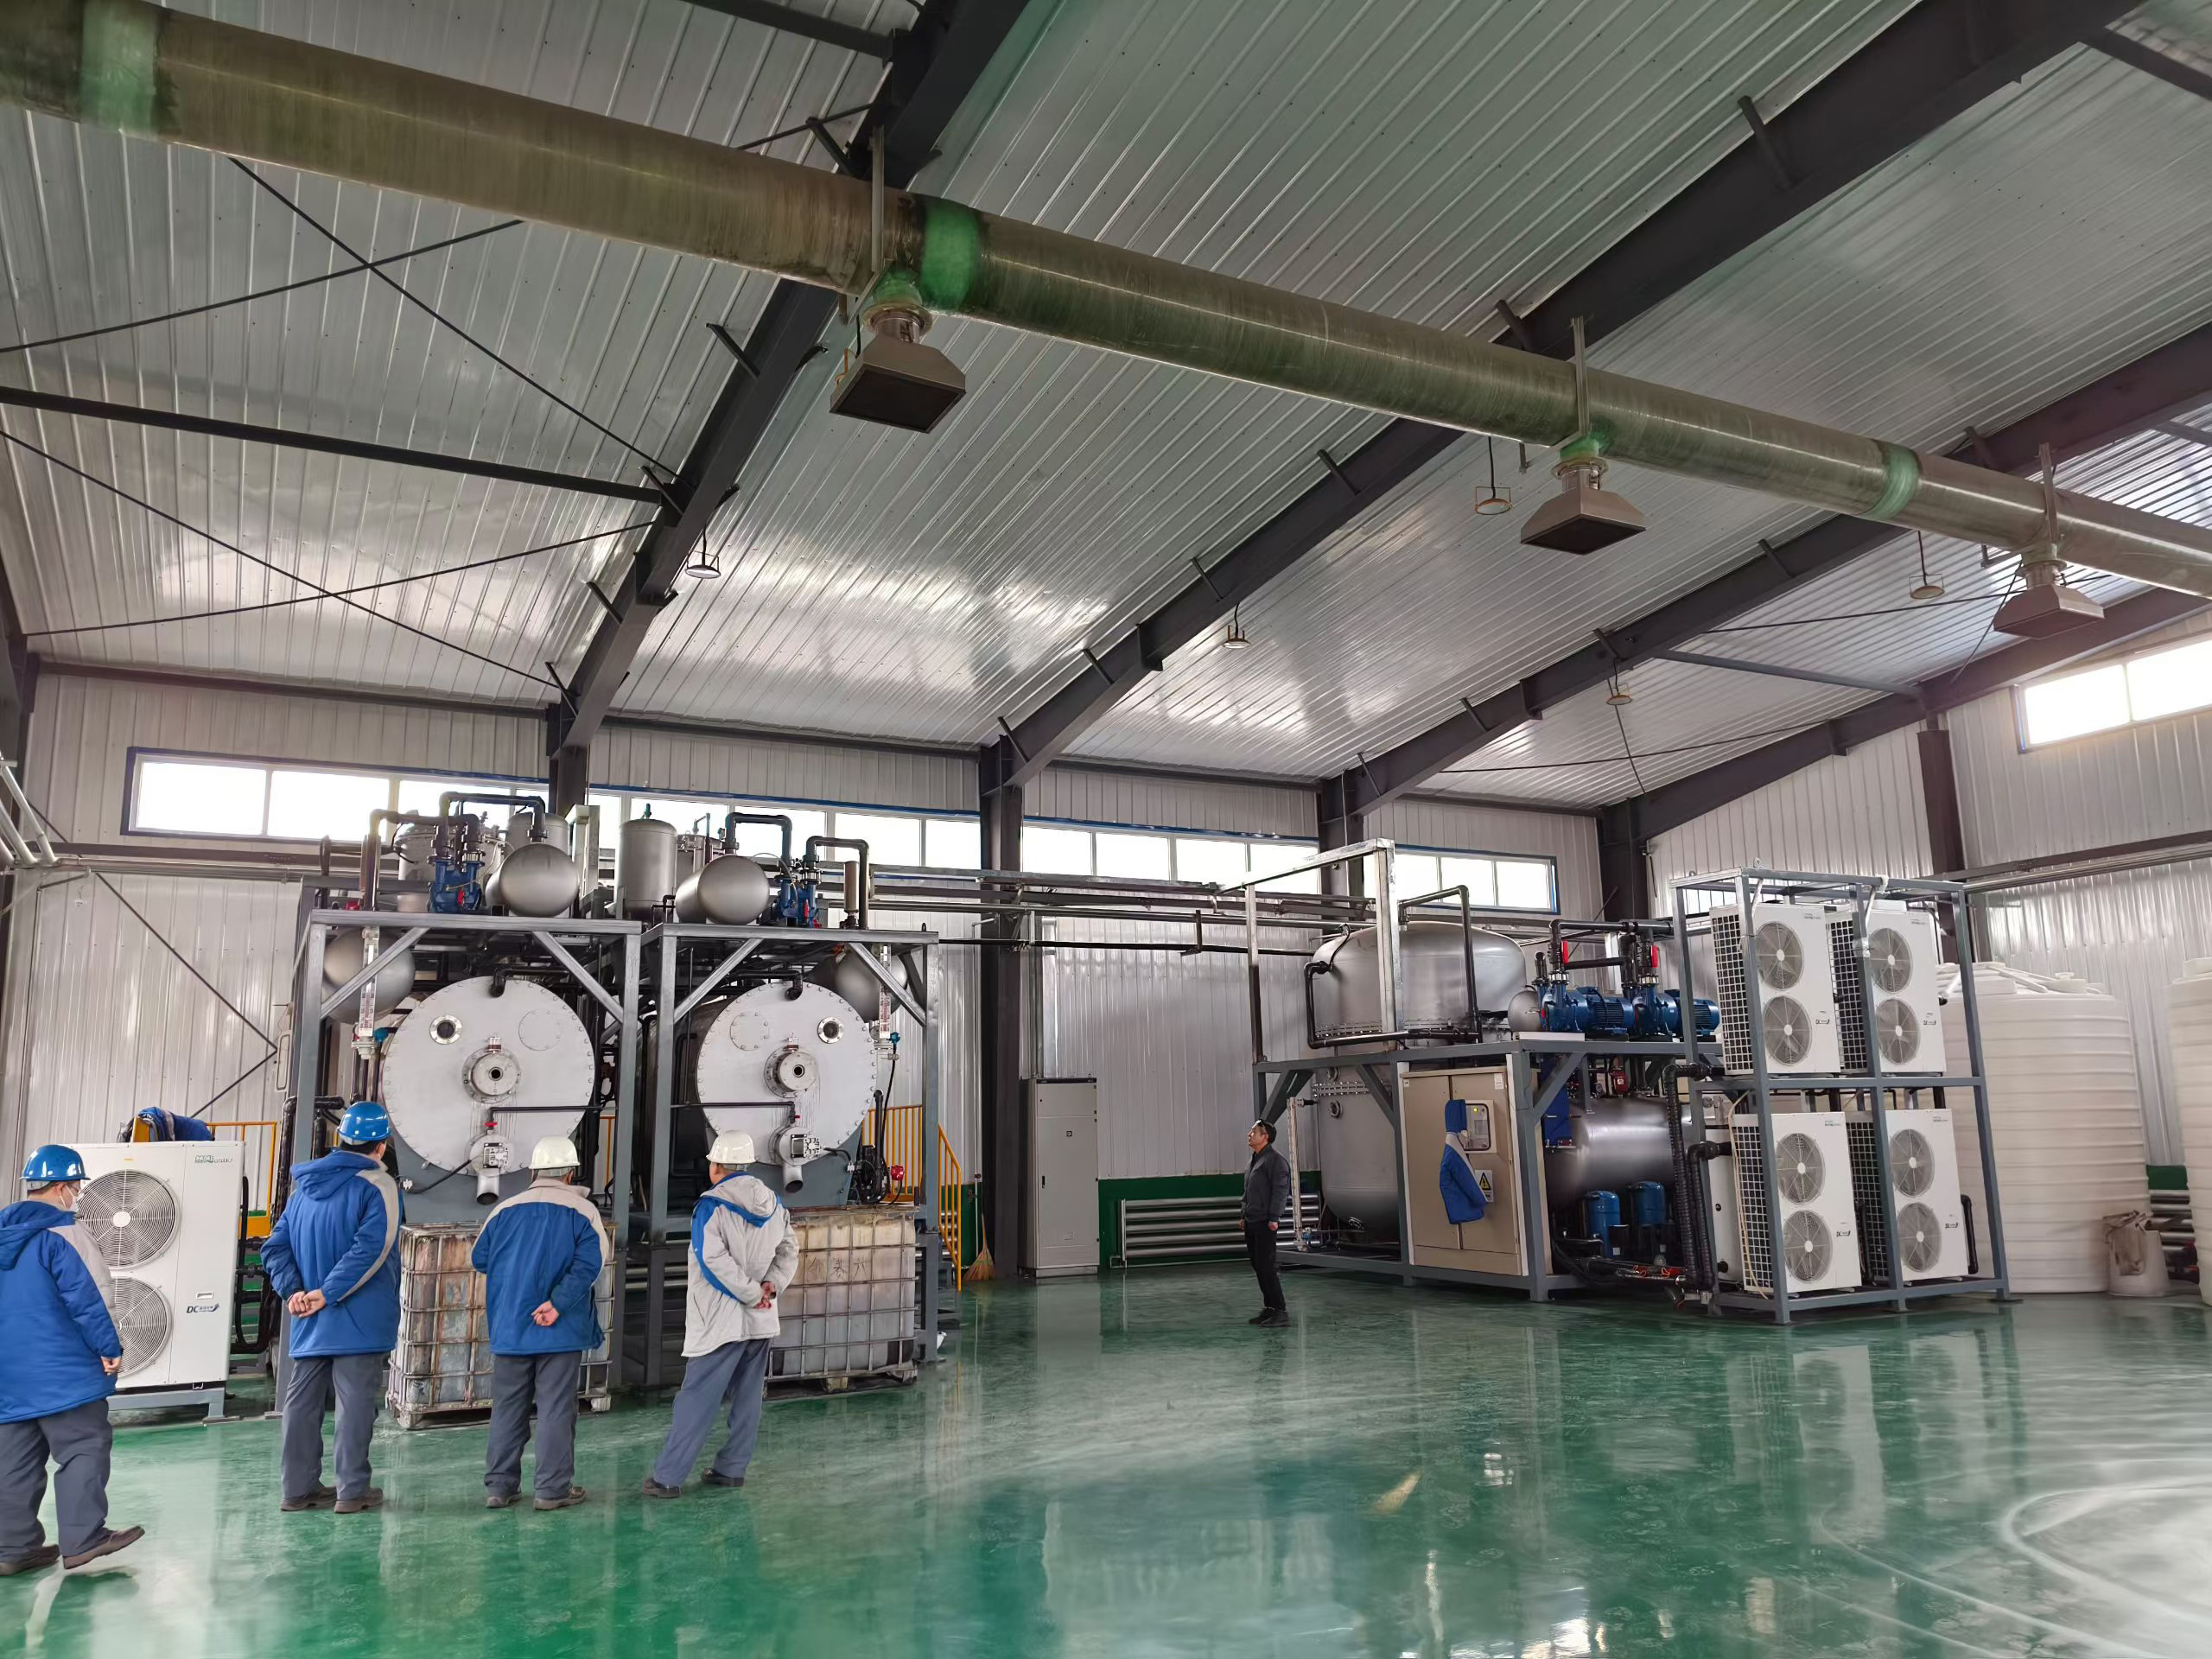
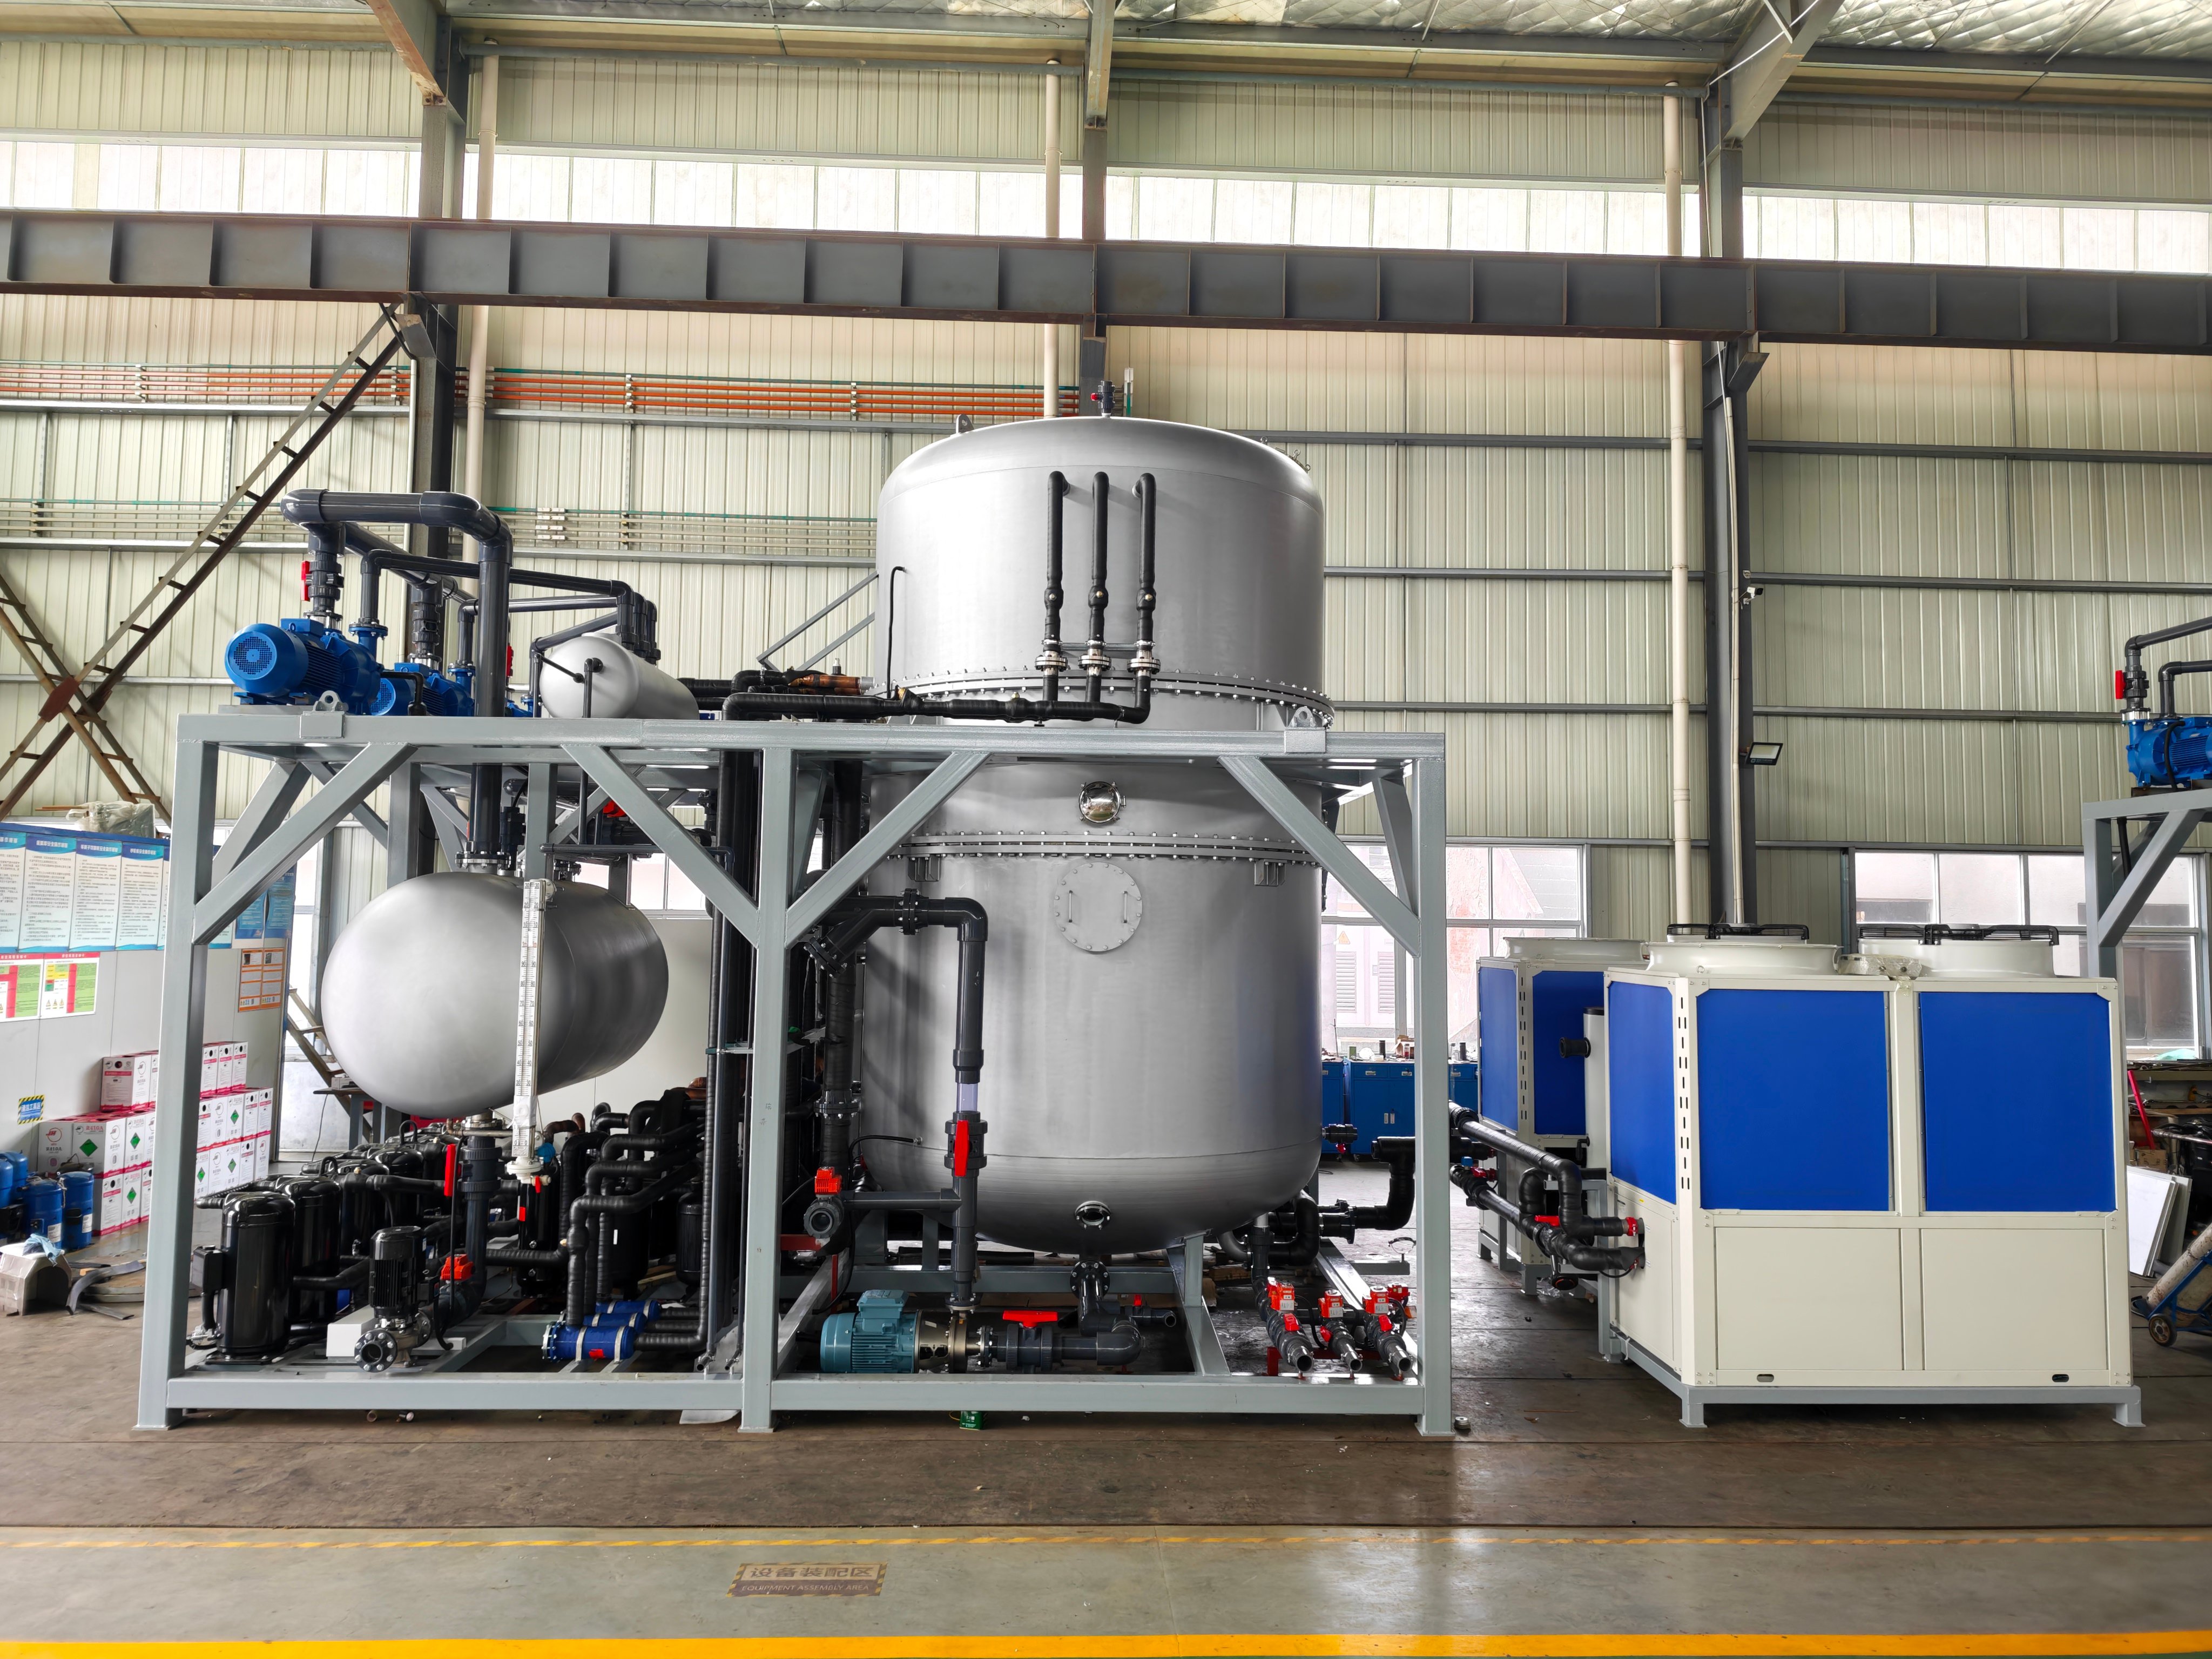
Low temperature evaporation equipment represents an advanced technological solution designed to handle volatile and heat-sensitive materials with precision and efficiency. This specialized machinery operates at significantly reduced temperatures, making it ideal for processing compounds that would degrade or decompose under conventional heating methods. Low temperature evaporation equipment utilizes innovative cooling and vacuum systems to achieve optimal evaporation rates while preserving product integrity and quality. The primary function of low temperature evaporation equipment involves separating liquid components from solids through controlled evaporation processes conducted at temperatures far below traditional evaporation methods. This technique proves particularly valuable in pharmaceutical, chemical, food processing, and biotechnology industries where maintaining compound stability is critical. The equipment operates by reducing atmospheric pressure within the chamber, which lowers the boiling point of liquids and enables efficient separation at gentle temperatures. Key technological features of low temperature evaporation equipment include advanced vacuum control systems, precision temperature regulation, rotary or wiped film designs, and automated monitoring capabilities. These components work synergistically to create an environment where delicate materials undergo evaporation without thermal damage. Modern low temperature evaporation equipment incorporates energy-efficient designs that reduce operational costs while maintaining superior performance standards. Applications span multiple industries including pharmaceutical manufacturing, herbal extraction, cannabis processing, essential oil refinement, and specialty chemical production. Organizations utilize low temperature evaporation equipment to concentrate valuable compounds, remove solvents safely, and achieve product purification objectives that conventional methods cannot accomplish reliably.

New Products

Low temperature evaporation equipment delivers substantial practical benefits that directly address the needs of businesses handling heat-sensitive materials. The most significant advantage involves product preservation, as the gentle processing conditions protect valuable compounds from thermal degradation, maintaining their chemical integrity and market value. Companies implementing low temperature evaporation equipment experience improved product quality metrics and reduced material loss throughout production cycles. Operational efficiency represents another compelling benefit of low temperature evaporation equipment. The advanced vacuum systems reduce processing times substantially compared to traditional evaporation methods, translating to faster production cycles and increased throughput capacity. This accelerated processing capability enables businesses to meet demanding production schedules without compromising quality standards. Energy efficiency distinguishes modern low temperature evaporation equipment from conventional alternatives. By operating at lower temperatures and utilizing sophisticated heat recovery systems, this equipment consumes significantly less energy per production batch. Organizations observe measurable reductions in utility costs while simultaneously decreasing their environmental footprint through lower energy consumption. Safety improvements emerge as another vital operational advantage. Low temperature evaporation equipment minimizes volatile organic compound emissions and reduces explosion risks associated with handling flammable solvents at elevated temperatures. Enhanced safety features protect both equipment and personnel while meeting increasingly stringent environmental regulations. The versatility of low temperature evaporation equipment allows processing diverse material types without equipment modifications. Businesses can transition between different compounds and applications flexibly, maximizing return on investment. This adaptability proves invaluable for manufacturers serving multiple market segments or developing new product formulations requiring specialized processing capabilities.

Latest News

Top 5 Vacuum Distillation Applications in Industry

24

Jul

Top 5 Vacuum Distillation Applications in Industry

Vacuum distillation applications have become essential across multiple industrial sectors, transforming how manufacturers separate, purify, and concentrate valuable materials. By operating below atmospheric pressure, vacuum distillation applications ...
View More
How to Optimize Your Evaporator System for Efficiency

24

Jul

How to Optimize Your Evaporator System for Efficiency

An evaporator system efficiency directly impacts your operational costs, production capacity, and environmental footprint in industrial processing. Whether you operate in chemical manufacturing, food processing, pharmaceutical production, or waste ma...
View More
Common Challenges in Industrial Water Treatment Solved

02

Sep

Common Challenges in Industrial Water Treatment Solved

Manufacturing facilities, chemical plants, and processing operations face mounting pressure to manage wastewater efficiently while meeting regulatory standards. Industrial water treatment remains one of the most critical operational functions across ...
View More
Low Temperature Heat Pump Evaporator: Energy Saving Guide

24

Jul

Low Temperature Heat Pump Evaporator: Energy Saving Guide

Industrial facilities continuously seek ways to reduce operational costs while maintaining peak performance. A low temperature heat pump evaporator represents one of the most effective technologies for achieving significant energy savings in thermal ...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

low temperature evaporation equipment

Advanced Vacuum Technology for Optimal Performance

Advanced Vacuum Technology for Optimal Performance

Low temperature evaporation equipment incorporates cutting-edge vacuum technology that enables precise control over chamber pressure and evaporation rates. This sophisticated system reduces atmospheric pressure within the processing chamber, effectively lowering the boiling points of target liquids and enabling efficient separation at temperatures significantly below conventional methods. The advanced vacuum technology maintains consistent pressure throughout extended production runs, ensuring uniform processing results and predictable output quality. Operators benefit from automated pressure monitoring systems that adjust vacuum levels in real-time, responding to material properties and processing requirements dynamically. This precision approach minimizes thermal stress on sensitive compounds while maximizing evaporation efficiency. Organizations using low temperature evaporation equipment with superior vacuum technology report enhanced product consistency, reduced batch-to-batch variations, and improved overall production reliability. The investment in quality vacuum systems ultimately protects valuable raw materials and maximizes profitability through superior product outcomes.
Precise Temperature Control Systems

Precise Temperature Control Systems

Low temperature evaporation equipment features precision temperature regulation mechanisms that maintain exact processing conditions throughout each cycle. These intelligent control systems utilize advanced sensors and feedback loops to keep material temperatures within narrowly defined parameters, preventing overheating and product degradation. The temperature precision available with modern low temperature evaporation equipment typically maintains variations within plus or minus one degree Celsius, ensuring reproducible results across multiple batches. Operators gain transparent visibility into temperature fluctuations through real-time monitoring displays and automated alerts that flag any deviations from target specifications. This level of control proves essential when processing pharmaceutical compounds, botanical extracts, or specialty chemicals where temperature sensitivity determines final product efficacy. Companies implementing low temperature evaporation equipment with superior temperature control experience significantly improved yield rates and enhanced product potency. The reliability of temperature management reduces waste materials and rework requirements, directly improving bottom-line profitability for processing operations.
Energy-Efficient Design Reducing Operating Costs

Energy-Efficient Design Reducing Operating Costs

Low temperature evaporation equipment incorporates energy-efficient design principles that substantially lower operational expenses without sacrificing performance or throughput capacity. The equipment utilizes optimized heat exchanger configurations and insulation systems that minimize energy waste during processing cycles. Modern low temperature evaporation equipment consumes considerably less electrical power and cooling resources compared to conventional evaporation methods, translating to measurable reductions in monthly utility bills. The efficient design of low temperature evaporation equipment also generates less waste heat, reducing facility cooling demands during peak production seasons. Many models incorporate variable-speed drive systems that automatically adjust motor speeds based on processing requirements, avoiding unnecessary power consumption during partial-load conditions. Organizations operating low temperature evaporation equipment consistently report energy savings of thirty to fifty percent compared to traditional evaporation equipment. These sustained cost reductions significantly improve profit margins while supporting corporate sustainability objectives and environmental responsibility commitments. The investment in energy-efficient low temperature evaporation equipment typically achieves full payback within two to three years through operational savings alone.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000