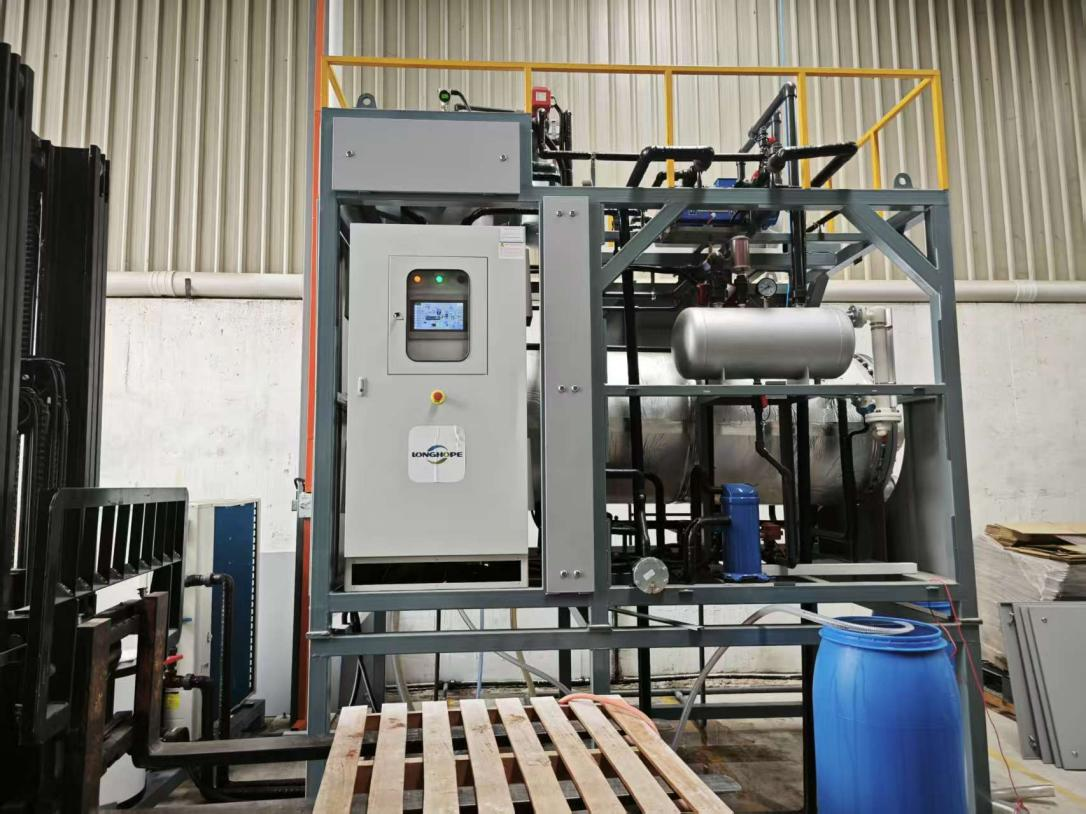
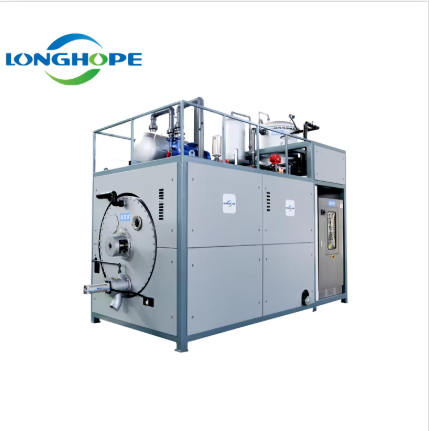
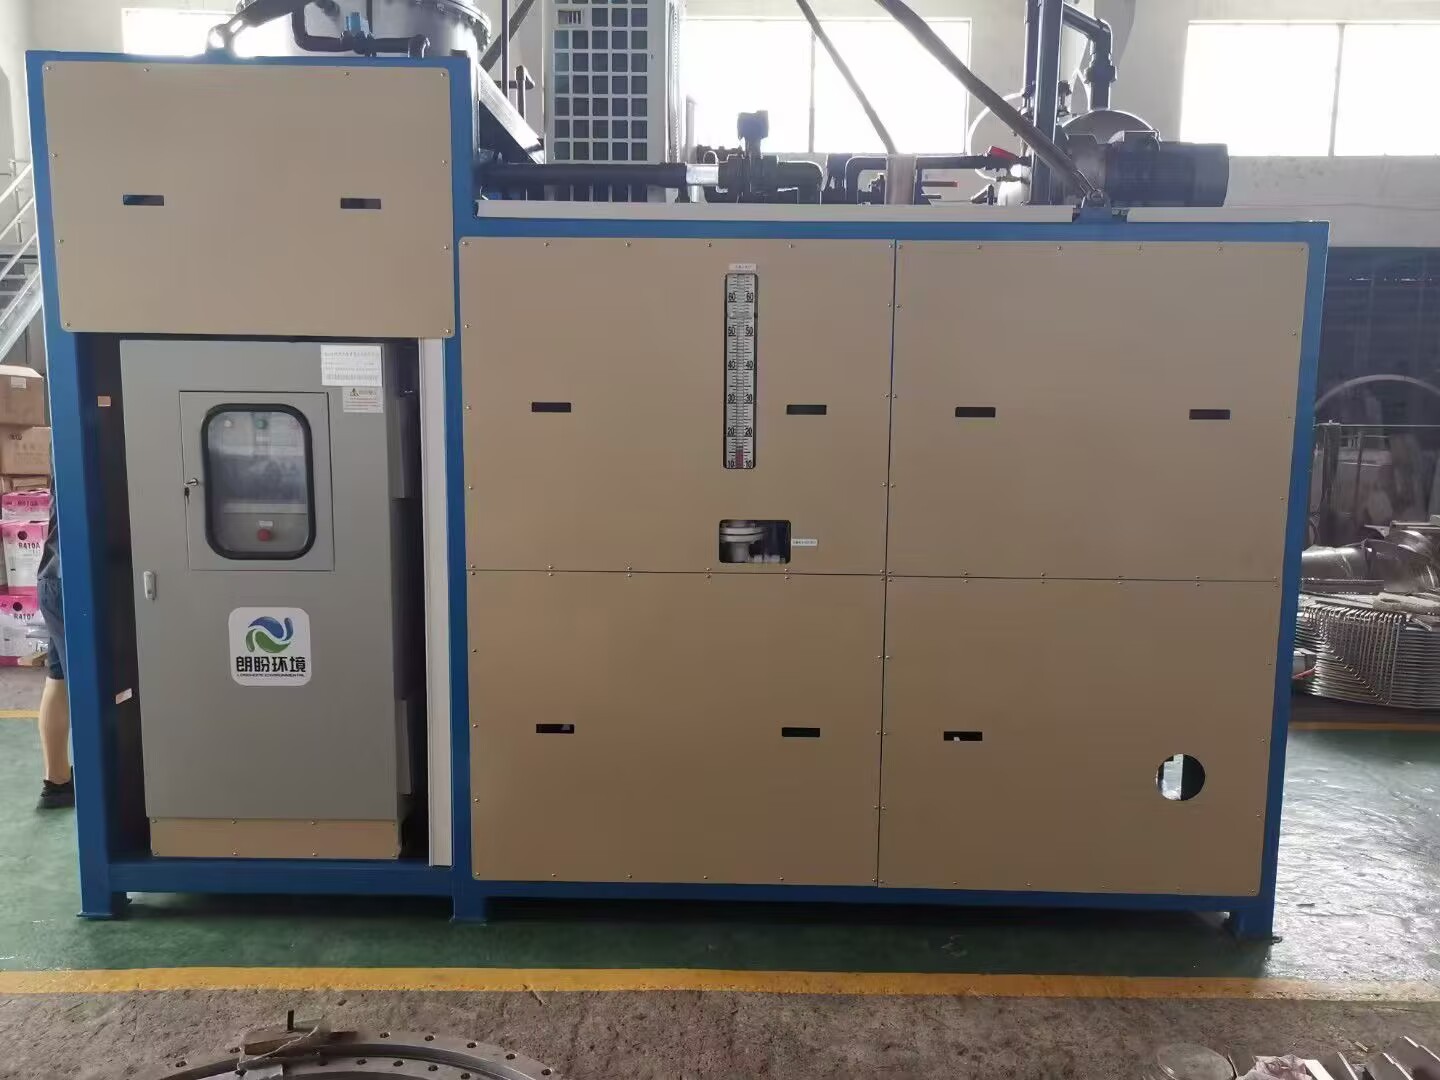
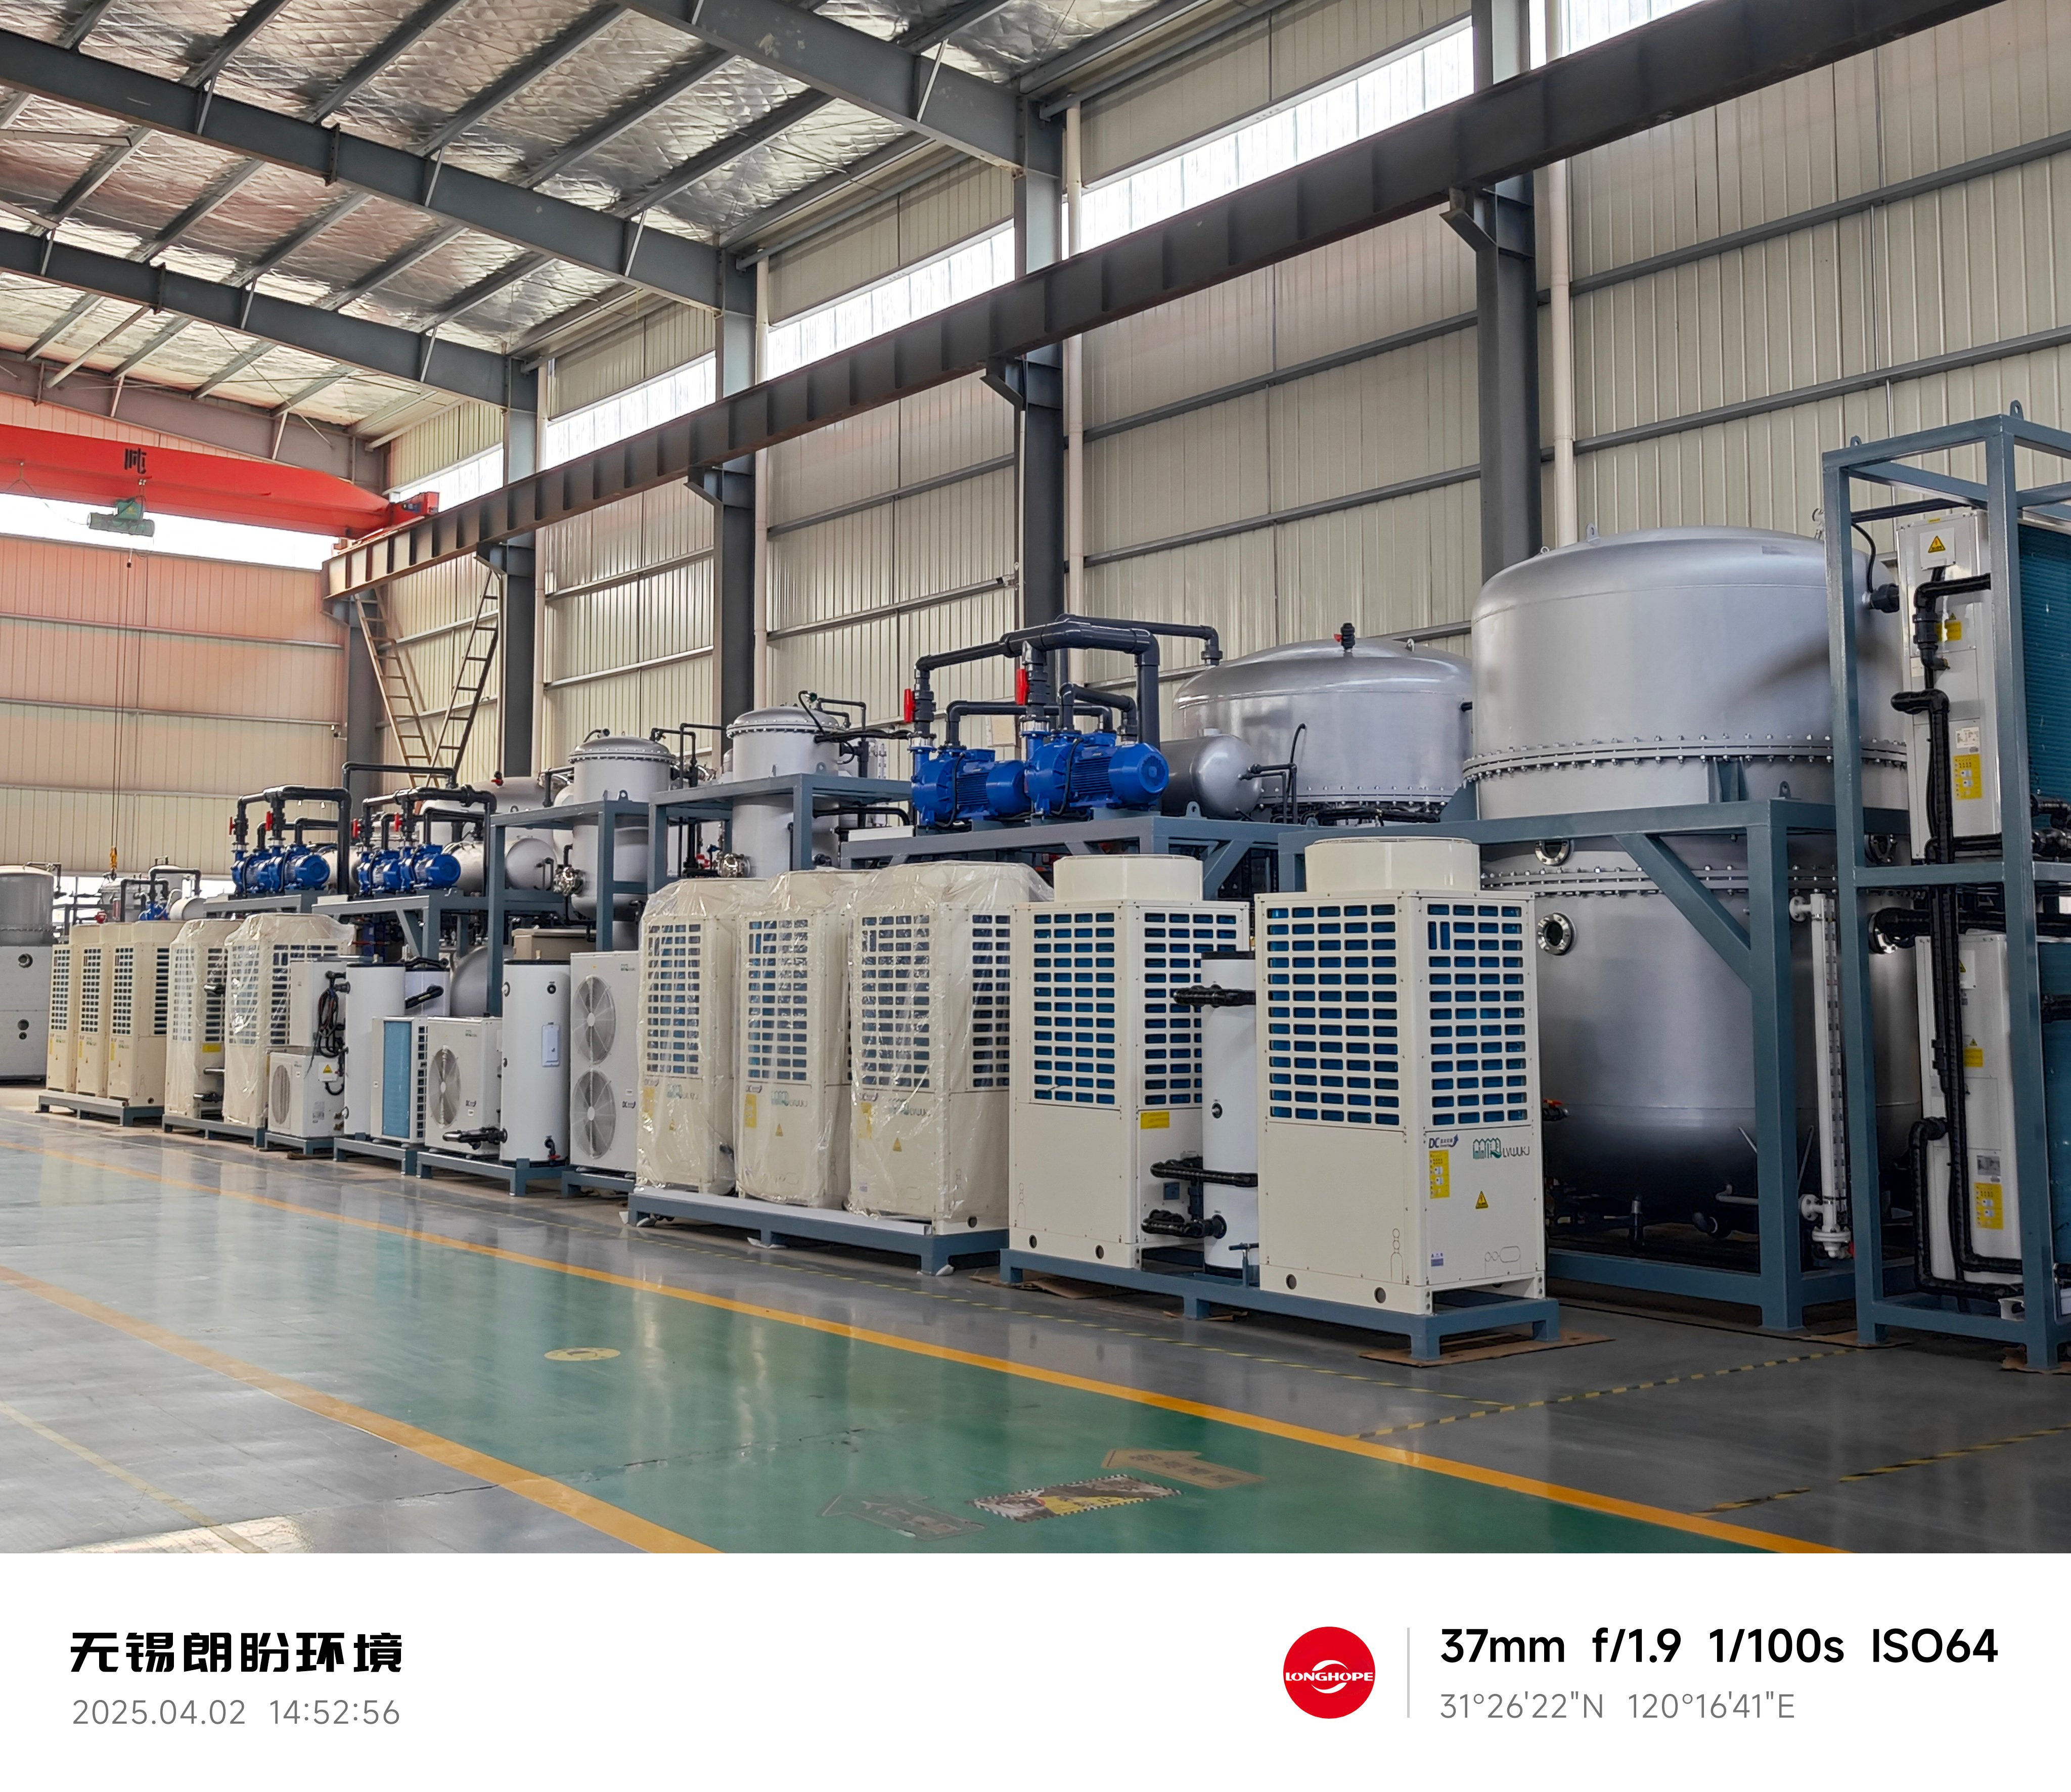
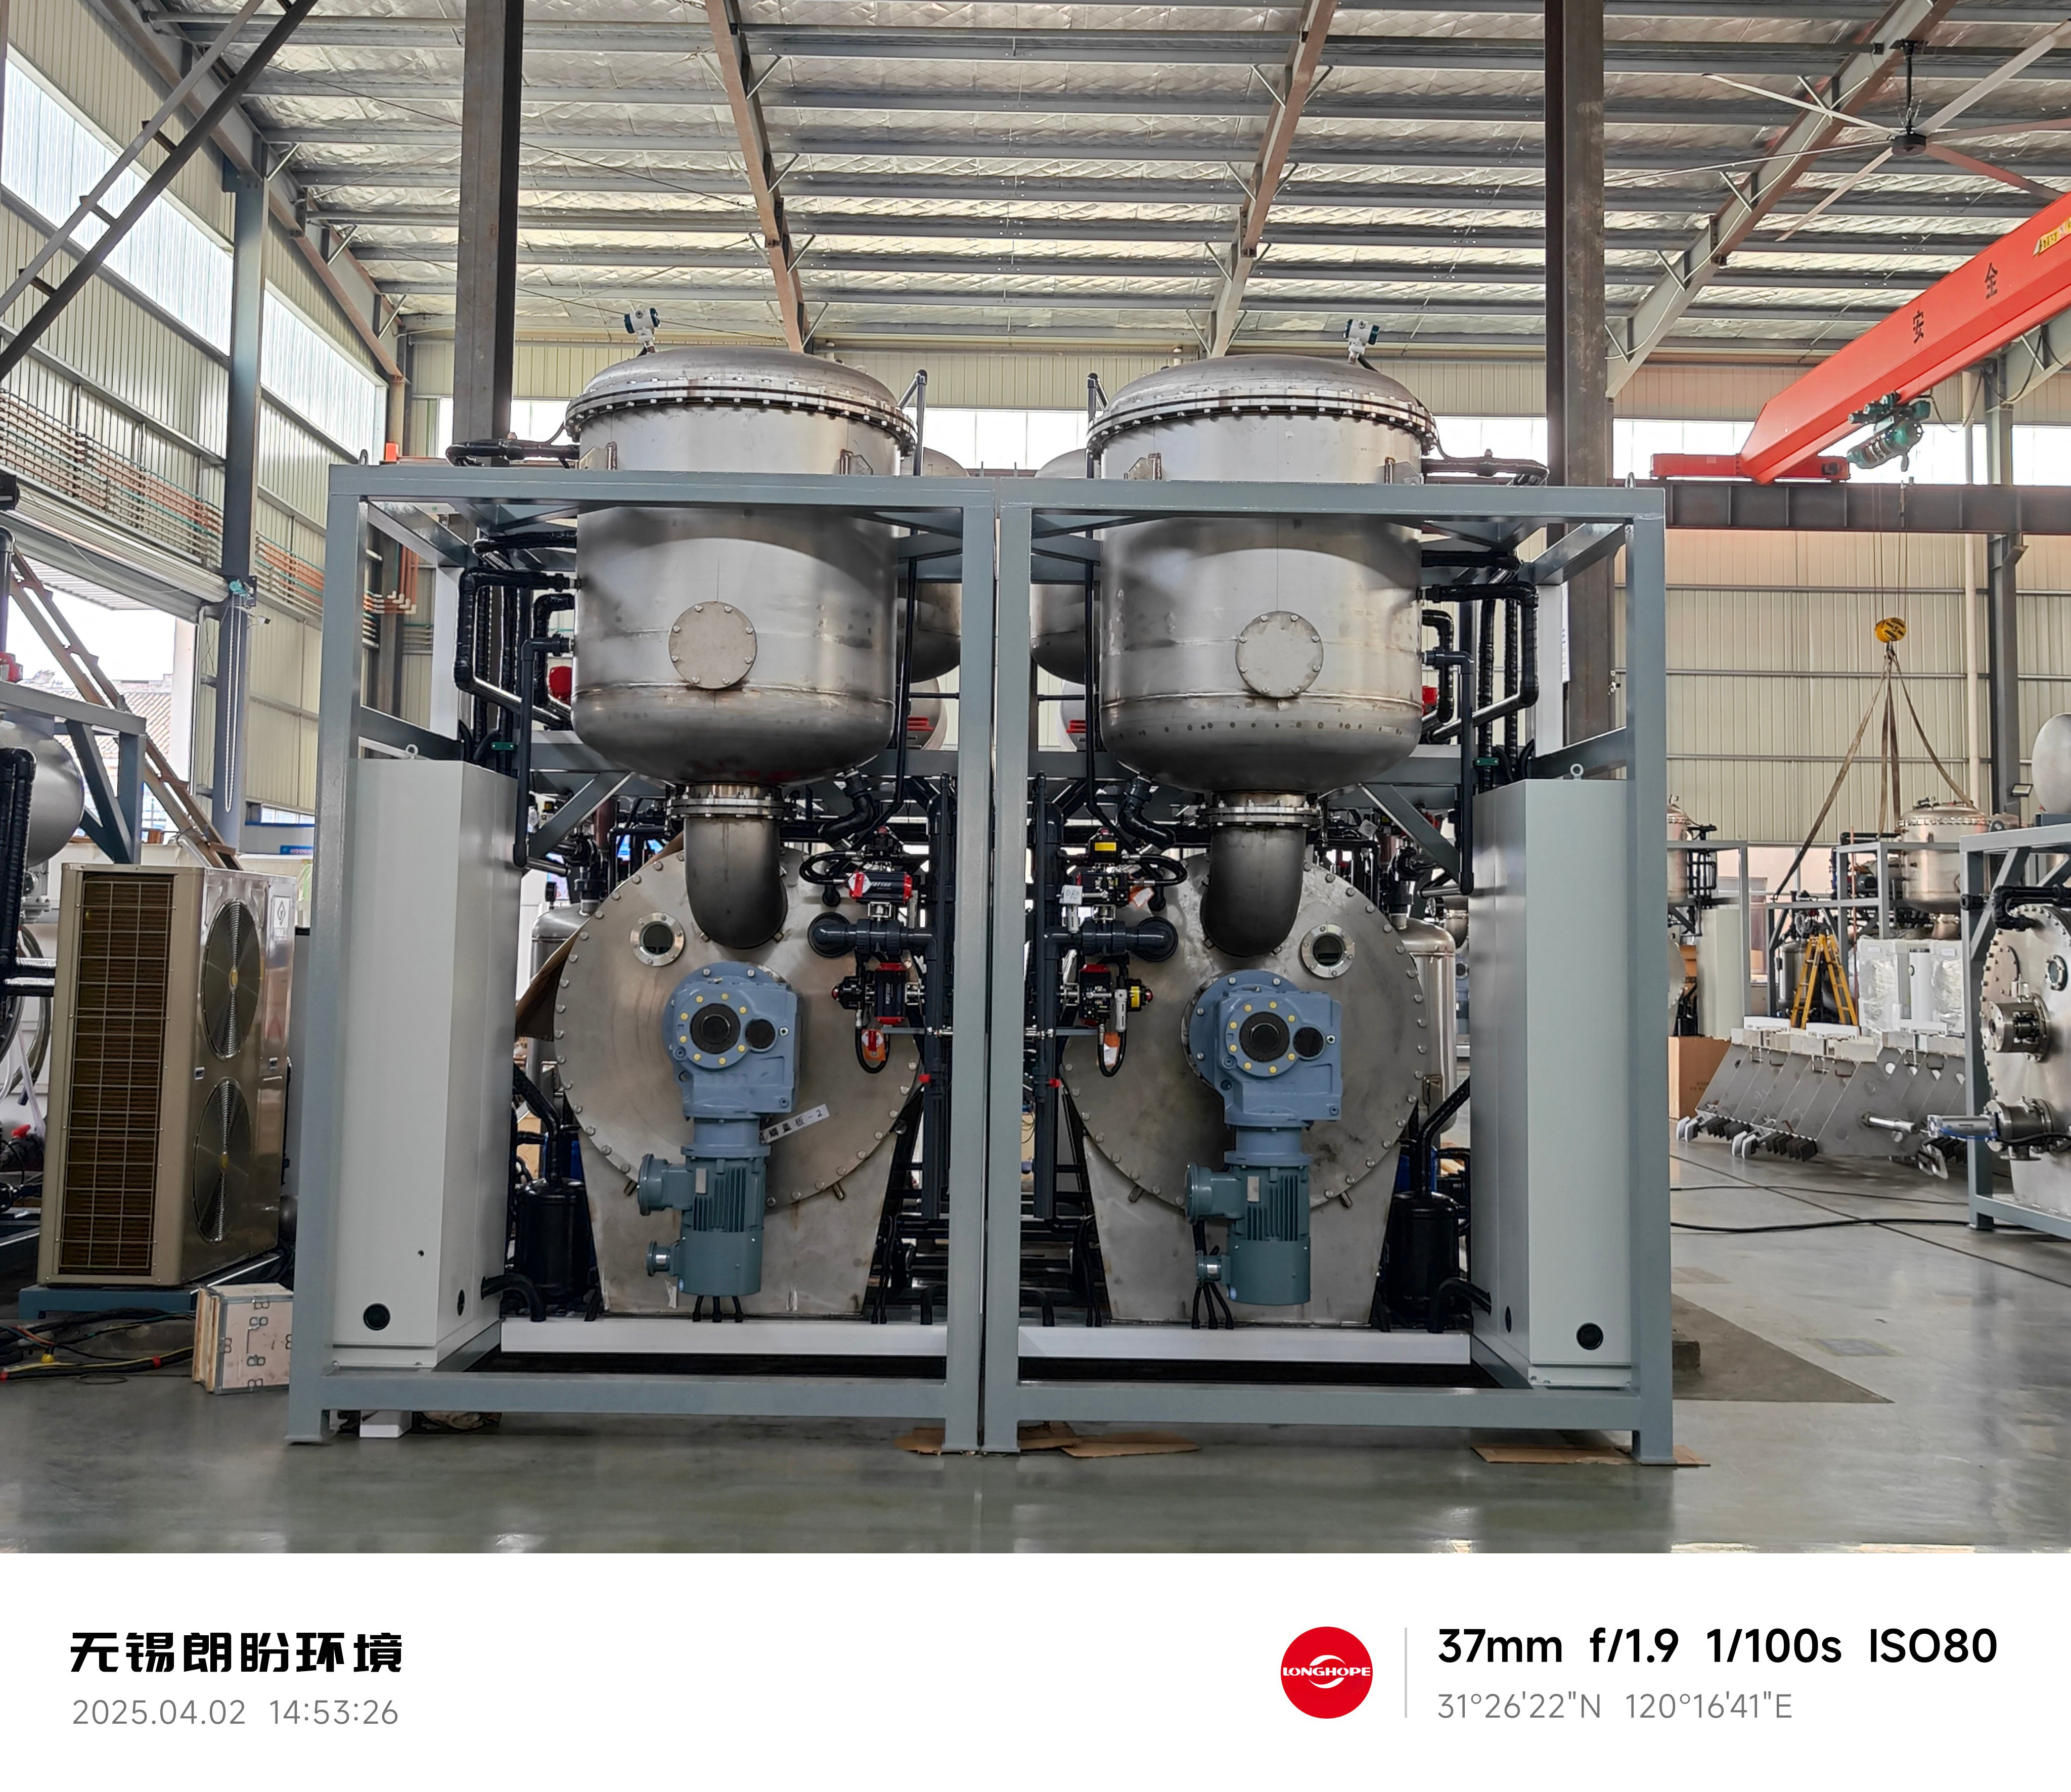
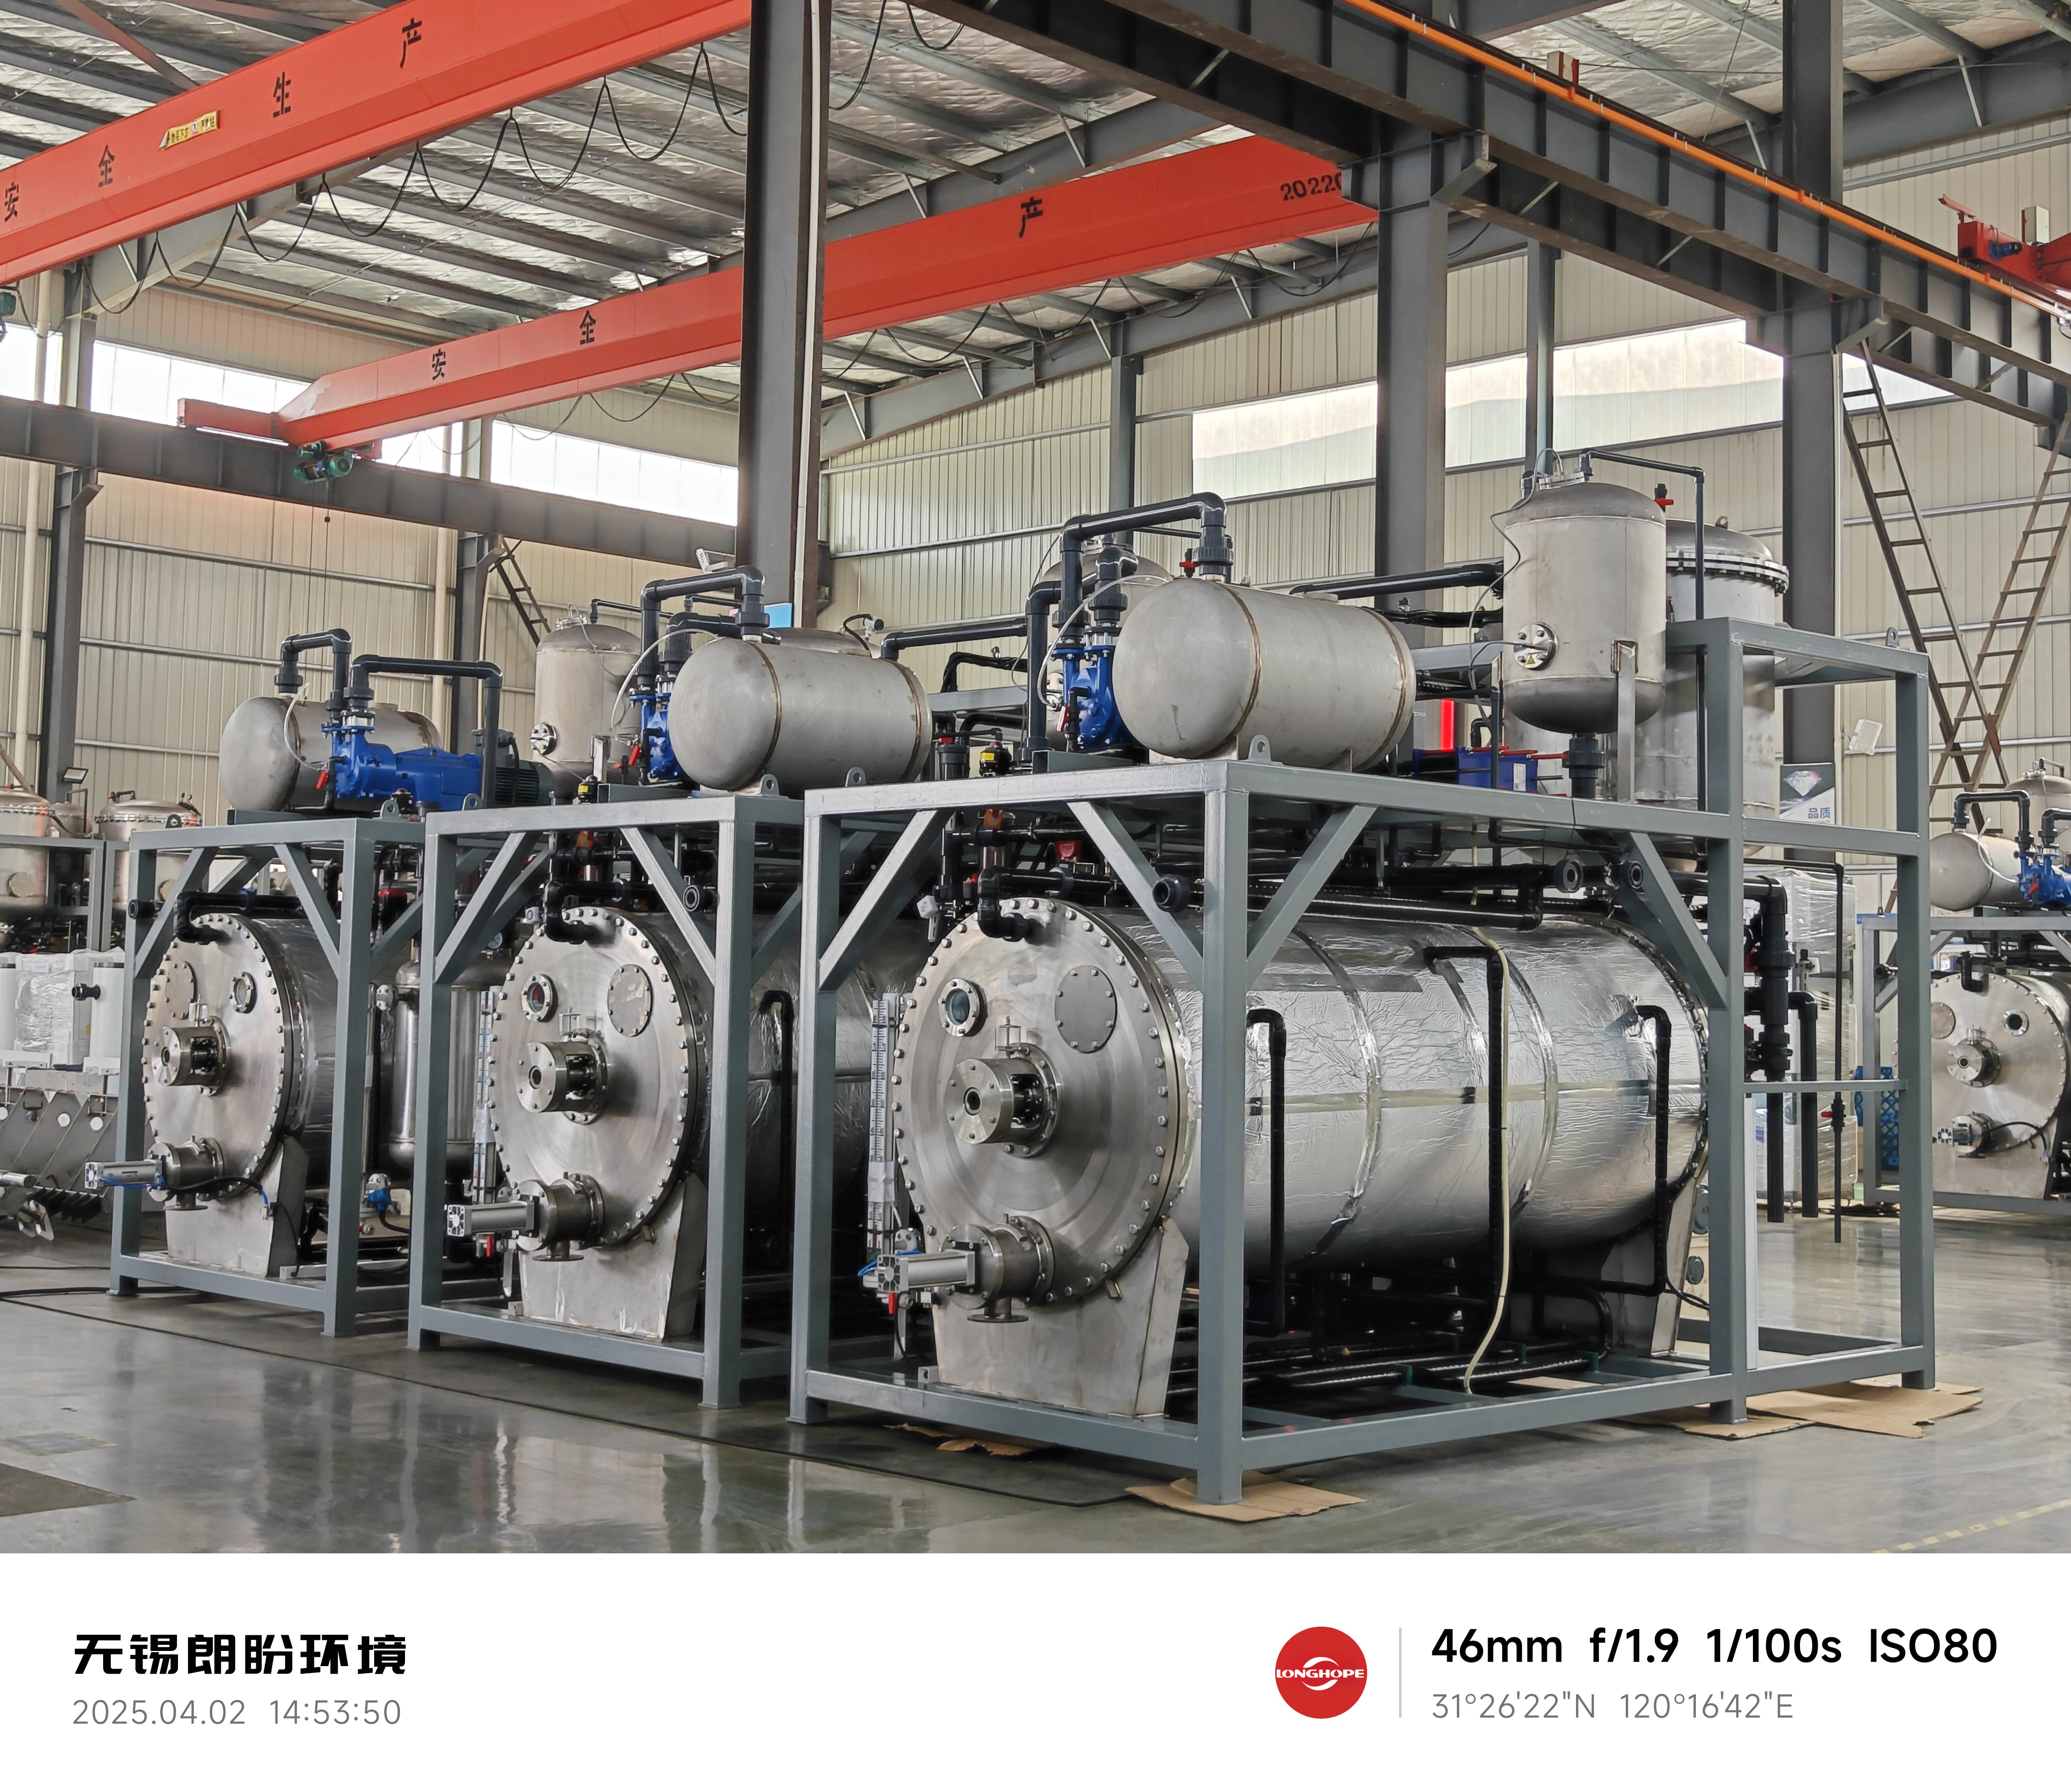
water treatment for industrial use
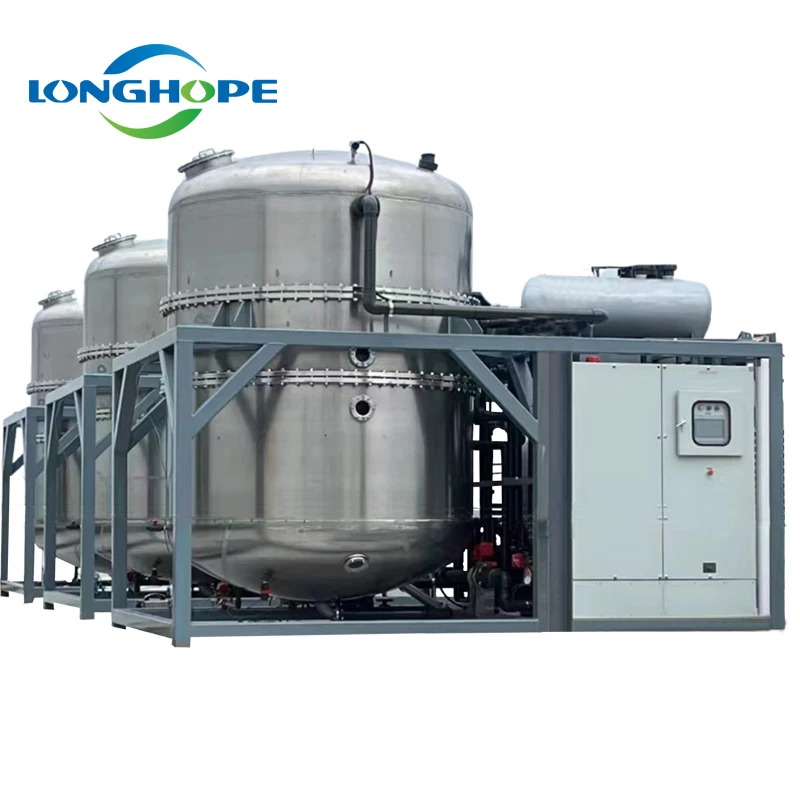
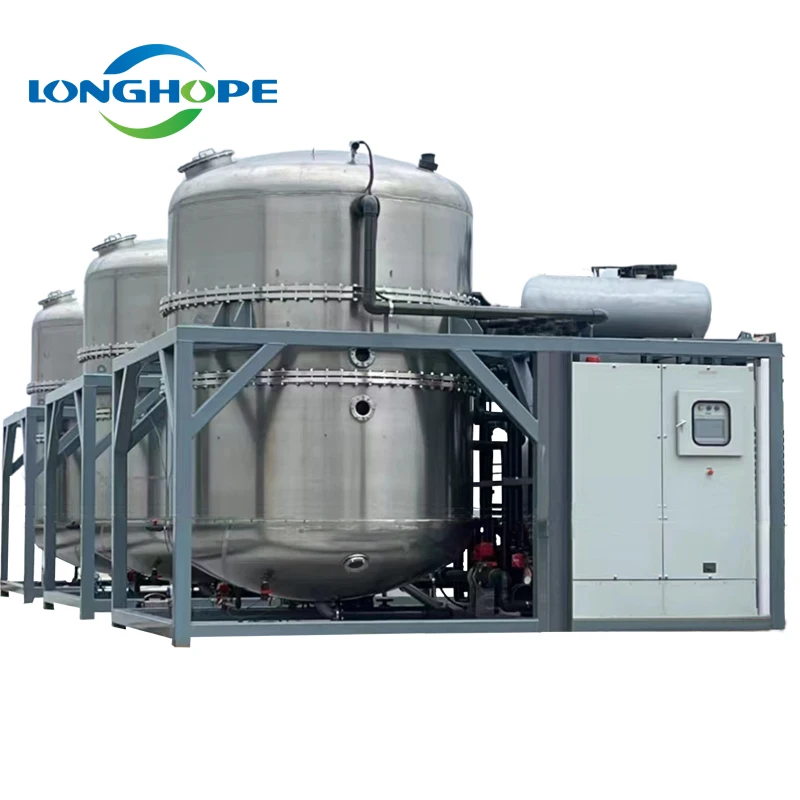
Water treatment for industrial use represents a critical process that purifies water for manufacturing, processing, and operational needs across diverse industries. This specialized water treatment for industrial use removes contaminants, suspended solids, chemicals, and microorganisms that could compromise product quality or equipment performance. Industrial facilities depend on water treatment for industrial use to meet stringent regulatory standards while maintaining efficient production cycles.
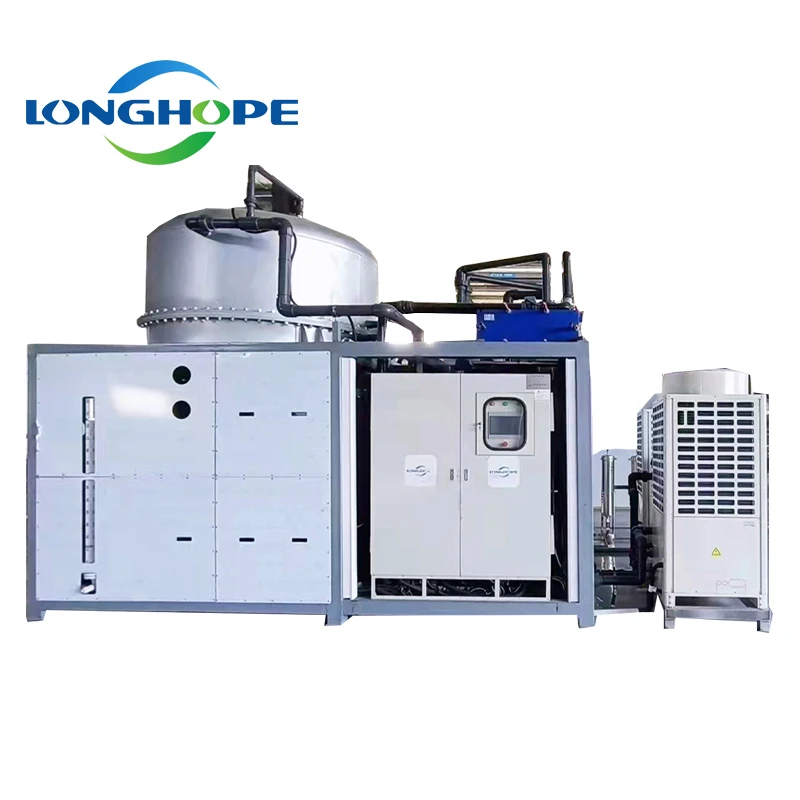
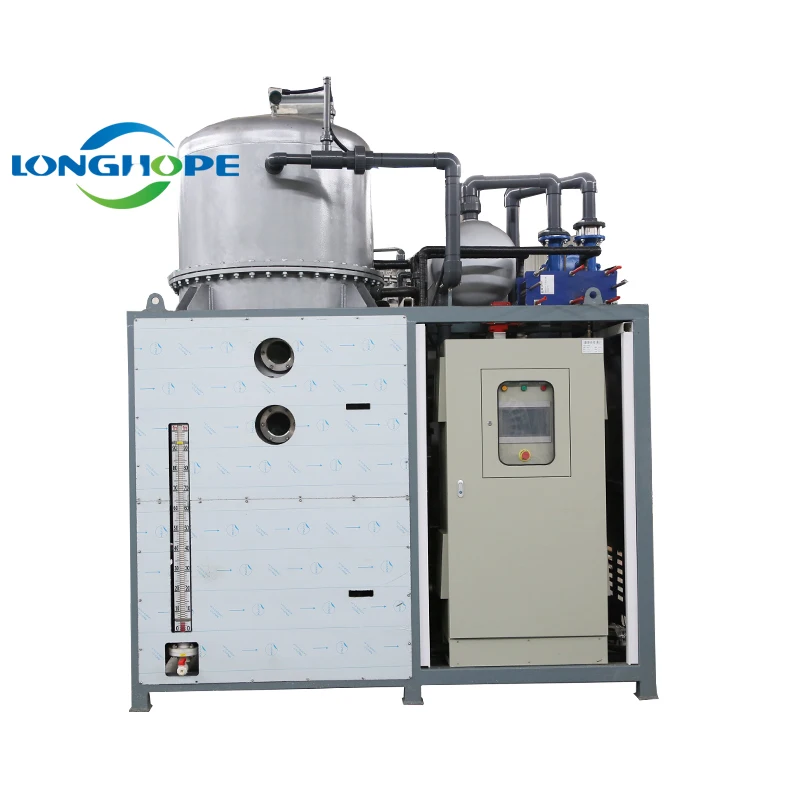
The main functions of water treatment for industrial use include filtration, chemical adjustment, sediment removal, and microbial control. Advanced water treatment for industrial use systems employ multimedia filters, reverse osmosis technology, ion exchange resins, and ultraviolet sterilization to achieve superior purification levels. These technological features ensure consistent water quality that prevents scaling, corrosion, and biological contamination in industrial equipment.
Applications of water treatment for industrial use span numerous sectors including food and beverage production, pharmaceutical manufacturing, power generation, semiconductor fabrication, and textile processing. Each industry requires customized water treatment for industrial use solutions tailored to specific contaminant profiles and quality standards. Modern water treatment for industrial use combines automation, real-time monitoring, and intelligent control systems to optimize performance while reducing operational costs and environmental impact.

 EN