Crystallization System | Industrial Crystal Separation

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

crystallization system

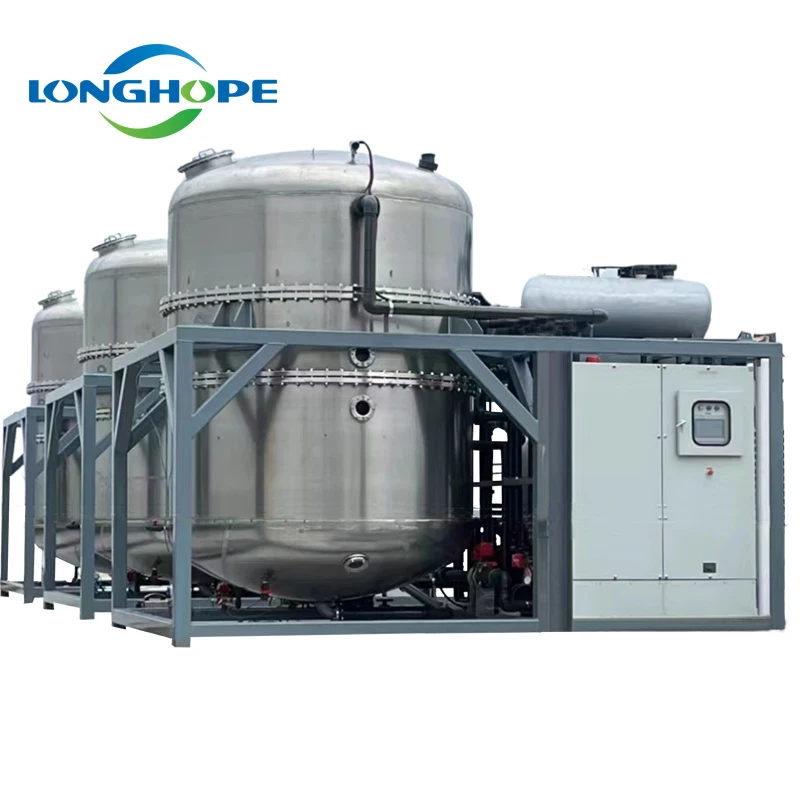
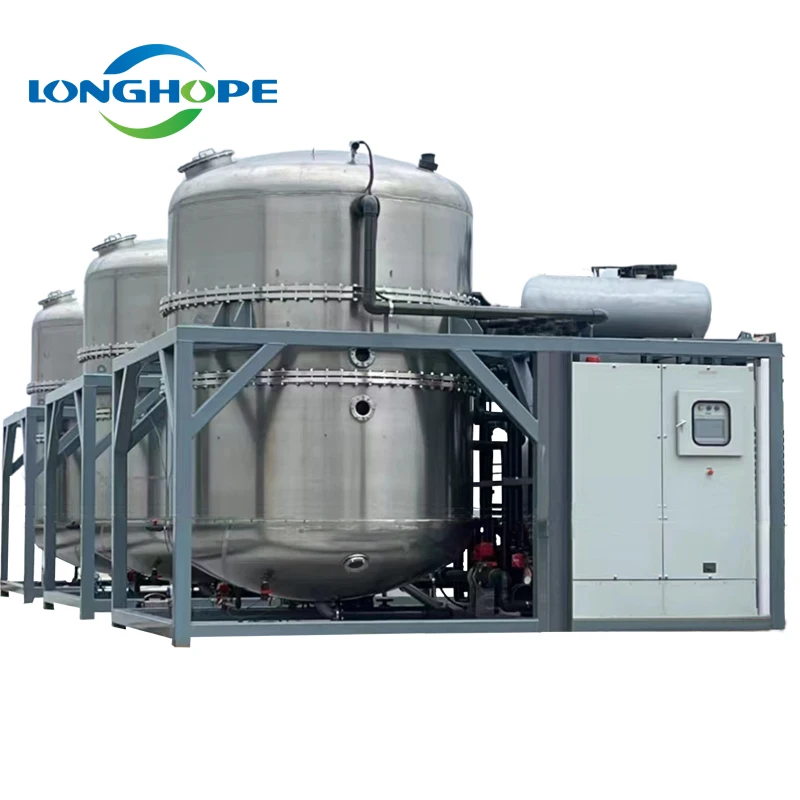
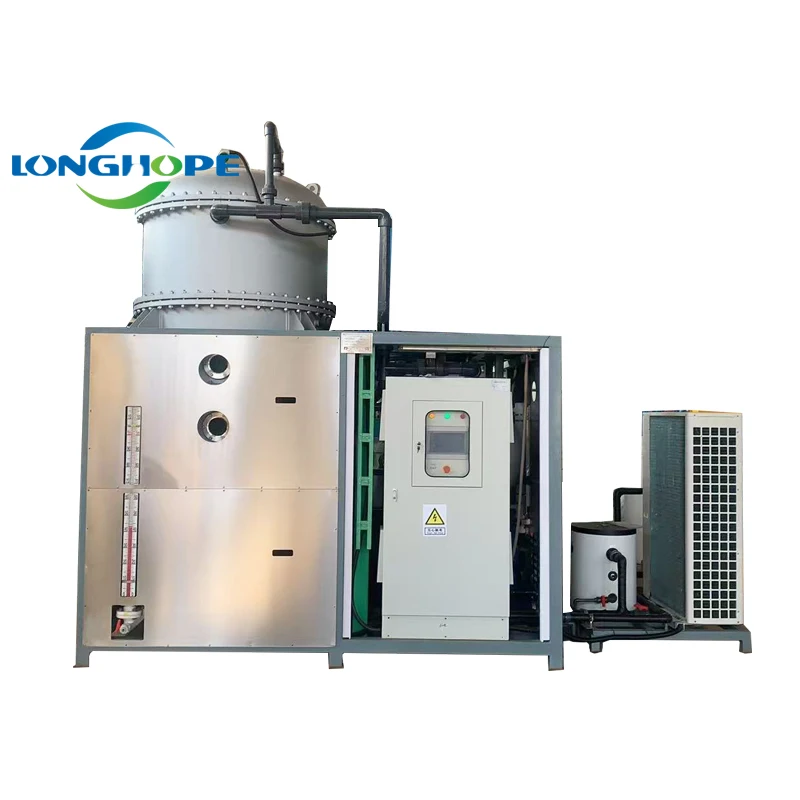
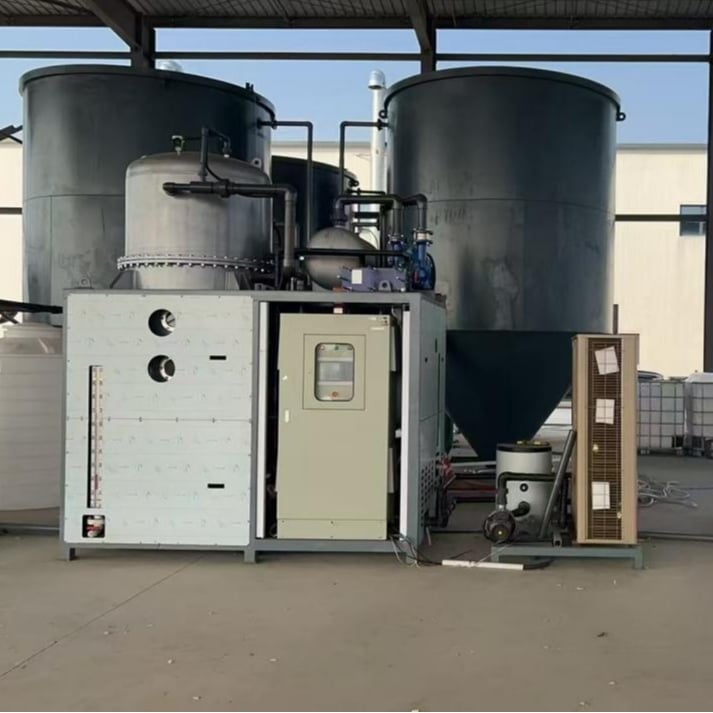
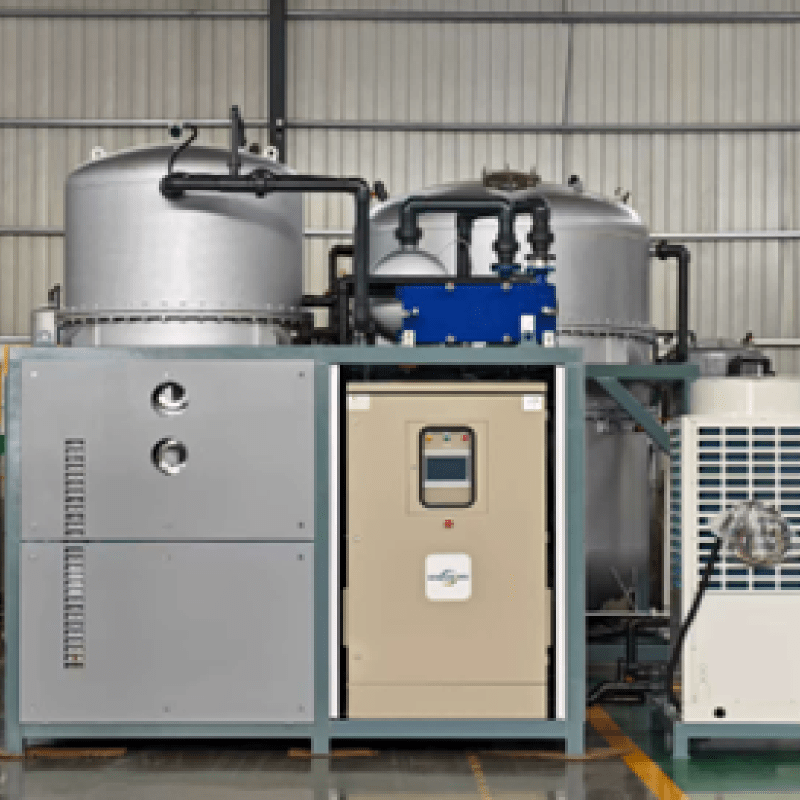
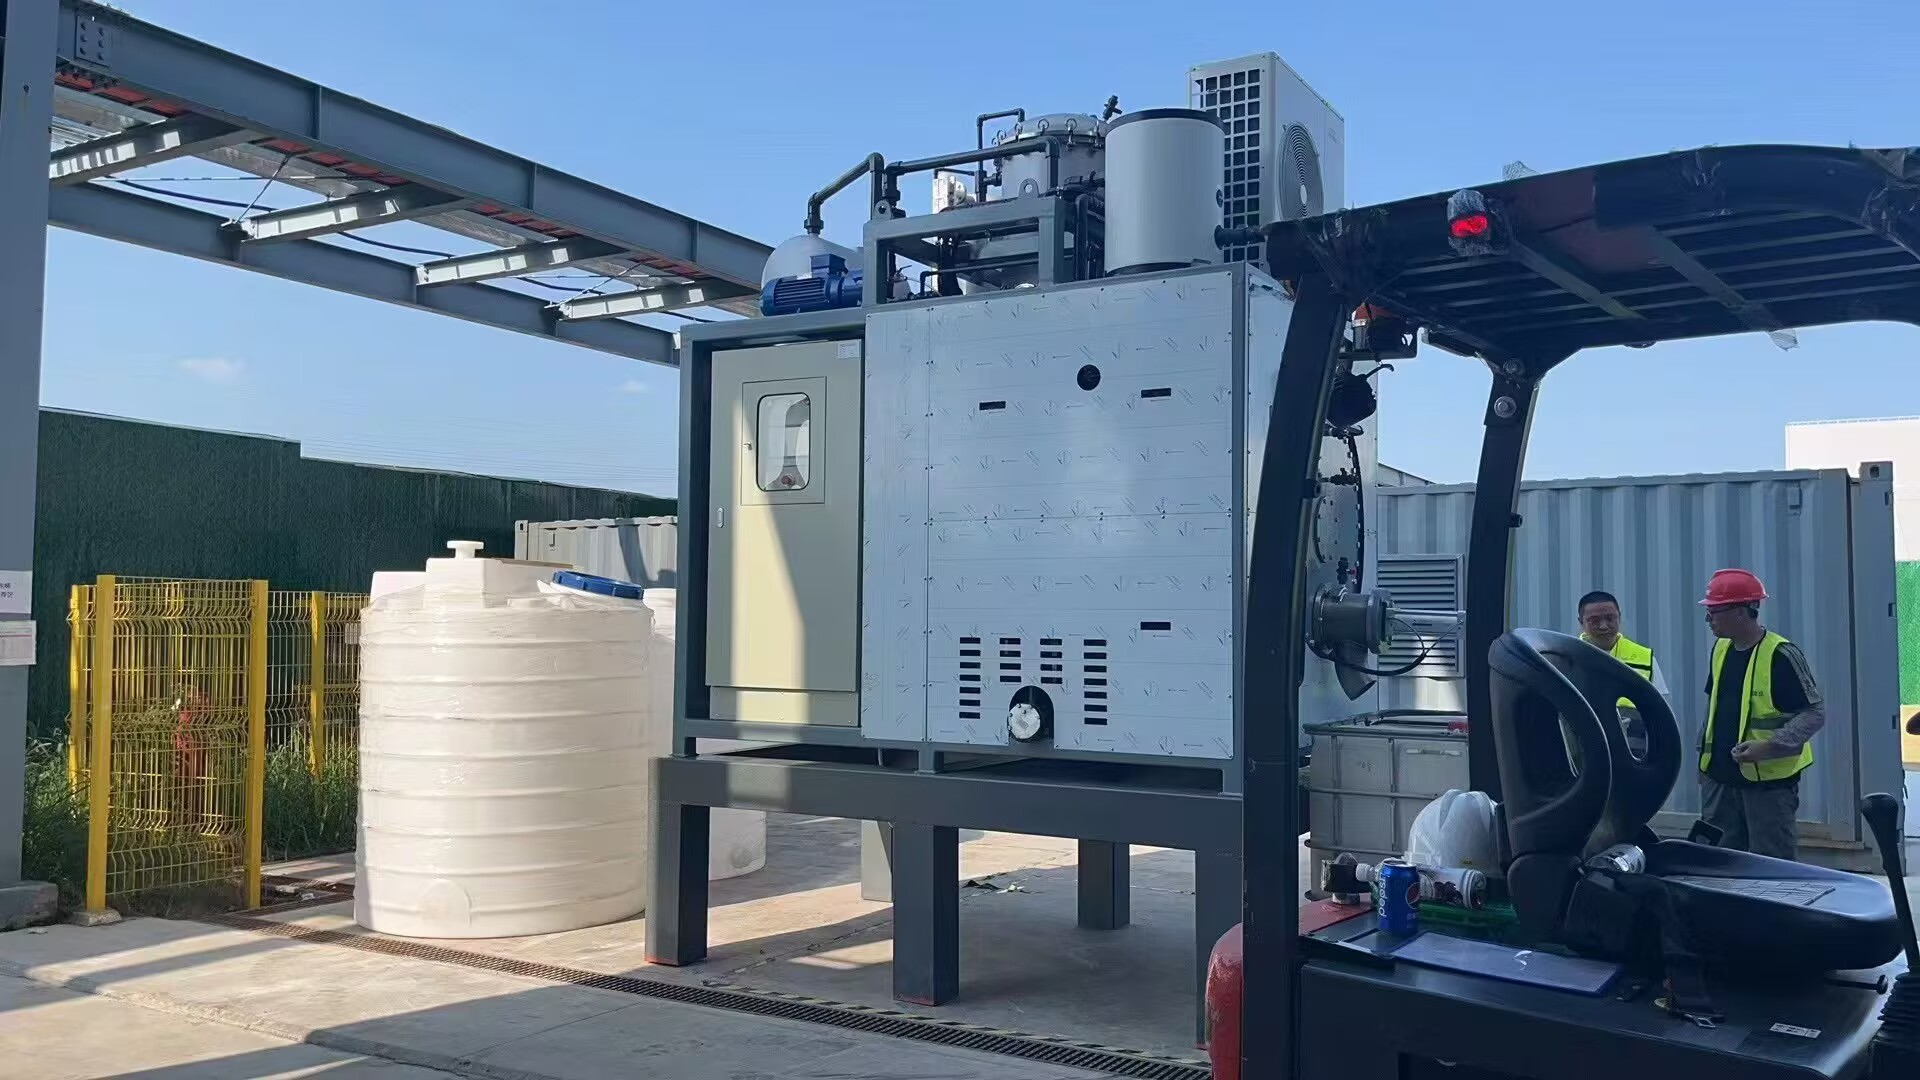
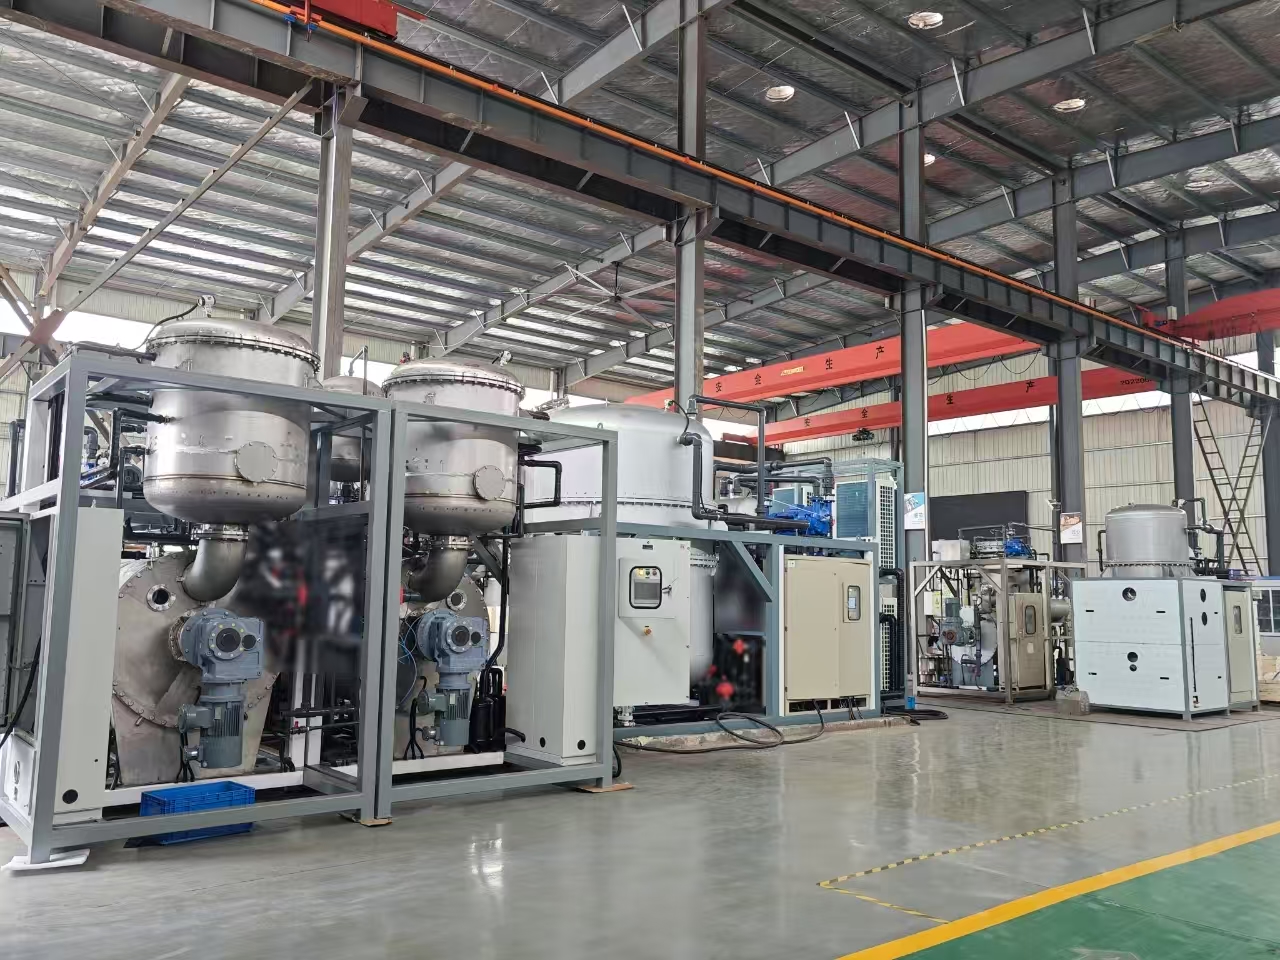
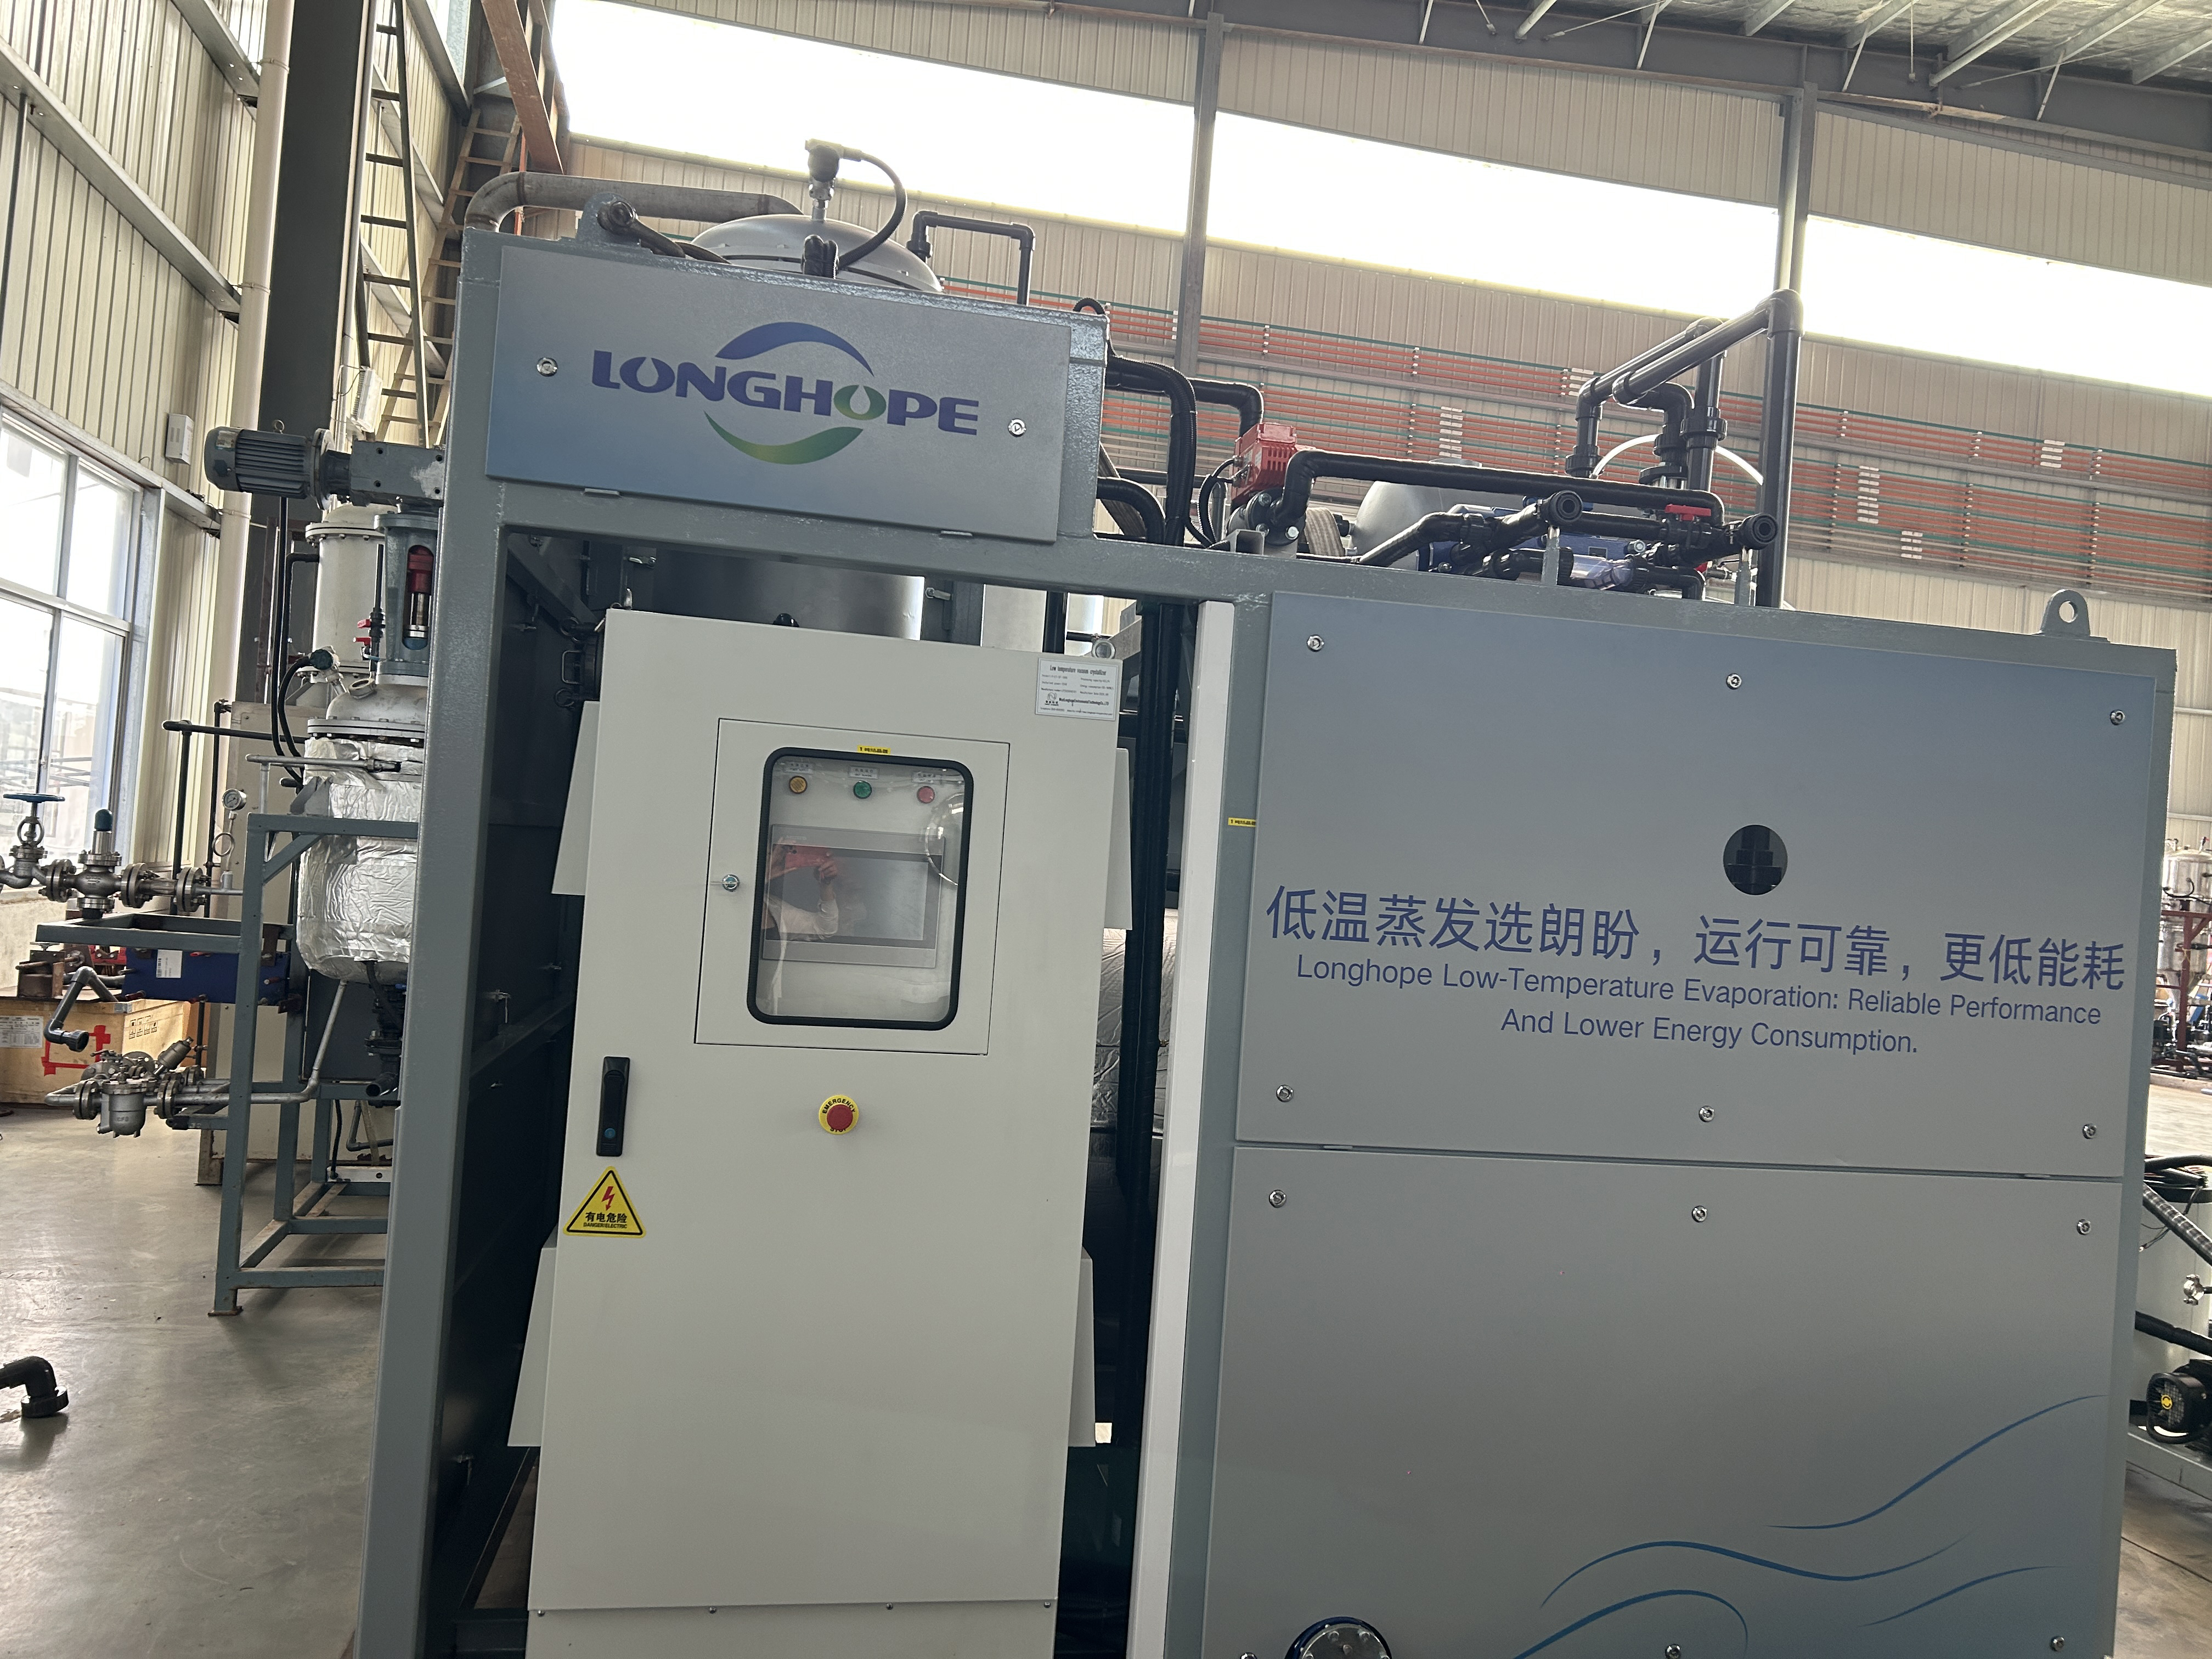
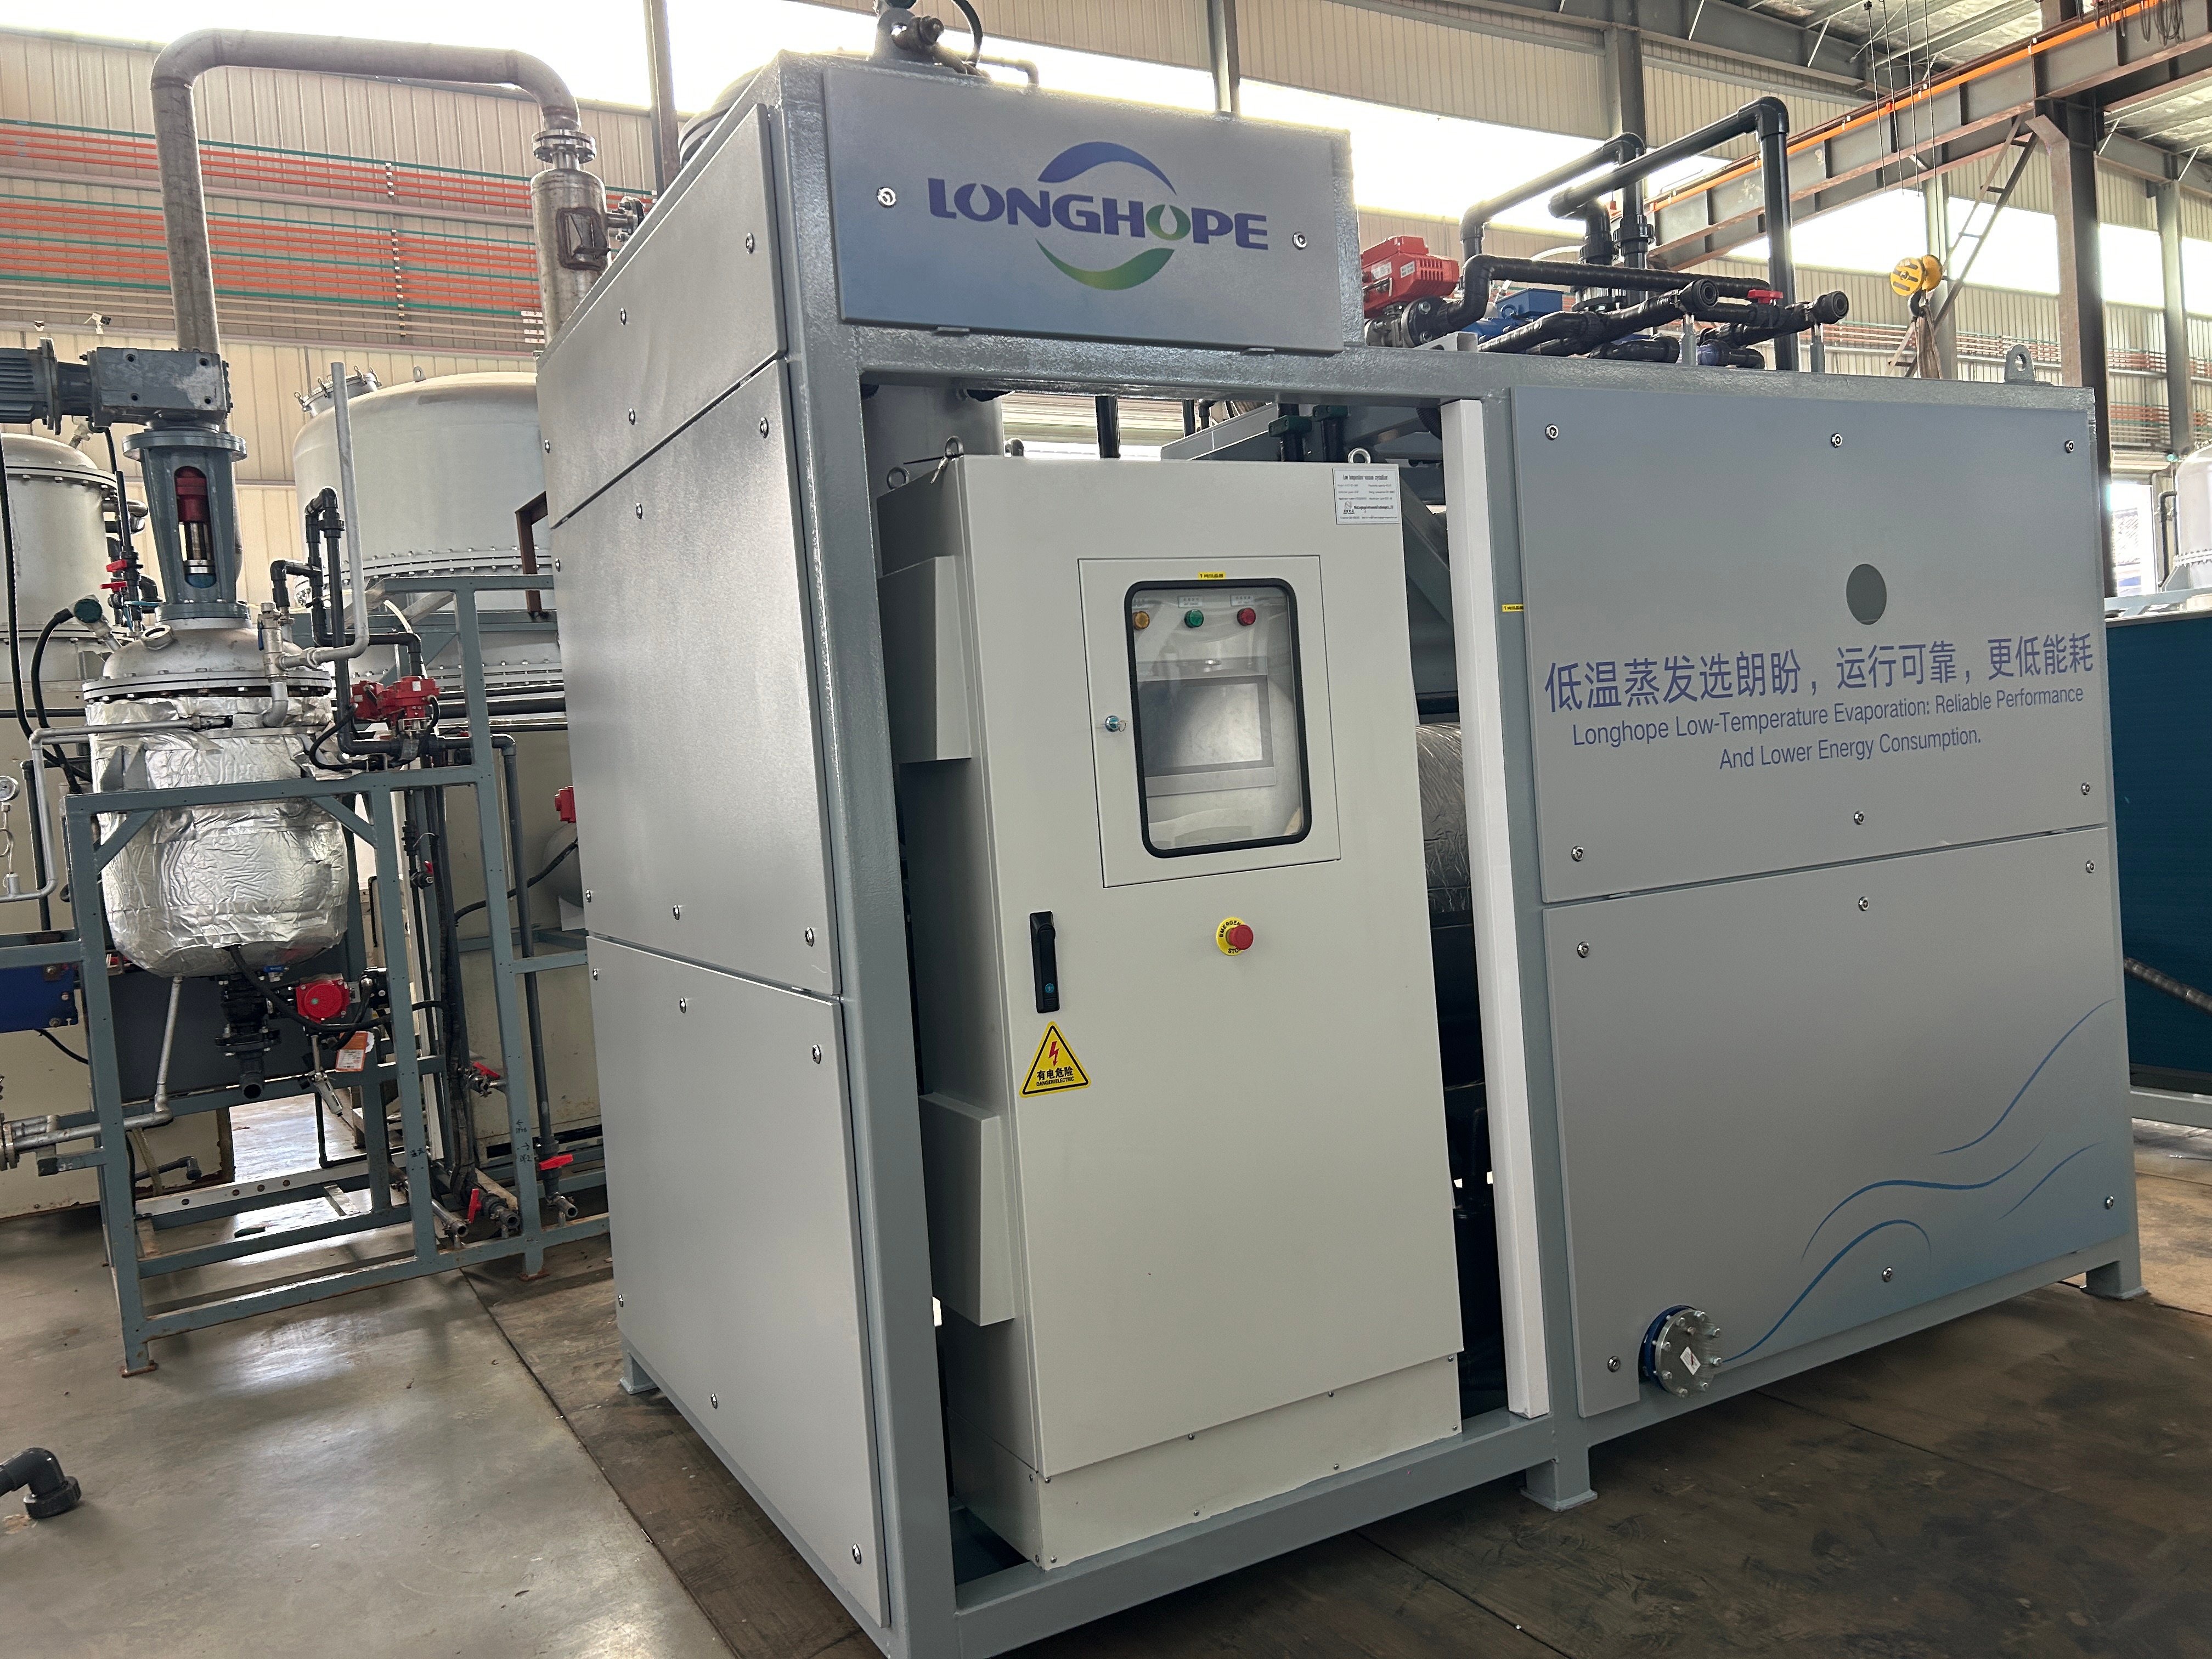
A crystallization system represents a sophisticated industrial solution designed to separate and purify dissolved substances through controlled crystal formation. This crystallization system operates by cooling or evaporating liquid solutions, causing solute molecules to arrange into organized crystal structures that can be easily harvested and processed. The primary function of a crystallization system involves transforming dissolved materials into pure solid crystals while removing impurities that remain in the mother liquor. Modern crystallization systems incorporate precision temperature control, automated monitoring equipment, and efficient mixing mechanisms to optimize crystal growth and product quality. These systems find extensive use across pharmaceutical manufacturing, chemical production, food processing, and material science industries. The technological features of a crystallization system include advanced cooling jackets, agitation systems, and real-time sensor technology that track concentration and temperature variables throughout the process. By implementing a crystallization system, manufacturers achieve superior purity levels compared to alternative separation methods. The versatility of a crystallization system makes it invaluable for processing diverse compounds ranging from salts and sugars to active pharmaceutical ingredients. Industrial applications demonstrate that a crystallization system consistently delivers uniform crystal sizes, improved yield rates, and reduced processing waste. Whether producing fine chemicals or bulk materials, a crystallization system provides the controlled environment necessary for reliable and repeatable results in modern manufacturing operations.

Popular Products

A crystallization system delivers substantial operational benefits that directly enhance manufacturing efficiency and product quality. This crystallization system enables manufacturers to achieve higher purity levels by selectively removing impurities while maintaining desired compound integrity. The operational advantages of a crystallization system include reduced energy consumption through optimized cooling cycles and automated process control that minimizes manual intervention and associated errors. Implementing a crystallization system improves production consistency by maintaining precise temperature and concentration parameters, resulting in uniform crystal morphology and size distribution. Cost savings emerge from a crystallization system's ability to maximize yield rates and minimize waste material that requires disposal or reprocessing. The environmental benefits of a crystallization system include reduced chemical consumption, lower water usage, and decreased waste generation compared to traditional separation methods. A crystallization system supports diverse applications across multiple industries, from pharmaceutical development requiring strict quality standards to food ingredient production demanding consistent specifications. Decision-making becomes simpler when choosing a crystallization system because the technology provides measurable improvements in throughput and product specifications that directly impact profitability. The scalability of a crystallization system allows businesses to expand production capacity without sacrificing quality or requiring complete equipment replacement. Maintenance requirements for a crystallization system remain manageable through straightforward cleaning procedures and replaceable component designs. User-friendly interfaces on modern crystallization system equipment enable operators to monitor progress, adjust parameters, and troubleshoot issues without extensive technical training. By investing in a crystallization system, organizations gain competitive advantages through superior product quality, faster production times, and enhanced operational reliability that strengthen market position and customer satisfaction.

Latest News

Benefits of Low Temperature Heat Pump Evaporator in Industry

24

Jul

Benefits of Low Temperature Heat Pump Evaporator in Industry

Industrial facilities worldwide face mounting pressure to reduce operating costs while maintaining production quality and environmental compliance. The low temperature heat pump evaporator has emerged as a transformative solution that addresses these...
View More
How to Optimize Your Evaporator System for Efficiency

24

Jul

How to Optimize Your Evaporator System for Efficiency

An evaporator system efficiency directly impacts your operational costs, production capacity, and environmental footprint in industrial processing. Whether you operate in chemical manufacturing, food processing, pharmaceutical production, or waste ma...
View More
Benefits of a Modern Evaporator System for Wastewater

24

Jul

Benefits of a Modern Evaporator System for Wastewater

Modern industrial facilities face mounting pressure to reduce wastewater disposal costs while meeting strict environmental regulations. An evaporator systems for wastewater represents a transformative solution that addresses both operational expenses...
View More
Vacuum Distillation Setup Maintenance for Longevity

02

Sep

Vacuum Distillation Setup Maintenance for Longevity

A vacuum distillation setup represents a significant investment in industrial separation technology, and protecting that investment requires a structured maintenance approach. Whether your vacuum distillation setup operates in a pharmaceutical labora...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

crystallization system

Precision Temperature Control Technology

Precision Temperature Control Technology

A crystallization system excels through advanced temperature management capabilities that maintain exact operating conditions throughout the crystallization process. The precision temperature control technology integrated into modern crystallization system equipment uses multiple sensors and computerized feedback loops to prevent temperature fluctuations that compromise crystal quality. This crystallization system feature enables operators to achieve consistent supersaturation levels, ensuring uniform nucleation and controlled crystal growth rates. The benefit of this technology extends beyond quality improvements, as maintaining optimal temperatures reduces energy waste and operational costs. A crystallization system with precision temperature control allows manufacturers to process temperature-sensitive compounds that would degrade under conventional methods. The reliability of temperature management in a crystallization system directly translates to predictable batch outcomes, reduced variability between production runs, and improved first-time-right manufacturing. Industries relying on strict specifications appreciate how this crystallization system feature delivers the consistency required for regulatory compliance and customer satisfaction. Temperature precision capabilities make a crystallization system indispensable for pharmaceutical applications where deviation from specifications compromises efficacy and safety.
Automated Crystal Separation and Recovery

Automated Crystal Separation and Recovery

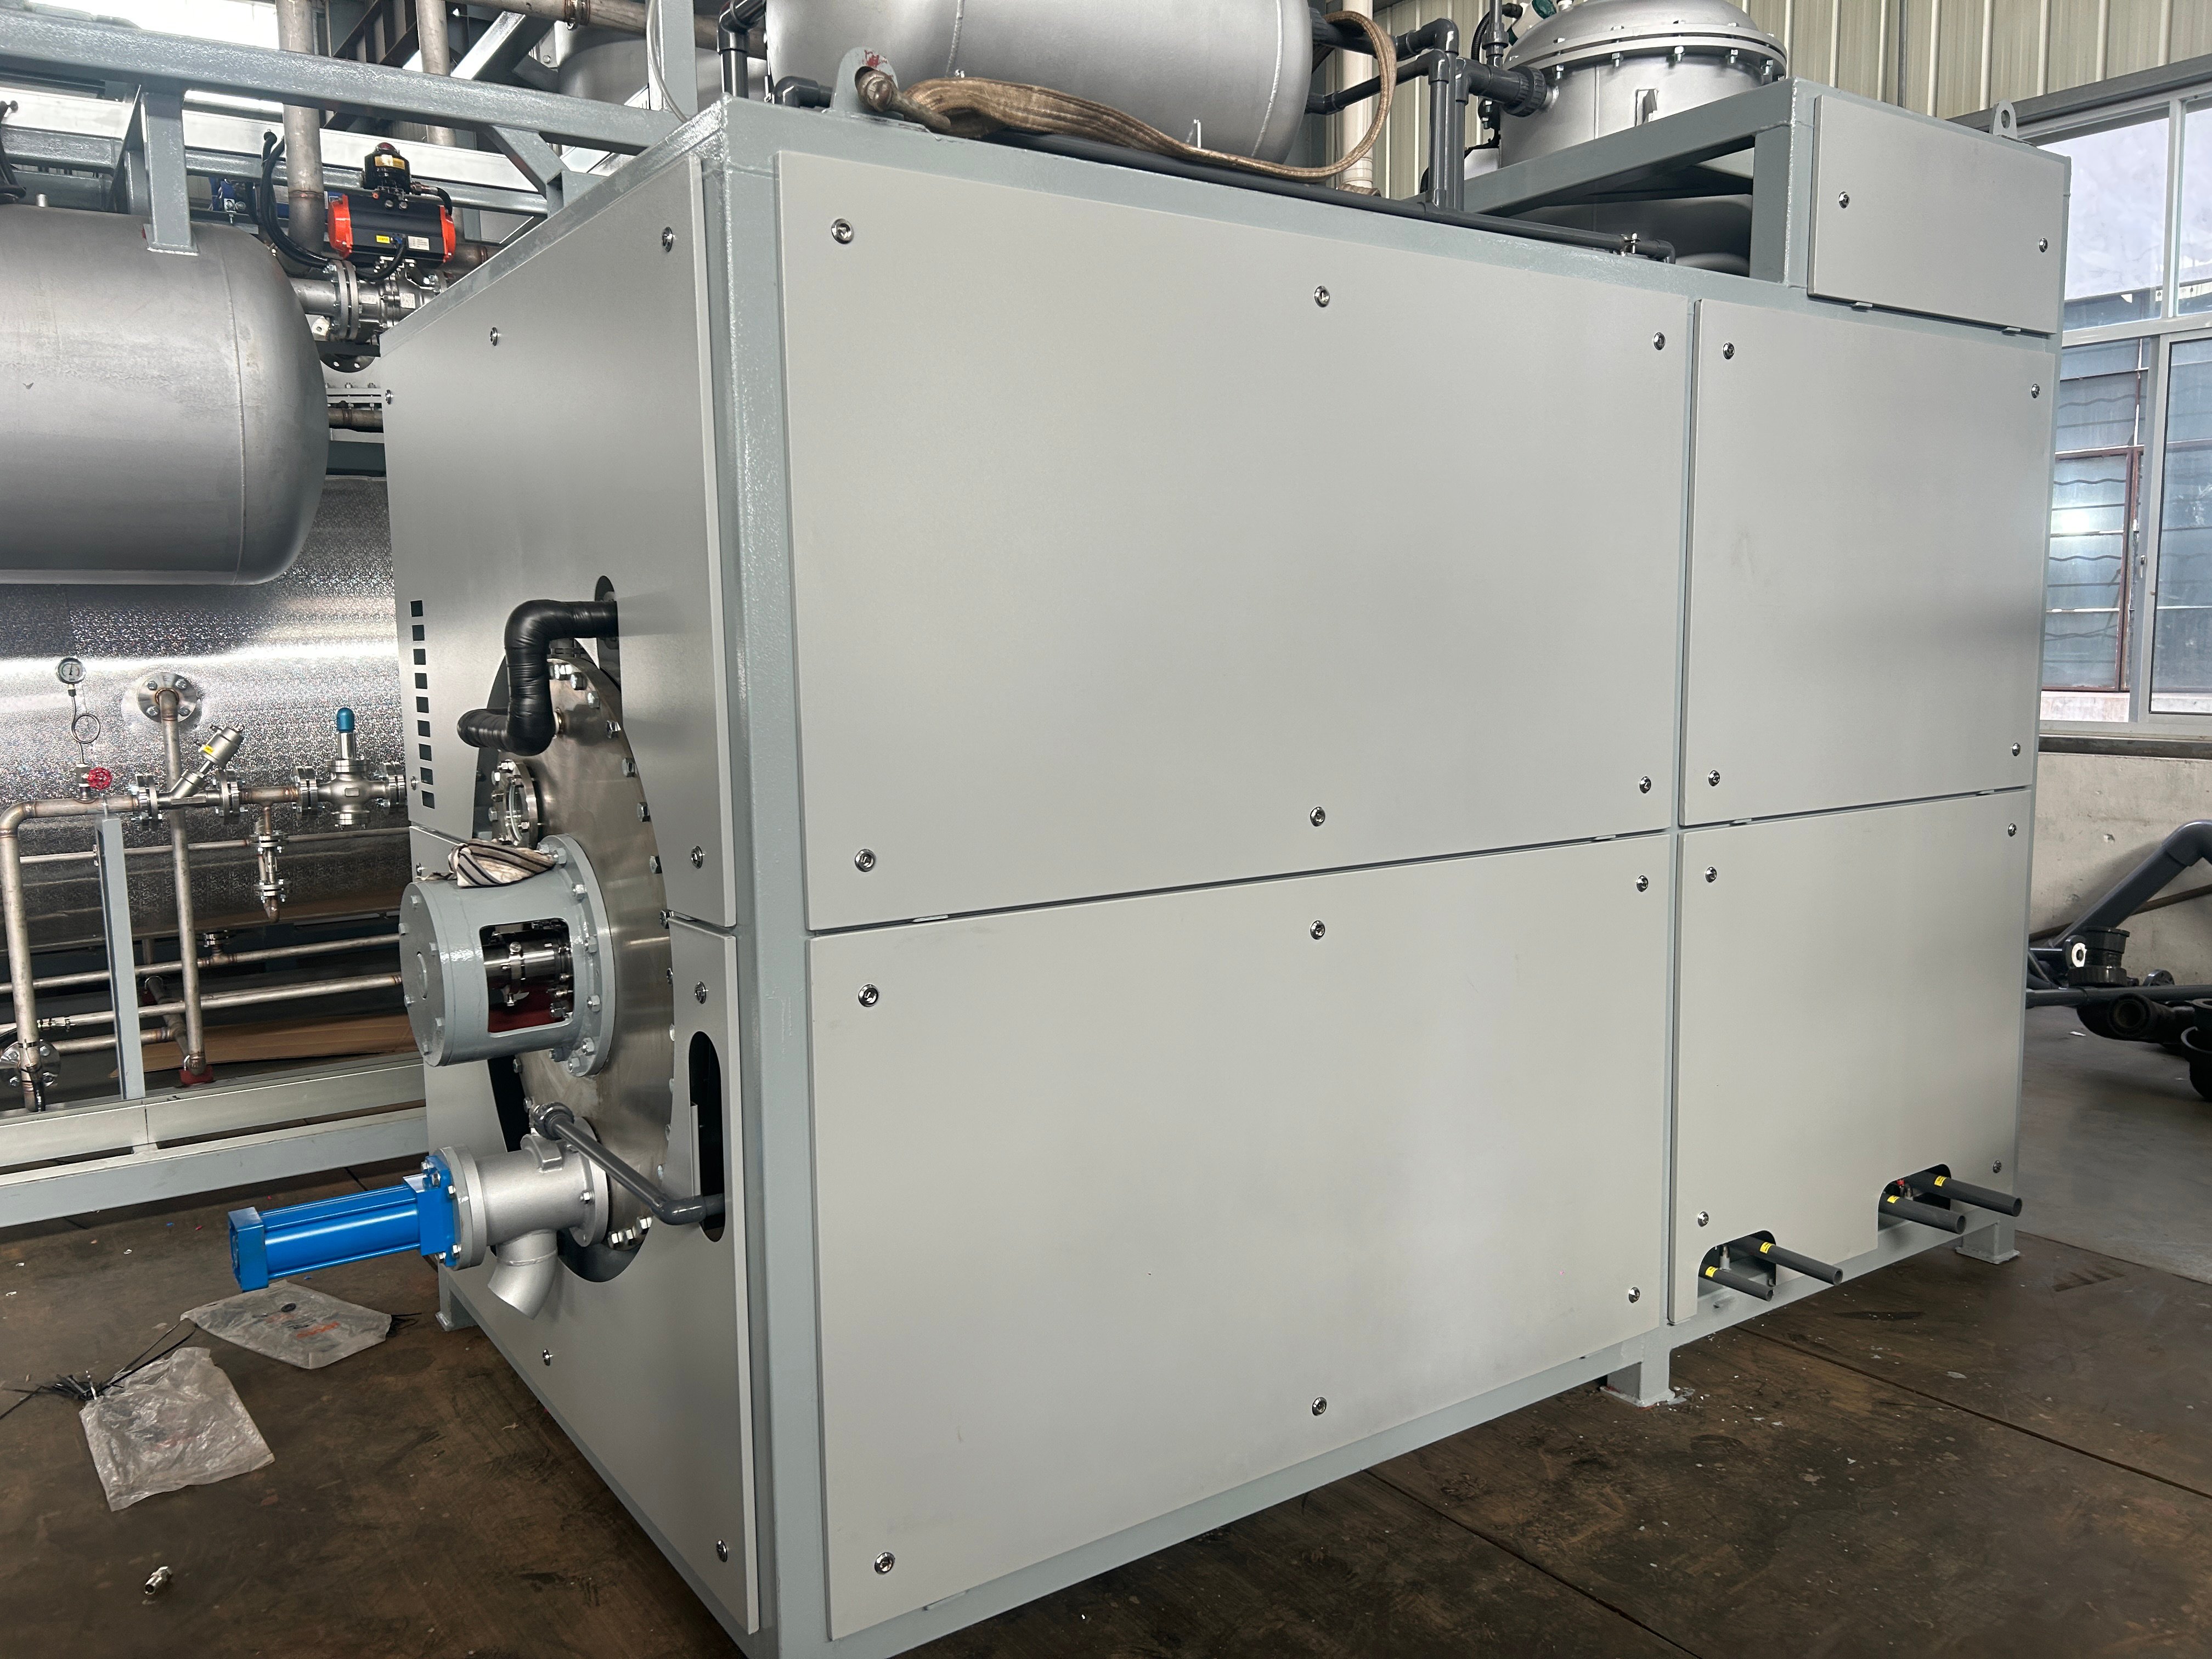
Modern crystallization system equipment incorporates automated mechanisms that efficiently separate crystals from mother liquor while maximizing product recovery rates. This crystallization system feature eliminates manual separation steps that introduce inconsistency and increase labor costs while reducing throughput. The automation technology within a crystallization system includes centrifugal separators, filtration systems, and pneumatic discharge mechanisms that operate seamlessly within integrated workflows. A crystallization system designed with automated recovery capabilities reduces processing time by condensing multiple operational steps into a single coordinated sequence. The practical benefit of this crystallization system functionality includes lower labor requirements, faster batch completion, and enhanced workplace safety by minimizing manual handling of hot solutions or harsh chemicals. Crystal recovery rates improve substantially with a crystallization system featuring optimized separation design, directly impacting profitability through increased yield percentages. This crystallization system advancement proves particularly valuable in high-volume production environments where manual separation creates bottlenecks. The consistent operation of a crystallization system's automated systems ensures repeatable results while enabling operators to allocate resources toward quality monitoring rather than physical separation tasks.
Real-Time Process Monitoring and Control

Real-Time Process Monitoring and Control

A crystallization system equipped with comprehensive monitoring capabilities provides operators with immediate visibility into process parameters and crystal development progress. This crystallization system feature uses multiple sensors tracking temperature, concentration, crystal size distribution, and pressure simultaneously throughout production cycles. The real-time data collection from a crystallization system enables rapid adjustments to process parameters when conditions deviate from target specifications, preventing batch failures before they occur. A crystallization system with advanced monitoring eliminates guesswork from production management, replacing assumptions with concrete measurements that inform decision-making. Operators benefit from a crystallization system's intuitive dashboards and alert systems that flag potential issues requiring immediate attention or corrective action. The predictive capabilities of modern crystallization system technology allow manufacturers to anticipate problems and optimize conditions proactively rather than reactively troubleshooting failures. This crystallization system advantage reduces downtime, improves throughput, and ensures consistent product specifications across all production batches. Data logging features integrated into a crystallization system create comprehensive documentation supporting regulatory compliance, quality audits, and continuous process improvement initiatives that strengthen manufacturing excellence.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000