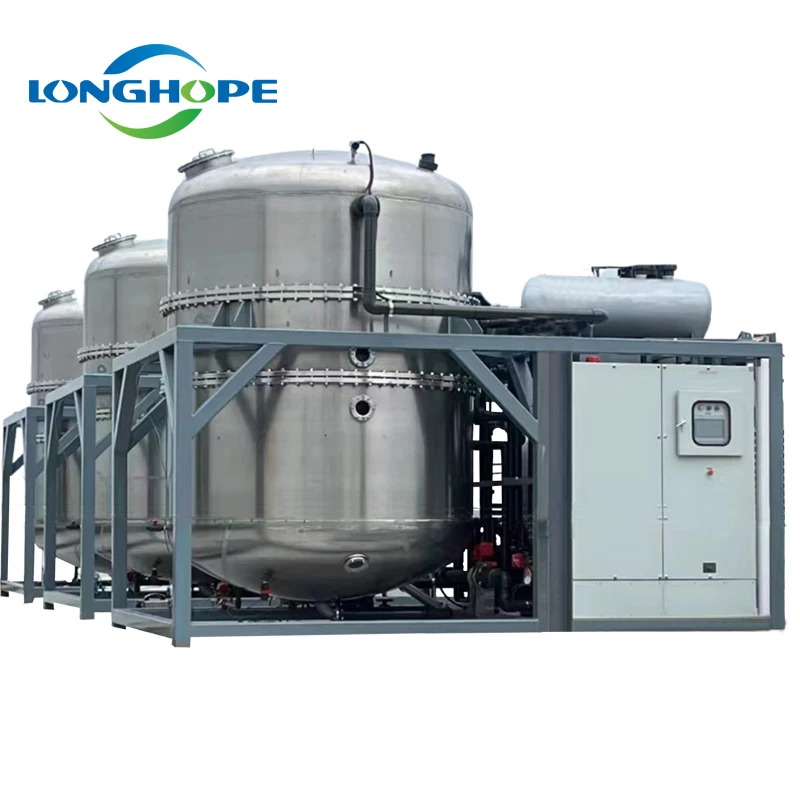
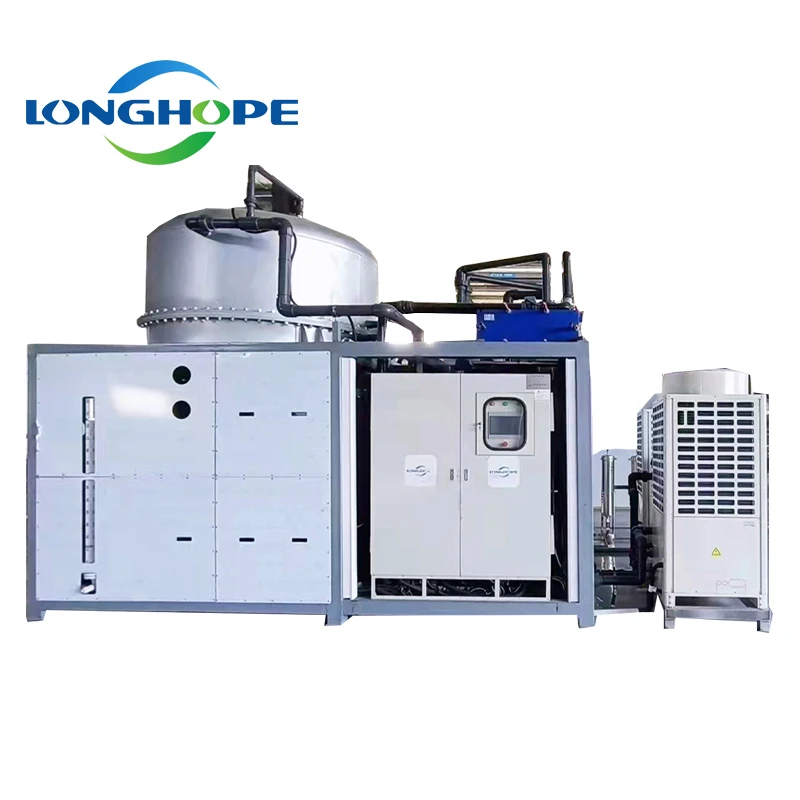
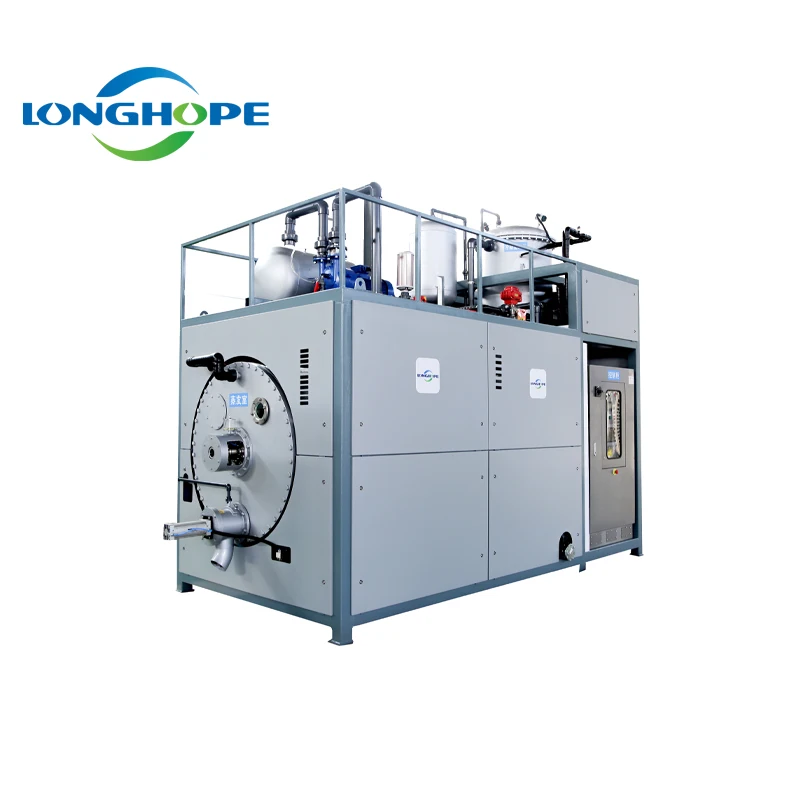
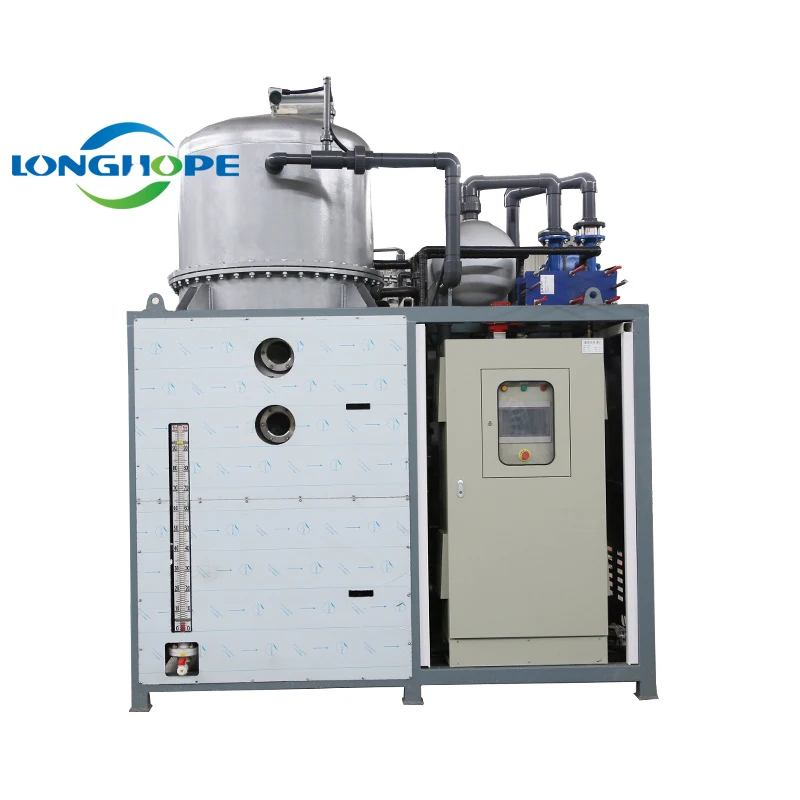
Evaporation Unit: Industrial Liquid Concentration

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

evaporation unit

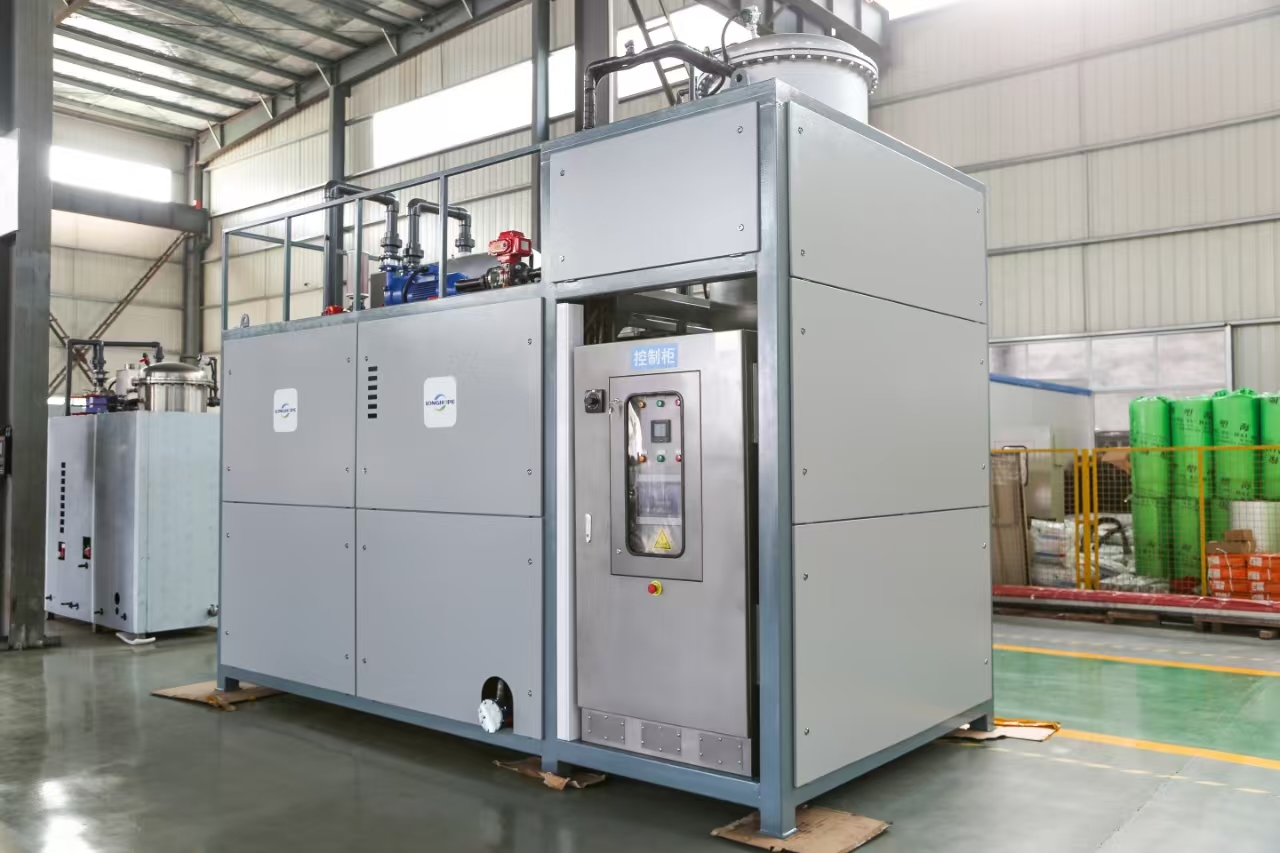
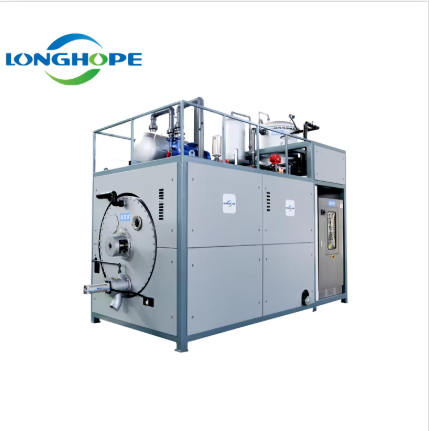
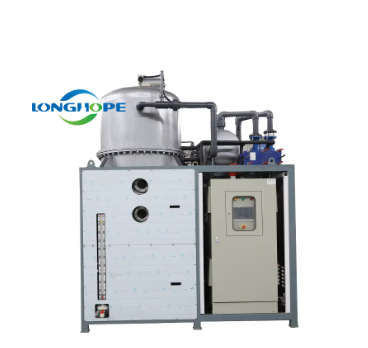
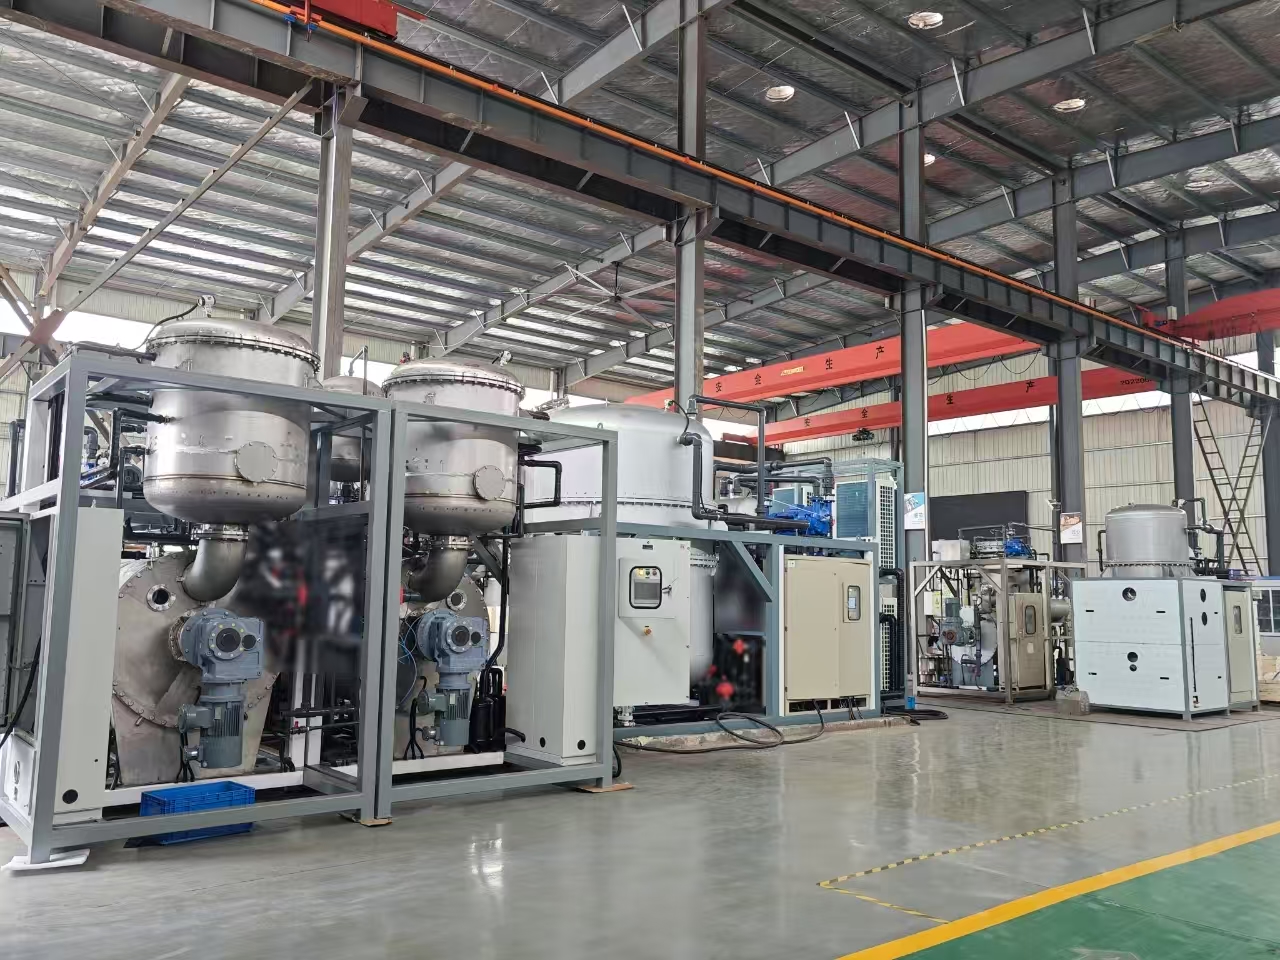
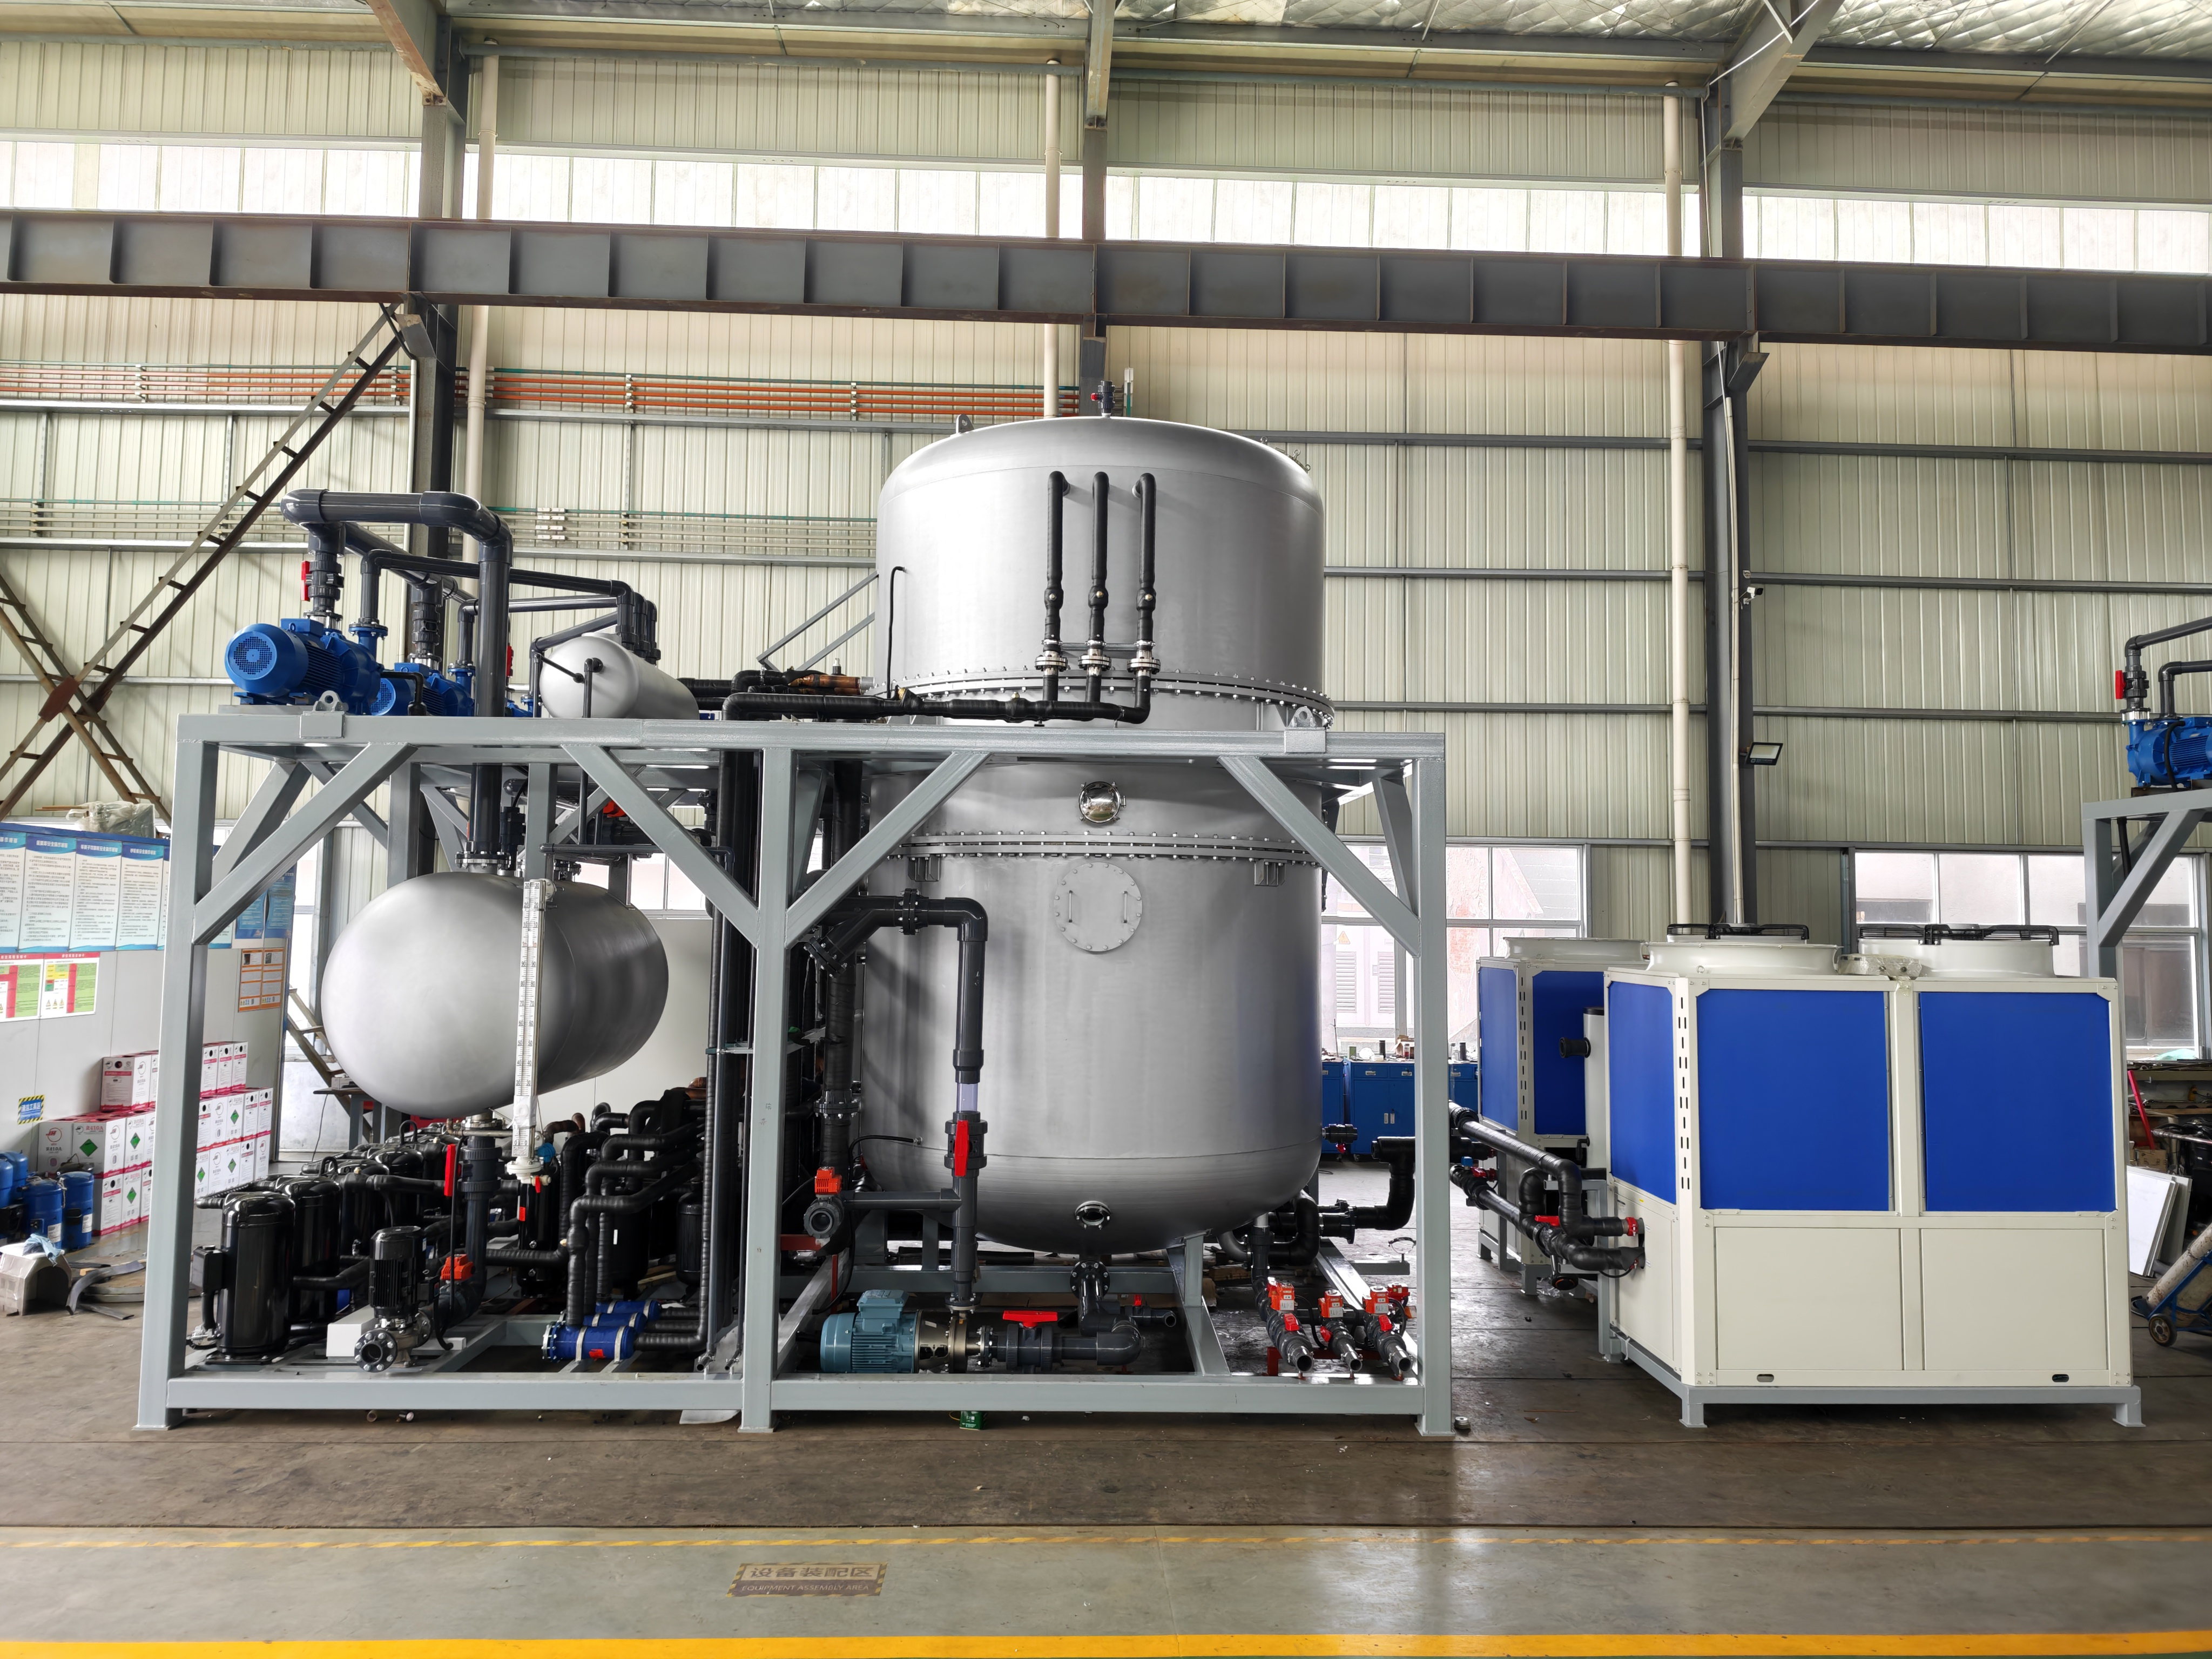
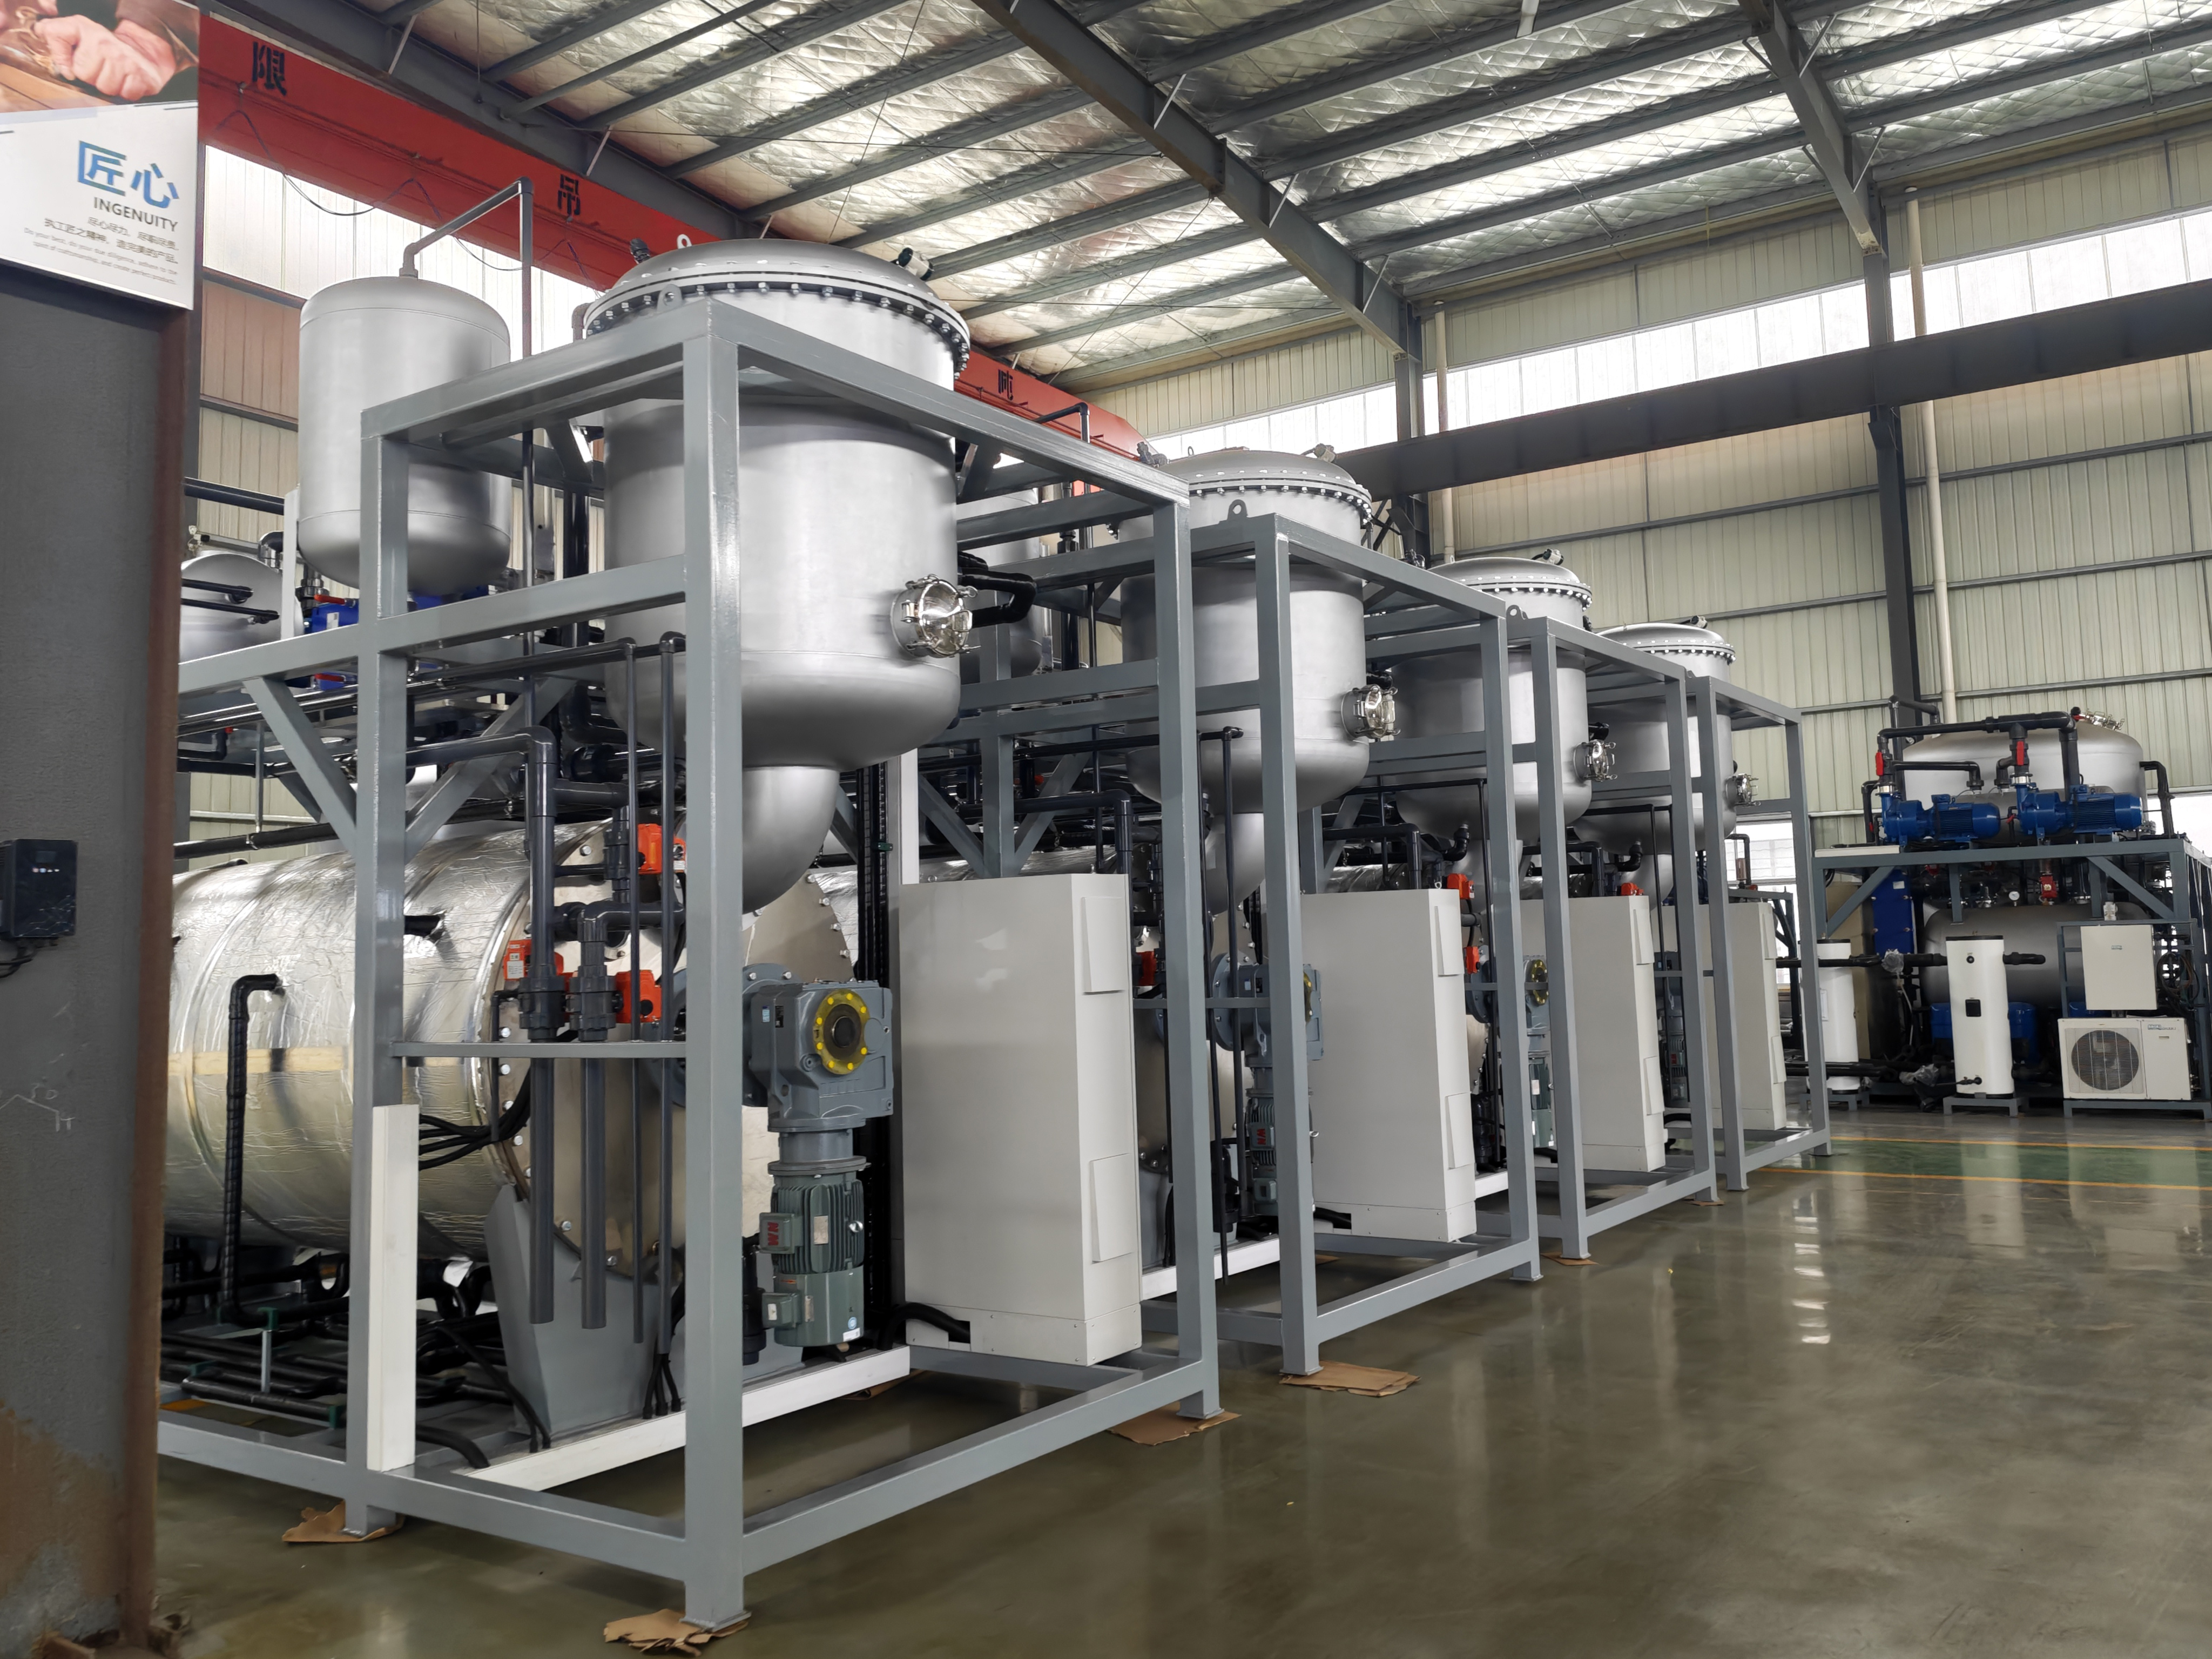
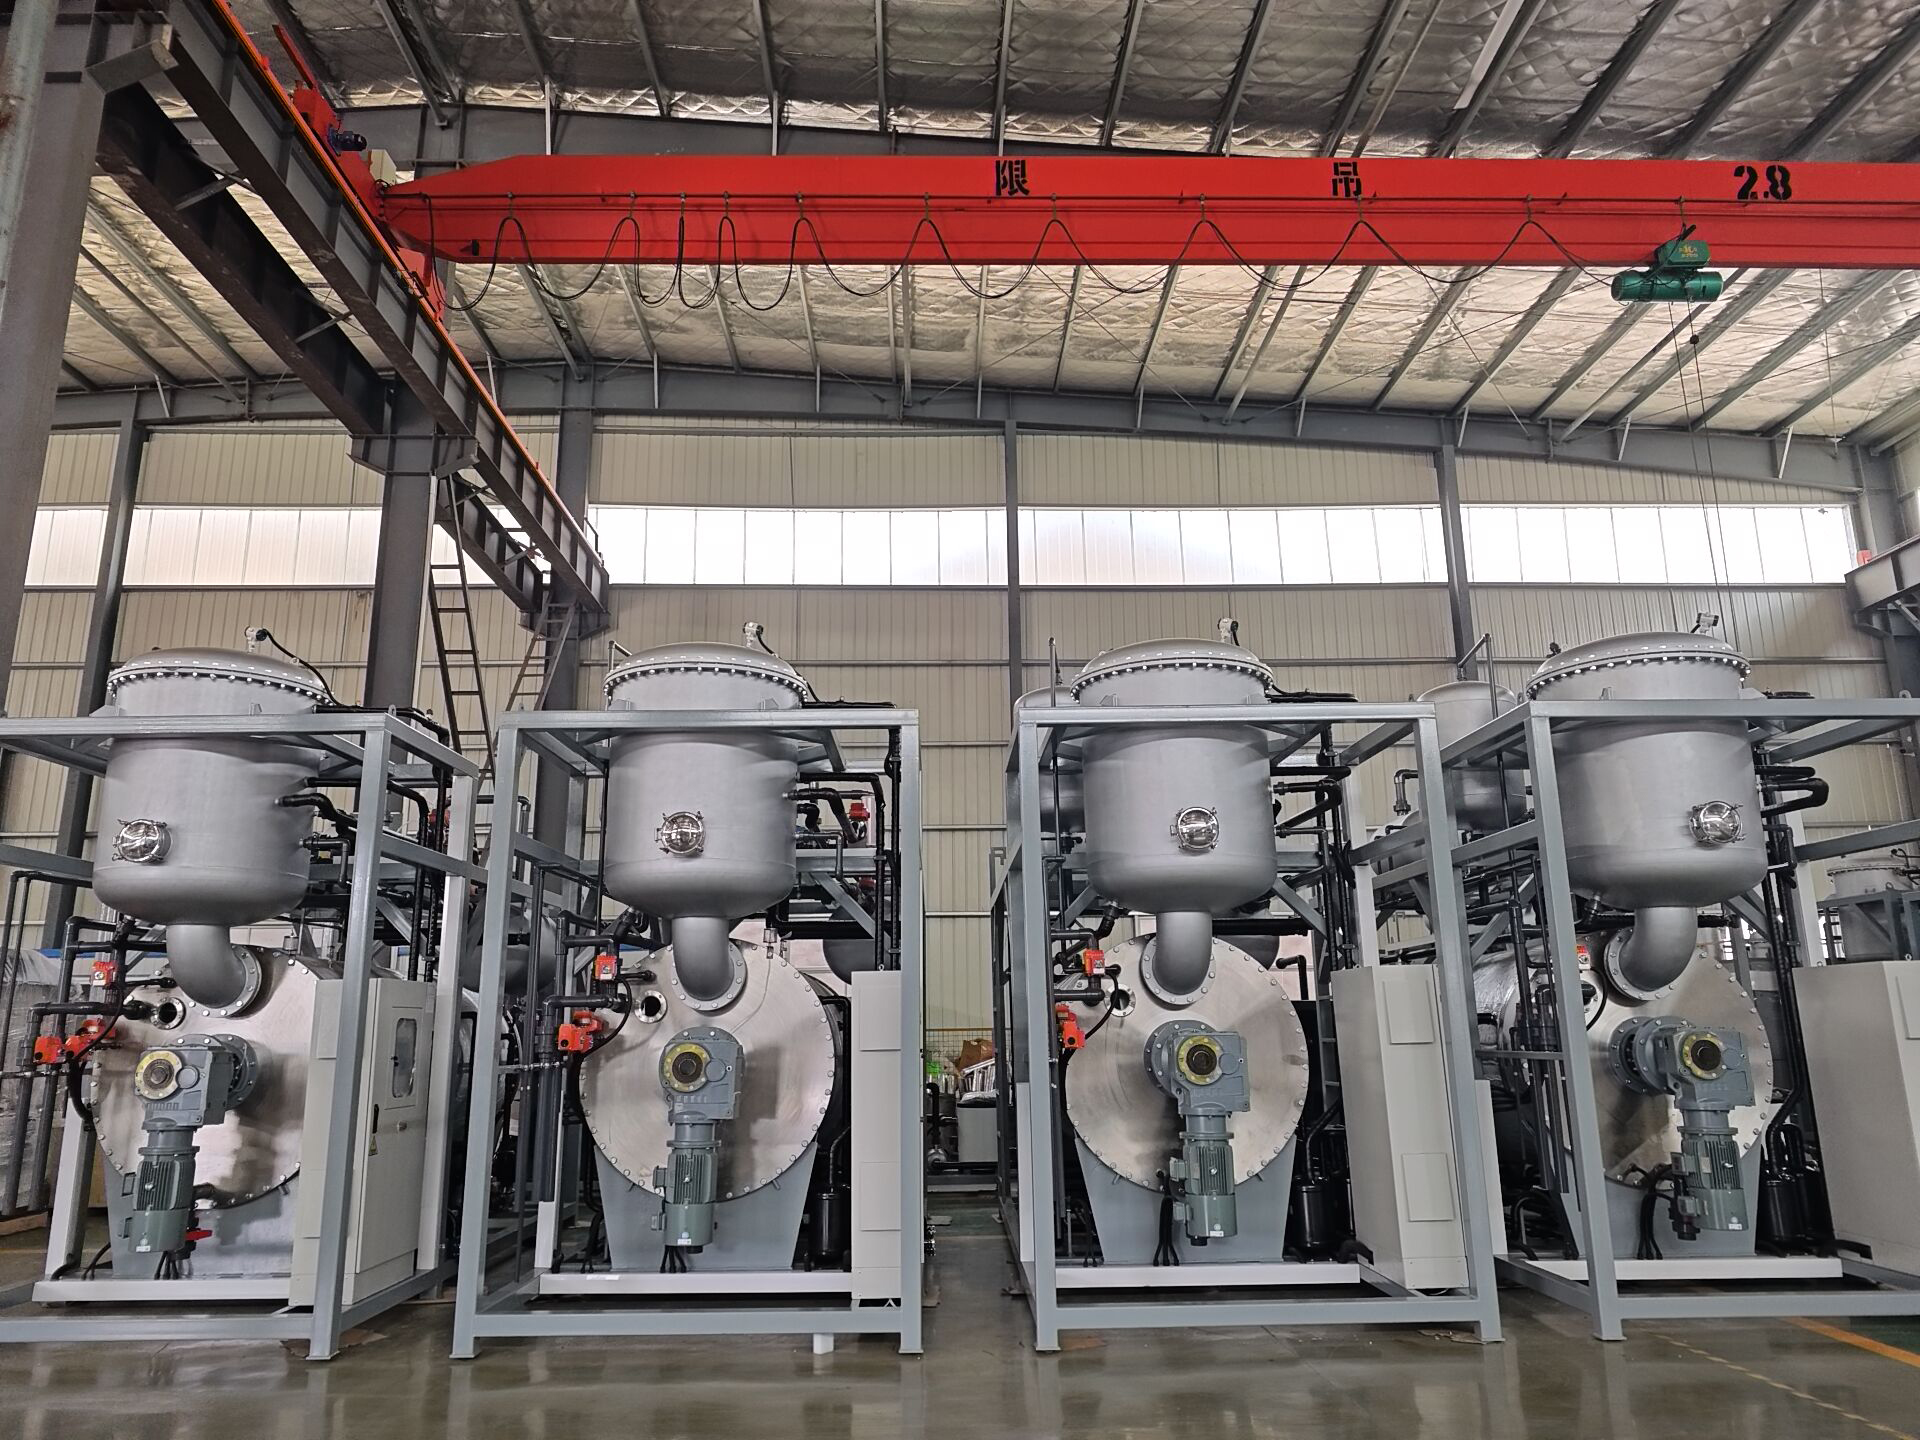
An evaporation unit is a sophisticated industrial equipment designed to remove liquid through the process of vaporization, converting liquid solutions into concentrated forms or recovering valuable materials. The evaporation unit operates by heating liquid to its boiling point, allowing water or other solvents to evaporate while leaving behind concentrated residue or desired substances. This evaporation unit serves multiple critical functions across various industries, including pharmaceutical manufacturing, food processing, chemical production, and waste management. The technological features of an evaporation unit typically include advanced heating systems, vacuum chambers, condensing mechanisms, and automated control systems that optimize energy efficiency. Modern evaporation unit designs incorporate energy-recovery technologies and multiple-effect evaporation systems that maximize operational performance while minimizing environmental impact. An evaporation unit can handle diverse applications, from concentrating fruit juices and dairy products to recovering solvents in chemical facilities. The evaporation unit also supports waste reduction initiatives by enabling companies to recover valuable compounds and reduce liquid disposal costs. These systems are engineered for continuous operation with minimal downtime, featuring stainless steel construction and corrosion-resistant components. An evaporation unit provides precise temperature control and pressure management, ensuring product quality and process consistency. Whether processing heat-sensitive materials or handling corrosive solutions, the evaporation unit remains a versatile solution for industrial separation and concentration needs.

New Product Recommendations

An evaporation unit delivers substantial operational benefits that directly improve your manufacturing efficiency and bottom-line profitability. By concentrating liquids to higher densities, an evaporation unit significantly reduces storage and transportation costs, allowing businesses to handle greater volumes of product with minimal space requirements. The energy-efficient design of a modern evaporation unit cuts operational expenses through advanced heat recovery systems that capture and reuse thermal energy throughout the process. An evaporation unit enables companies to recover valuable solvents and materials that would otherwise be discarded as waste, creating new revenue streams while supporting sustainability initiatives. For pharmaceutical and food companies, an evaporation unit maintains strict quality standards by operating under controlled temperature and pressure conditions, preventing product degradation or contamination. The automated monitoring systems found in an evaporation unit reduce labor costs and human error, enabling smaller teams to manage larger production volumes effectively. An evaporation unit provides consistent, repeatable results that meet strict industry regulations and quality certifications required across sectors. Businesses benefit from an evaporation unit's versatility, as it adapts to process various liquid types and concentrations without requiring complete system reconfiguration. The robust construction of an evaporation unit ensures long service life with minimal maintenance requirements, protecting your capital investment. Companies implementing an evaporation unit experience reduced environmental impact through decreased wastewater generation and lower carbon footprints. The flexibility offered by an evaporation unit allows businesses to scale operations efficiently as production demands increase, supporting sustainable growth strategies without proportional infrastructure expansion.

Tips And Tricks

Vacuum Distillation System Maintenance Best Practices

24

Jul

Vacuum Distillation System Maintenance Best Practices

Proper vacuum distillation system maintenance is critical for industries relying on separation, purification, and concentration processes. A well-maintained vacuum distillation system ensures consistent product quality, minimizes operational downtime...
View More
How Industrial Water Treatment Saves Costs and Resources

24

Jul

How Industrial Water Treatment Saves Costs and Resources

Industrial water treatment represents one of the most significant opportunities for manufacturing facilities to reduce operational expenses while protecting environmental resources. Organizations across industries face mounting pressure to minimize w...
View More
Vacuum Distillation: Key Benefits for Industrial Use

24

Jul

Vacuum Distillation: Key Benefits for Industrial Use

Vacuum distillation has become an essential separation technology across numerous industrial sectors, offering superior performance compared to conventional atmospheric distillation methods. By operating under reduced pressure conditions, vacuum dist...
View More
Benefits of a Modern Evaporator System for Wastewater

24

Jul

Benefits of a Modern Evaporator System for Wastewater

Modern industrial facilities face mounting pressure to reduce wastewater disposal costs while meeting strict environmental regulations. An evaporator systems for wastewater represents a transformative solution that addresses both operational expenses...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

evaporation unit

Energy-Efficient Heat Recovery Technology

Energy-Efficient Heat Recovery Technology

Modern evaporation unit systems integrate advanced heat recovery mechanisms that capture thermal energy from vapor condensation and redirect it back into the evaporation process. This intelligent energy recycling dramatically reduces fuel consumption and operational costs while maintaining consistent processing temperatures. An evaporation unit equipped with multiple-effect technology can process liquids through sequential stages, where the vapor generated in one stage provides heat for the next stage. This cascading process significantly improves thermal efficiency compared to conventional single-stage systems. The energy-efficient design of an evaporation unit translates directly into lower utility bills and reduced environmental impact. Companies utilizing an evaporation unit with heat recovery capabilities report energy savings of up to fifty percent compared to traditional evaporation methods. The sophisticated control systems integrated into an evaporation unit automatically optimize heat distribution and maintain peak efficiency throughout the production cycle. Investment in an evaporation unit with energy recovery technology typically pays for itself within two to three years through cumulative energy savings. This advanced technology makes an evaporation unit an environmentally responsible choice for forward-thinking manufacturers committed to reducing their carbon footprint.
Precision Concentration and Product Quality Control

Precision Concentration and Product Quality Control

An evaporation unit provides unmatched precision in liquid concentration, delivering consistent results that meet the strictest industry standards. Advanced sensors and automated control systems within an evaporation unit continuously monitor temperature, pressure, and concentration levels, making real-time adjustments to maintain optimal processing conditions. The evaporation unit ensures that heat-sensitive materials like pharmaceutical compounds, dairy products, and botanical extracts maintain their integrity and nutritional value throughout the concentration process. Companies using an evaporation unit can achieve exact concentration targets, eliminating batch variations that compromise product consistency. The sealed evaporation unit design prevents contamination and oxidation, protecting valuable compounds from degradation. An evaporation unit's precise control mechanisms allow operators to process diverse materials with different viscosities and thermal sensitivities without compromising quality. The evaporation unit reduces the risk of product loss due to overheating or improper processing, protecting valuable raw materials and maximizing yield. With an evaporation unit, manufacturers achieve higher product grades, commanding premium market prices. The reliability of an evaporation unit means customers receive consistently superior products batch after batch.
Durable Construction and Low Maintenance Requirements

Durable Construction and Low Maintenance Requirements

An evaporation unit is constructed from premium stainless steel and corrosion-resistant materials engineered to withstand harsh industrial environments and aggressive processing conditions. The robust design of an evaporation unit ensures extended service life spanning fifteen to twenty years with proper maintenance protocols. An evaporation unit features modular components that simplify repairs and replacements, minimizing production downtime when maintenance becomes necessary. The durable evaporation unit construction resists chemical corrosion, scaling, and mechanical wear, maintaining performance integrity throughout its operational lifespan. Companies benefit from an evaporation unit's low maintenance requirements, which significantly reduce long-term ownership costs compared to equipment requiring frequent repairs. The evaporation unit's self-cleaning capabilities and anti-fouling technologies prevent material buildup inside processing chambers, extending intervals between deep maintenance cycles. The sealed, enclosed design of an evaporation unit protects internal components from environmental contamination and reduces cleaning frequency. An evaporation unit's straightforward maintenance procedures mean your existing staff can handle routine servicing without specialized technical training. Choosing an evaporation unit represents a wise long-term investment that delivers reliable performance and minimal operational disruptions.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000