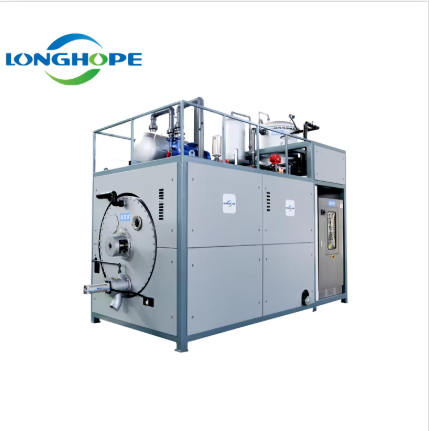
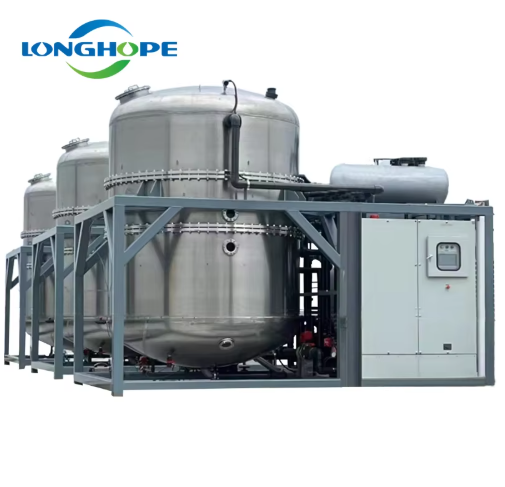
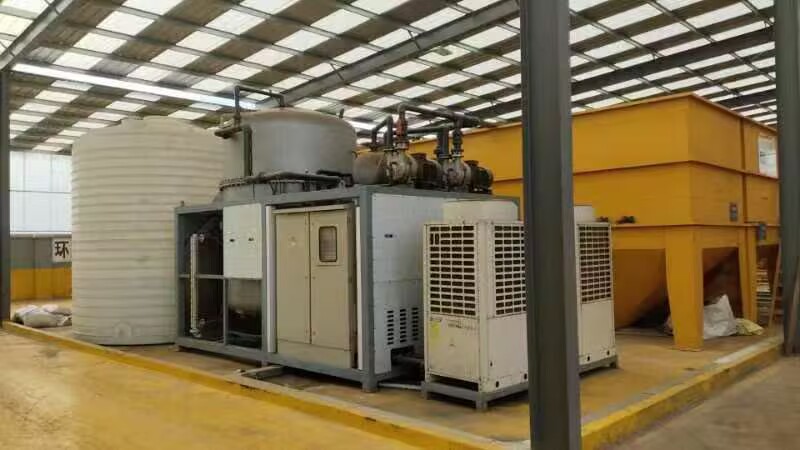
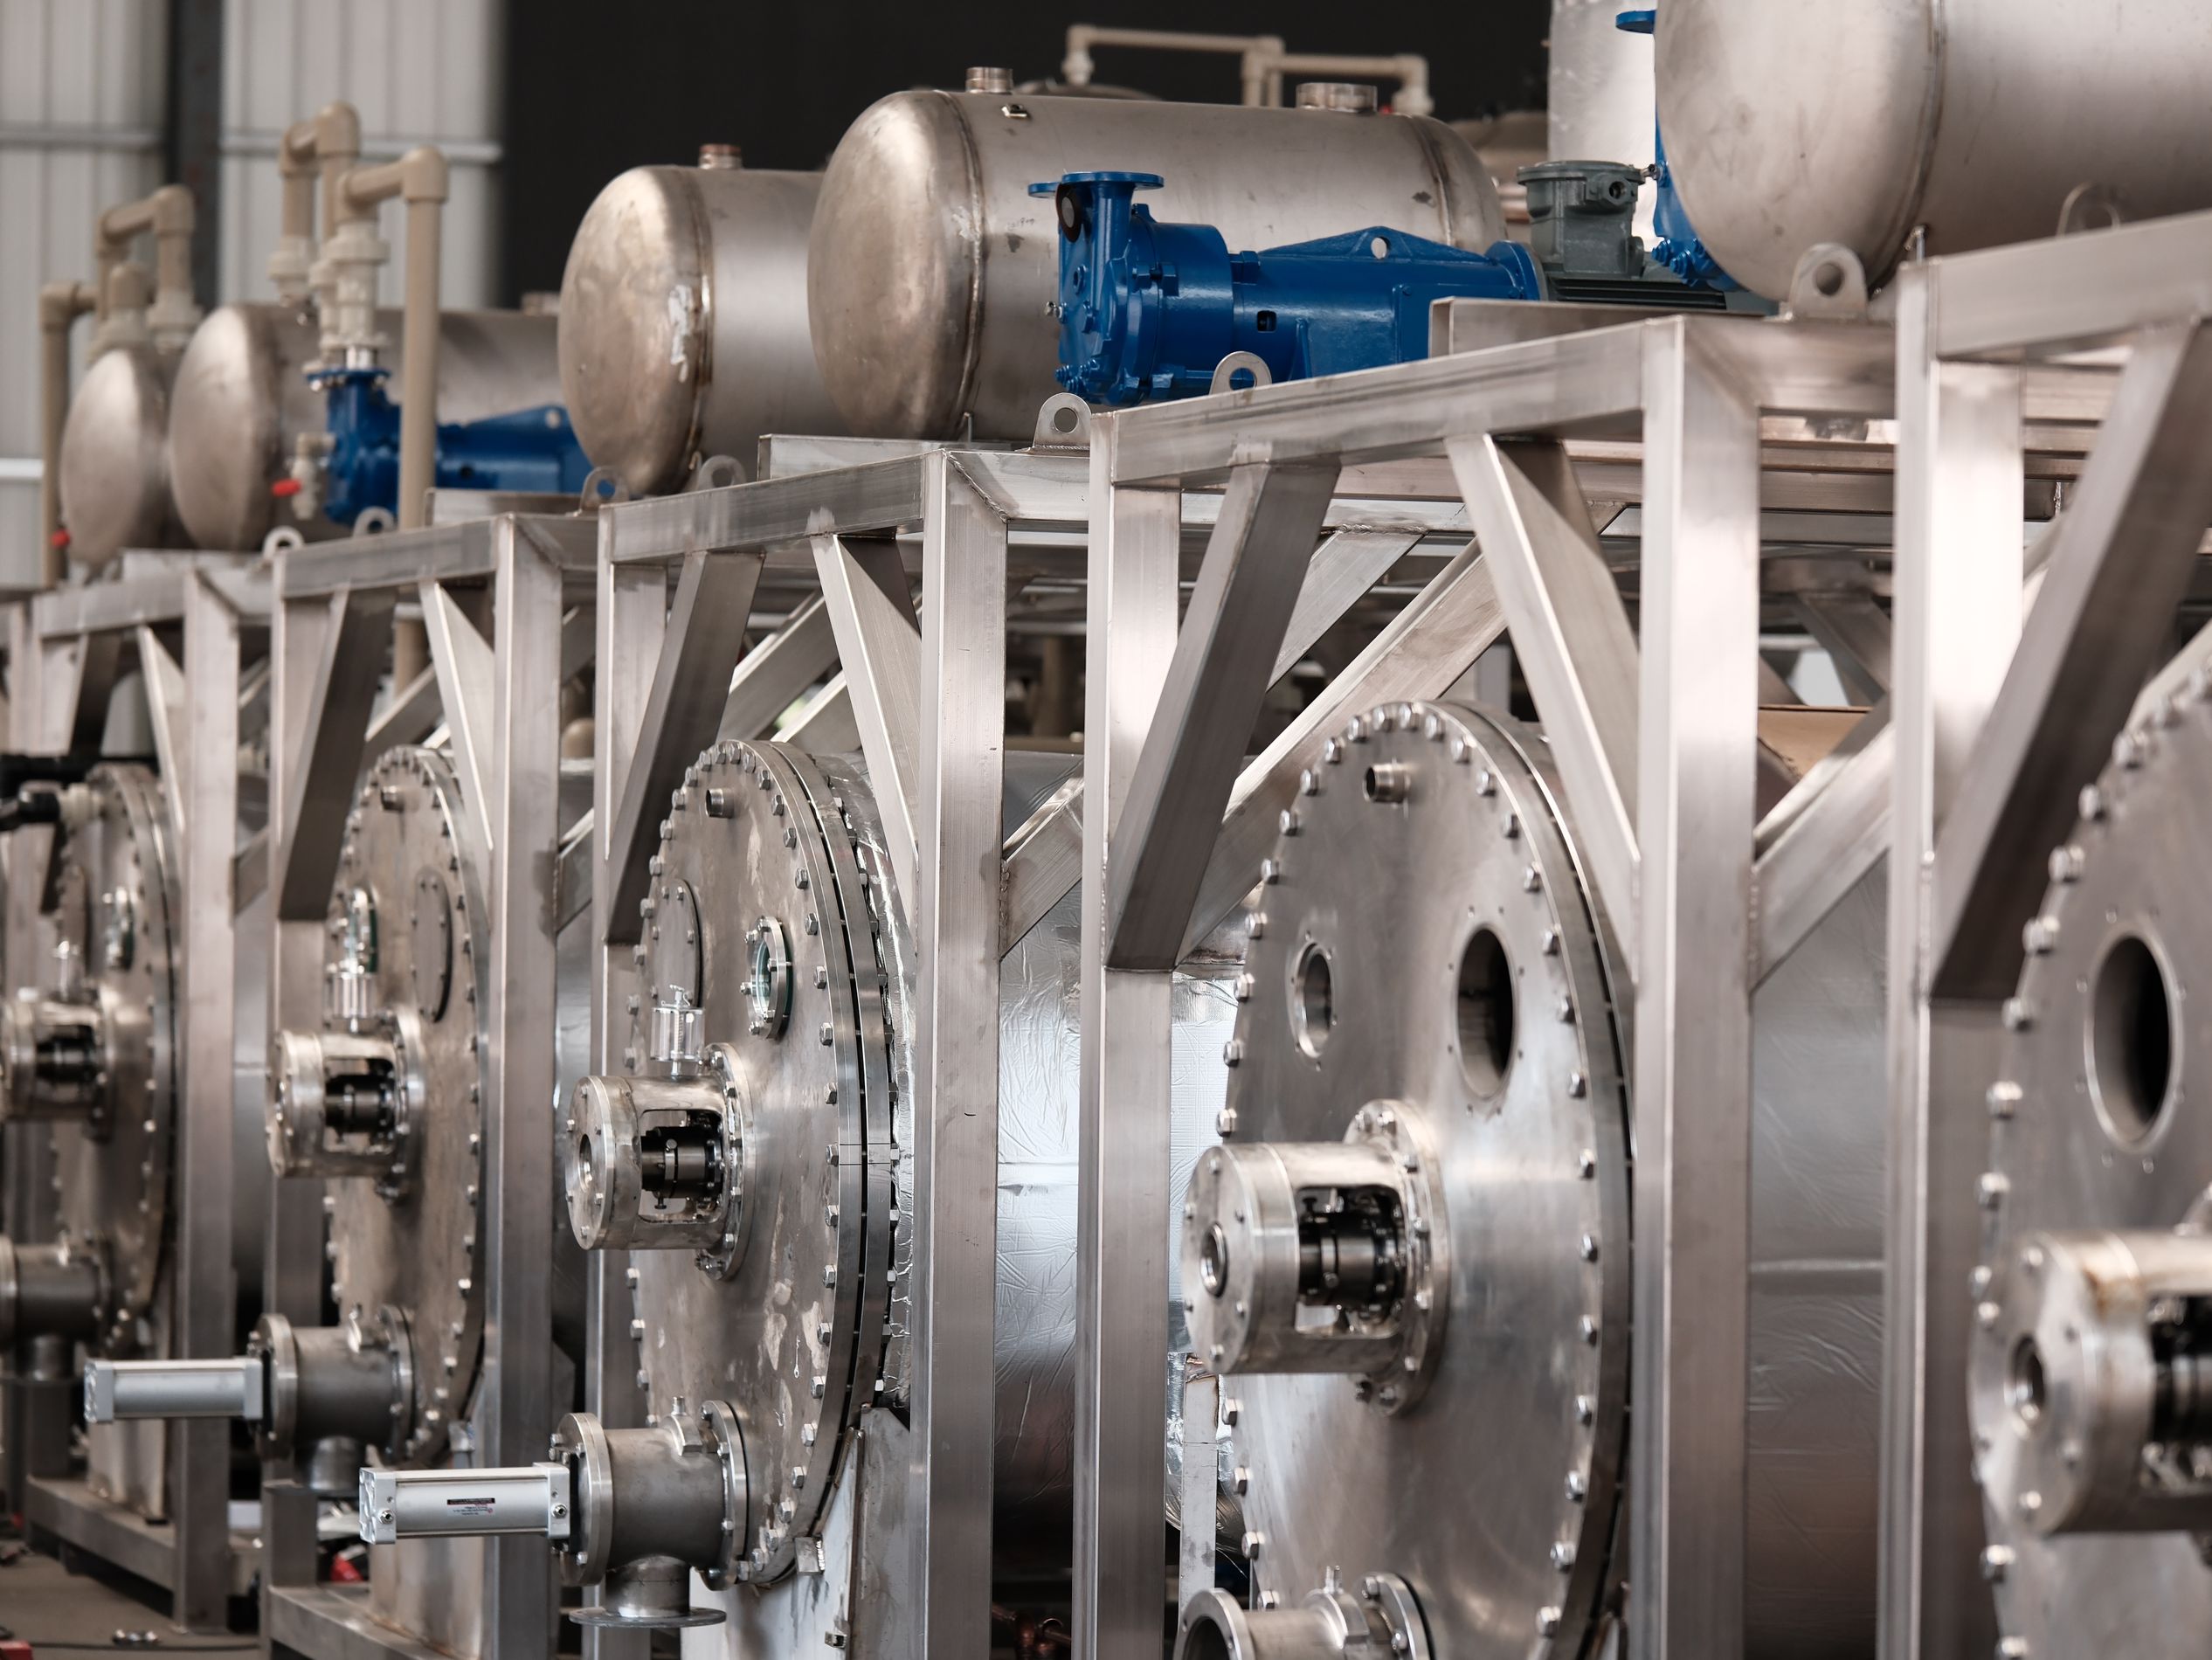
industrial vacuum evaporation unit
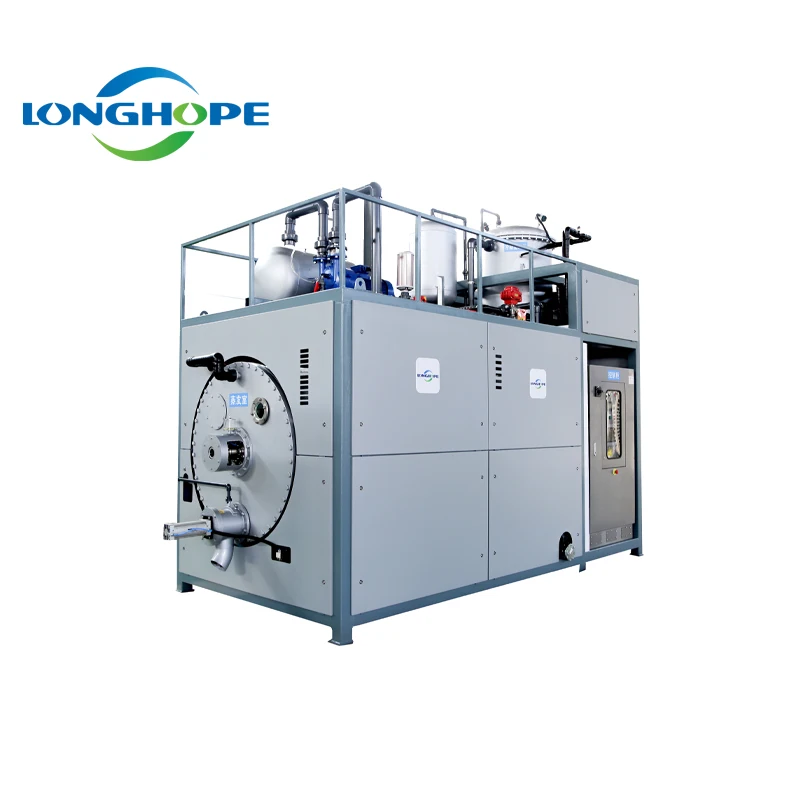
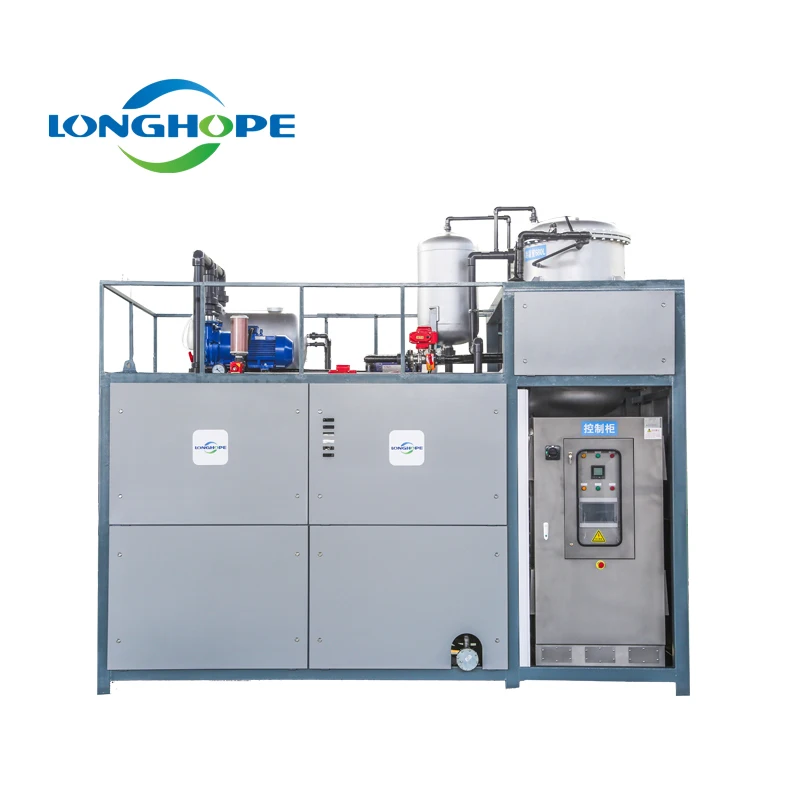
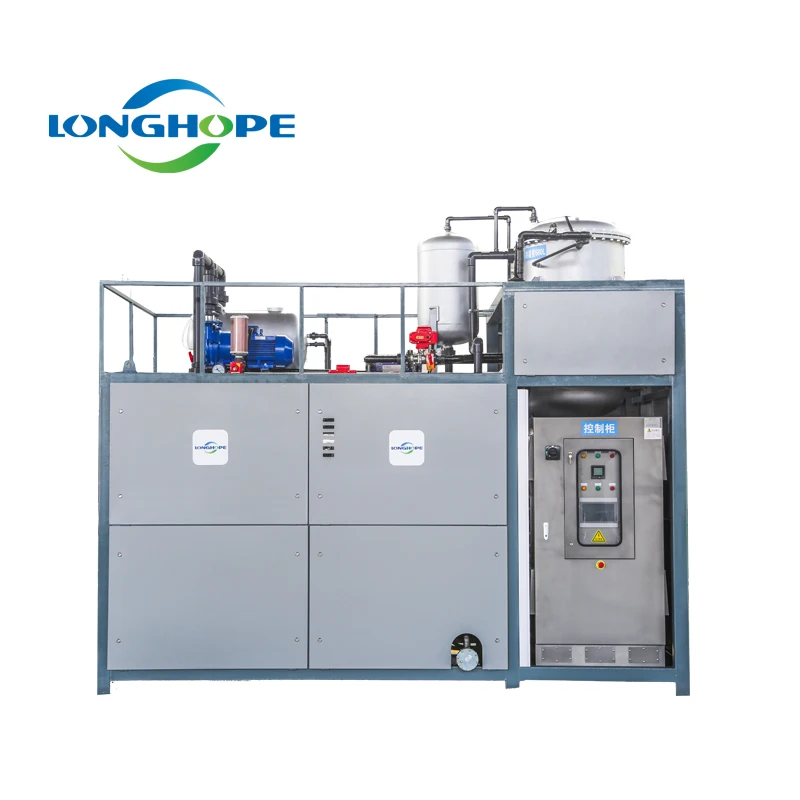
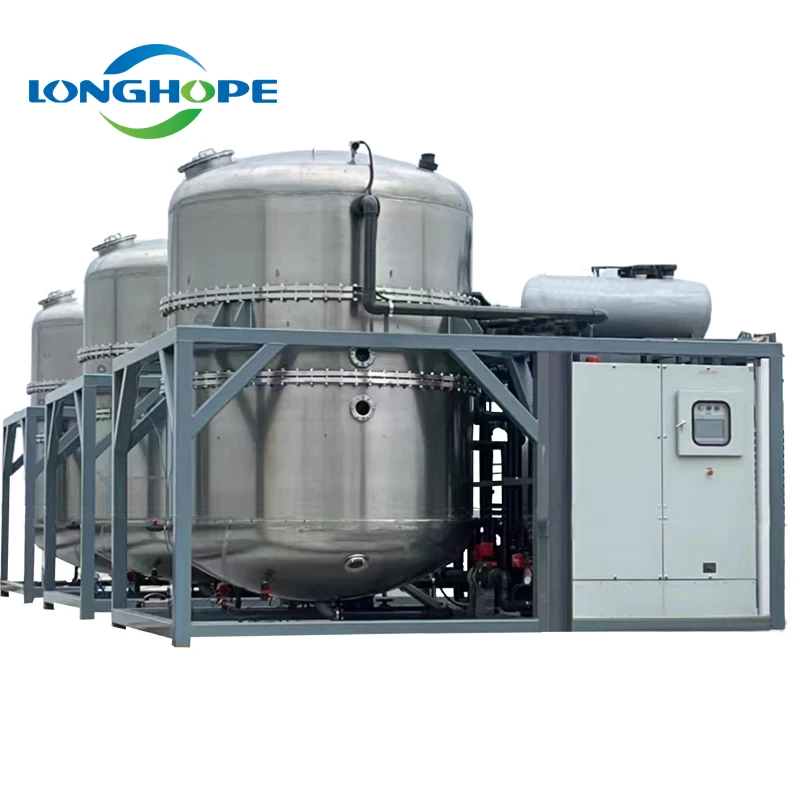
An industrial vacuum evaporation unit represents a sophisticated solution for liquid separation and concentration processes across manufacturing sectors. This advanced equipment operates by reducing pressure within a sealed chamber, allowing liquids to evaporate at lower temperatures than conventional methods. The industrial vacuum evaporation unit utilizes heat exchangers, condensers, and vacuum pumps to efficiently remove solvents, water, or other volatile components from industrial solutions.
The core functionality of an industrial vacuum evaporation unit involves heating liquid feed materials while maintaining reduced atmospheric pressure. This combination enables rapid evaporation without thermal degradation of heat-sensitive compounds. The system captures evaporated vapors in condensers, where they transform back into liquid form for collection or recycling.
Key technological features include automated control systems, energy-efficient heat recovery mechanisms, and customizable chamber configurations. Modern industrial vacuum evaporation unit designs incorporate digital monitoring for temperature, pressure, and flow rates, ensuring consistent output quality. The equipment handles diverse liquid compositions, from pharmaceutical solutions to chemical waste streams and food processing byproducts.
Applications span multiple industries including pharmaceuticals, chemicals, food processing, waste management, and manufacturing. An industrial vacuum evaporation unit proves invaluable for concentrating valuable solutions, recovering solvents, reducing waste volumes, and producing purified end products. Industries rely on this technology to meet environmental regulations while recovering material costs through solvent recycling and waste reduction.

 EN