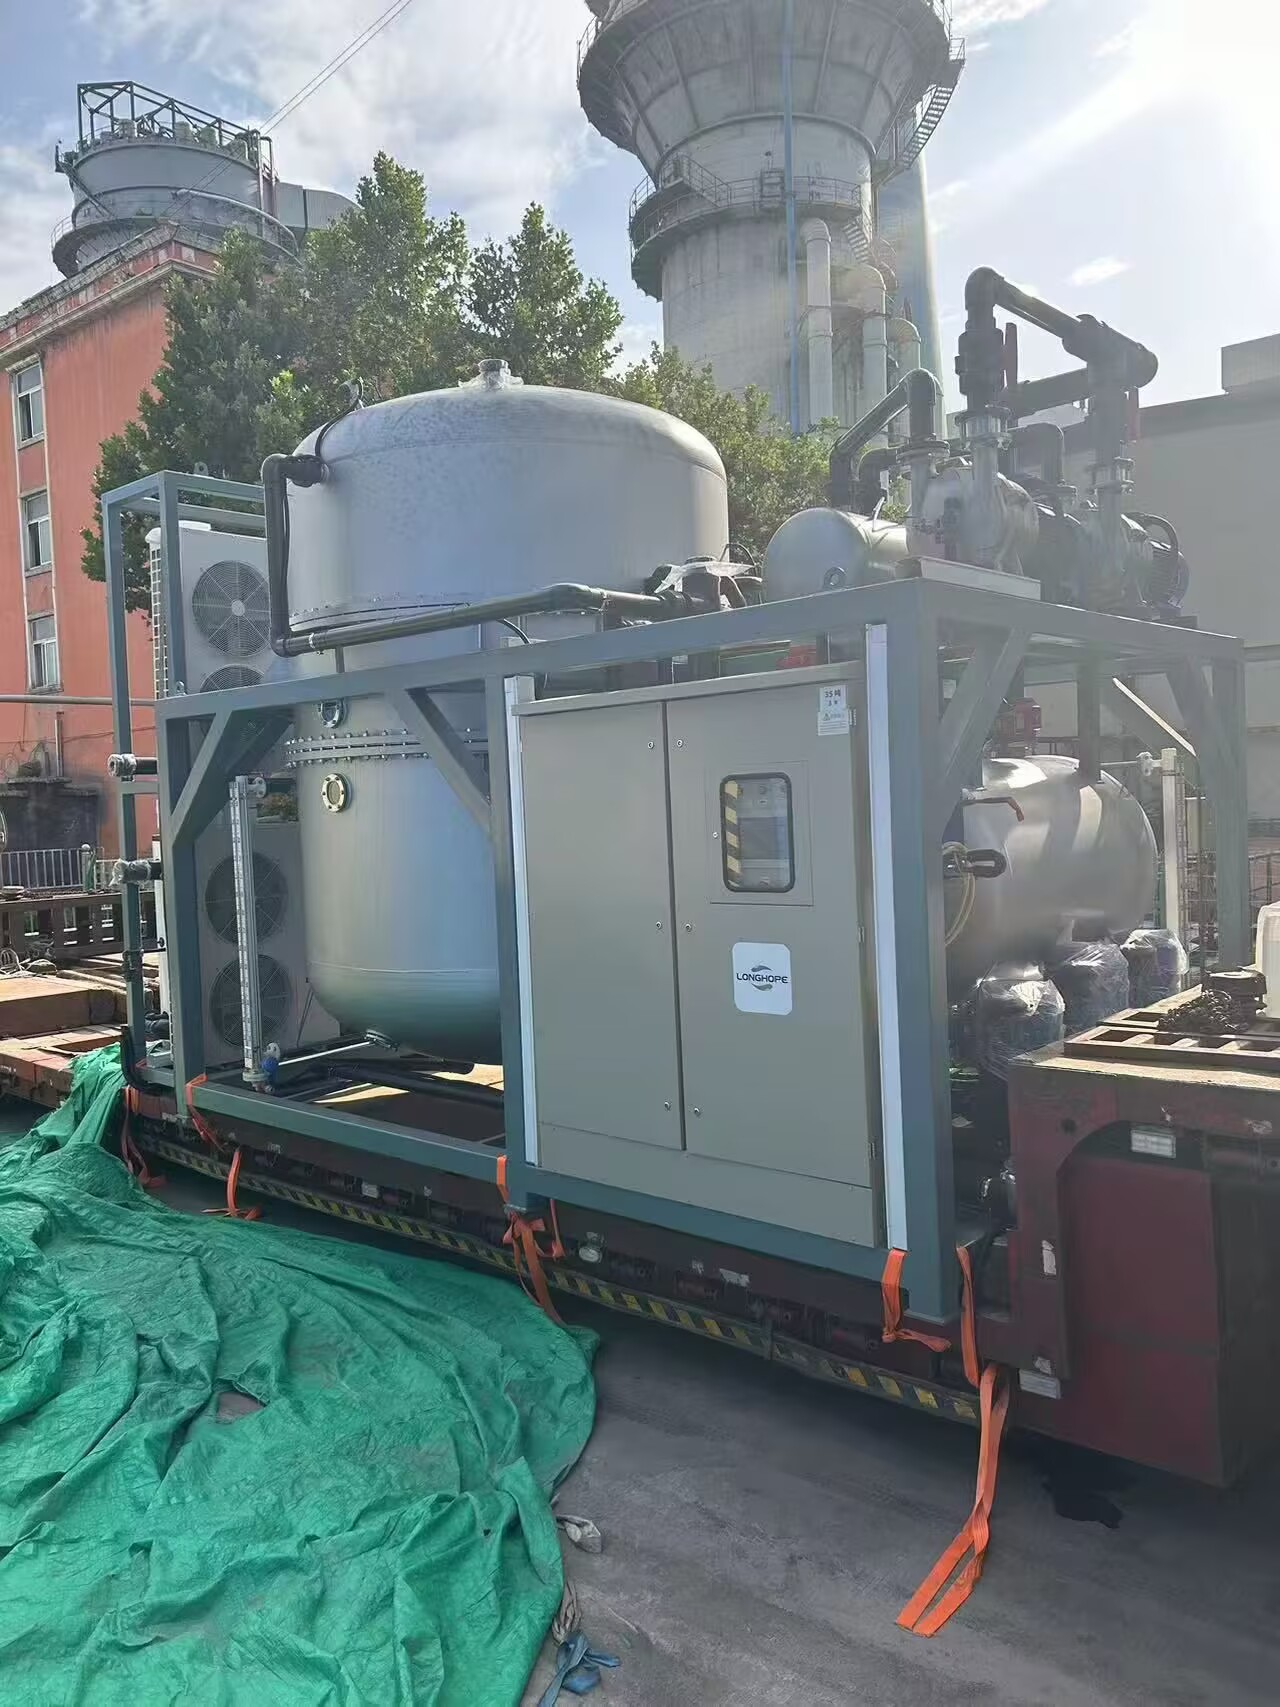
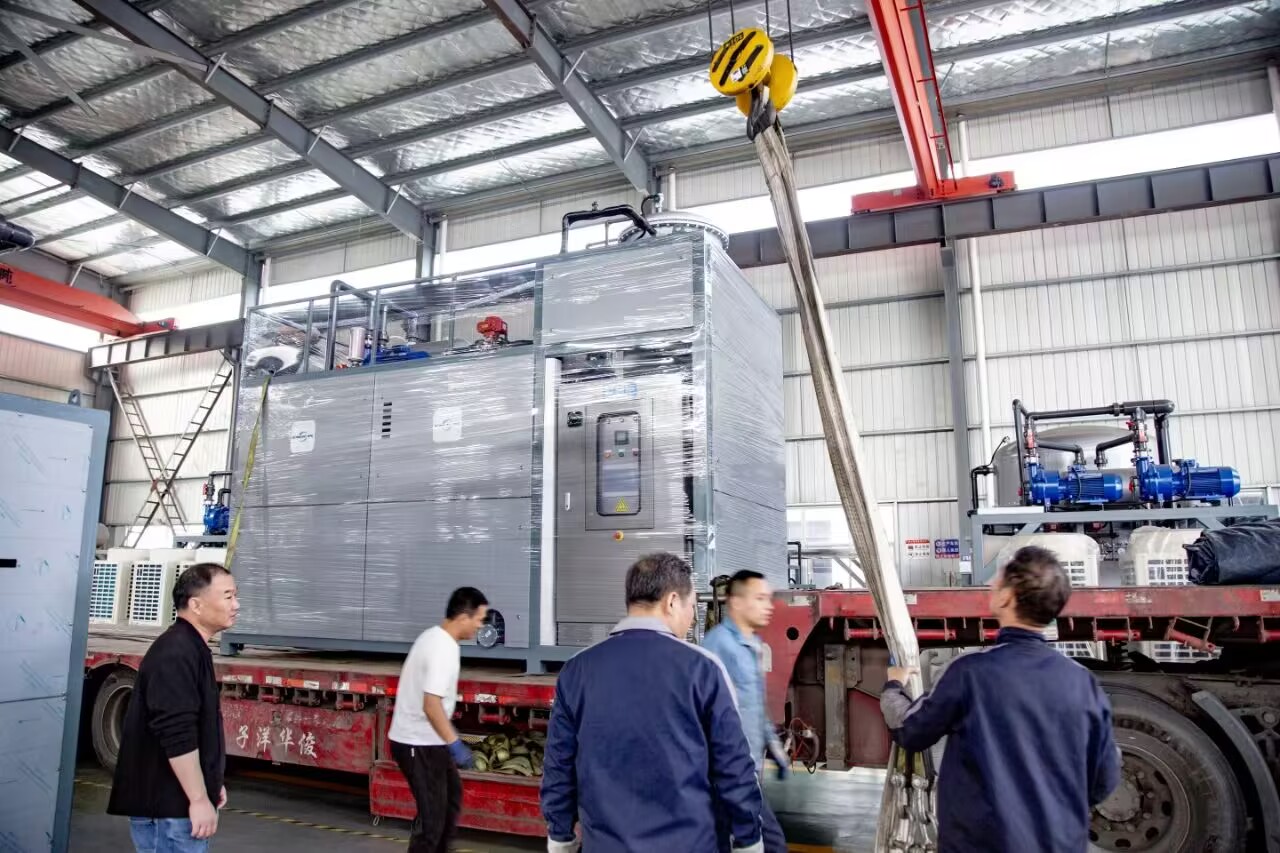
Industrial Vacuum Distillation Equipment

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

industrial vacuum distillation equipment

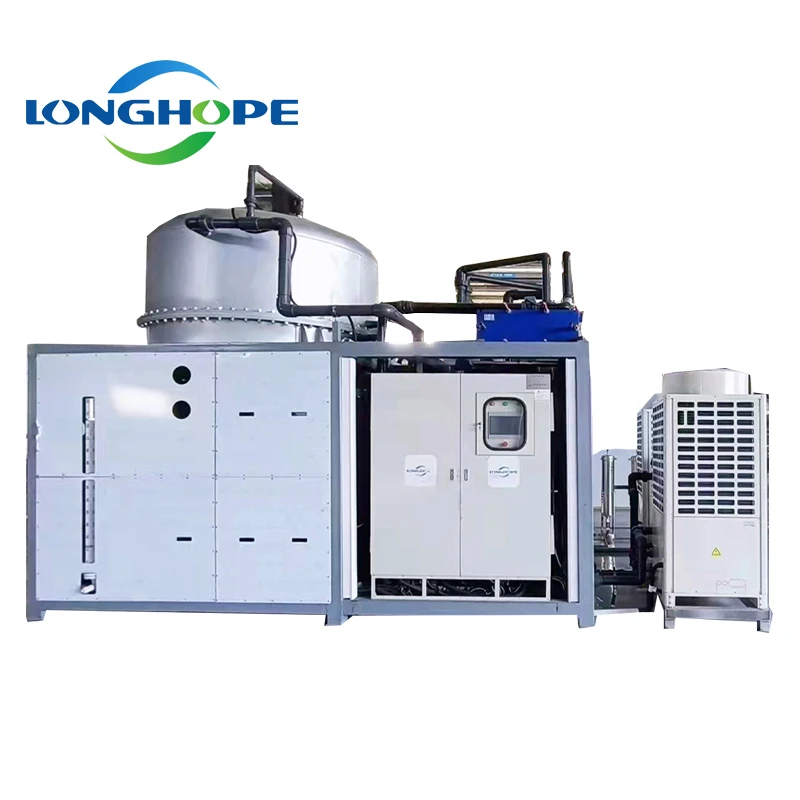
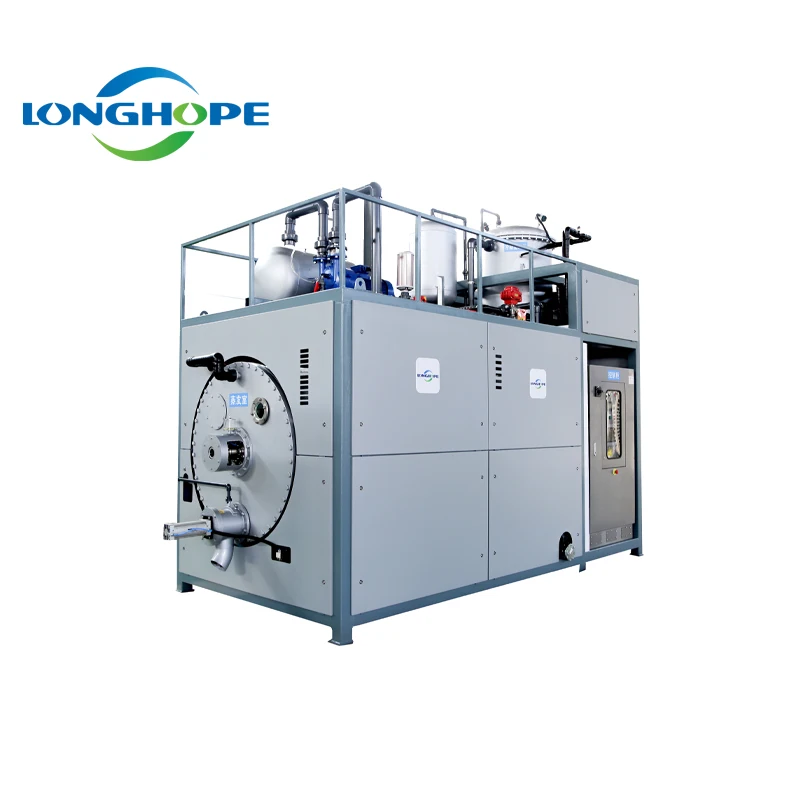
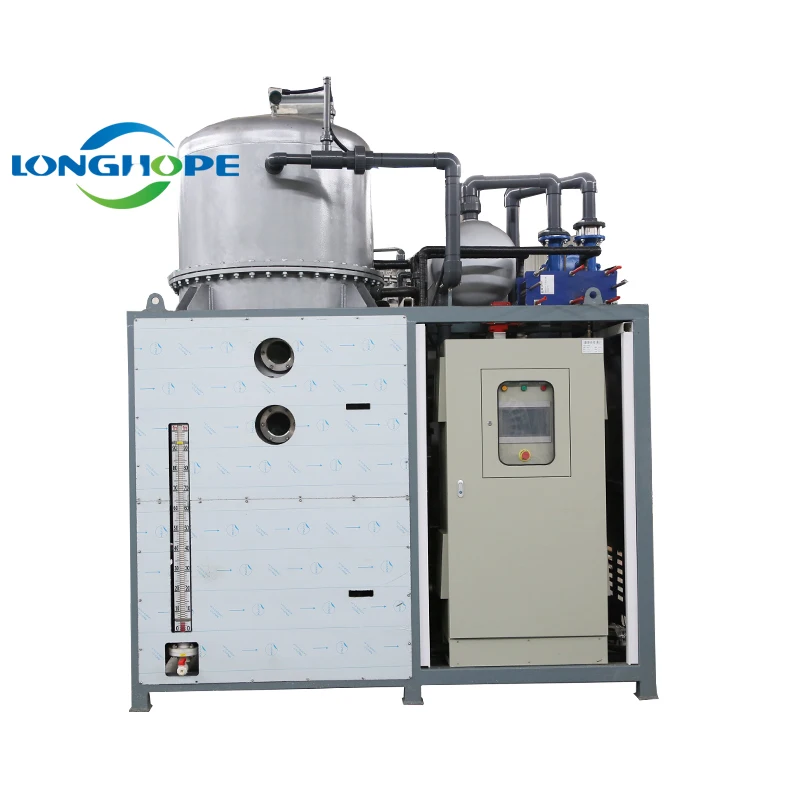
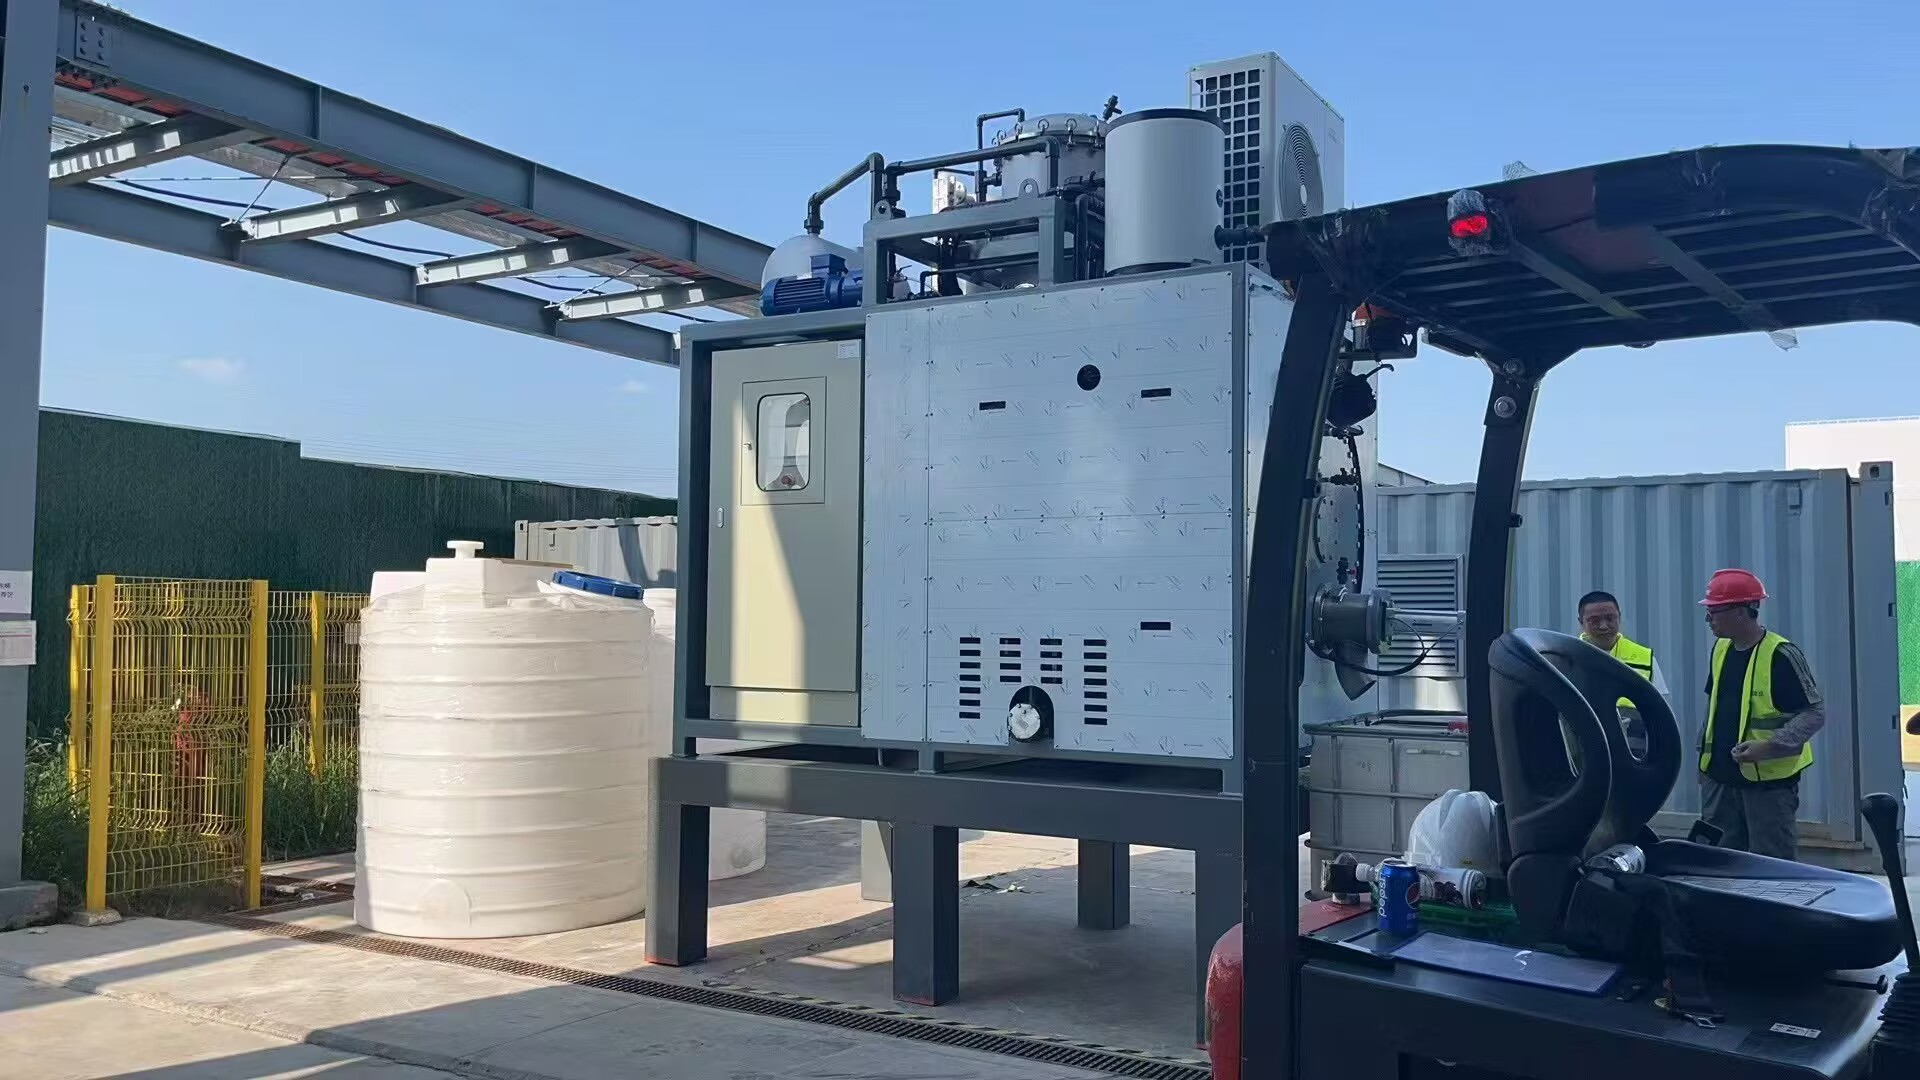
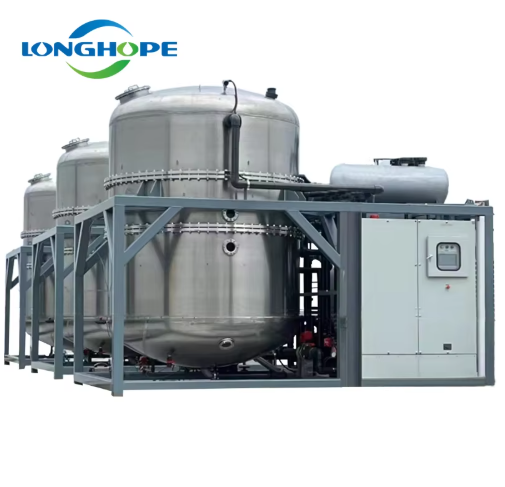
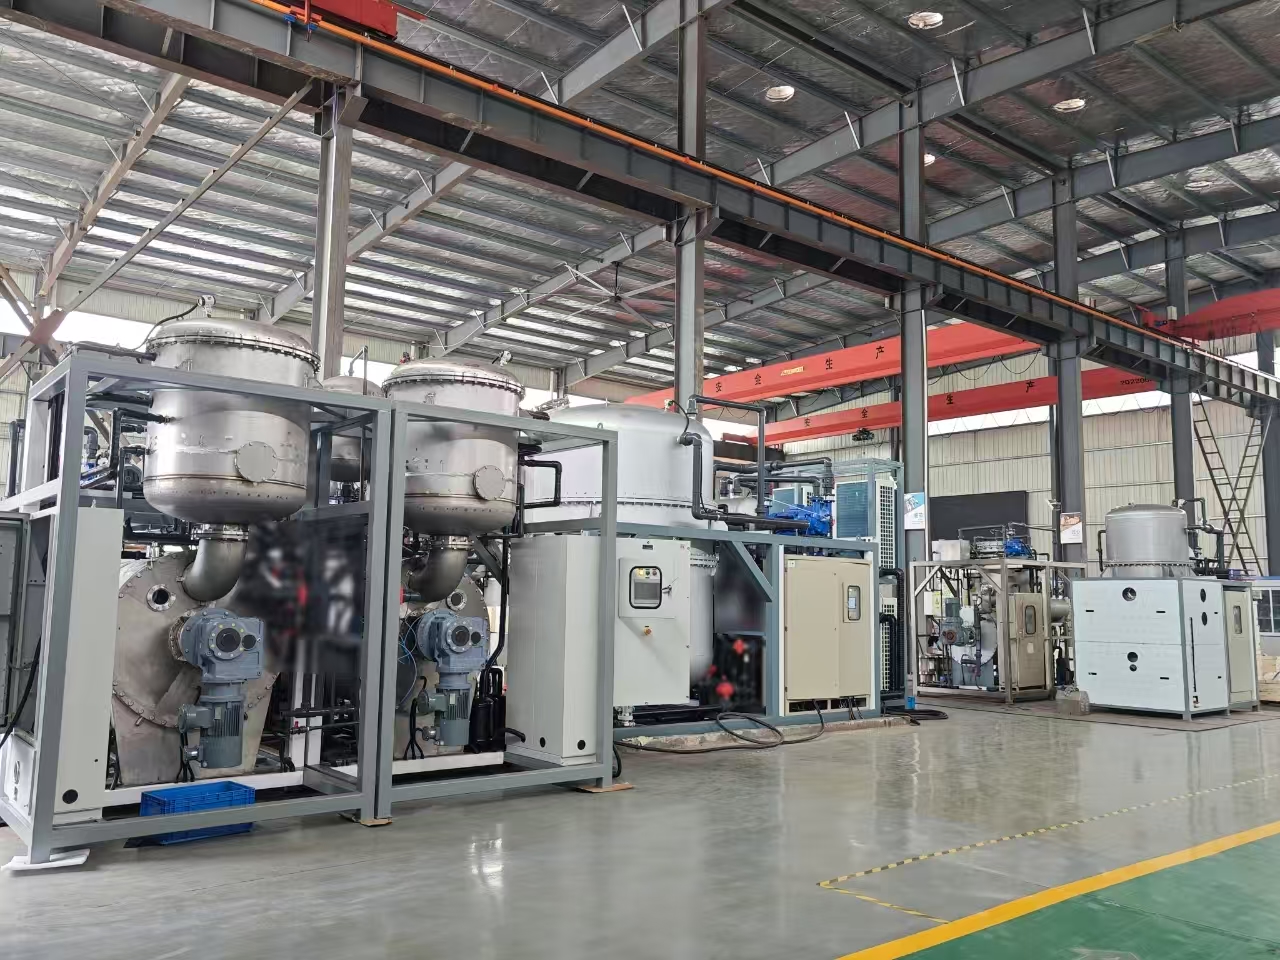
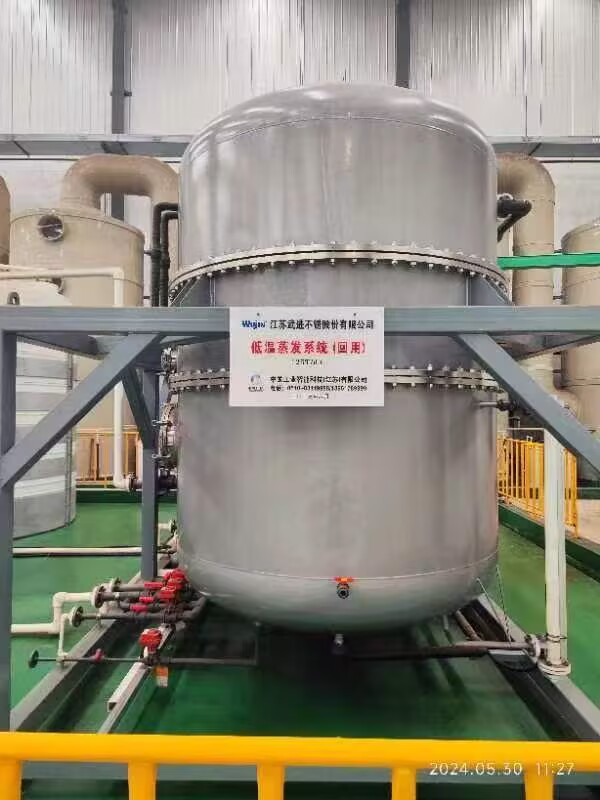
Industrial vacuum distillation equipment represents a cutting-edge solution for separating and purifying liquid mixtures through reduced-pressure evaporation processes. This specialized machinery operates by lowering atmospheric pressure within a sealed chamber, allowing volatile components to evaporate at significantly lower temperatures than conventional distillation methods would require. The primary function of industrial vacuum distillation equipment is to achieve precise separation of temperature-sensitive materials without causing thermal degradation. By reducing pressure, the equipment lowers boiling points, making it ideal for processing heat-sensitive compounds such as essential oils, pharmaceuticals, and specialty chemicals. The industrial vacuum distillation equipment performs continuous or batch operations depending on production requirements. Technologically, industrial vacuum distillation equipment incorporates advanced vacuum pumps, condensers, collection vessels, and automated control systems. These components work synergistically to maintain optimal pressure levels and temperature conditions throughout the distillation cycle. Modern systems feature digital monitoring, real-time pressure adjustment, and safety mechanisms to protect operators and equipment. Applications span multiple industries including pharmaceuticals, cosmetics, food processing, and petrochemicals. The industrial vacuum distillation equipment excels in recovering valuable compounds, removing unwanted substances, and producing high-purity end products. Whether processing natural extracts or synthetic chemicals, this equipment delivers consistent results with minimal product loss and maximum efficiency for demanding industrial operations.

New Product Recommendations

Industrial vacuum distillation equipment delivers substantial practical benefits that directly improve operational efficiency and product quality for manufacturing businesses. The primary advantage lies in its ability to process heat-sensitive materials without thermal degradation, enabling companies to recover valuable compounds that traditional distillation methods would destroy. Operationally, industrial vacuum distillation equipment significantly reduces energy consumption by requiring lower operating temperatures. This translates directly into reduced utility costs and improved profitability for facilities running continuous production schedules. The equipment also accelerates separation processes compared to conventional methods, increasing throughput and maximizing production capacity within existing facility constraints. For potential customers, industrial vacuum distillation equipment provides superior product purity and consistency. The controlled low-temperature environment preserves product integrity, resulting in higher-quality end products that command premium market prices. This quality assurance becomes crucial for pharmaceutical and cosmetic applications where regulatory compliance demands specific purity standards. Application suitability extends across diverse industries requiring delicate separation processes. Companies processing botanical extracts, specialty oils, or pharmaceutical precursors find industrial vacuum distillation equipment indispensable for maintaining compound integrity. The equipment's versatility accommodates various feedstock types and viscosities without requiring major modifications. From a business decision perspective, investing in industrial vacuum distillation equipment represents a strategic advantage. The technology reduces material waste, improves product yields, and enables processing of previously challenging compounds. Long-term operational reliability combined with lower maintenance requirements compared to alternative separation technologies makes this equipment a financially sound investment for growth-focused manufacturers.

Latest News

How to Optimize Your Evaporator System for Efficiency

24

Jul

How to Optimize Your Evaporator System for Efficiency

An evaporator system efficiency directly impacts your operational costs, production capacity, and environmental footprint in industrial processing. Whether you operate in chemical manufacturing, food processing, pharmaceutical production, or waste ma...
View More
How Low Temperature Heat Pump Evaporator Cuts Energy Costs

24

Jul

How Low Temperature Heat Pump Evaporator Cuts Energy Costs

Industrial operations consume significant energy, and equipment efficiency directly impacts profitability. A low temperature heat pump evaporator represents a transformative approach to reducing energy expenditure while maintaining operational perfor...
View More
Low Temperature Heat Pump Evaporator: Energy Saving Guide

24

Jul

Low Temperature Heat Pump Evaporator: Energy Saving Guide

Industrial facilities continuously seek ways to reduce operational costs while maintaining peak performance. A low temperature heat pump evaporator represents one of the most effective technologies for achieving significant energy savings in thermal ...
View More
Benefits of a Modern Evaporator System for Wastewater

24

Jul

Benefits of a Modern Evaporator System for Wastewater

Modern industrial facilities face mounting pressure to reduce wastewater disposal costs while meeting strict environmental regulations. An evaporator systems for wastewater represents a transformative solution that addresses both operational expenses...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

industrial vacuum distillation equipment

Temperature-Controlled Processing for Heat-Sensitive Materials

Temperature-Controlled Processing for Heat-Sensitive Materials

Industrial vacuum distillation equipment uniquely protects temperature-sensitive compounds by operating at dramatically reduced boiling points. When pressure decreases inside the sealed chamber, volatile substances evaporate without exposure to excessive heat that would cause chemical breakdown or quality degradation. This capability proves invaluable for pharmaceutical manufacturers processing active ingredients, cosmetic producers working with delicate plant extracts, and food companies handling flavor compounds. Traditional distillation exposes these materials to temperatures exceeding 200 degrees Celsius, inevitably causing decomposition. Industrial vacuum distillation equipment maintains operating temperatures often below 60 degrees Celsius while achieving complete separation. This breakthrough technology enables companies to process previously unstable materials safely and reliably, recovering maximum product value. The preserved compound integrity directly results in premium-quality final products meeting strict industry standards. For customers working with heat-sensitive materials, industrial vacuum distillation equipment becomes an essential investment that transforms processing possibilities and competitive market positioning.
Energy Efficiency and Operational Cost Reduction

Energy Efficiency and Operational Cost Reduction

Industrial vacuum distillation equipment substantially reduces energy consumption compared to conventional distillation technologies, delivering measurable cost savings across production operations. The reduced-pressure environment requires significantly lower temperatures for evaporation, minimizing heating system demands and associated utility expenses. Facilities operating industrial vacuum distillation equipment typically report 40-60 percent reductions in energy requirements for equivalent separation volumes. This efficiency advantage compounds over time, representing substantial annual savings for high-volume producers. Lower operating temperatures also extend equipment lifespan and reduce maintenance costs, further improving total cost of ownership. Industrial vacuum distillation equipment qualifies for energy-efficiency incentives in many jurisdictions, providing additional financial benefits. The combination of reduced energy consumption, lower maintenance demands, and extended equipment life makes this investment remarkably cost-effective. Organizations seeking competitive advantage through operational excellence find industrial vacuum distillation equipment delivers measurable financial returns while supporting sustainability objectives and reducing carbon footprints.
Continuous Operation with Automated Monitoring and Control

Continuous Operation with Automated Monitoring and Control

Modern industrial vacuum distillation equipment features sophisticated automation systems enabling continuous operation with minimal human intervention. Advanced control systems monitor pressure, temperature, flow rates, and product specifications in real-time, automatically adjusting parameters to maintain optimal distillation conditions. Operators can program multiple batch sequences, allowing industrial vacuum distillation equipment to execute complex production schedules autonomously throughout extended periods. Digital sensors and automated valves respond instantly to process changes, ensuring consistent product quality and safety. This automation capability reduces labor requirements while dramatically improving operational efficiency and product consistency. Industrial vacuum distillation equipment equipped with remote monitoring capabilities allows supervisory personnel to oversee operations from centralized control centers, enhancing safety and enabling rapid response to any anomalies. The combination of continuous processing capacity and sophisticated automation transforms production workflows, enabling facilities to maximize throughput while maintaining strict quality standards. Companies implementing industrial vacuum distillation equipment experience improved productivity metrics, enhanced workplace safety, and substantially greater production flexibility.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000