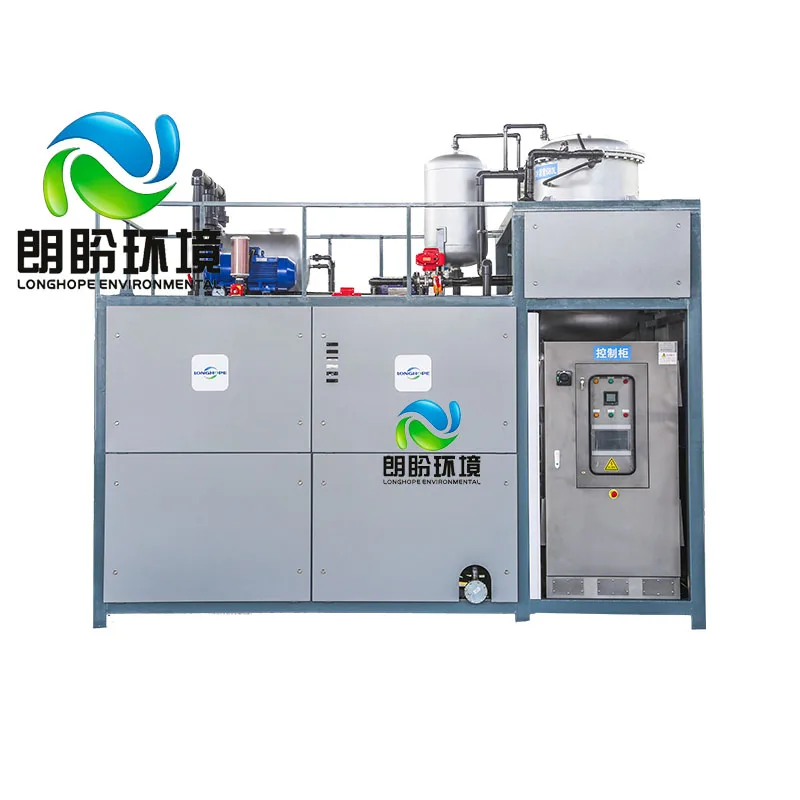
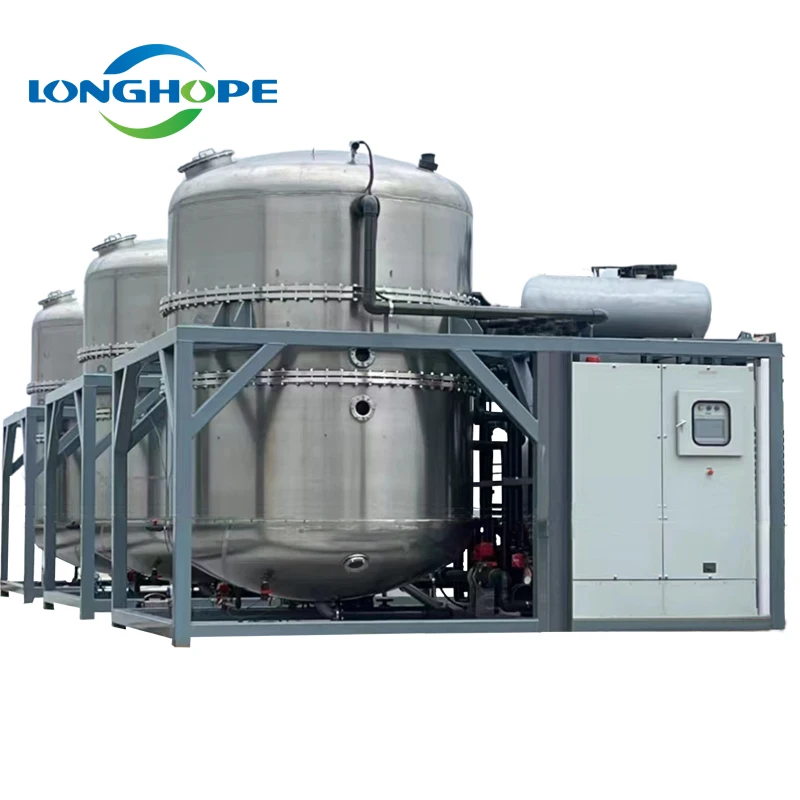
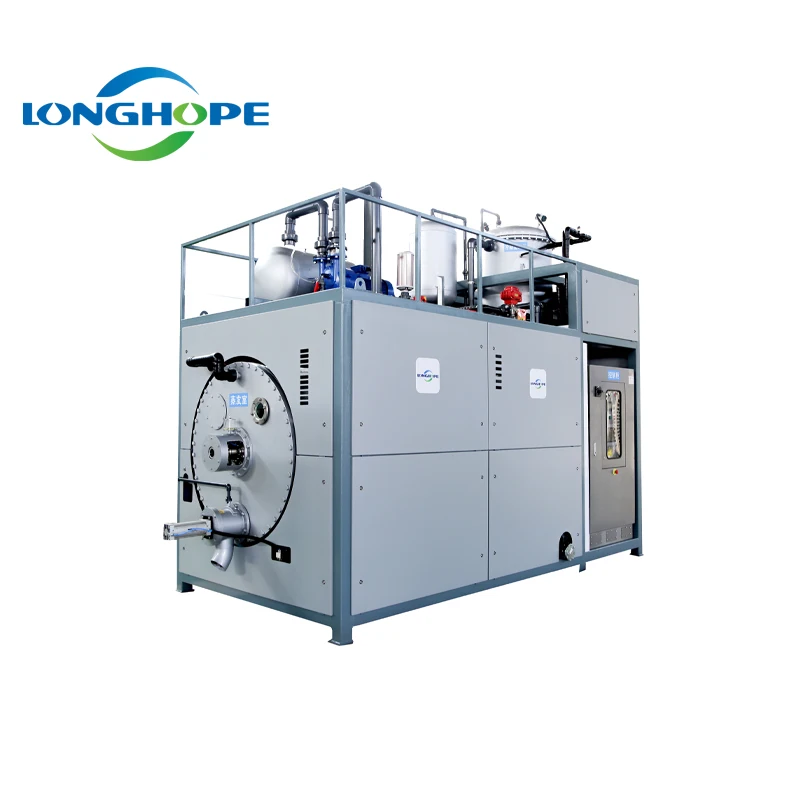
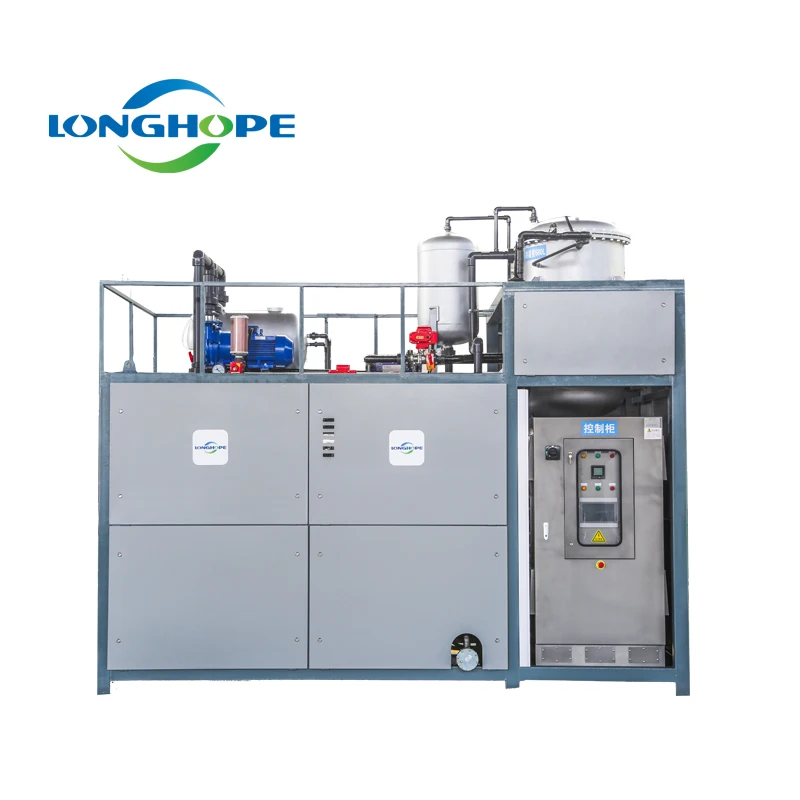
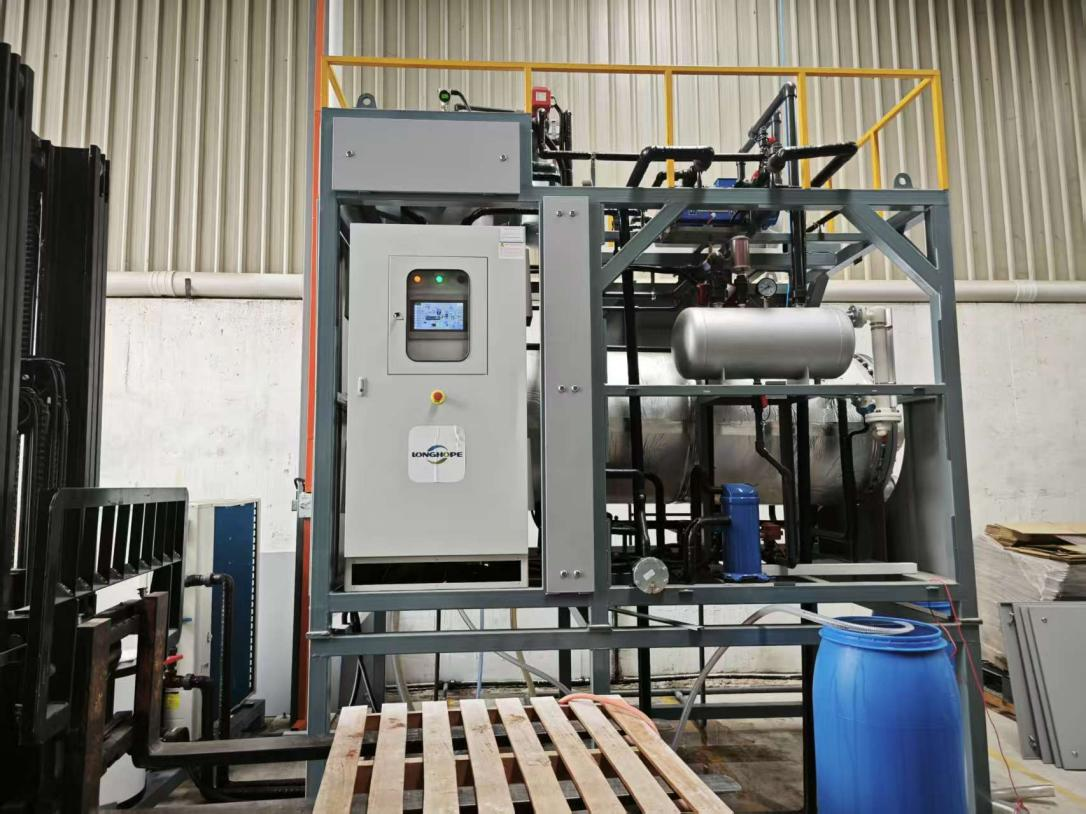
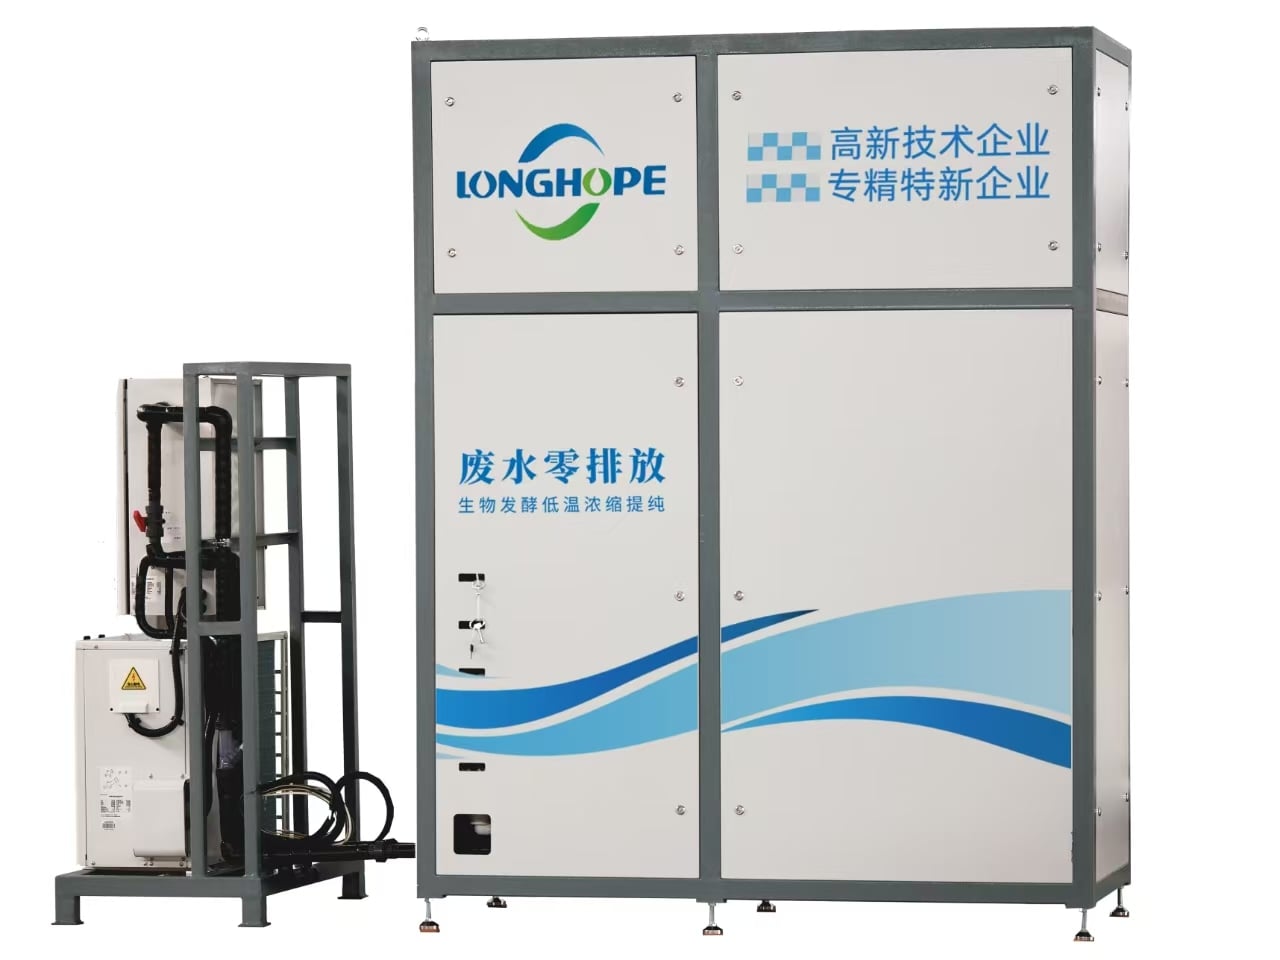
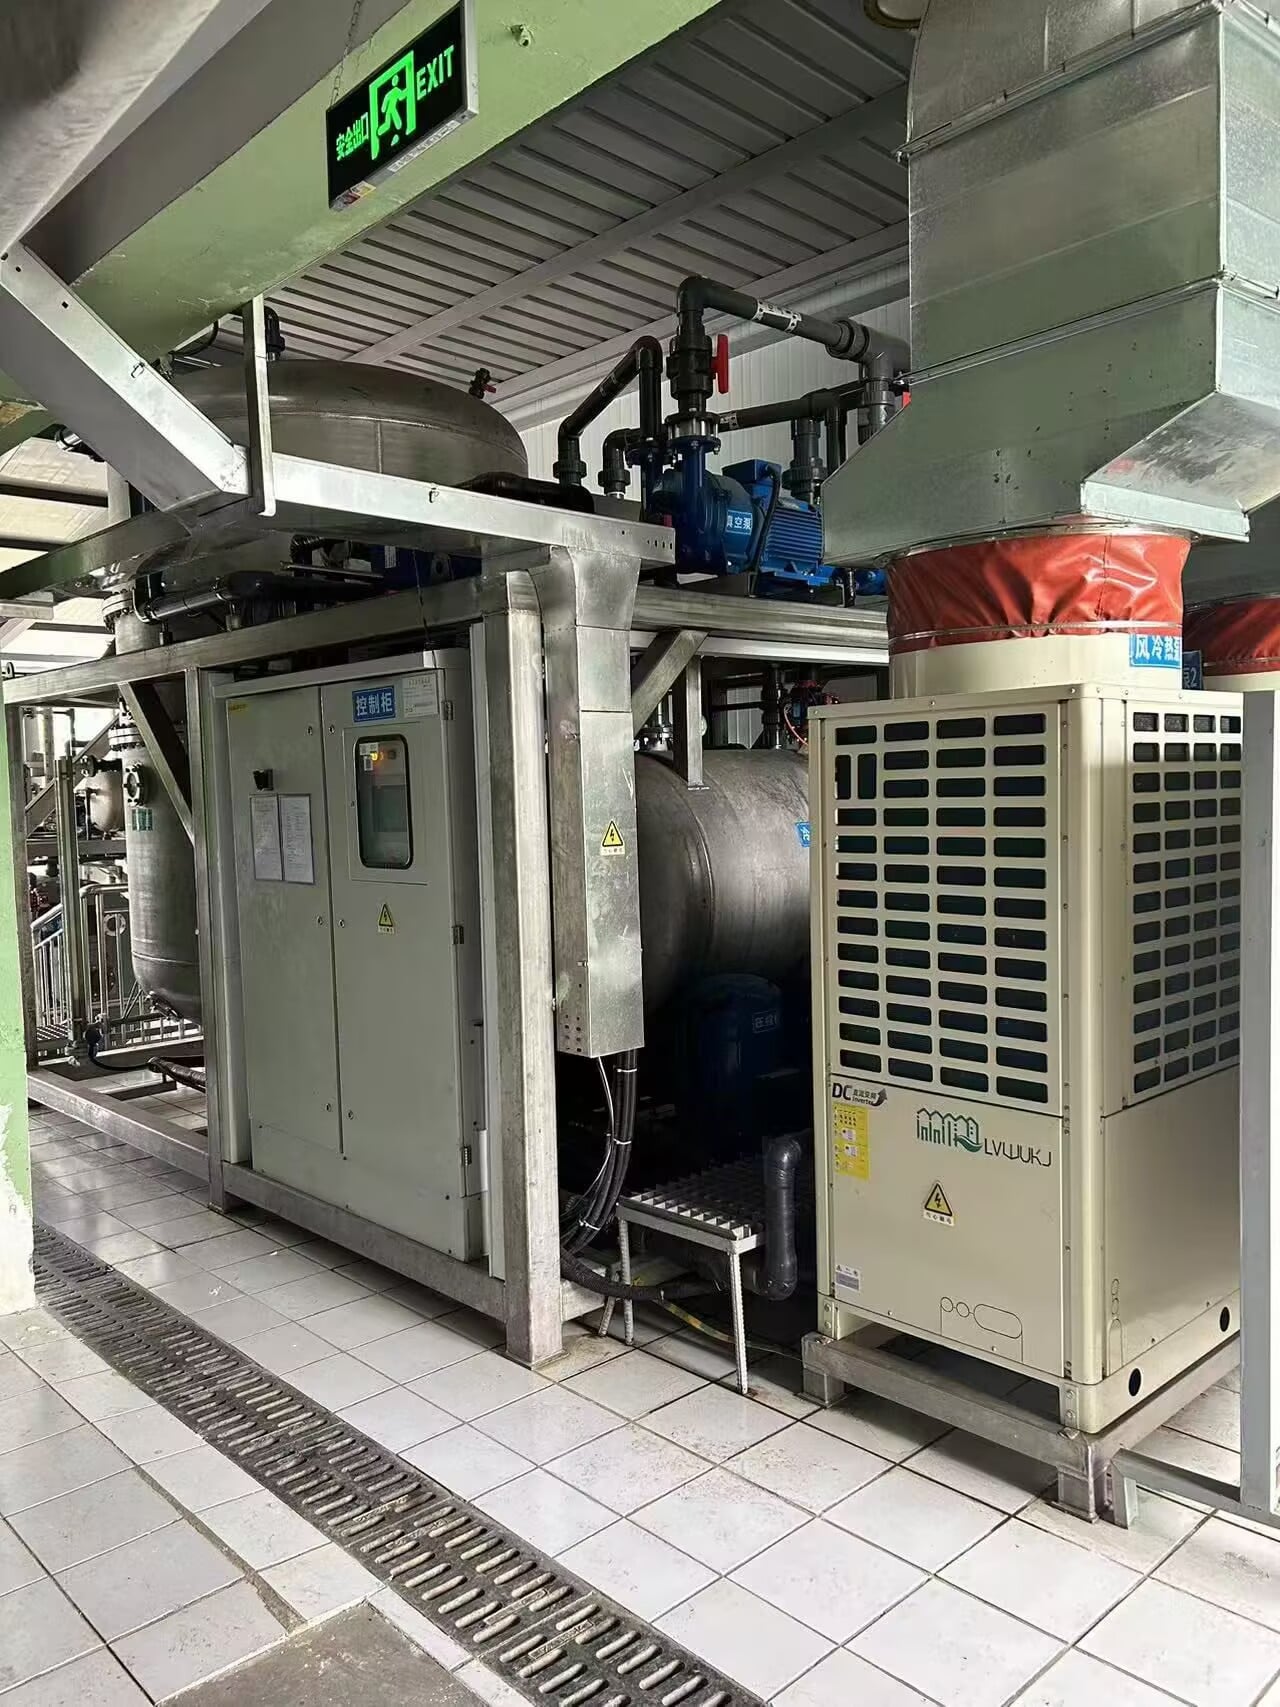
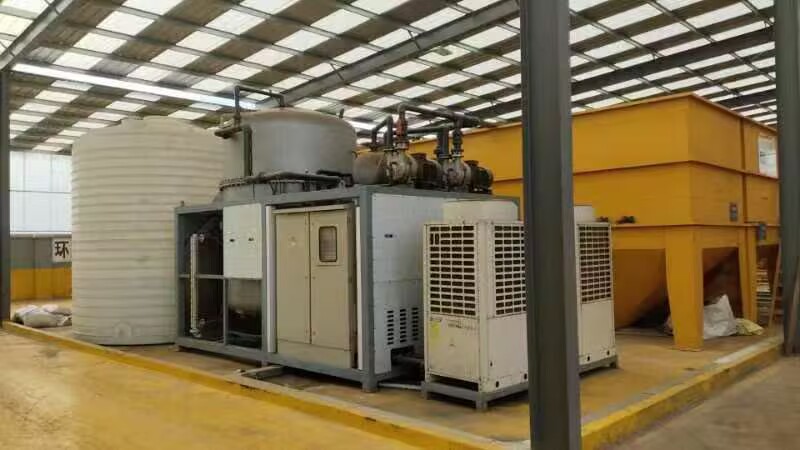
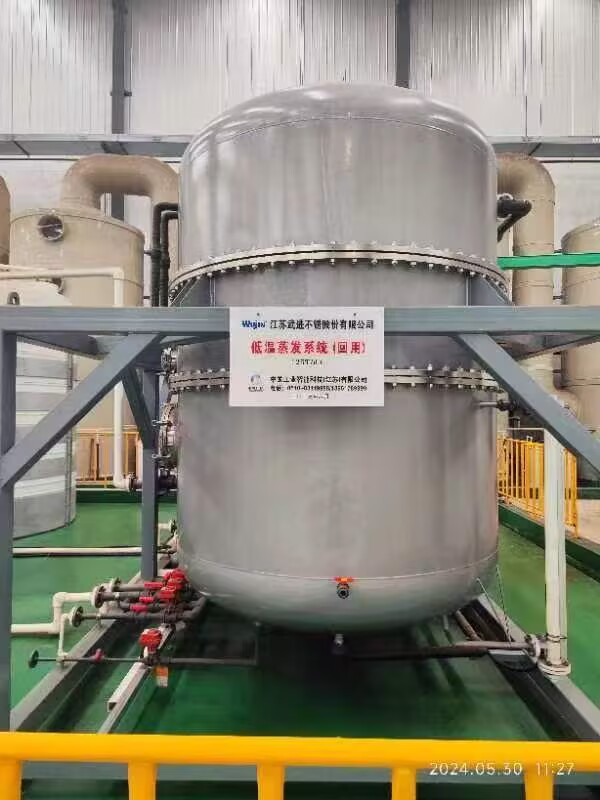
industrial vacuum distillation system
An industrial vacuum distillation system represents a sophisticated separation technology designed to purify and refine liquid compounds at reduced pressure levels. This advanced industrial vacuum distillation system operates by lowering atmospheric pressure within a sealed chamber, which decreases the boiling points of various substances, enabling efficient separation without excessive heat exposure. The primary function of an industrial vacuum distillation system is to separate temperature-sensitive materials, crude oils, and complex hydrocarbon mixtures that would degrade under conventional distillation conditions.
The technological features of an industrial vacuum distillation system include precision vacuum pumps, heated columns, condensation systems, and automated control mechanisms. These components work synergistically to maintain optimal operating conditions while protecting sensitive compounds from thermal degradation. An industrial vacuum distillation system typically incorporates advanced instrumentation for monitoring temperature, pressure, and separation efficiency in real time.
Applications for an industrial vacuum distillation system span multiple industries, including petroleum refining, pharmaceutical manufacturing, chemical processing, food production, and waste recycling. This equipment proves invaluable when processing high-boiling-point materials, essential oils, bitumen products, and specialty chemicals. The industrial vacuum distillation system delivers superior product quality by preventing unwanted chemical reactions caused by excessive heat exposure. Industries increasingly rely on this technology to meet stringent purity standards while maximizing yield from their feedstock materials and reducing operational waste significantly.

 EN