Industrial Vacuum Concentration System | Efficient Liquid Processing

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

industrial vacuum concentration system

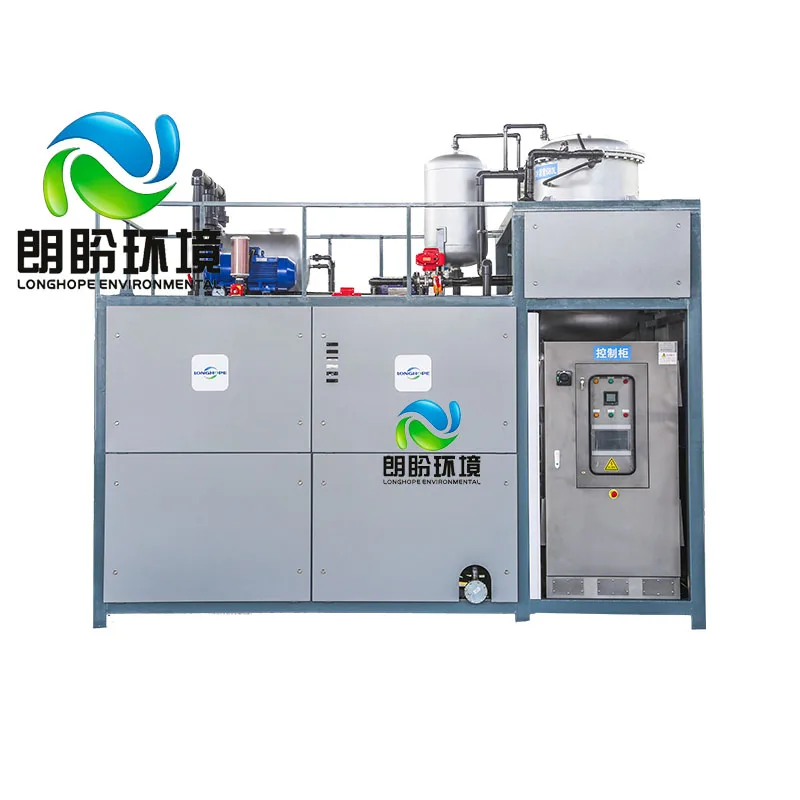
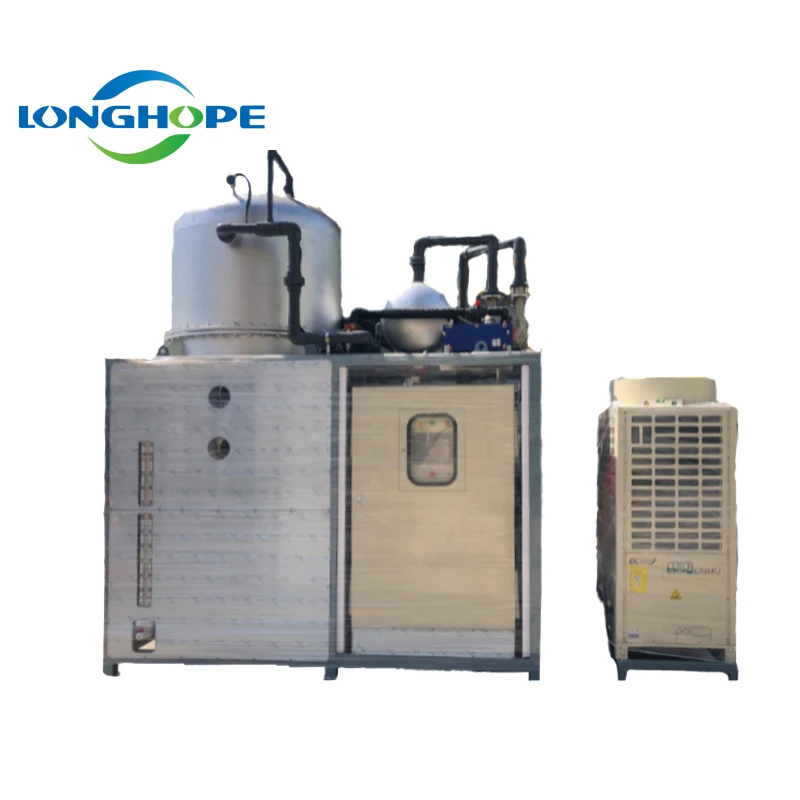
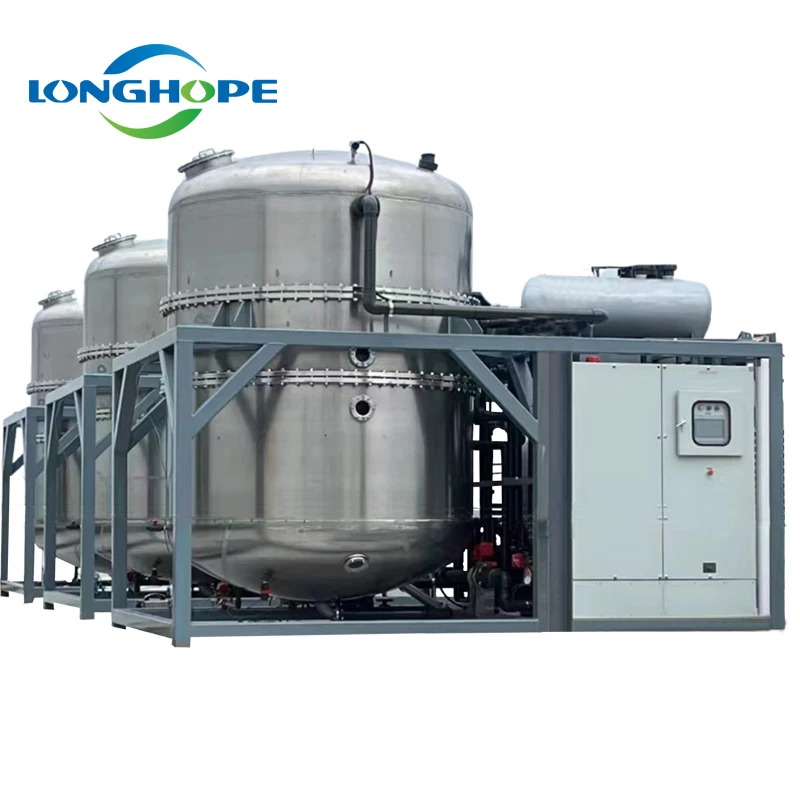
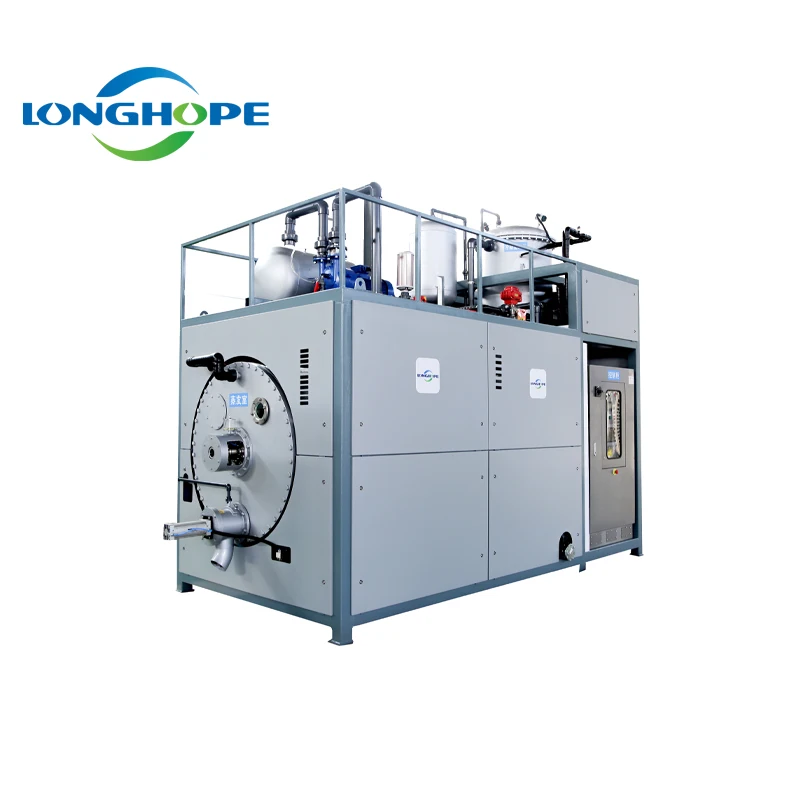
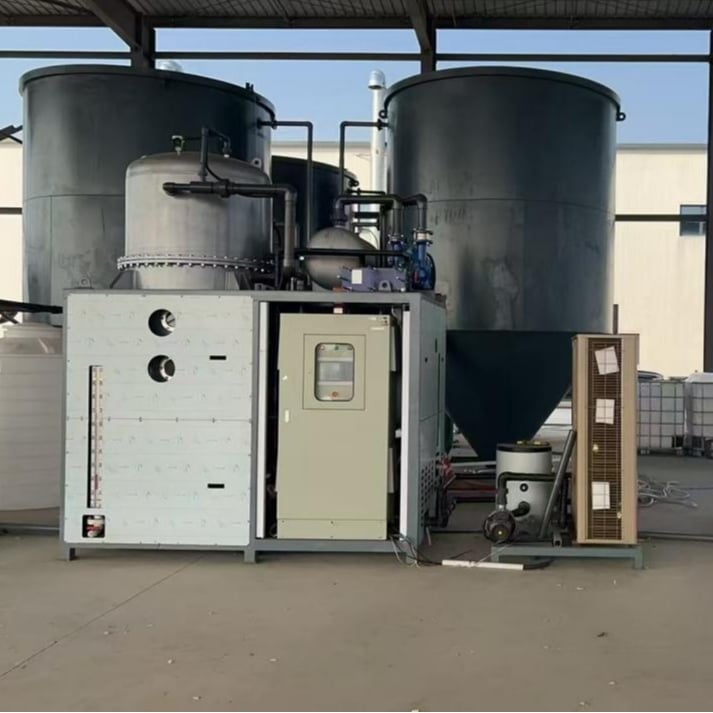
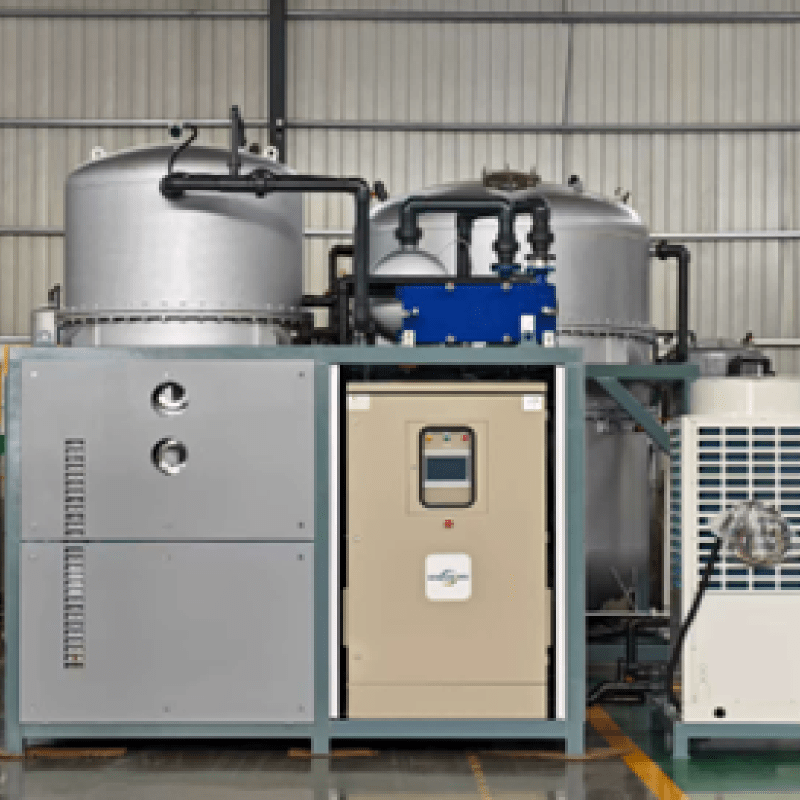
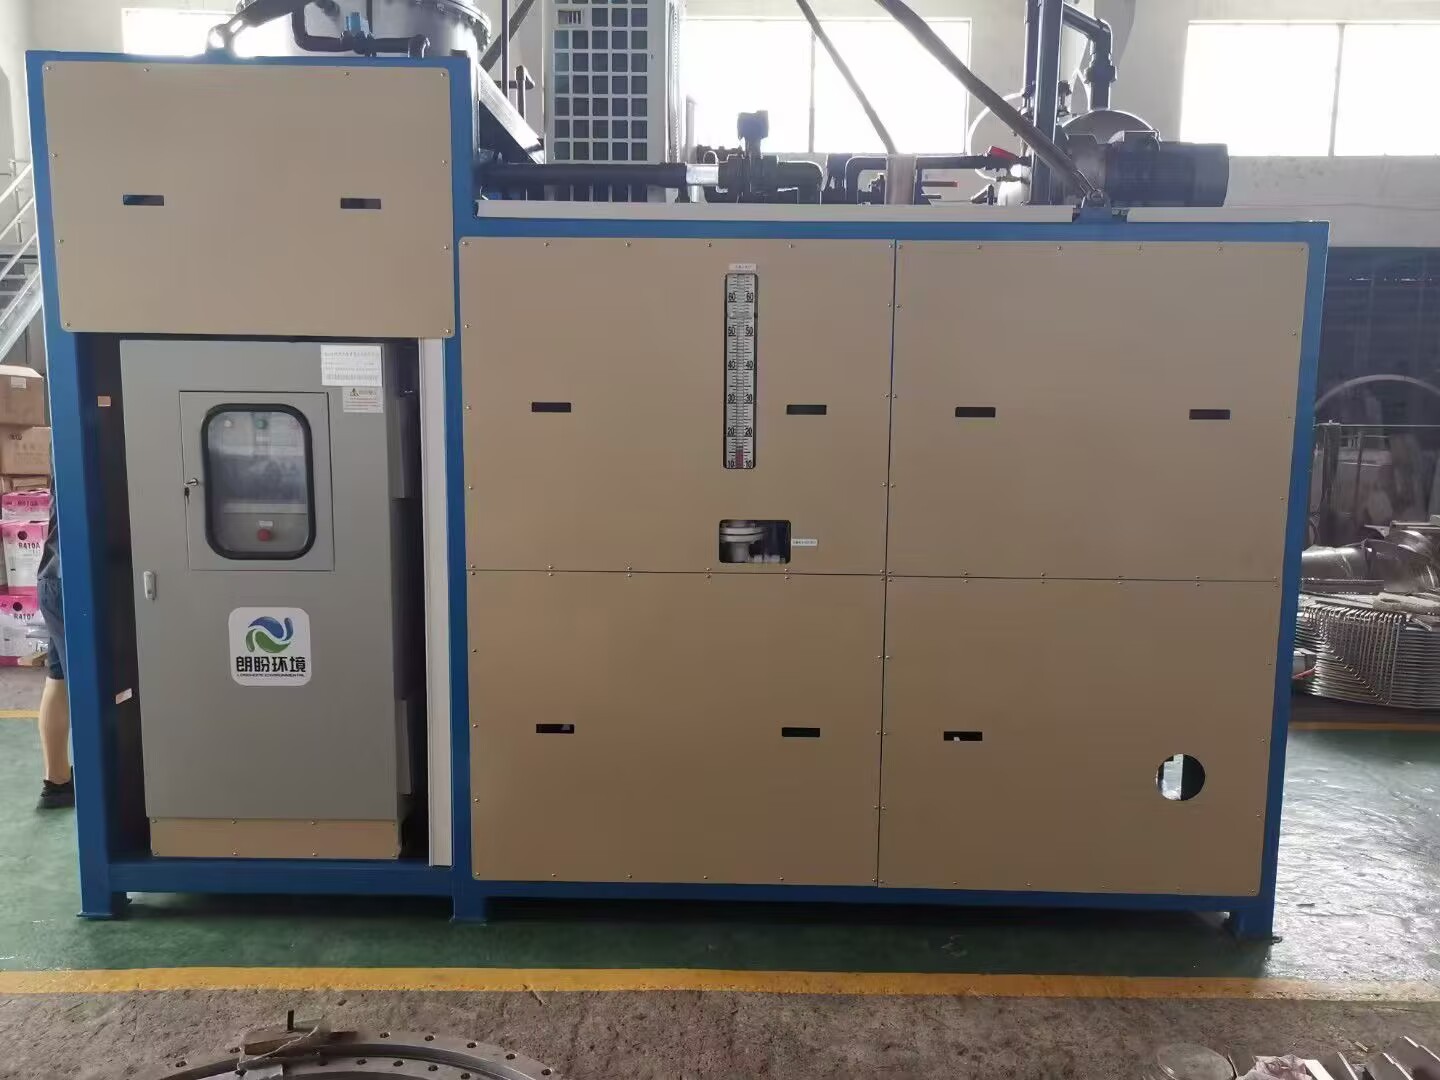
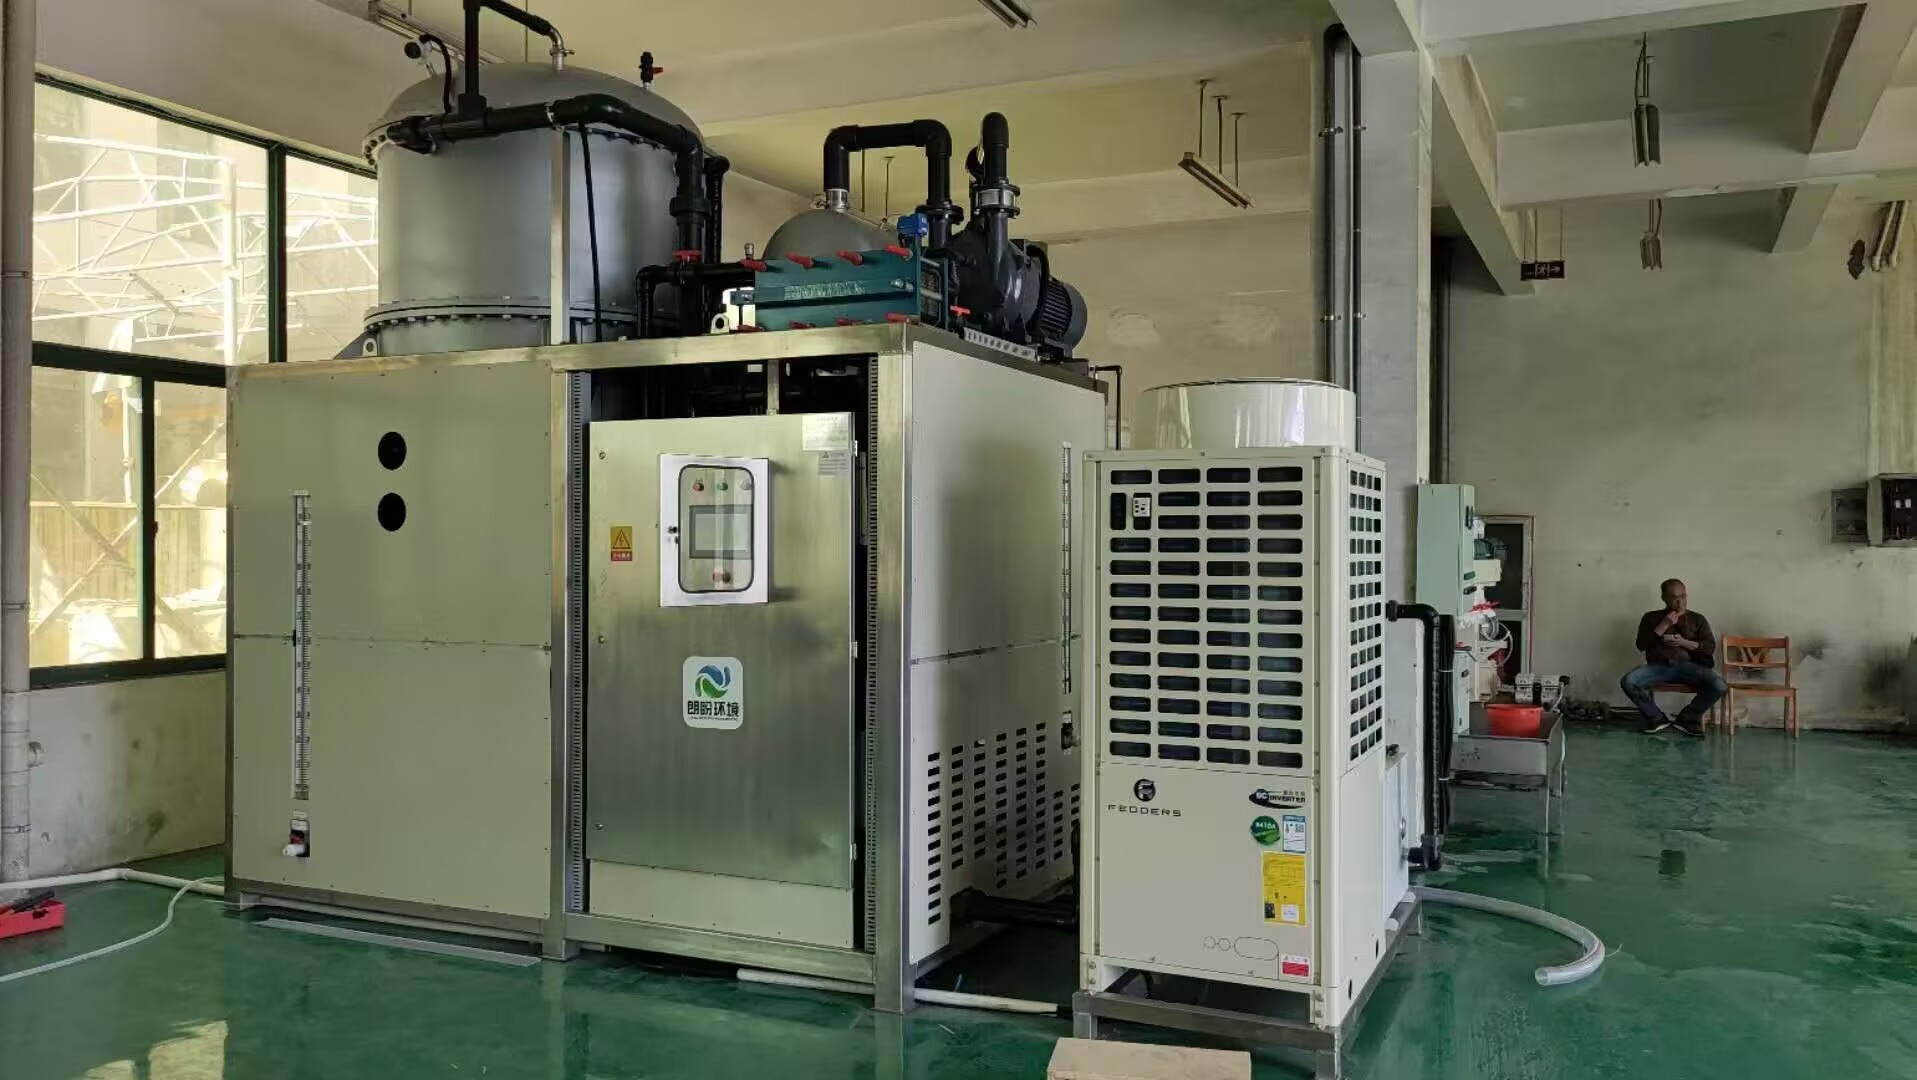
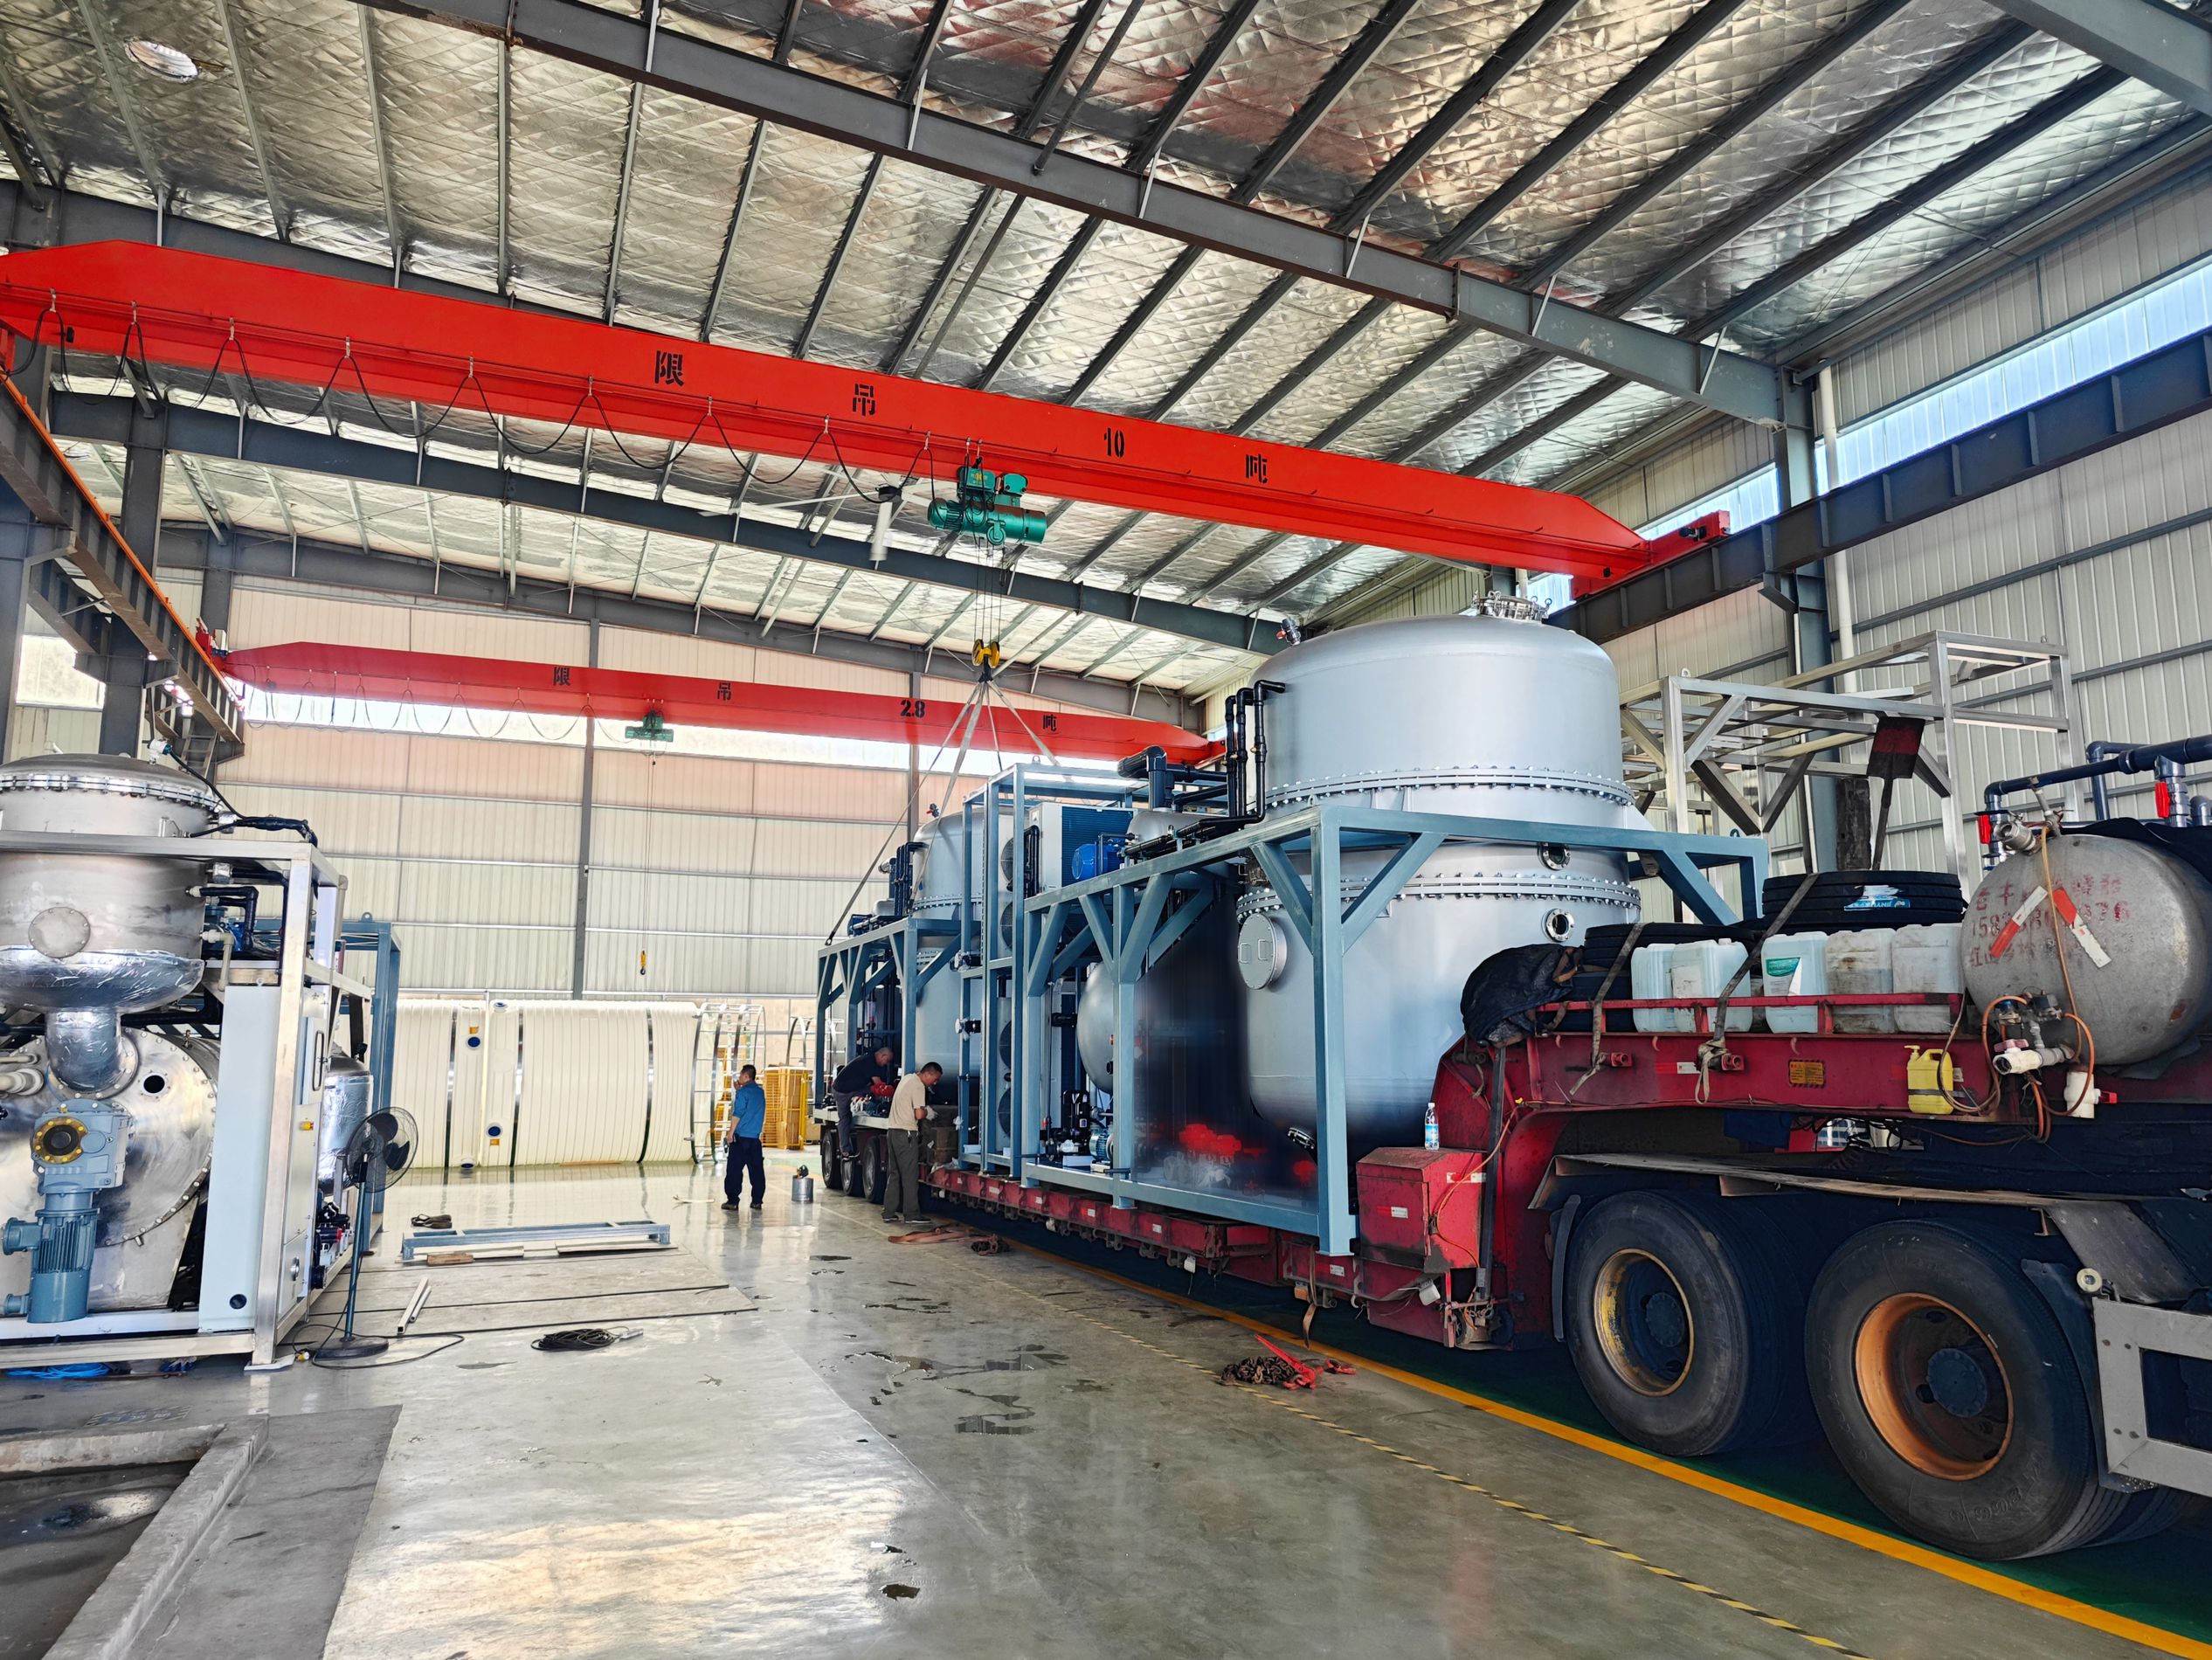
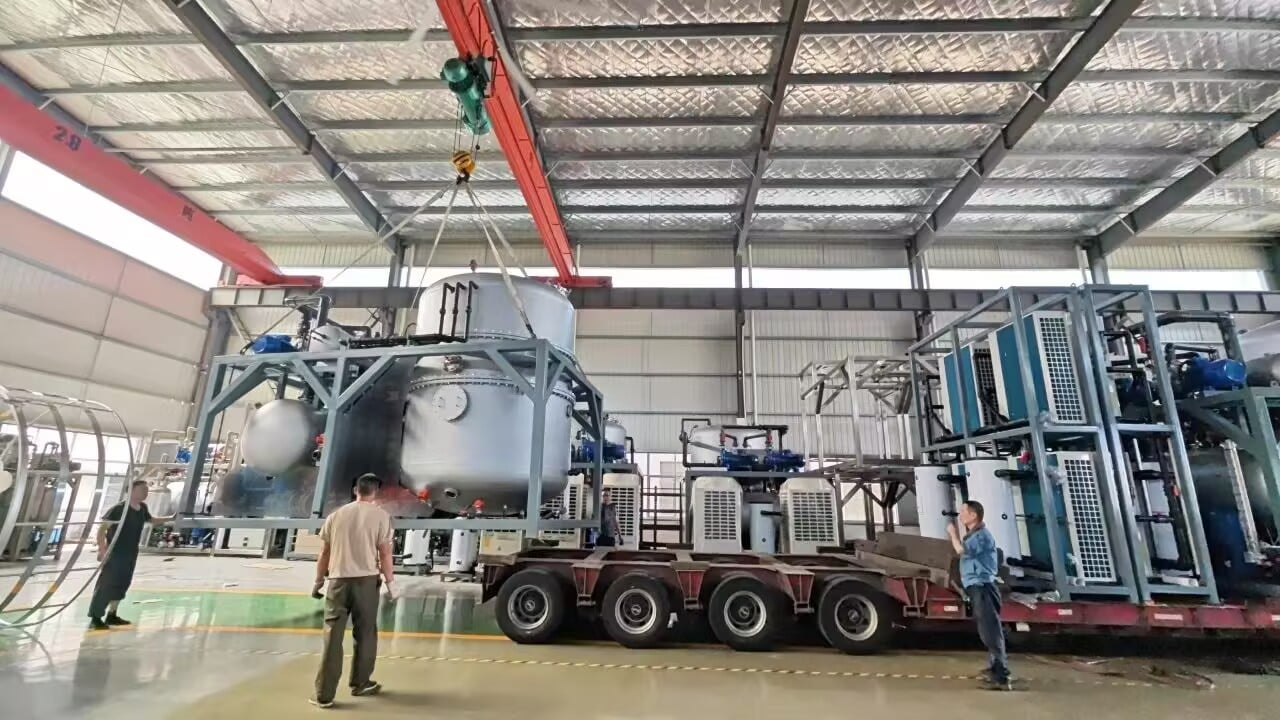
An industrial vacuum concentration system represents a sophisticated technology designed to efficiently reduce liquid volumes through controlled evaporation under reduced pressure conditions. This advanced equipment serves critical functions across multiple manufacturing sectors, enabling companies to concentrate solutions, recover valuable materials, and process industrial waste streams effectively. The industrial vacuum concentration system operates by lowering atmospheric pressure within a chamber, which decreases the boiling point of liquids and accelerates evaporation at lower temperatures. This gentle processing method preserves heat-sensitive compounds, making it ideal for pharmaceutical, food, chemical, and environmental applications. The system incorporates robust components including vacuum pumps, condensers, heating mechanisms, and separation vessels that work in harmony to achieve optimal concentration results. Key technological features of an industrial vacuum concentration system include precise temperature control, scalable capacity options, and automated monitoring systems. These features ensure consistent product quality while minimizing energy consumption and operational costs. The industrial vacuum concentration system excels at processing challenging materials that conventional methods cannot handle effectively. Applications span diverse industries where concentration and purification are essential. Pharmaceutical manufacturers utilize the industrial vacuum concentration system for extracting active ingredients, while food processors employ it for juice concentration and flavor preservation. Environmental companies apply this technology for treating industrial effluents and recovering valuable resources. The industrial vacuum concentration system's versatility and reliability make it an indispensable asset for modern industrial operations seeking efficiency and product excellence.

New Products

The industrial vacuum concentration system delivers substantial operational advantages that directly enhance productivity and profitability for manufacturing enterprises. By operating under reduced pressure, this system concentrates liquids at significantly lower temperatures compared to conventional evaporation methods, preserving delicate compounds and reducing thermal degradation of sensitive materials. Operational efficiency represents a major advantage of the industrial vacuum concentration system. The system reduces processing time substantially while consuming considerably less energy than traditional heating methods. This efficiency translates directly into lower operational costs and faster production cycles, enabling companies to increase output without expanding facility infrastructure or utility budgets. The industrial vacuum concentration system provides exceptional versatility across multiple industry applications. Whether processing pharmaceutical solutions, food products, or industrial waste streams, this equipment adapts to diverse operational requirements with minimal modifications. The system handles viscous, corrosive, and temperature-sensitive materials that would damage or destroy conventional concentration equipment. Quality improvement stands as another critical advantage. The gentle concentration process maintains product integrity, flavor profiles, nutritional content, and pharmaceutical efficacy. Companies achieve superior end products that command premium market prices and customer loyalty. The industrial vacuum concentration system enables significant waste reduction and environmental compliance. By efficiently recovering valuable materials from process streams, businesses minimize disposal costs while extracting additional revenue from byproducts. This sustainable approach aligns with modern environmental regulations and corporate responsibility initiatives. Mainten ability and reliability further benefit operators. Industrial vacuum concentration system designs incorporate durable construction and straightforward maintenance protocols, minimizing downtime and extending equipment lifespan. Advanced automation features reduce labor requirements and human error, improving consistency and safety throughout operations. These practical benefits make the industrial vacuum concentration system a sound investment for companies prioritizing efficiency, quality, and sustainable growth.

Practical Tips

Low Temperature Heat Pump Evaporator Maintenance Best Practices

24

Jul

Low Temperature Heat Pump Evaporator Maintenance Best Practices

Effective low temperature heat pump evaporator maintenance is essential for preserving system efficiency, extending equipment lifespan, and preventing costly downtime in industrial refrigeration applications. The evaporator represents a critical heat...
View More
Benefits of Low Temperature Heat Pump Evaporator in Industry

24

Jul

Benefits of Low Temperature Heat Pump Evaporator in Industry

Industrial facilities worldwide face mounting pressure to reduce operating costs while maintaining production quality and environmental compliance. The low temperature heat pump evaporator has emerged as a transformative solution that addresses these...
View More
Industrial Water Treatment Technologies for 2026

02

Sep

Industrial Water Treatment Technologies for 2026

Industrial water treatment remains one of the most critical operational priorities across manufacturing, chemical processing, food production, and energy sectors. As facilities face increasingly stringent environmental regulations, rising operational...
View More
Evaporator System Maintenance: Tips for Longevity

24

Jul

Evaporator System Maintenance: Tips for Longevity

Evaporator system maintenance is critical to ensuring your industrial cooling and waste-water treatment equipment operates reliably and efficiently over the long term. Whether your facility relies on evaporator systems for refrigeration, heat exchang...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

industrial vacuum concentration system

Energy-Efficient Performance Under Reduced Pressure

Energy-Efficient Performance Under Reduced Pressure

The industrial vacuum concentration system achieves remarkable energy efficiency by operating under controlled vacuum conditions that significantly lower boiling points. This breakthrough approach enables effective concentration at temperatures 20-40 degrees Celsius below atmospheric boiling points, reducing thermal energy requirements substantially. Companies implementing this industrial vacuum concentration system experience dramatic reductions in utility expenses, with energy consumption dropping by 40-60% compared to conventional evaporation techniques. The system's intelligent heating control mechanisms optimize energy usage dynamically, adjusting power input based on real-time process conditions. For large-scale operations processing thousands of gallons daily, these energy savings accumulate into millions of dollars annually. The industrial vacuum concentration system's efficient design also reduces facility cooling requirements, creating additional indirect energy savings. Environmental consciousness drives many purchasing decisions, and this system delivers measurable sustainability benefits alongside economic advantages. The reduced energy footprint helps companies meet corporate carbon reduction targets while improving their competitive positioning in environmentally conscious markets.
Superior Product Quality and Material Preservation

Superior Product Quality and Material Preservation

The industrial vacuum concentration system excels at protecting heat-sensitive materials that conventional methods inevitably damage. Pharmaceutical companies benefit enormously from this capability, as delicate molecular structures survive the gentle concentration process intact, preserving therapeutic effectiveness and bioavailability. The industrial vacuum concentration system maintains nutritional content in food products, preventing vitamin degradation and flavor compound loss that characterize traditional evaporation. Food manufacturers report superior taste profiles and extended shelf stability using this advanced technology. Chemical processors rely on the industrial vacuum concentration system to prevent unwanted reactions and decomposition of valuable compounds. The precise temperature control and oxygen-limited environment minimize oxidation and thermal breakdown. Quality metrics consistently demonstrate that products concentrated using an industrial vacuum concentration system exceed those created through conventional methods. This quality advantage directly translates into customer satisfaction, regulatory compliance, and market differentiation. Companies leveraging this superior quality positioning capture premium pricing opportunities and strengthen brand reputation in competitive markets.
Scalable Capacity and Flexible Operational Design

Scalable Capacity and Flexible Operational Design

The industrial vacuum concentration system offers exceptional scalability, accommodating everything from laboratory-scale research to massive industrial production volumes. Manufacturers can select system configurations matching their specific throughput requirements, processing anywhere from 50 gallons to 10,000+ gallons daily. This flexibility makes the industrial vacuum concentration system suitable for startups initiating operations and established enterprises expanding capacity. Modular design components allow straightforward upgrades as business needs evolve, protecting initial capital investments. The industrial vacuum concentration system adapts effortlessly to processing different materials and concentrations without extensive reconfiguration. Operators switch between pharmaceutical solutions, food products, and chemical streams using simple parameter adjustments. This operational flexibility eliminates dedicated equipment requirements, reducing capital expenditures and facility space needs. The industrial vacuum concentration system's adaptability proves invaluable for contract manufacturers serving diverse clients with varying concentration requirements. Advanced automation interfaces enable operators with minimal training to manage sophisticated processes effectively, expanding workforce capabilities without expensive specialist hiring.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000