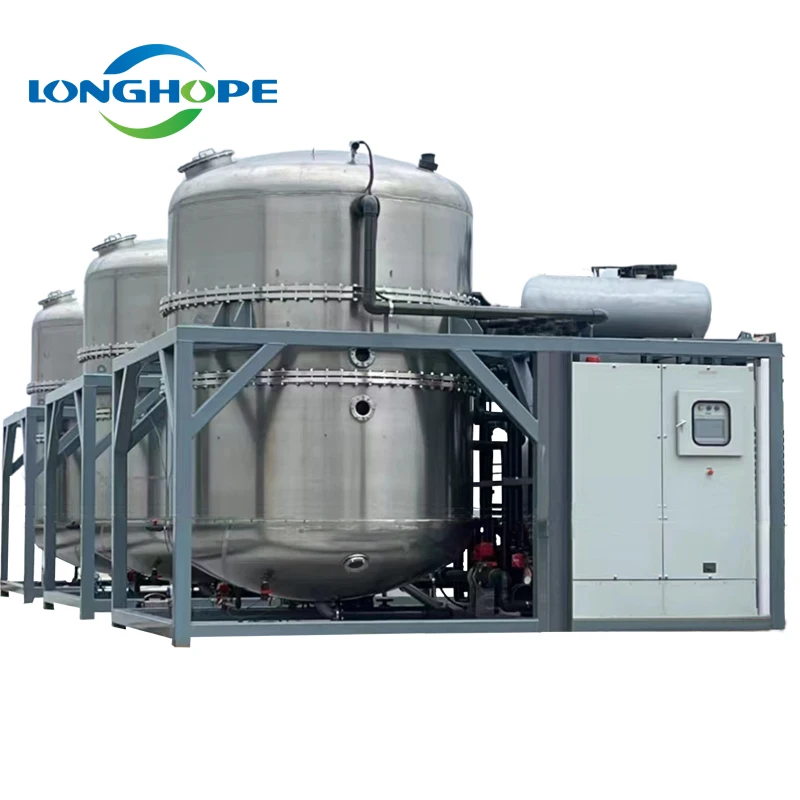
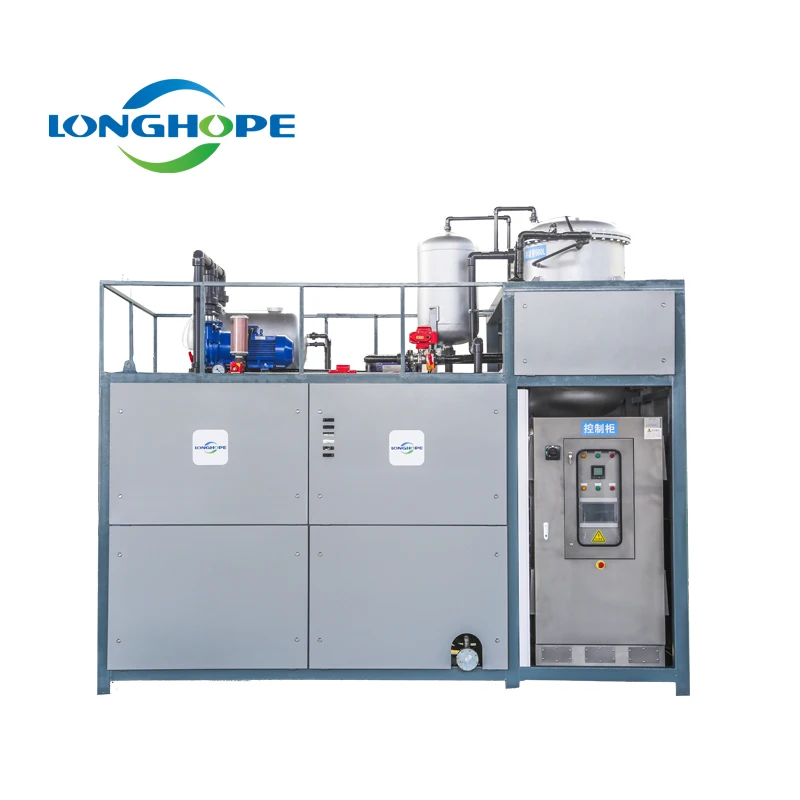
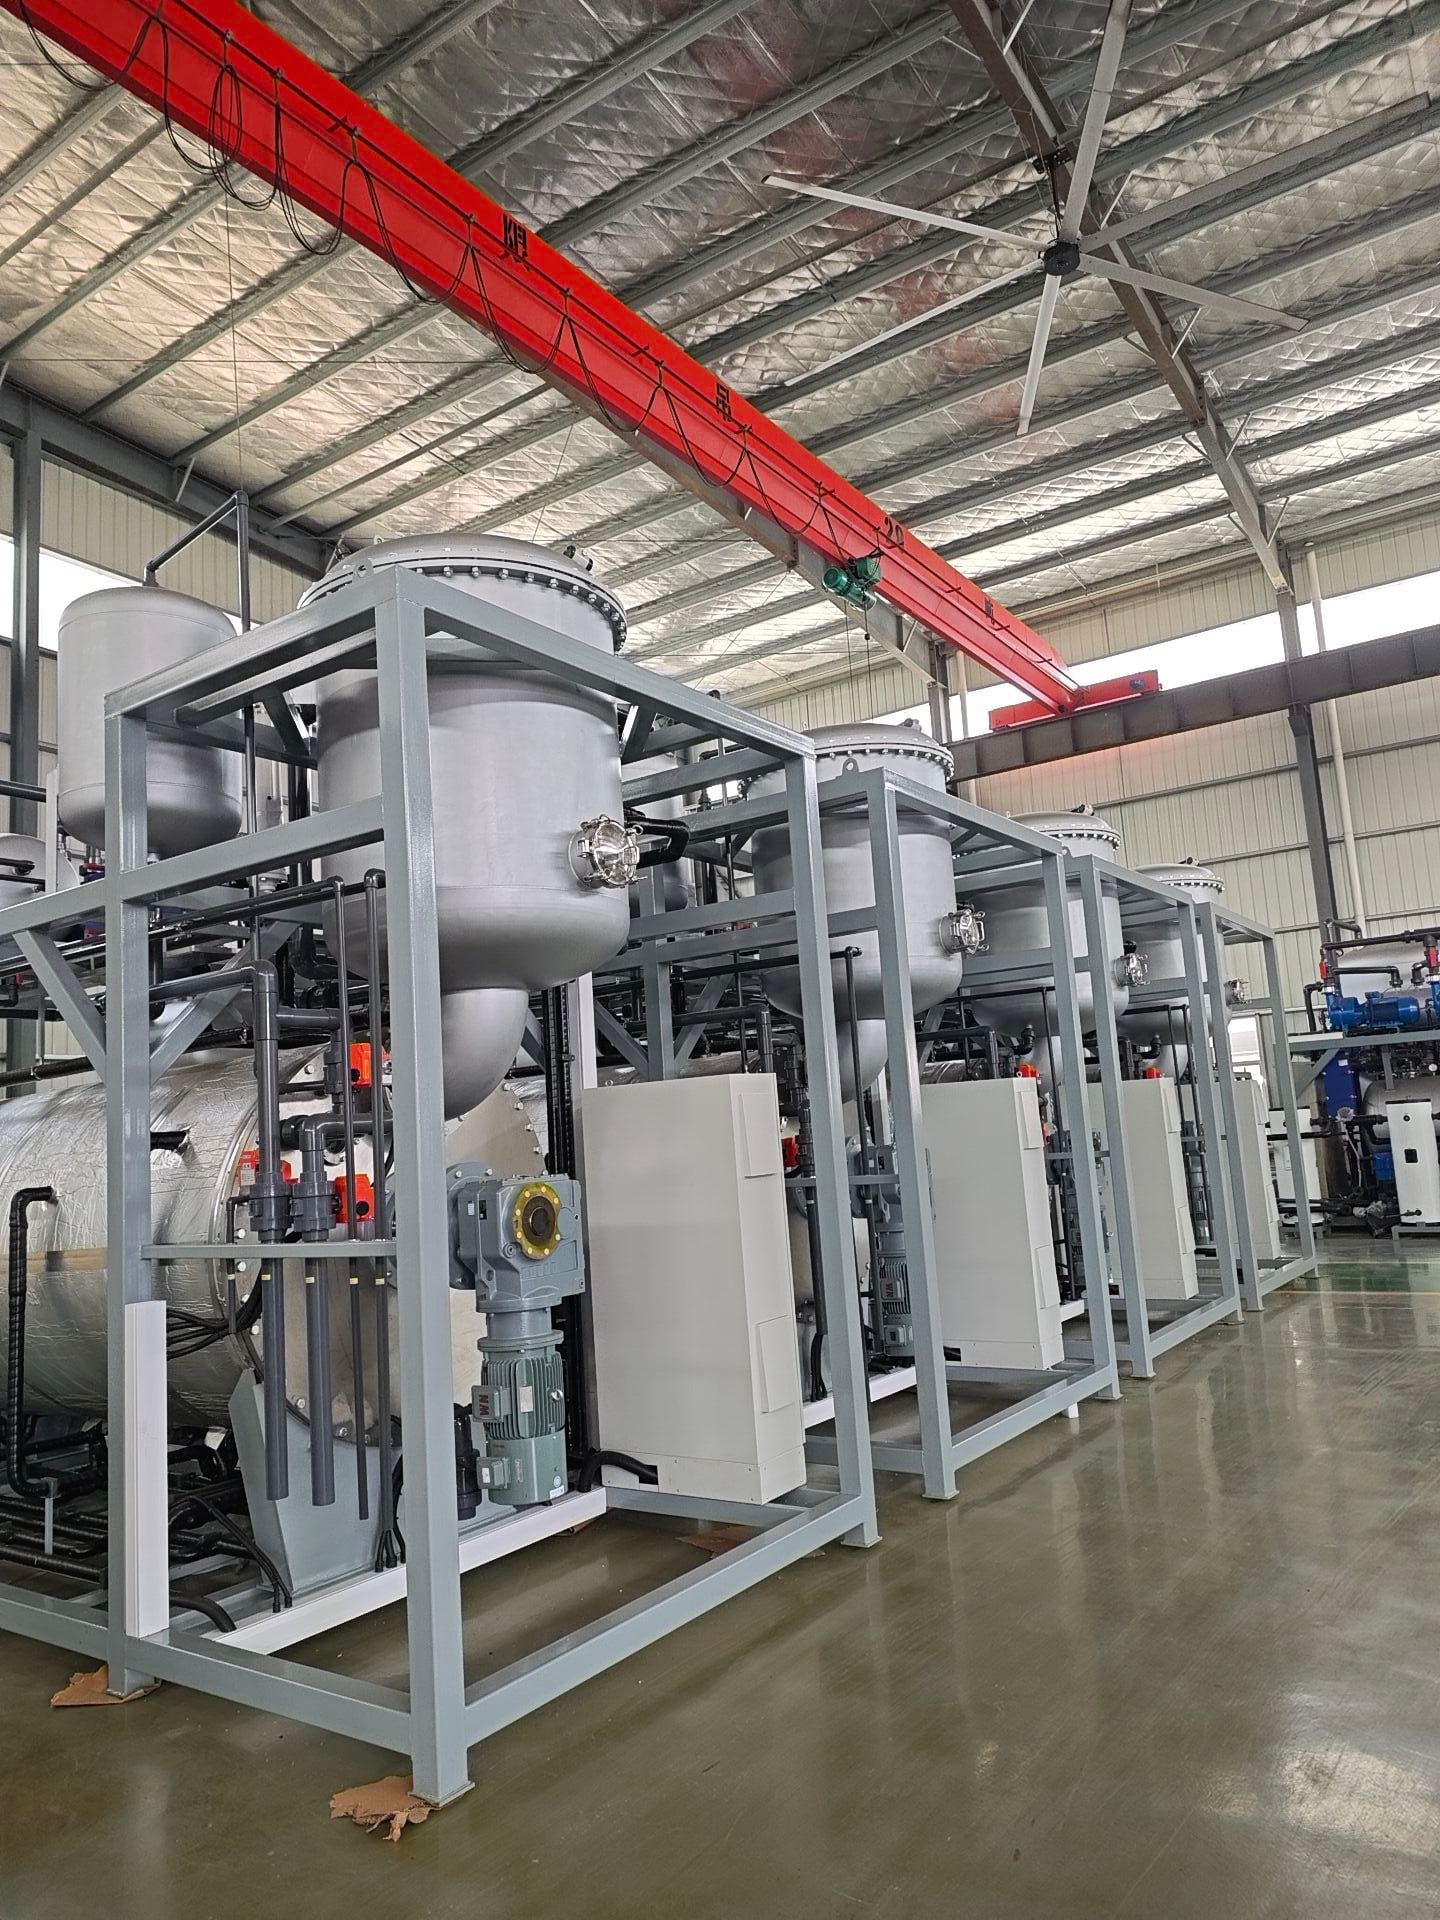
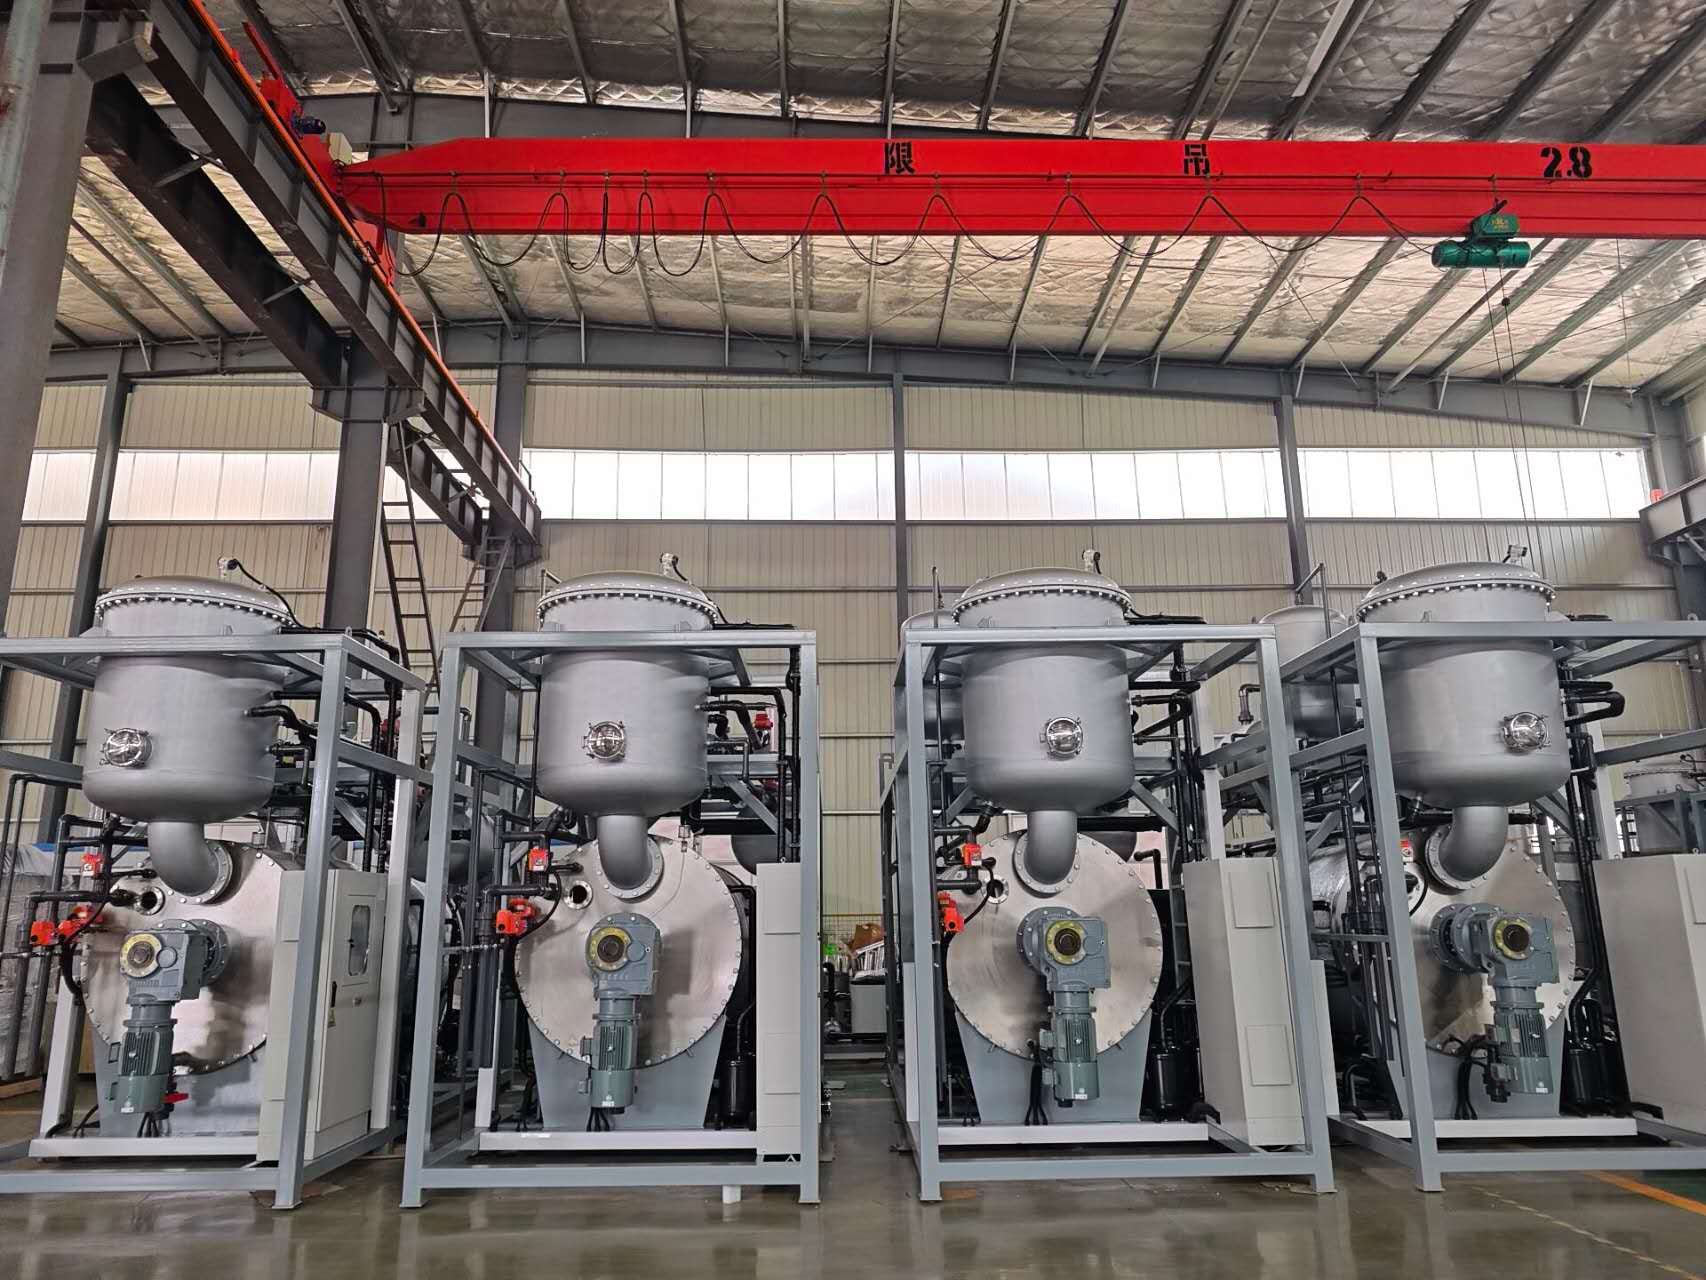
Low Temperature Concentration Equipment

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

low temperature concentration equipment

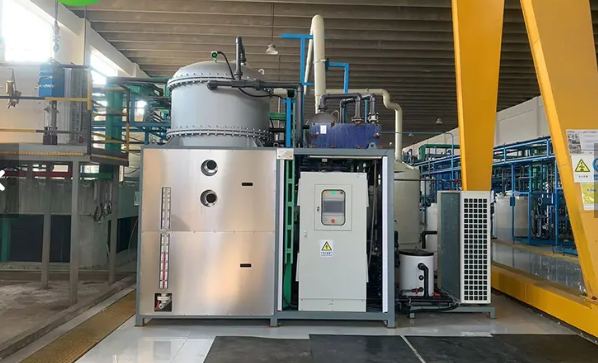
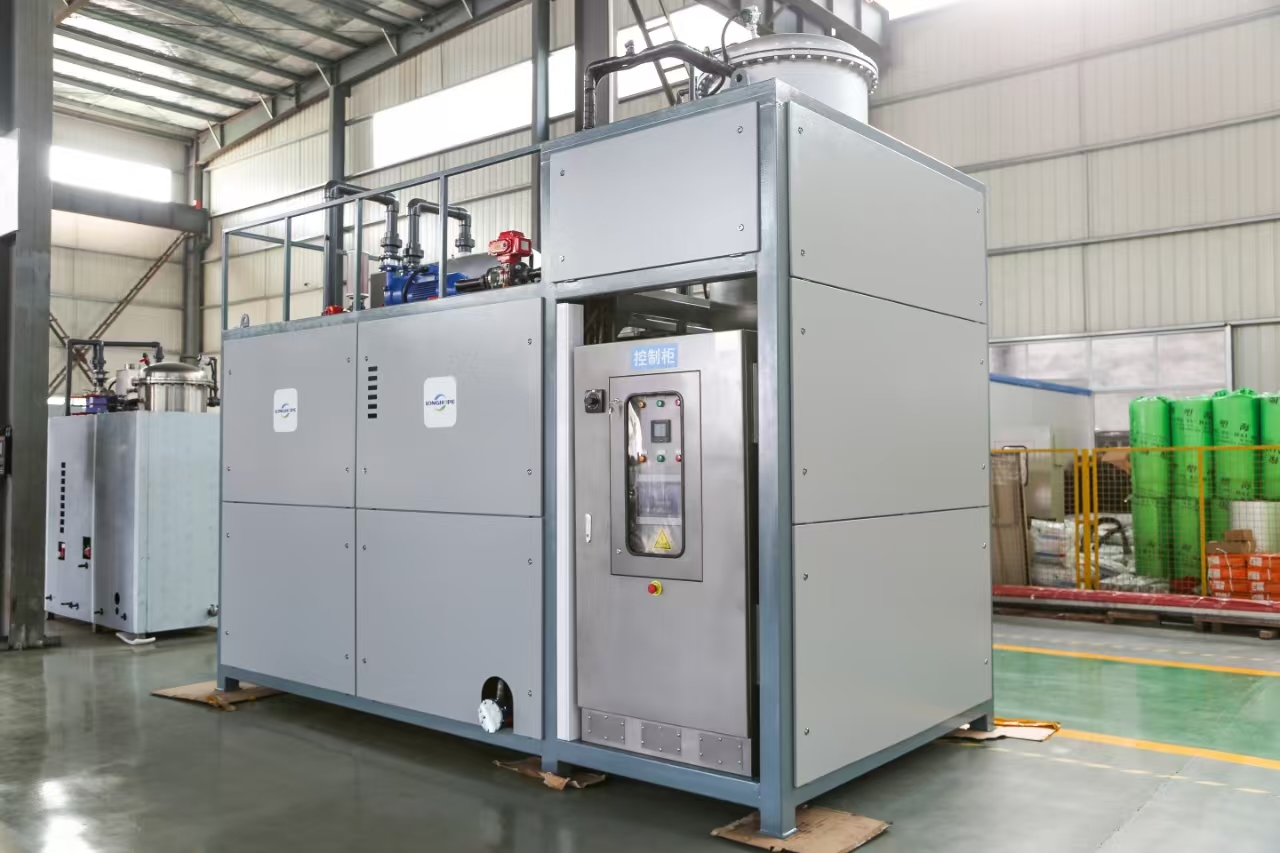
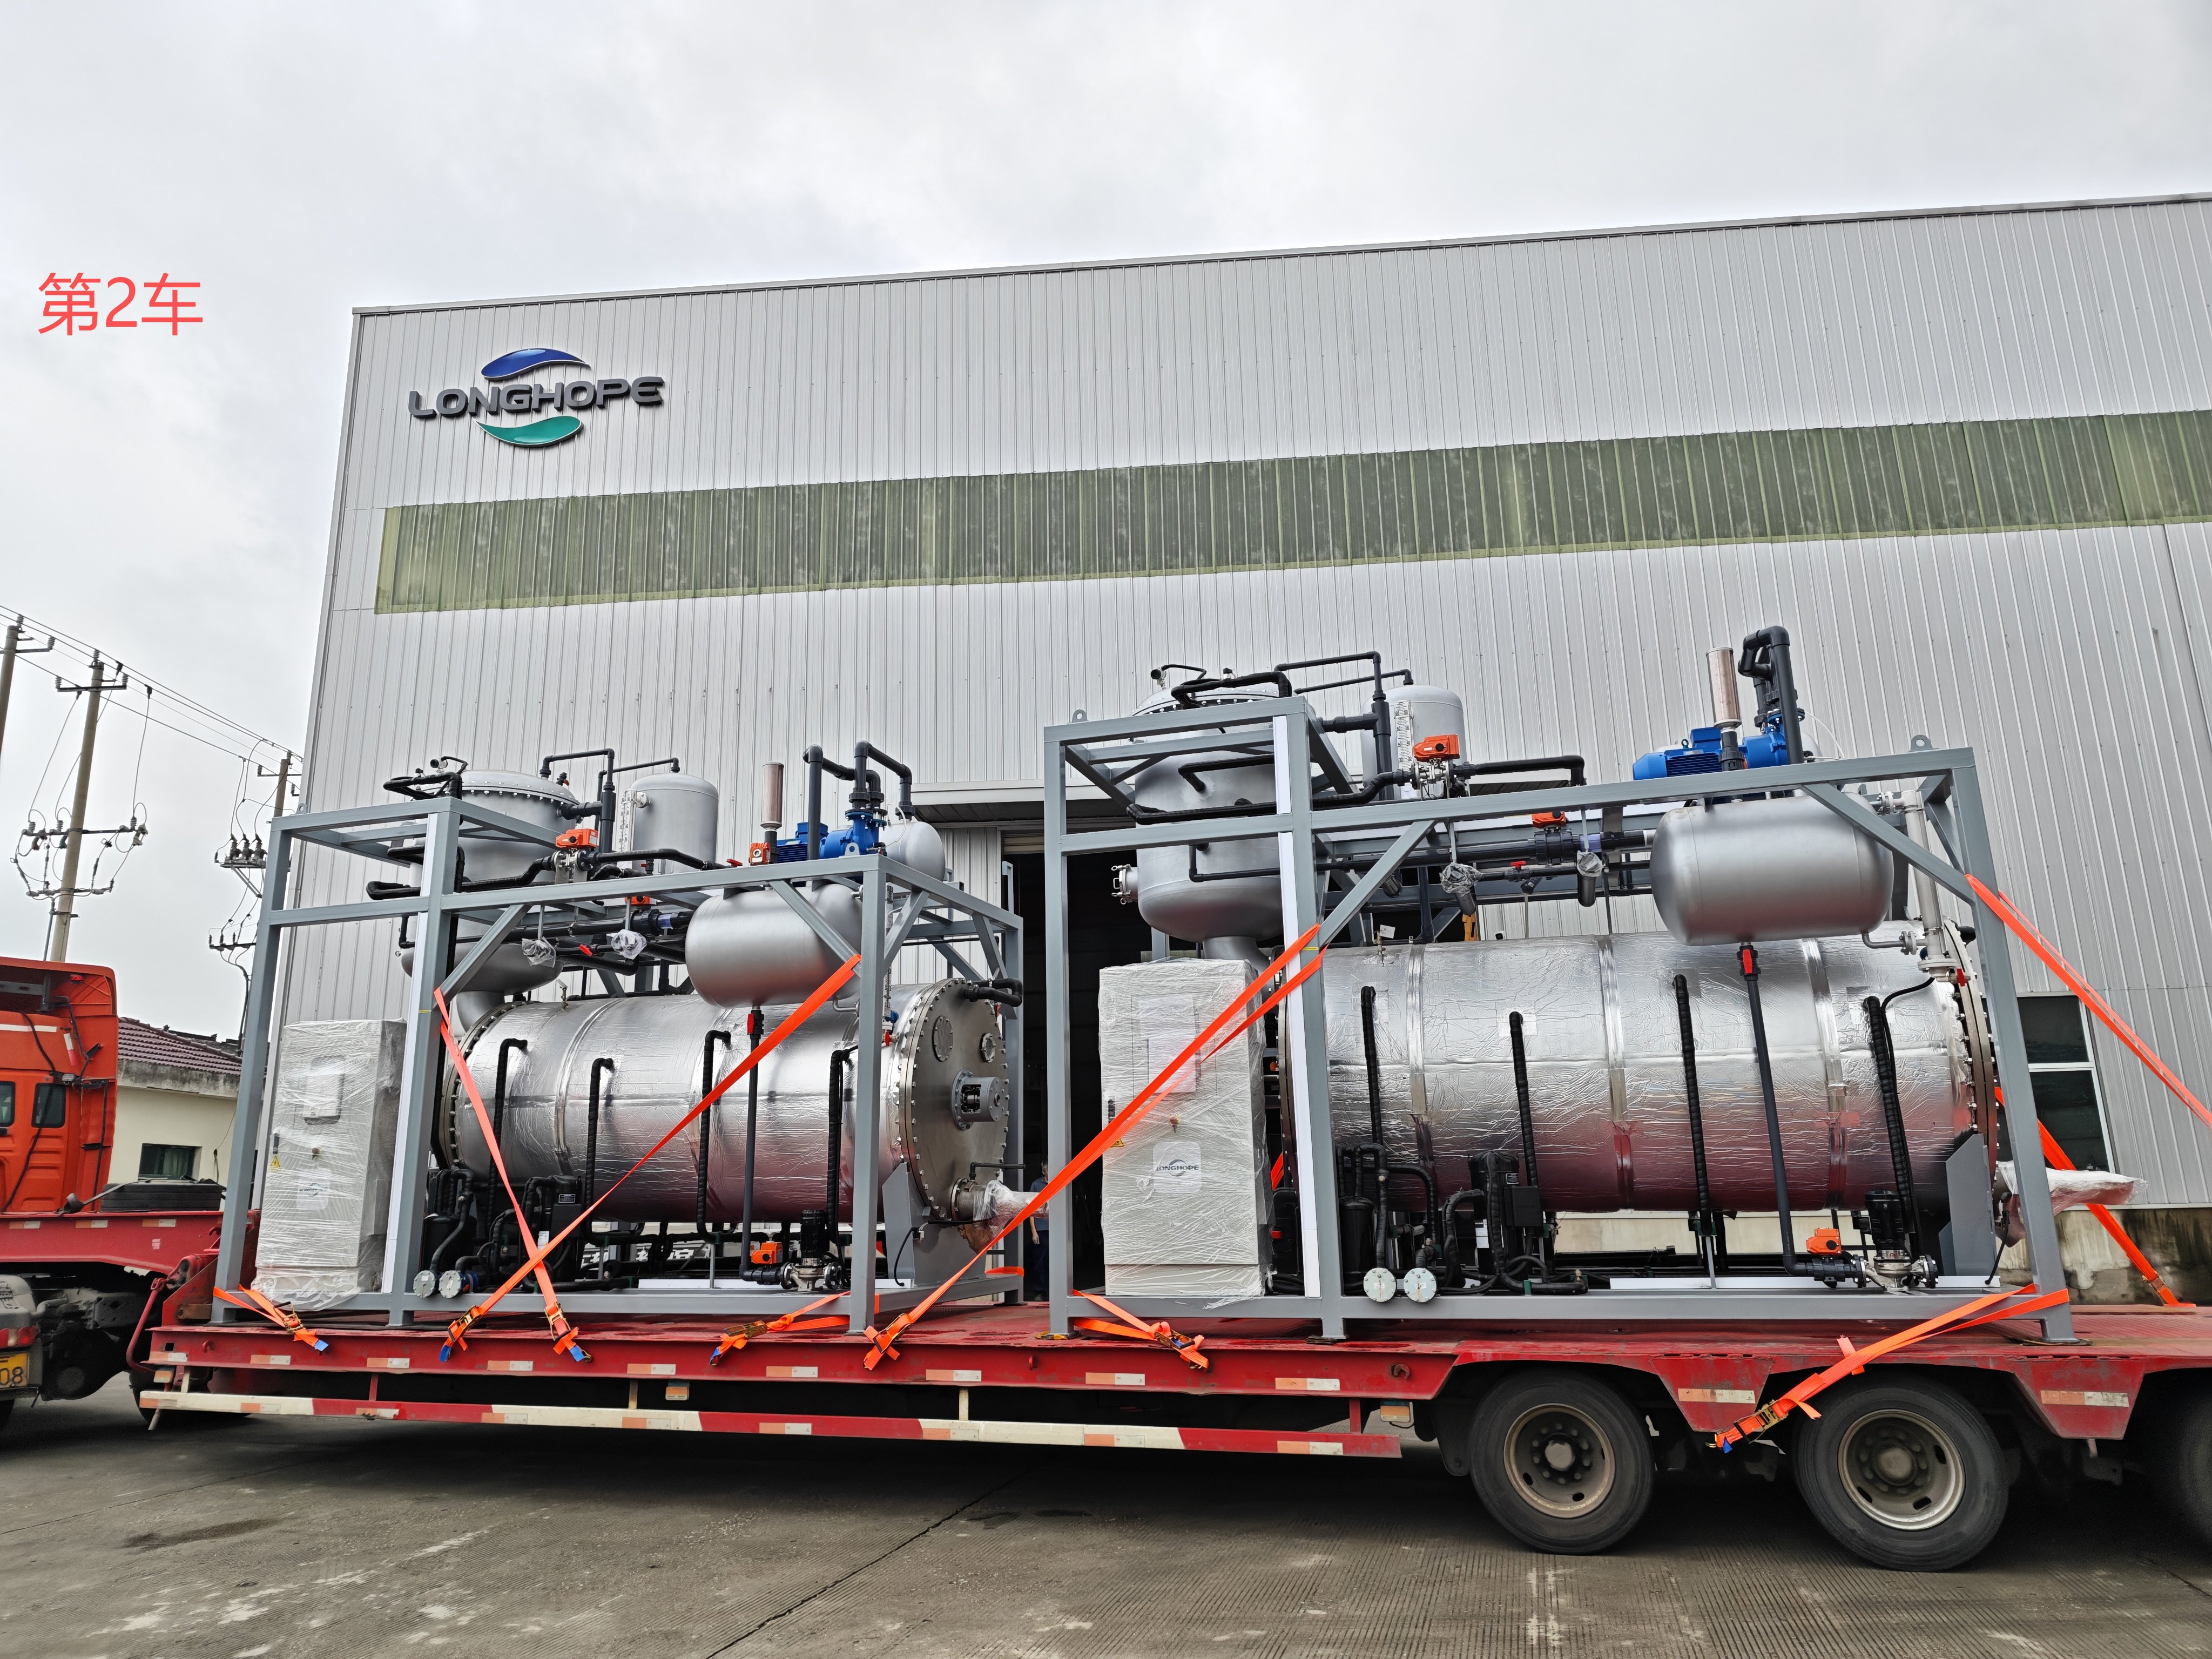
Low temperature concentration equipment represents an advanced industrial solution designed to extract, concentrate, and preserve valuable components from liquid materials while maintaining optimal quality standards. This specialized low temperature concentration equipment operates at reduced thermal conditions, preventing degradation of heat-sensitive substances commonly found in pharmaceutical, food, and chemical manufacturing environments. The primary function of low temperature concentration equipment involves removing excess liquid through evaporation while preserving the integrity of active compounds, nutrients, and beneficial properties. Advanced low temperature concentration equipment utilizes vacuum distillation, membrane separation, and reverse osmosis technologies to achieve superior concentration results without exposing materials to excessive heat exposure. Key technological features include precision temperature control systems, automated vacuum management, and multi-stage separation processes. Low temperature concentration equipment incorporates intelligent monitoring systems that maintain consistent operational parameters throughout the concentration cycle. The equipment features corrosion-resistant construction materials suitable for demanding industrial applications. Applications for low temperature concentration equipment span numerous industries. Pharmaceutical manufacturers rely on this equipment for concentrating herbal extracts and medicinal compounds. Food processing facilities utilize low temperature concentration equipment to concentrate juices, essential oils, and nutritional supplements while preserving flavor profiles and nutritional value. Chemical companies employ this technology for recovering valuable solvents and refining specialty chemicals without thermal degradation. The versatility of low temperature concentration equipment makes it essential for operations requiring precision, quality preservation, and maximum product yield. Modern facilities increasingly adopt low temperature concentration equipment to meet stringent regulatory requirements and consumer demands for superior product quality in competitive markets.

Popular Products

Low temperature concentration equipment delivers substantial operational advantages that directly enhance productivity and product quality for diverse manufacturing operations. The most significant benefit involves preserving heat-sensitive materials that would otherwise degrade under conventional high-temperature concentration methods. This preservation capability ensures maximum recovery of valuable active compounds, directly improving profitability and product performance. Operational efficiency represents another compelling advantage. Low temperature concentration equipment reduces energy consumption compared to traditional concentration methods, resulting in lower operational costs and reduced environmental impact. The automated control systems minimize manual intervention requirements, allowing facility operators to focus on other critical production tasks while maintaining consistent concentration accuracy. Product quality improvements form the foundation of customer value when using low temperature concentration equipment. By eliminating thermal stress, manufacturers consistently produce superior products with enhanced flavor, potency, and nutritional value. This quality advantage translates into improved market competitiveness and customer satisfaction rates. Application suitability makes low temperature concentration equipment invaluable across industries. Pharmaceutical manufacturers can concentrate sensitive plant extracts without compromising medicinal properties. Food producers can concentrate juices and oils while maintaining natural taste and beneficial compounds. Cosmetic manufacturers preserve fragrance and active ingredient effectiveness during concentration processes. Decision-useful product context reveals that investing in low temperature concentration equipment represents a strategic choice for forward-thinking manufacturers. The equipment accommodates various liquid types and viscosities, providing operational flexibility for evolving production requirements. Long-term reliability and minimal maintenance demands reduce total cost of ownership significantly. Facilities utilizing low temperature concentration equipment achieve compliance with strict quality standards and regulatory requirements more effectively. The technology enables manufacturers to market products with superior quality certifications, appealing to premium market segments. Return on investment typically materializes within 18-24 months through improved yields and reduced waste generation.

Tips And Tricks

Top 5 Low Temperature Heat Pump Evaporator Applications

24

Jul

Top 5 Low Temperature Heat Pump Evaporator Applications

The low temperature heat pump evaporator represents a critical advancement in industrial thermal management and energy efficiency. This innovative component enables heat pump systems to operate effectively at reduced temperatures, making it indispens...
View More
Vacuum Distillation System Maintenance Best Practices

24

Jul

Vacuum Distillation System Maintenance Best Practices

Proper vacuum distillation system maintenance is critical for industries relying on separation, purification, and concentration processes. A well-maintained vacuum distillation system ensures consistent product quality, minimizes operational downtime...
View More
Industrial Water Treatment Technologies for 2026

02

Sep

Industrial Water Treatment Technologies for 2026

Industrial water treatment remains one of the most critical operational priorities across manufacturing, chemical processing, food production, and energy sectors. As facilities face increasingly stringent environmental regulations, rising operational...
View More
Vacuum Distillation: Key Benefits for Industrial Use

24

Jul

Vacuum Distillation: Key Benefits for Industrial Use

Vacuum distillation has become an essential separation technology across numerous industrial sectors, offering superior performance compared to conventional atmospheric distillation methods. By operating under reduced pressure conditions, vacuum dist...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

low temperature concentration equipment

Superior Heat-Sensitive Material Preservation

Superior Heat-Sensitive Material Preservation

Low temperature concentration equipment excels at maintaining the integrity of delicate compounds that cannot withstand conventional high-temperature processing. This specialized capability preserves valuable active ingredients, essential oils, and nutritional components that would otherwise deteriorate under thermal stress. The equipment's advanced vacuum technology enables effective concentration at significantly reduced temperatures, typically between 20-50 degrees Celsius, far below standard concentration thresholds. This preservation advantage proves critical for pharmaceutical applications where medicinal potency depends on maintaining complex molecular structures. Food and beverage manufacturers benefit equally, as low temperature concentration equipment preserves natural flavors, aromas, and nutritional profiles that define product quality. The technology enables manufacturers to produce premium-grade concentrated products commanding higher market prices. Pharmaceutical companies using low temperature concentration equipment report superior extract quality and increased active compound yields compared to conventional methods. Food producers achieve concentrated products with flavor profiles identical to fresh source materials. This preservation capability represents the most significant competitive advantage of low temperature concentration equipment, enabling manufacturers to differentiate products in competitive markets through verifiable quality superiority and customer satisfaction improvements.
Energy-Efficient Operations and Cost Reduction

Energy-Efficient Operations and Cost Reduction

Low temperature concentration equipment demonstrates exceptional energy efficiency, consuming substantially less power than conventional high-temperature concentration systems. The vacuum-based operation requires minimal heating energy, typically reducing operational electricity consumption by 40-60 percent compared to traditional methods. This efficiency directly translates into measurable cost savings that accumulate significantly across extended production periods. The economic advantages of low temperature concentration equipment extend beyond energy savings to include reduced maintenance expenses and extended equipment lifespan. Lower operating temperatures minimize thermal stress on equipment components, reducing wear rates and maintenance frequency. Facility managers report substantially fewer equipment failures and replacement needs when utilizing low temperature concentration equipment versus conventional alternatives. Operational cost reduction through low temperature concentration equipment adoption enables competitive pricing advantages while maintaining profitability margins. Manufacturers can reinvest savings into product development, quality improvements, or facility expansion initiatives. The financial benefits of low temperature concentration equipment prove particularly significant for high-volume production facilities processing millions of units annually, where cumulative energy savings reach substantial annual figures and dramatically impact bottom-line profitability.
Regulatory Compliance and Quality Assurance Excellence

Regulatory Compliance and Quality Assurance Excellence

Modern manufacturing faces increasingly stringent regulatory requirements for product safety, purity, and quality documentation. Low temperature concentration equipment enables manufacturers to meet these demanding standards with consistent reliability and comprehensive quality assurance capabilities. The equipment's automated monitoring systems generate detailed operational records documenting every concentration cycle, providing essential evidence for regulatory audits and certification processes. Quality parameters maintained by low temperature concentration equipment exceed industry standards across pharmaceutical, food, and chemical sectors. Manufacturers achieve consistent product specifications, reducing batch rejections and rework requirements. The equipment's precision control systems ensure every production run meets exacting quality standards, building customer confidence and supporting premium market positioning. Regulatory agencies recognize low temperature concentration equipment as best-practice technology that demonstrates manufacturer commitment to quality excellence. Food manufacturers qualify for premium certifications by utilizing low temperature concentration equipment, accessing higher-value market segments. Pharmaceutical companies ensure compliance with Good Manufacturing Practice requirements more effectively when employing this advanced technology. Overall, low temperature concentration equipment investment strengthens regulatory standing while reducing compliance-related costs and operational risks.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000