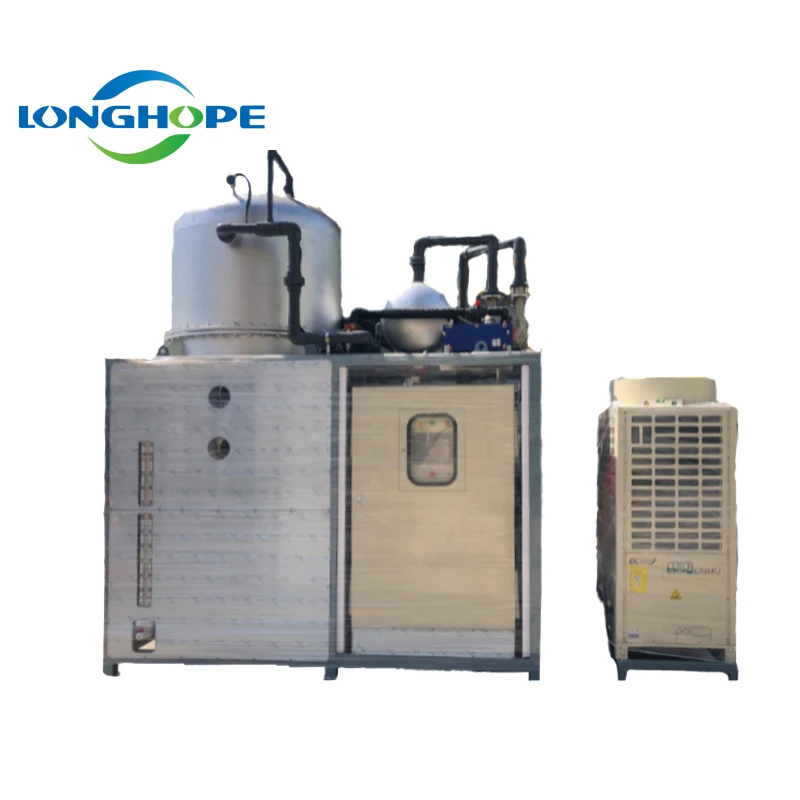
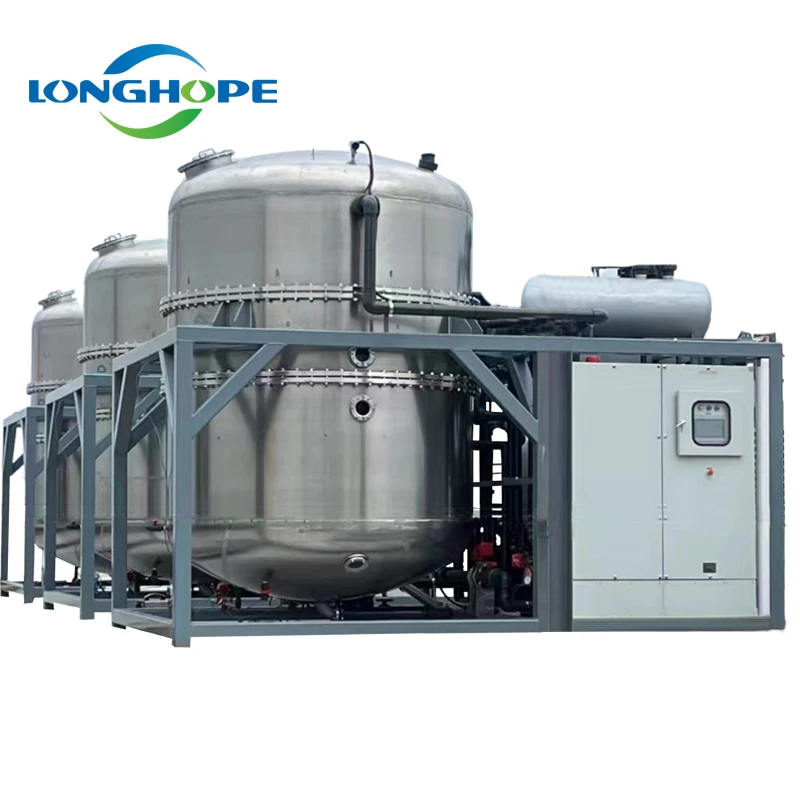
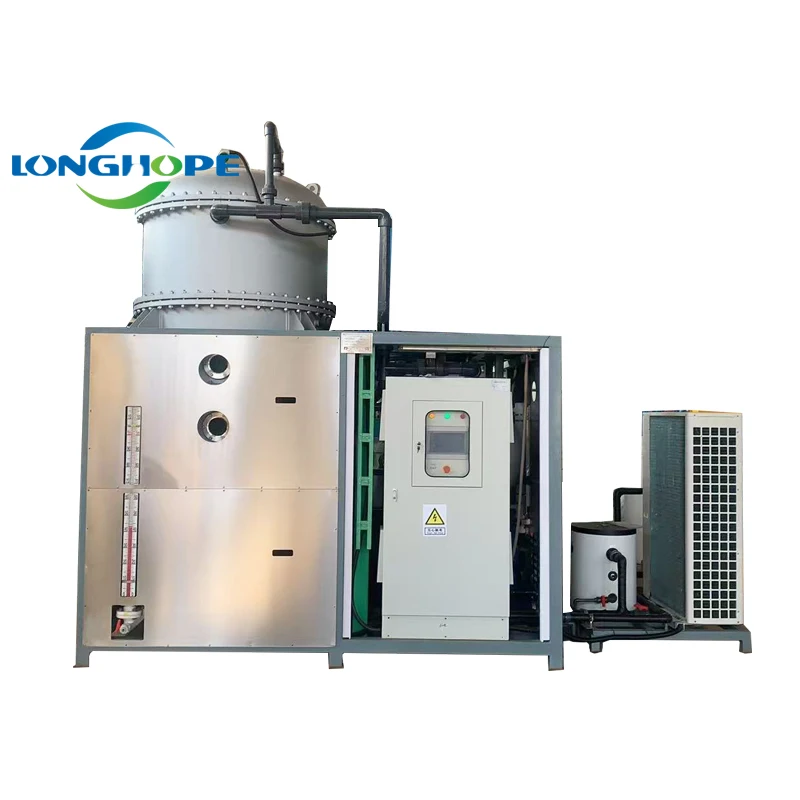
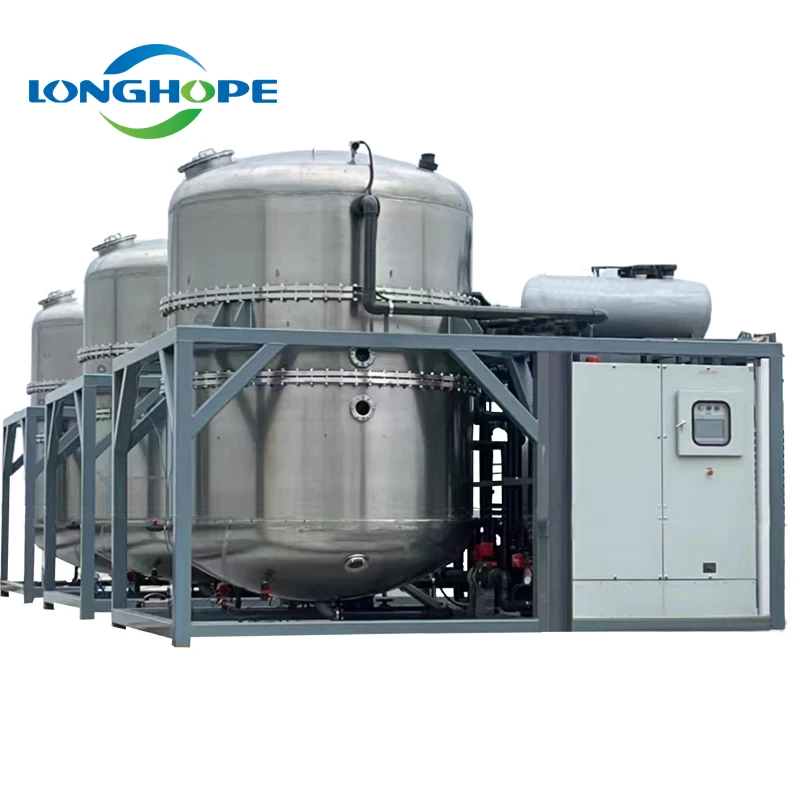
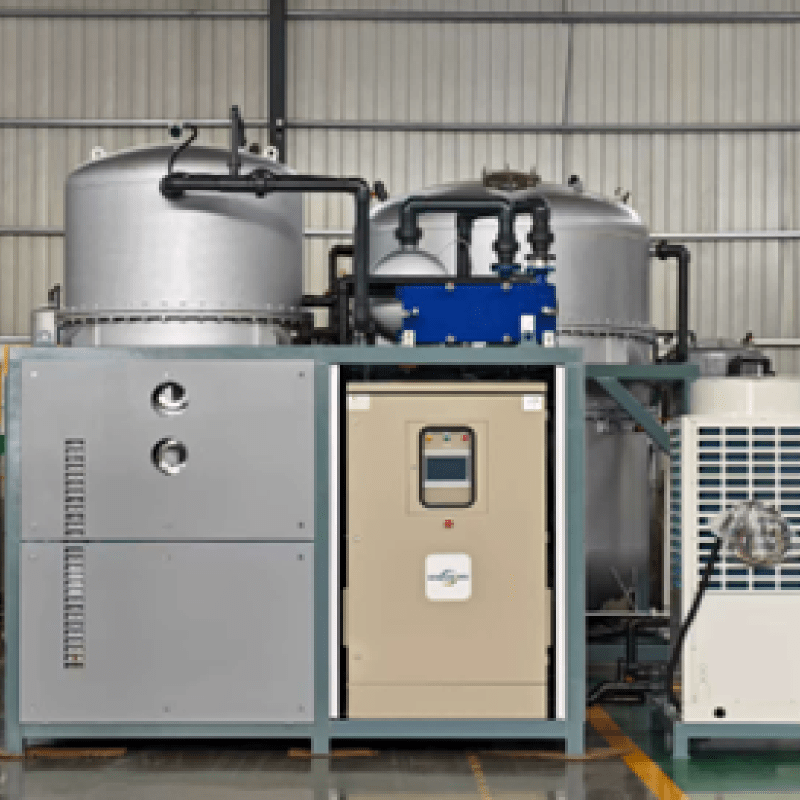
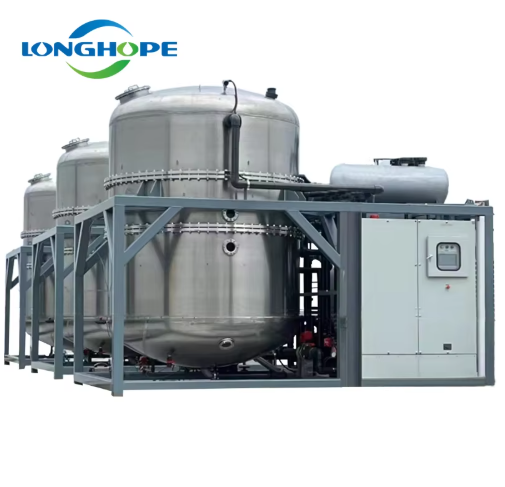
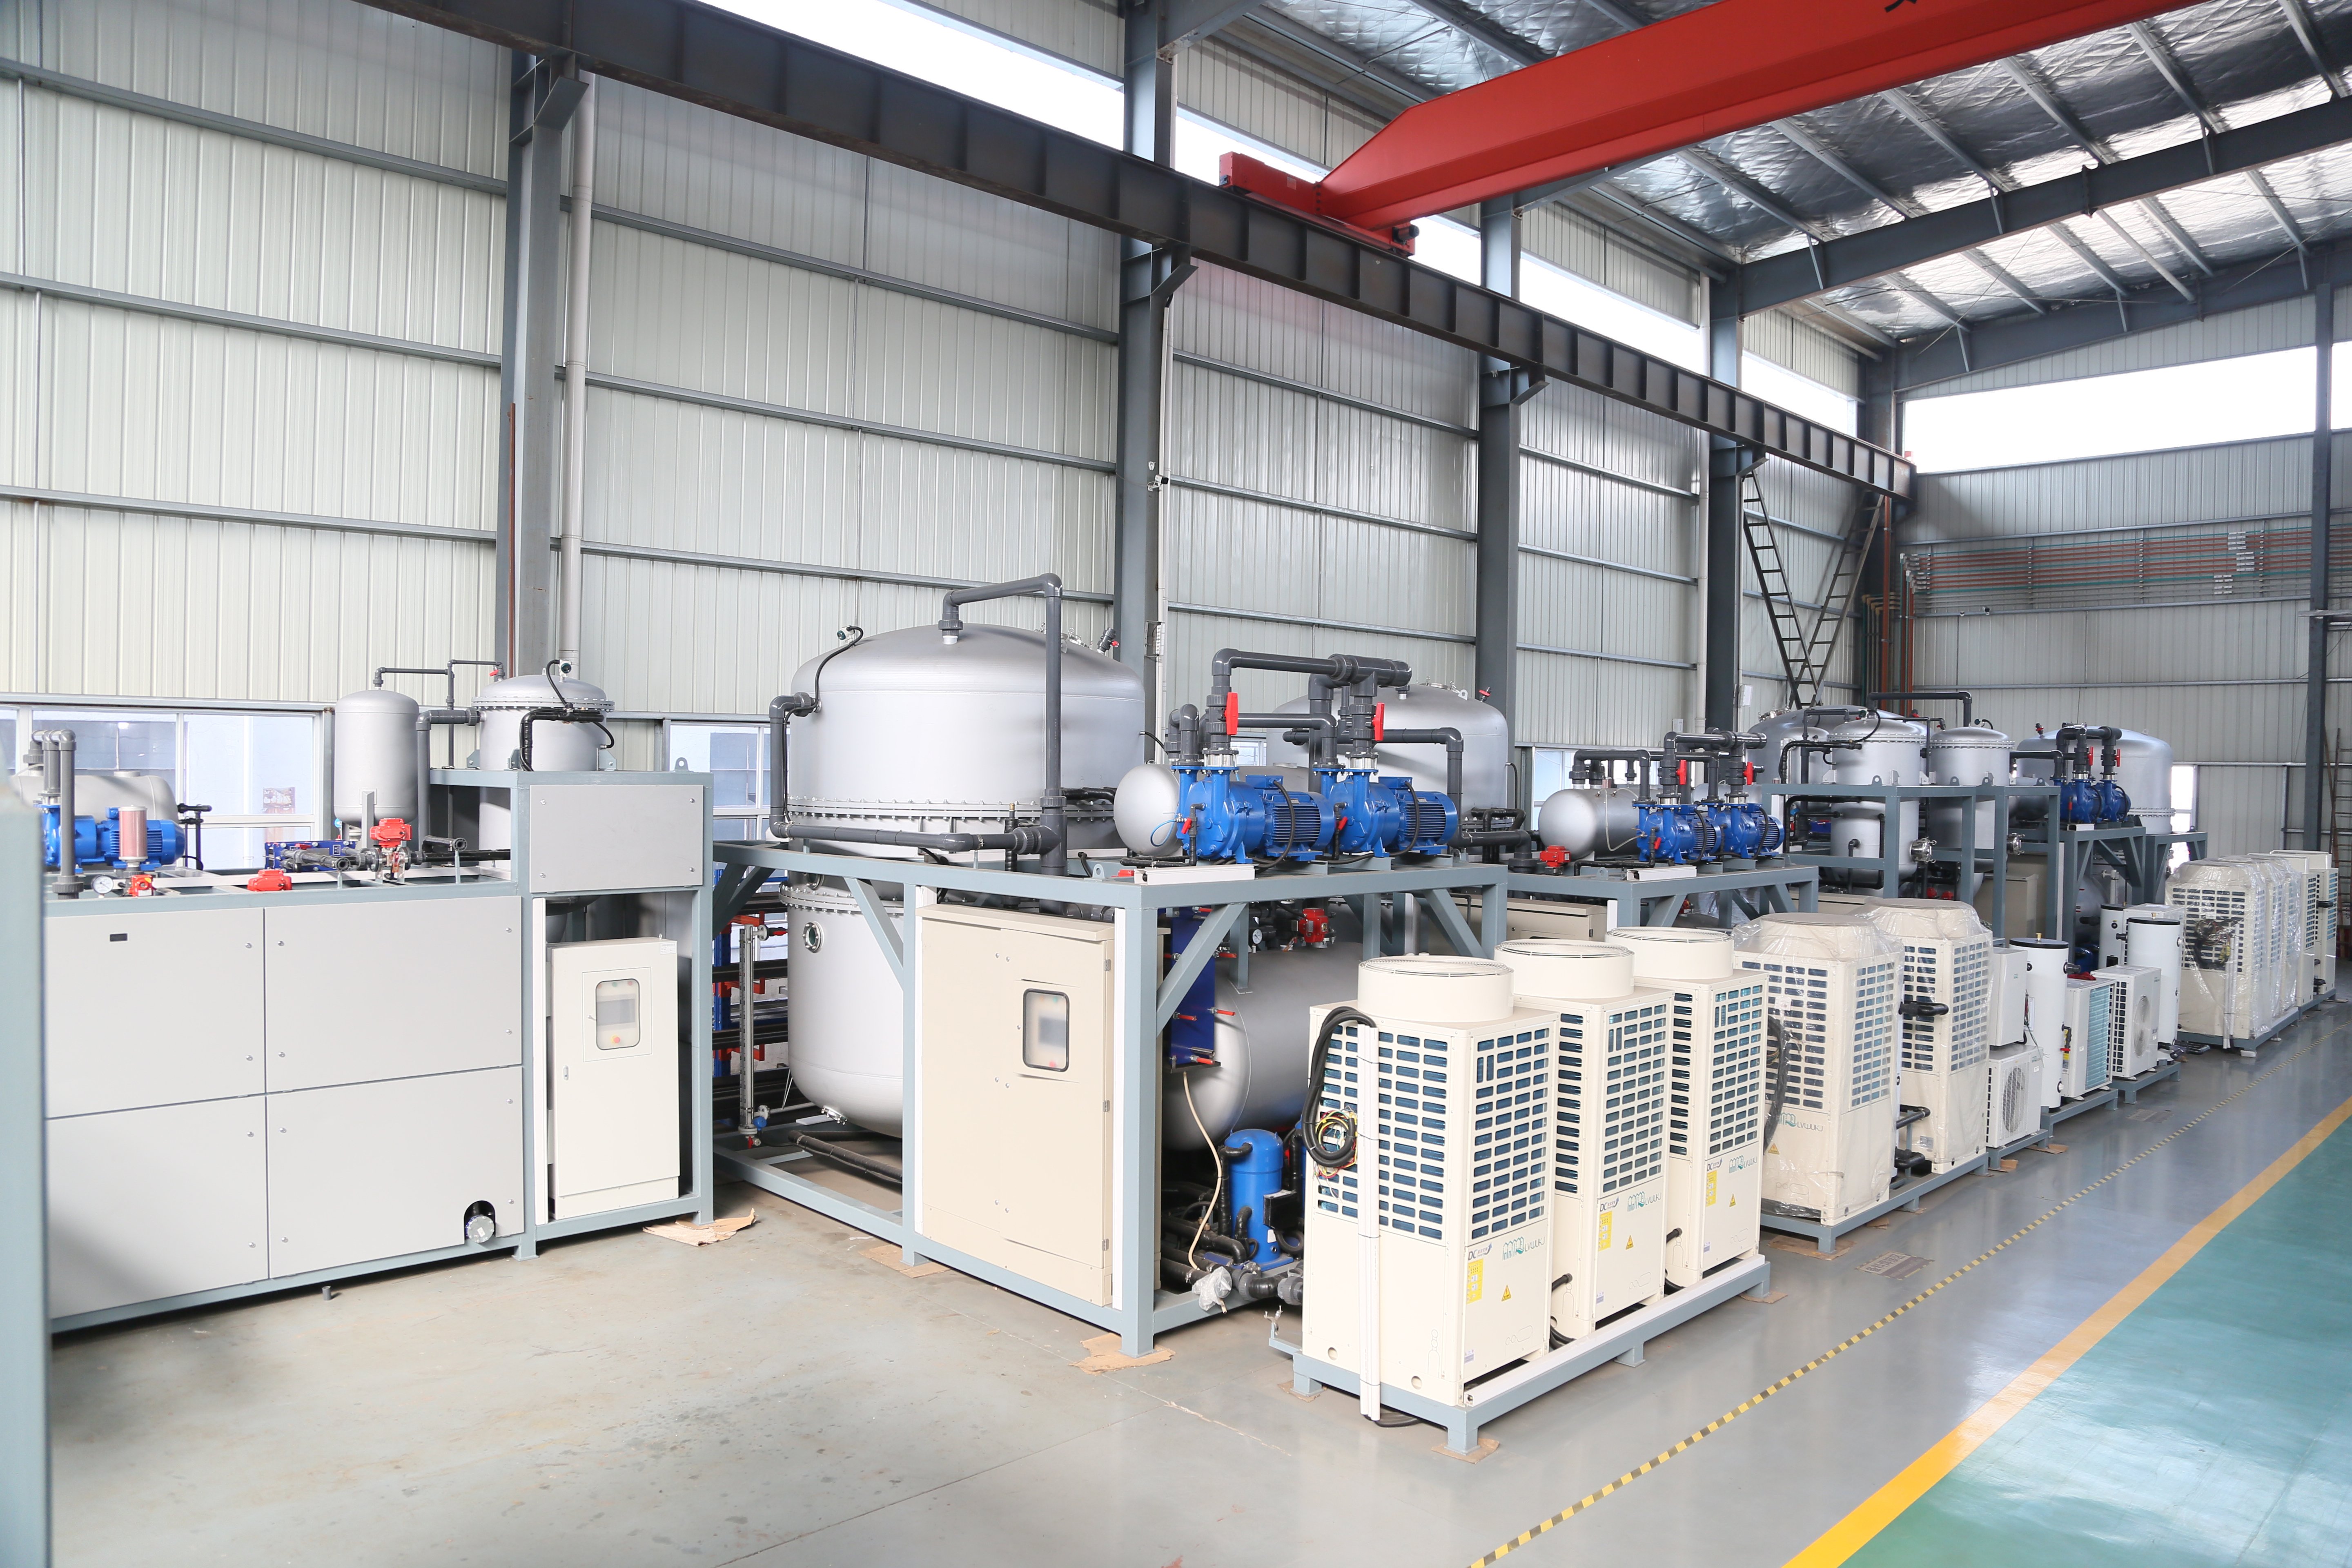
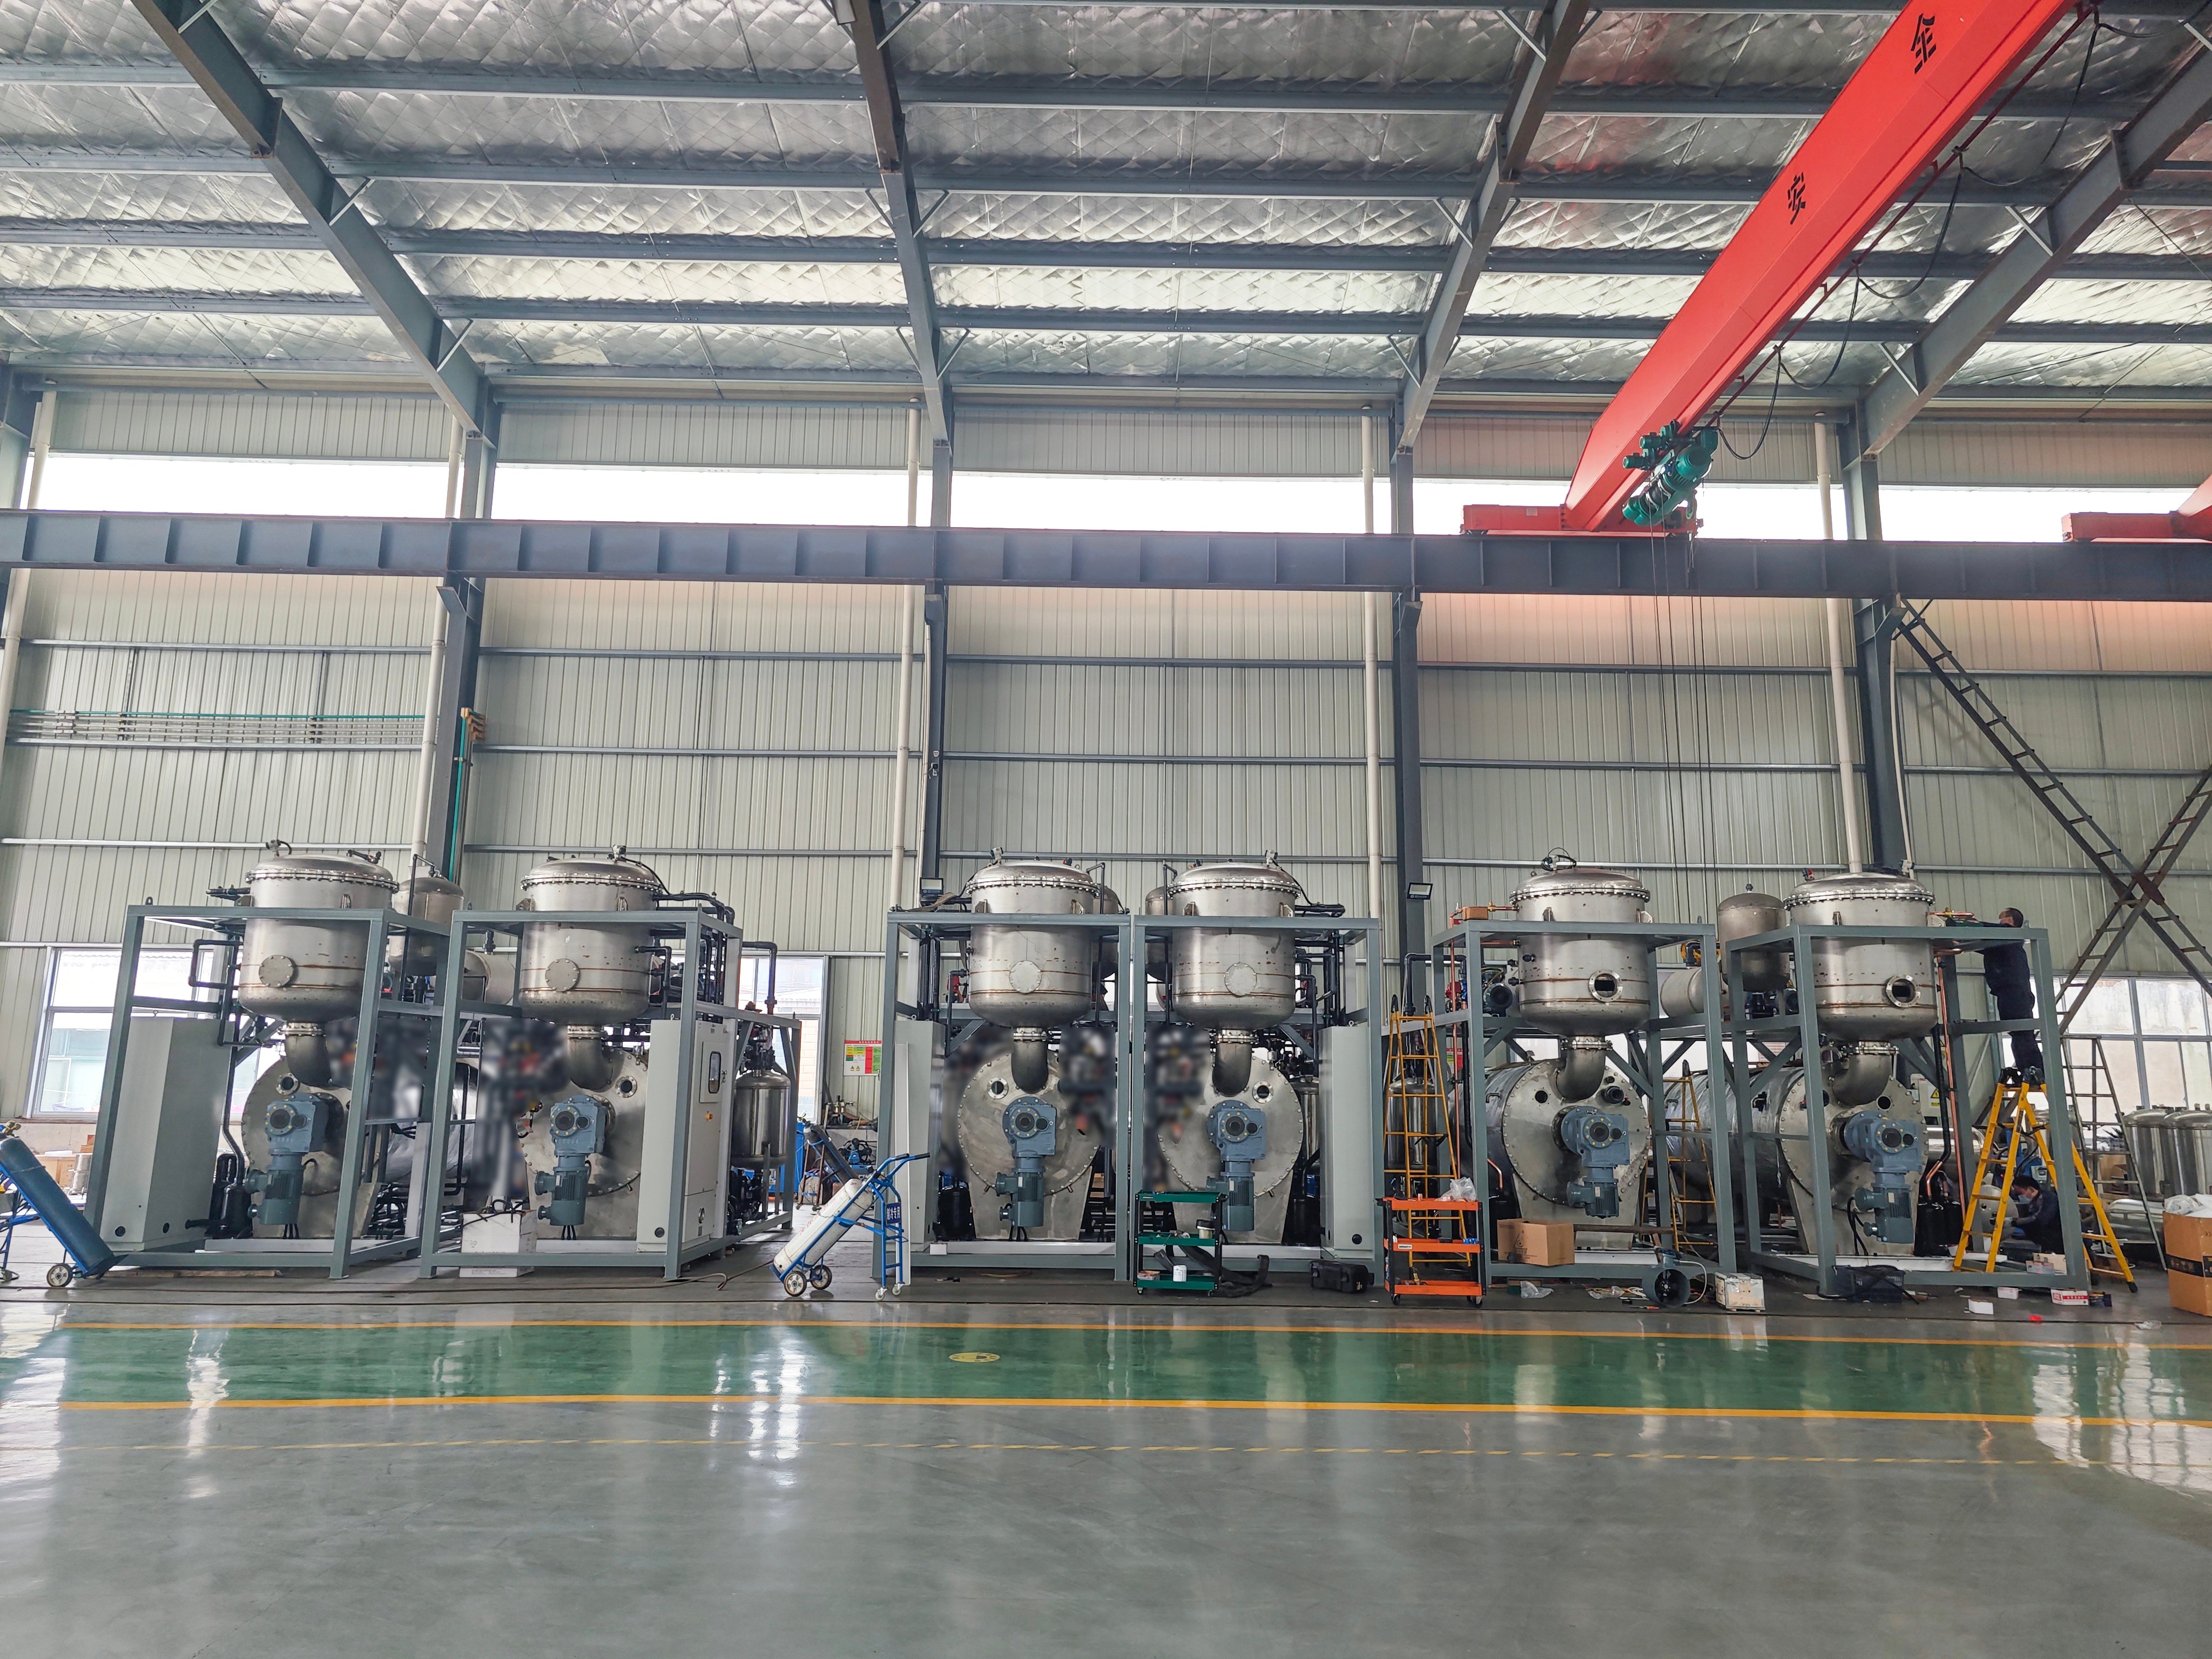
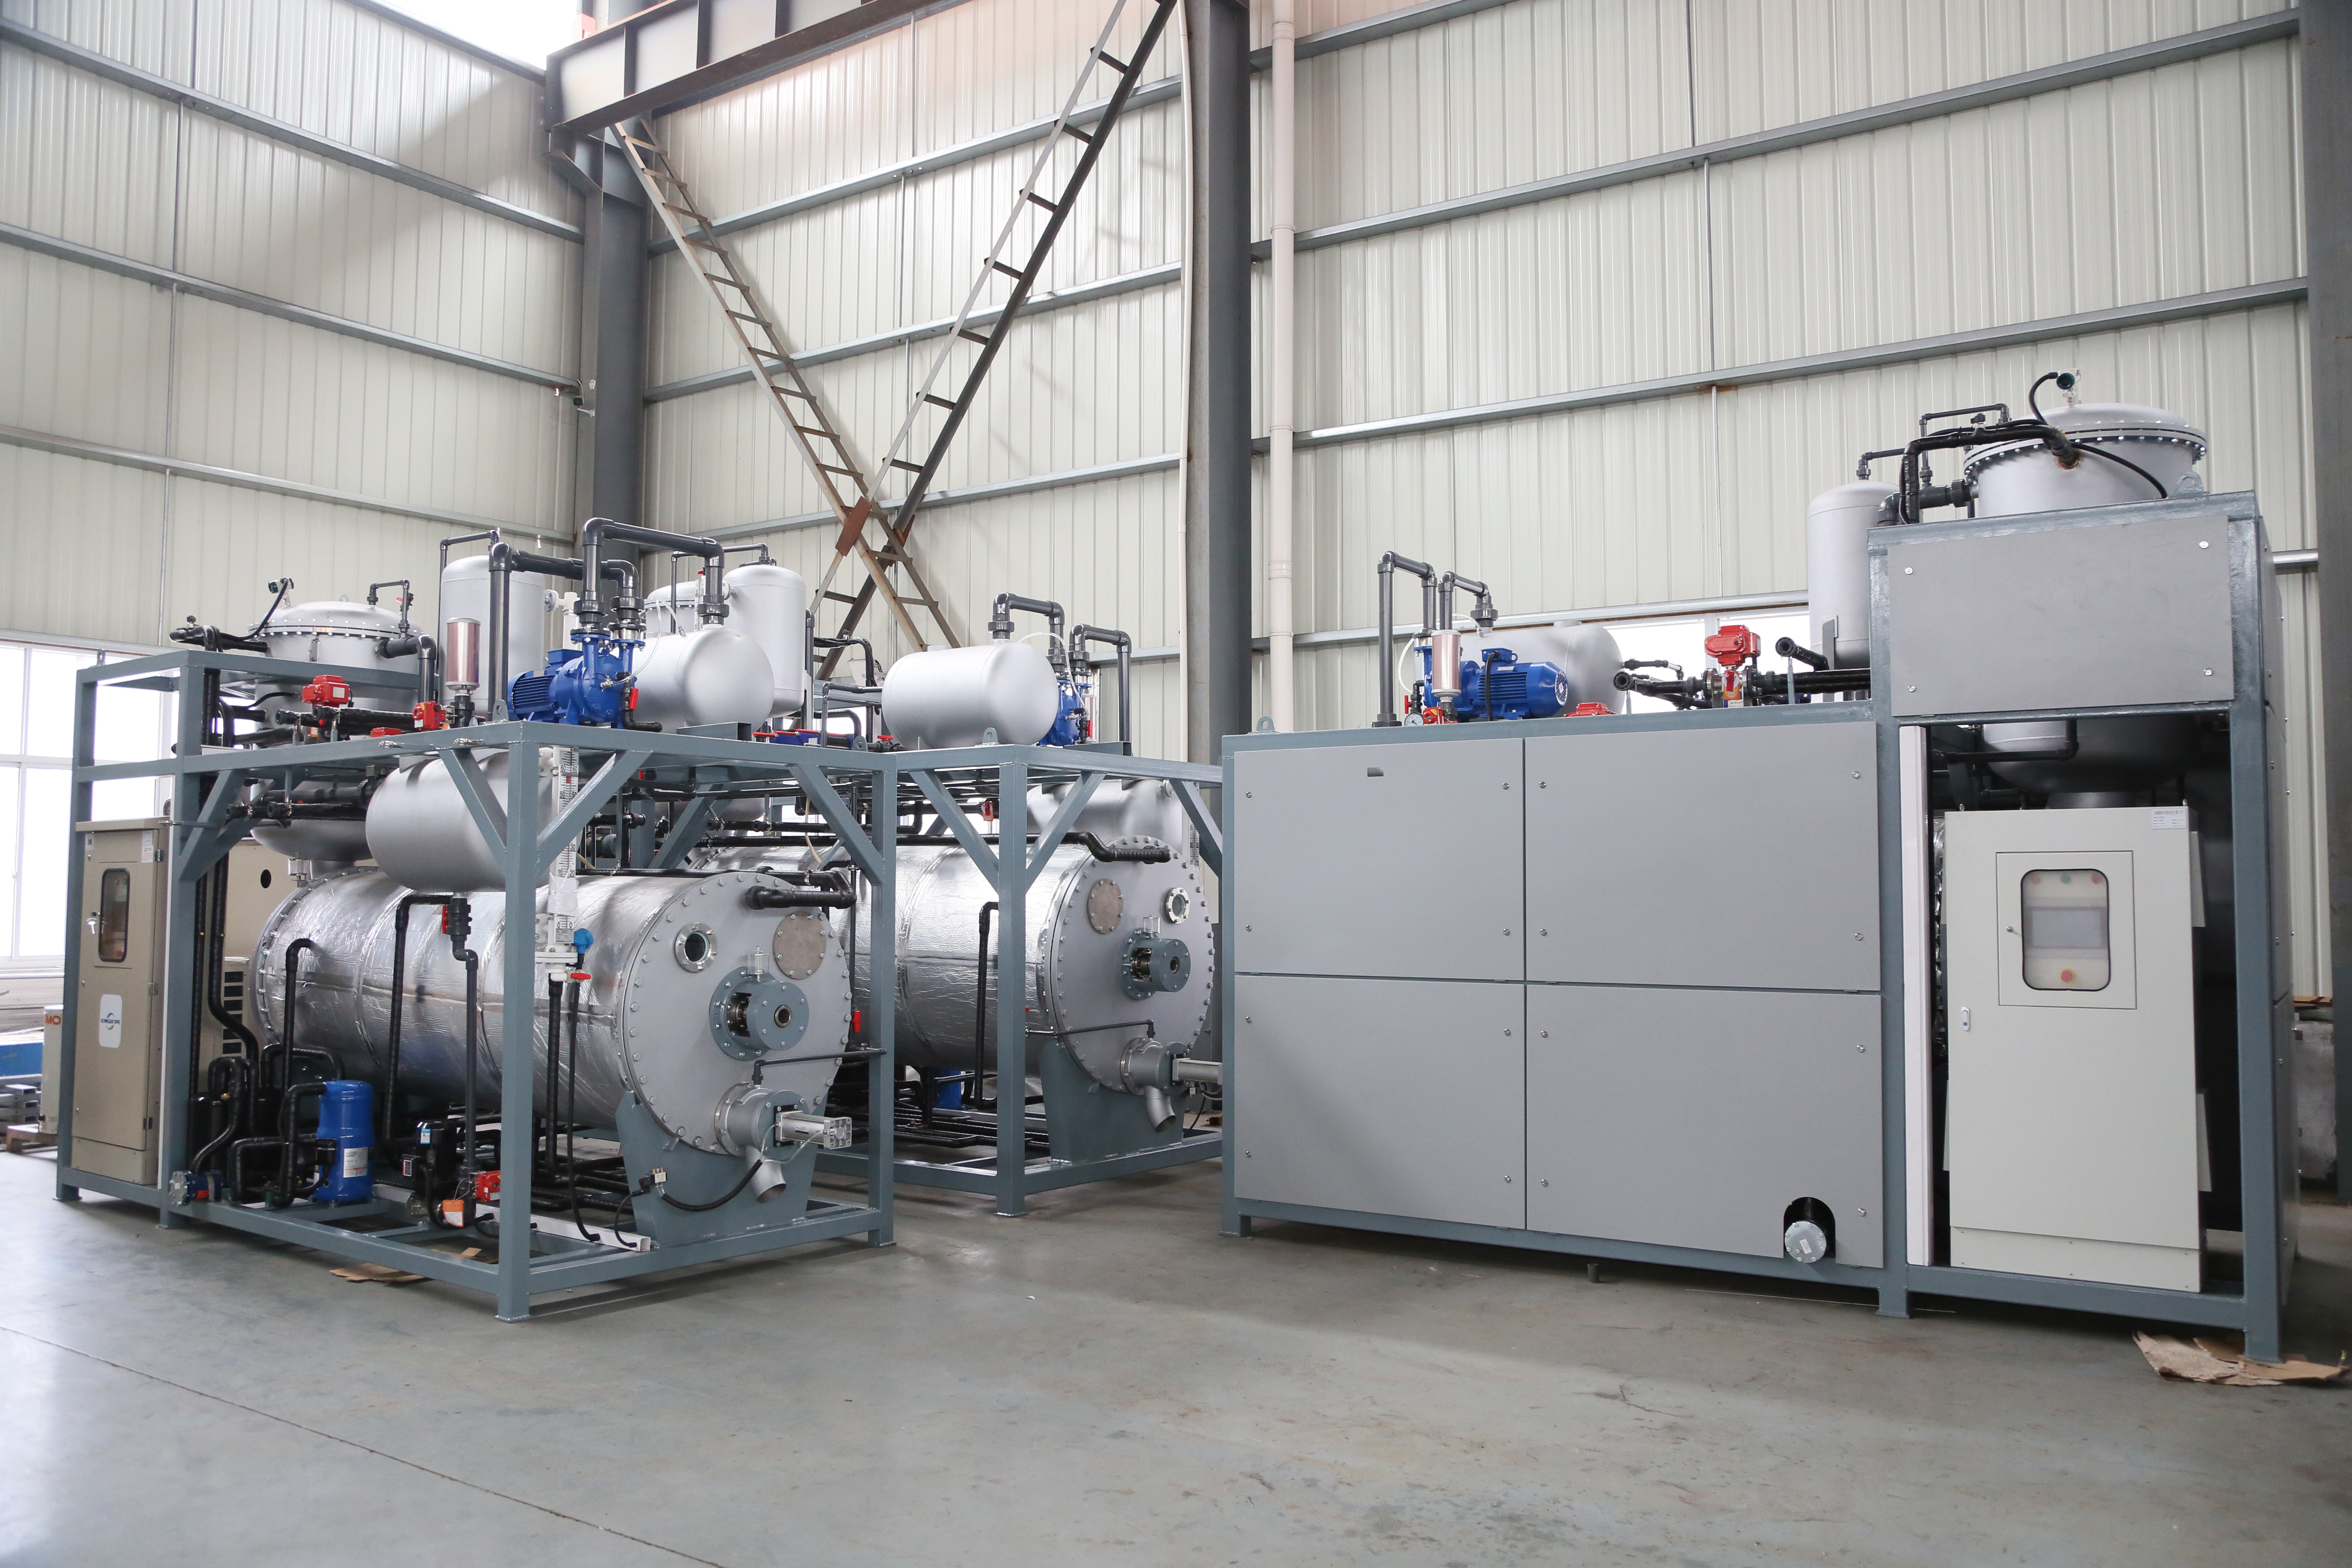
Low Temperature Heat Pump Evaporation Equipment

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

low temperature heat pump evaporation equipment

Low temperature heat pump evaporation equipment represents an advanced thermal management solution designed to handle demanding industrial and commercial applications. This innovative system operates efficiently at reduced temperature ranges, making it ideal for processes requiring precise thermal control. The low temperature heat pump evaporation equipment utilizes cutting-edge refrigeration technology to extract heat from fluid streams while simultaneously evaporating liquids in challenging conditions. The primary function of low temperature heat pump evaporation equipment is to concentrate liquid solutions and separate water or solvents from dissolved solids through a sustainable evaporation process. By maintaining lower operational temperatures, this equipment prevents thermal degradation of sensitive materials and reduces energy consumption compared to traditional evaporation systems. The technology integrates heat pump technology with evaporation chambers, allowing operators to recover and reuse thermal energy efficiently. Key technological features include variable-speed compressors, intelligent temperature control systems, and enhanced heat transfer surfaces that maximize efficiency. The low temperature heat pump evaporation equipment accommodates various industrial applications, from pharmaceutical and food processing to chemical manufacturing and wastewater treatment. Its modular design allows customization for specific operational requirements, while robust construction ensures durability in demanding environments. The system operates with minimal environmental impact, utilizing eco-friendly refrigerants and reducing overall carbon footprint through optimized energy recovery mechanisms.

New Product Releases

Low temperature heat pump evaporation equipment delivers substantial operational and financial benefits for industrial organizations. The primary advantage lies in energy efficiency—this equipment consumes significantly less power than conventional evaporation systems by capturing and reusing waste heat throughout the process. Operating at reduced temperatures protects sensitive compounds from thermal damage, making the low temperature heat pump evaporation equipment essential for pharmaceutical, cosmetic, and specialty chemical applications. Financial benefits are compelling. The low temperature heat pump evaporation equipment reduces operational costs through lower energy consumption and minimal maintenance requirements. Users experience faster return on investment due to improved process efficiency and reduced thermal losses. The equipment handles larger evaporation volumes without proportionally increasing energy input, translating to superior cost-per-unit metrics across production scales. Operational advantages include consistent product quality and enhanced process control. The system's intelligent temperature management ensures uniform evaporation rates, preventing product degradation and maintaining desired material properties. Installation flexibility accommodates various facility configurations, from compact spaces to large-scale industrial plants. The low temperature heat pump evaporation equipment requires minimal operator intervention thanks to automated controls and real-time monitoring systems. Environmental suitability makes this technology attractive for sustainability-focused organizations. Reduced energy consumption directly decreases operational carbon emissions, supporting corporate environmental goals. The equipment's reliability and longevity minimize replacement frequency and associated waste. Industries handling volatile or hazardous liquids benefit from the low temperature heat pump evaporation equipment's ability to manage these materials safely while maintaining workplace safety standards and regulatory compliance.

Latest News

Benefits of Low Temperature Heat Pump Evaporator in Industry

24

Jul

Benefits of Low Temperature Heat Pump Evaporator in Industry

Industrial facilities worldwide face mounting pressure to reduce operating costs while maintaining production quality and environmental compliance. The low temperature heat pump evaporator has emerged as a transformative solution that addresses these...
View More
Industrial Wastewater Treatment Systems: Buyer's Guide

02

Sep

Industrial Wastewater Treatment Systems: Buyer's Guide

Selecting the right industrial wastewater treatment systems represents one of the most critical infrastructure decisions for manufacturing, processing, and production facilities. Industrial wastewater treatment systems handle complex liquid waste str...
View More
How Low Temperature Heat Pump Evaporator Cuts Energy Costs

24

Jul

How Low Temperature Heat Pump Evaporator Cuts Energy Costs

Industrial operations consume significant energy, and equipment efficiency directly impacts profitability. A low temperature heat pump evaporator represents a transformative approach to reducing energy expenditure while maintaining operational perfor...
View More
Vacuum Distillation: Key Benefits for Industrial Use

24

Jul

Vacuum Distillation: Key Benefits for Industrial Use

Vacuum distillation has become an essential separation technology across numerous industrial sectors, offering superior performance compared to conventional atmospheric distillation methods. By operating under reduced pressure conditions, vacuum dist...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

low temperature heat pump evaporation equipment

Superior Energy Efficiency Through Heat Recovery

Superior Energy Efficiency Through Heat Recovery

The low temperature heat pump evaporation equipment incorporates advanced heat recovery technology that captures thermal energy typically wasted in conventional systems. This sophisticated mechanism extracts heat from exhaust streams and reintroduces it into the evaporation process, dramatically reducing overall energy consumption. The system's variable-speed compressor adjusts operational intensity based on real-time processing demands, optimizing efficiency across varying production loads. Users typically experience 40-60% energy savings compared to traditional evaporation methods. The low temperature heat pump evaporation equipment's heat recovery capabilities translate directly into reduced utility bills and lower operational expenses. This energy efficiency advantage proves particularly valuable for continuous-operation facilities processing large liquid volumes, where cumulative energy savings reach substantial annual figures and significantly improve profitability margins.
Precise Temperature Control for Sensitive Materials

Precise Temperature Control for Sensitive Materials

Low temperature heat pump evaporation equipment excels at managing temperature-sensitive compounds that degrade under conventional high-heat processing. The system maintains strict temperature parameters through intelligent control algorithms and real-time sensor feedback, ensuring optimal conditions throughout evaporation cycles. This precision prevents unwanted chemical reactions, preserves product potency, and maintains material integrity that premium applications demand. Industries handling pharmaceuticals, essential oils, and specialty chemicals benefit enormously from the low temperature heat pump evaporation equipment's capability to process delicate substances without compromising quality. The equipment's ability to operate at temperatures 30-50 degrees lower than traditional systems enables processors to handle materials previously considered unsuitable for cost-effective evaporation. This technological advantage opens new market opportunities and allows manufacturers to expand product portfolios while maintaining stringent quality standards and regulatory certifications.
Minimal Environmental Impact and Sustainable Operations

Minimal Environmental Impact and Sustainable Operations

The low temperature heat pump evaporation equipment represents an environmentally responsible choice for modern industrial operations. The system utilizes eco-friendly refrigerants and generates minimal thermal emissions, supporting corporate sustainability initiatives and meeting increasingly strict environmental regulations. Reduced energy consumption directly correlates with decreased carbon footprint, making this technology attractive for organizations committed to climate-positive practices. The low temperature heat pump evaporation equipment's longevity and reliability minimize replacement frequency, reducing electronic waste and manufacturing impacts. The system's efficient design eliminates unnecessary heat discharge into surrounding environments, preventing thermal pollution. Industrial facilities adopting low temperature heat pump evaporation equipment demonstrate measurable environmental commitments while maintaining profitability through operational cost reductions. This alignment of environmental responsibility with economic advantage positions the technology as essential infrastructure for forward-thinking manufacturers seeking competitive advantages through sustainable excellence.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000