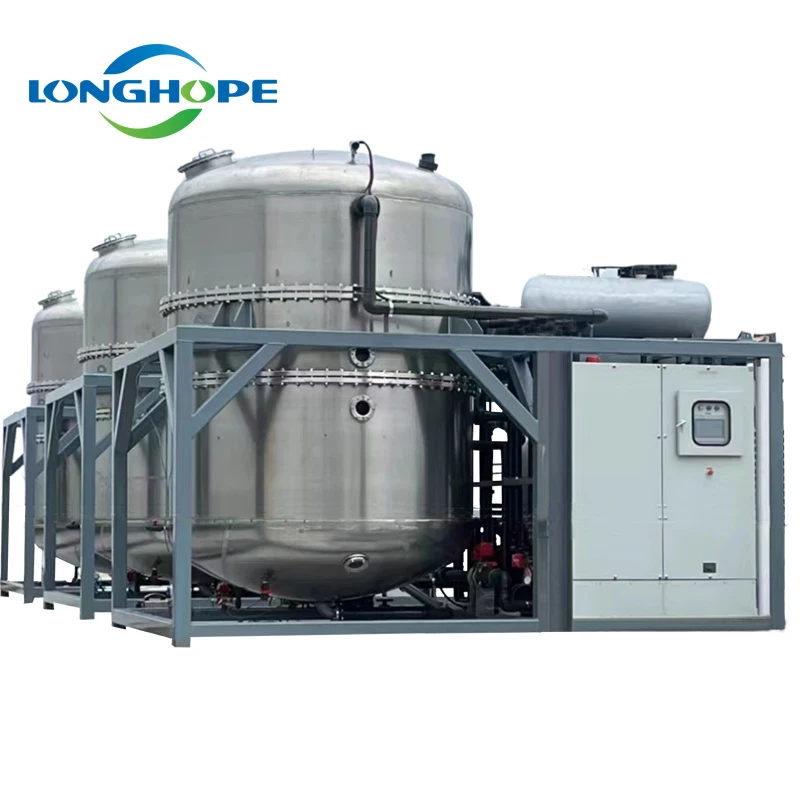
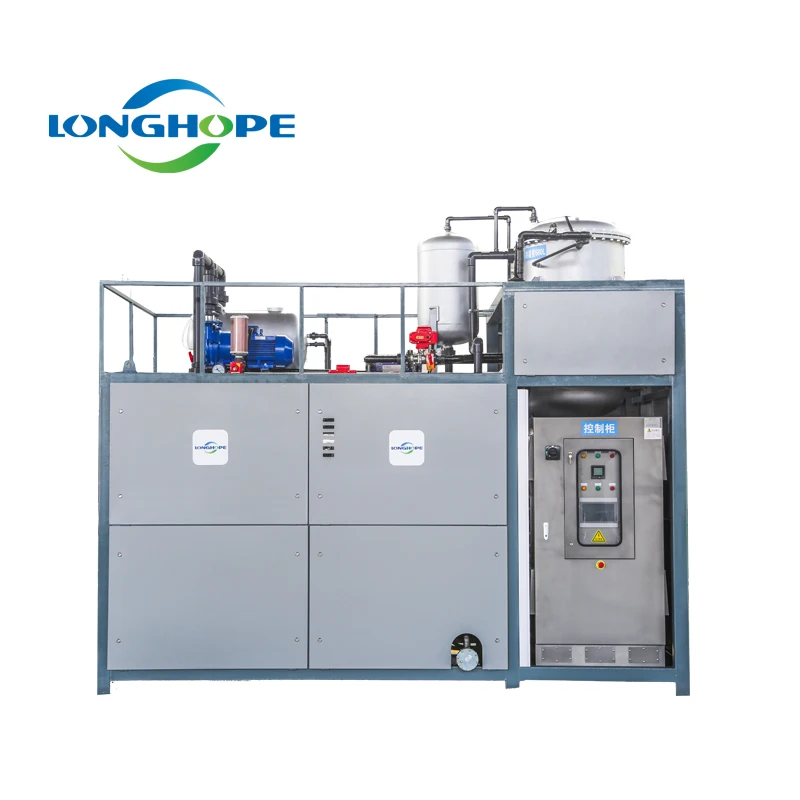
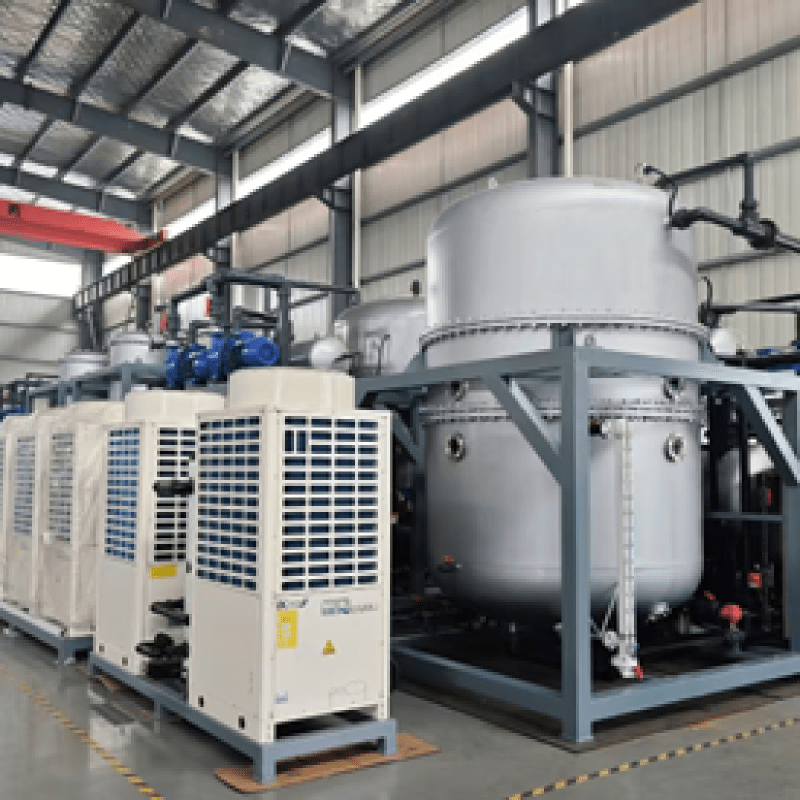
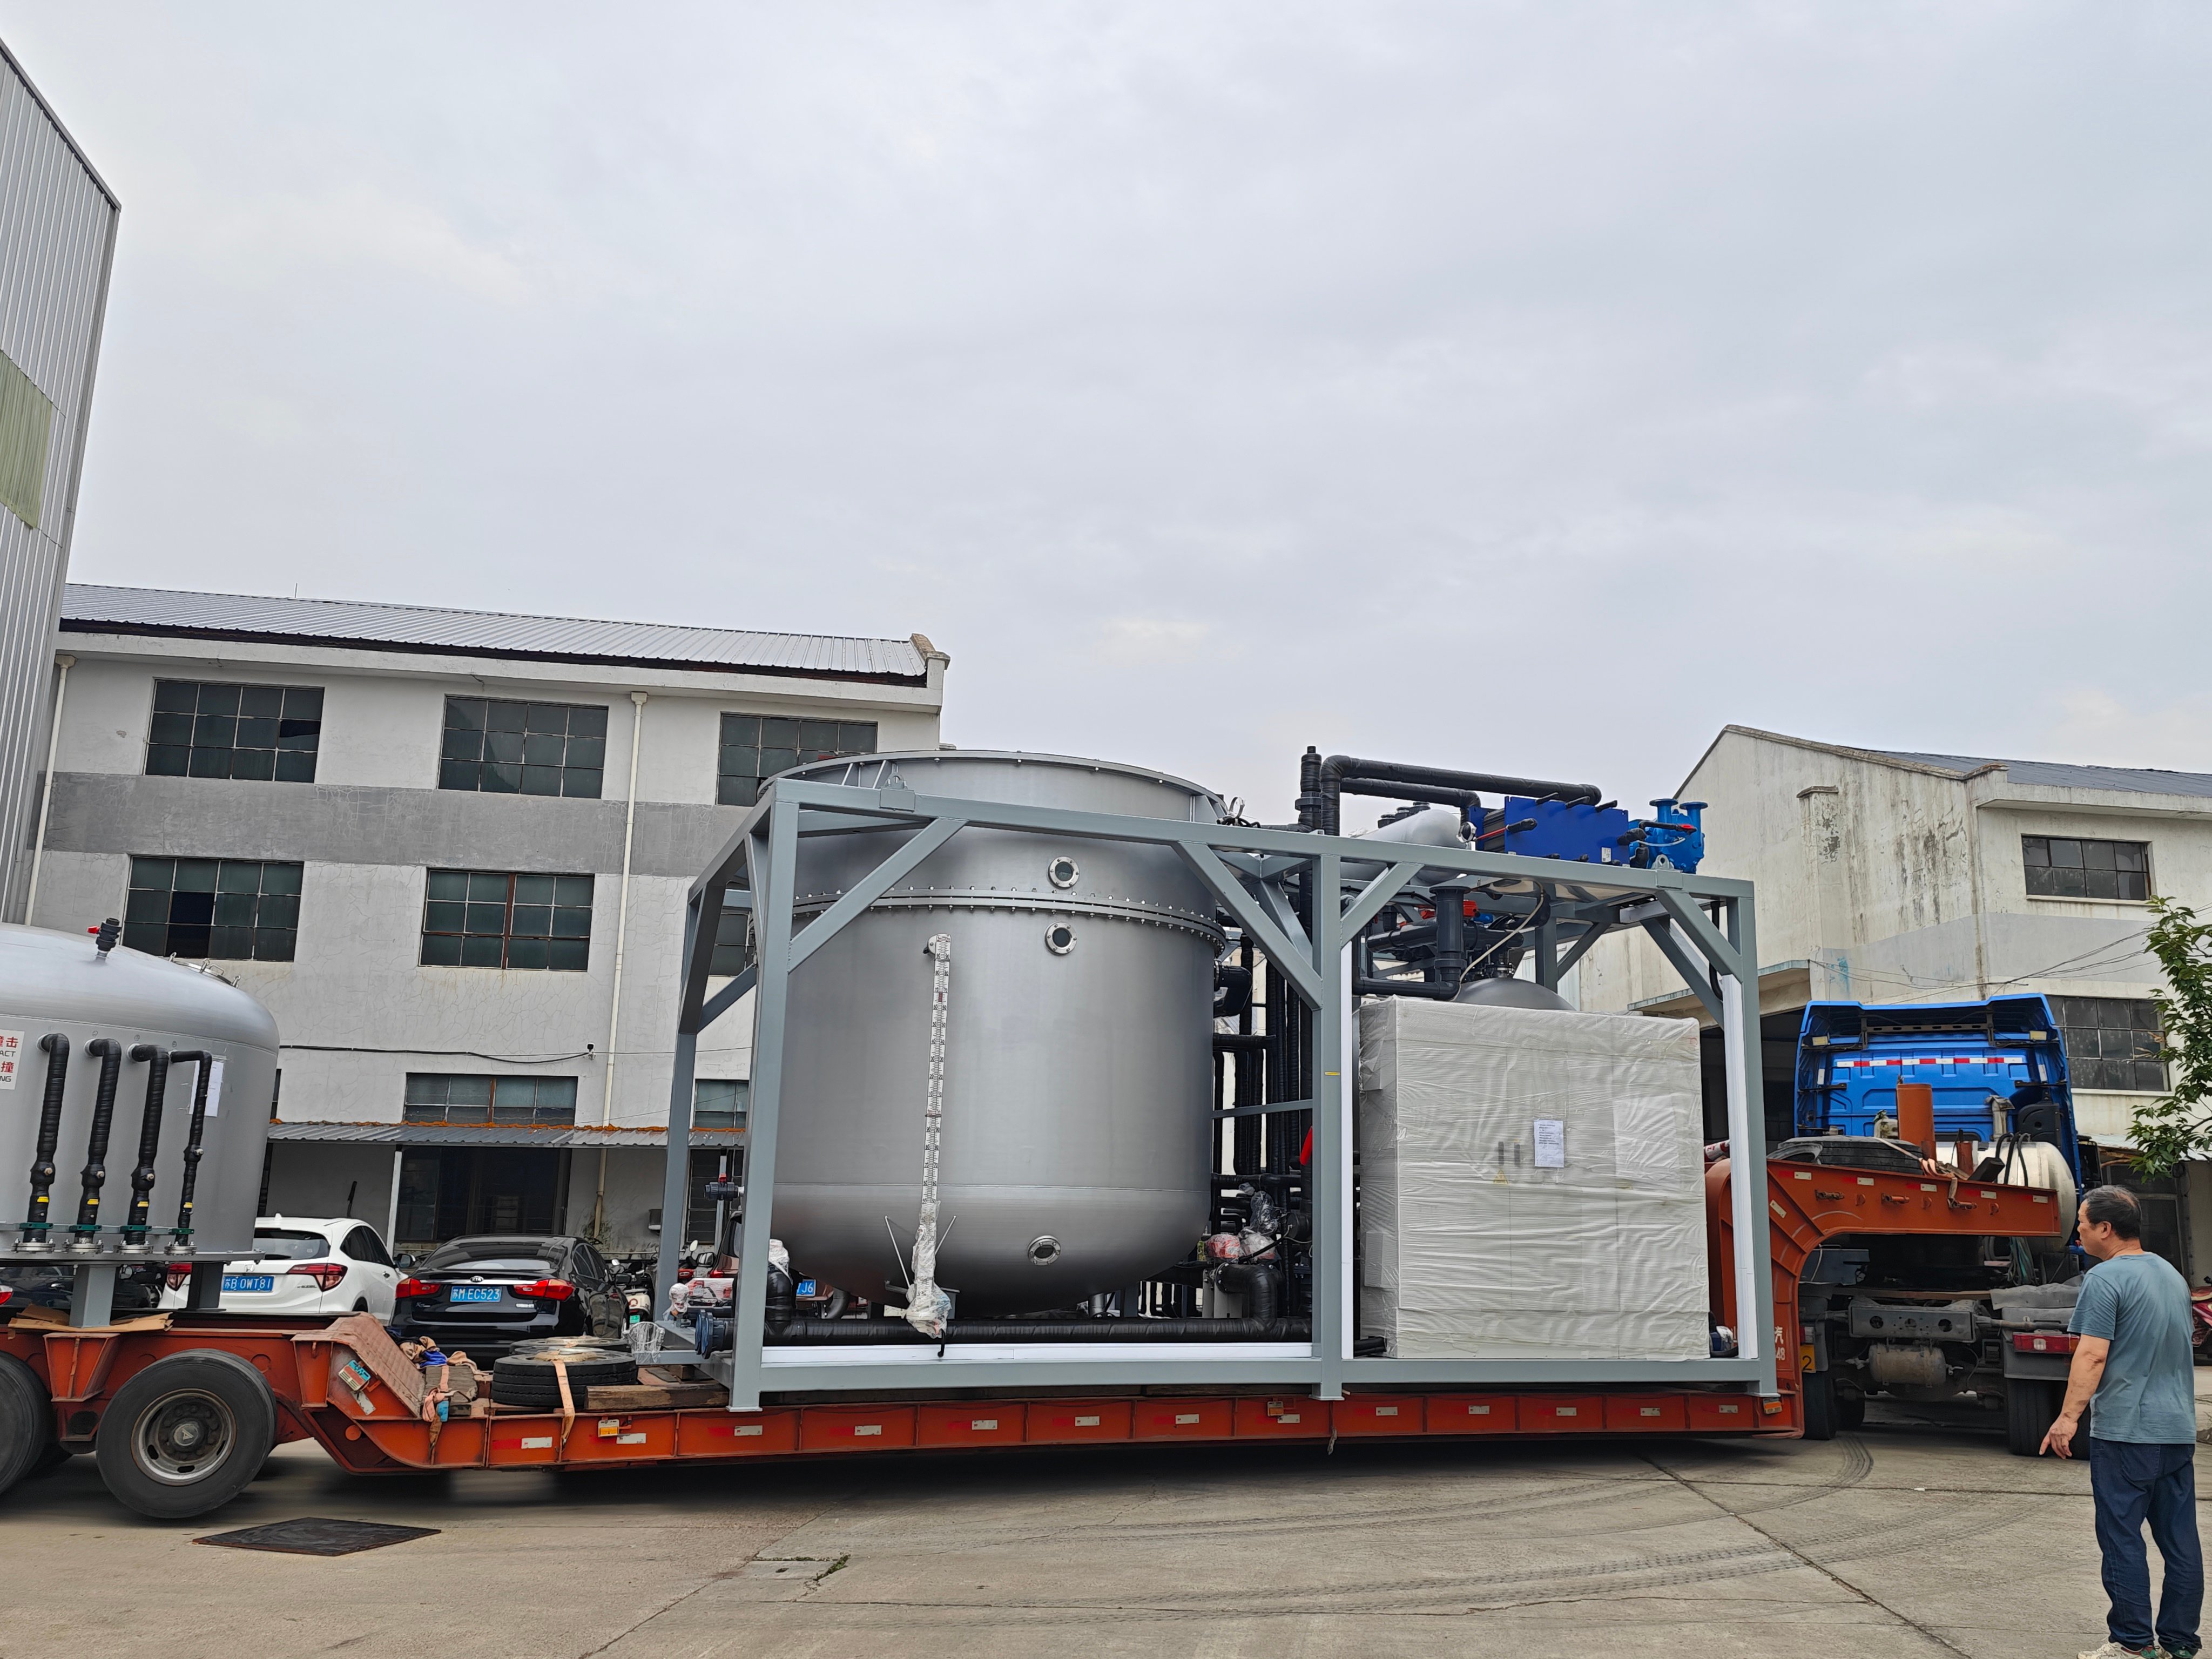
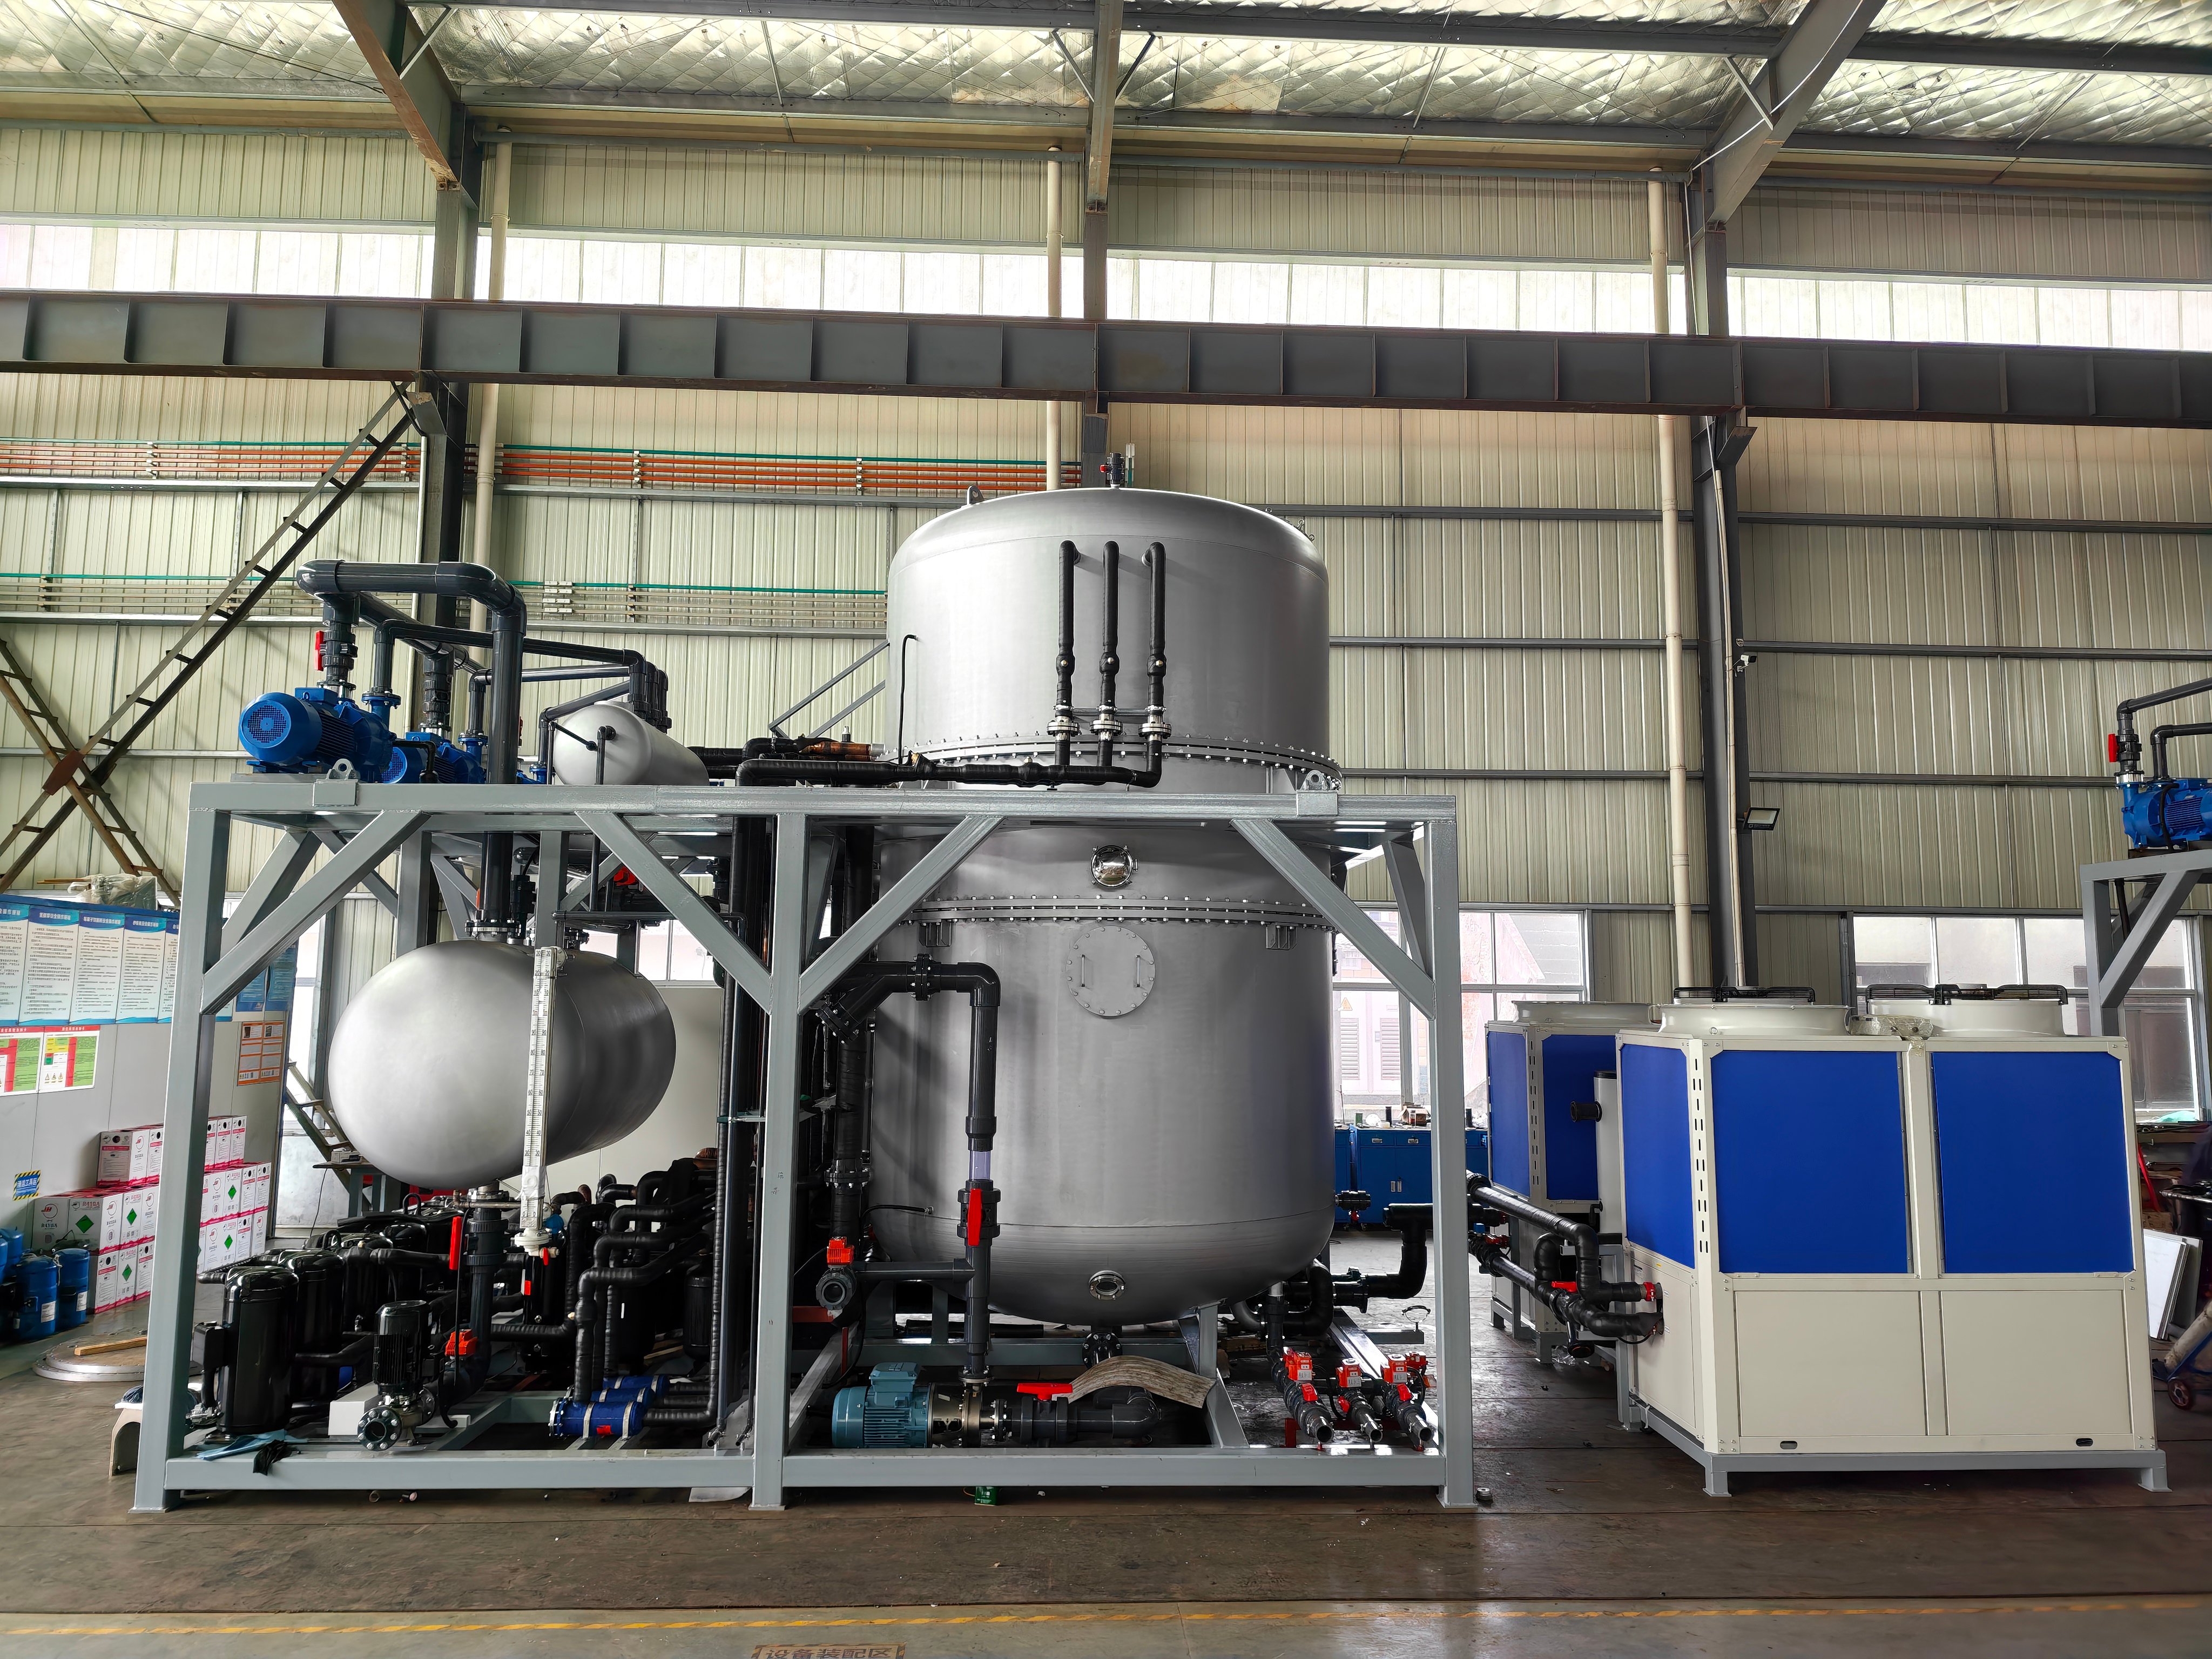
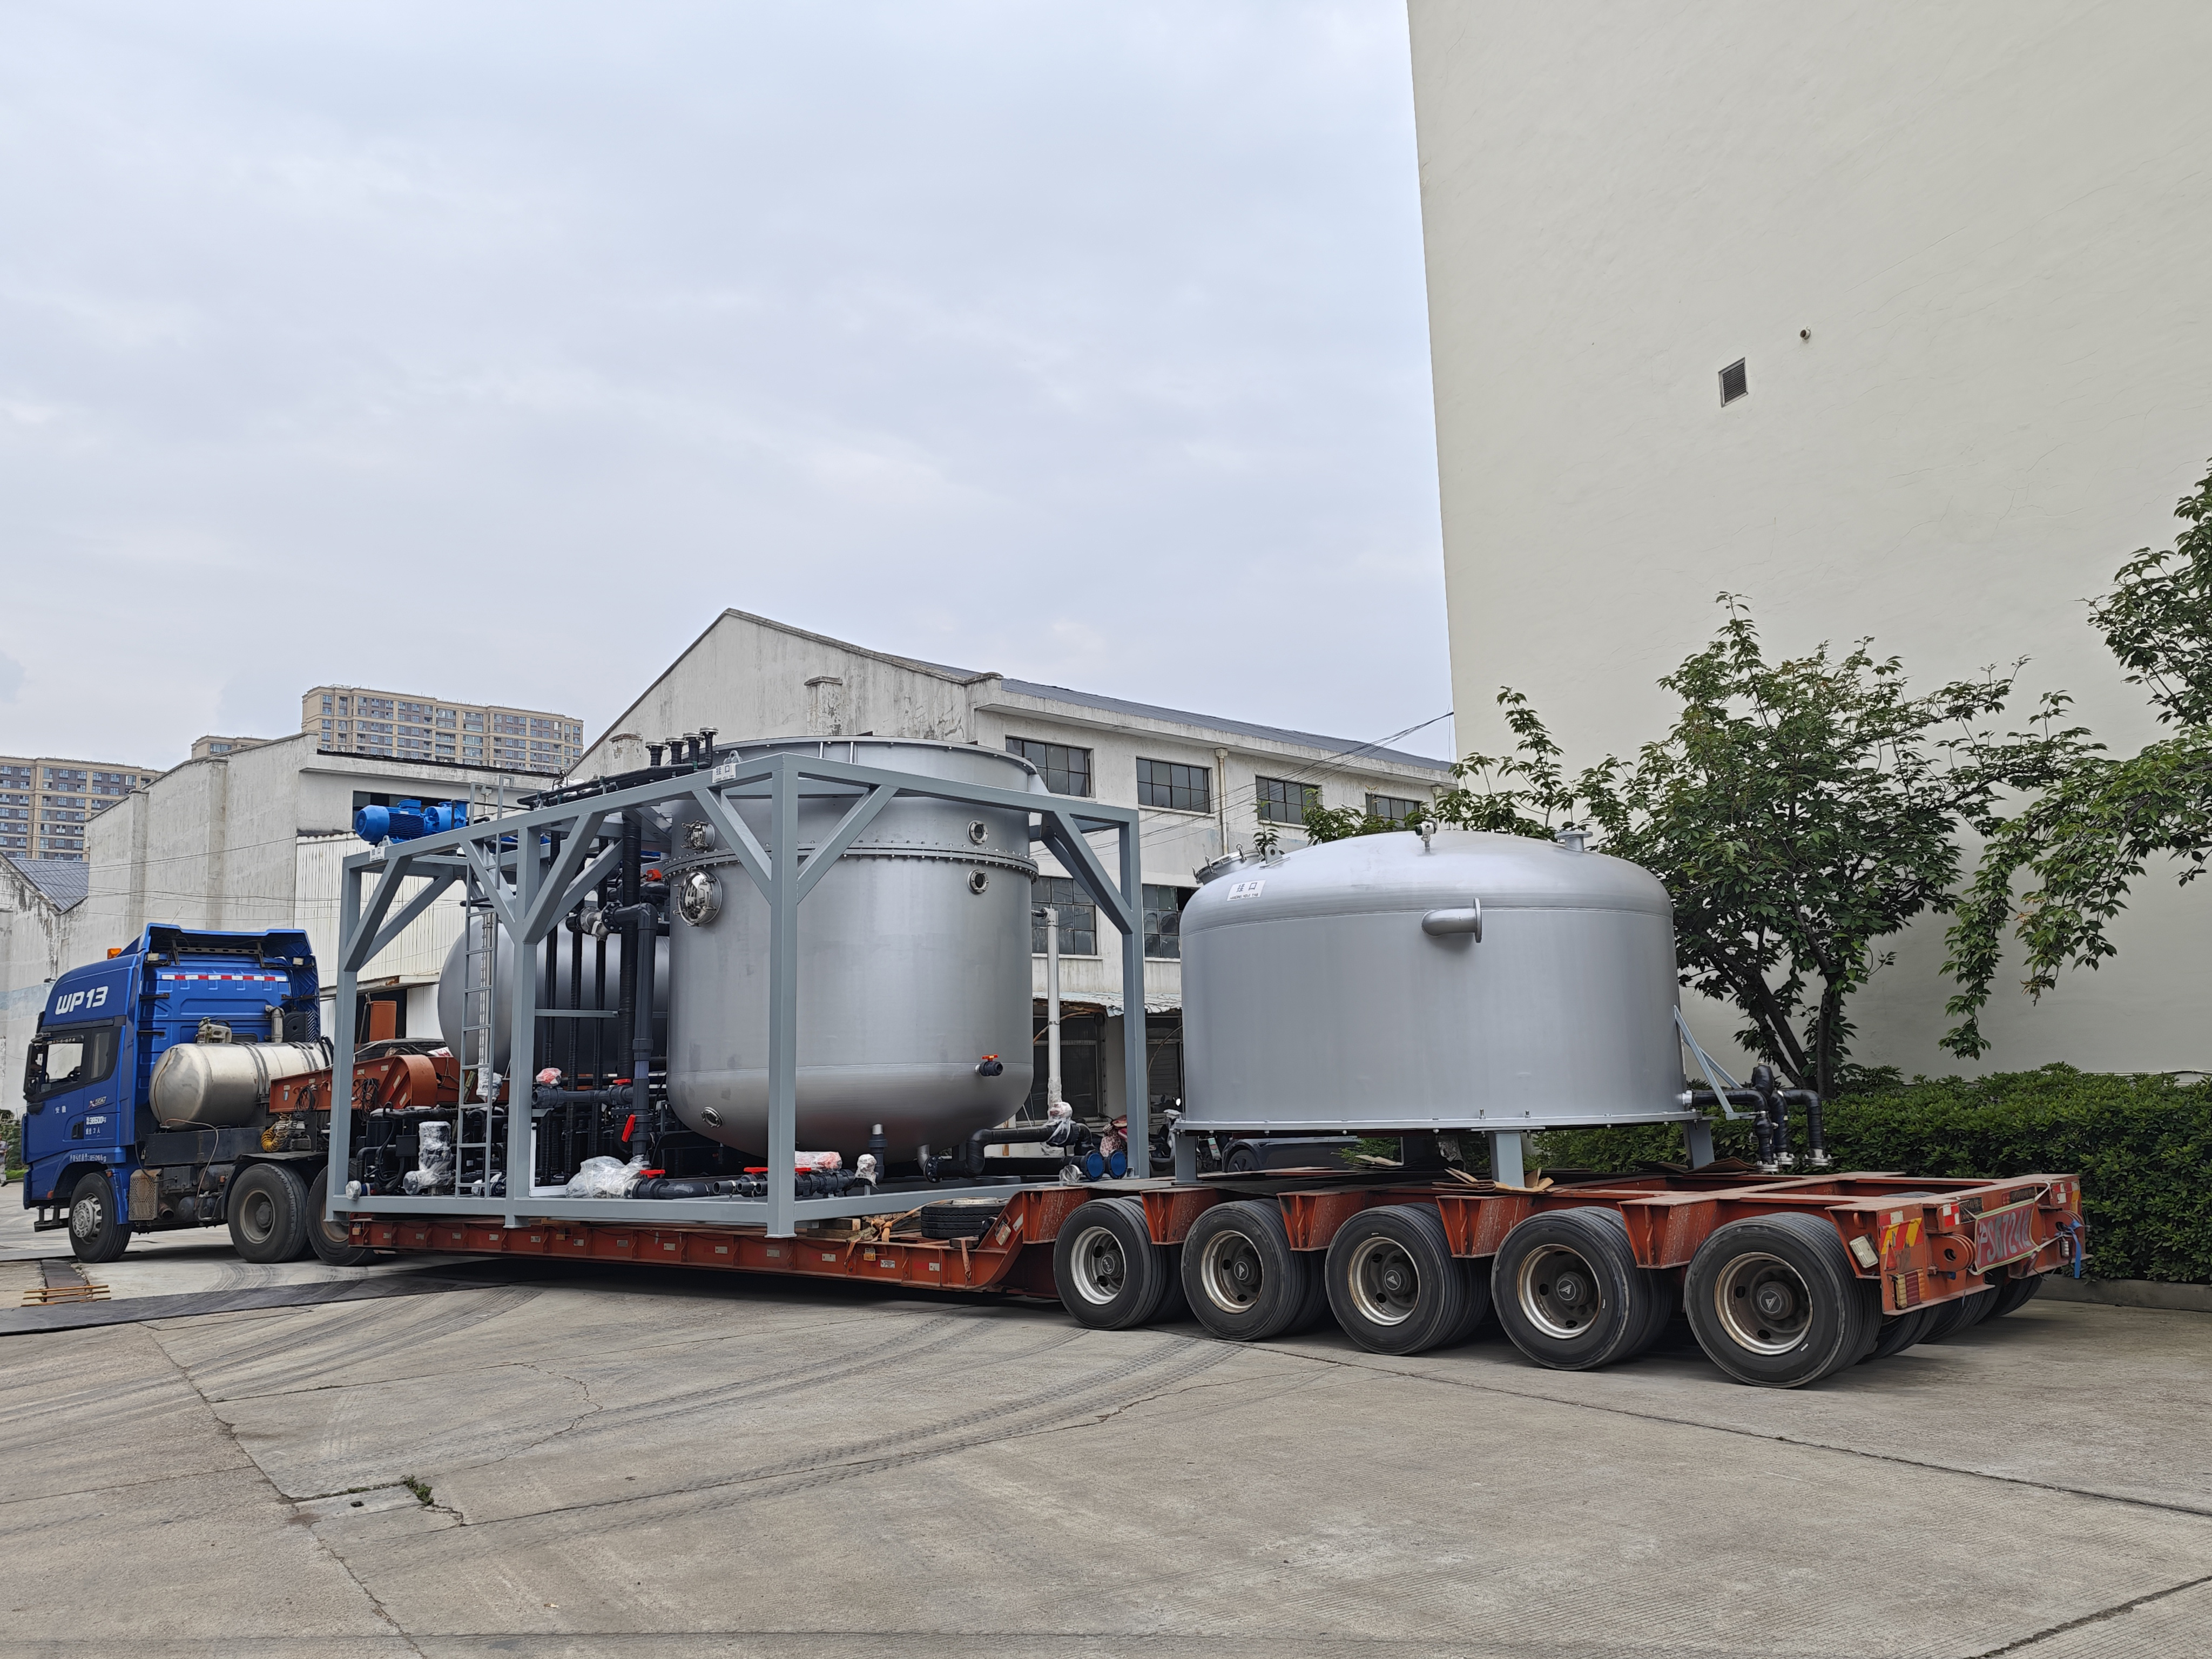
Vacuum Evaporation Concentration System

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

vacuum evaporation concentration system

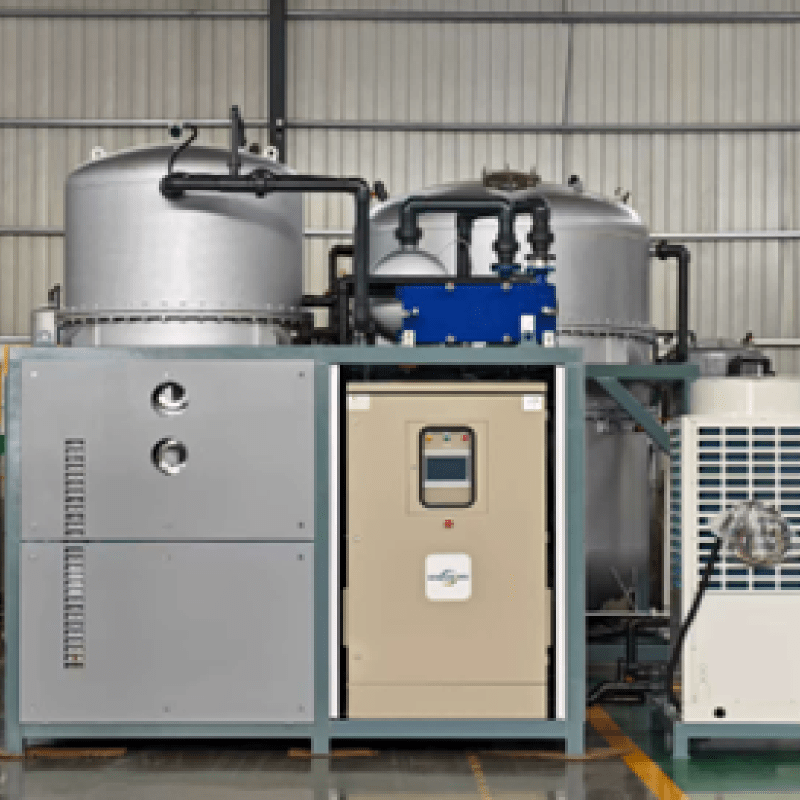
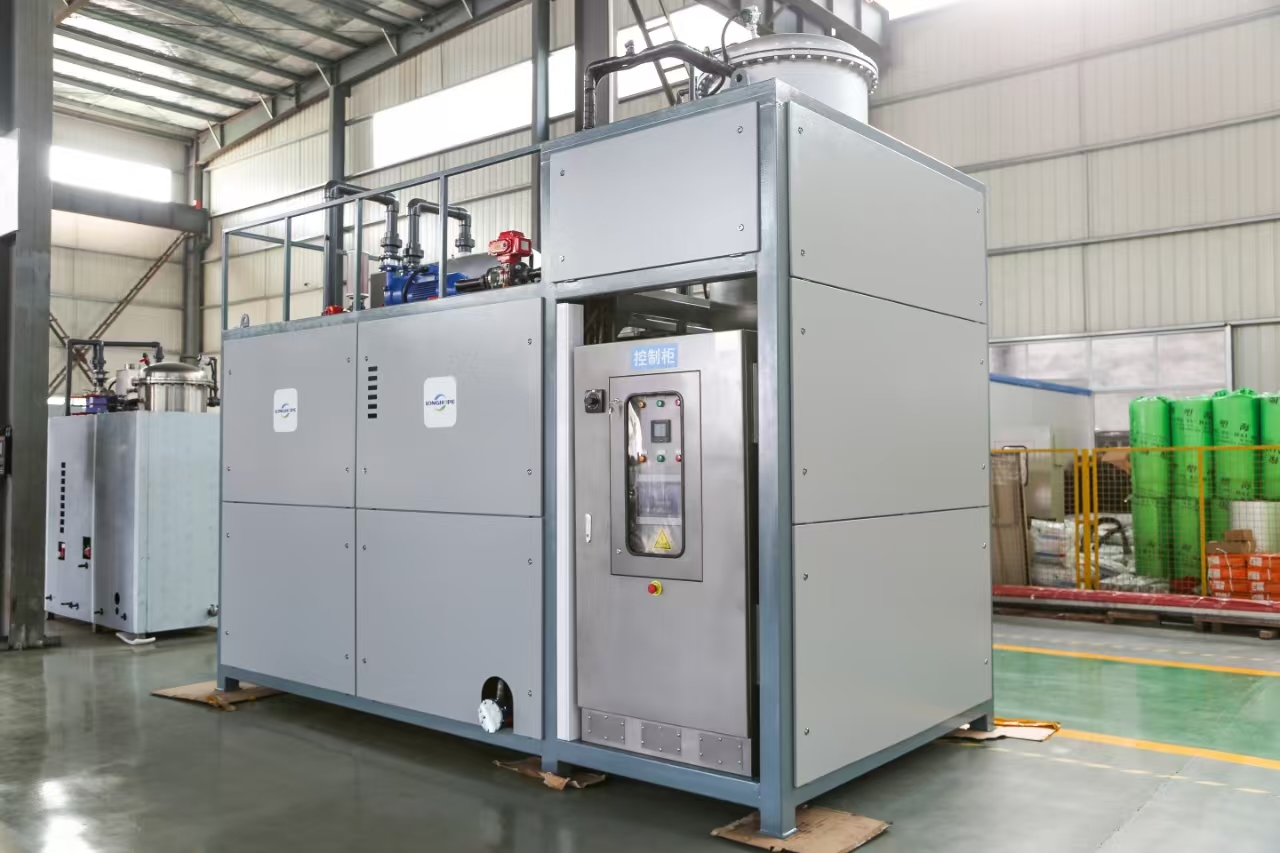
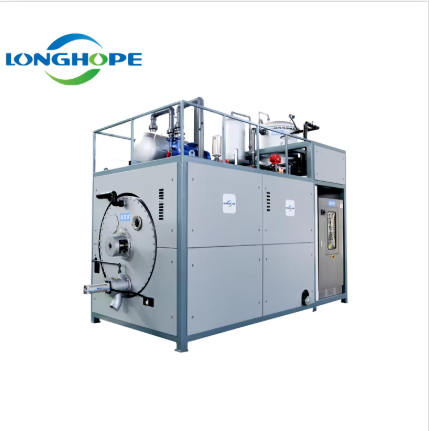
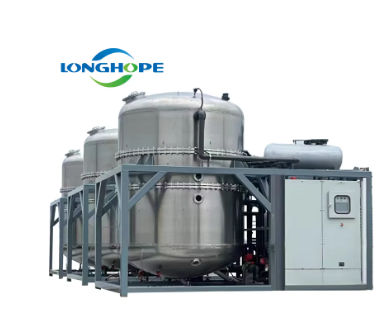
A vacuum evaporation concentration system is an advanced industrial technology designed to remove solvents and moisture from liquid solutions through controlled evaporation under reduced pressure conditions. This vacuum evaporation concentration system operates by lowering atmospheric pressure within a sealed chamber, which significantly reduces the boiling point of liquids, allowing efficient separation without excessive heat exposure. The vacuum evaporation concentration system is particularly valuable for processing heat-sensitive materials, pharmaceuticals, chemicals, and food products that would degrade under conventional heating methods. The primary function of a vacuum evaporation concentration system involves transforming dilute solutions into concentrated forms by selectively removing unwanted liquid components. This process enhances product quality, reduces storage and transportation costs, and improves overall operational efficiency. Key technological features include precision temperature control, automated monitoring systems, and corrosion-resistant materials that ensure reliable long-term performance. The vacuum evaporation concentration system utilizes multiple effect stages and advanced condenser technology to maximize energy efficiency while minimizing operational expenses. Applications span across diverse industries. Pharmaceutical manufacturers rely on this technology to concentrate active ingredients while preserving their therapeutic properties. Food and beverage producers use vacuum evaporation concentration systems to create concentrated juices, syrups, and extracts. Chemical processing facilities employ this equipment for solvent recovery and waste reduction. Environmental remediation companies apply vacuum evaporation concentration systems to treat contaminated water and industrial wastewater. The versatility and effectiveness of modern vacuum evaporation concentration systems make them indispensable for businesses seeking sustainable, cost-effective concentration solutions.

New Products

The vacuum evaporation concentration system delivers substantial operational advantages that directly impact your bottom line and production efficiency. First, this technology dramatically reduces energy consumption compared to traditional evaporation methods. By operating under reduced pressure, the vacuum evaporation concentration system lowers liquid boiling points, requiring significantly less heat input while maintaining superior concentration rates. This translates to measurable cost savings on energy bills and reduced environmental impact across your operations. Second, the vacuum evaporation concentration system protects valuable products through gentle processing conditions. Heat-sensitive materials, including pharmaceuticals, natural extracts, and specialty chemicals, remain stable throughout the concentration process. Unlike conventional boiling methods that risk product degradation, this system preserves product integrity, quality, and market value. Your finished products maintain their desired characteristics, resulting in higher customer satisfaction and premium pricing opportunities. Third, the vacuum evaporation concentration system maximizes material recovery rates, converting waste streams into valuable concentrated products. This capability supports circular economy initiatives while reducing disposal costs. Industrial facilities process more material efficiently, increasing throughput without expanding floor space or adding equipment. Fourth, operational flexibility sets this system apart. The vacuum evaporation concentration system handles diverse liquid compositions, viscosities, and concentrations, adapting to your changing production needs without extensive modifications. Staff training becomes straightforward due to automated controls and intuitive interfaces. Finally, the vacuum evaporation concentration system proves particularly suitable for regulated industries where product traceability and consistency matter. Automated monitoring and precise parameter control generate detailed documentation supporting compliance requirements. This reduces regulatory risks and audit preparation time significantly.

Tips And Tricks

Benefits of Low Temperature Heat Pump Evaporator in Industry

24

Jul

Benefits of Low Temperature Heat Pump Evaporator in Industry

Industrial facilities worldwide face mounting pressure to reduce operating costs while maintaining production quality and environmental compliance. The low temperature heat pump evaporator has emerged as a transformative solution that addresses these...
View More
Vacuum Distillation System Maintenance Best Practices

24

Jul

Vacuum Distillation System Maintenance Best Practices

Proper vacuum distillation system maintenance is critical for industries relying on separation, purification, and concentration processes. A well-maintained vacuum distillation system ensures consistent product quality, minimizes operational downtime...
View More
How Industrial Water Treatment Saves Costs and Resources

24

Jul

How Industrial Water Treatment Saves Costs and Resources

Industrial water treatment represents one of the most significant opportunities for manufacturing facilities to reduce operational expenses while protecting environmental resources. Organizations across industries face mounting pressure to minimize w...
View More
Vacuum Distillation vs Traditional Distillation Methods

24

Jul

Vacuum Distillation vs Traditional Distillation Methods

Vacuum distillation and traditional distillation methods represent two distinct approaches to separating liquid mixtures through controlled evaporation and condensation. Understanding the differences between vacuum distillation and traditional distil...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

vacuum evaporation concentration system

Energy-Efficient Concentration Technology

Energy-Efficient Concentration Technology

The vacuum evaporation concentration system stands out through its exceptional energy efficiency, consuming substantially less power than conventional evaporation equipment. Operating under reduced atmospheric pressure, this system lowers the boiling point of target liquids dramatically, requiring minimal thermal input to achieve rapid evaporation. For organizations managing significant production volumes, this energy advantage compounds monthly, resulting in thousands of dollars in utility cost savings. The vacuum evaporation concentration system incorporates advanced heat recovery mechanisms that capture and reuse thermal energy from the condensation process, further optimizing resource utilization. Industries worldwide have witnessed their operational carbon footprints shrink considerably after implementing this technology. The vacuum evaporation concentration system demonstrates payback periods typically ranging from eighteen to thirty-six months, making it an attractive long-term investment. Companies operating in energy-conscious regions particularly value this technology for maintaining competitive advantage while meeting sustainability commitments.
Superior Product Quality Preservation

Superior Product Quality Preservation

The vacuum evaporation concentration system excels at maintaining product integrity throughout the concentration process, protecting heat-sensitive compounds from thermal degradation. Pharmaceutical manufacturers, natural product extractors, and specialty chemical producers rely on this capability to preserve active ingredients, nutritional content, and desired characteristics. Lower operating temperatures mean vitamins, enzymes, and delicate molecular structures remain intact and functional. The vacuum evaporation concentration system enables processing of premium products that command higher market values precisely because quality remains uncompromised. This feature distinguishes the vacuum evaporation concentration system from alternatives that risk product quality for speed. Food manufacturers leverage this advantage to create premium concentrated juices and extracts maintaining vibrant colors, authentic flavors, and nutritional profiles. Quality assurance teams consistently report improved product consistency and reduced batch rejection rates after transitioning to this technology. Enhanced product marketability directly translates to increased revenue and customer loyalty.
Versatile Application Across Industries

Versatile Application Across Industries

The vacuum evaporation concentration system demonstrates remarkable adaptability across diverse industrial sectors and applications. From pharmaceutical concentration to food processing, from chemical manufacturing to environmental remediation, this equipment handles virtually any liquid concentration challenge efficiently. The vacuum evaporation concentration system accommodates varying viscosities, compositions, and concentration targets through adjustable operational parameters. Industries benefit from deploying single equipment platforms addressing multiple concentration requirements without purchasing specialized machinery. Chemical plants utilize the vacuum evaporation concentration system for solvent recovery, waste minimization, and byproduct concentration. Dairy facilities employ it for milk and whey concentration. Mining operations apply this technology to recover valuable minerals from process solutions. The vacuum evaporation concentration system's engineering flexibility supports custom configurations matching specific production environments and regulatory requirements. This versatility eliminates expensive redundant equipment investments while streamlining maintenance procedures across your facility.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000