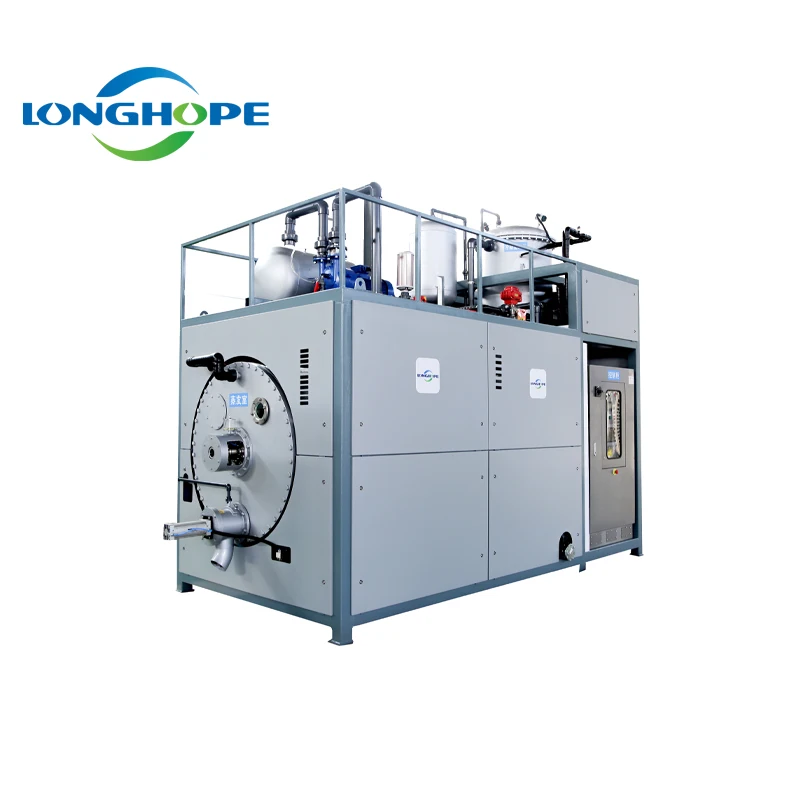
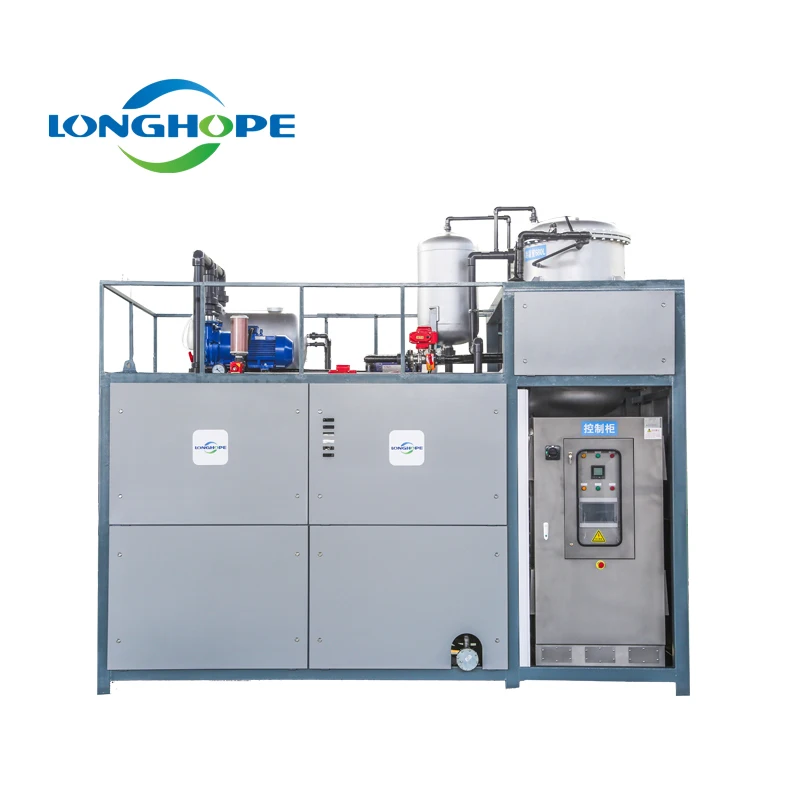
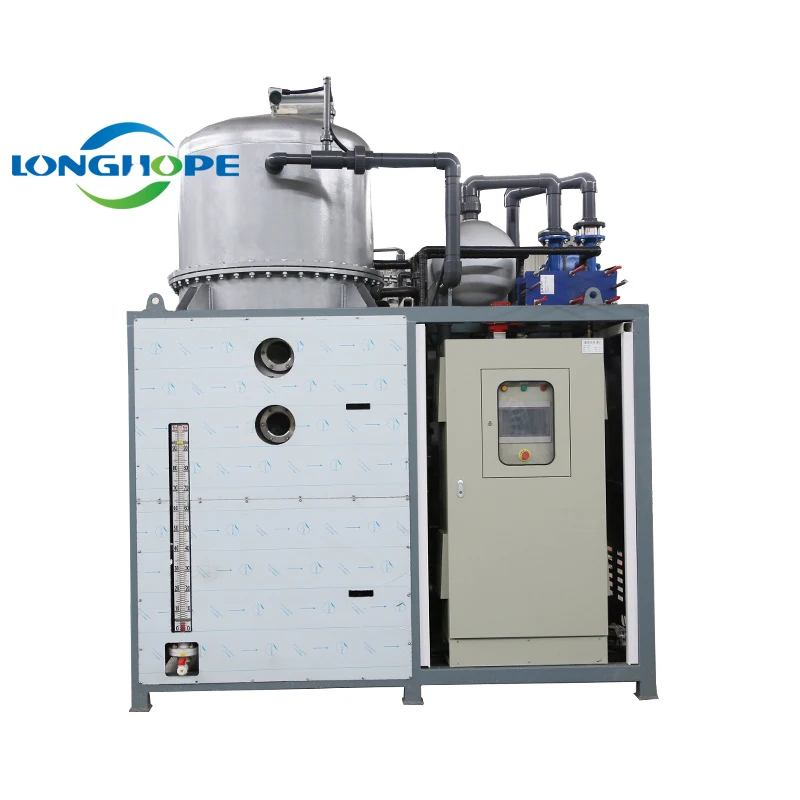
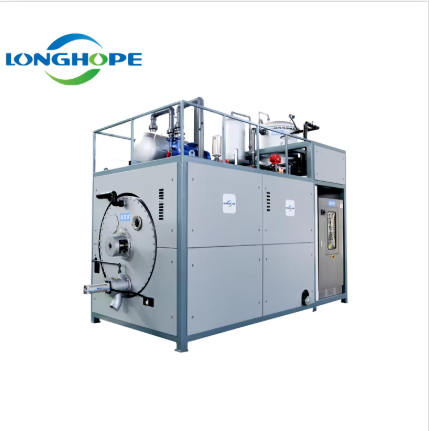
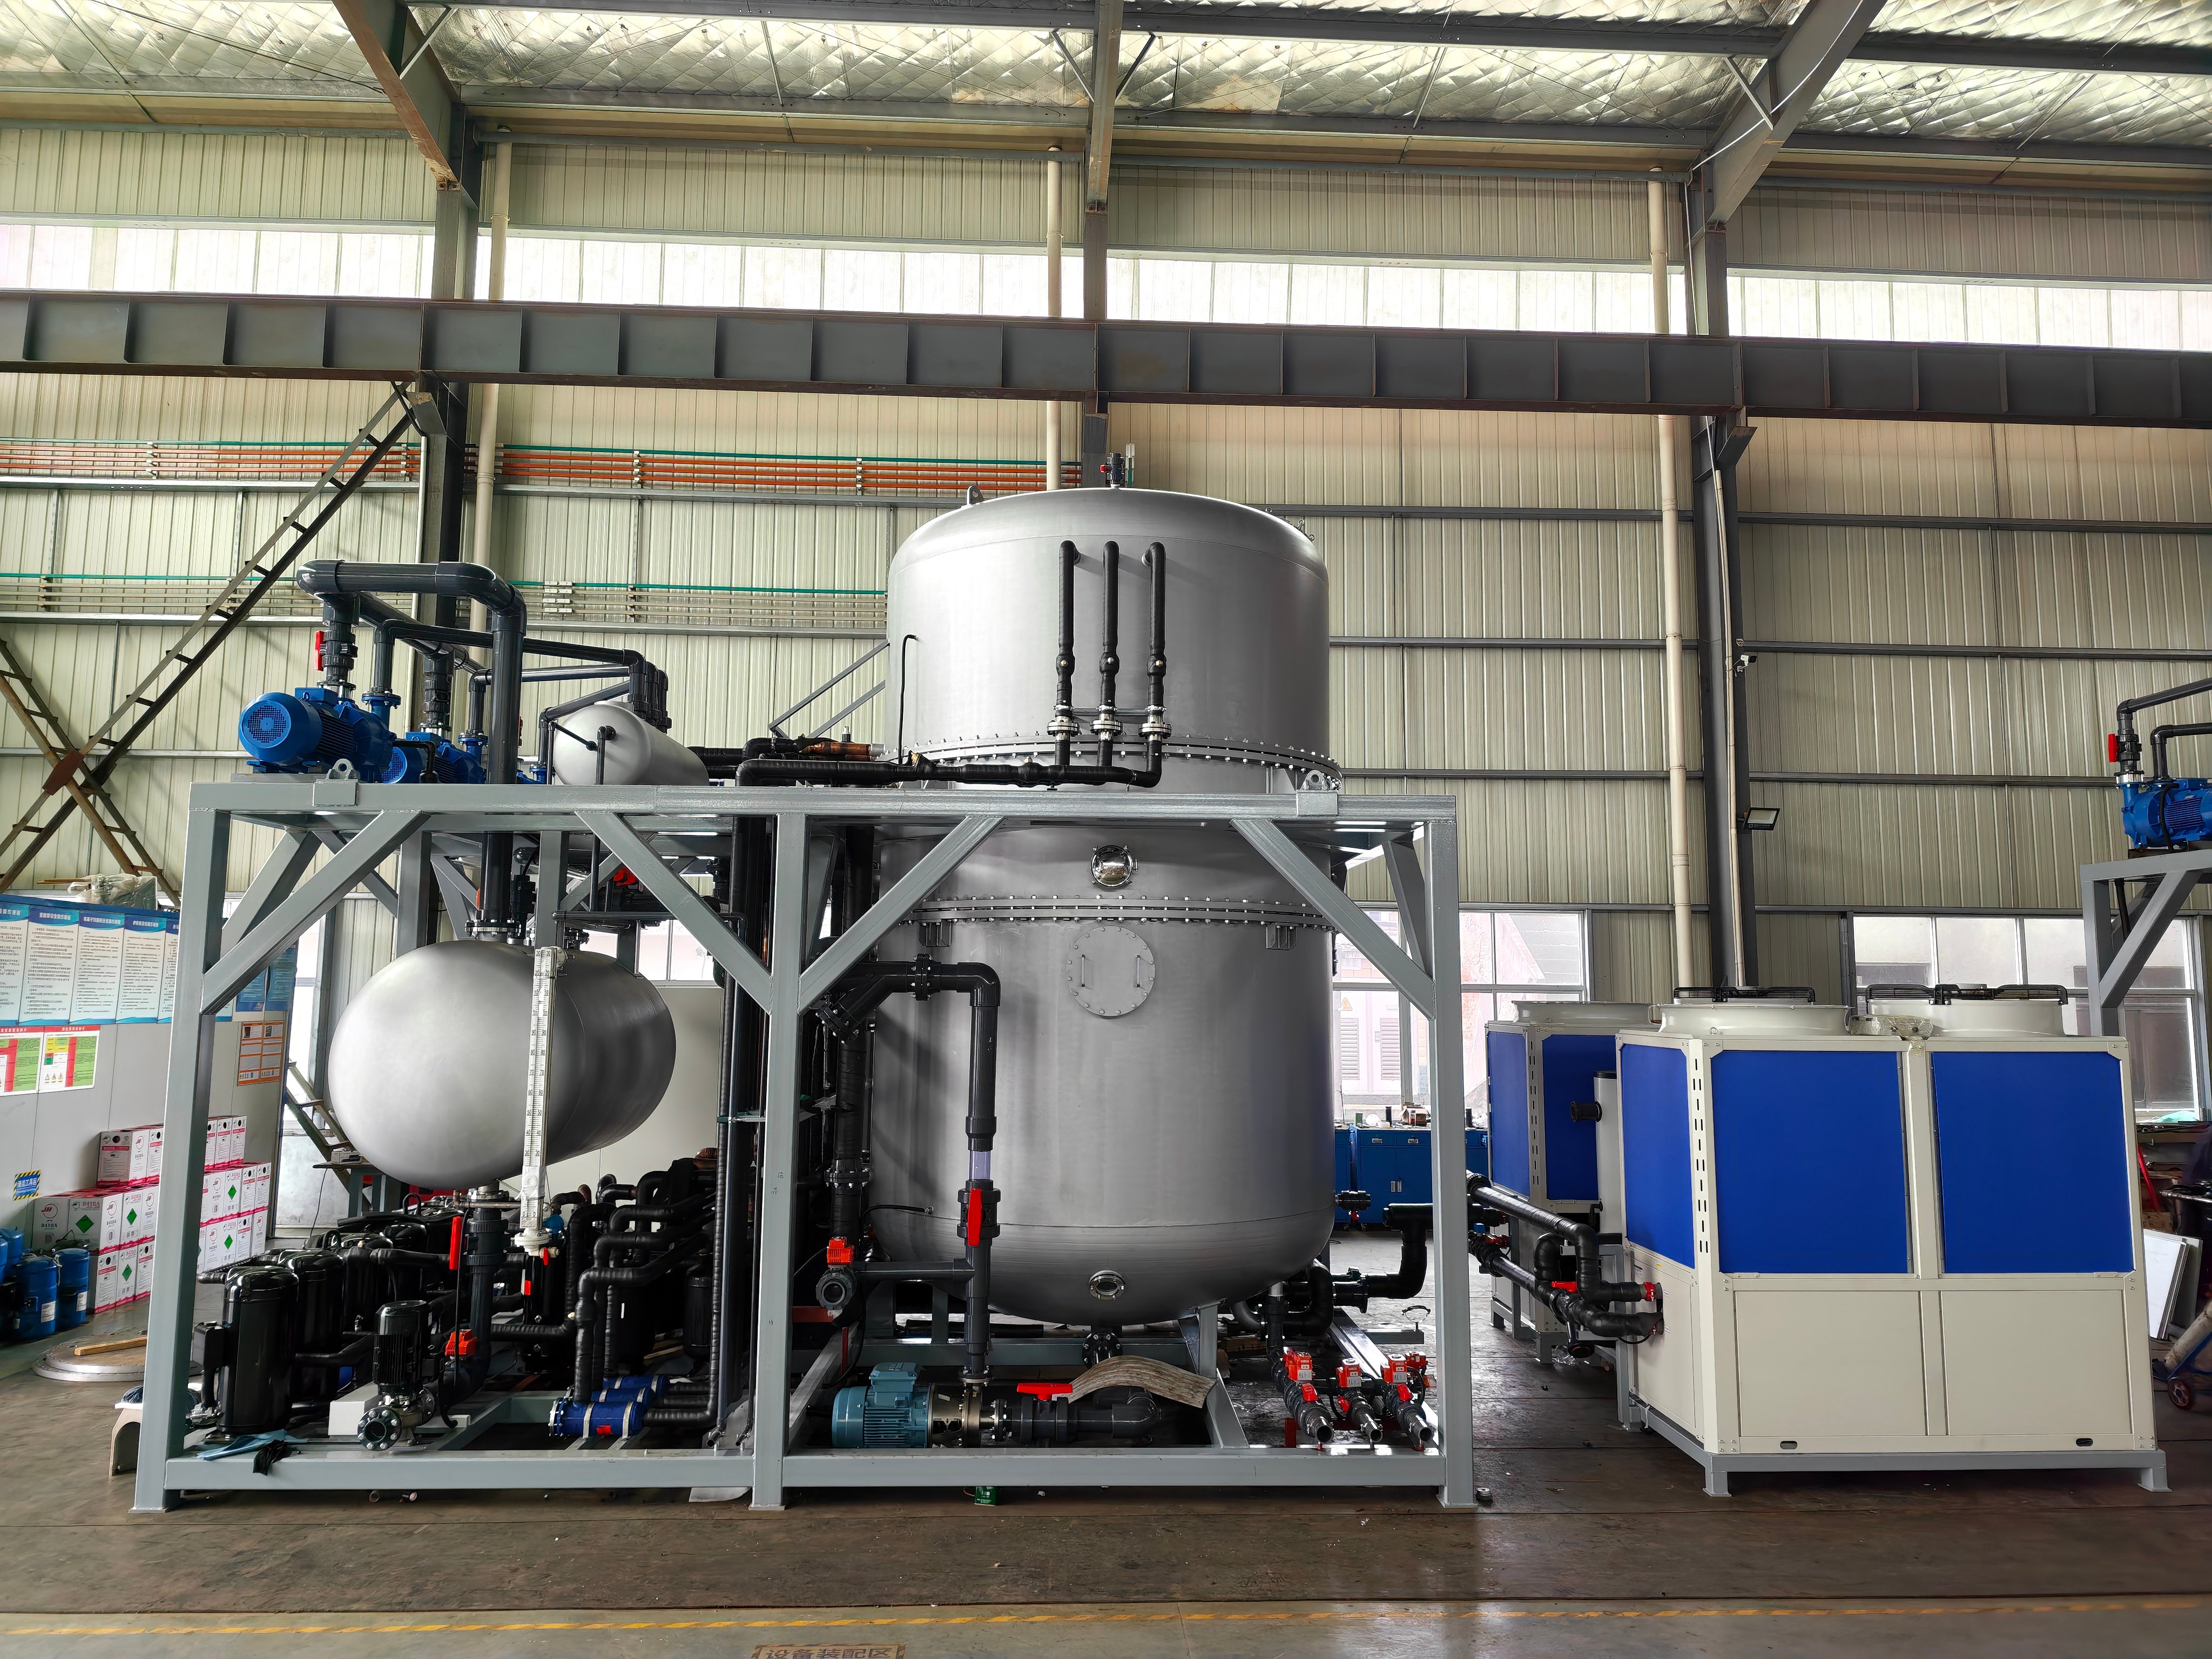
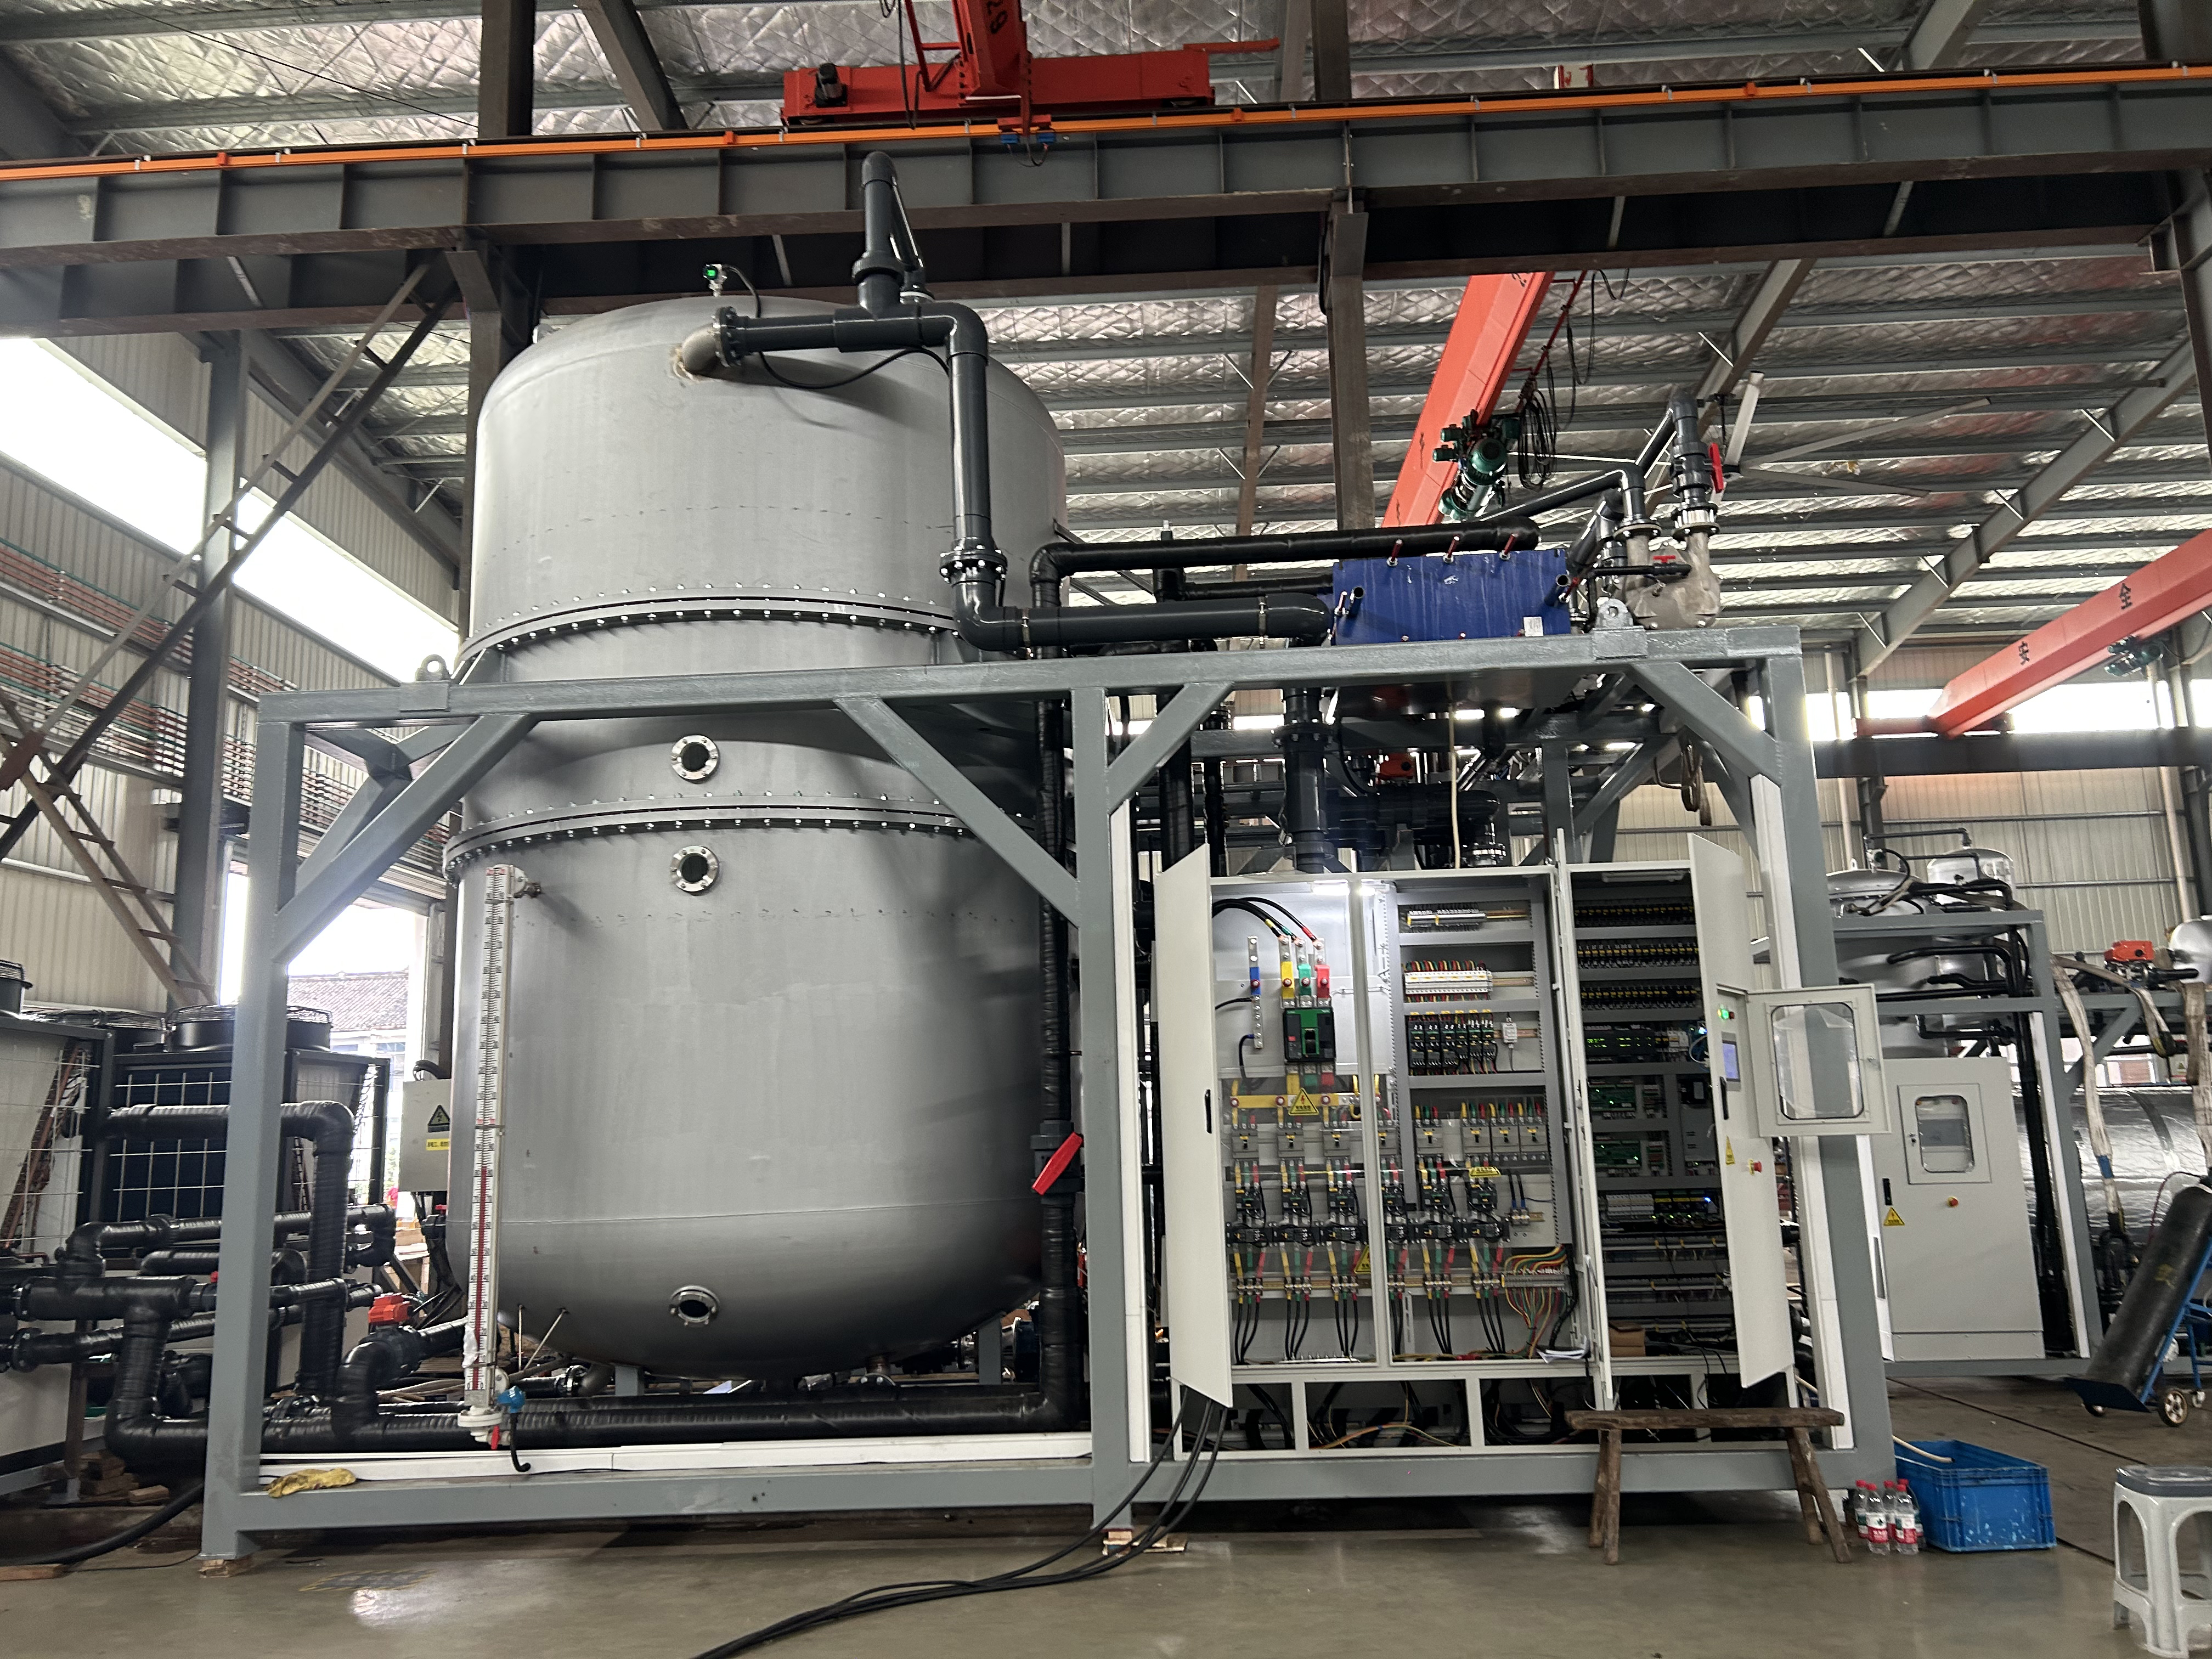
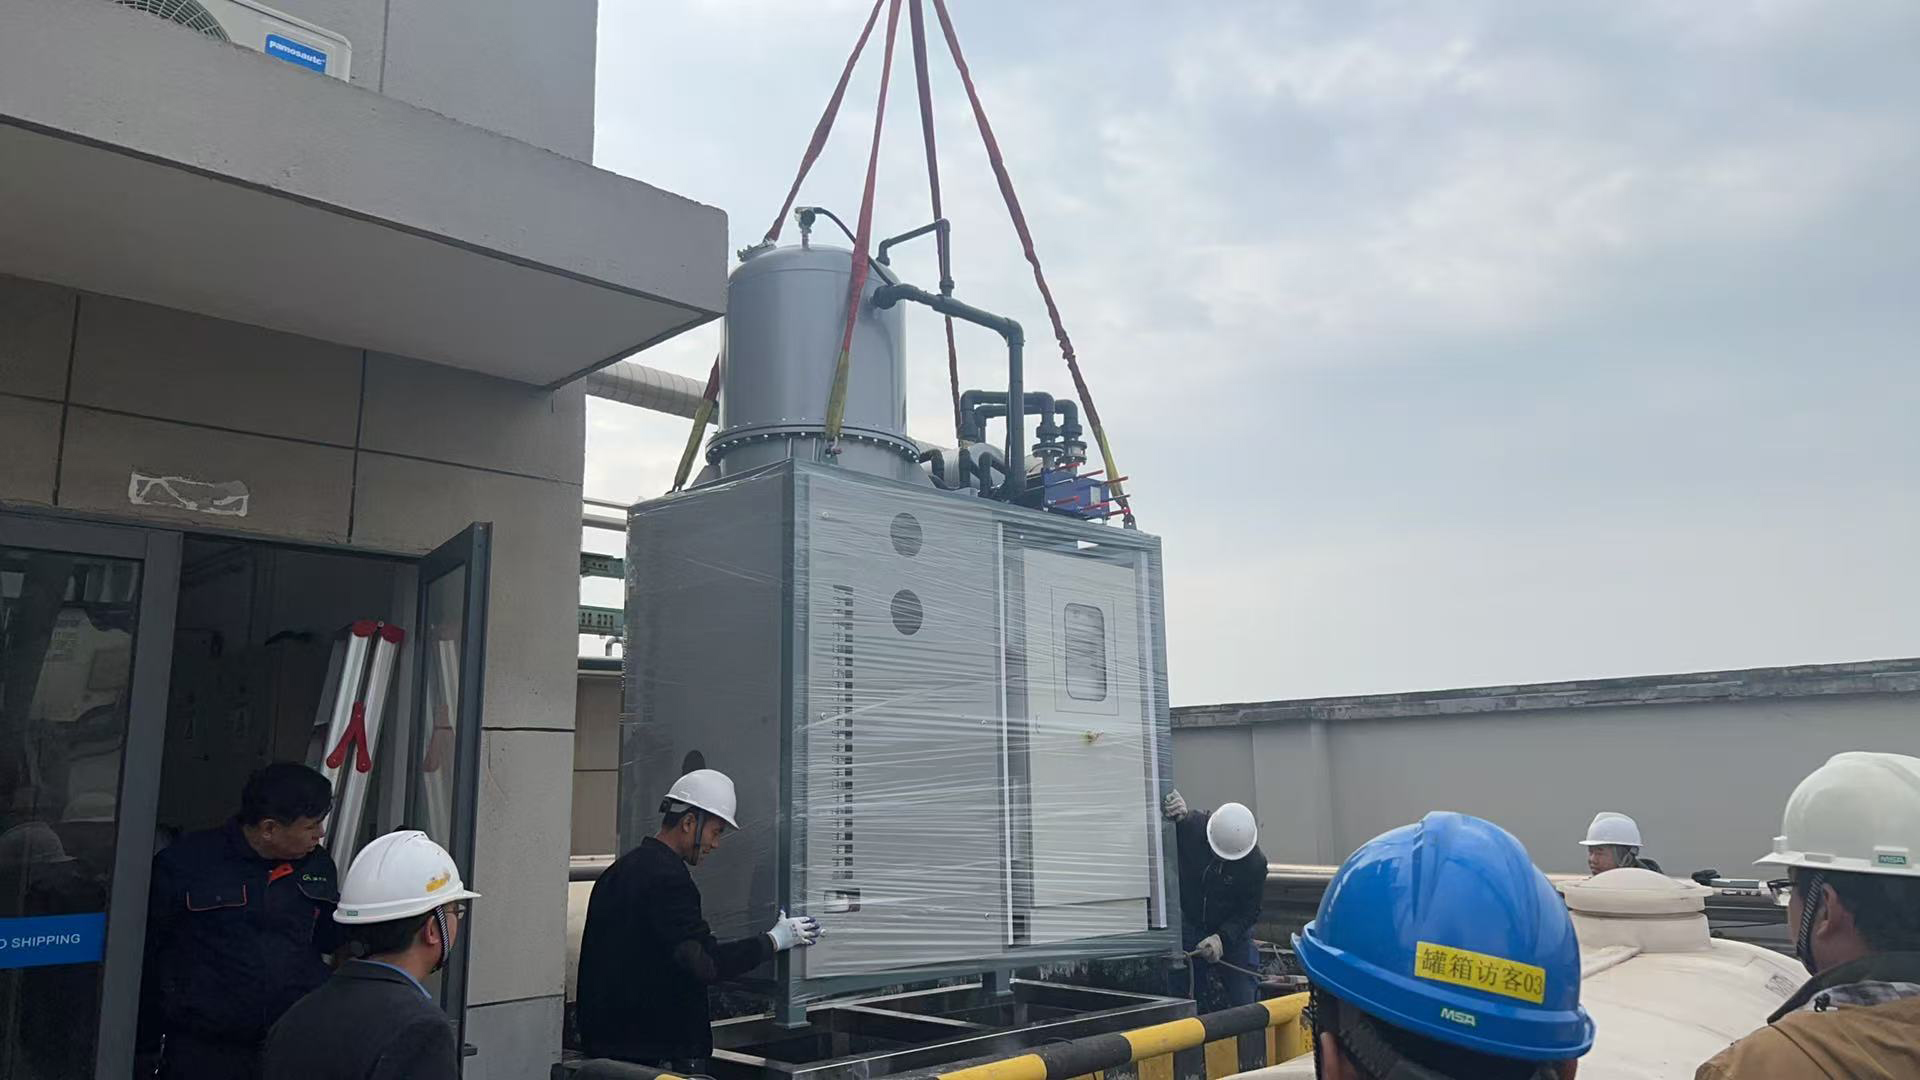
industrial vacuum evaporator concentrator
An industrial vacuum evaporator concentrator represents a sophisticated processing solution designed to efficiently reduce liquid volumes through controlled evaporation under reduced pressure conditions. This specialized equipment serves manufacturing facilities, chemical plants, pharmaceutical companies, and food processing operations seeking reliable concentration methods.
The industrial vacuum evaporator concentrator operates by lowering atmospheric pressure within an enclosed chamber, thereby reducing the boiling point of target liquids. This fundamental principle enables gentle yet effective evaporation, preserving heat-sensitive compounds and producing concentrated solutions with minimal thermal degradation.
Core technological features of an industrial vacuum evaporator concentrator include vacuum pump systems, heating elements, condensation units, and automated control mechanisms. Multiple evaporator designs—falling film, rising film, and scraped surface configurations—address diverse application requirements. The industrial vacuum evaporator concentrator integrates temperature regulation, pressure monitoring, and safety interlocks to ensure consistent, controlled operation.
Applications span numerous industries. The industrial vacuum evaporator concentrator concentrates fruit juices, dairy products, and pharmaceuticals. It recovers valuable solvents from manufacturing processes, reduces wastewater volumes for environmental compliance, and concentrates chemical solutions requiring precise specifications.
Key advantages include energy efficiency through reduced operating temperatures, product quality preservation, space optimization via compact designs, and waste reduction capabilities. The industrial vacuum evaporator concentrator delivers superior performance compared to conventional atmospheric evaporation methods, making it an essential investment for modern industrial operations seeking efficiency and quality outcomes.

 EN