Vacuum Concentration Plant Solutions

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

vacuum concentration plant

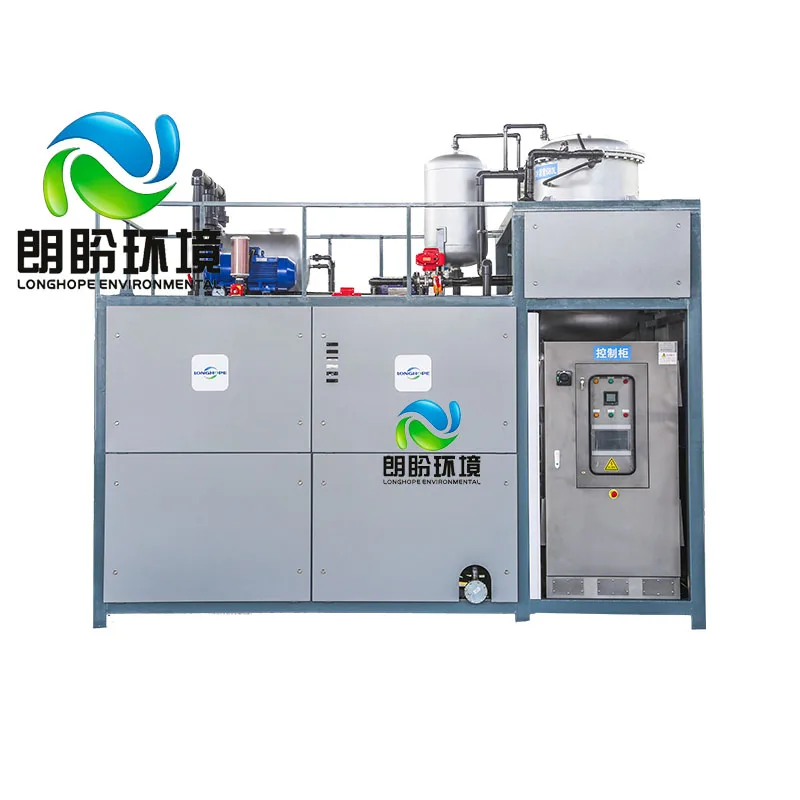
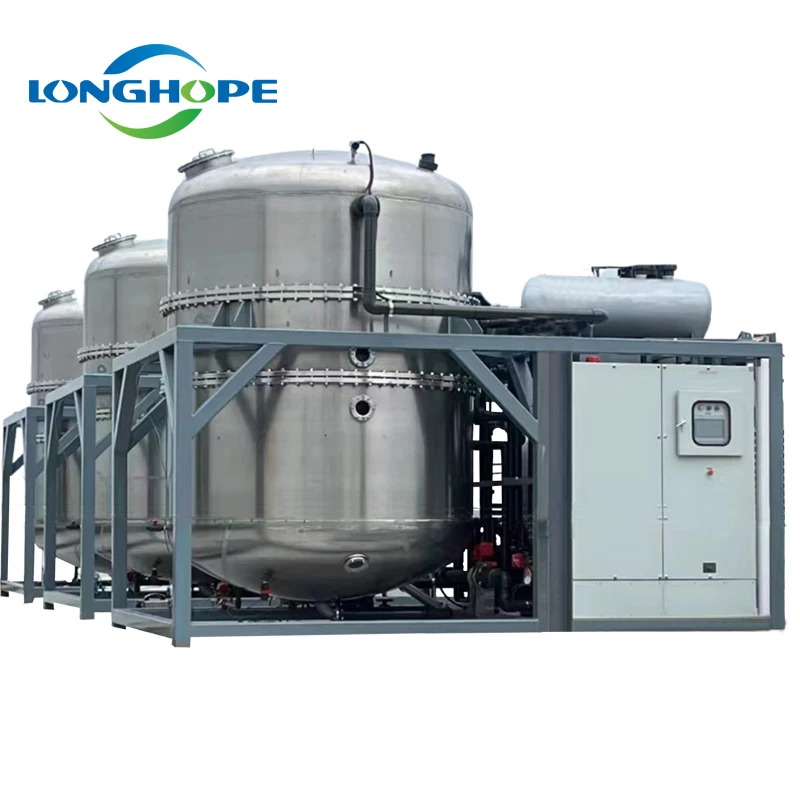
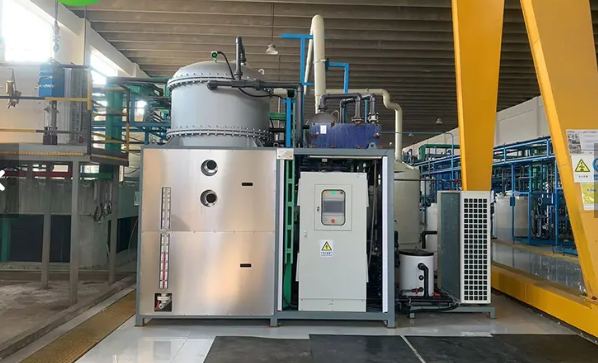
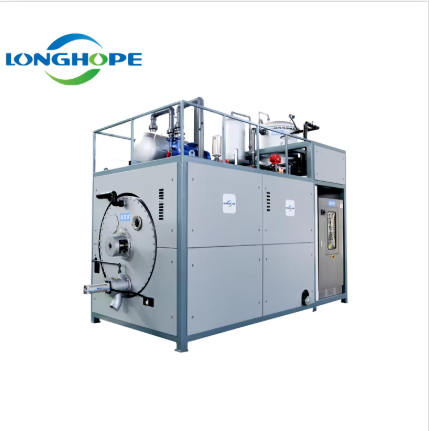
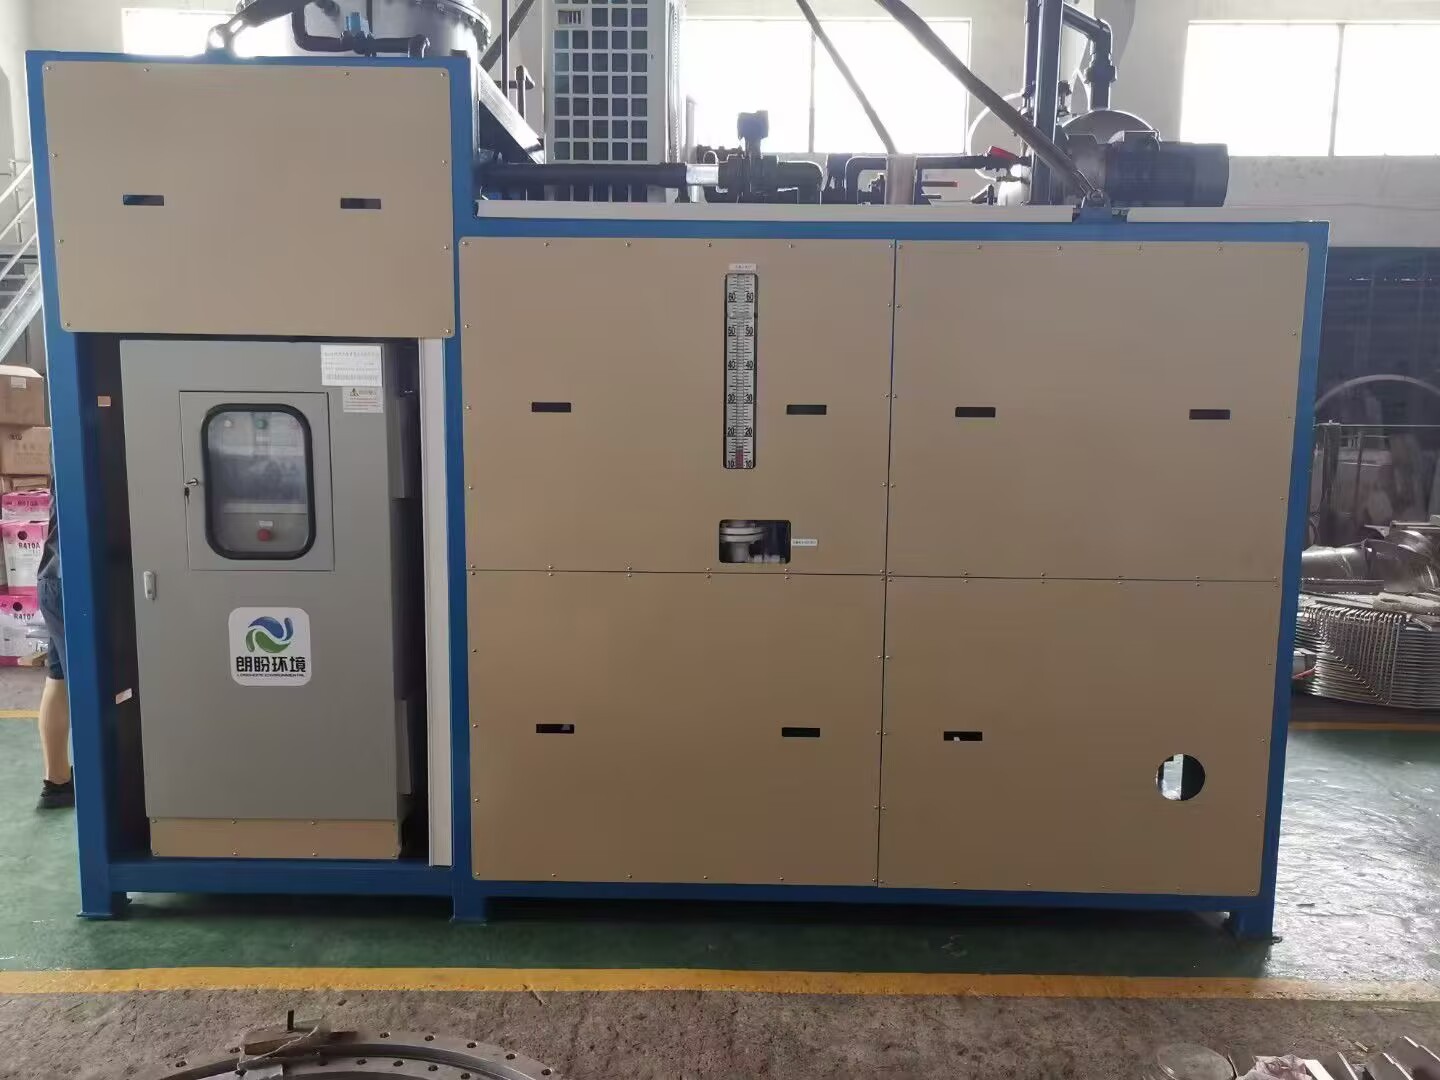
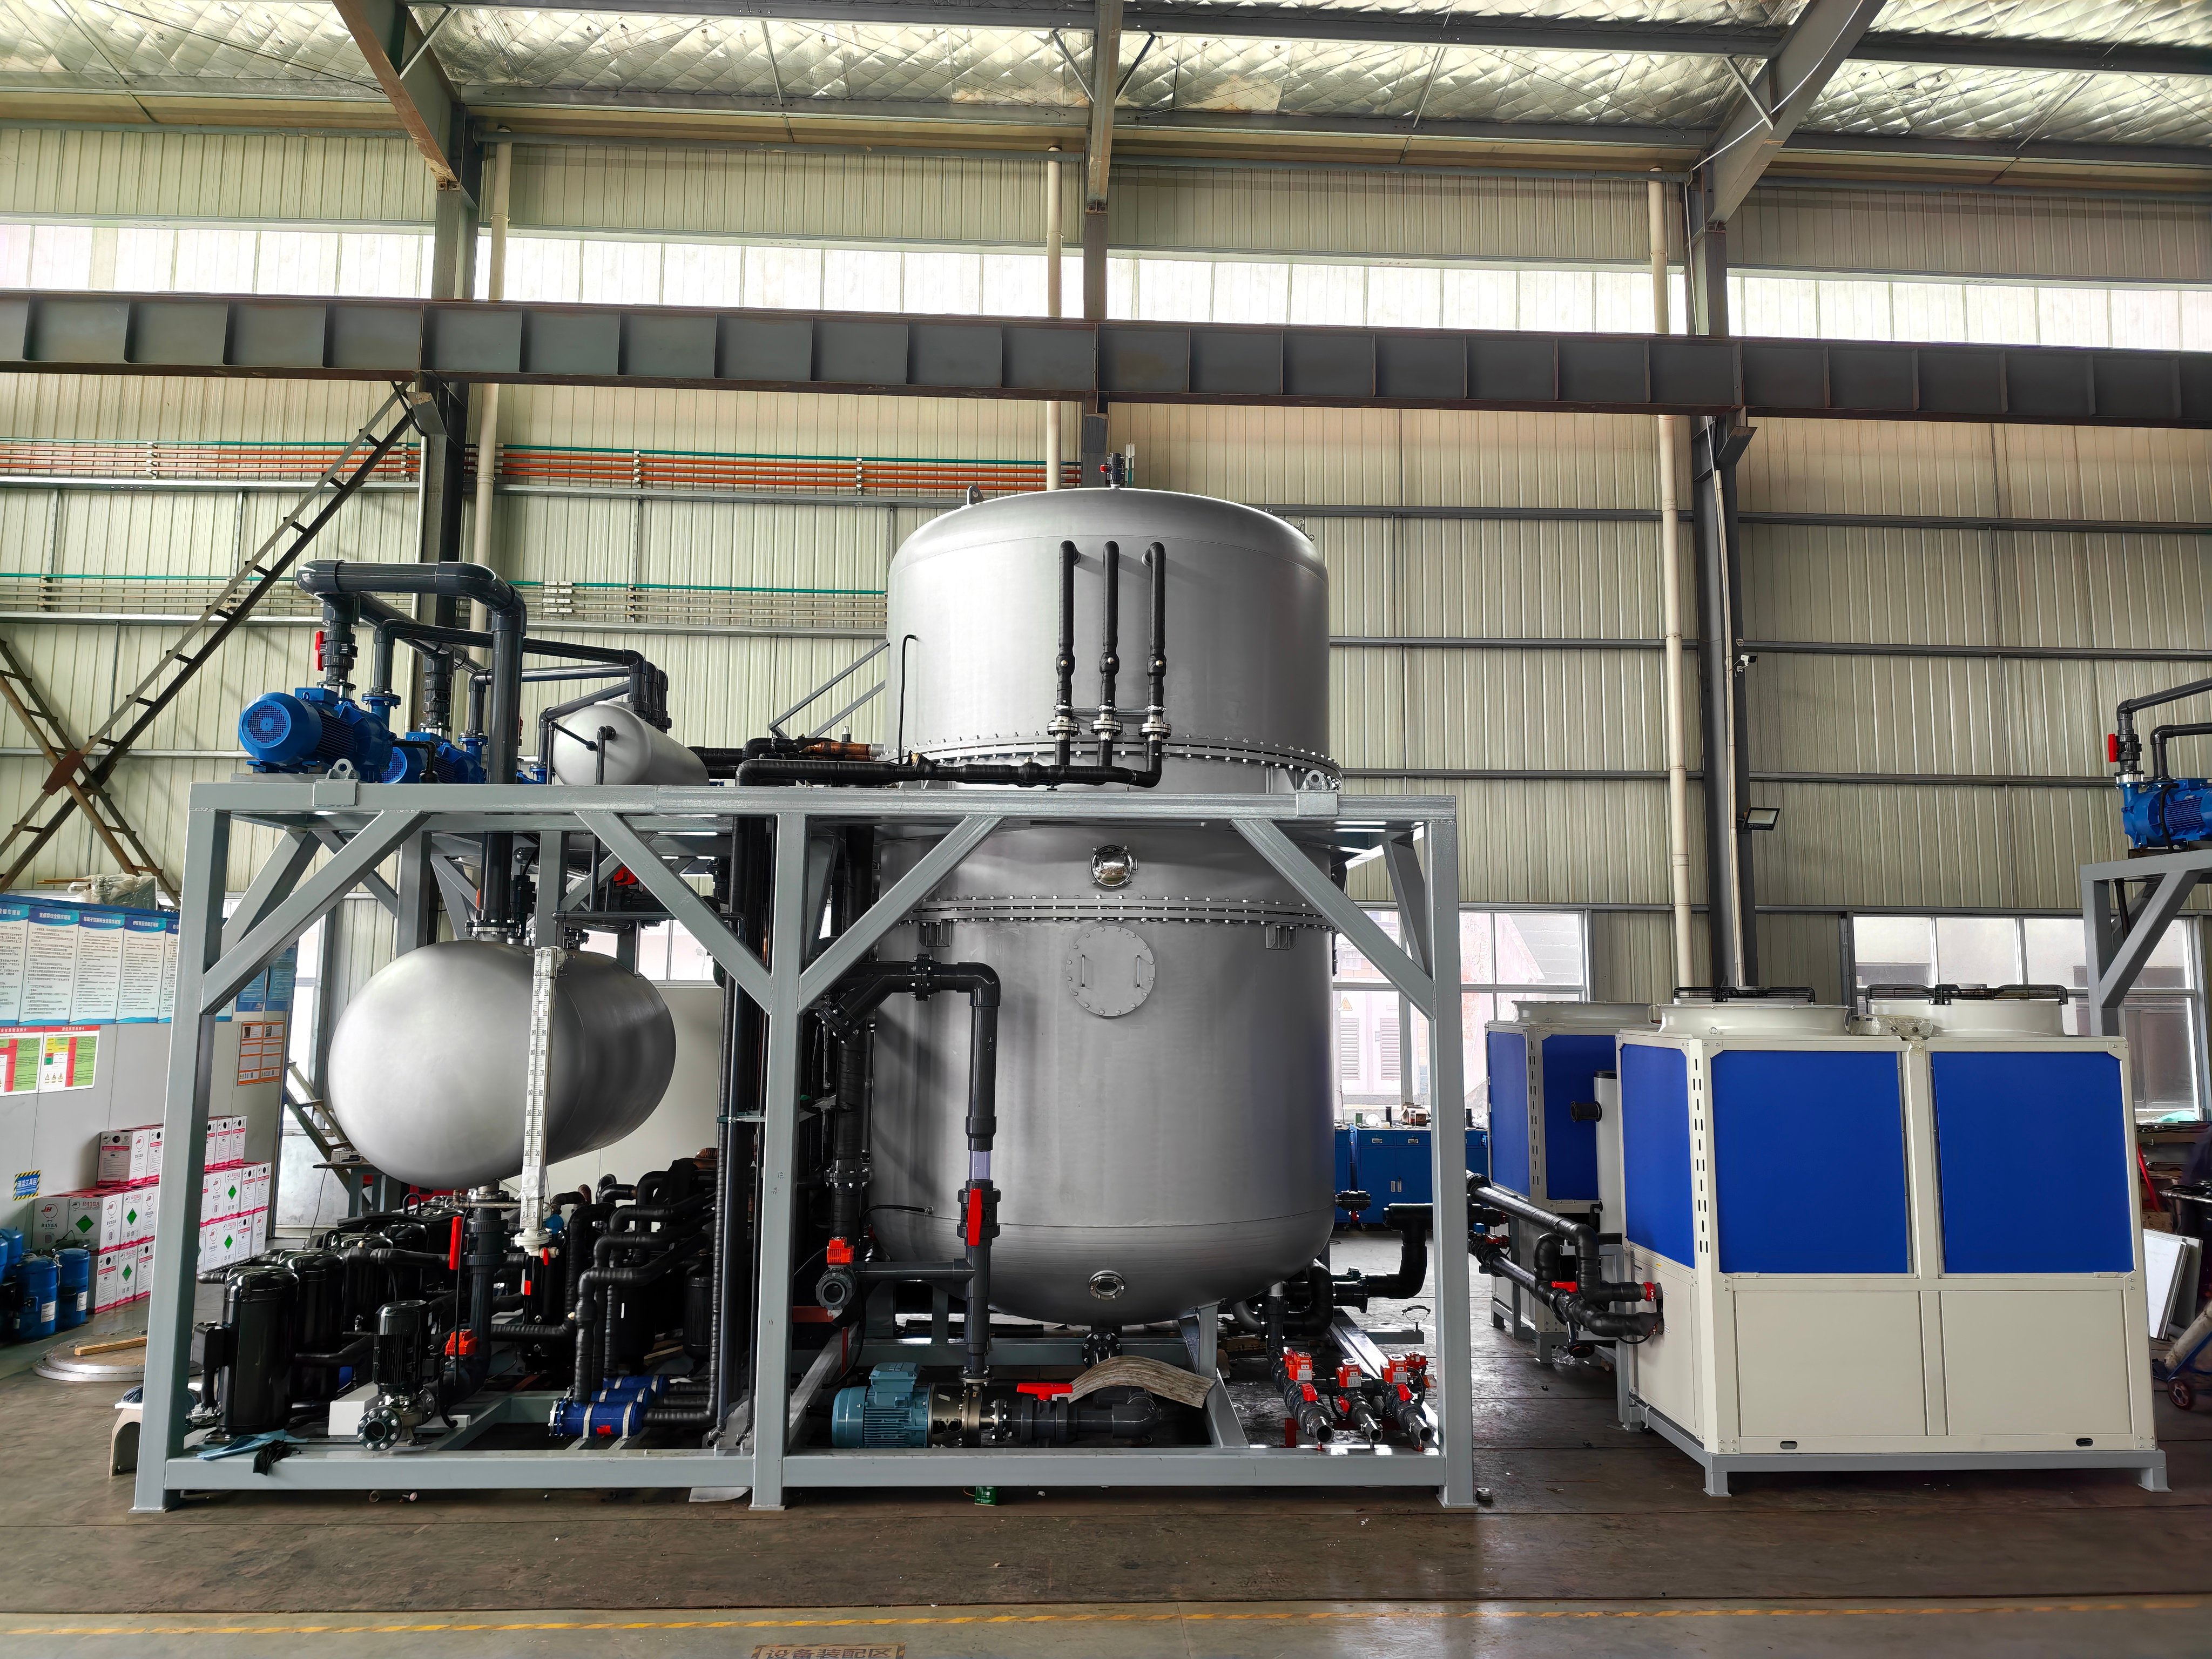
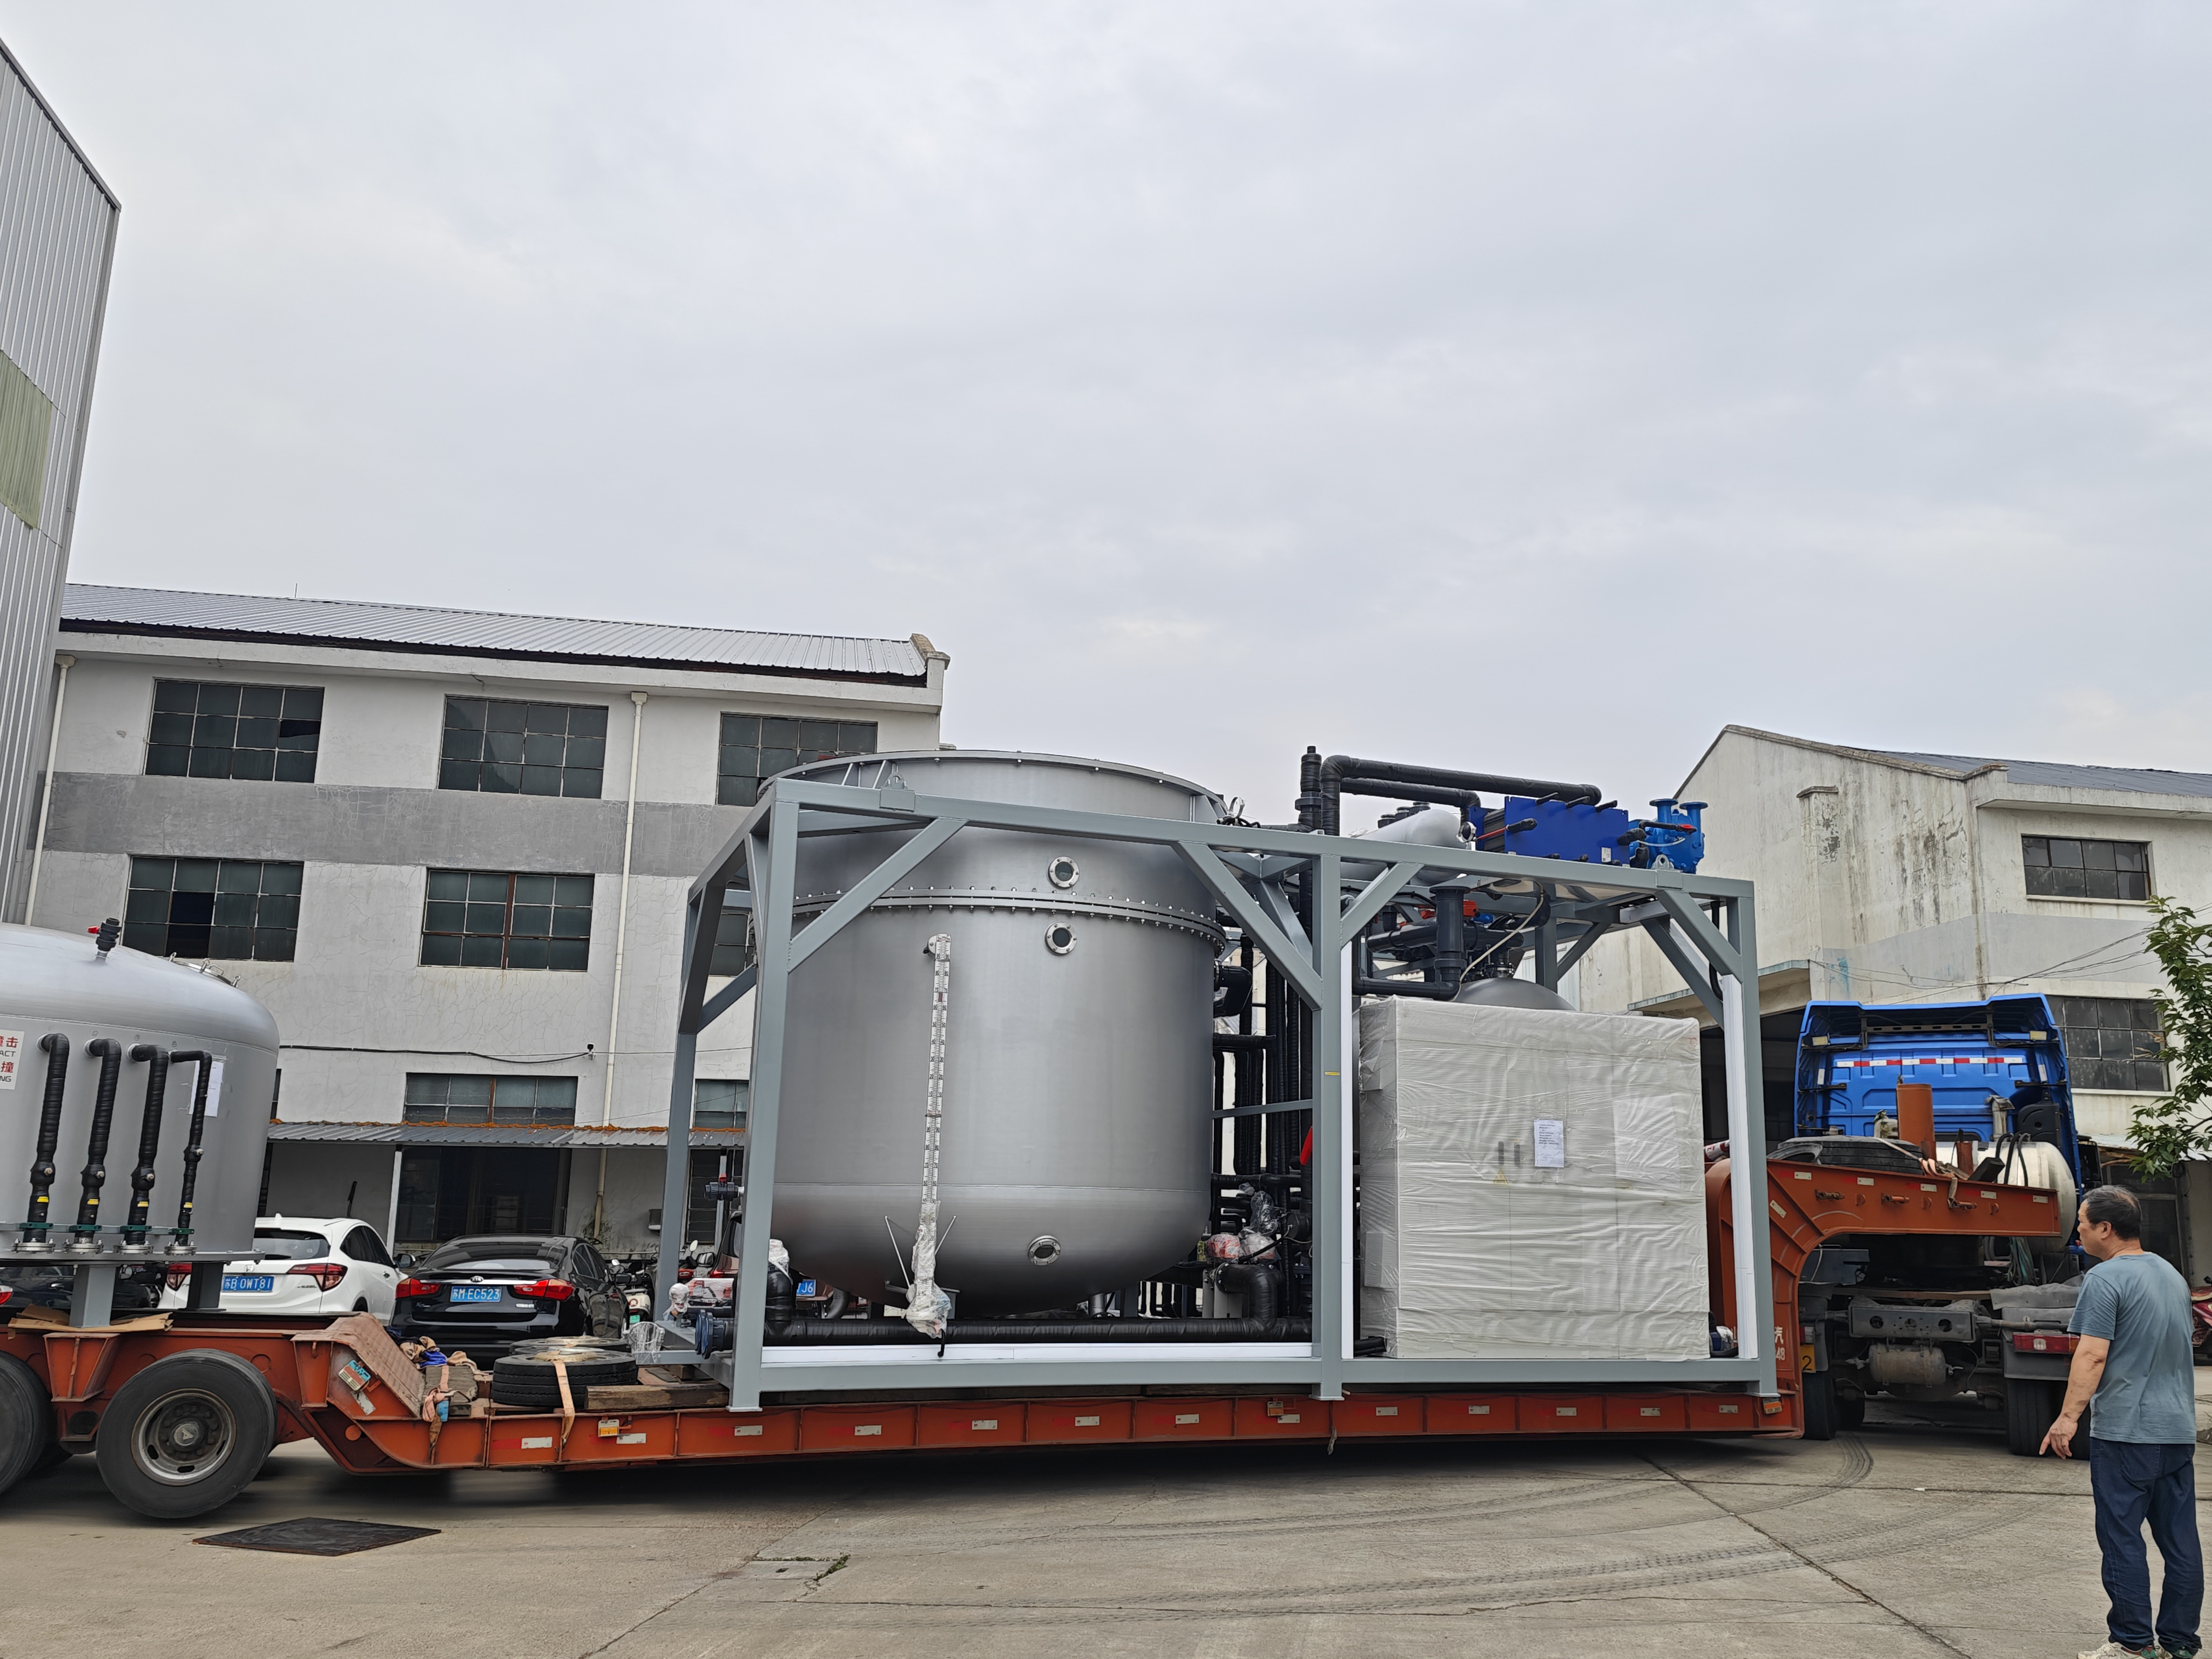
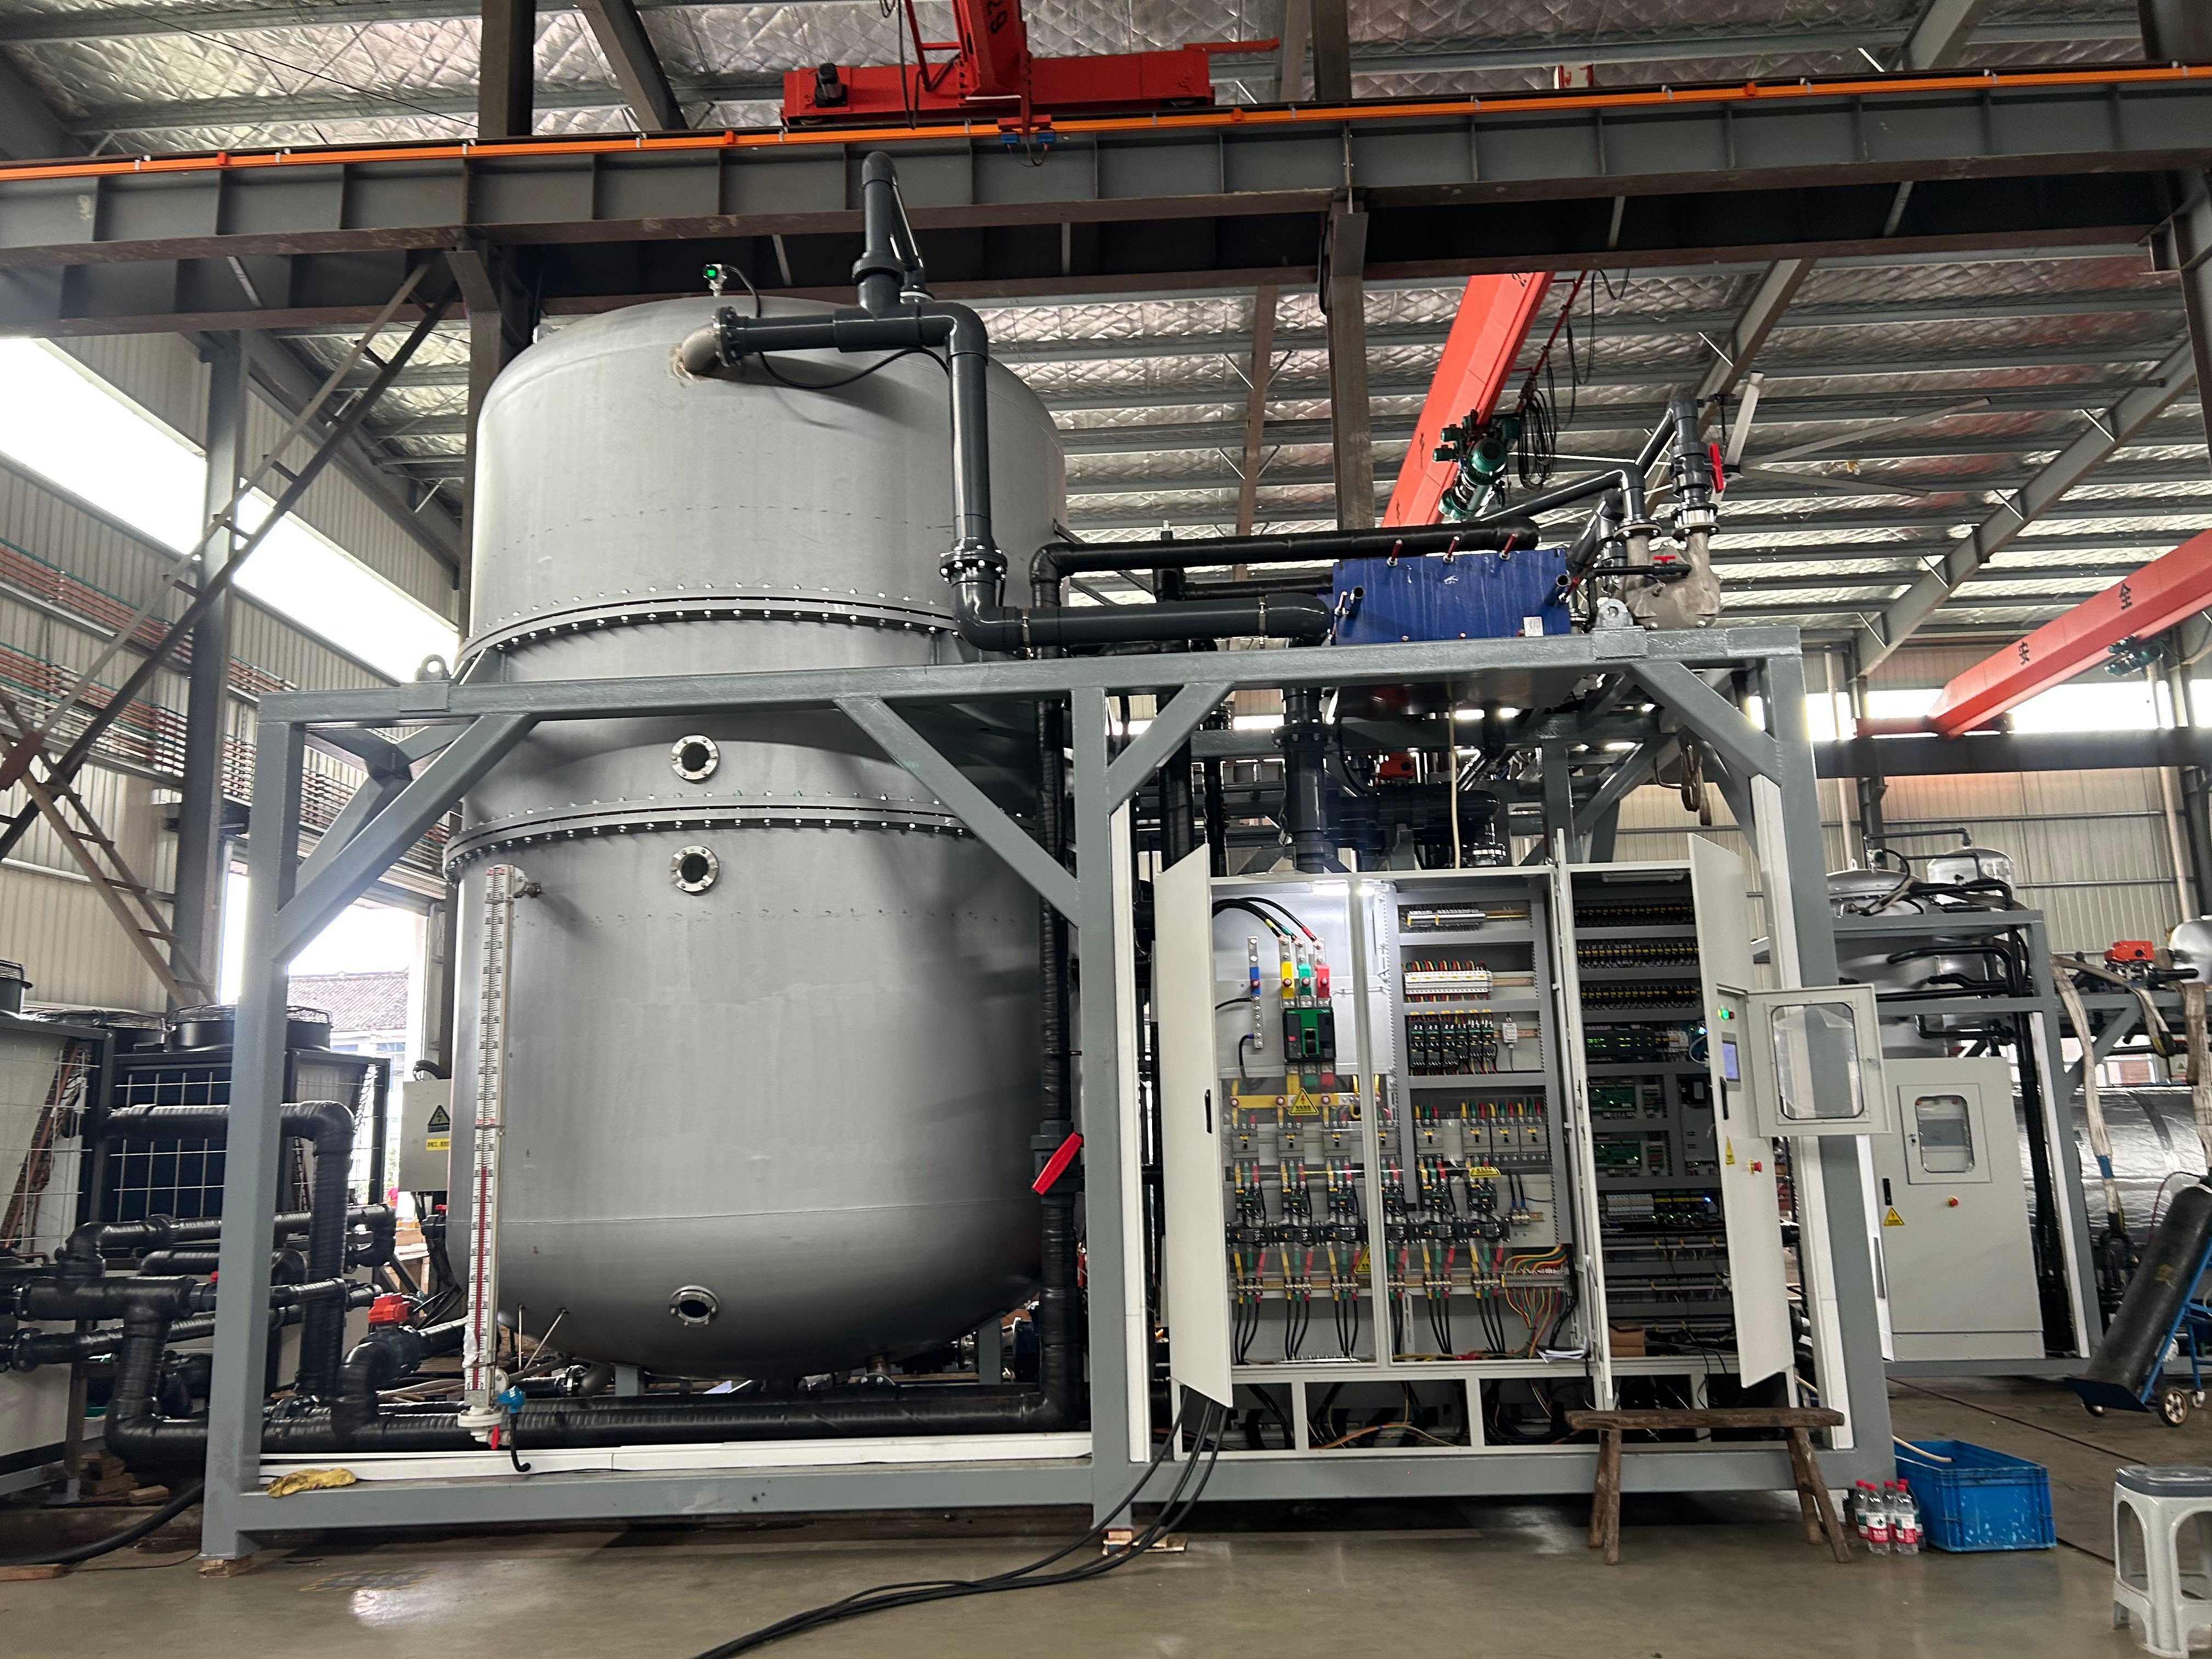
A vacuum concentration plant is an advanced industrial system designed to remove liquids from solutions through evaporation under reduced pressure conditions. This specialized vacuum concentration plant operates by lowering atmospheric pressure, which decreases the boiling point of liquids, enabling efficient evaporation at lower temperatures. The technology behind a vacuum concentration plant makes it ideal for processing heat-sensitive materials that would degrade at standard atmospheric conditions. The vacuum concentration plant functions by drawing vapor away from the liquid surface, creating a pressure differential that accelerates the concentration process. Modern vacuum concentration plant equipment incorporates multiple stages of heating, evaporation, and condensation to maximize efficiency and product quality. The system typically includes vacuum pumps, heat exchangers, separators, and collection vessels that work together seamlessly. A vacuum concentration plant serves numerous industries requiring liquid concentration without thermal damage. Pharmaceutical manufacturers rely on vacuum concentration plant technology to preserve active ingredients while reducing liquid volume. The food and beverage sector utilizes vacuum concentration plant systems for juice concentration, flavoring extraction, and syrup production. Chemical processing facilities employ vacuum concentration plant equipment for solvent recovery and chemical concentration. Environmental applications include wastewater treatment and industrial liquid recycling. The vacuum concentration plant delivers consistent results by maintaining precise temperature and pressure parameters throughout operation. Advanced automation in modern vacuum concentration plant systems ensures reproducible outcomes and minimal product loss. Energy efficiency represents a key advantage of vacuum concentration plant technology, as lower operating temperatures reduce overall energy consumption compared to conventional evaporation methods.

New Product Releases

The vacuum concentration plant offers transformative benefits for businesses seeking to improve production efficiency and product quality. One primary advantage of the vacuum concentration plant is its ability to process temperature-sensitive materials without causing degradation or quality loss. This capability proves invaluable for pharmaceutical, food, and cosmetic manufacturers who must preserve delicate compounds while reducing liquid volume. Operational efficiency represents another critical benefit of the vacuum concentration plant. By operating under reduced pressure, the vacuum concentration plant achieves faster evaporation rates compared to atmospheric evaporation methods, reducing processing time and increasing throughput. This accelerated performance translates directly to improved production capacity and faster turnaround times for your operations. Cost savings emerge as a significant advantage when implementing a vacuum concentration plant. The reduced operating temperature means lower energy consumption throughout the concentration cycle. The vacuum concentration plant's efficient design minimizes product waste and maximizes material recovery, directly improving your bottom line. Additionally, the vacuum concentration plant requires less frequent maintenance due to reduced thermal stress on equipment components. Flexibility represents a key operational benefit of the vacuum concentration plant system. The technology adapts to various liquid types and concentration requirements, making the vacuum concentration plant suitable for diverse applications across multiple industries. Whether processing pharmaceutical solutions, food products, or industrial chemicals, the vacuum concentration plant delivers reliable results. Environmental responsibility strengthens when choosing the vacuum concentration plant for your facility. Lower energy consumption reduces your carbon footprint, while improved material recovery minimizes waste disposal requirements. The vacuum concentration plant supports sustainable manufacturing practices while delivering superior performance and profitability for your organization.

Tips And Tricks

Top 5 Low Temperature Heat Pump Evaporator Applications

24

Jul

Top 5 Low Temperature Heat Pump Evaporator Applications

The low temperature heat pump evaporator represents a critical advancement in industrial thermal management and energy efficiency. This innovative component enables heat pump systems to operate effectively at reduced temperatures, making it indispens...
View More
How Industrial Water Treatment Saves Costs and Resources

24

Jul

How Industrial Water Treatment Saves Costs and Resources

Industrial water treatment represents one of the most significant opportunities for manufacturing facilities to reduce operational expenses while protecting environmental resources. Organizations across industries face mounting pressure to minimize w...
View More
Industrial Water Treatment Technologies for 2026

02

Sep

Industrial Water Treatment Technologies for 2026

Industrial water treatment remains one of the most critical operational priorities across manufacturing, chemical processing, food production, and energy sectors. As facilities face increasingly stringent environmental regulations, rising operational...
View More
Evaporator System Maintenance: Tips for Longevity

24

Jul

Evaporator System Maintenance: Tips for Longevity

Evaporator system maintenance is critical to ensuring your industrial cooling and waste-water treatment equipment operates reliably and efficiently over the long term. Whether your facility relies on evaporator systems for refrigeration, heat exchang...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

vacuum concentration plant

Advanced Temperature Control Technology

Advanced Temperature Control Technology

The vacuum concentration plant incorporates sophisticated temperature management systems that protect product integrity during the concentration process. Unlike conventional evaporation methods, the vacuum concentration plant operates at significantly lower temperatures by utilizing reduced pressure conditions, preventing thermal damage to sensitive compounds. This advanced feature of the vacuum concentration plant proves essential for pharmaceutical manufacturers processing active pharmaceutical ingredients, food processors concentrating heat-sensitive juices and extracts, and chemical companies handling delicate solvents. The precision temperature control within the vacuum concentration plant ensures consistent product quality across all production batches. By maintaining optimal temperature ranges, the vacuum concentration plant protects nutrient content, preserves flavor profiles, and maintains chemical stability. This capability transforms the vacuum concentration plant into an indispensable tool for industries where product quality directly impacts market competitiveness and customer satisfaction.
Energy-Efficient Operations and Cost Reduction

Energy-Efficient Operations and Cost Reduction

Operating a vacuum concentration plant delivers substantial energy savings compared to traditional evaporation systems. The reduced boiling point created by the vacuum concentration plant's pressure reduction means lower heat input requirements throughout the entire process. This energy efficiency of the vacuum concentration plant translates into measurable cost reductions across your operational budget. Industrial facilities implementing the vacuum concentration plant report energy consumption reductions of 30-50% compared to conventional methods. The vacuum concentration plant's design minimizes heat losses through advanced insulation and efficient heat exchanger technology. Beyond energy savings, the vacuum concentration plant reduces water usage for cooling systems, addressing sustainability concerns while lowering operational expenses. The long-term financial benefits of the vacuum concentration plant extend across years of operation, making it a smart investment for facilities prioritizing both profitability and environmental responsibility.
Versatile Applications Across Multiple Industries

Versatile Applications Across Multiple Industries

The vacuum concentration plant demonstrates remarkable versatility, serving diverse industries with varying concentration requirements and product characteristics. Pharmaceutical manufacturers trust the vacuum concentration plant for concentrating active ingredients, herbal extracts, and vitamin solutions while maintaining therapeutic potency. Food processors utilize the vacuum concentration plant for apple juice concentration, honey processing, and flavoring production, preserving natural taste and nutritional value. Chemical industries employ the vacuum concentration plant for solvent recovery, chemical concentration, and specialized liquid processing. Environmental remediation facilities use the vacuum concentration plant for wastewater treatment and industrial liquid recycling applications. The adaptive nature of the vacuum concentration plant allows operators to adjust pressure and temperature parameters to match specific product requirements. This flexibility means the vacuum concentration plant can serve multiple product lines within a single facility. Whether your industry requires gentle processing of delicate compounds or efficient concentration of robust industrial liquids, the vacuum concentration plant provides reliable, adaptable solutions for your unique operational needs.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000