Vacuum Concentration Unit Guide

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

vacuum concentration unit

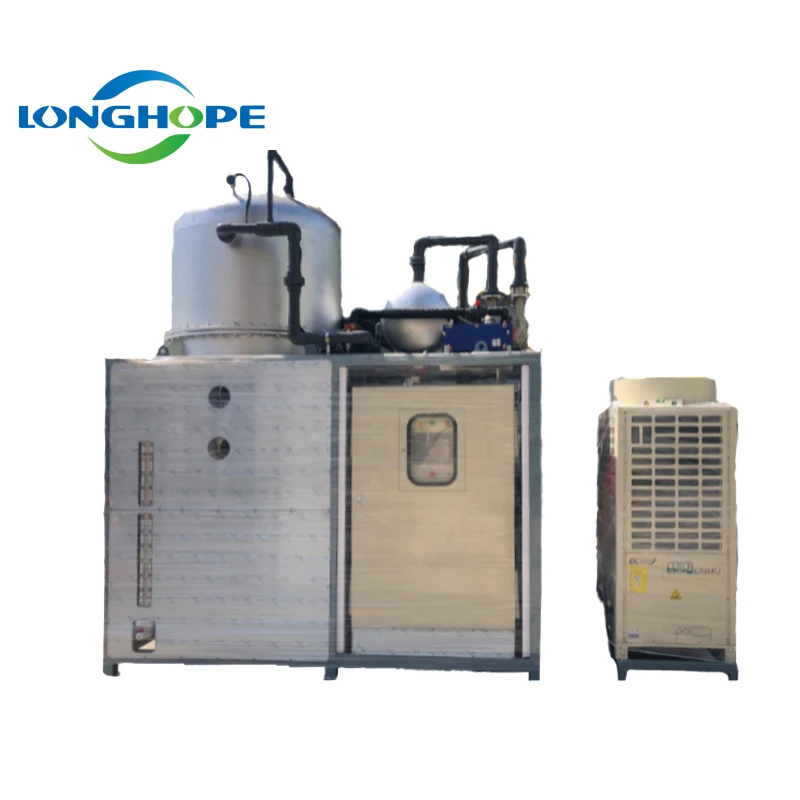
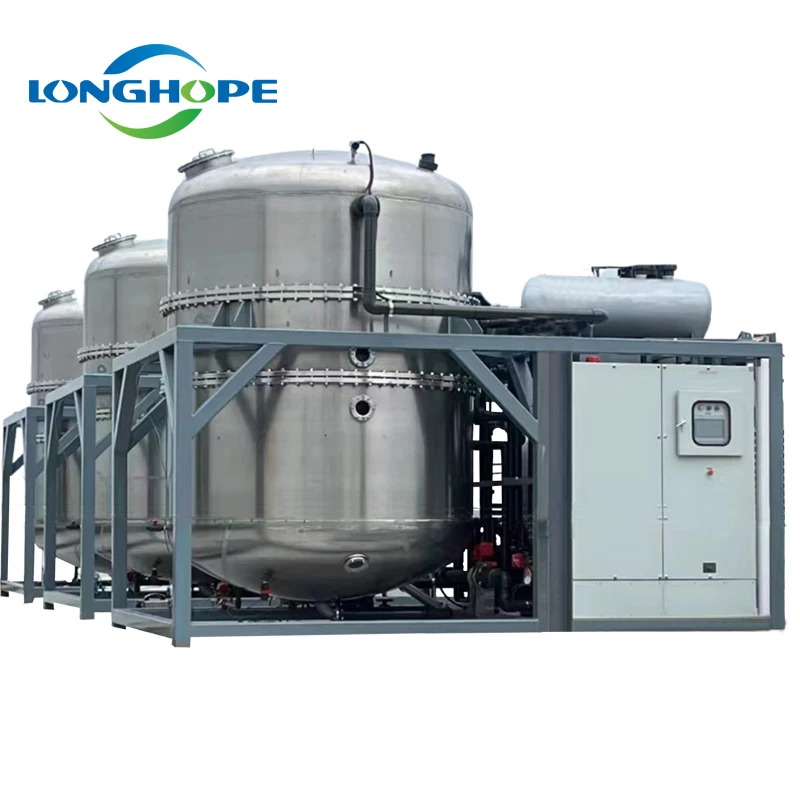
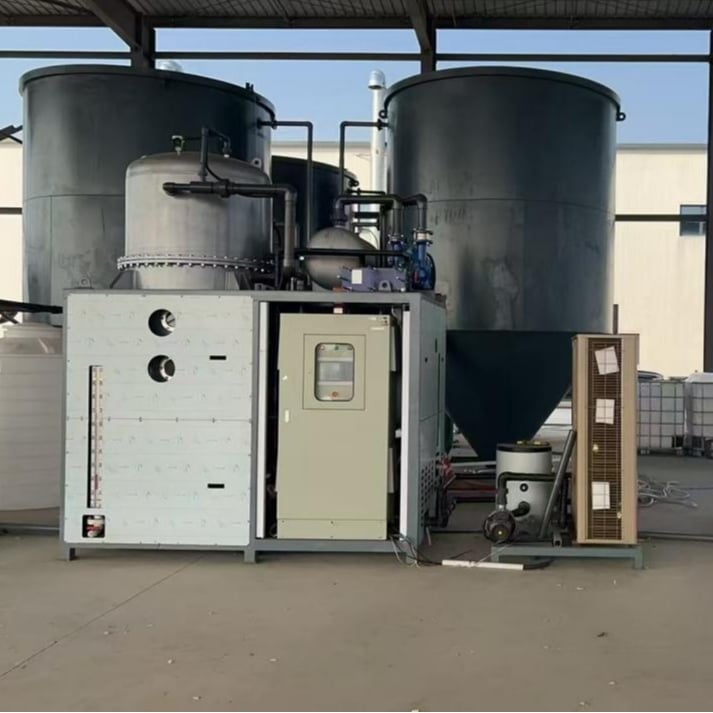
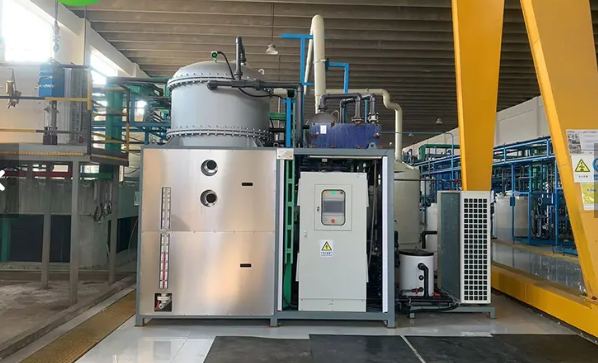
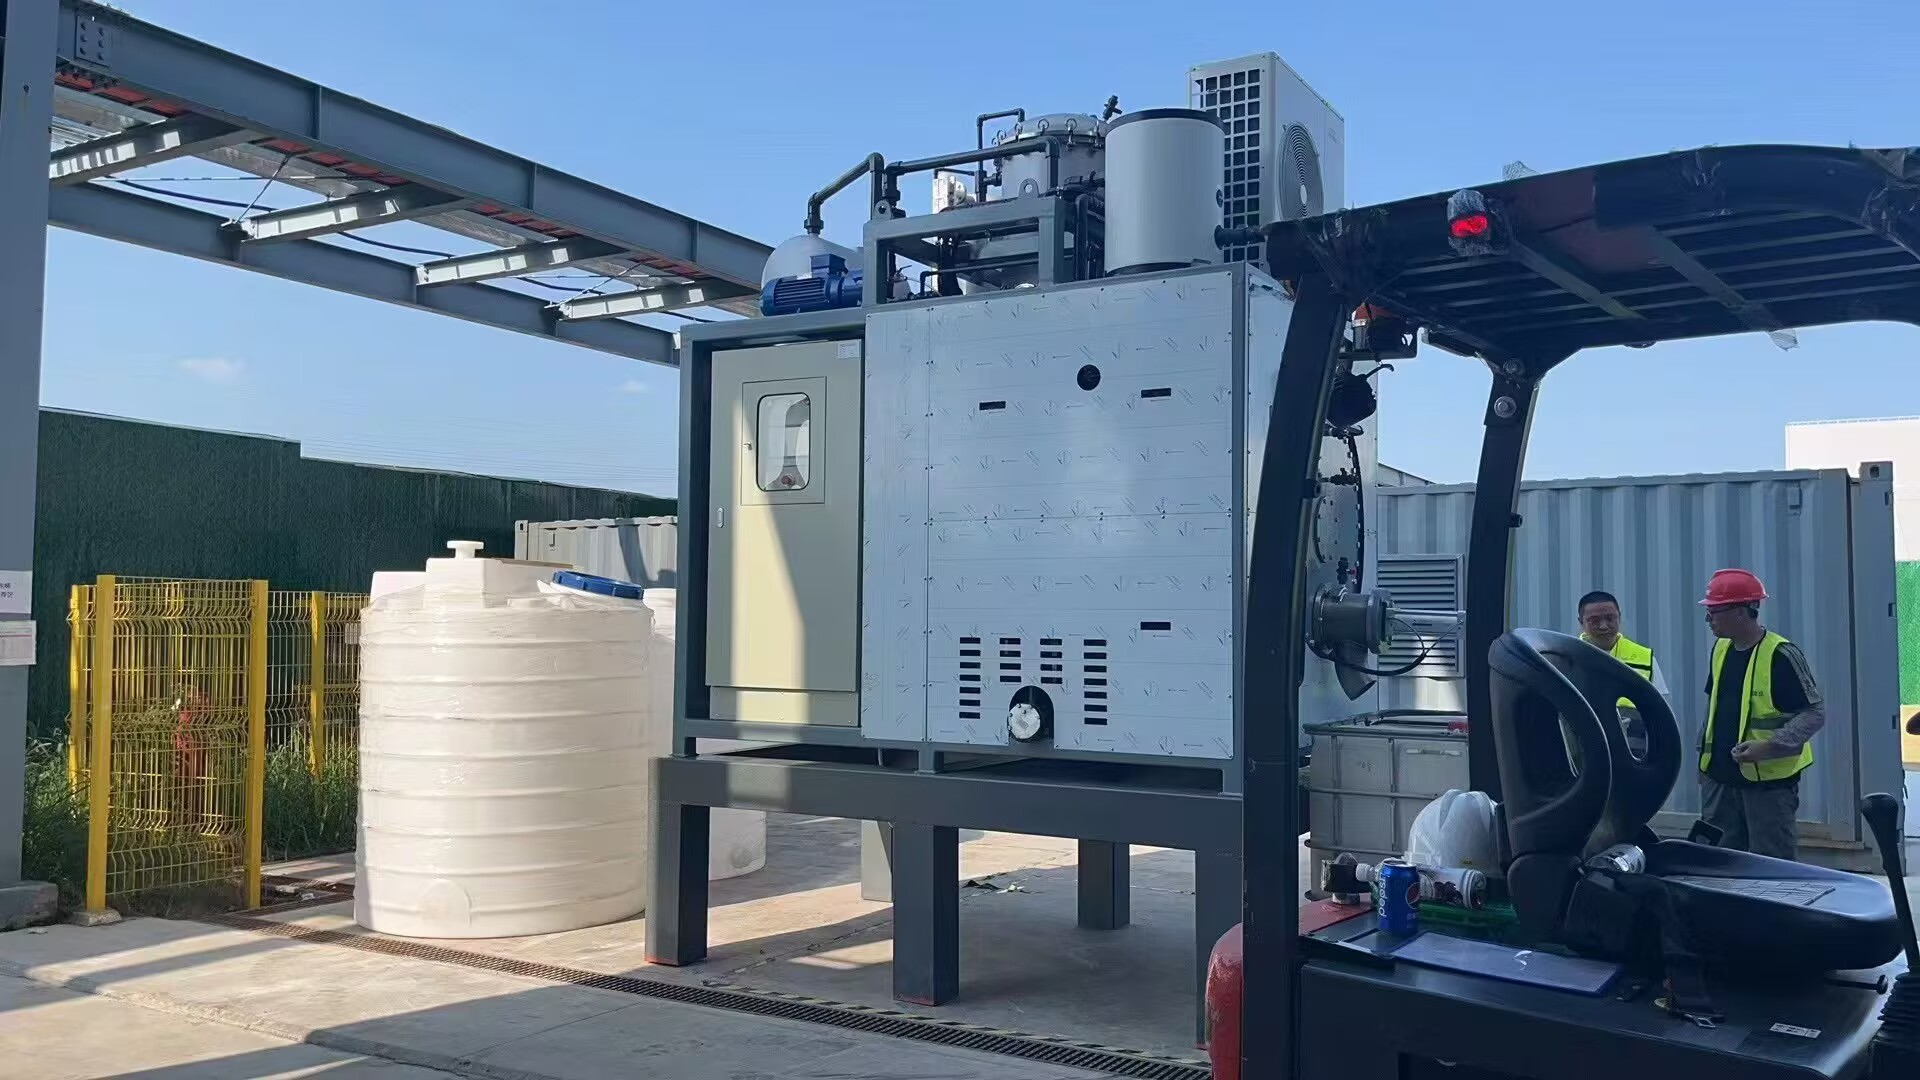
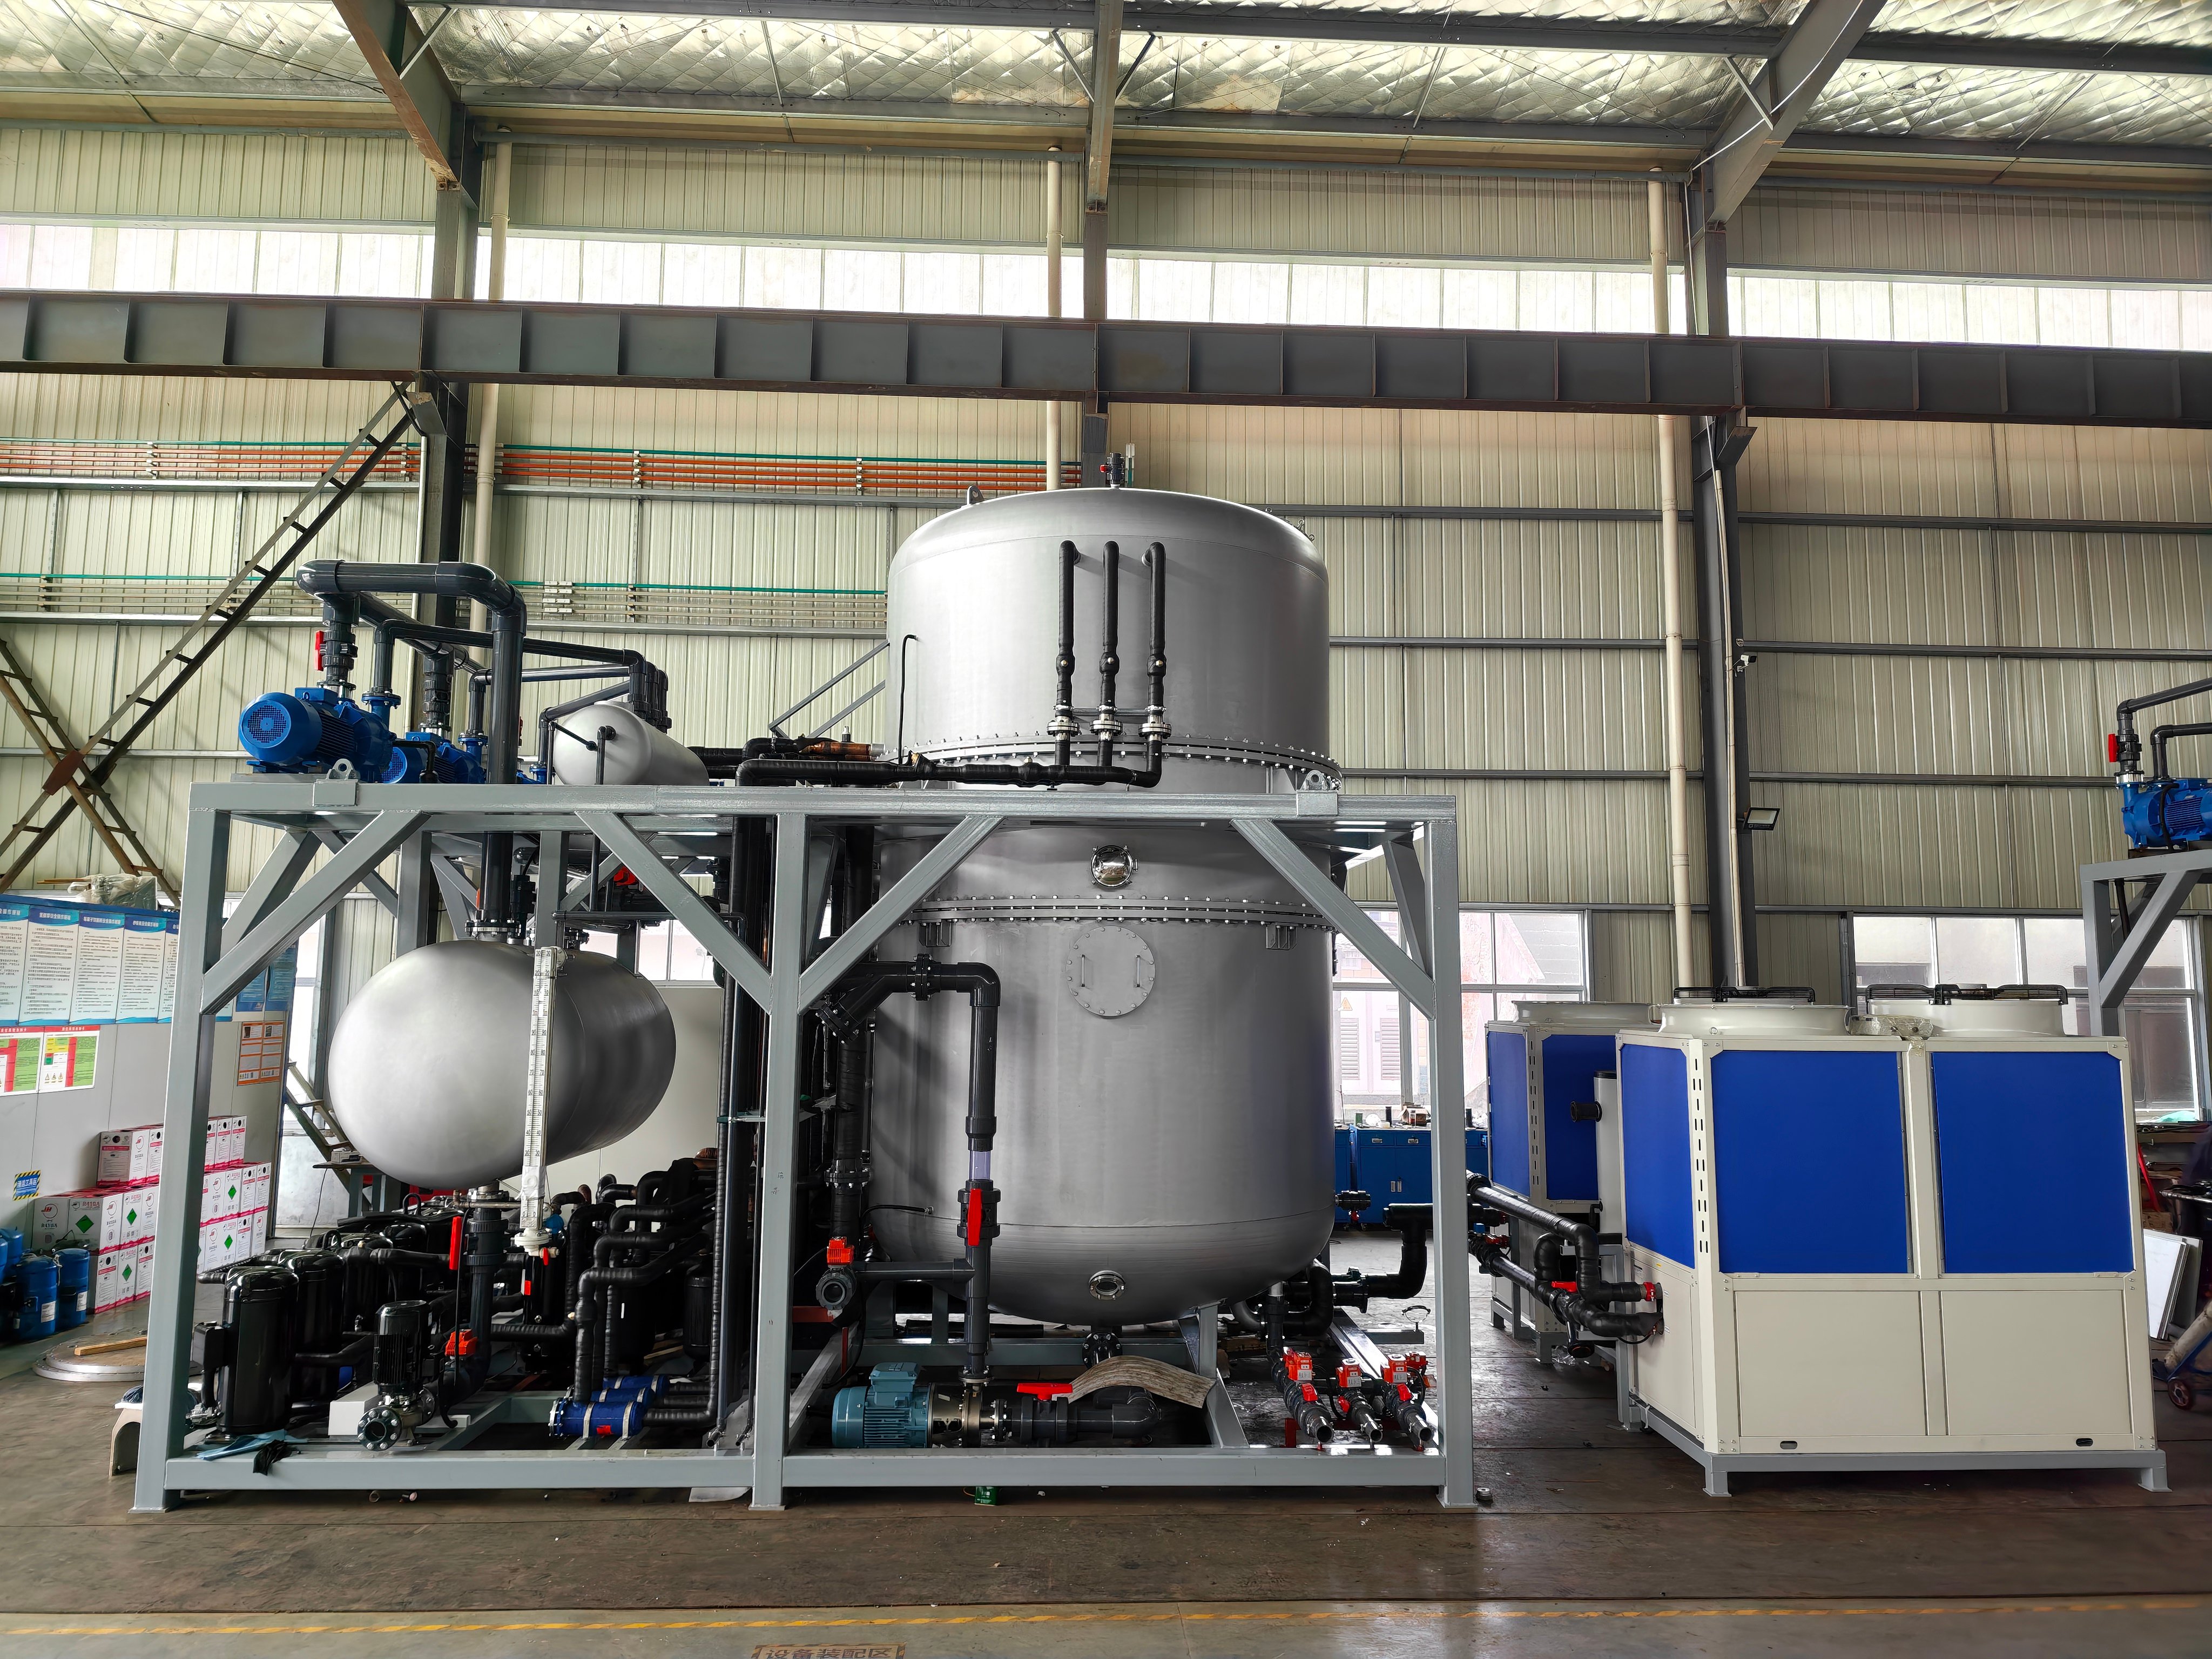
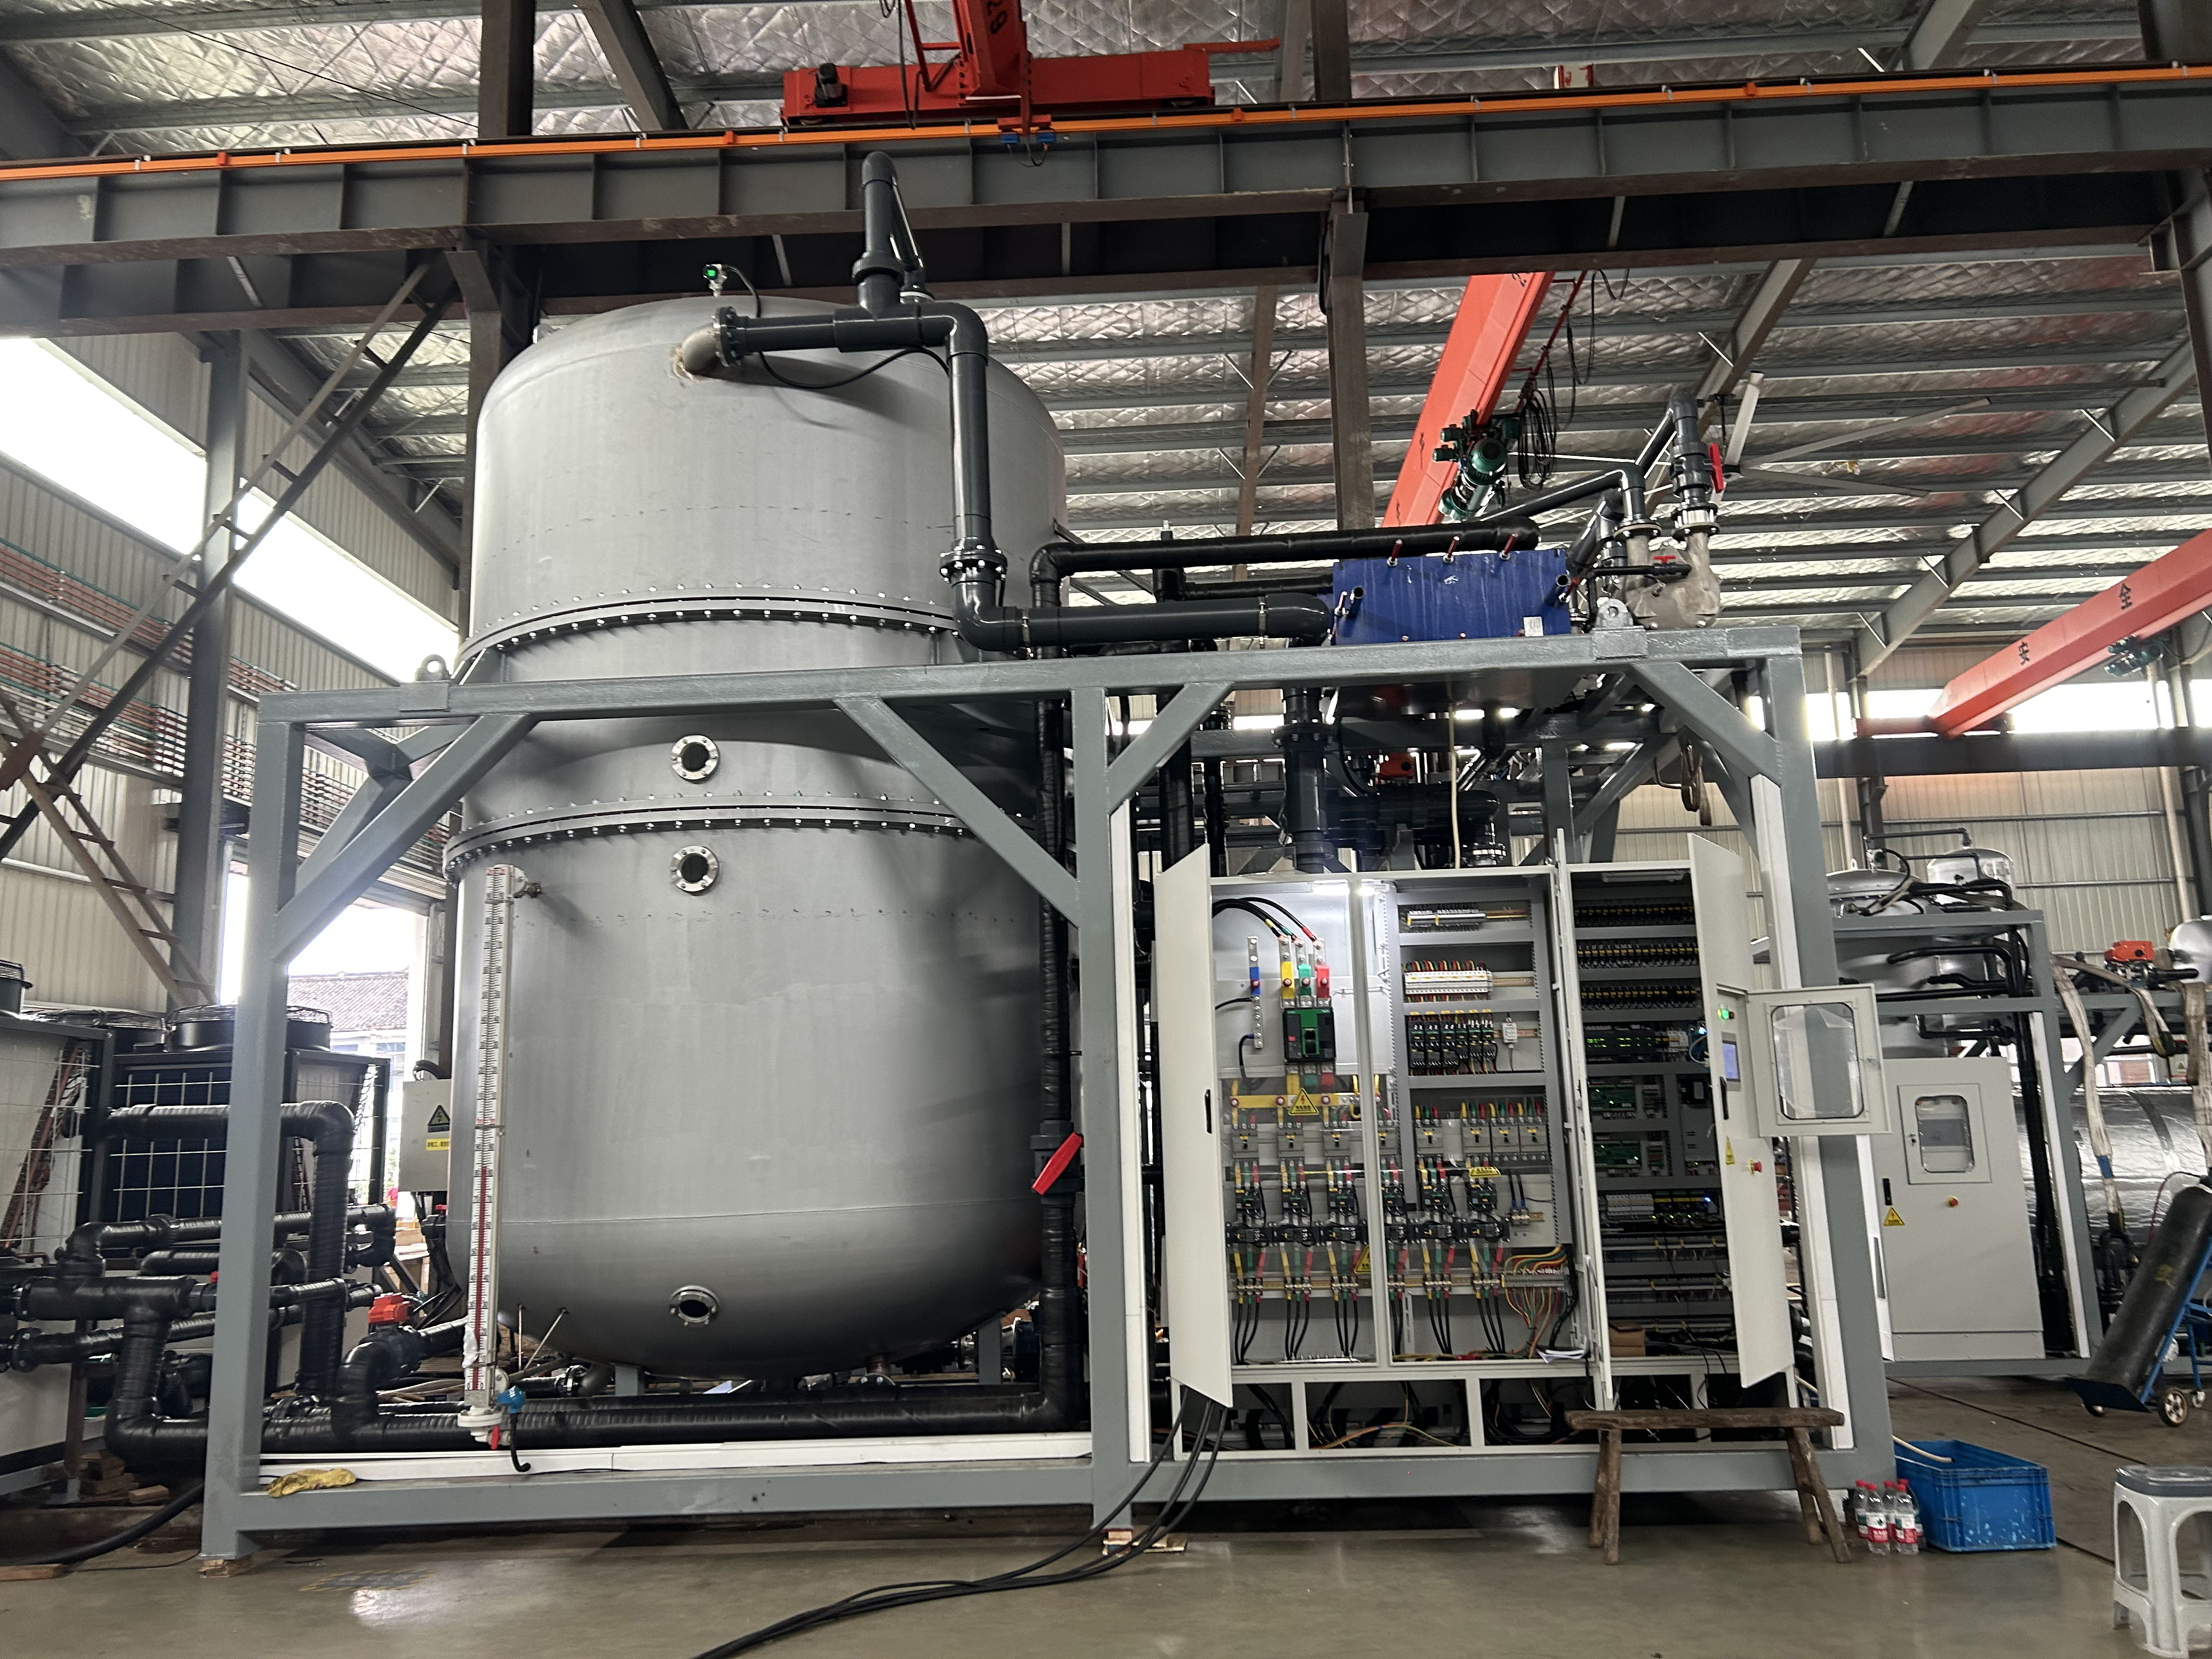
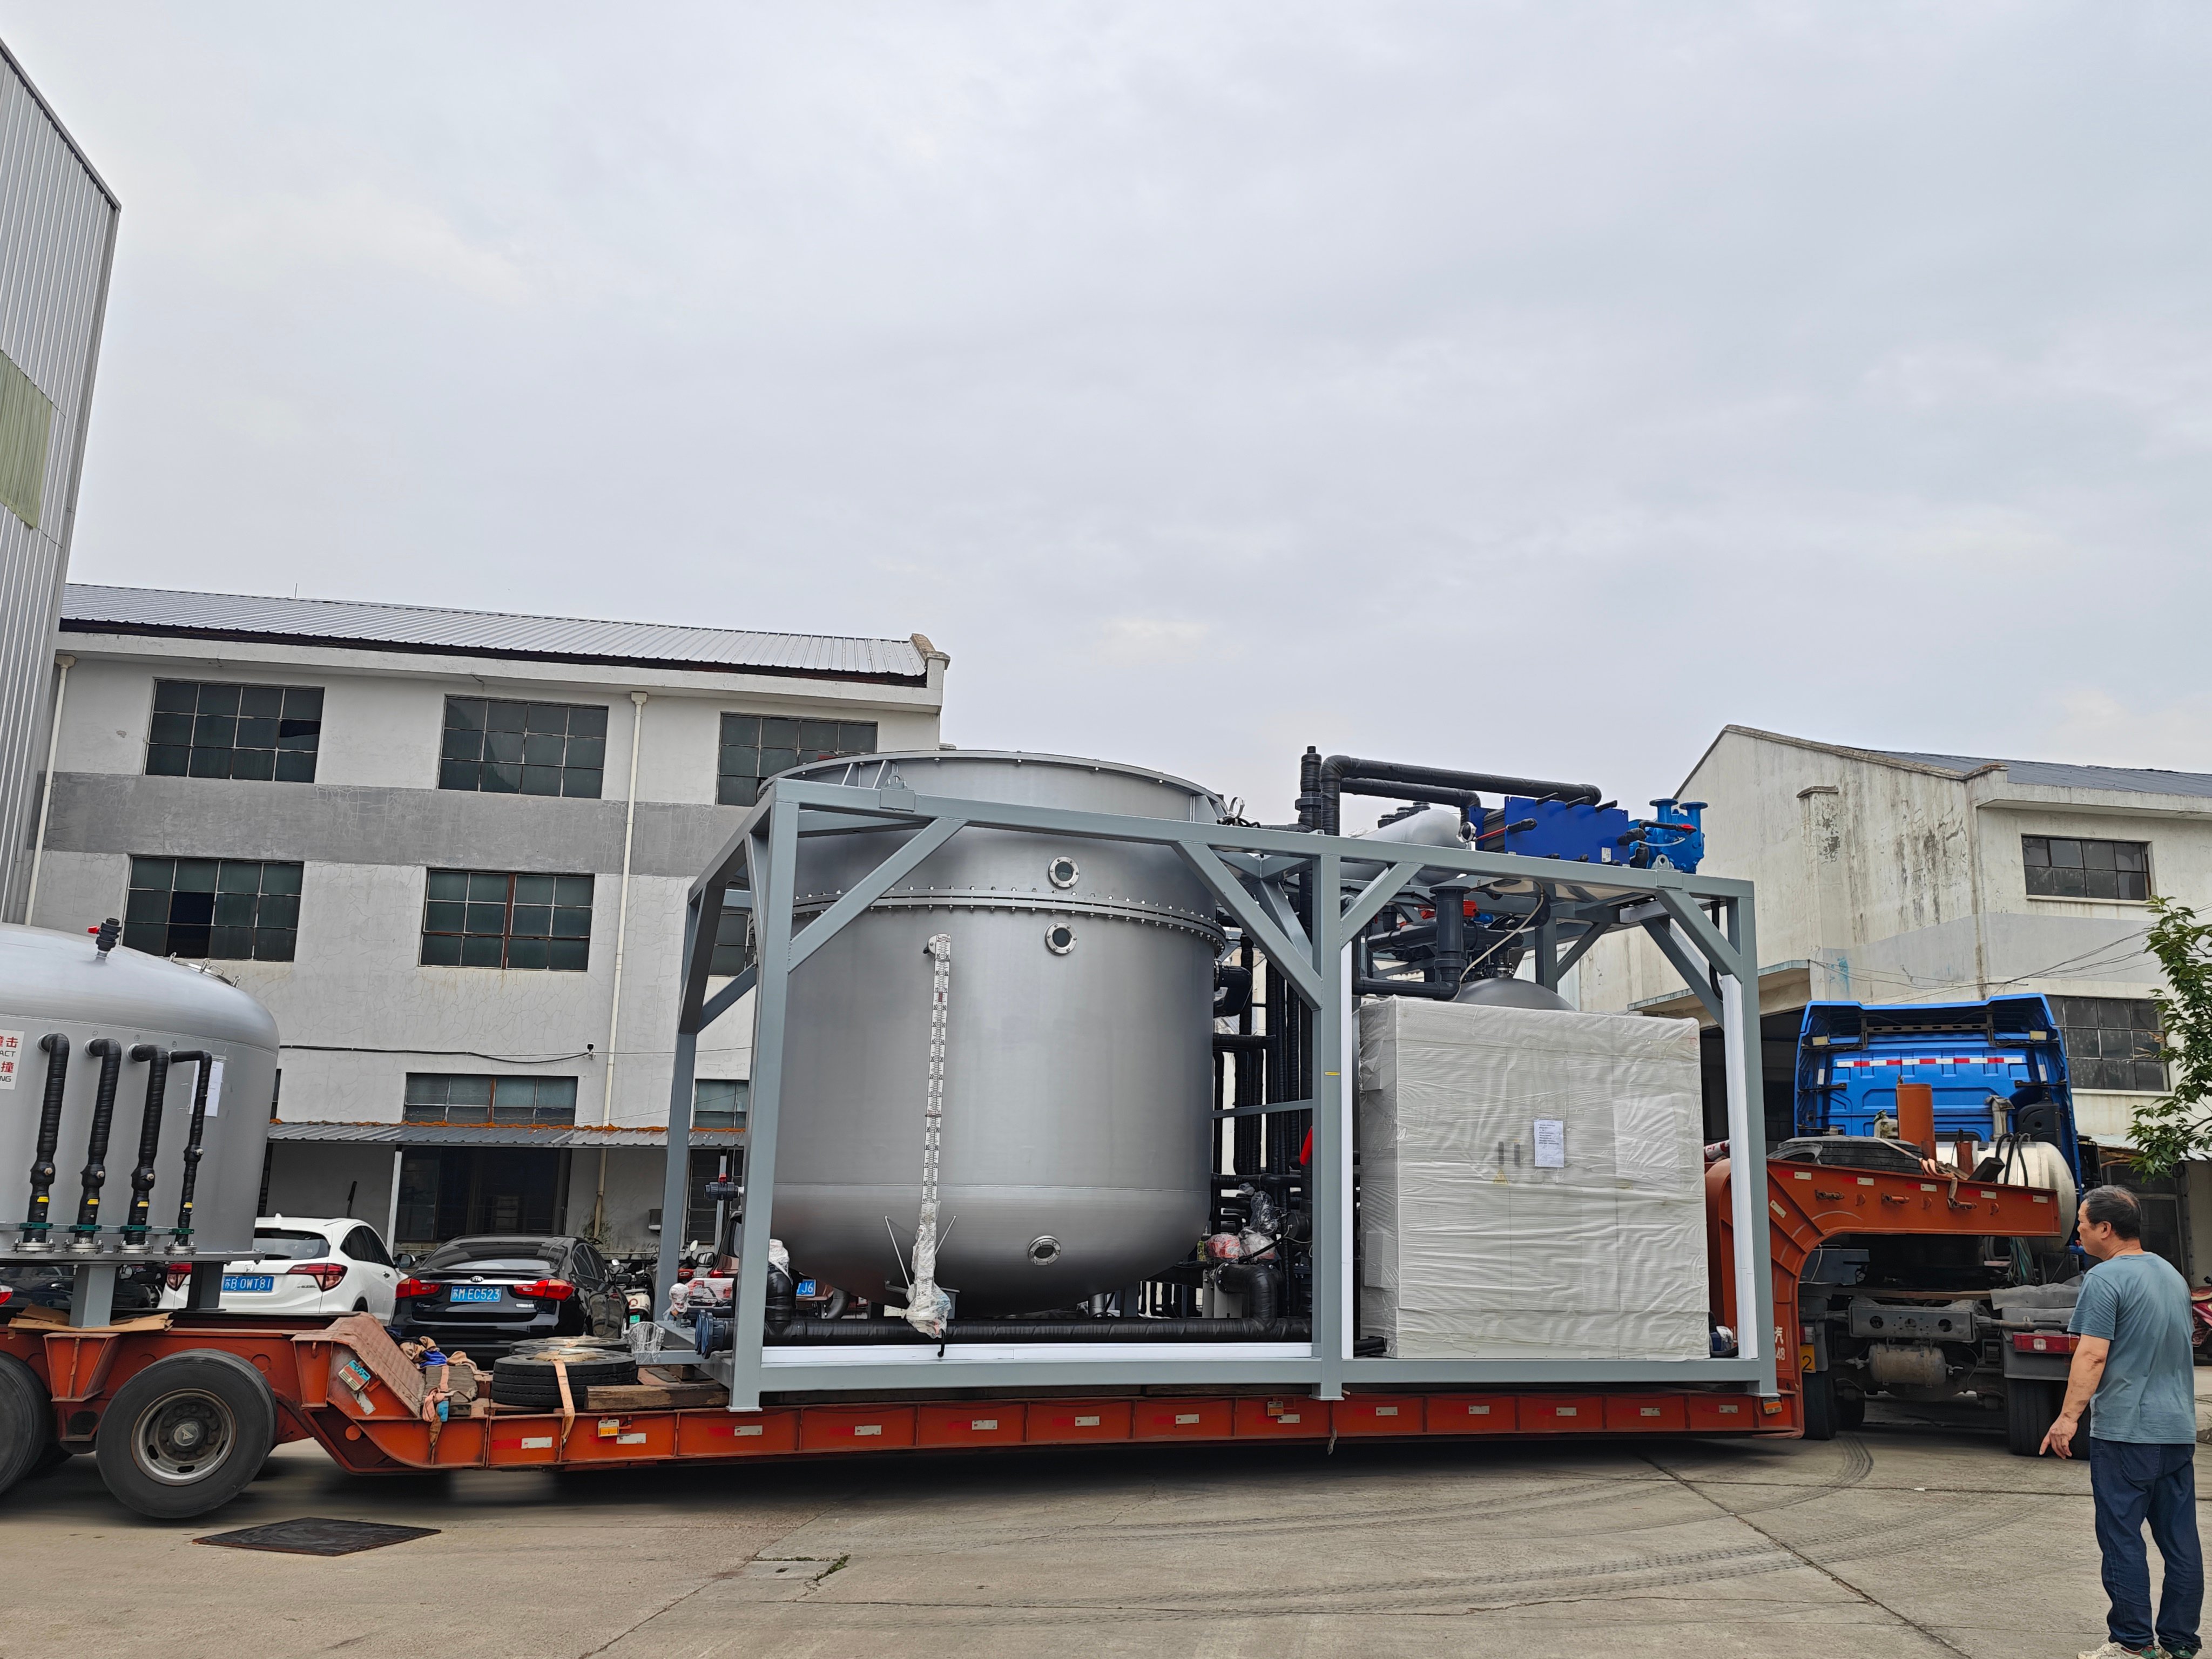
A vacuum concentration unit is a specialized piece of laboratory and industrial equipment designed to rapidly remove solvents and volatile compounds from liquid samples through reduced pressure evaporation. This vacuum concentration unit operates by lowering atmospheric pressure around the sample, which significantly decreases the boiling point of target substances, enabling efficient solvent removal at lower temperatures compared to conventional heating methods. The primary function of a vacuum concentration unit is to concentrate samples by eliminating unwanted liquids while preserving heat-sensitive compounds. The vacuum concentration unit accomplishes this through a combination of vacuum pumps, condensers, and temperature-controlled heating elements that work in harmony. When pressure inside the chamber drops, molecules escape more readily from the liquid phase, traveling through cooling coils where they condense back into liquid form for collection or disposal. Key technological features of a modern vacuum concentration unit include adjustable temperature controls, programmable timer functions, multiple rotor speeds, and digital display systems. The vacuum concentration unit typically incorporates centrifugal force in rotary evaporation models, which enhances mass transfer and accelerates solvent removal processes. These systems are engineered with durable glassware components and reliable mechanical seals to withstand continuous laboratory use. Applications for a vacuum concentration unit span numerous industries and research fields. Pharmaceutical laboratories use the vacuum concentration unit for drug formulation and sample preparation. Environmental testing facilities employ these units for analyzing contaminated water samples. Food science companies utilize the vacuum concentration unit to extract and concentrate flavor compounds. Chemical research departments rely on vacuum concentration units for purifying and concentrating experimental materials, making this equipment indispensable in modern analytical laboratories.

Popular Products

A vacuum concentration unit delivers substantial practical benefits that directly address the needs of researchers and industrial professionals. The most compelling advantage is the remarkable speed of solvent removal compared to traditional evaporation methods. By operating under reduced pressure, the vacuum concentration unit accelerates the entire concentration process, allowing operators to complete multiple samples daily rather than waiting extended periods, which dramatically improves workflow efficiency and research productivity. Operational benefits of using a vacuum concentration unit include superior temperature control and sample protection. Since reduced pressure enables evaporation at lower temperatures, the vacuum concentration unit prevents thermal degradation of heat-sensitive compounds such as vitamins, enzymes, and pharmaceuticals. This protective capability makes the vacuum concentration unit ideal for processing delicate biological and chemical materials that would deteriorate under conventional heating. The vacuum concentration unit offers exceptional versatility across applications, accommodating various sample types and volumes. Whether processing small laboratory samples or larger batches, the vacuum concentration unit adapts to different operational requirements. This flexibility makes the vacuum concentration unit a valuable investment for multi-disciplinary facilities handling diverse research projects. Cost-effectiveness represents another significant advantage of choosing a vacuum concentration unit. By reducing processing time and minimizing sample loss through thermal degradation, the vacuum concentration unit ultimately decreases operational expenses per sample. Additionally, the vacuum concentration unit's energy-efficient operation consumes less electricity than conventional evaporation equipment, contributing to lower utility costs and improved sustainability metrics for facilities seeking to reduce their environmental footprint while maintaining high-quality analytical results.

Latest News

Top 5 Low Temperature Heat Pump Evaporator Applications

24

Jul

Top 5 Low Temperature Heat Pump Evaporator Applications

The low temperature heat pump evaporator represents a critical advancement in industrial thermal management and energy efficiency. This innovative component enables heat pump systems to operate effectively at reduced temperatures, making it indispens...
View More
Benefits of Low Temperature Heat Pump Evaporator in Industry

24

Jul

Benefits of Low Temperature Heat Pump Evaporator in Industry

Industrial facilities worldwide face mounting pressure to reduce operating costs while maintaining production quality and environmental compliance. The low temperature heat pump evaporator has emerged as a transformative solution that addresses these...
View More
Common Challenges in Industrial Water Treatment Solved

02

Sep

Common Challenges in Industrial Water Treatment Solved

Manufacturing facilities, chemical plants, and processing operations face mounting pressure to manage wastewater efficiently while meeting regulatory standards. Industrial water treatment remains one of the most critical operational functions across ...
View More
Top 5 Evaporator System Design Features for Industry

24

Jul

Top 5 Evaporator System Design Features for Industry

Selecting the right evaporator system design is critical for industrial operations managing wastewater treatment, chemical processing, and liquid concentration challenges. An effective evaporator system design determines not only operational efficien...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

vacuum concentration unit

Rapid Solvent Removal Technology

Rapid Solvent Removal Technology

The vacuum concentration unit incorporates advanced rapid solvent removal technology that dramatically accelerates the evaporation process. By reducing atmospheric pressure within the chamber, the vacuum concentration unit creates optimal conditions for volatile compounds to escape from liquid samples quickly and efficiently. This technological advantage means researchers can process samples in hours rather than days, significantly boosting laboratory productivity. The vacuum concentration unit's rotary evaporation mechanism combines rotation with vacuum conditions, multiplying the contact surface area between sample and chamber walls. This enhanced mass transfer mechanism sets the vacuum concentration unit apart from conventional methods, making it the preferred choice for time-sensitive research applications. Laboratories implementing a vacuum concentration unit report completing approximately three times more samples daily compared to static evaporation techniques.
Thermal Protection for Sensitive Compounds

Thermal Protection for Sensitive Compounds

A premium vacuum concentration unit preserves the integrity of heat-sensitive materials through its innovative low-temperature evaporation process. Since the vacuum concentration unit operates under reduced pressure, volatile compounds boil at substantially lower temperatures, protecting valuable pharmaceutical compounds, biological extracts, and delicate chemical specimens from degradation. This thermal protection capability makes the vacuum concentration unit essential in pharmaceutical development, where active ingredients must remain chemically unchanged. The vacuum concentration unit's temperature management system maintains precise control throughout processing, preventing unwanted reactions or decomposition. Researchers working with vitamins, antibodies, or essential oils particularly value how the vacuum concentration unit preserves compound potency and effectiveness. This protective feature directly translates to improved research outcomes and product quality, making the vacuum concentration unit an investment in scientific excellence.
Reliable Performance and Durability

Reliable Performance and Durability

The vacuum concentration unit is engineered with robust construction standards that ensure dependable performance across demanding laboratory environments. High-quality vacuum concentration units feature reinforced glassware components, precision mechanical seals, and industrial-grade pumps designed for continuous daily operation. The vacuum concentration unit's construction quality means facilities experience minimal downtime and reduced maintenance requirements, directly lowering operational costs. Superior craftsmanship in the vacuum concentration unit translates to consistent, reproducible results that meet rigorous analytical standards. Modern vacuum concentration units incorporate fail-safe systems and pressure monitoring technology that prevent equipment damage and sample loss. Investing in a well-designed vacuum concentration unit provides long-term reliability, with many units delivering excellent performance across five to ten years of intensive laboratory use, making it a financially sensible choice for institutions prioritizing equipment longevity and cost efficiency.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000