Industrial Liquid Concentrator Systems

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

industrial liquid concentrator

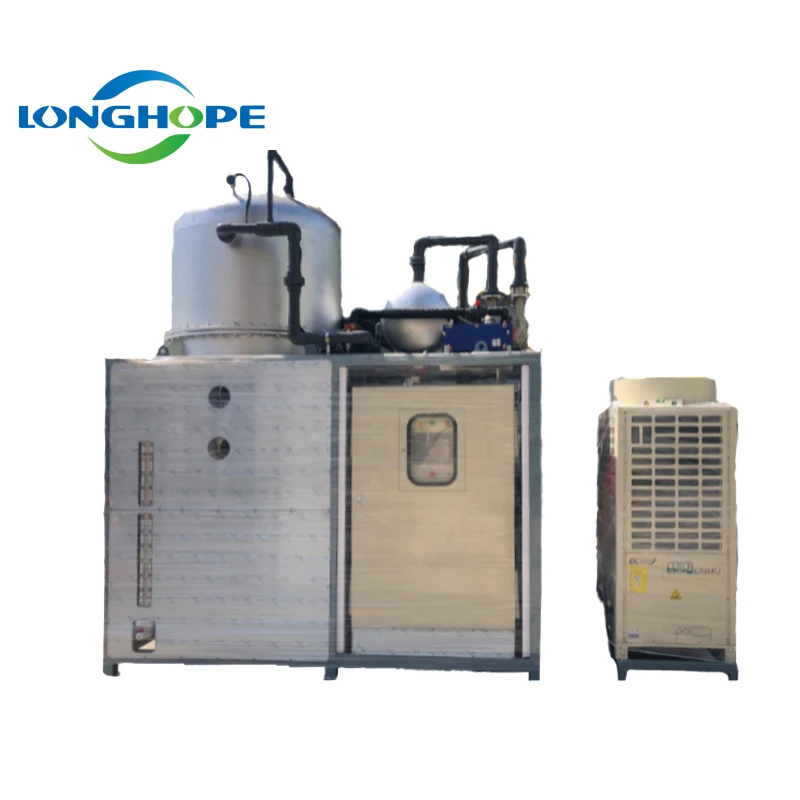
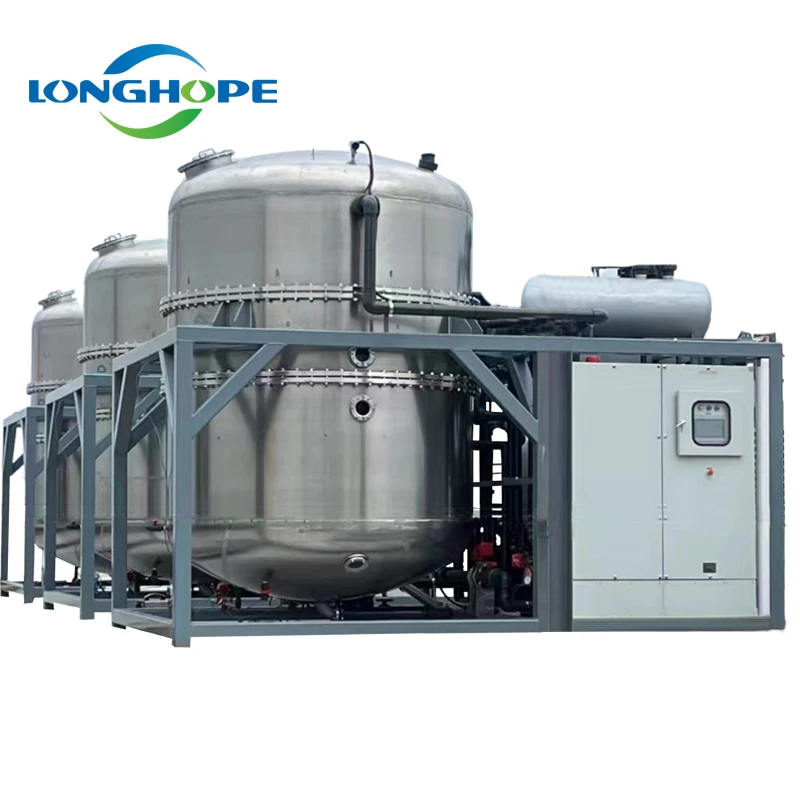
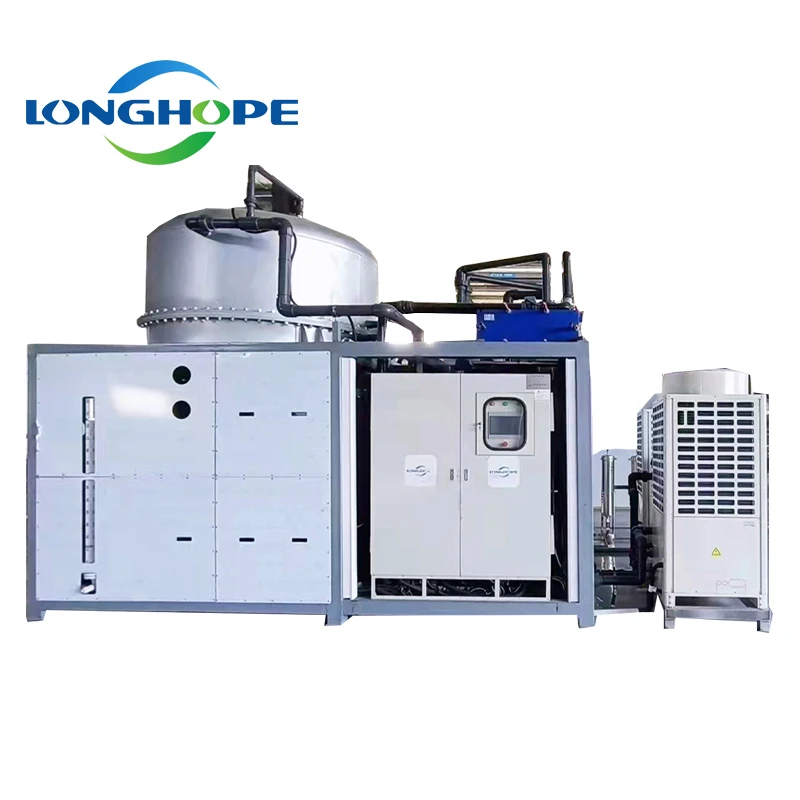
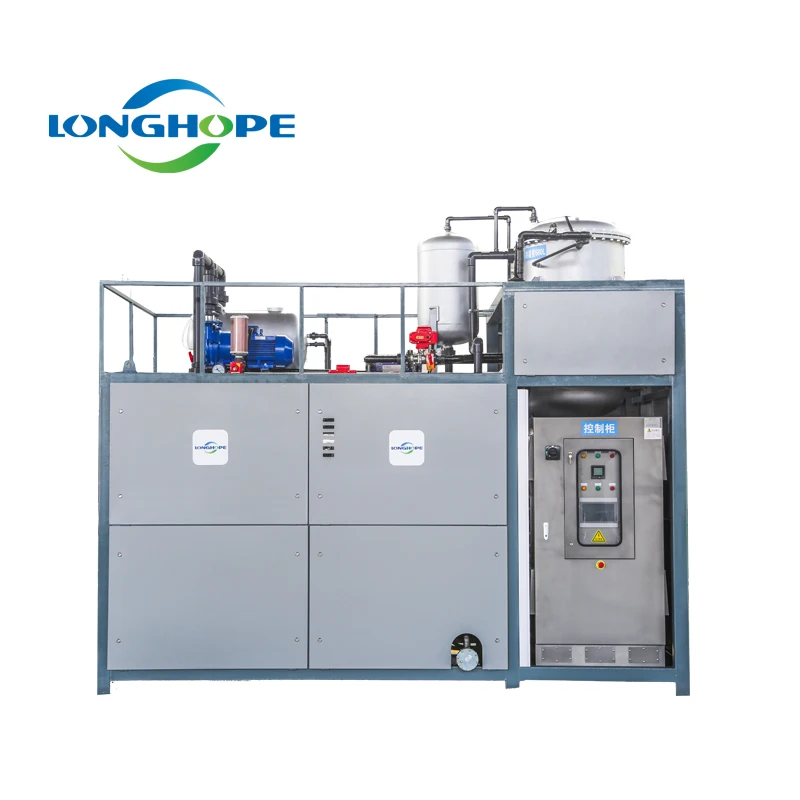
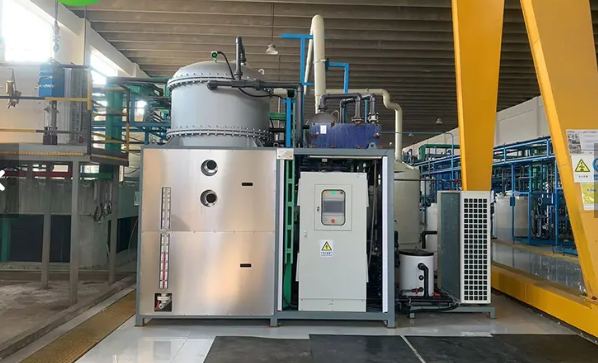
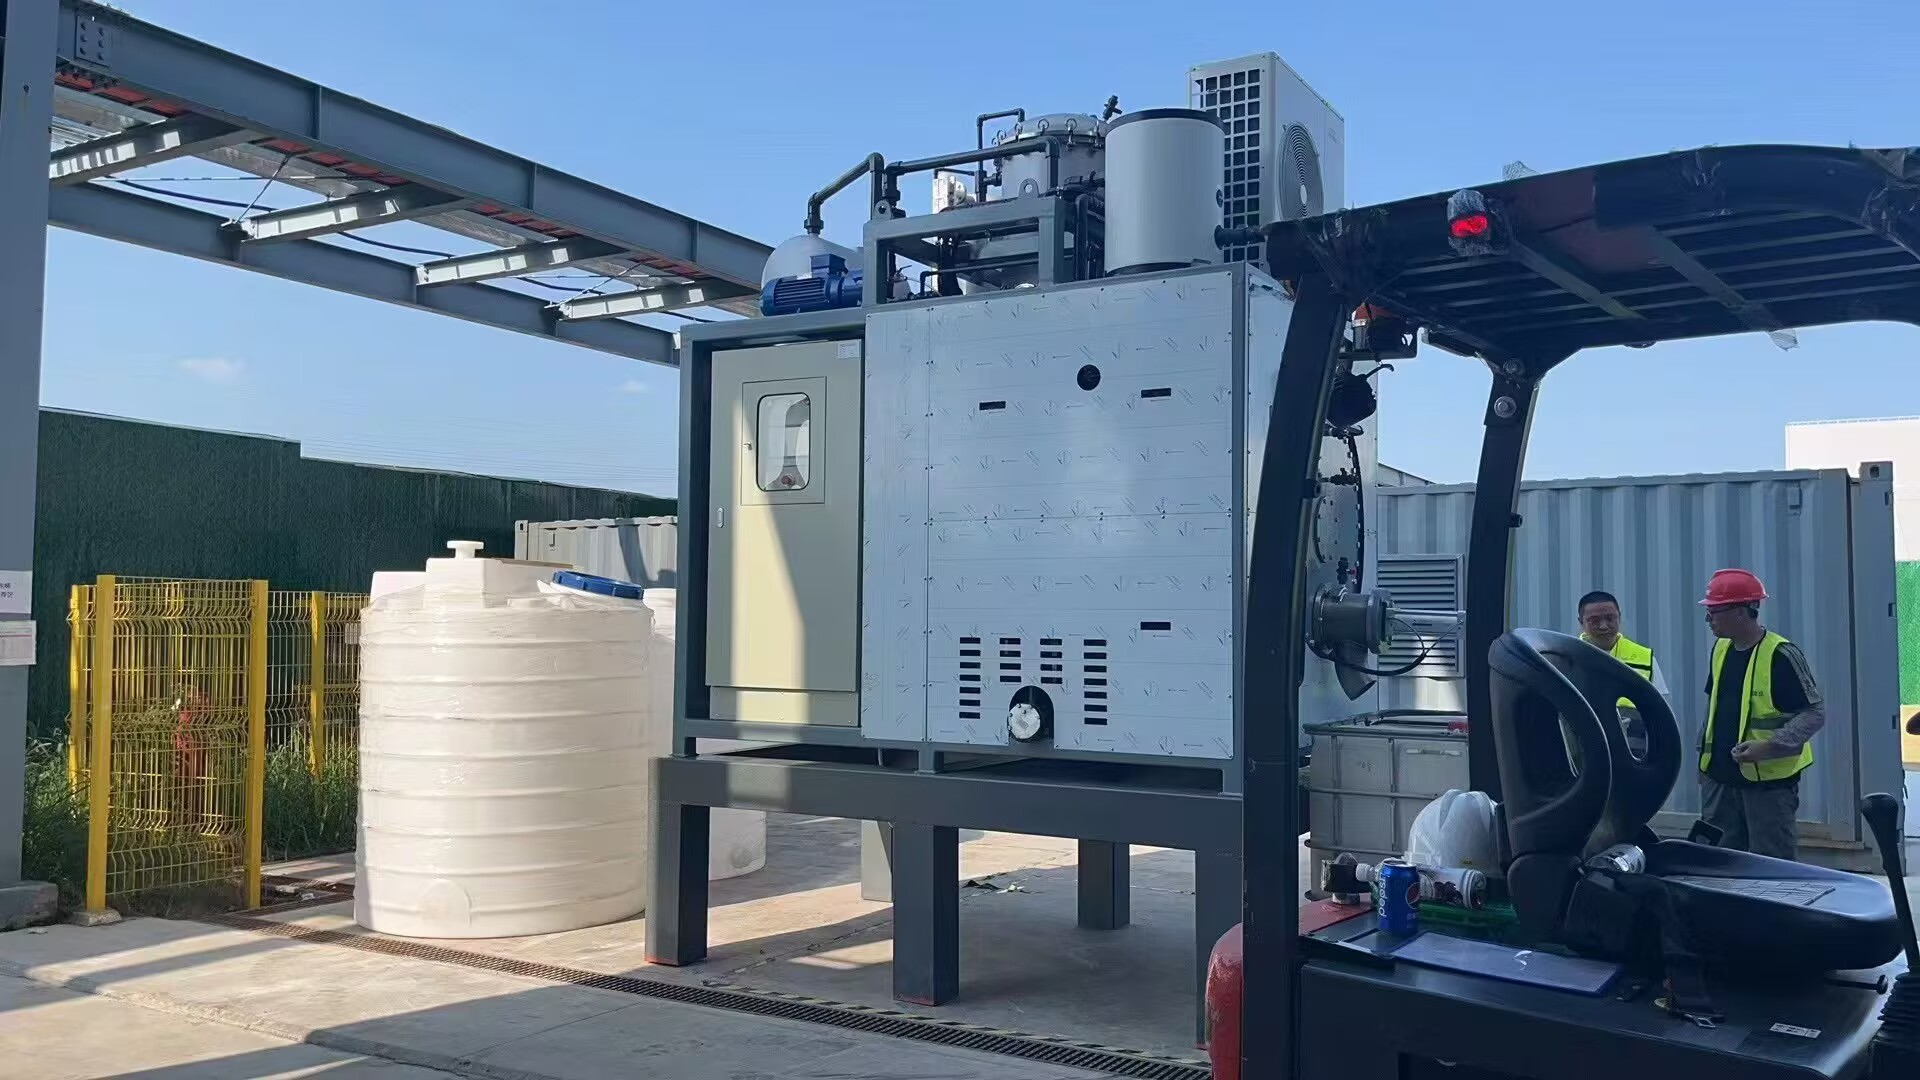
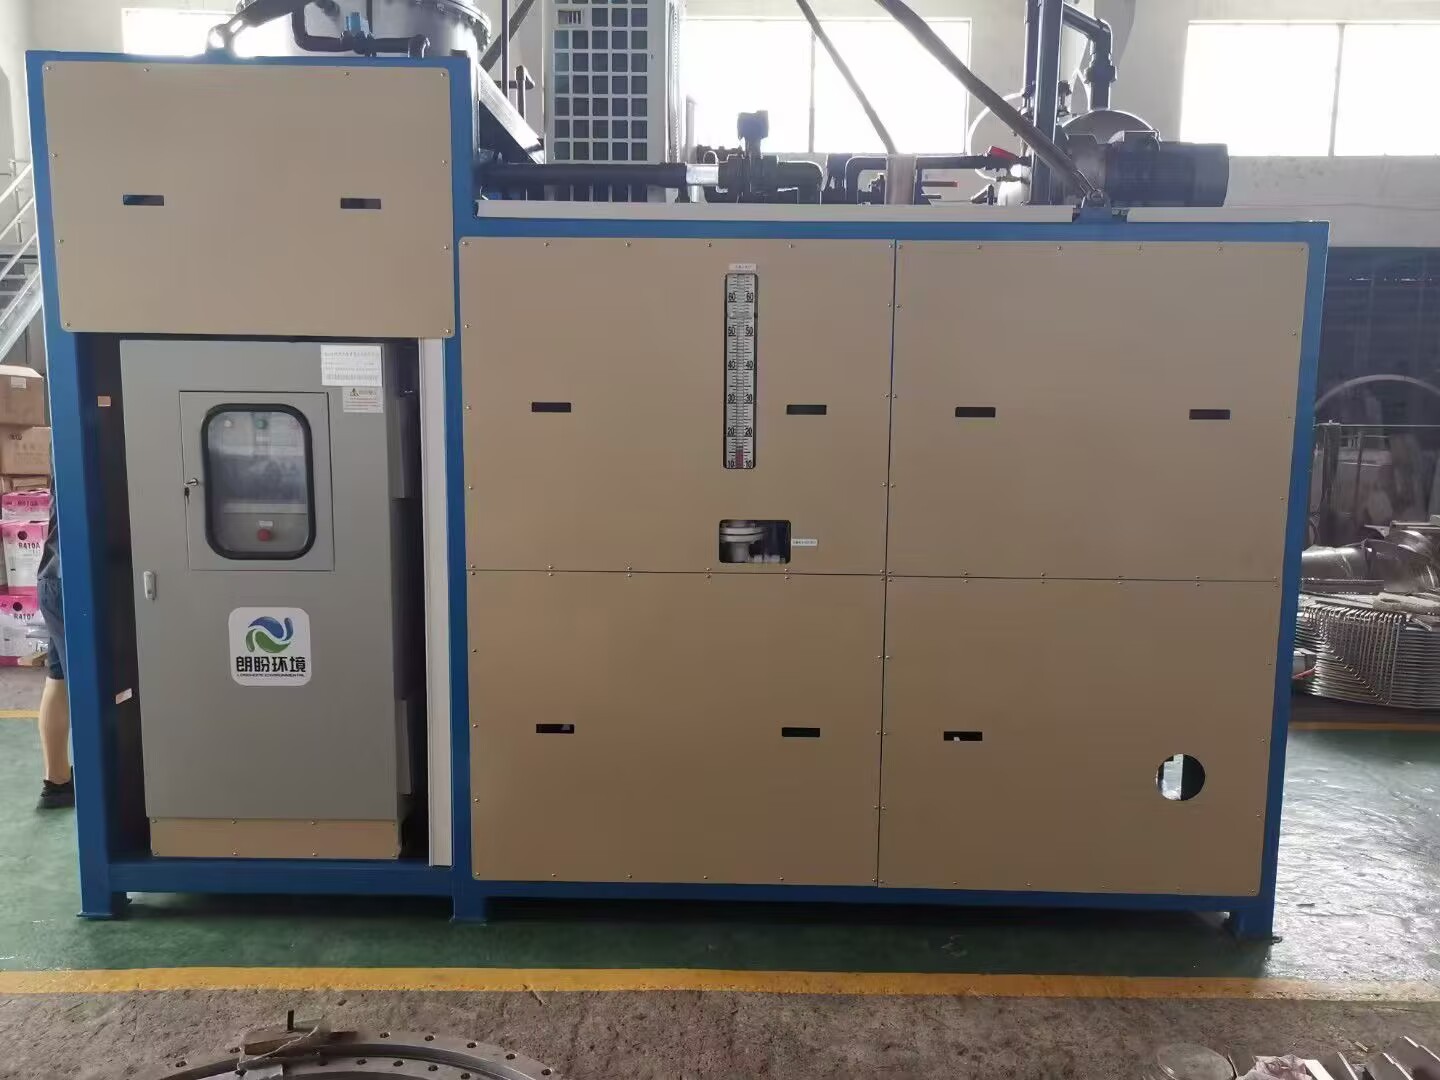
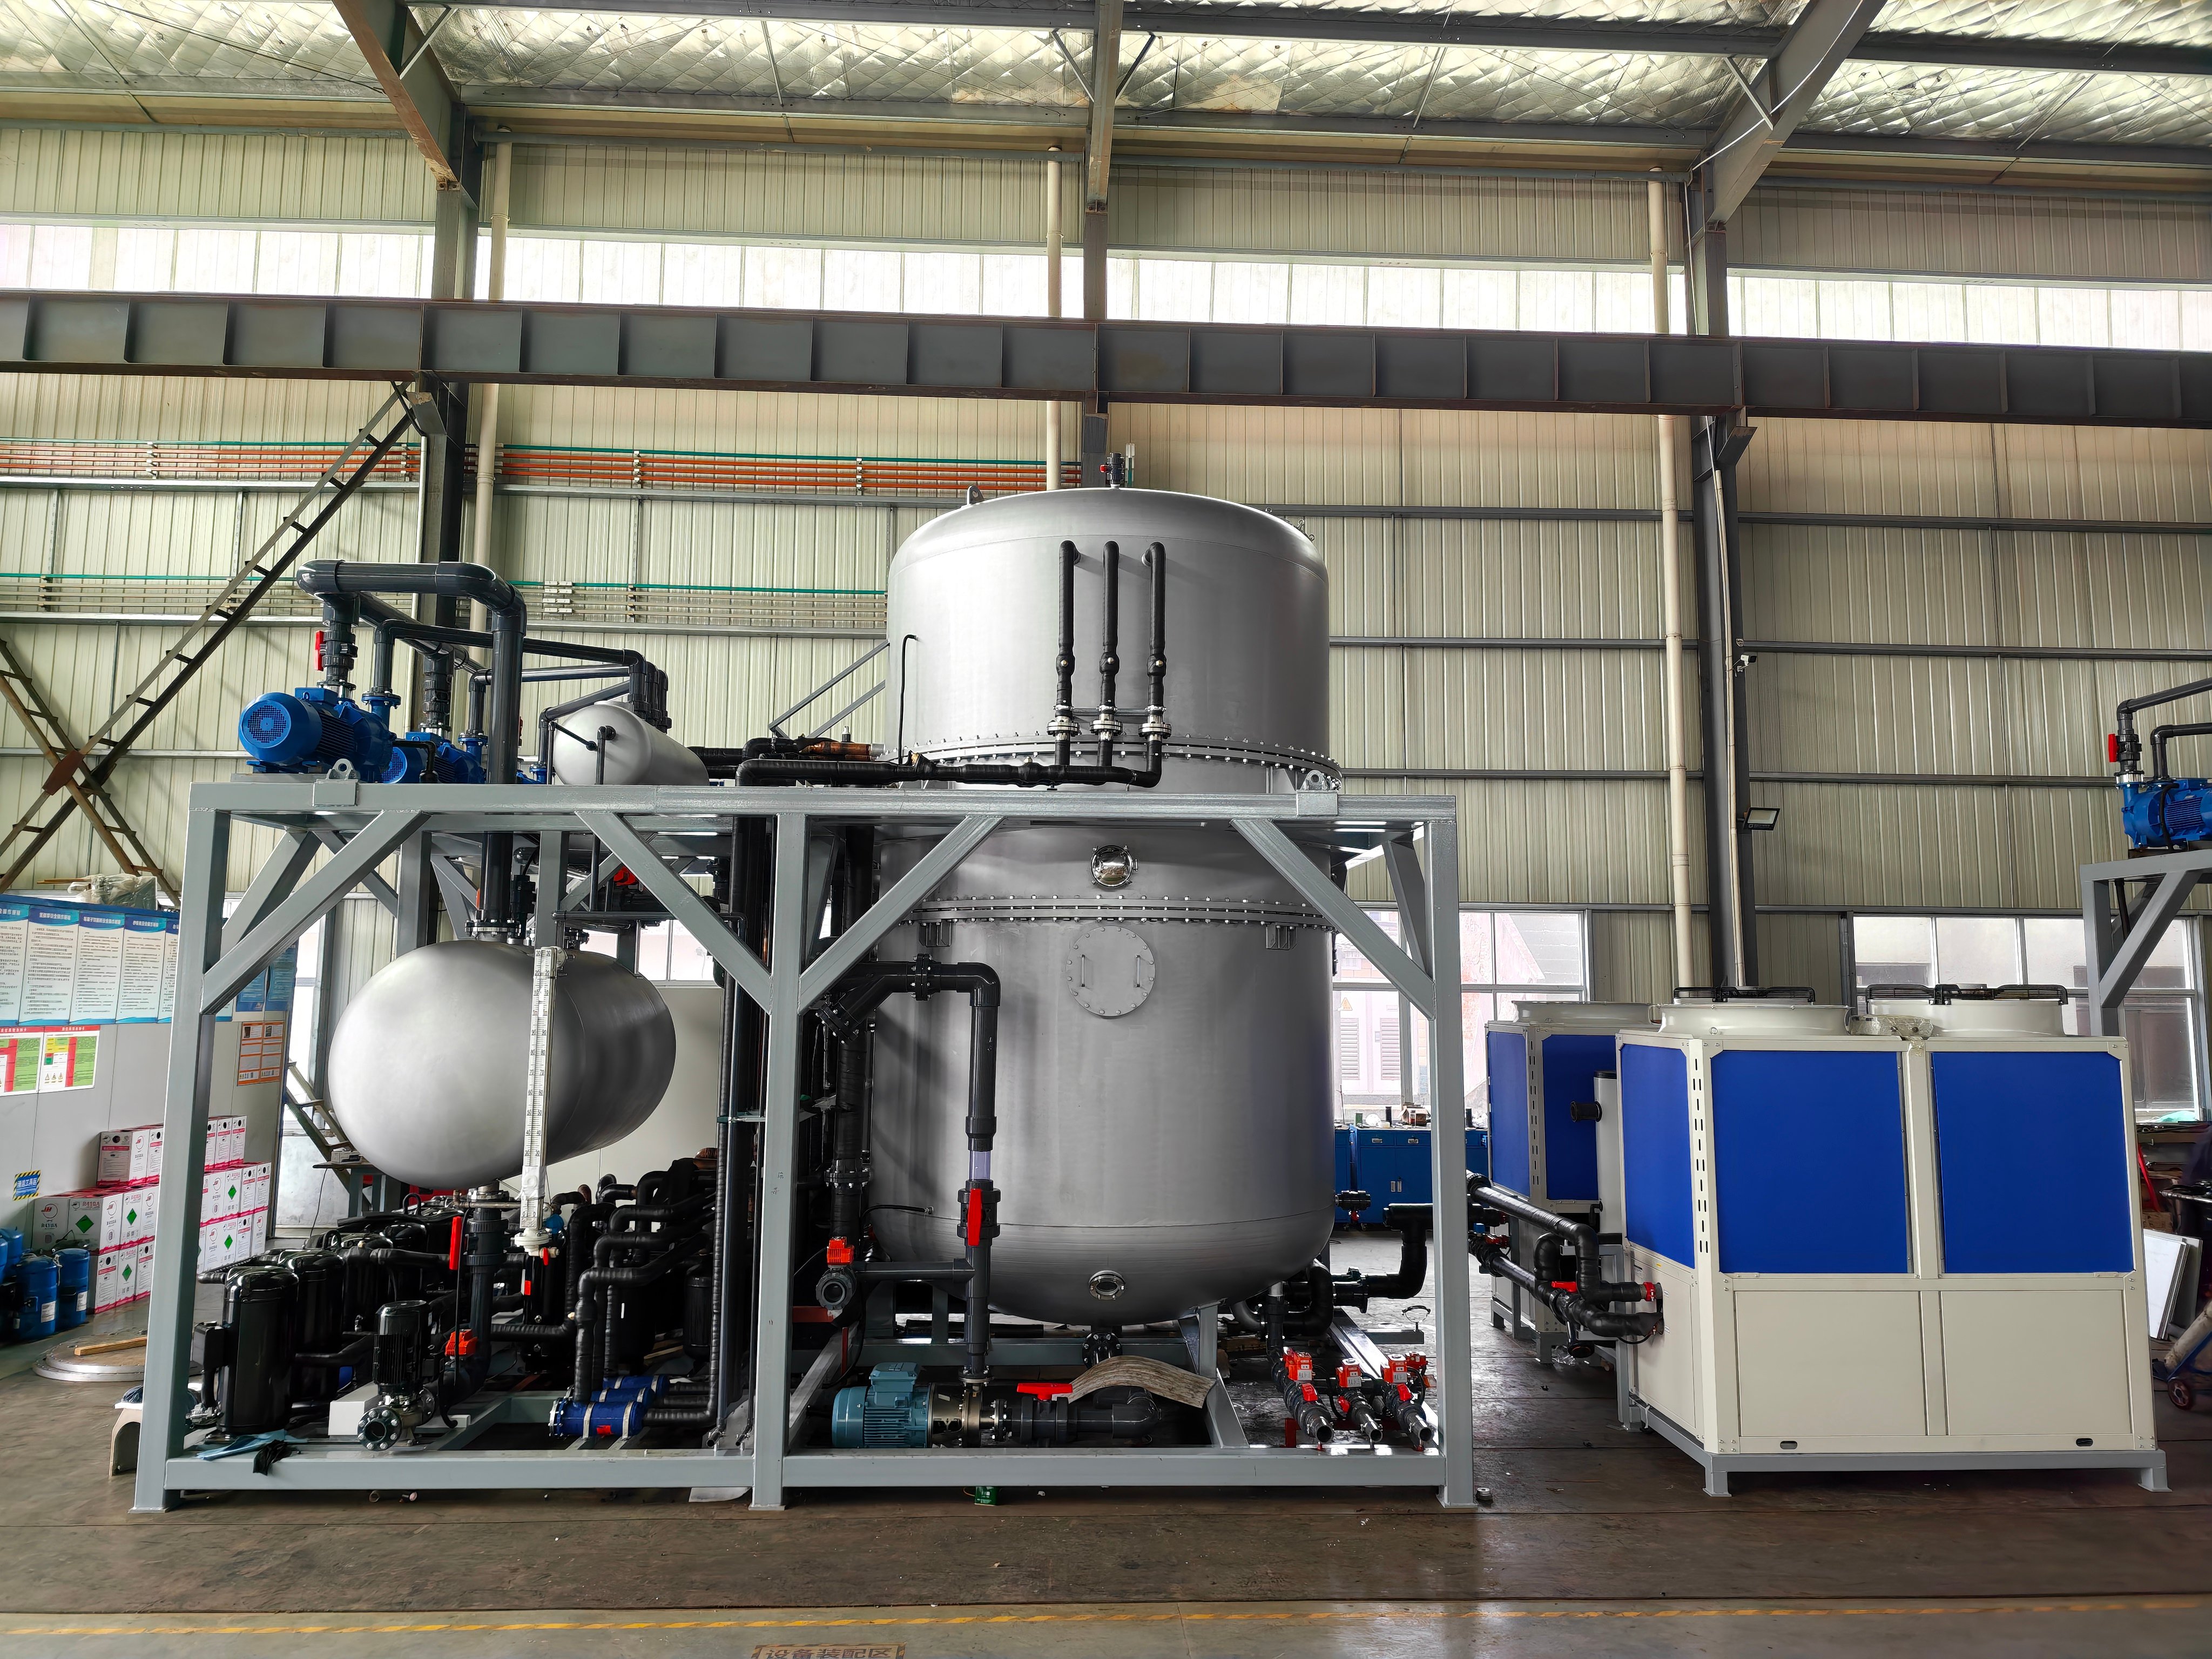
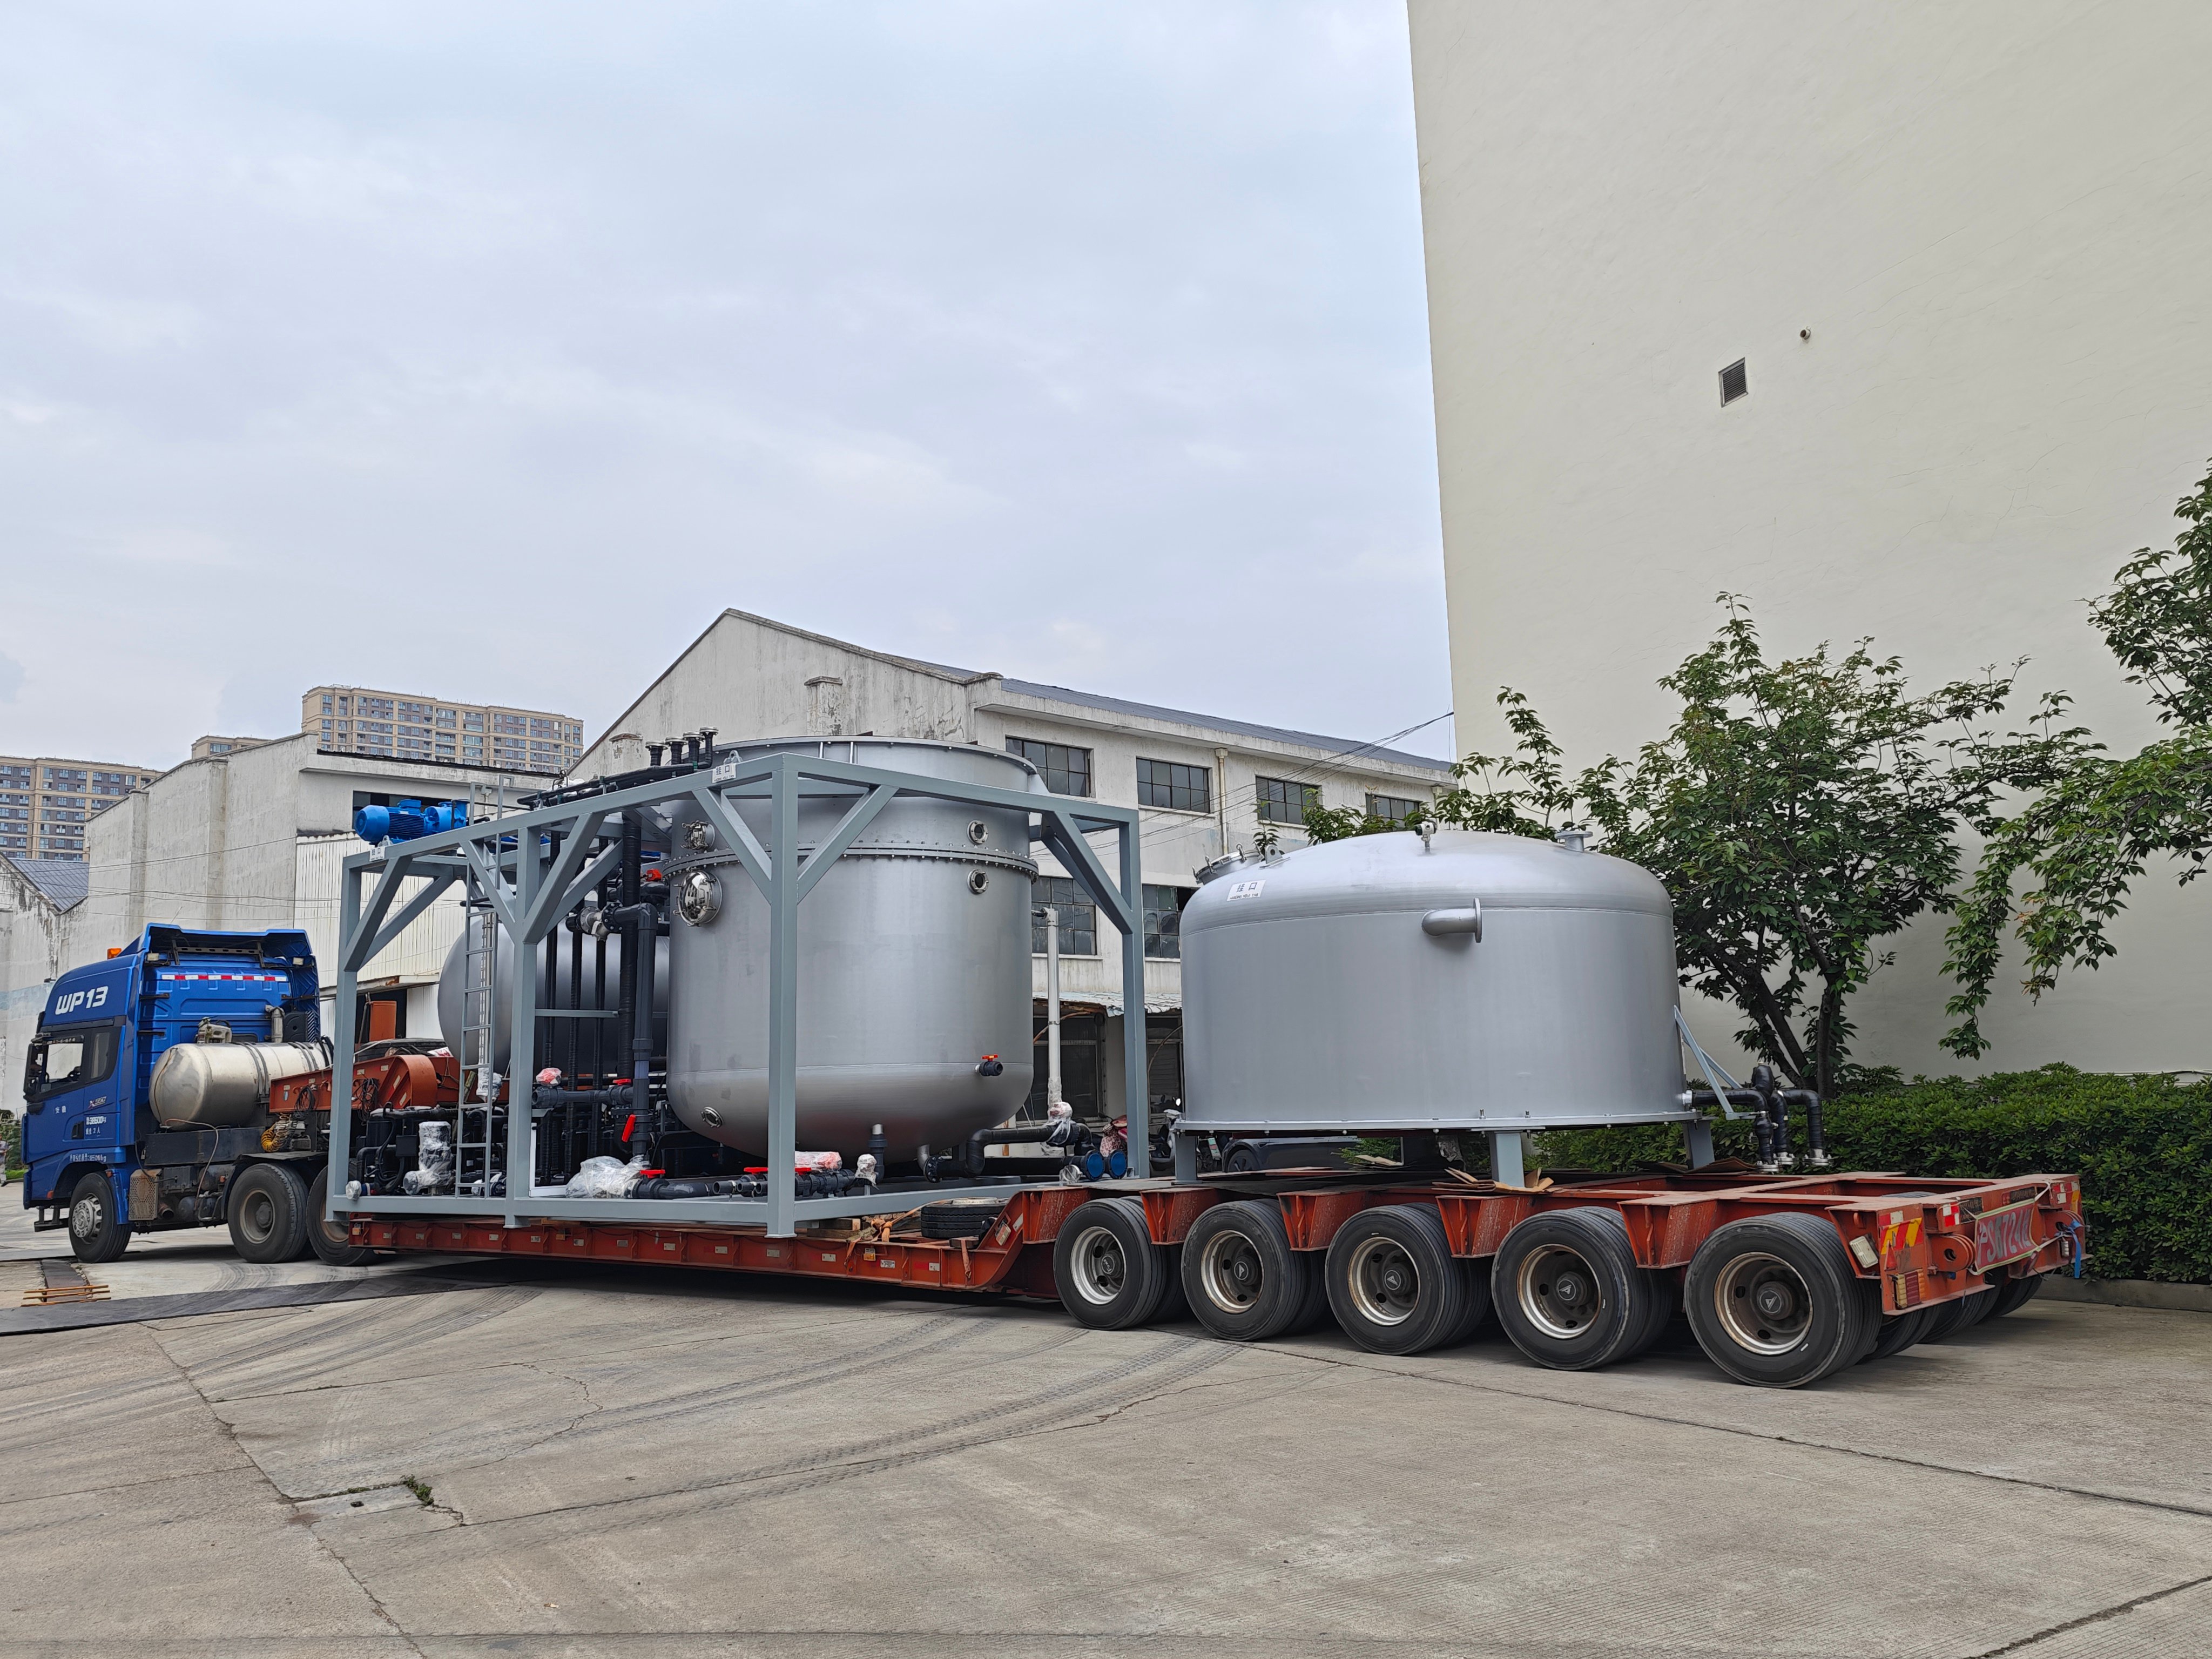
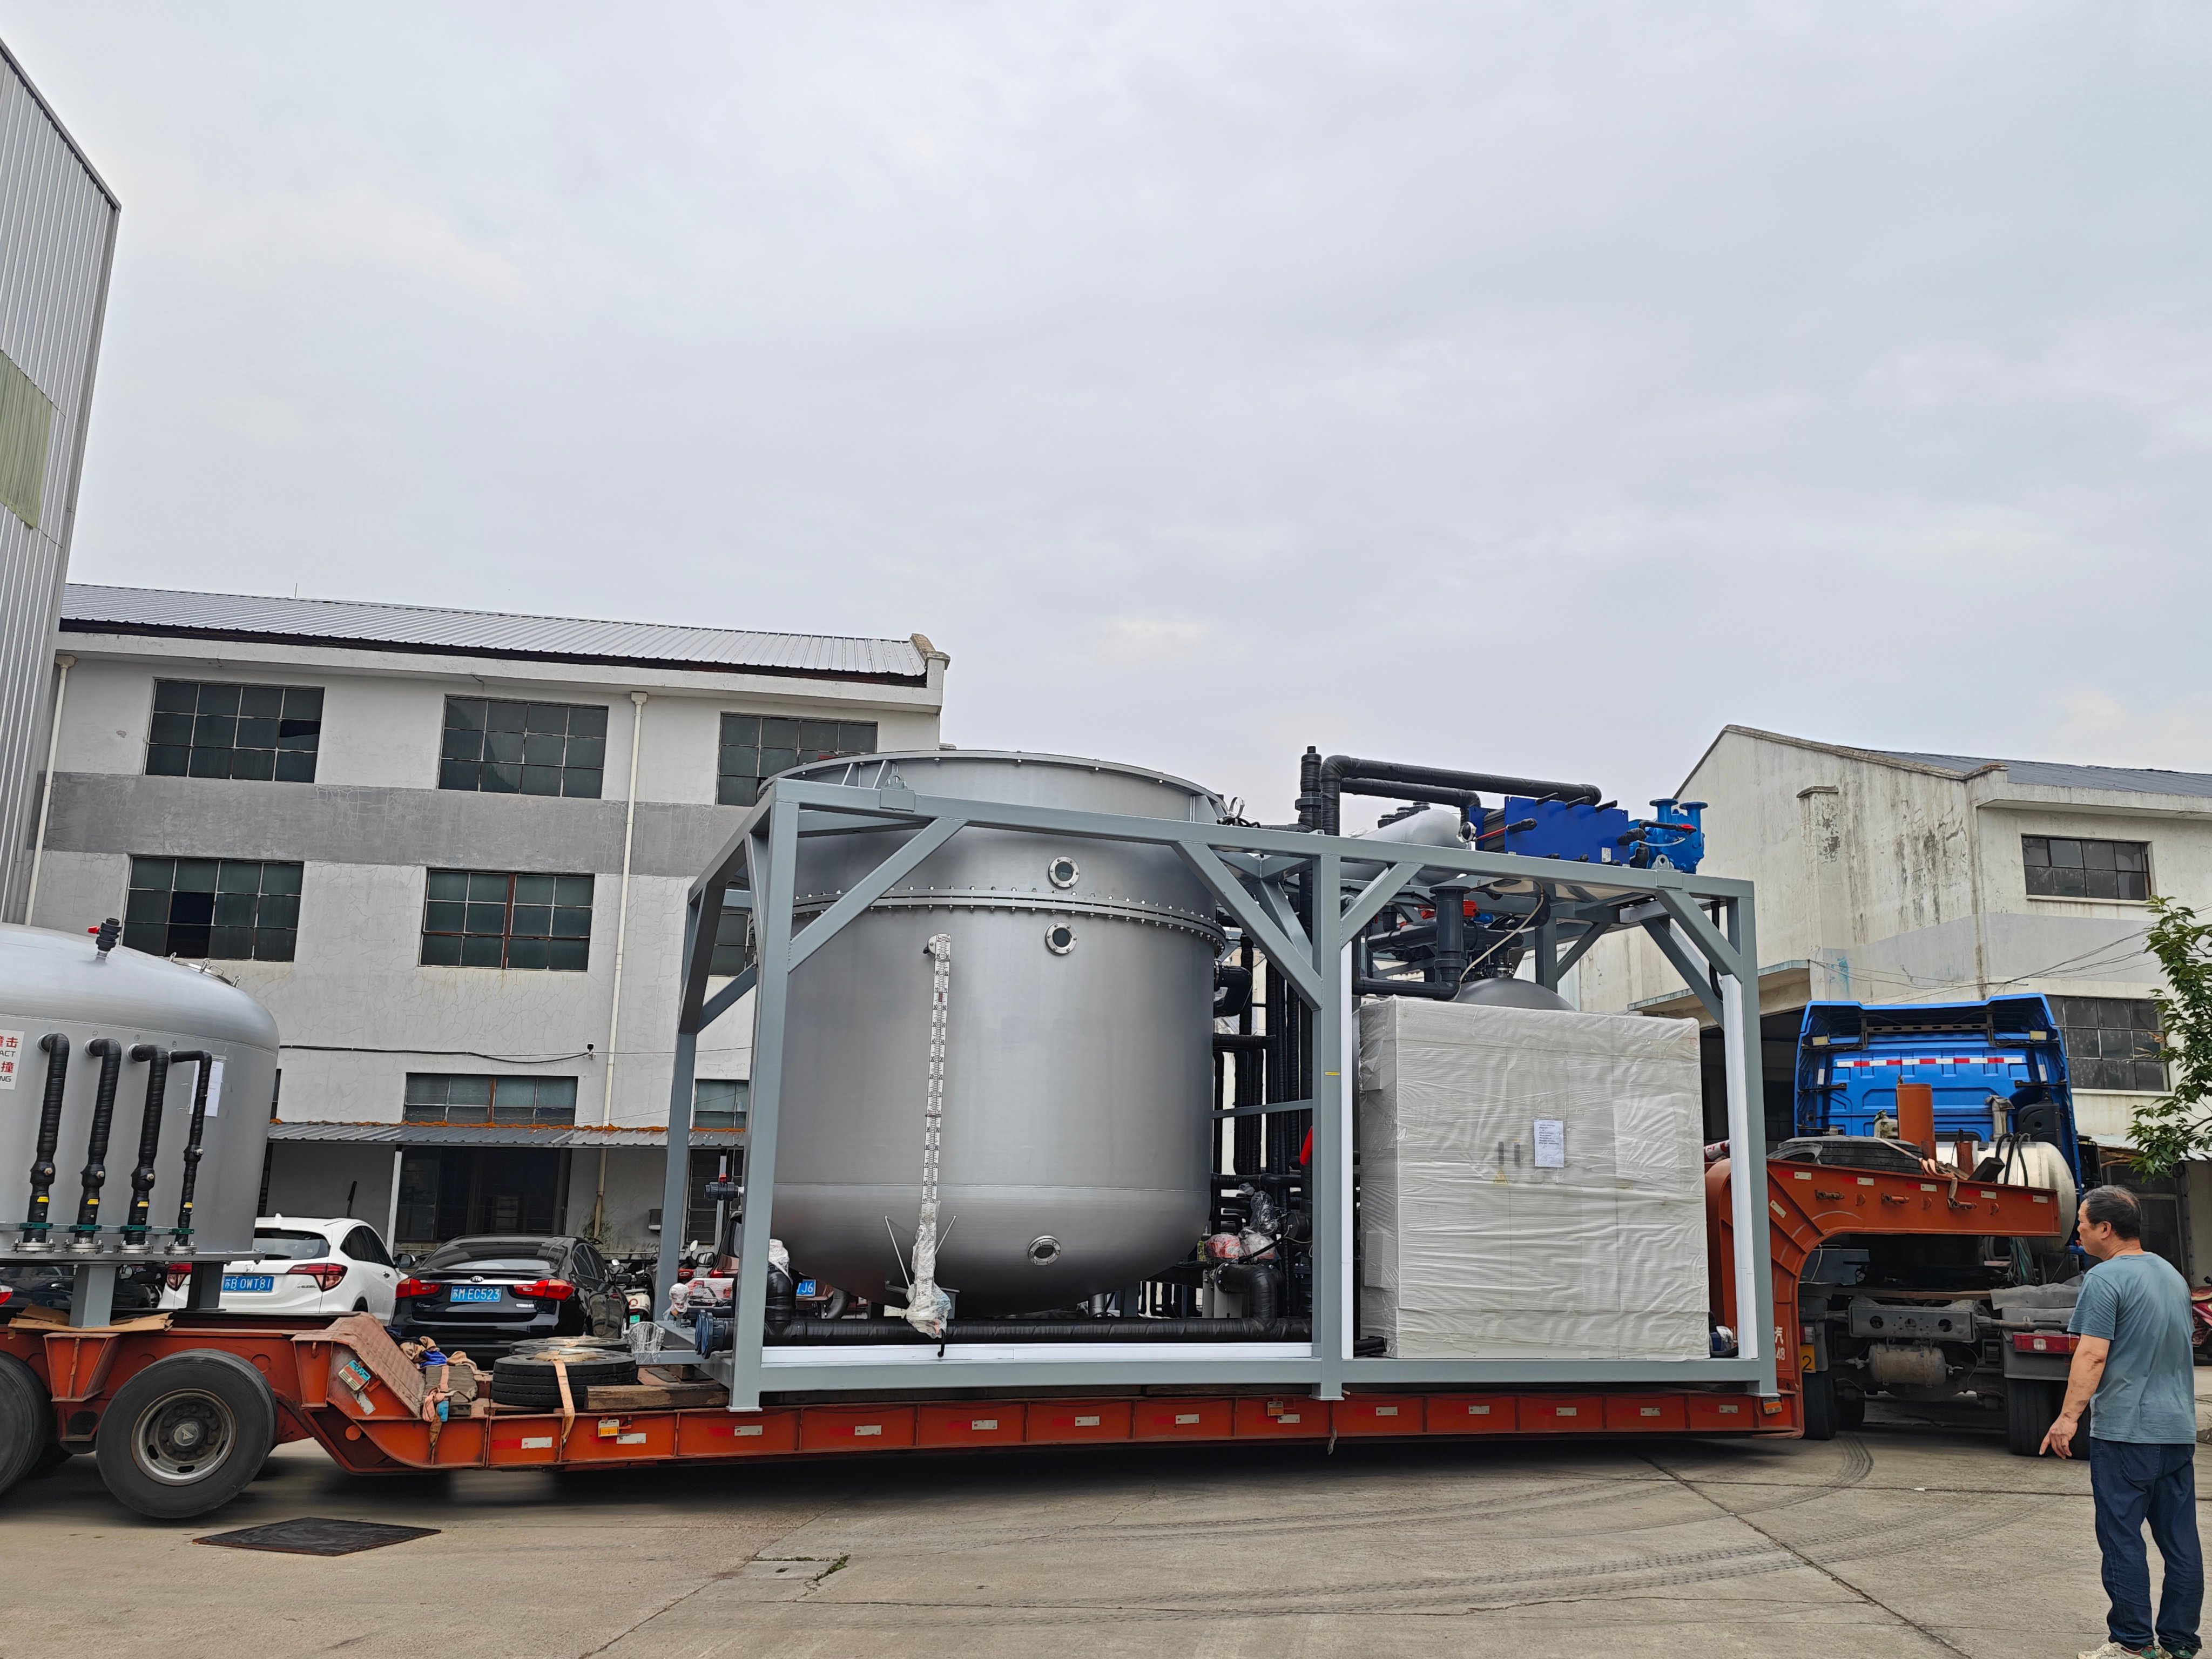
An industrial liquid concentrator is a specialized piece of equipment designed to reduce the volume of liquid substances by removing water or other solvents through various concentration methods. This sophisticated machinery plays a critical role in manufacturing, chemical processing, food production, and waste management industries. The industrial liquid concentrator operates by separating unwanted liquids from valuable concentrated materials, making it an essential tool for businesses seeking to optimize their production efficiency. The primary function of an industrial liquid concentrator involves processing large volumes of dilute solutions and transforming them into highly concentrated forms. This equipment utilizes advanced technological features including evaporation systems, membrane filtration, and thermal concentration technology to achieve precise results. Modern industrial liquid concentrator systems incorporate automated controls, real-time monitoring, and energy-efficient designs that minimize operational costs while maximizing output quality. Applications for an industrial liquid concentrator span numerous industries. In pharmaceutical manufacturing, this equipment concentrates active ingredients from solutions. Food and beverage producers use industrial liquid concentrator technology to create juice concentrates, flavor extracts, and syrup products. Chemical manufacturers rely on concentration processes to produce specialized compounds and derivatives. Environmental management facilities employ industrial liquid concentrator systems to treat wastewater and recover valuable materials from liquid waste streams. The technological sophistication of modern industrial liquid concentrator equipment enables precise control over concentration levels, temperature management, and processing duration. These machines deliver consistent results while maintaining product quality and integrity throughout the concentration process. Investment in an industrial liquid concentrator represents a strategic decision for companies aiming to enhance productivity, reduce material waste, and improve profitability across their operations.

Popular Products

An industrial liquid concentrator delivers substantial operational benefits that directly impact your business bottom line and production capabilities. This equipment works efficiently to reduce processing time, allowing your facility to handle larger volumes of material without expanding floor space or workforce. The straightforward operation of an industrial liquid concentrator means your team requires minimal specialized training to achieve optimal results consistently. From a practical perspective, implementing an industrial liquid concentrator significantly reduces material waste by recovering valuable concentrated products that would otherwise be discarded. Your company saves money on waste disposal costs while simultaneously generating more saleable product from each batch processed. The energy-efficient design of modern industrial liquid concentrator units lowers utility expenses, contributing to improved profit margins across your production operations. An industrial liquid concentrator provides exceptional versatility, accommodating various liquid types and concentration requirements across different applications. Whether you're processing chemical solutions, food ingredients, or pharmaceutical compounds, this equipment adapts to your specific needs without requiring complete system redesign. The durable construction ensures your industrial liquid concentrator investment delivers reliable performance year after year with minimal maintenance demands. Customers benefit from the improved product quality that results from precise concentration control. An industrial liquid concentrator maintains optimal processing conditions, preventing product degradation while achieving exact concentration specifications required by your market. This consistency strengthens your reputation with clients who depend on uniform quality standards. The rapid return on investment makes an industrial liquid concentrator an intelligent choice for forward-thinking companies. Reduced material costs, decreased processing time, and lower operational expenses combine to create substantial financial advantages. Your decision to implement an industrial liquid concentrator positions your business for sustainable growth and competitive strength in demanding markets.

Latest News

Top 5 Low Temperature Heat Pump Evaporator Applications

24

Jul

Top 5 Low Temperature Heat Pump Evaporator Applications

The low temperature heat pump evaporator represents a critical advancement in industrial thermal management and energy efficiency. This innovative component enables heat pump systems to operate effectively at reduced temperatures, making it indispens...
View More
Common Challenges in Industrial Water Treatment Solved

02

Sep

Common Challenges in Industrial Water Treatment Solved

Manufacturing facilities, chemical plants, and processing operations face mounting pressure to manage wastewater efficiently while meeting regulatory standards. Industrial water treatment remains one of the most critical operational functions across ...
View More
Top 5 Evaporator System Design Features for Industry

24

Jul

Top 5 Evaporator System Design Features for Industry

Selecting the right evaporator system design is critical for industrial operations managing wastewater treatment, chemical processing, and liquid concentration challenges. An effective evaporator system design determines not only operational efficien...
View More
Evaporator System Maintenance: Tips for Longevity

24

Jul

Evaporator System Maintenance: Tips for Longevity

Evaporator system maintenance is critical to ensuring your industrial cooling and waste-water treatment equipment operates reliably and efficiently over the long term. Whether your facility relies on evaporator systems for refrigeration, heat exchang...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

industrial liquid concentrator

Advanced Concentration Technology for Superior Results

Advanced Concentration Technology for Superior Results

Modern industrial liquid concentrator systems incorporate cutting-edge evaporation and separation technologies that deliver exceptional concentration levels with minimal product loss. The industrial liquid concentrator employs multi-stage processing that systematically removes unwanted liquids while preserving valuable components. Advanced sensors within the industrial liquid concentrator continuously monitor processing conditions, automatically adjusting parameters to maintain perfect concentration ratios. This technological superiority ensures your facility achieves results that consistently exceed industry standards. The precision engineering of an industrial liquid concentrator means you can concentrate materials to exact specifications, meeting even the most demanding client requirements. Investing in an industrial liquid concentrator with advanced technology protects your competitive advantage by enabling you to produce superior quality concentrated products that command premium market prices.
Energy-Efficient Operations Reducing Operating Costs

Energy-Efficient Operations Reducing Operating Costs

The industrial liquid concentrator features intelligent energy management systems that substantially decrease utility consumption compared to traditional processing methods. Optimized heat recovery mechanisms within your industrial liquid concentrator capture and recycle thermal energy, minimizing wasted resources throughout the concentration cycle. The streamlined design of an industrial liquid concentrator reduces electricity demands while maintaining maximum processing capacity and throughput. Operating an industrial liquid concentrator with modern energy-efficient technology directly reduces your monthly utility bills, improving overall profitability. The thermal insulation and automated controls integrated into an industrial liquid concentrator prevent energy waste during idle periods and between processing cycles. By choosing an industrial liquid concentrator designed for efficiency, your company makes an environmentally responsible decision while simultaneously achieving significant cost savings that positively impact your financial performance.
Reliable Performance with Minimal Maintenance Requirements

Reliable Performance with Minimal Maintenance Requirements

An industrial liquid concentrator delivers dependable, consistent operation day after day with straightforward maintenance protocols that don't disrupt your production schedule. The robust construction of an industrial liquid concentrator withstands demanding industrial environments while maintaining peak performance throughout its operational lifespan. Durable materials used in an industrial liquid concentrator construction resist corrosion and degradation from harsh chemicals and processing conditions. The industrial liquid concentrator design minimizes moving parts and complex mechanisms that frequently require service, reducing downtime and maintenance expenses. Manufacturer support and readily available replacement components ensure your industrial liquid concentrator continues operating smoothly whenever issues arise. The reliability of an industrial liquid concentrator means your facility maintains consistent production output, fulfilling customer orders on schedule without unexpected interruptions. This dependability makes an industrial liquid concentrator an essential asset for businesses where production reliability directly impacts revenue and customer relationships.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000