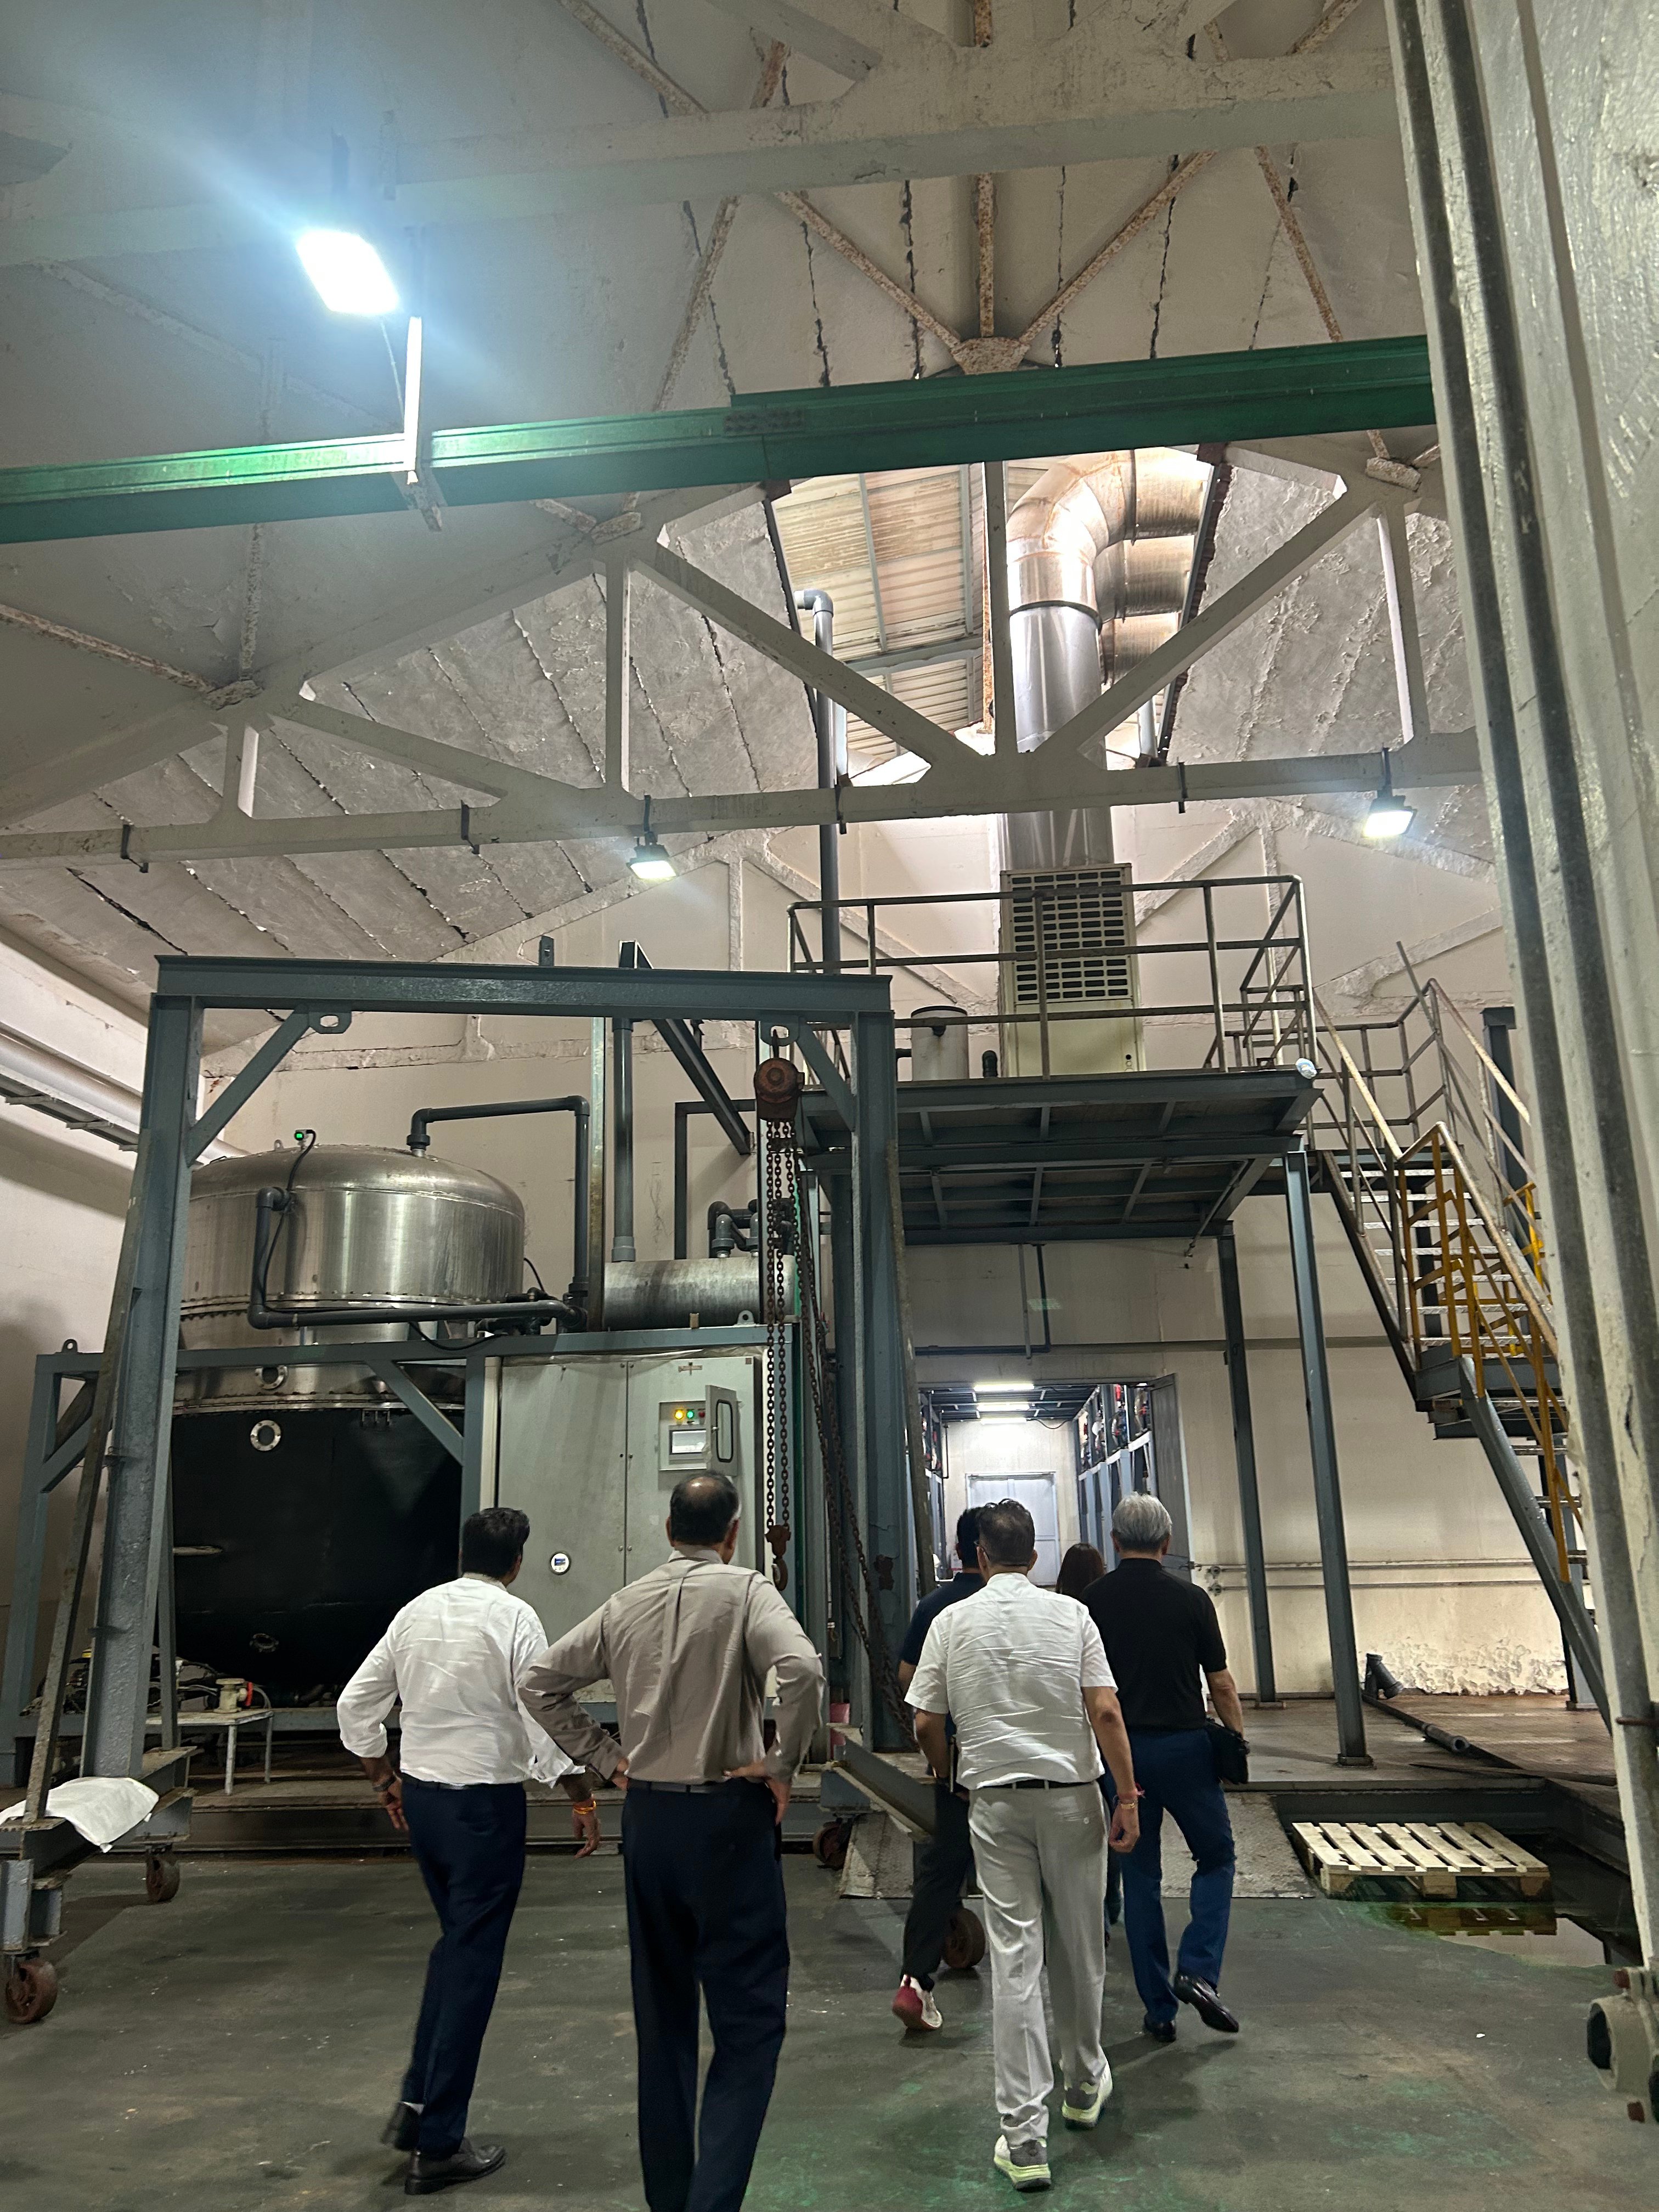
Customized Crystallizer System Solutions

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

customized crystallizer system

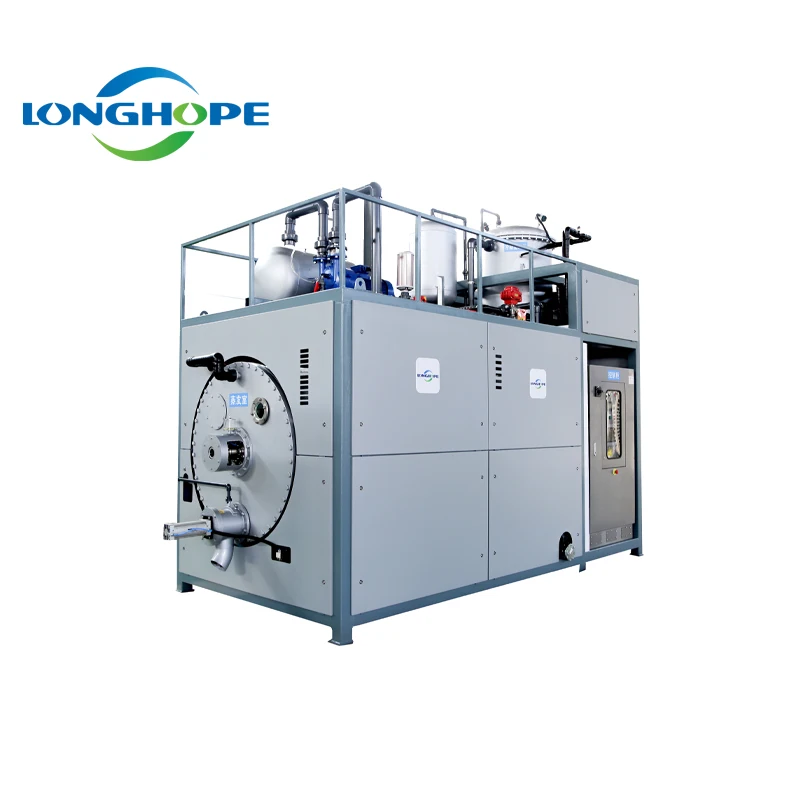
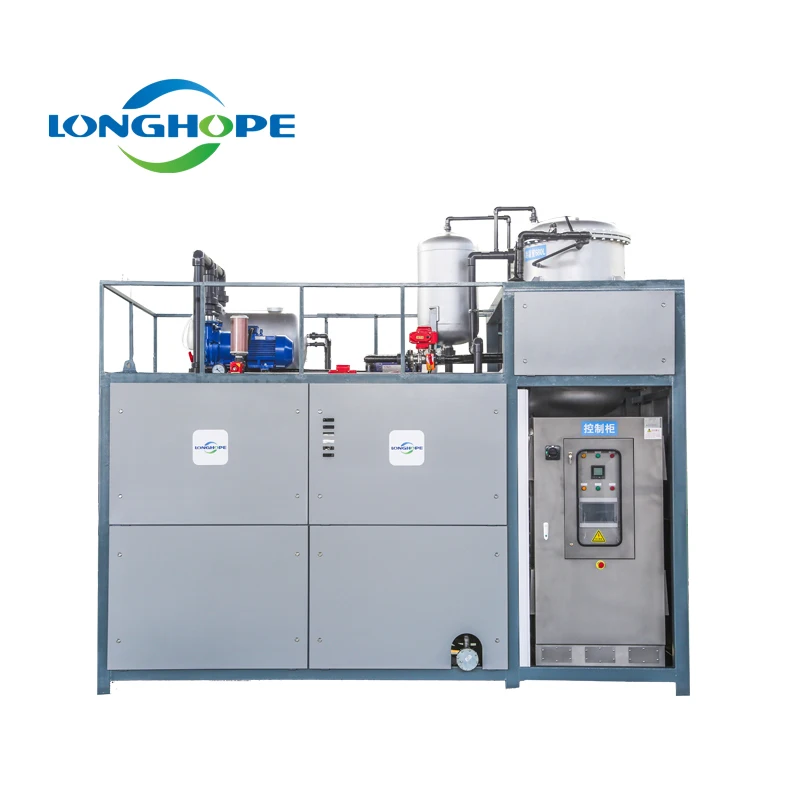
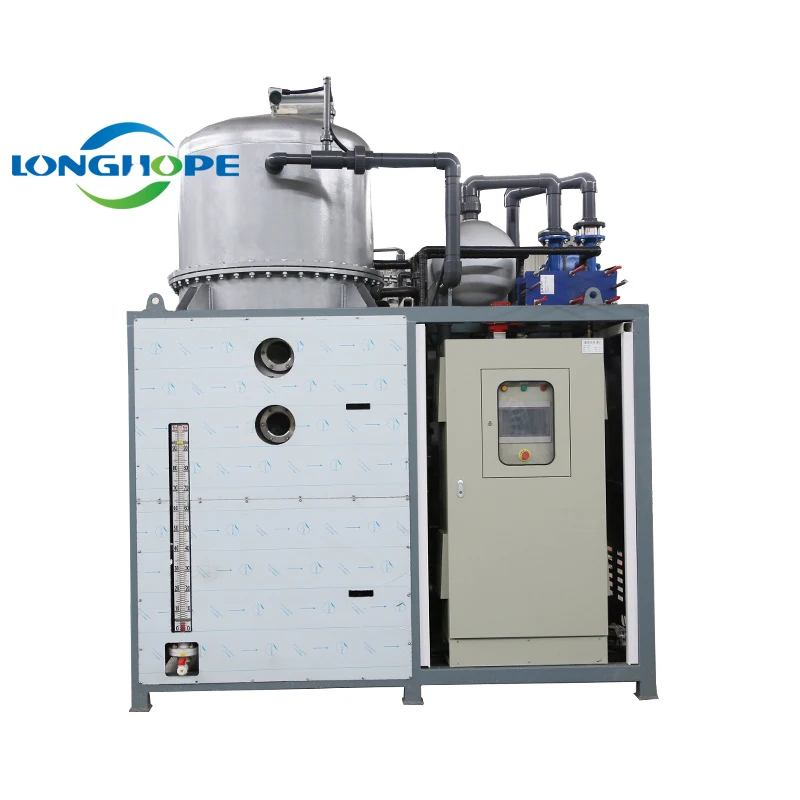
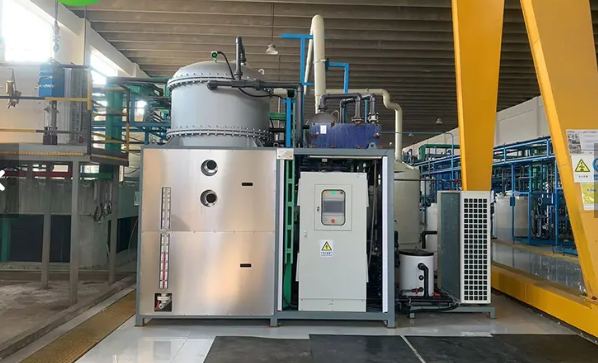
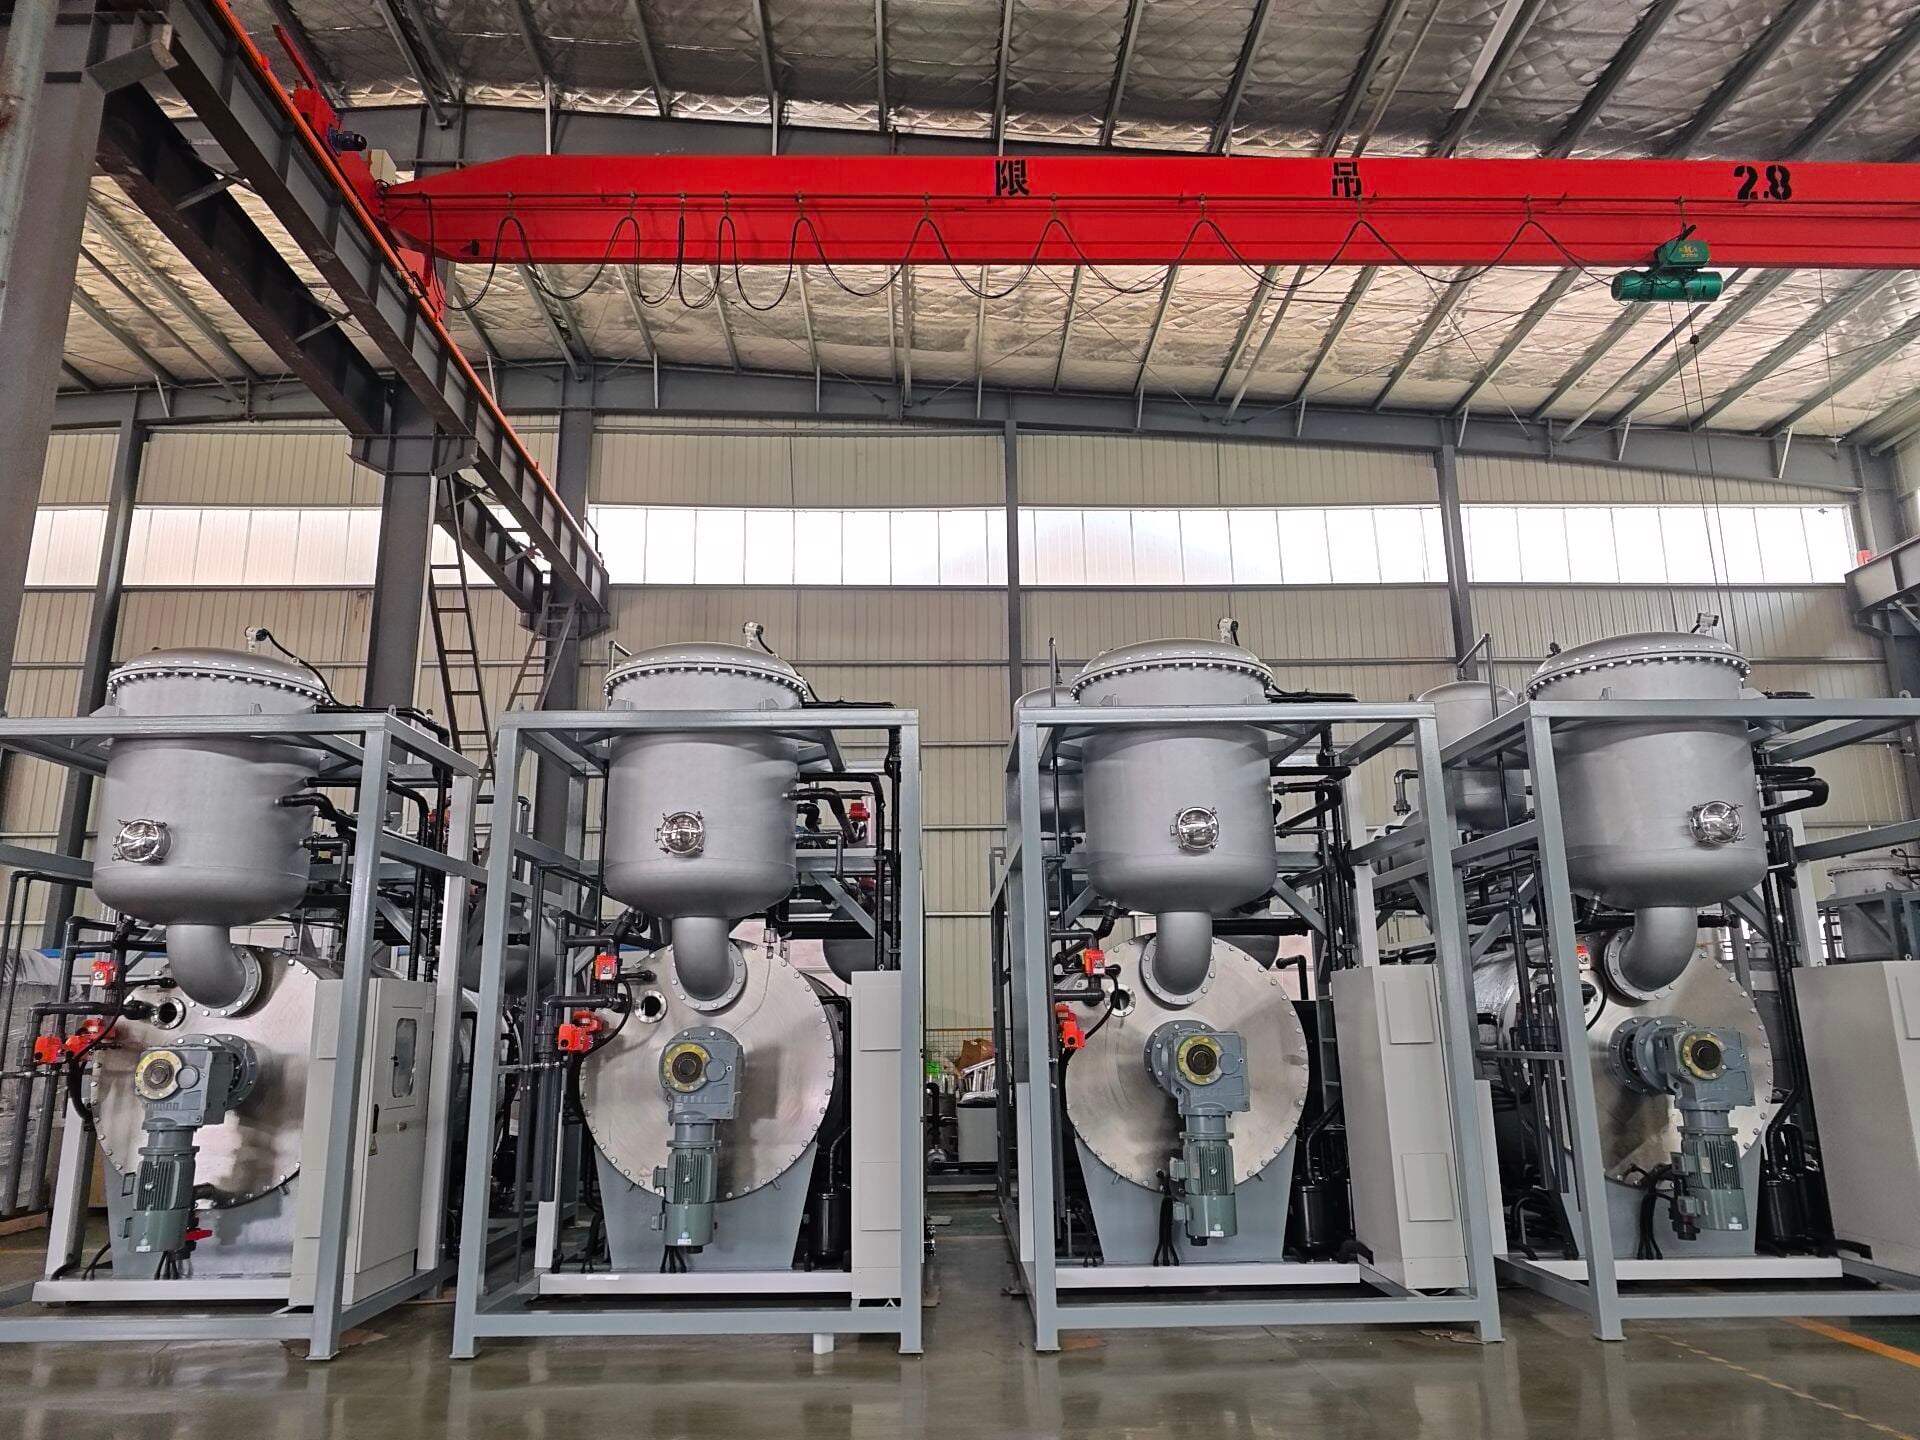
A customized crystallizer system represents an advanced industrial solution designed to meet specific crystallization requirements across diverse manufacturing environments. This specialized equipment facilitates the transformation of dissolved substances into solid crystal forms through precisely controlled conditions. The customized crystallizer system operates by managing temperature, pressure, and agitation parameters to achieve optimal crystal growth and purity levels. The technological features of a customized crystallizer system include automated temperature regulation, sophisticated monitoring sensors, and adaptable vessel configurations. These components work synergistically to produce consistent, high-quality crystals while minimizing energy consumption. The system employs advanced control algorithms that respond in real-time to changing conditions, ensuring repeatable results across production cycles. Applications for a customized crystallizer system span pharmaceutical manufacturing, chemical processing, food production, and specialty materials development. Industries requiring precise crystal size distribution and composition rely heavily on this technology. The customized crystallizer system addresses unique challenges posed by different chemical properties, crystallization rates, and product specifications. Whether processing inorganic salts, organic compounds, or complex biochemicals, this equipment delivers reliable performance. Organizations implementing a customized crystallizer system gain competitive advantages through improved product quality, reduced waste, and enhanced operational efficiency. The versatility of a customized crystallizer system makes it invaluable for facilities managing multiple product lines with varying crystallization demands.

New Product Recommendations

Investing in a customized crystallizer system delivers substantial operational and financial benefits for manufacturing organizations. The primary advantage centers on achieving consistent product quality while reducing production costs through optimized resource utilization. A customized crystallizer system adapts to your specific materials and production volumes, eliminating inefficiencies associated with generic equipment. Operational benefits become immediately apparent through enhanced control mechanisms. Your facility gains the ability to fine-tune crystallization parameters, resulting in superior crystal uniformity and reduced impurities. A customized crystallizer system minimizes equipment downtime by incorporating maintenance-friendly designs tailored to your workflow requirements. The system's flexibility allows seamless transitions between different products without extensive recalibration, streamlining your production schedule. Financial advantages emerge through improved yield rates and reduced material waste. By implementing a customized crystallizer system, manufacturers recover higher percentages of valuable crystalline products, directly impacting profitability. Energy efficiency represents another significant benefit, as the system operates at optimal settings for your specific applications rather than compromising with one-size-fits-all solutions. A customized crystallizer system proves particularly valuable for facilities processing temperature-sensitive materials or requiring stringent purity standards. The equipment provides exceptional performance in pharmaceutical contexts where regulatory compliance demands precise documentation and repeatable results. Small to mid-sized producers benefit substantially from a customized crystallizer system's scalability and cost-effectiveness compared to enterprise-level alternatives. Decision-useful context shows that organizations adopting a customized crystallizer system typically achieve return on investment within eighteen to thirty-six months through improved operational metrics and market competitiveness. Your facility becomes positioned for growth without requiring complete equipment replacement as demands evolve.

Tips And Tricks

Top 5 Low Temperature Heat Pump Evaporator Applications

24

Jul

Top 5 Low Temperature Heat Pump Evaporator Applications

The low temperature heat pump evaporator represents a critical advancement in industrial thermal management and energy efficiency. This innovative component enables heat pump systems to operate effectively at reduced temperatures, making it indispens...
View More
Benefits of Low Temperature Heat Pump Evaporator in Industry

24

Jul

Benefits of Low Temperature Heat Pump Evaporator in Industry

Industrial facilities worldwide face mounting pressure to reduce operating costs while maintaining production quality and environmental compliance. The low temperature heat pump evaporator has emerged as a transformative solution that addresses these...
View More
Industrial Water Treatment Technologies for 2026

02

Sep

Industrial Water Treatment Technologies for 2026

Industrial water treatment remains one of the most critical operational priorities across manufacturing, chemical processing, food production, and energy sectors. As facilities face increasingly stringent environmental regulations, rising operational...
View More
Common Challenges in Industrial Water Treatment Solved

02

Sep

Common Challenges in Industrial Water Treatment Solved

Manufacturing facilities, chemical plants, and processing operations face mounting pressure to manage wastewater efficiently while meeting regulatory standards. Industrial water treatment remains one of the most critical operational functions across ...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

customized crystallizer system

Precision Temperature Control Technology

Precision Temperature Control Technology

The customized crystallizer system incorporates sophisticated temperature management capabilities that maintain exact conditions throughout crystallization cycles. This precision proves essential for materials requiring specific thermal profiles to achieve desired crystal structures. The advanced heating and cooling mechanisms integrated into a customized crystallizer system respond instantaneously to detected variations, preventing unwanted crystallization patterns or product degradation. Your production team gains complete visibility into temperature trends through real-time dashboards, enabling proactive adjustments before quality issues arise. The customized crystallizer system's thermal precision directly translates to superior crystal formation, consistent particle size distribution, and reduced batch failures. This technological advantage becomes particularly valuable in pharmaceutical and specialty chemical manufacturing where crystalline form directly impacts bioavailability or product performance. Organizations leveraging the precise temperature capabilities of a customized crystallizer system achieve quality metrics that exceed industry standards while maintaining production timelines and cost targets.
Scalable Design for Growing Operations

Scalable Design for Growing Operations

A customized crystallizer system accommodates your facility's expansion plans through modular, scalable architecture that grows with your production demands. Unlike fixed equipment, this system adapts to increased throughput without requiring complete replacement or extensive facility modifications. The customized crystallizer system's flexible vessel sizes and processing capacities allow manufacturers to serve expanding markets efficiently. Your investment remains protected as business needs evolve, making a customized crystallizer system a strategic long-term asset. The adaptable nature of this equipment enables small producers to compete with larger manufacturers while maintaining personalized service and quality standards. A customized crystallizer system's scalability extends beyond capacity to include product diversification, allowing facilities to crystallize new materials as market opportunities emerge. This flexibility positions your organization for sustained growth without stranding existing equipment investments. Companies implementing a customized crystallizer system with scalability features report reduced capital expenditure over product lifecycles compared to traditional sequential equipment purchases.
Compliance and Quality Documentation Features

Compliance and Quality Documentation Features

The customized crystallizer system integrates comprehensive data logging and reporting capabilities that satisfy stringent regulatory requirements across industries. Automated documentation systems embedded within a customized crystallizer system track every parameter, timestamp, and variation throughout production runs, creating audit trails that exceed FDA and international standards. Regulatory agencies approving pharmaceuticals and specialty chemicals demand such meticulous records, and a customized crystallizer system delivers this functionality as a standard feature. Your quality assurance team accesses detailed analytics demonstrating process consistency and enabling rapid root cause analysis if deviations occur. The customized crystallizer system's documentation capabilities dramatically reduce compliance preparation time and audit response burden. Organizations utilizing a customized crystallizer system experience fewer regulatory challenges and faster product approvals through demonstrable process control and repeatability. This advantage extends beyond pharmaceutical applications to any industry where product traceability or quality certification proves essential. A customized crystallizer system's built-in compliance features essentially provide insurance against costly recalls or regulatory sanctions while building customer confidence through transparent quality documentation.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000