industrial crystallization system supplier
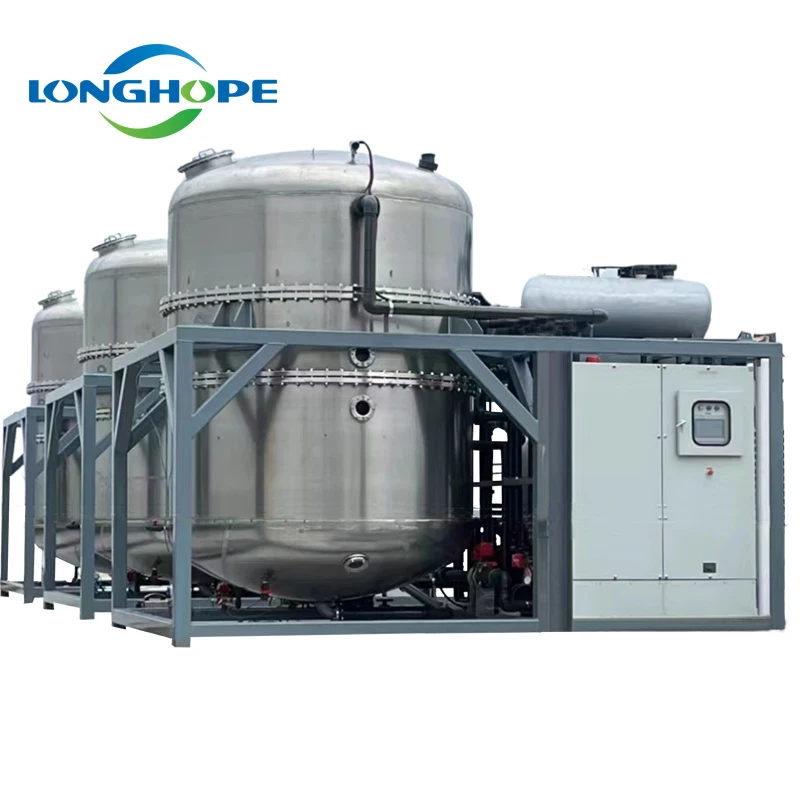
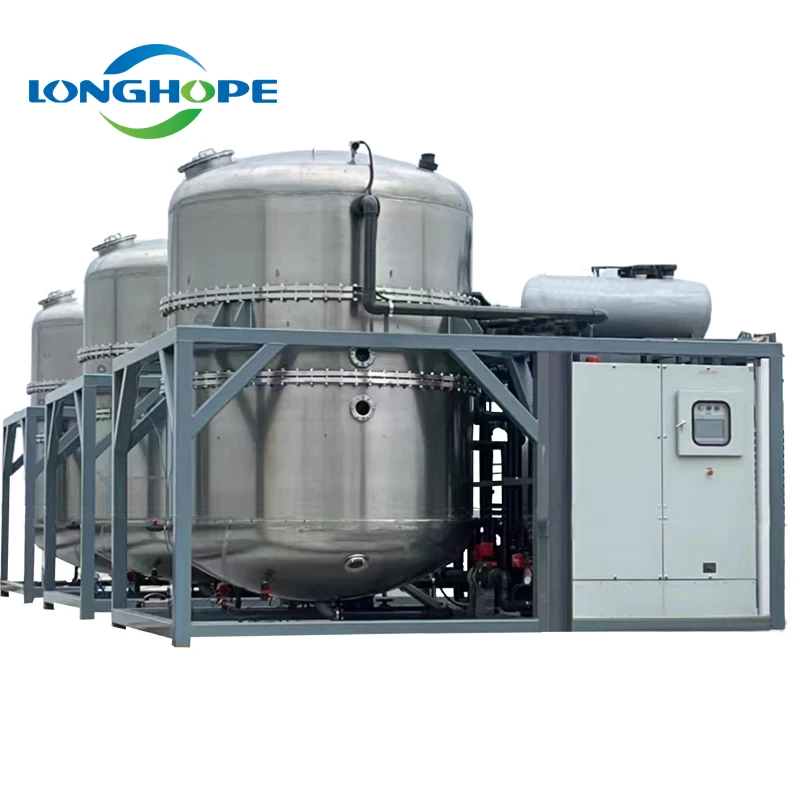
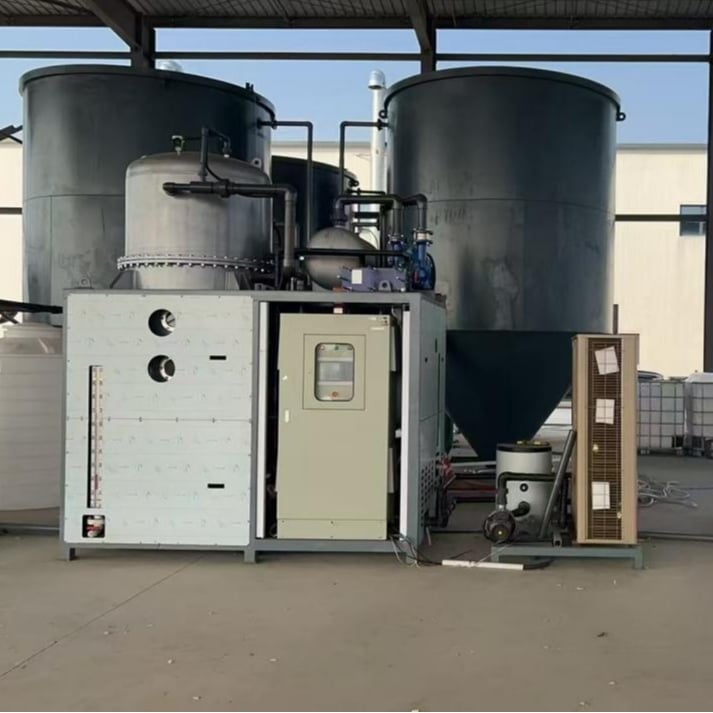
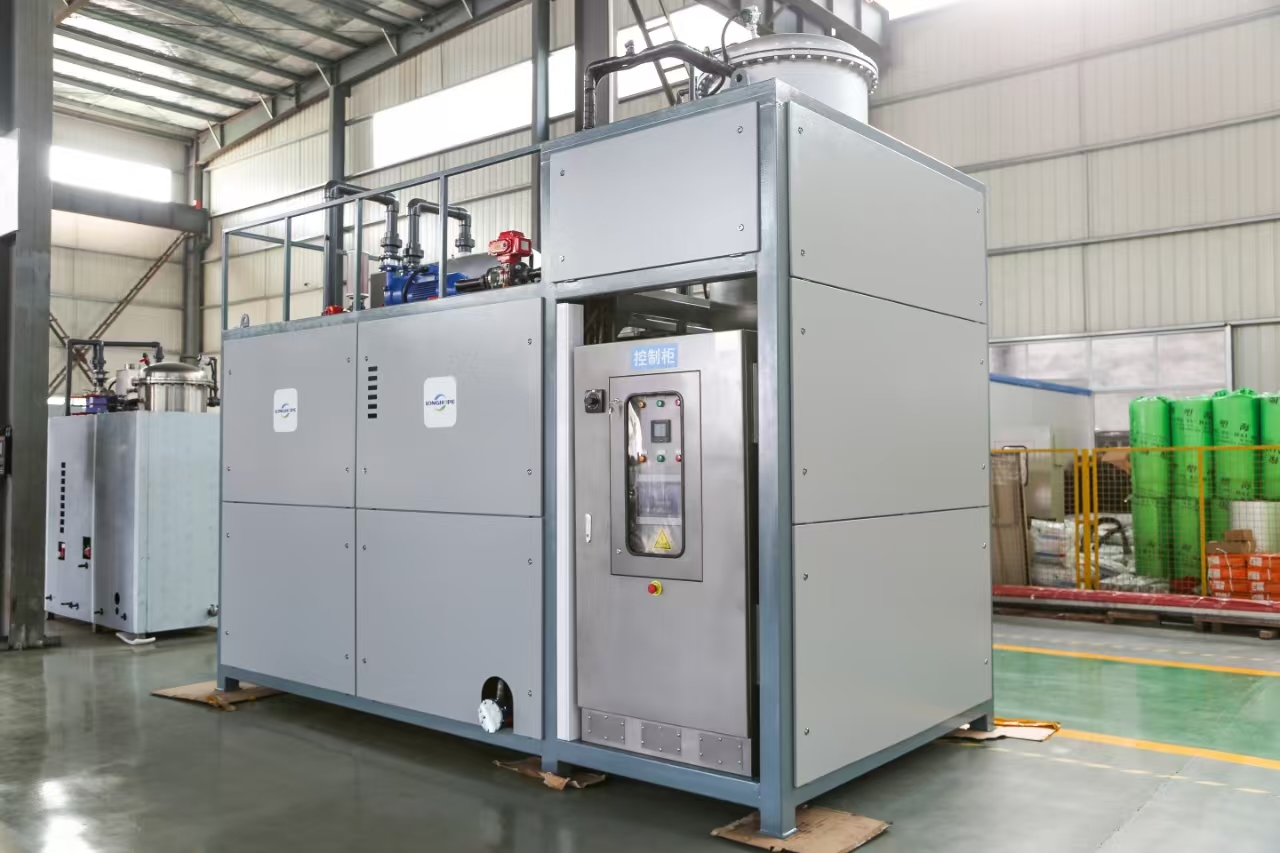
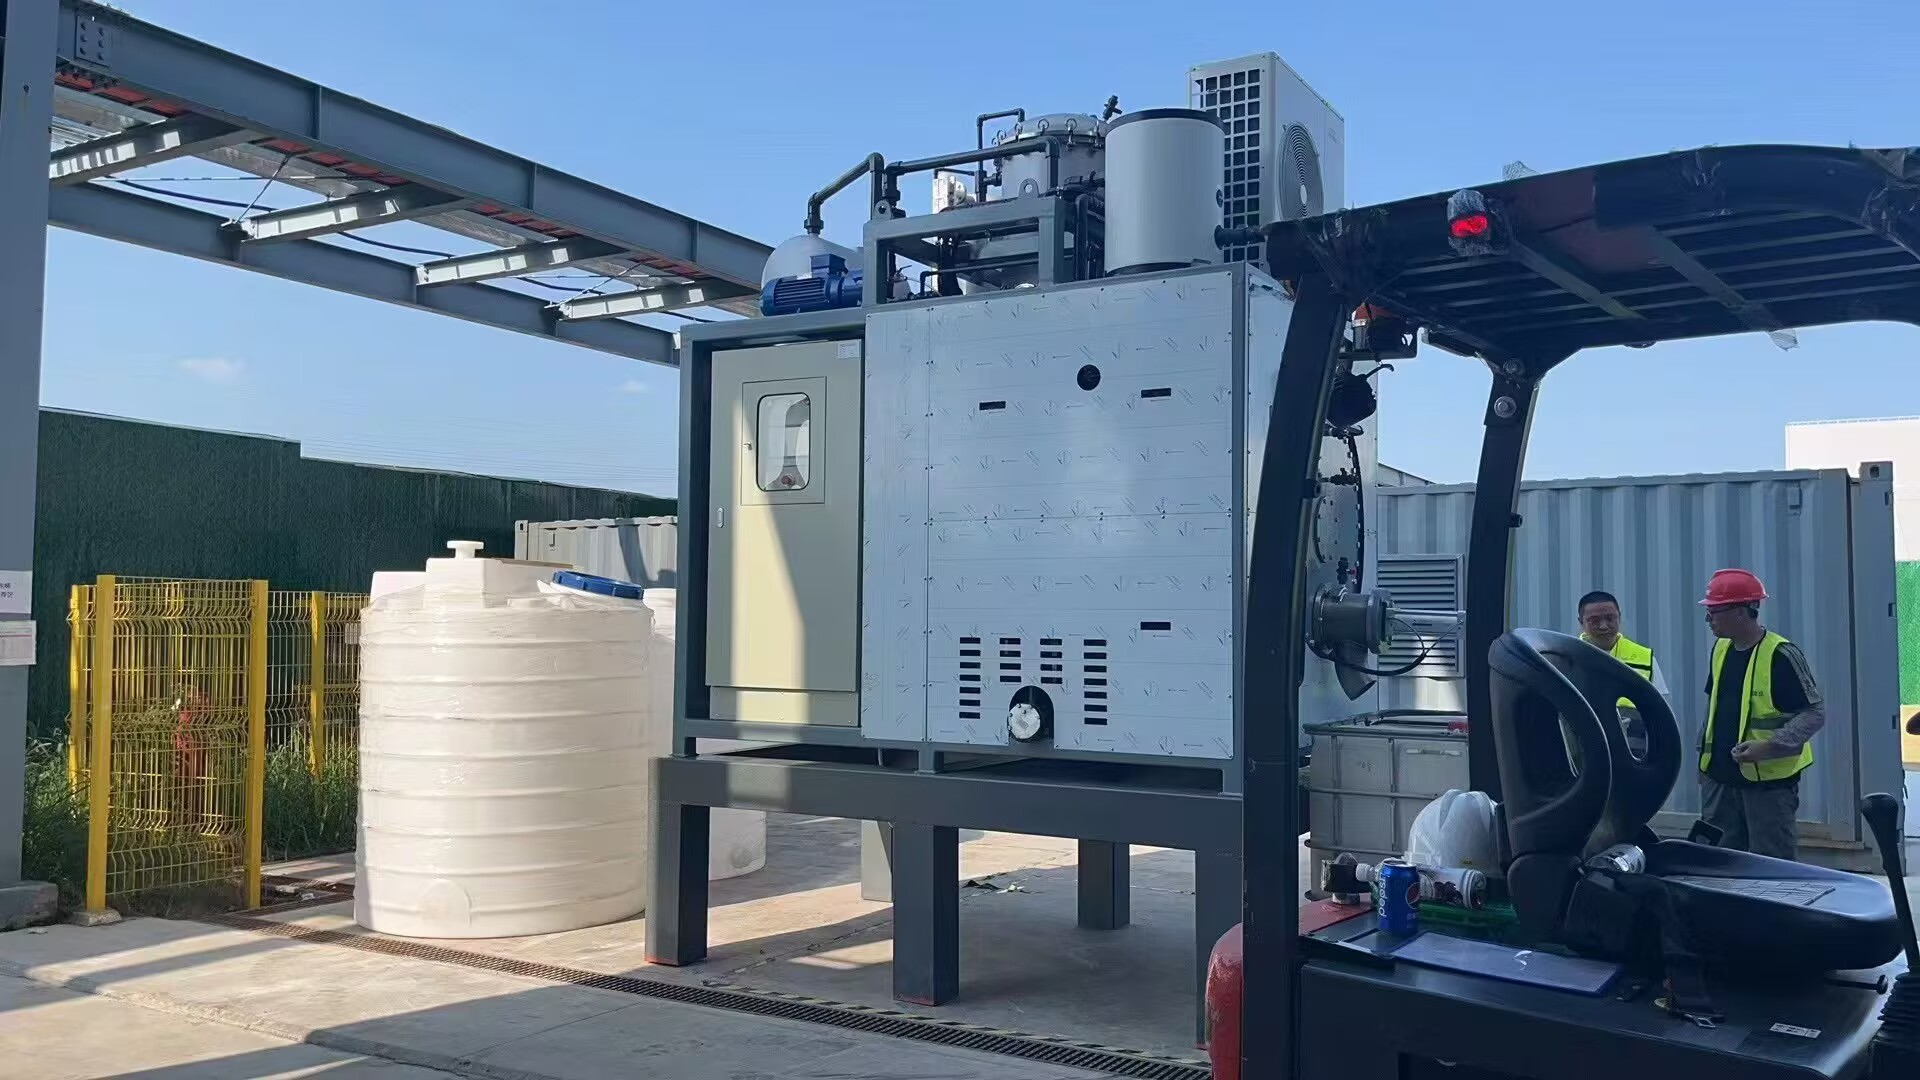
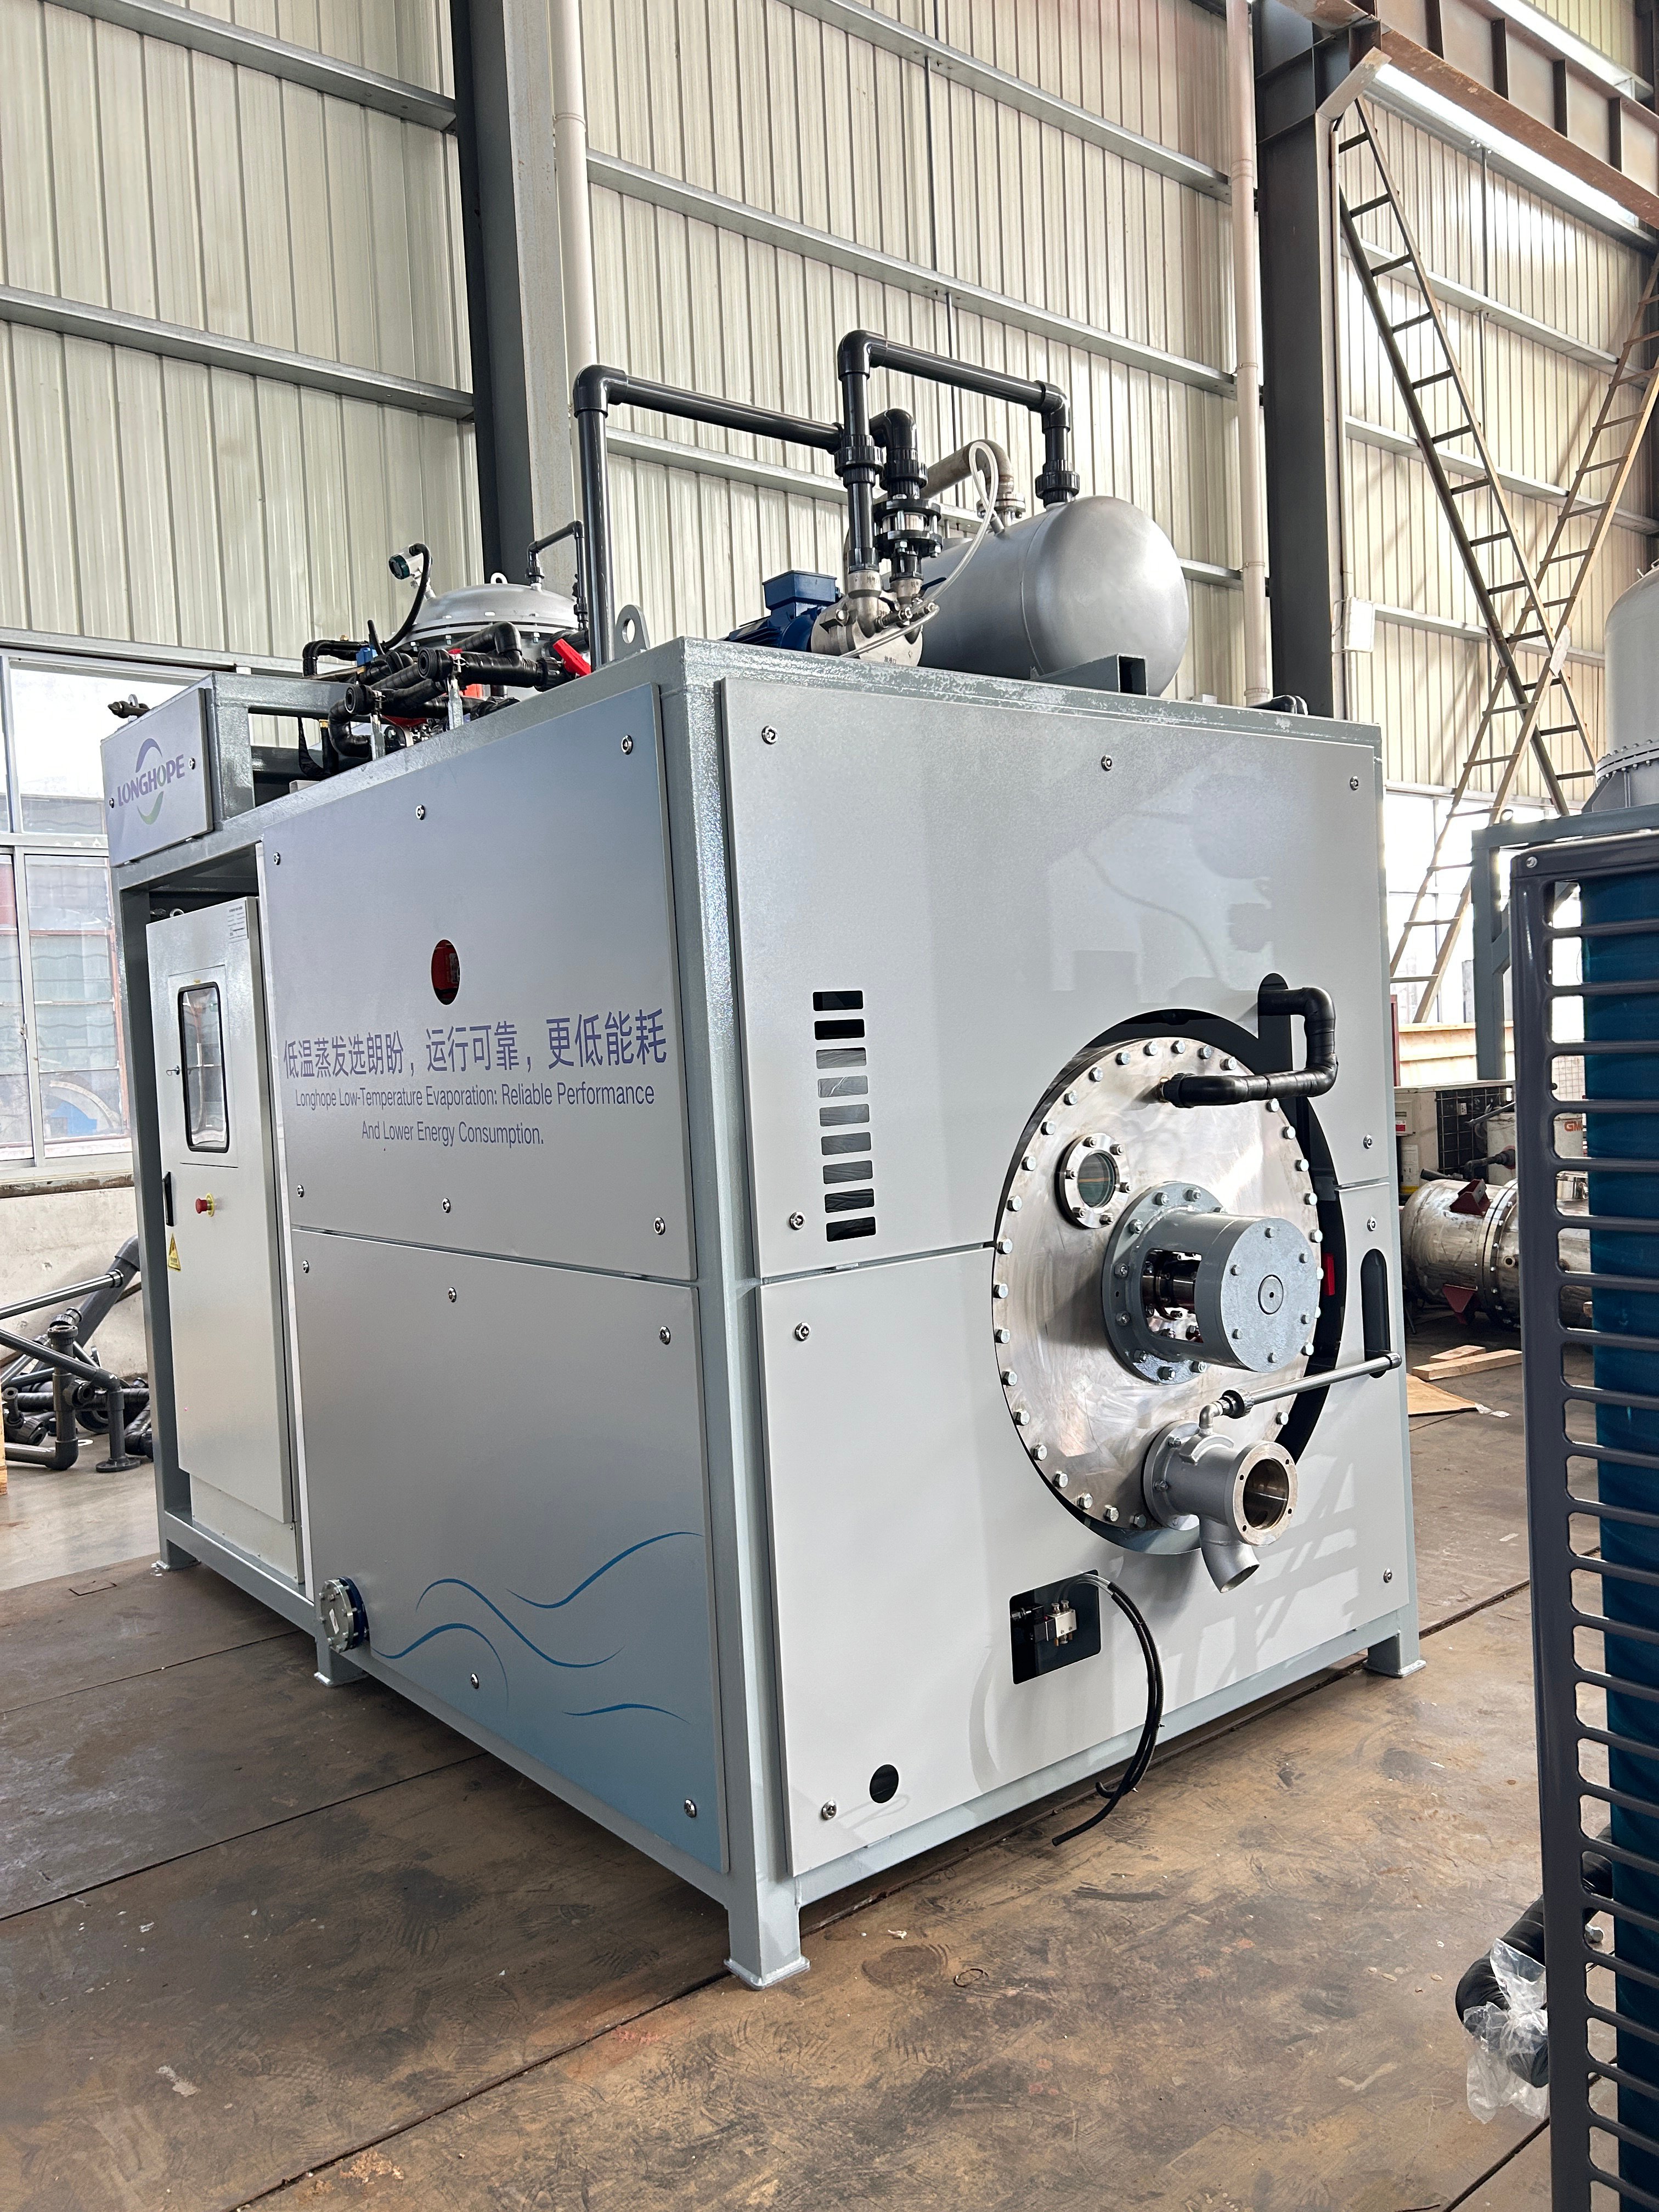
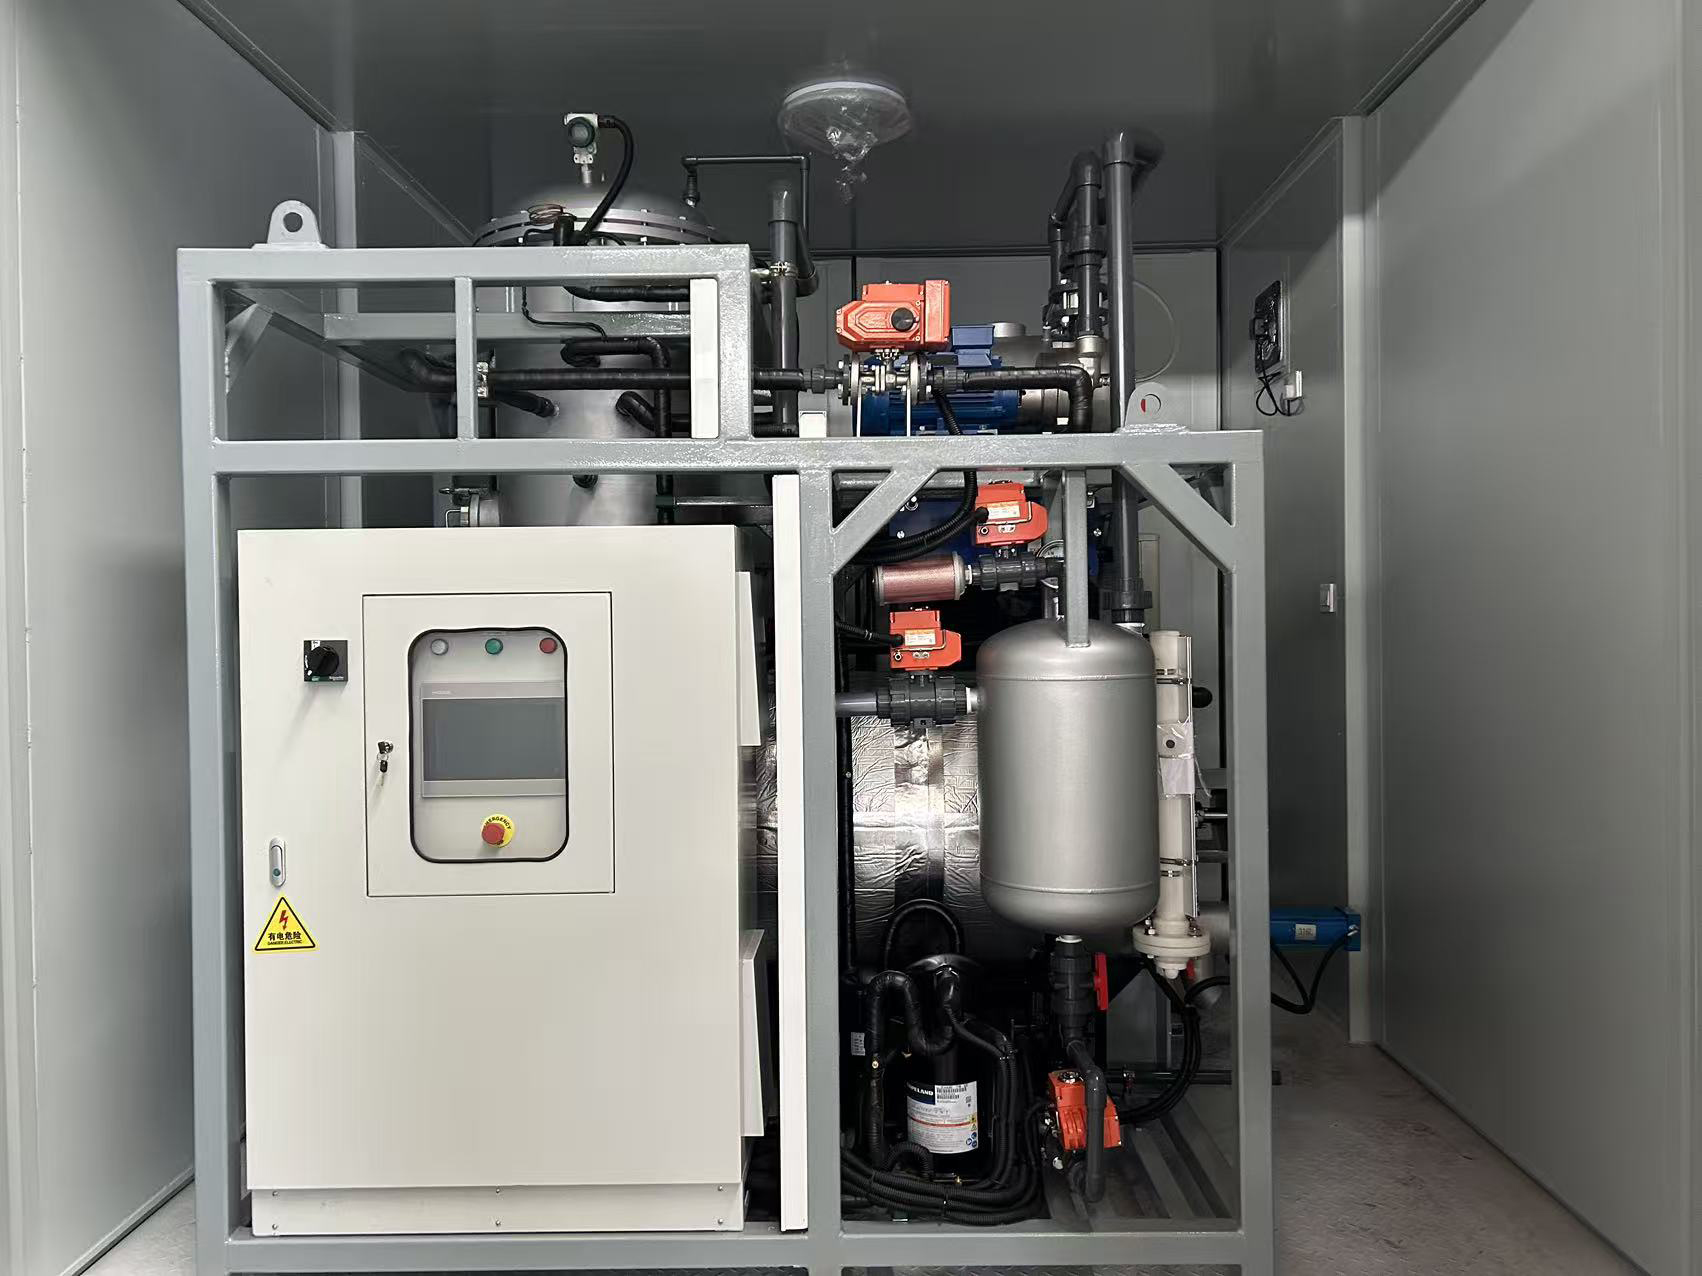
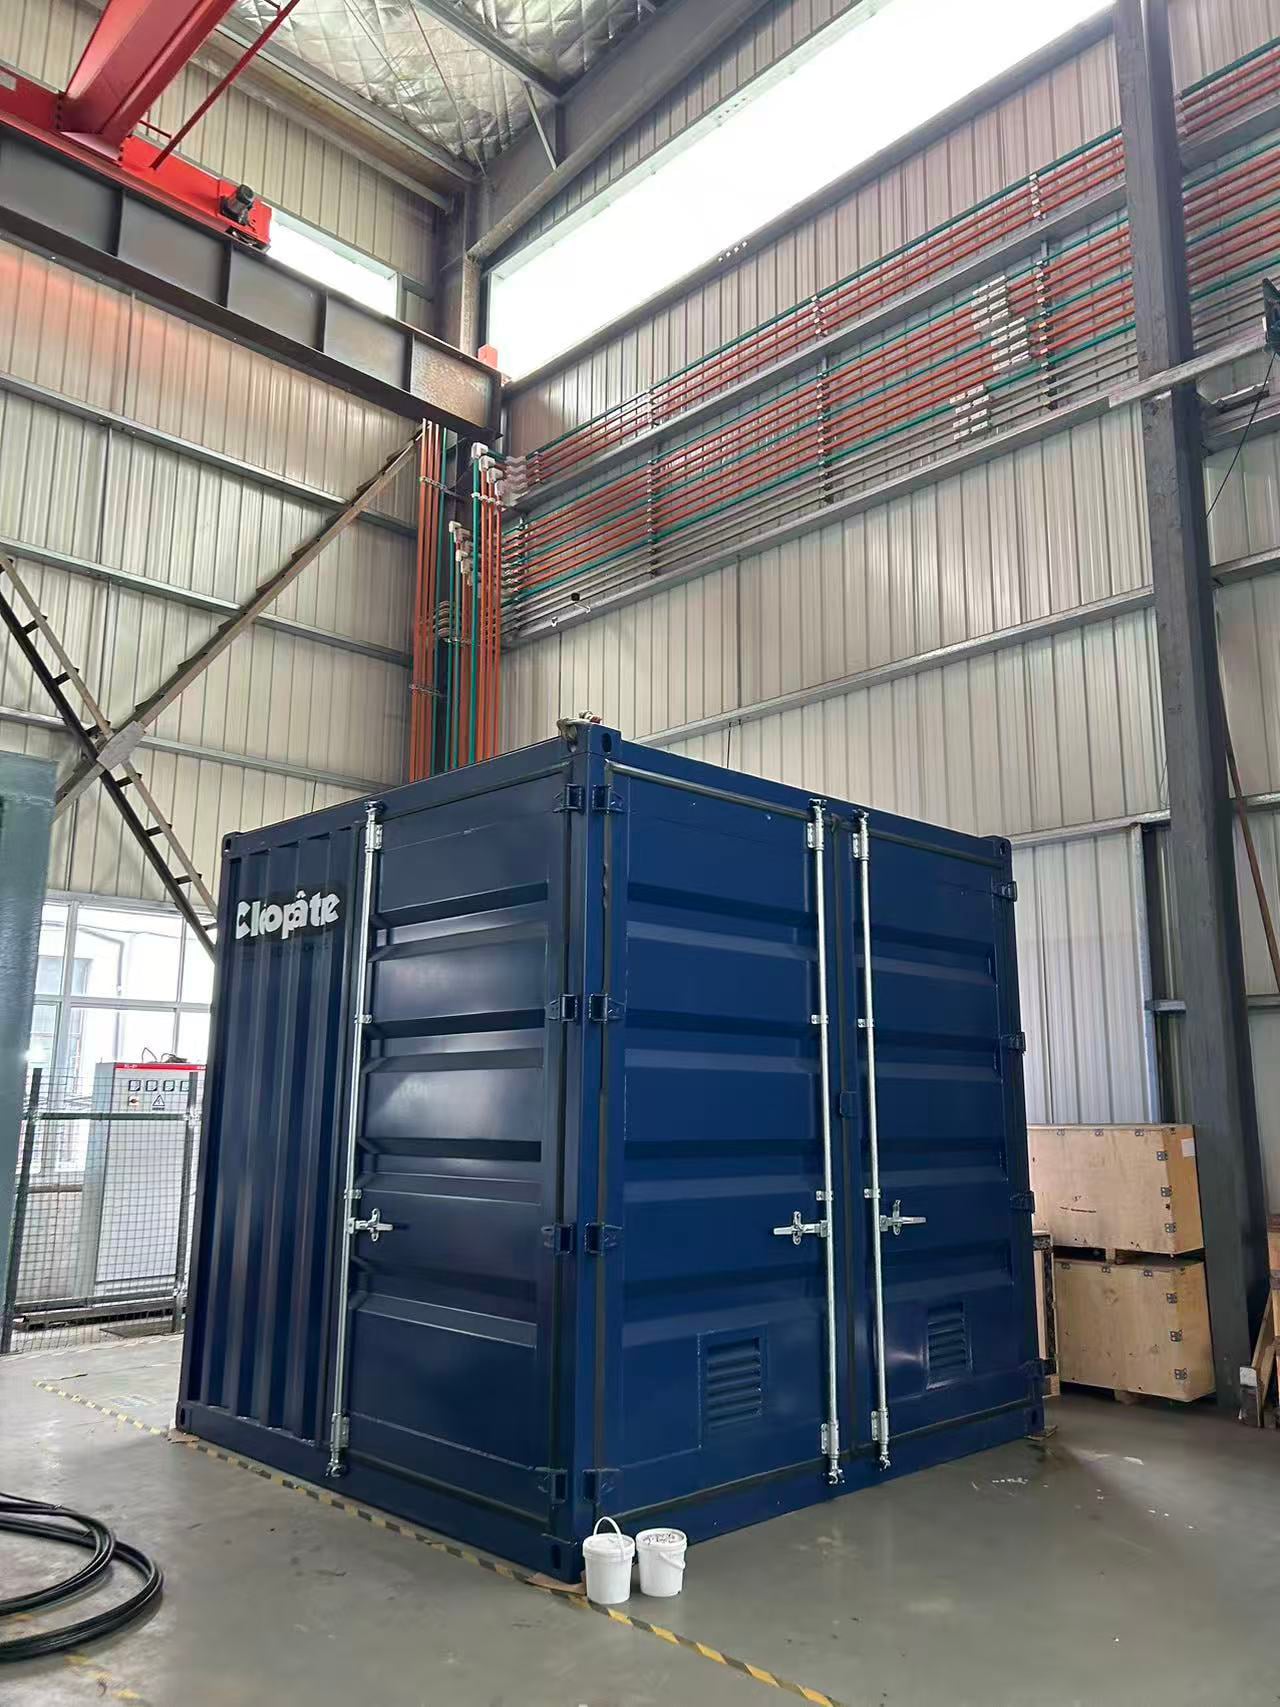
An industrial crystallization system supplier provides specialized equipment and solutions designed to facilitate the crystallization process in manufacturing environments. These systems are essential for industries requiring precise crystal formation, including pharmaceuticals, chemicals, food processing, and materials science. An industrial crystallization system supplier delivers comprehensive technology that controls temperature, pressure, and solution concentration to achieve optimal crystal growth and purity. The main functions include cooling crystallization, evaporative crystallization, and reactive crystallization, each tailored to specific production requirements. Technological features of systems offered by an industrial crystallization system supplier encompass advanced temperature control mechanisms, automated monitoring systems, and scalable designs suitable for both laboratory and large-scale production. These suppliers integrate cutting-edge sensors and data management systems that ensure consistent quality and reproducibility throughout the crystallization process. Applications span diverse sectors where crystal quality directly impacts final product performance. Pharmaceutical manufacturers rely on crystallization systems to produce active pharmaceutical ingredients with precise particle sizes and polymorphic forms. Chemical processors utilize these technologies for salt separation and purification. Food industry applications include sugar crystallization and specialty ingredient production. An industrial crystallization system supplier understands that selecting the right crystallization technology requires expertise in process engineering and material science. They provide not only equipment but also technical consultation to optimize crystallization parameters. Modern systems feature energy-efficient designs that reduce operational costs while maintaining superior product quality. The scalability of equipment from an industrial crystallization system supplier allows businesses to expand production capacity without replacing entire systems, making it a long-term investment in manufacturing excellence.

 EN