Wastewater Crystallizer Manufacturer Solutions

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

wastewater crystallizer manufacturer

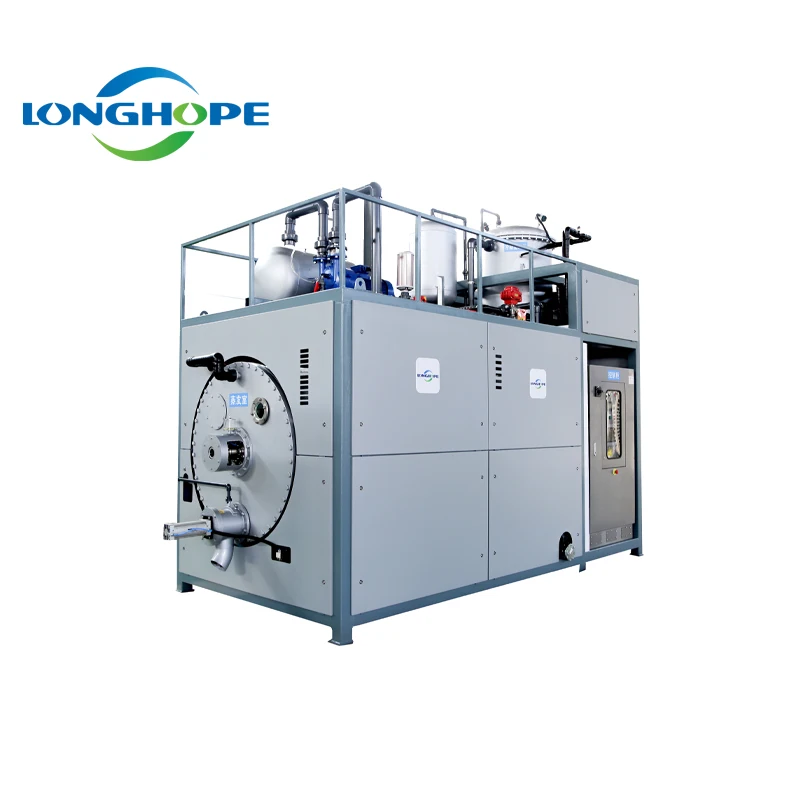
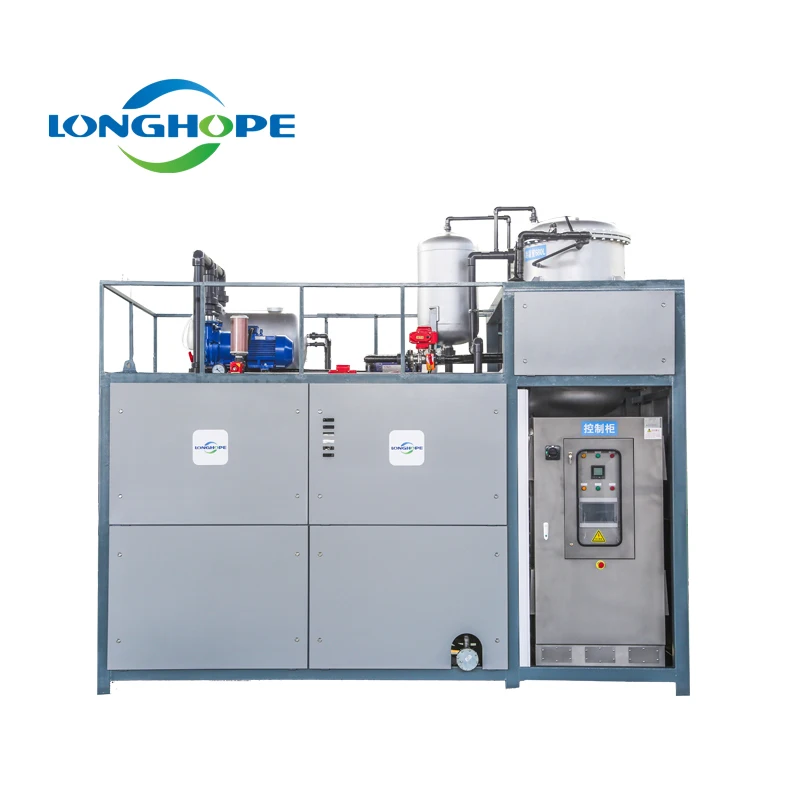
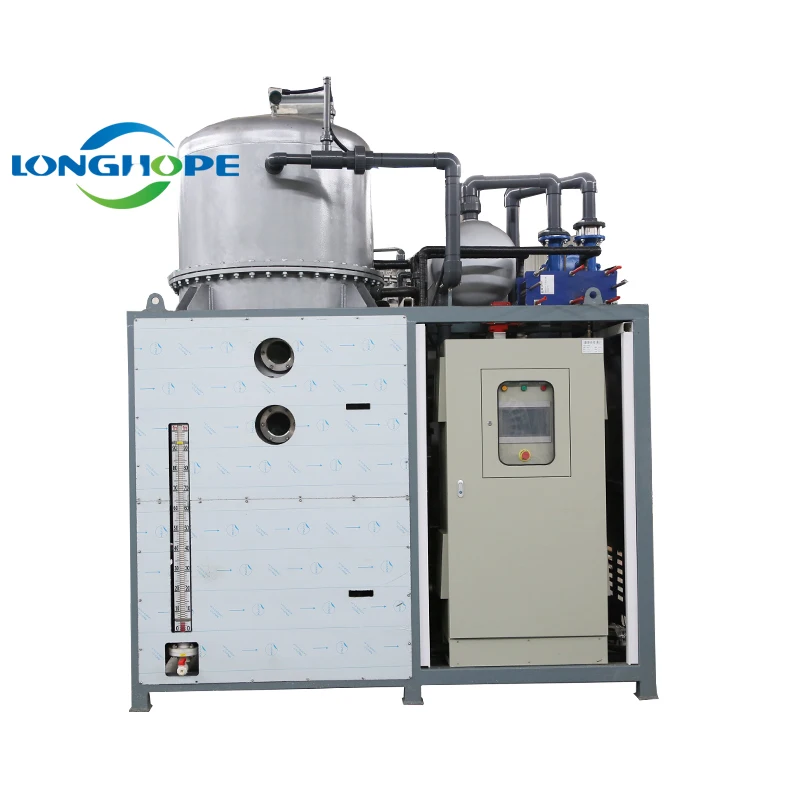
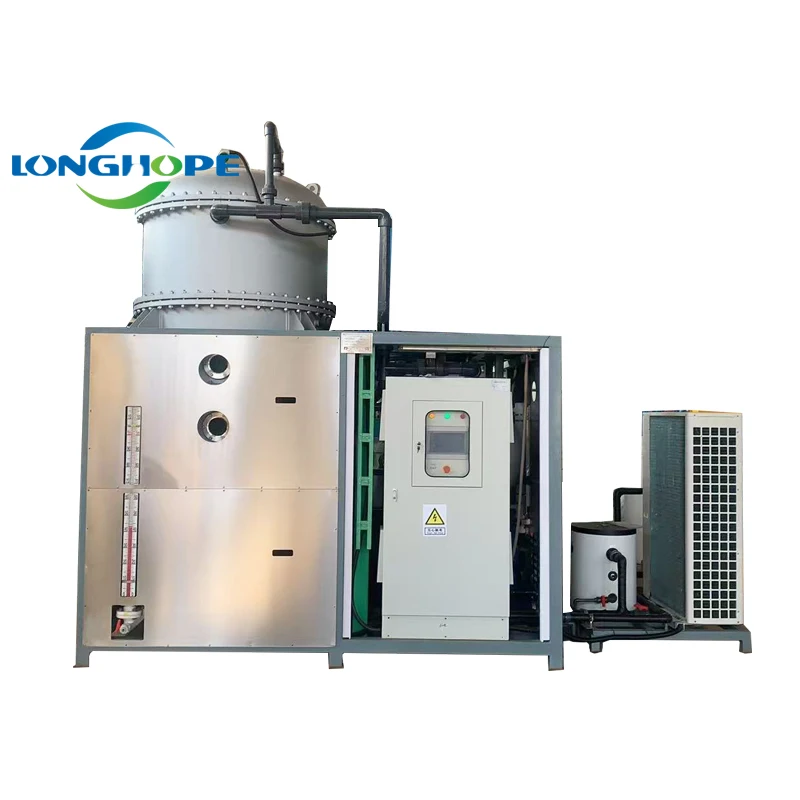
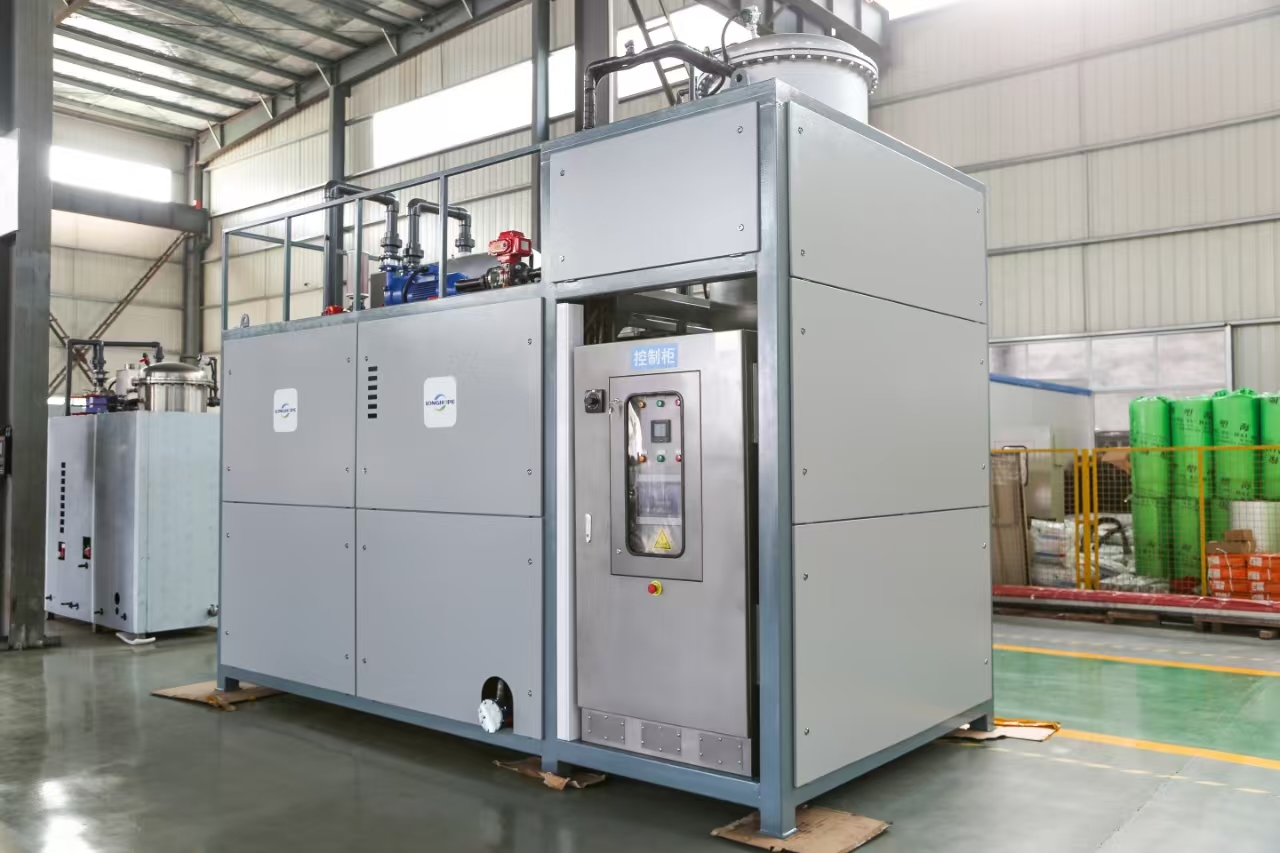
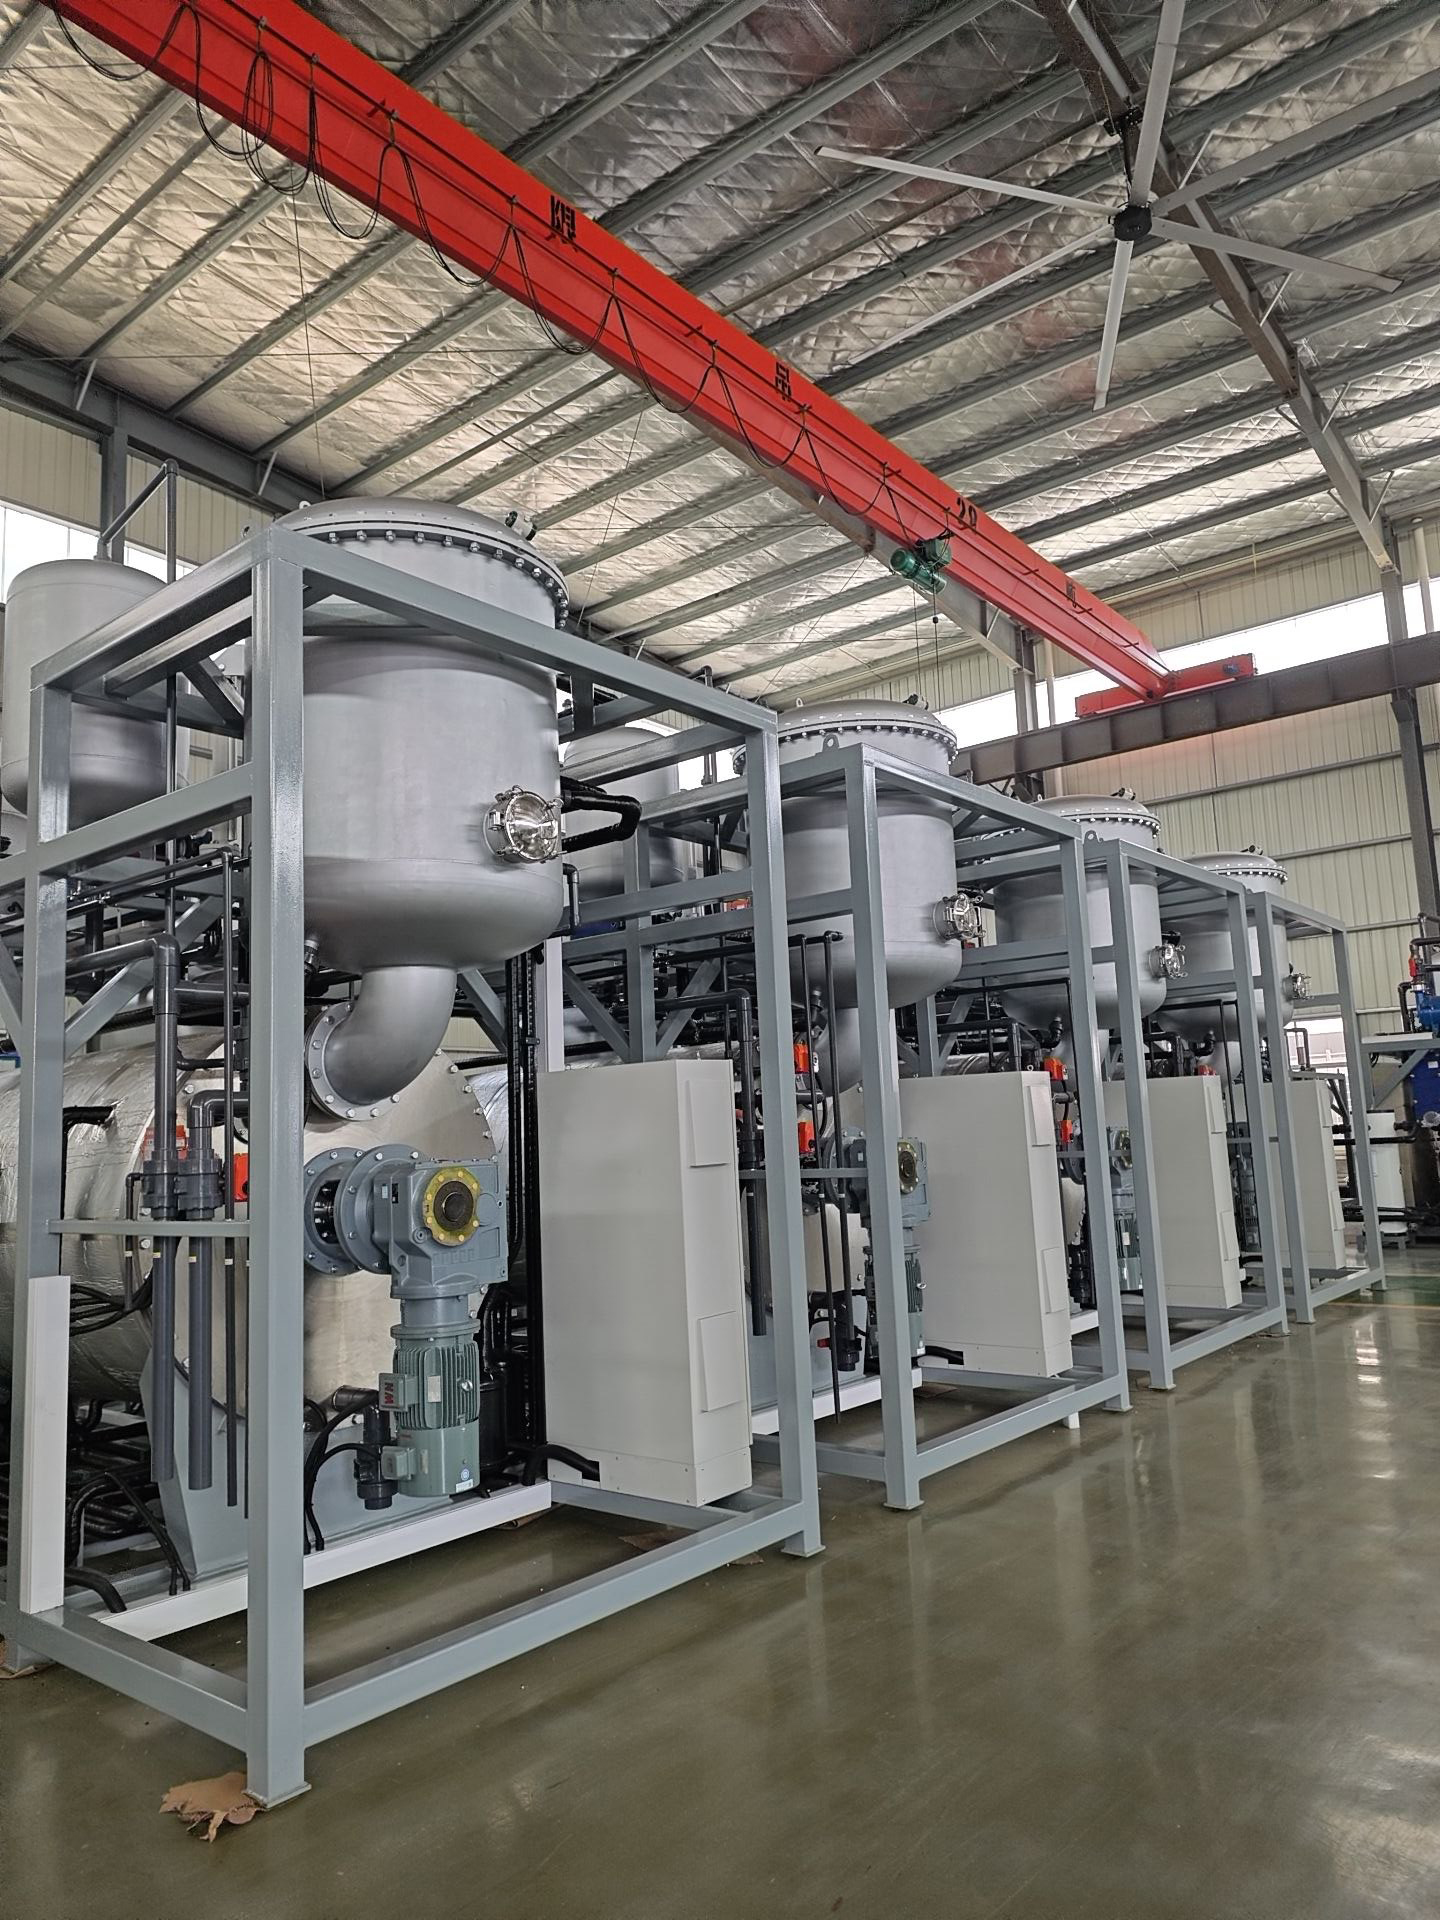
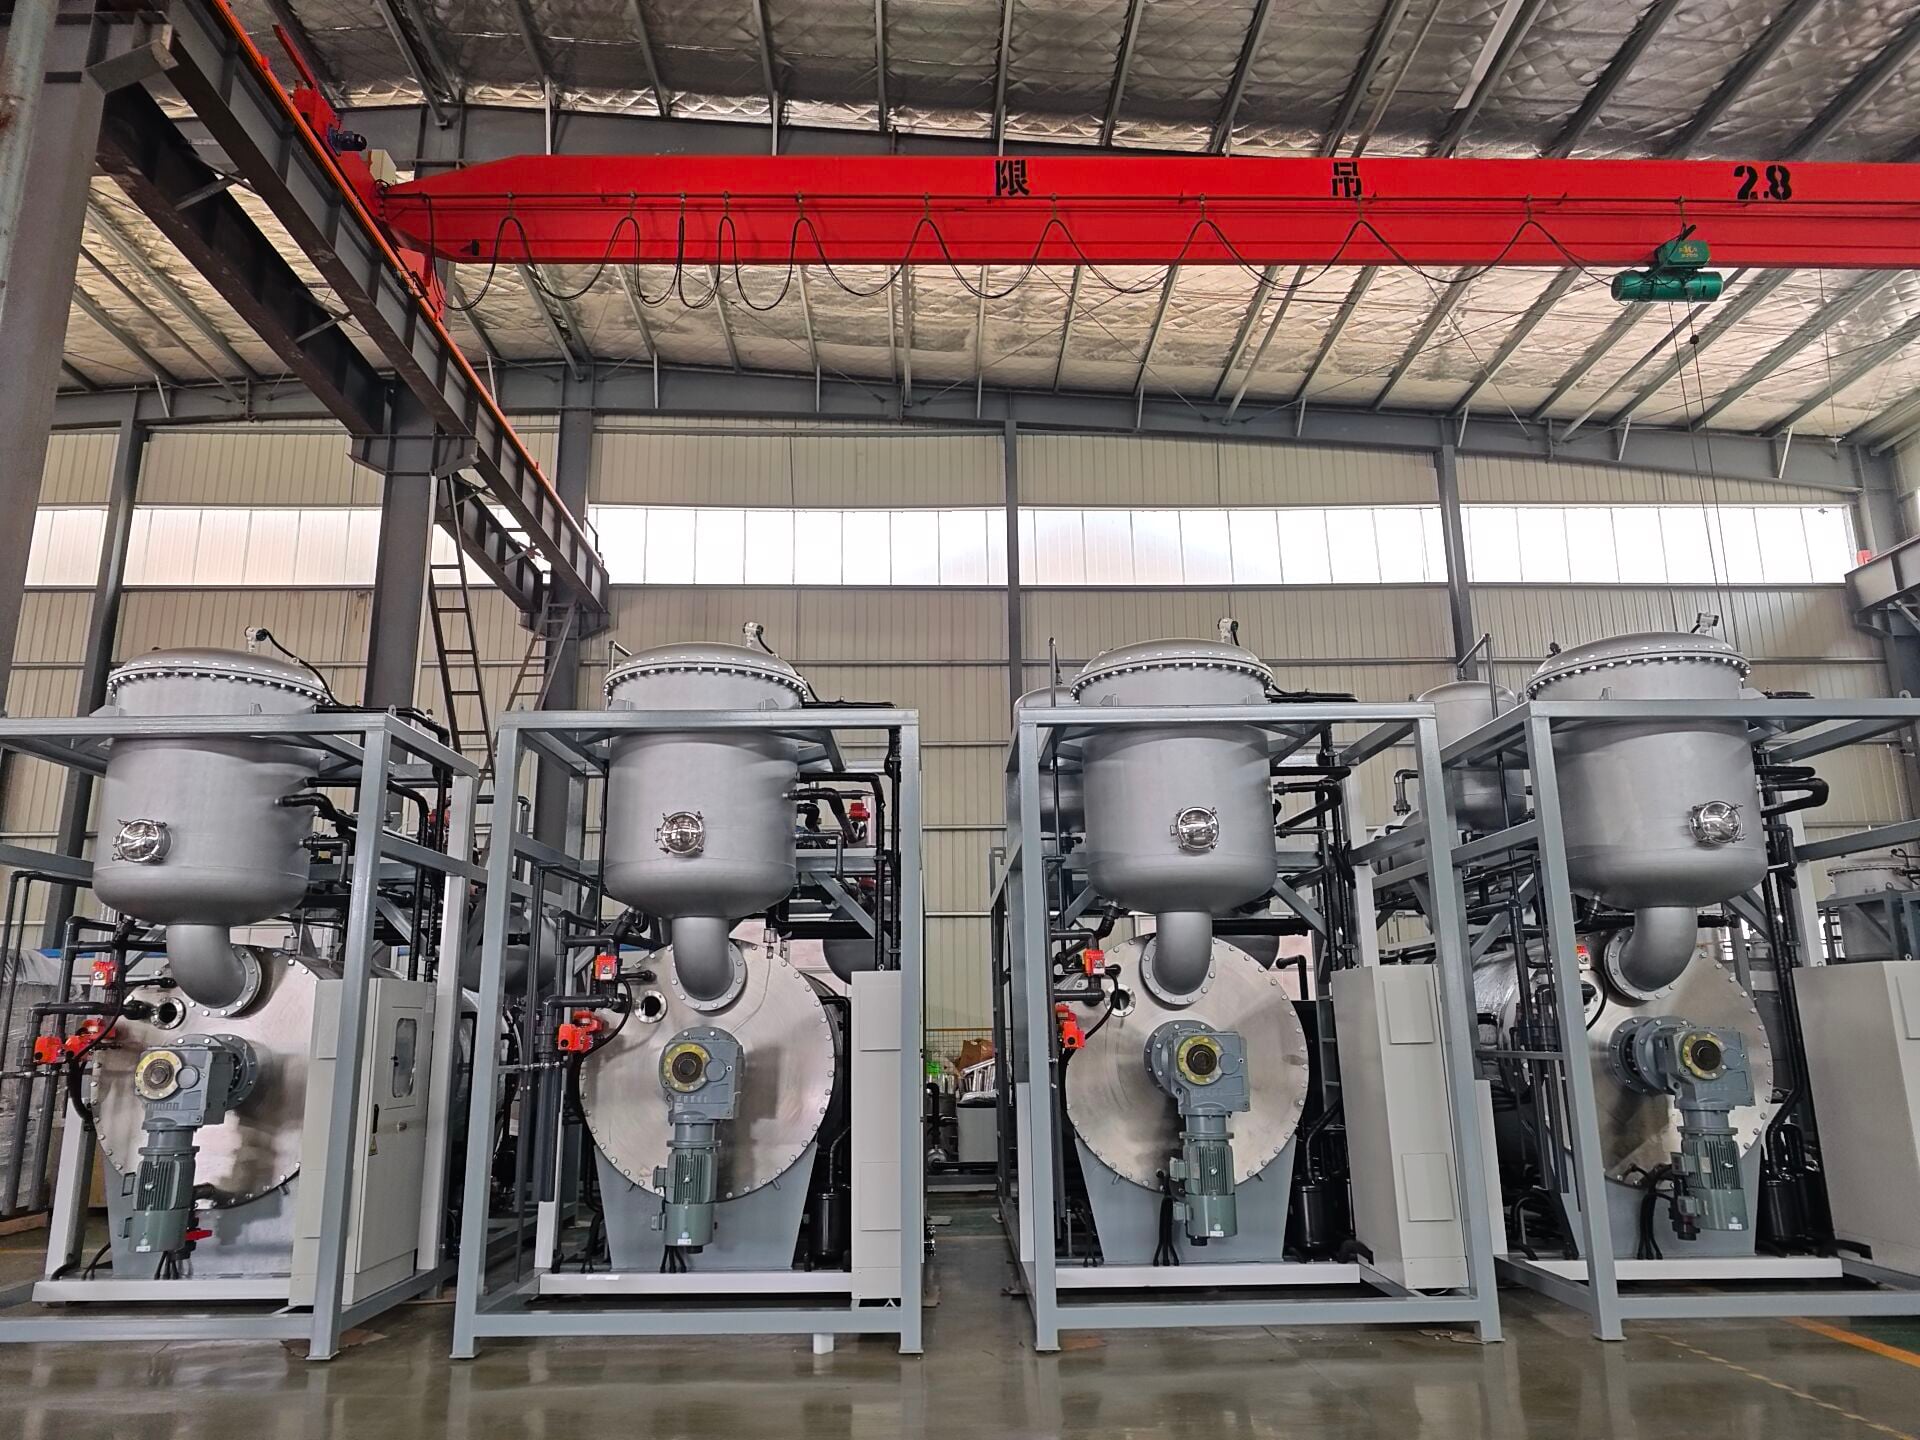
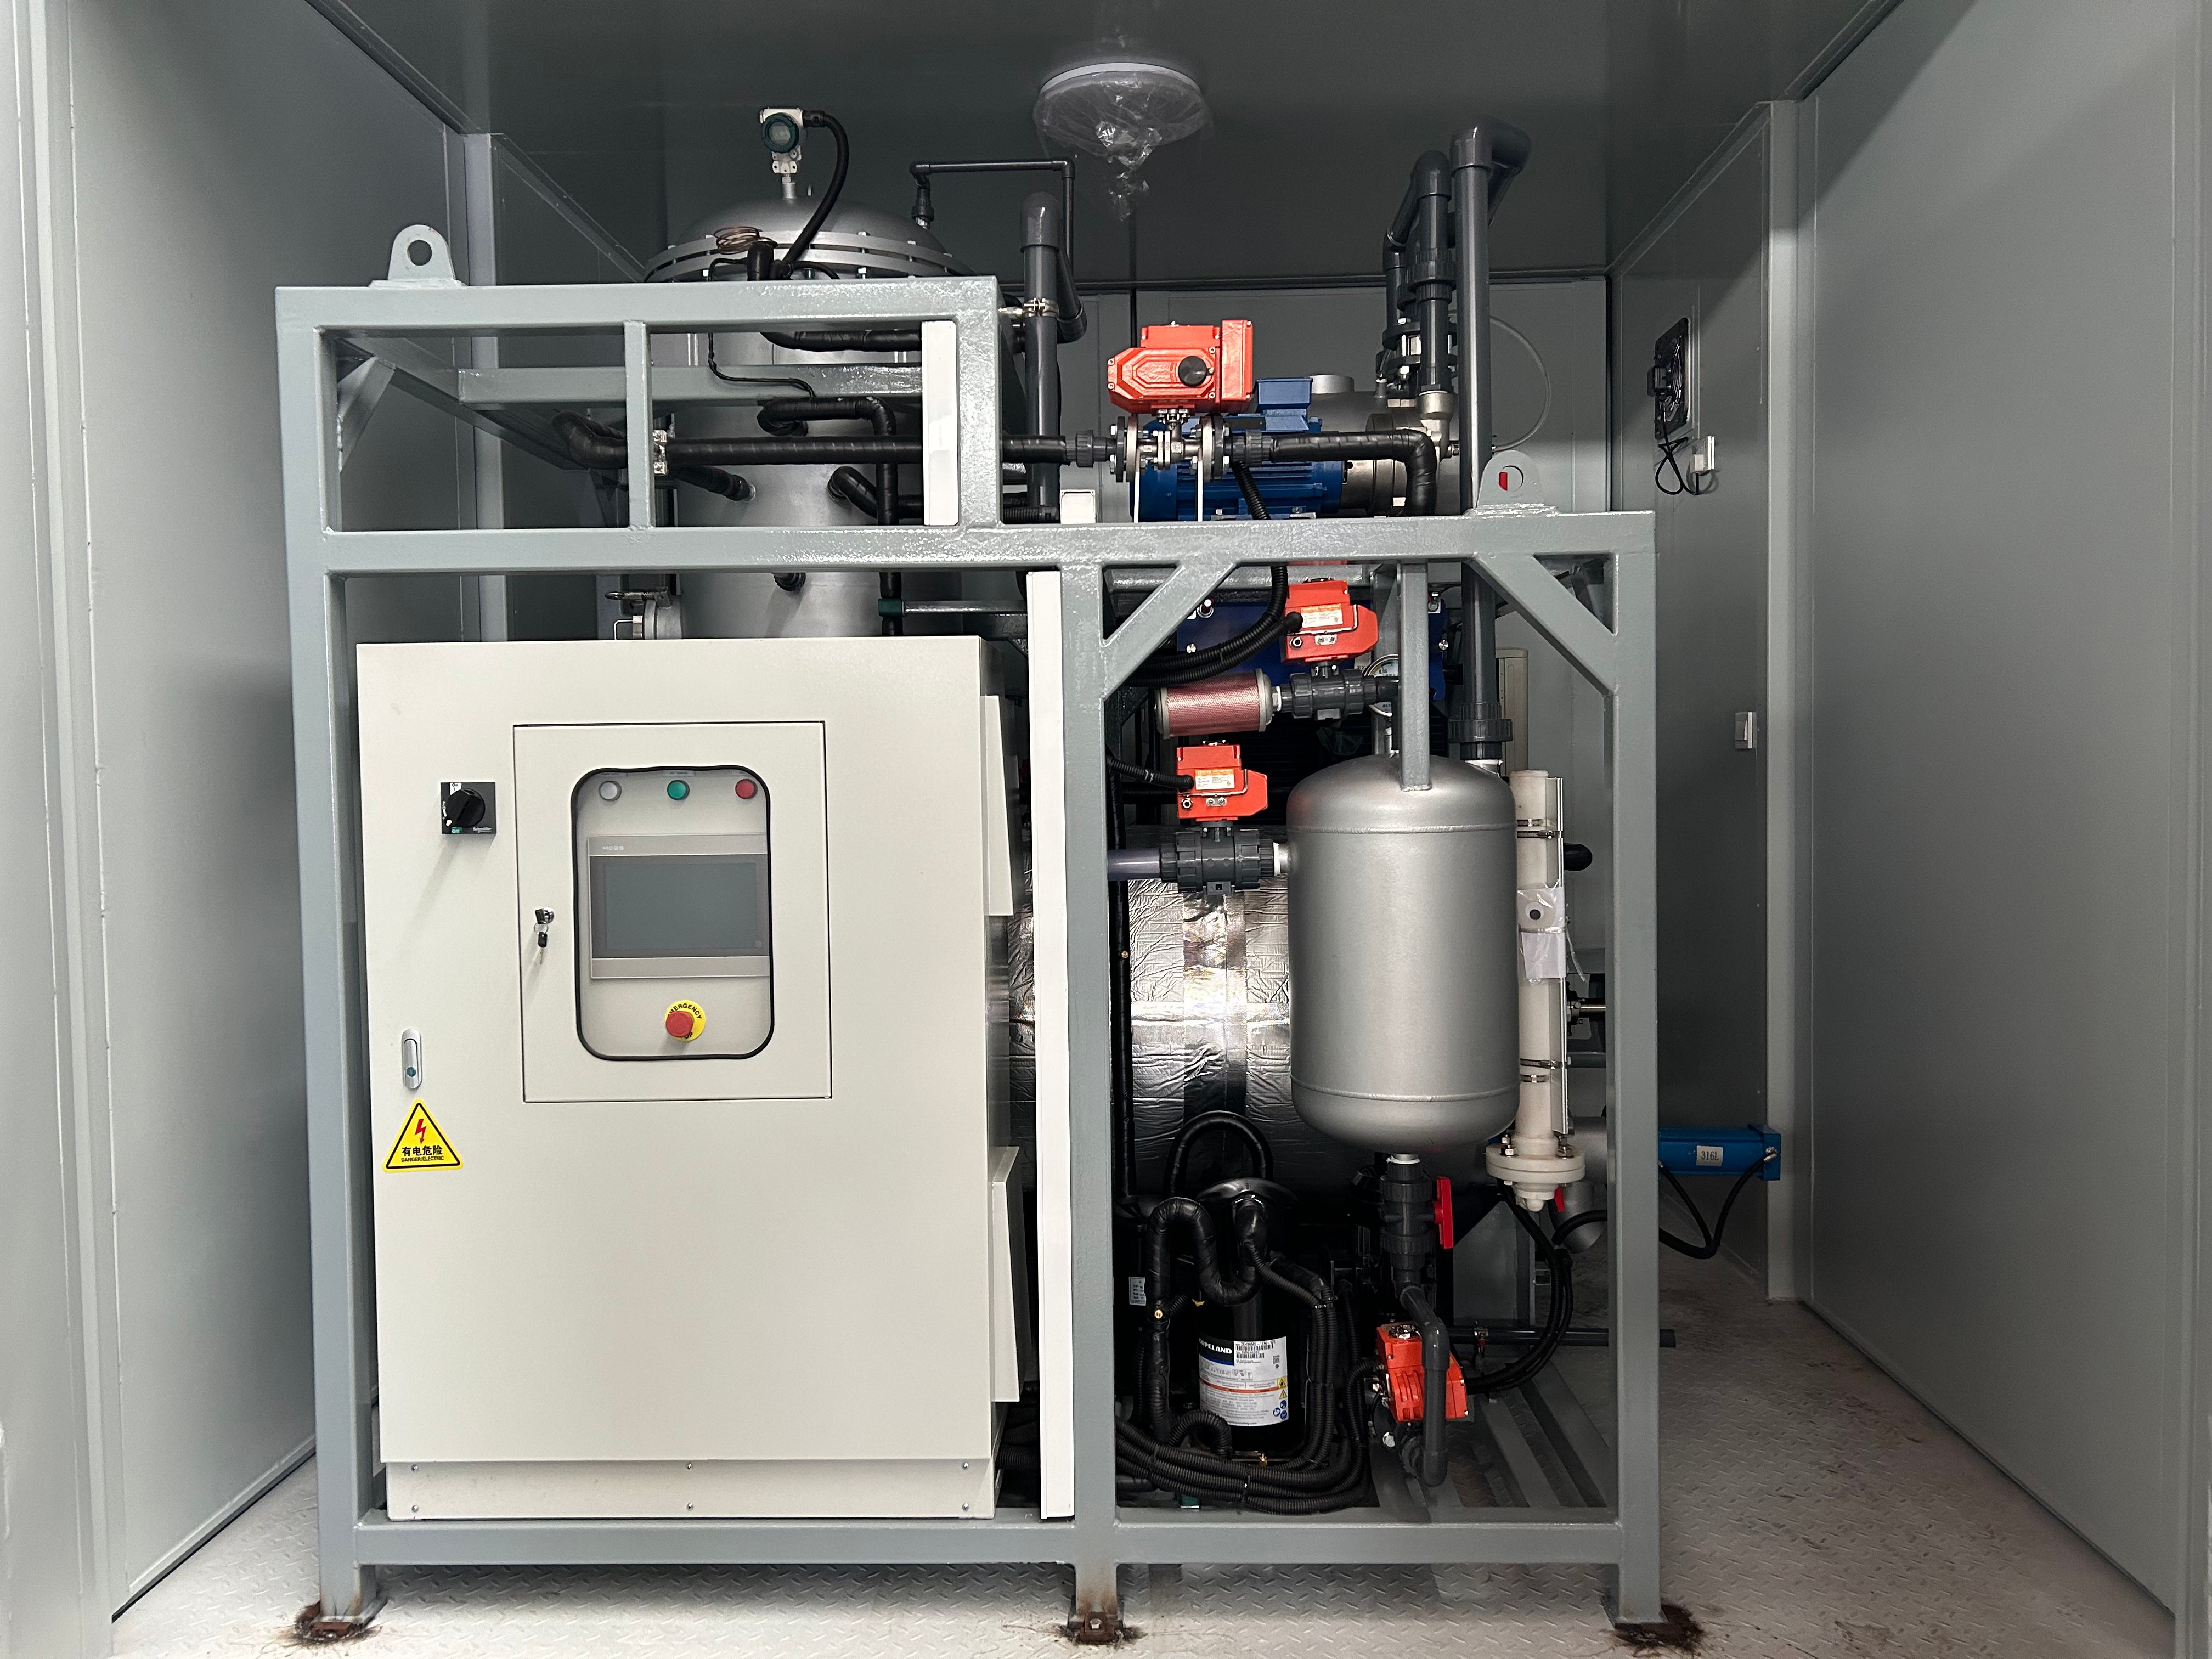
A wastewater crystallizer manufacturer specializes in designing and producing advanced equipment that transforms liquid waste streams into solid crystalline products through innovative separation technology. These systems represent a significant breakthrough in industrial waste management, offering facilities the ability to recover valuable materials while dramatically reducing disposal costs and environmental impact. The wastewater crystallizer manufacturer produces equipment that operates on crystallization principles, where dissolved solids are separated from liquid through controlled cooling, heating, or evaporation processes. This technology enables treatment of challenging wastewaters including brines, industrial effluents, and byproduct streams that traditional methods struggle to handle effectively. Key technological features of equipment from a wastewater crystallizer manufacturer include advanced heat exchange systems, automated crystallization control mechanisms, and integrated material handling capabilities. These systems utilize precision temperature management and specialized crystal growth chambers to optimize separation efficiency and product quality. Applications span multiple industries including chemical manufacturing, pharmaceutical production, food processing, mining operations, and metal finishing facilities. The wastewater crystallizer manufacturer serves any sector generating high-concentration waste streams requiring treatment before discharge or beneficial reuse. Industrial plants benefit from recovering salts, minerals, and other valuable compounds previously lost to disposal, while simultaneously achieving regulatory compliance and environmental stewardship objectives that align with sustainability initiatives and corporate responsibility standards.

New Products

A wastewater crystallizer manufacturer delivers substantial operational and financial benefits that transform how industrial facilities manage challenging waste streams. These systems provide cost-effective solutions by converting waste liabilities into valuable recovered products, directly improving bottom-line economics and reducing long-term disposal expenses significantly. Operational benefits are immediate and measurable. The wastewater crystallizer manufacturer's equipment operates continuously with minimal downtime, featuring automated monitoring systems that optimize performance without constant manual intervention. Maintenance requirements remain low due to durable construction and simplified internal mechanisms, reducing workforce demands and associated labor costs substantially. For specific applications, businesses treating brine solutions, salt-laden effluents, or mineral-rich wastewaters gain exceptional value. A wastewater crystallizer manufacturer provides tailored solutions addressing unique characteristics of different waste streams, ensuring optimal results whether handling organic compounds, inorganic salts, or complex industrial byproducts. Environmental advantages cannot be overstated. Installing equipment from a wastewater crystallizer manufacturer eliminates problematic liquid discharges, dramatically reducing environmental liability and regulatory compliance risks. Facilities achieve zero-liquid discharge capabilities, protecting water resources while generating recoverable solid products. Business decision-making becomes clearer with crystallization technology. Return on investment typically occurs within two to four years through reduced disposal fees, recovered material value, and operational savings. The wastewater crystallizer manufacturer's solutions position companies as environmental leaders, enhancing corporate reputation and meeting increasingly stringent regulatory requirements that competitors still struggle to address effectively.

Latest News

Vacuum Distillation System Maintenance Best Practices

24

Jul

Vacuum Distillation System Maintenance Best Practices

Proper vacuum distillation system maintenance is critical for industries relying on separation, purification, and concentration processes. A well-maintained vacuum distillation system ensures consistent product quality, minimizes operational downtime...
View More
Industrial Water Treatment Technologies for 2026

02

Sep

Industrial Water Treatment Technologies for 2026

Industrial water treatment remains one of the most critical operational priorities across manufacturing, chemical processing, food production, and energy sectors. As facilities face increasingly stringent environmental regulations, rising operational...
View More
Low Temperature Heat Pump Evaporator: Energy Saving Guide

24

Jul

Low Temperature Heat Pump Evaporator: Energy Saving Guide

Industrial facilities continuously seek ways to reduce operational costs while maintaining peak performance. A low temperature heat pump evaporator represents one of the most effective technologies for achieving significant energy savings in thermal ...
View More
How to Design an Efficient Vacuum Distillation Setup

02

Sep

How to Design an Efficient Vacuum Distillation Setup

Designing an efficient vacuum distillation setup requires careful attention to equipment selection, operational parameters, and system layout. A properly engineered vacuum distillation setup maximizes separation efficiency while minimizing energy con...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

wastewater crystallizer manufacturer

Advanced Crystallization Technology for Maximum Recovery

Advanced Crystallization Technology for Maximum Recovery

Leading wastewater crystallizer manufacturer equipment features sophisticated crystallization chambers designed to maximize material recovery rates and product purity. Advanced temperature control systems maintain optimal conditions throughout the crystallization process, ensuring consistent crystal formation and separation efficiency. The wastewater crystallizer manufacturer integrates automated feedback mechanisms that continuously adjust operating parameters, responding dynamically to influent stream variations. This intelligent automation eliminates manual adjustments while maintaining peak performance across changing conditions. High-capacity equipment handles substantial waste volumes while maintaining superior separation quality, directly translating to increased recovered material value and reduced processing time per unit volume.
Sustainable Zero-Liquid Discharge Solutions

Sustainable Zero-Liquid Discharge Solutions

Environmental responsibility drives selection of equipment from a wastewater crystallizer manufacturer, which delivers genuine zero-liquid discharge capabilities eliminating harmful effluent discharges completely. The wastewater crystallizer manufacturer's systems separate dissolved solids from liquid streams with exceptional efficiency, producing clean recirculated water meeting reuse standards. This transformative capability protects freshwater resources while reducing facility water consumption and associated utility costs dramatically. Facilities operating crystallization systems achieve environmental certifications and regulatory compliance effortlessly, establishing competitive advantages in sustainability-conscious markets. Companies employing this wastewater crystallizer manufacturer technology demonstrate genuine commitment to environmental stewardship while accessing substantial operational benefits and economic advantages simultaneously.
Exceptional Return on Investment and Cost Savings

Exceptional Return on Investment and Cost Savings

Financial benefits from investing in equipment from a wastewater crystallizer manufacturer emerge quickly through multiple revenue streams and expense reductions. Recovered crystalline products generate direct income streams or reduce material procurement costs, while eliminating expensive waste disposal fees provides immediate savings. The wastewater crystallizer manufacturer's equipment operates with low energy requirements compared to alternative treatment methods, reducing utility consumption substantially. Automated operation minimizes labor requirements, further improving profitability and operational efficiency metrics. Industrial facilities typically achieve complete investment recovery within two to four years, after which equipment generates pure profit through recovered material value and sustained operational savings, making this wastewater crystallizer manufacturer investment highly attractive for strategic facility planning.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000