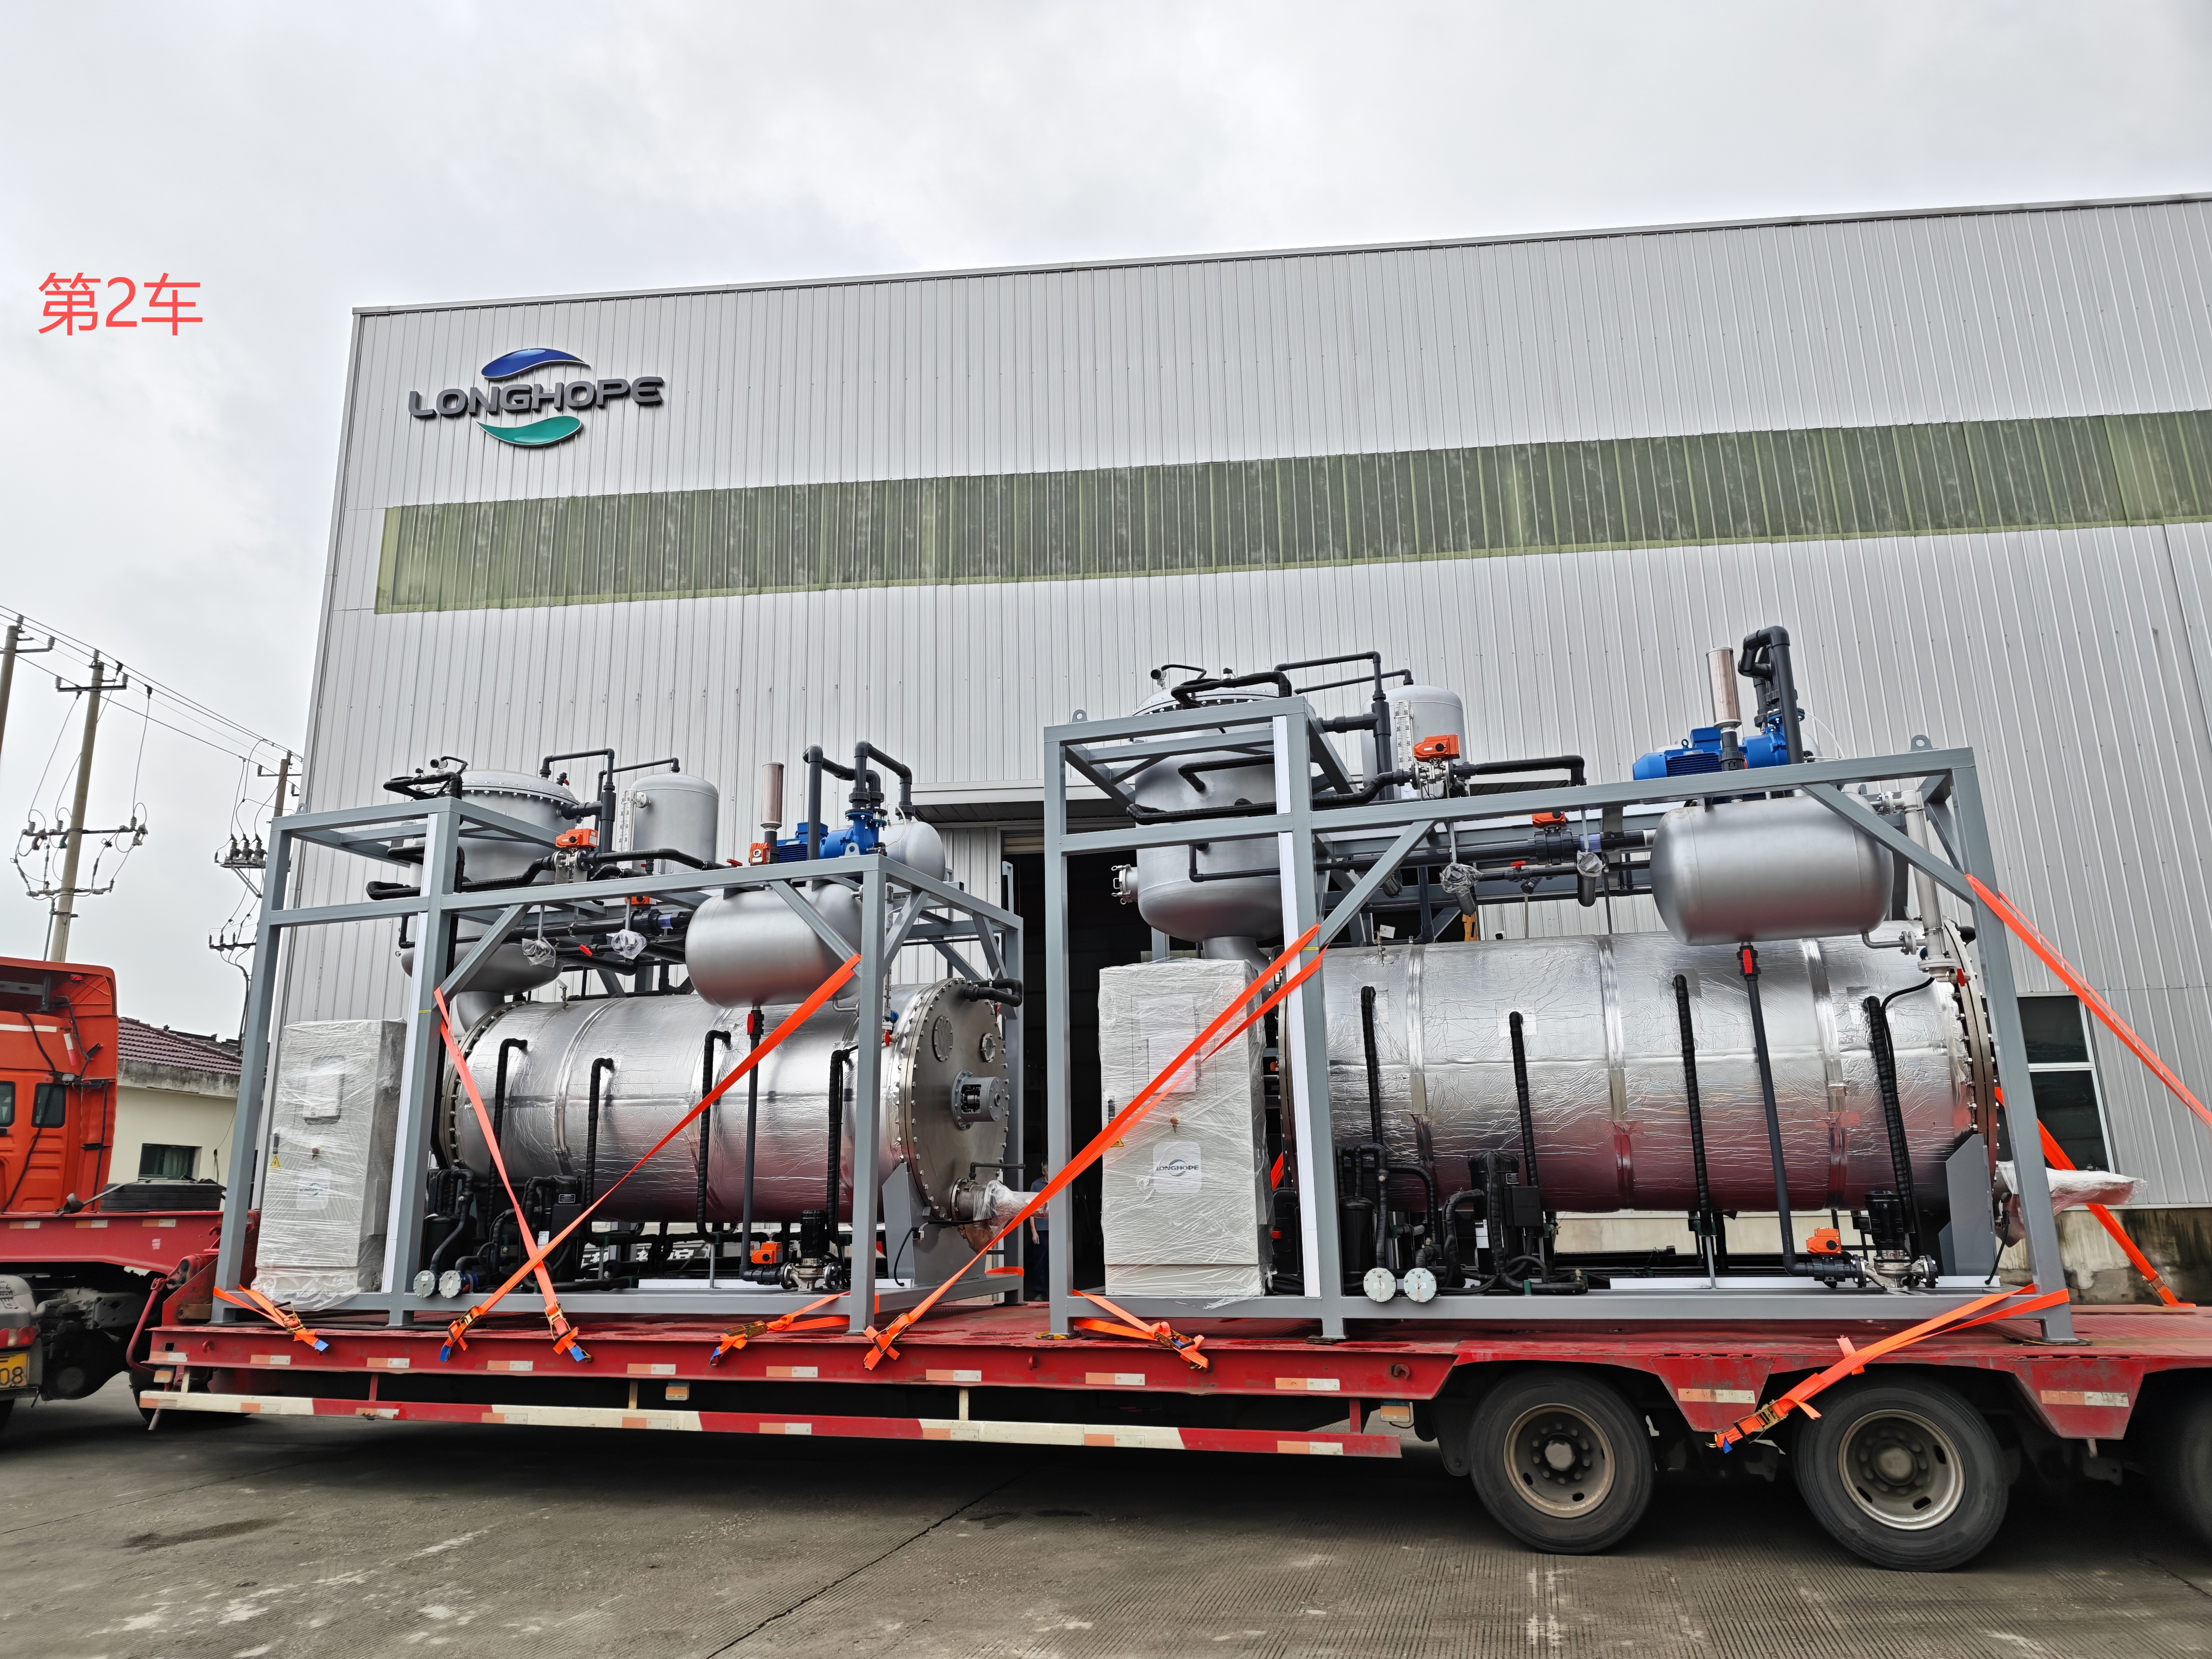
industrial crystallization system
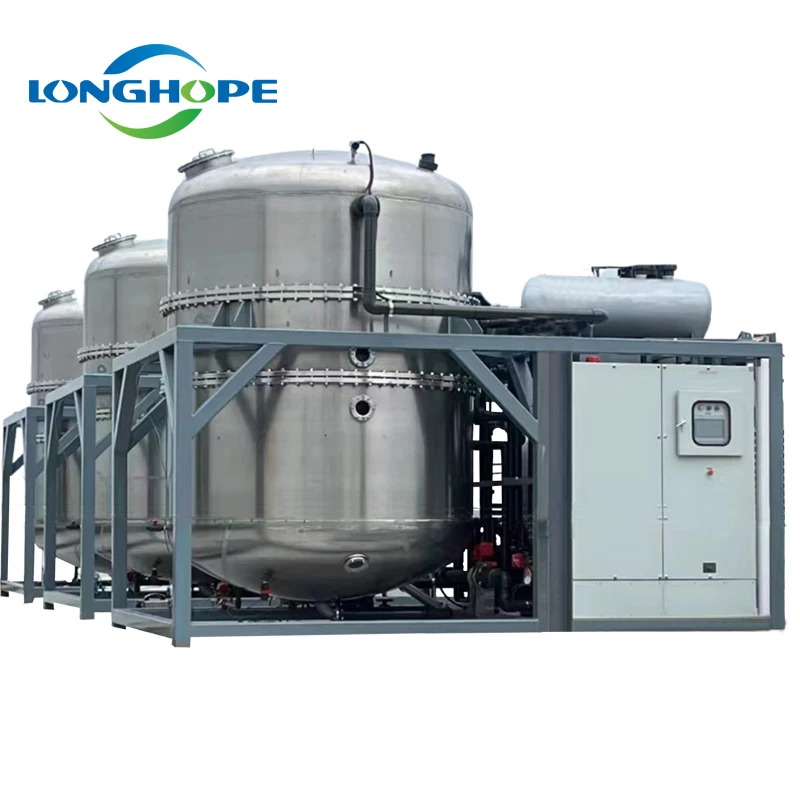
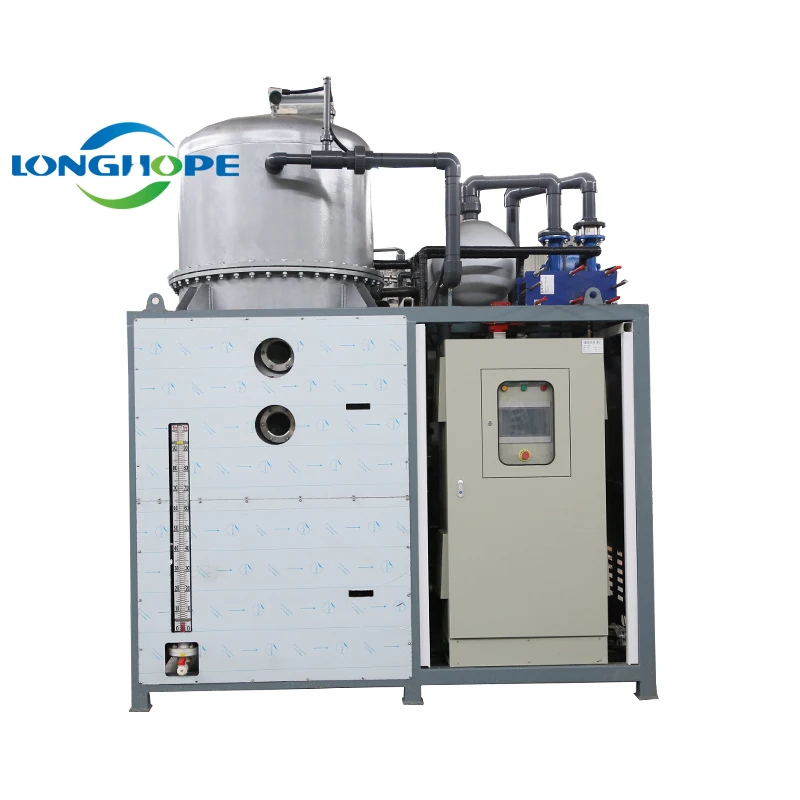
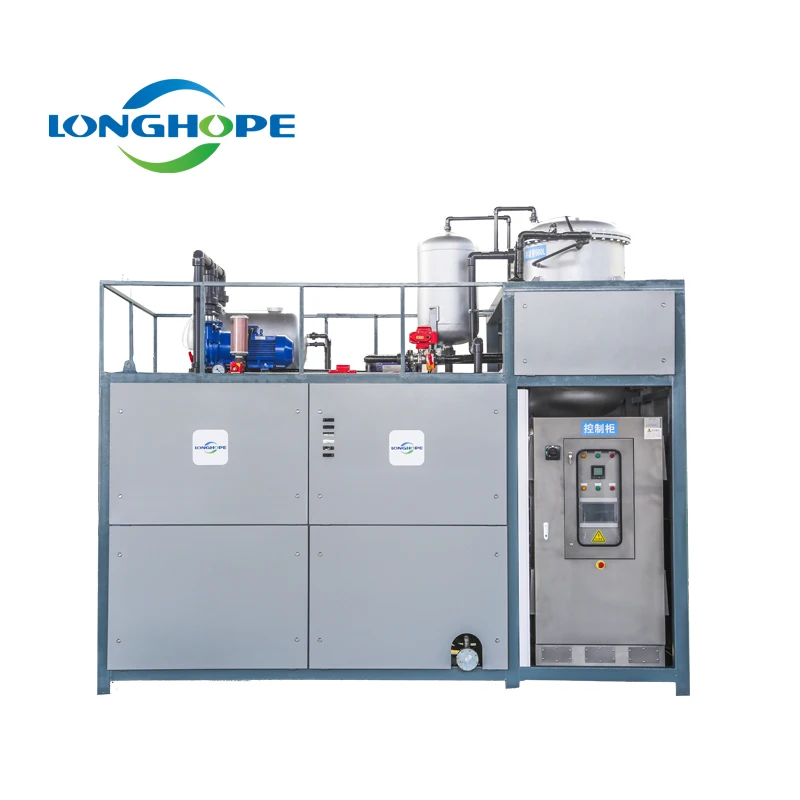
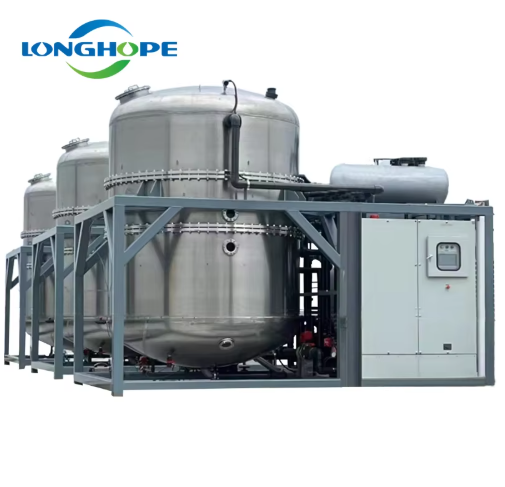
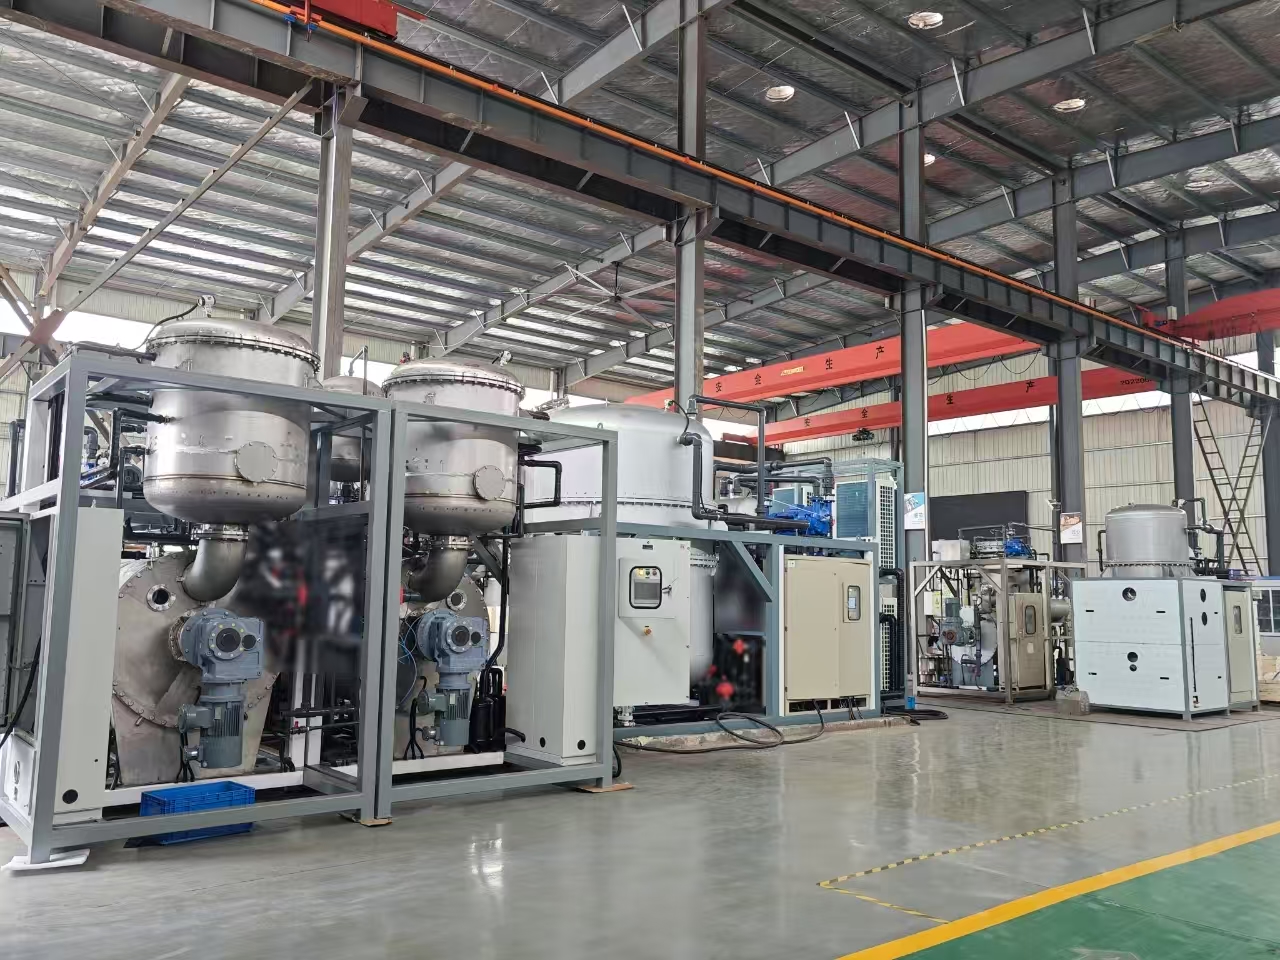
An industrial crystallization system is a sophisticated piece of equipment designed to separate dissolved solids from liquid solutions through controlled crystal formation and growth. This system plays a vital role in numerous manufacturing processes across pharmaceuticals, chemicals, food production, and materials science industries.
The industrial crystallization system operates by manipulating temperature, concentration, and agitation to encourage crystalline structure development. As solutions cool or become supersaturated, dissolved particles bond together, forming pure crystals that can be easily separated from the remaining liquid mother liquor. This process enables manufacturers to achieve high-purity products efficiently.
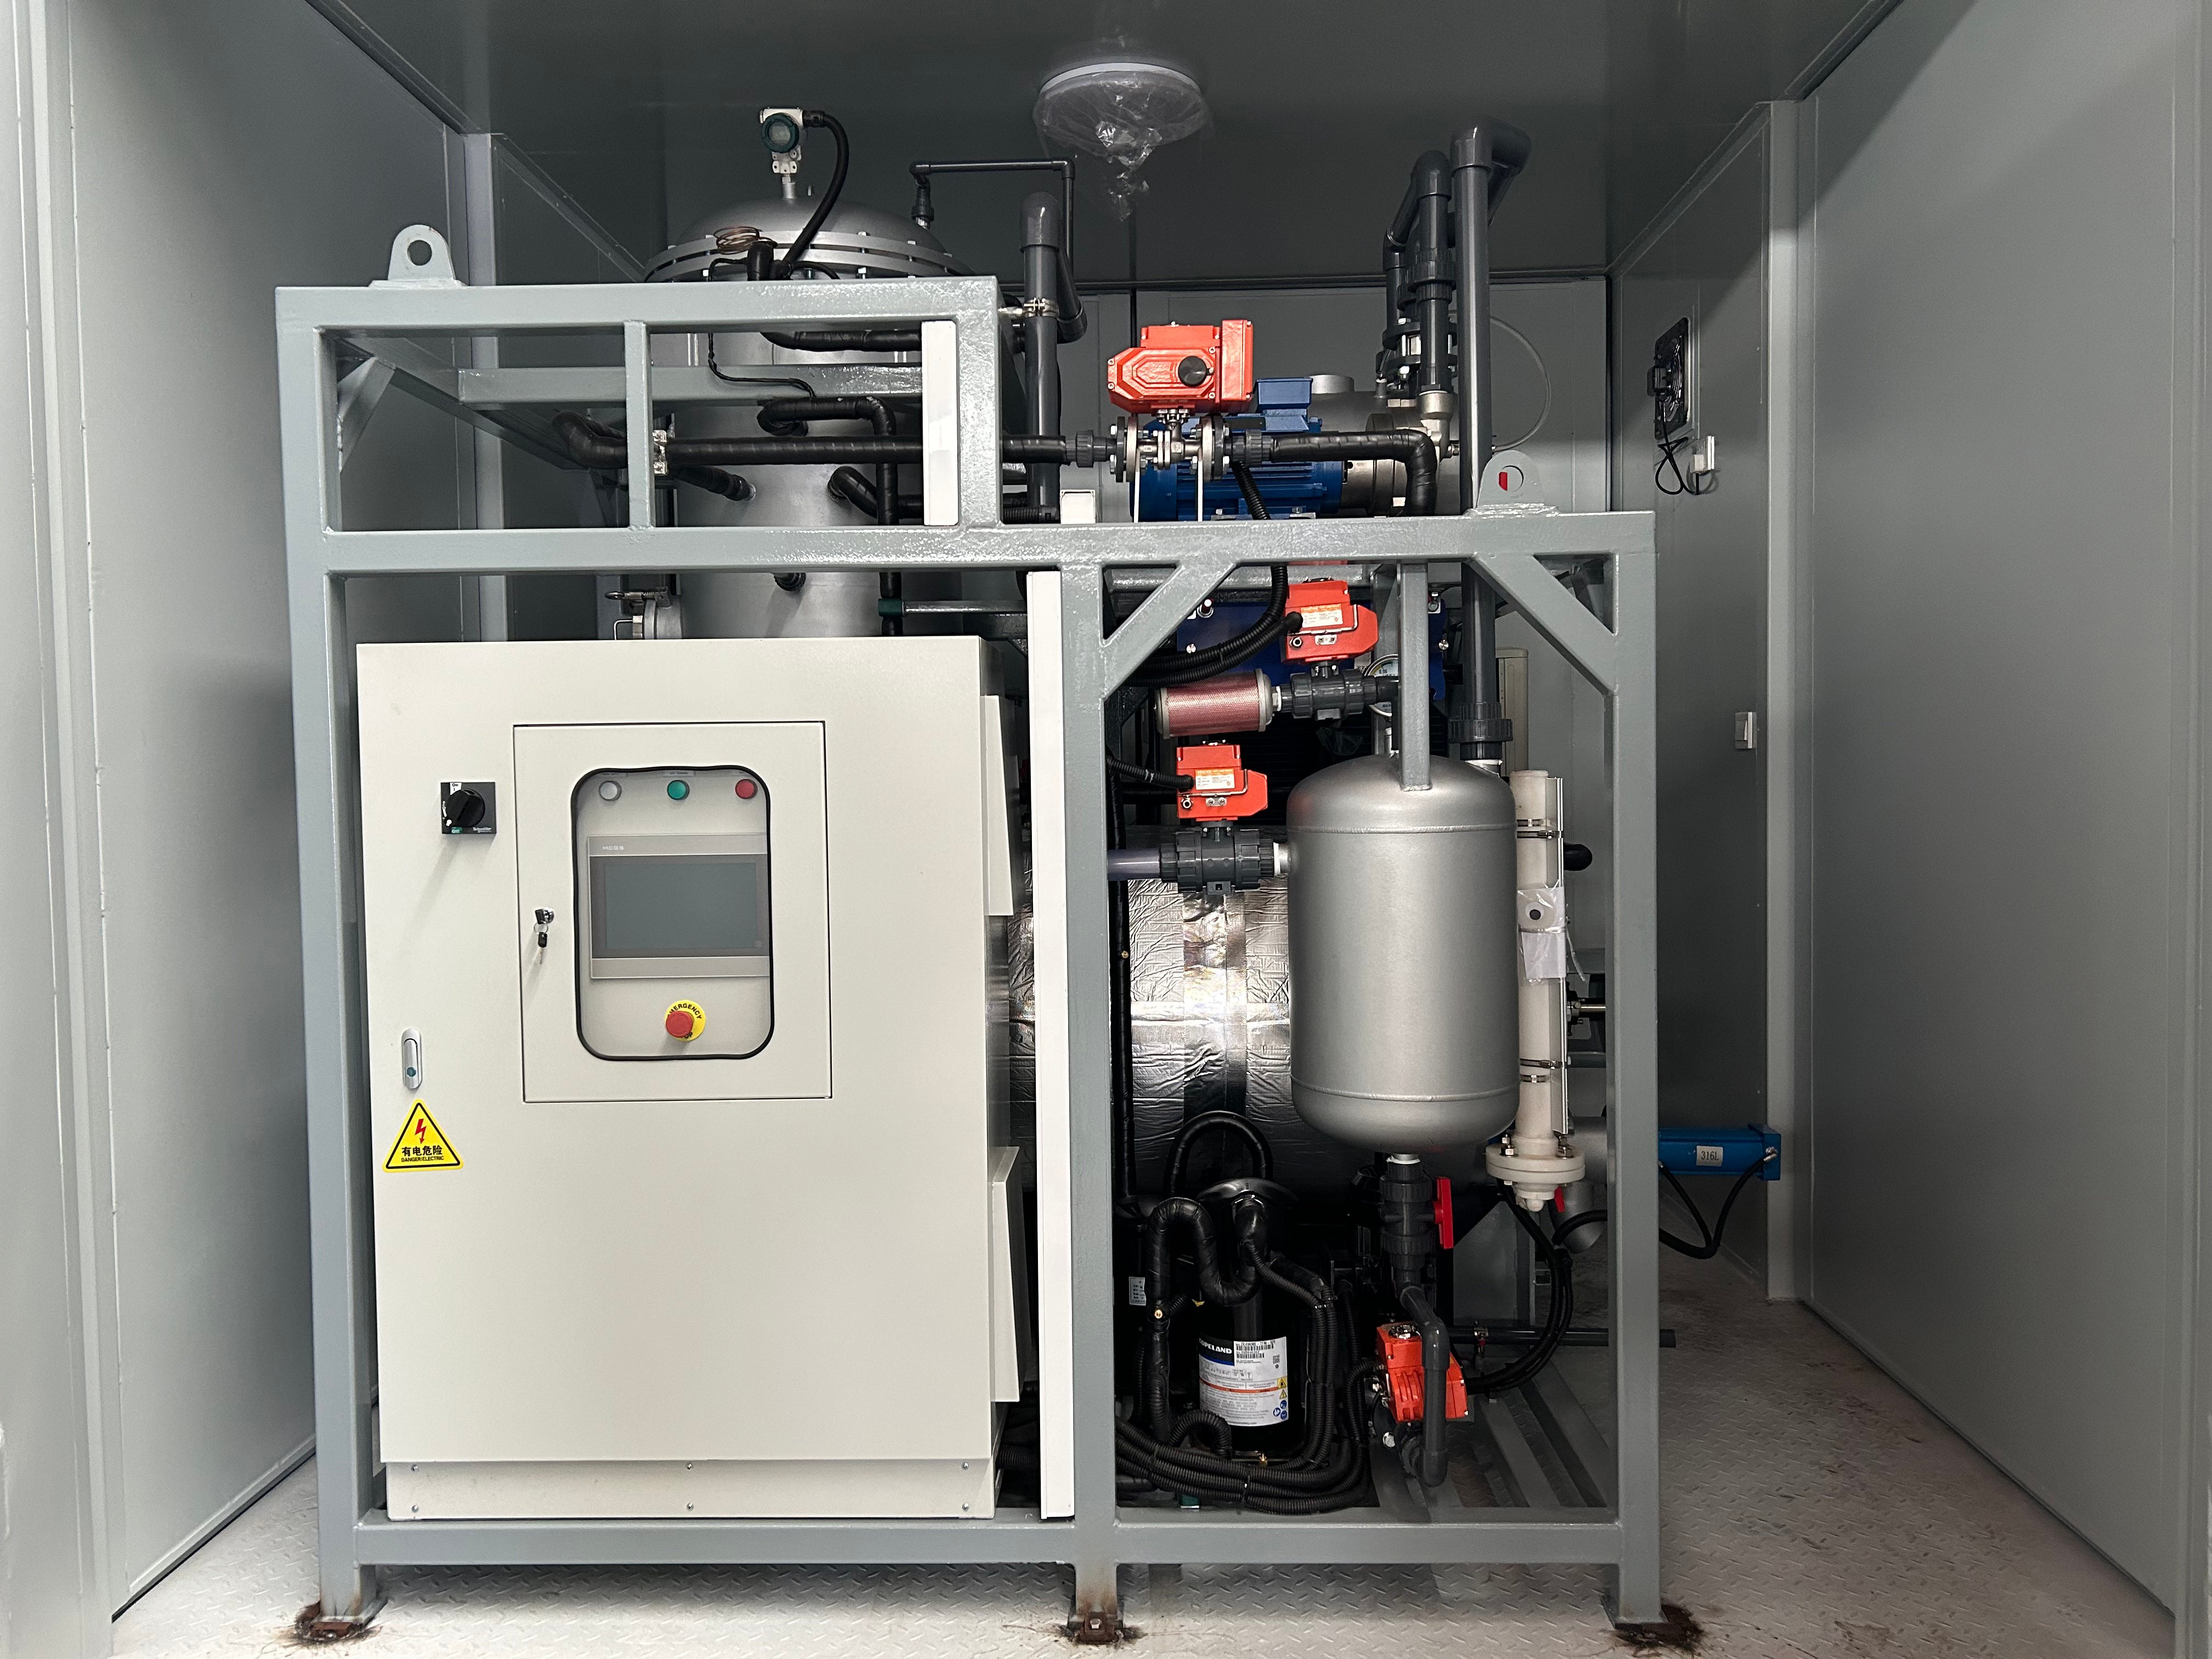
Key technological features of an industrial crystallization system include precise temperature control mechanisms, advanced mixing capabilities, automated monitoring systems, and scalable vessel designs. Modern systems incorporate digital sensors and control interfaces that track crystallization progress in real time, allowing operators to optimize batch parameters for consistent results.
The industrial crystallization system serves multiple critical applications. In pharmaceutical manufacturing, it purifies active ingredients and produces uniform crystal sizes for better bioavailability. Chemical producers use these systems for salt separation, pigment production, and intermediate compound isolation. Food manufacturers employ crystallization for sugar refining, salt processing, and specialty ingredient production.
Industrial crystallization systems deliver superior product purity, reduced waste, improved yield rates, and enhanced process reliability compared to traditional separation methods. Their versatility makes them indispensable for businesses seeking competitive advantages in quality and efficiency across diverse industrial sectors.

 EN