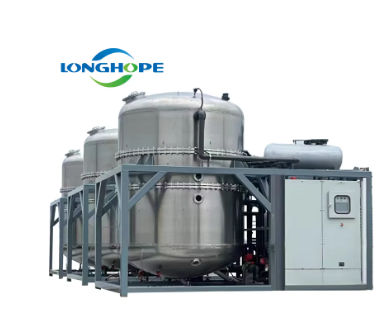
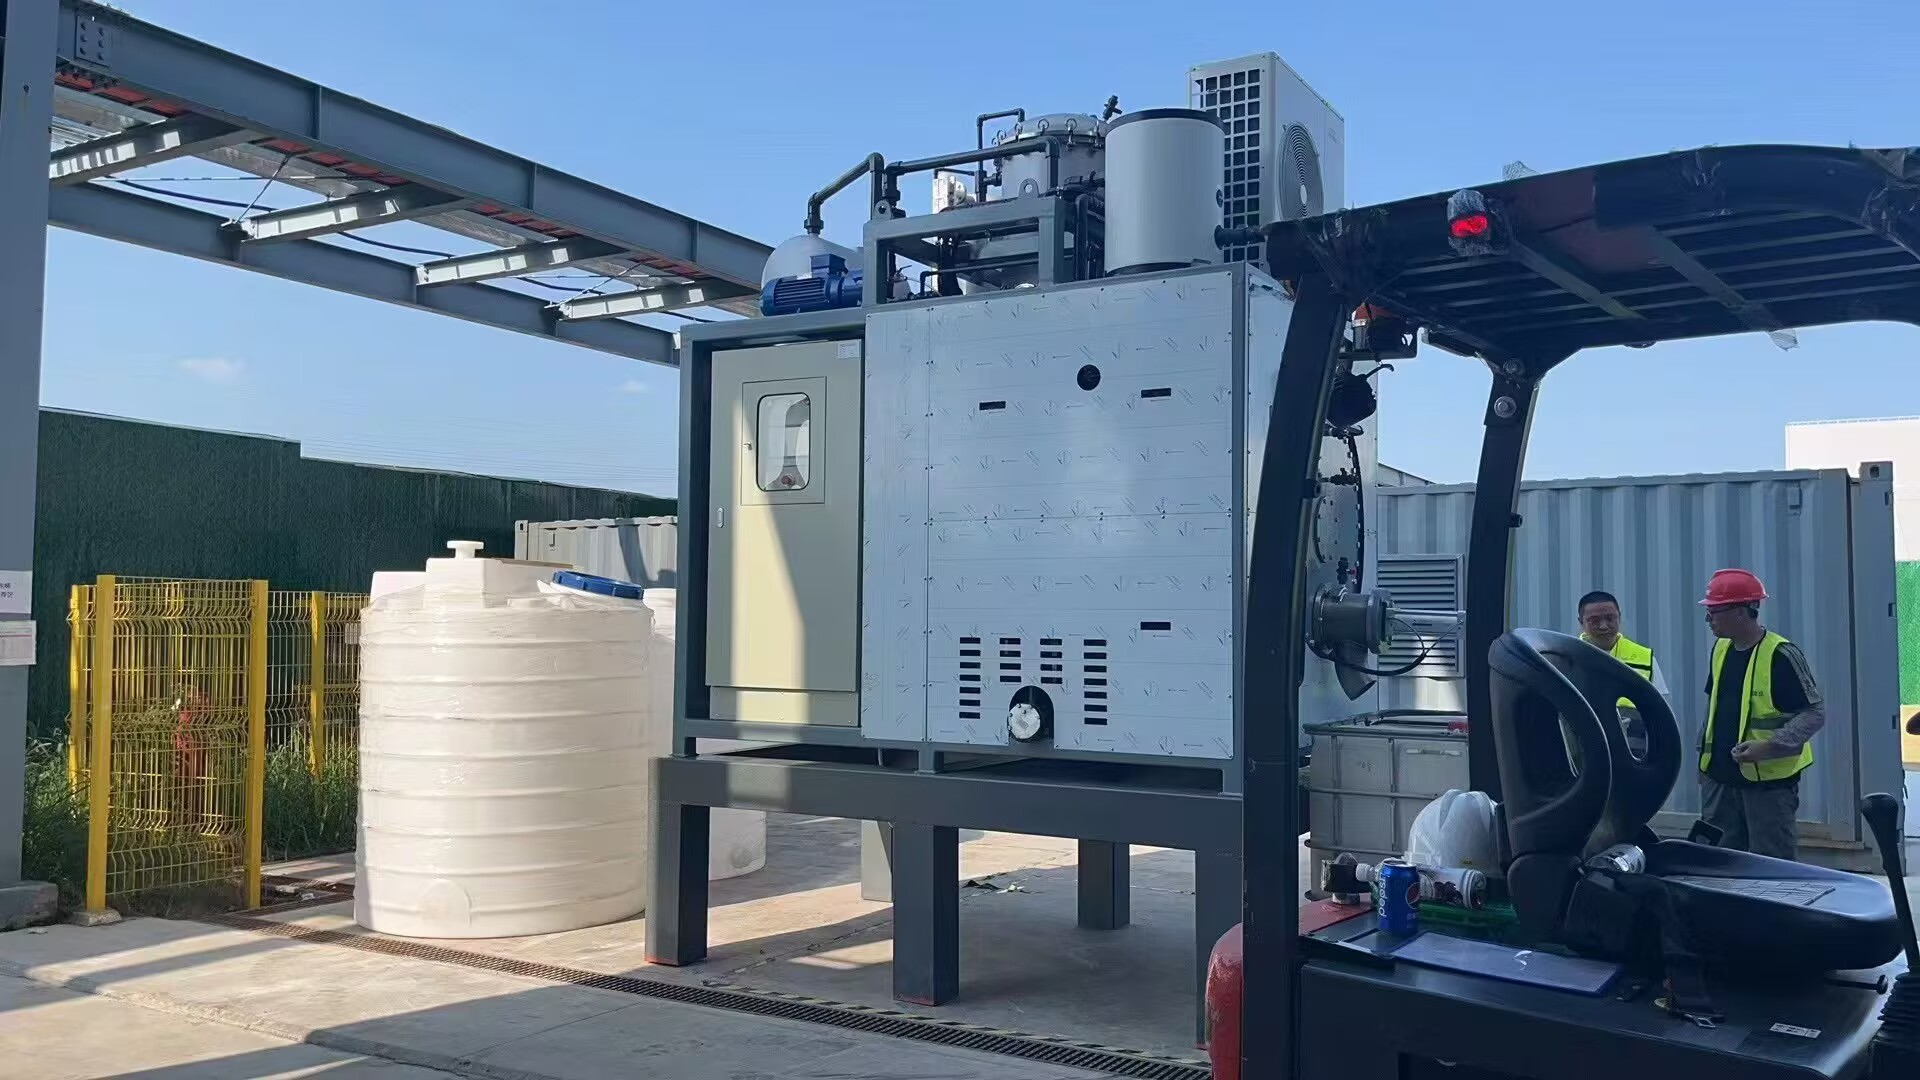
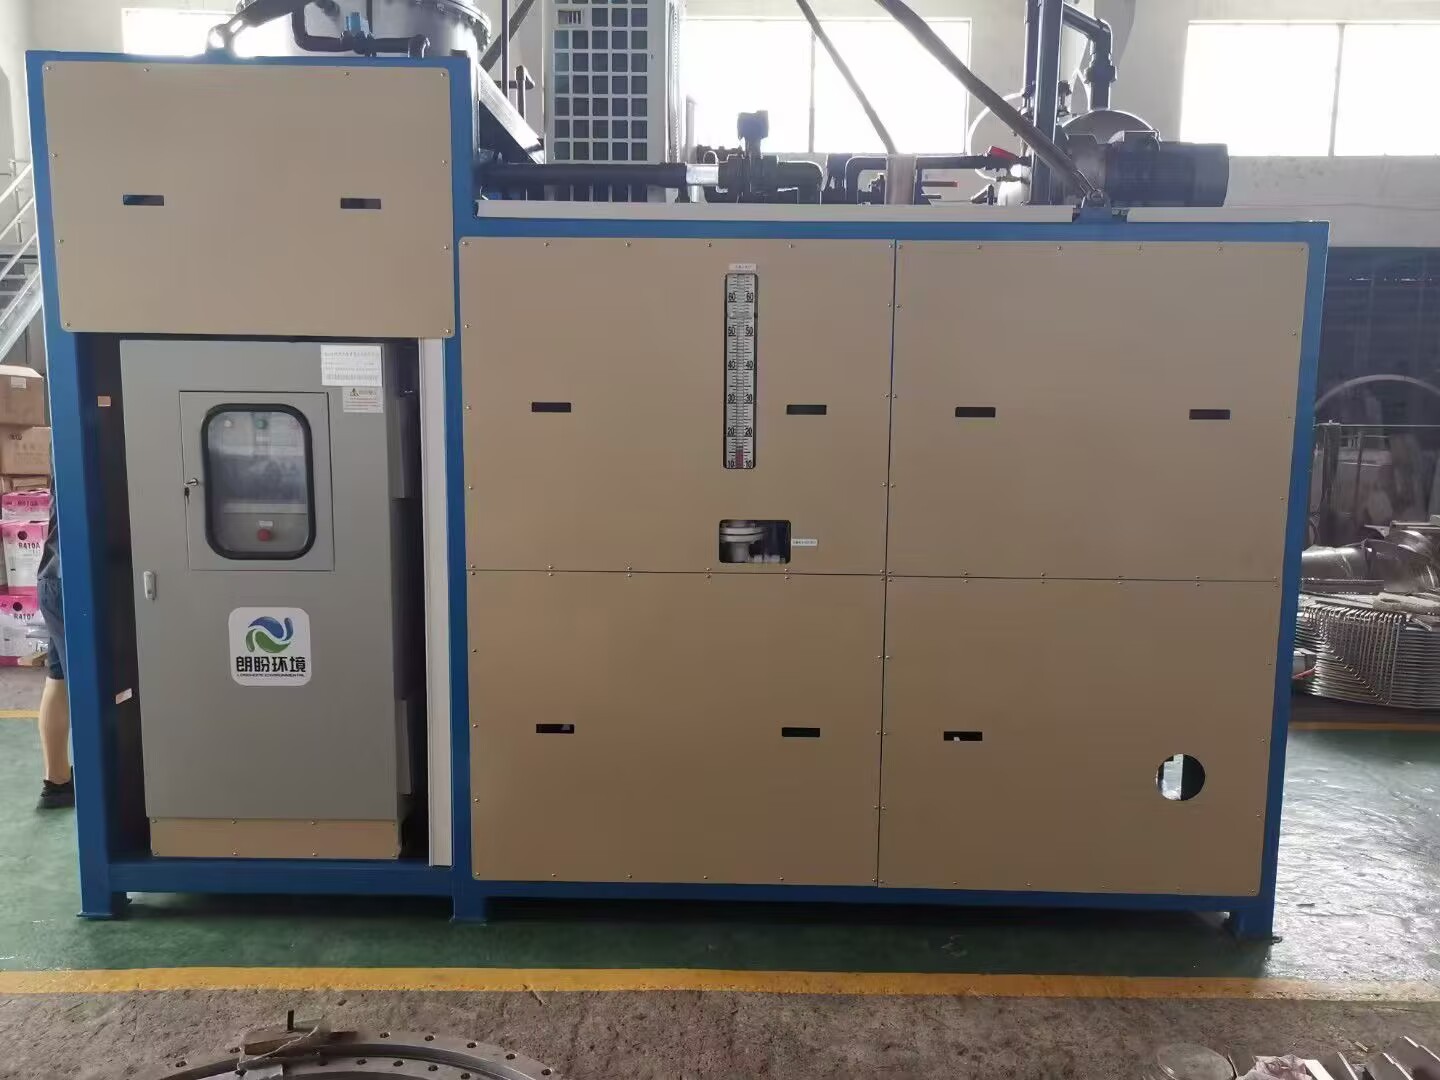
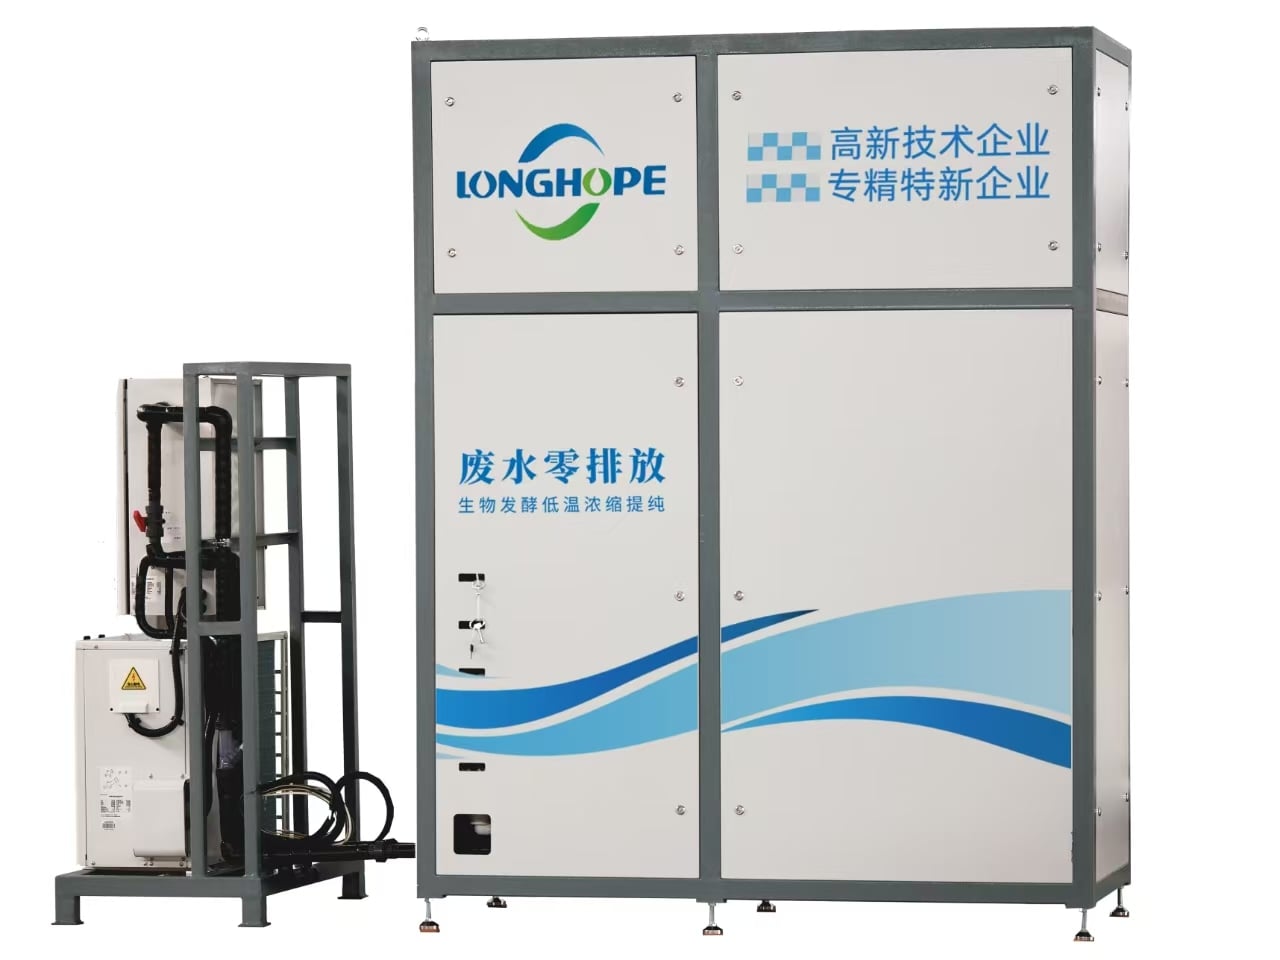
Heat Pump Crystallizer: Advanced Thermal Technology

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

heat pump crystallizer

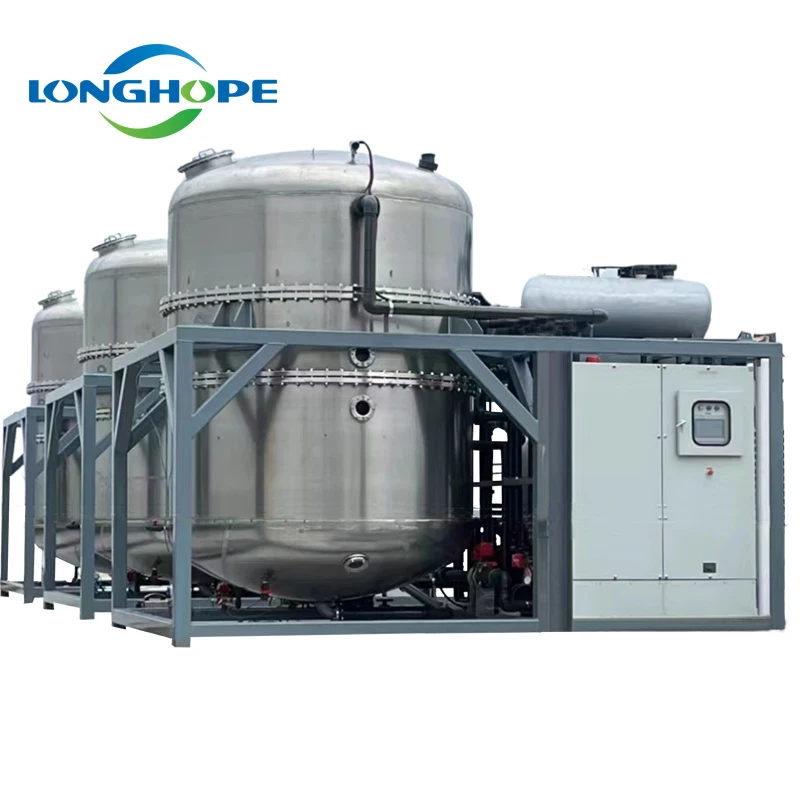
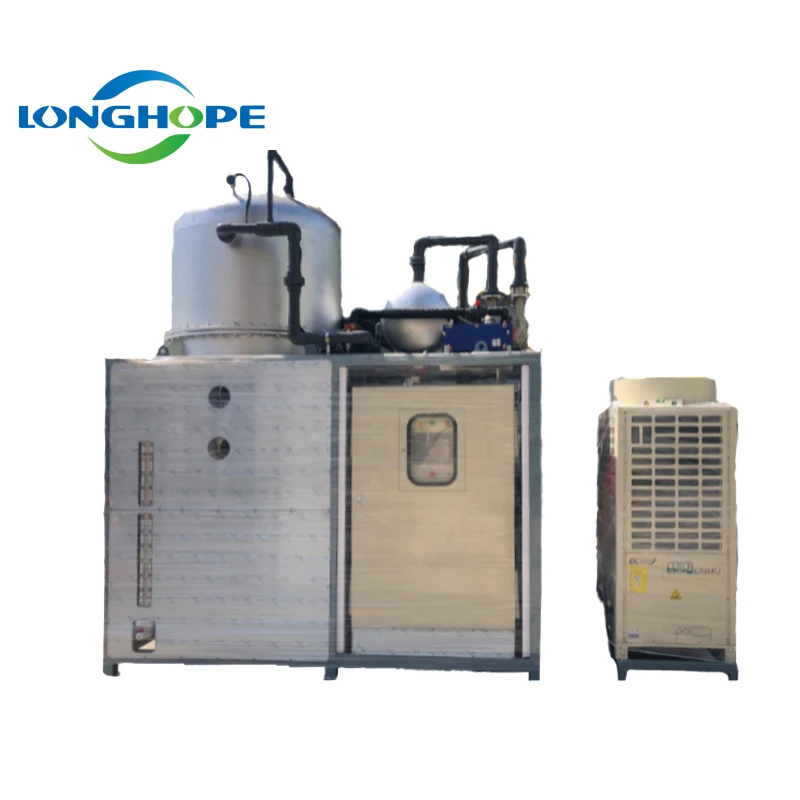
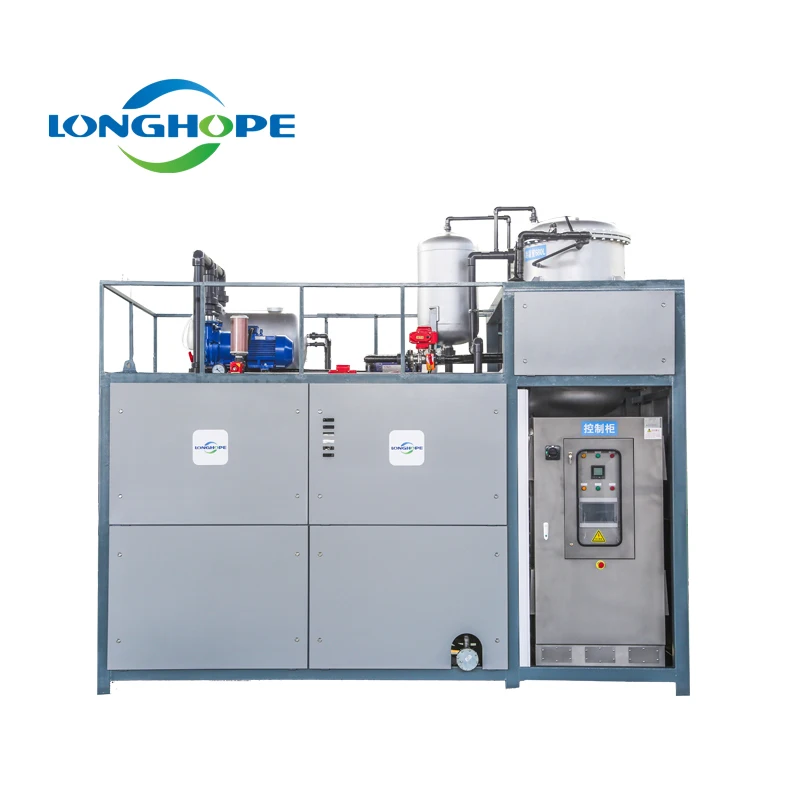
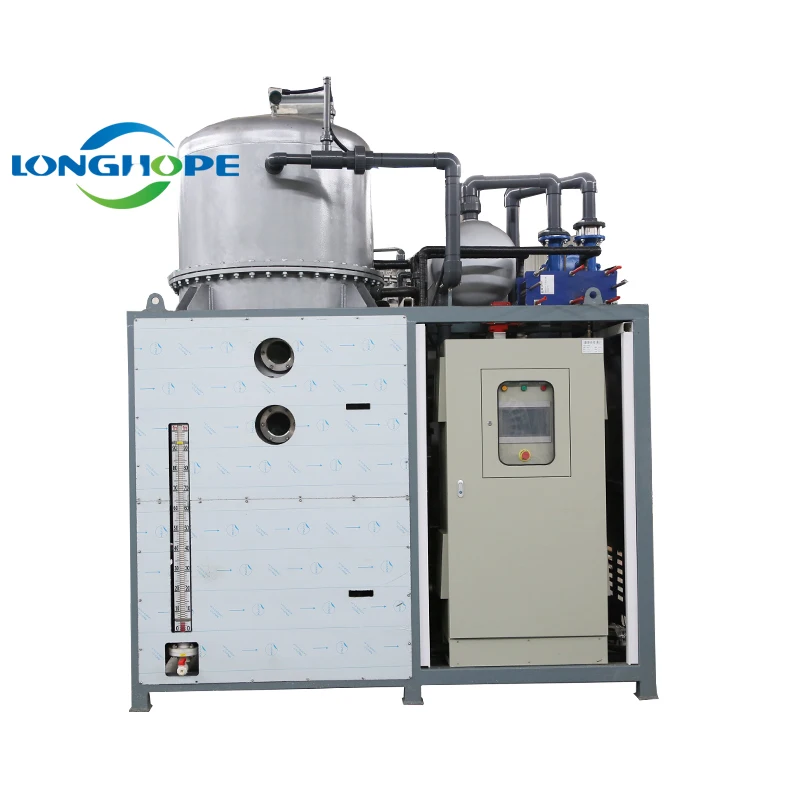
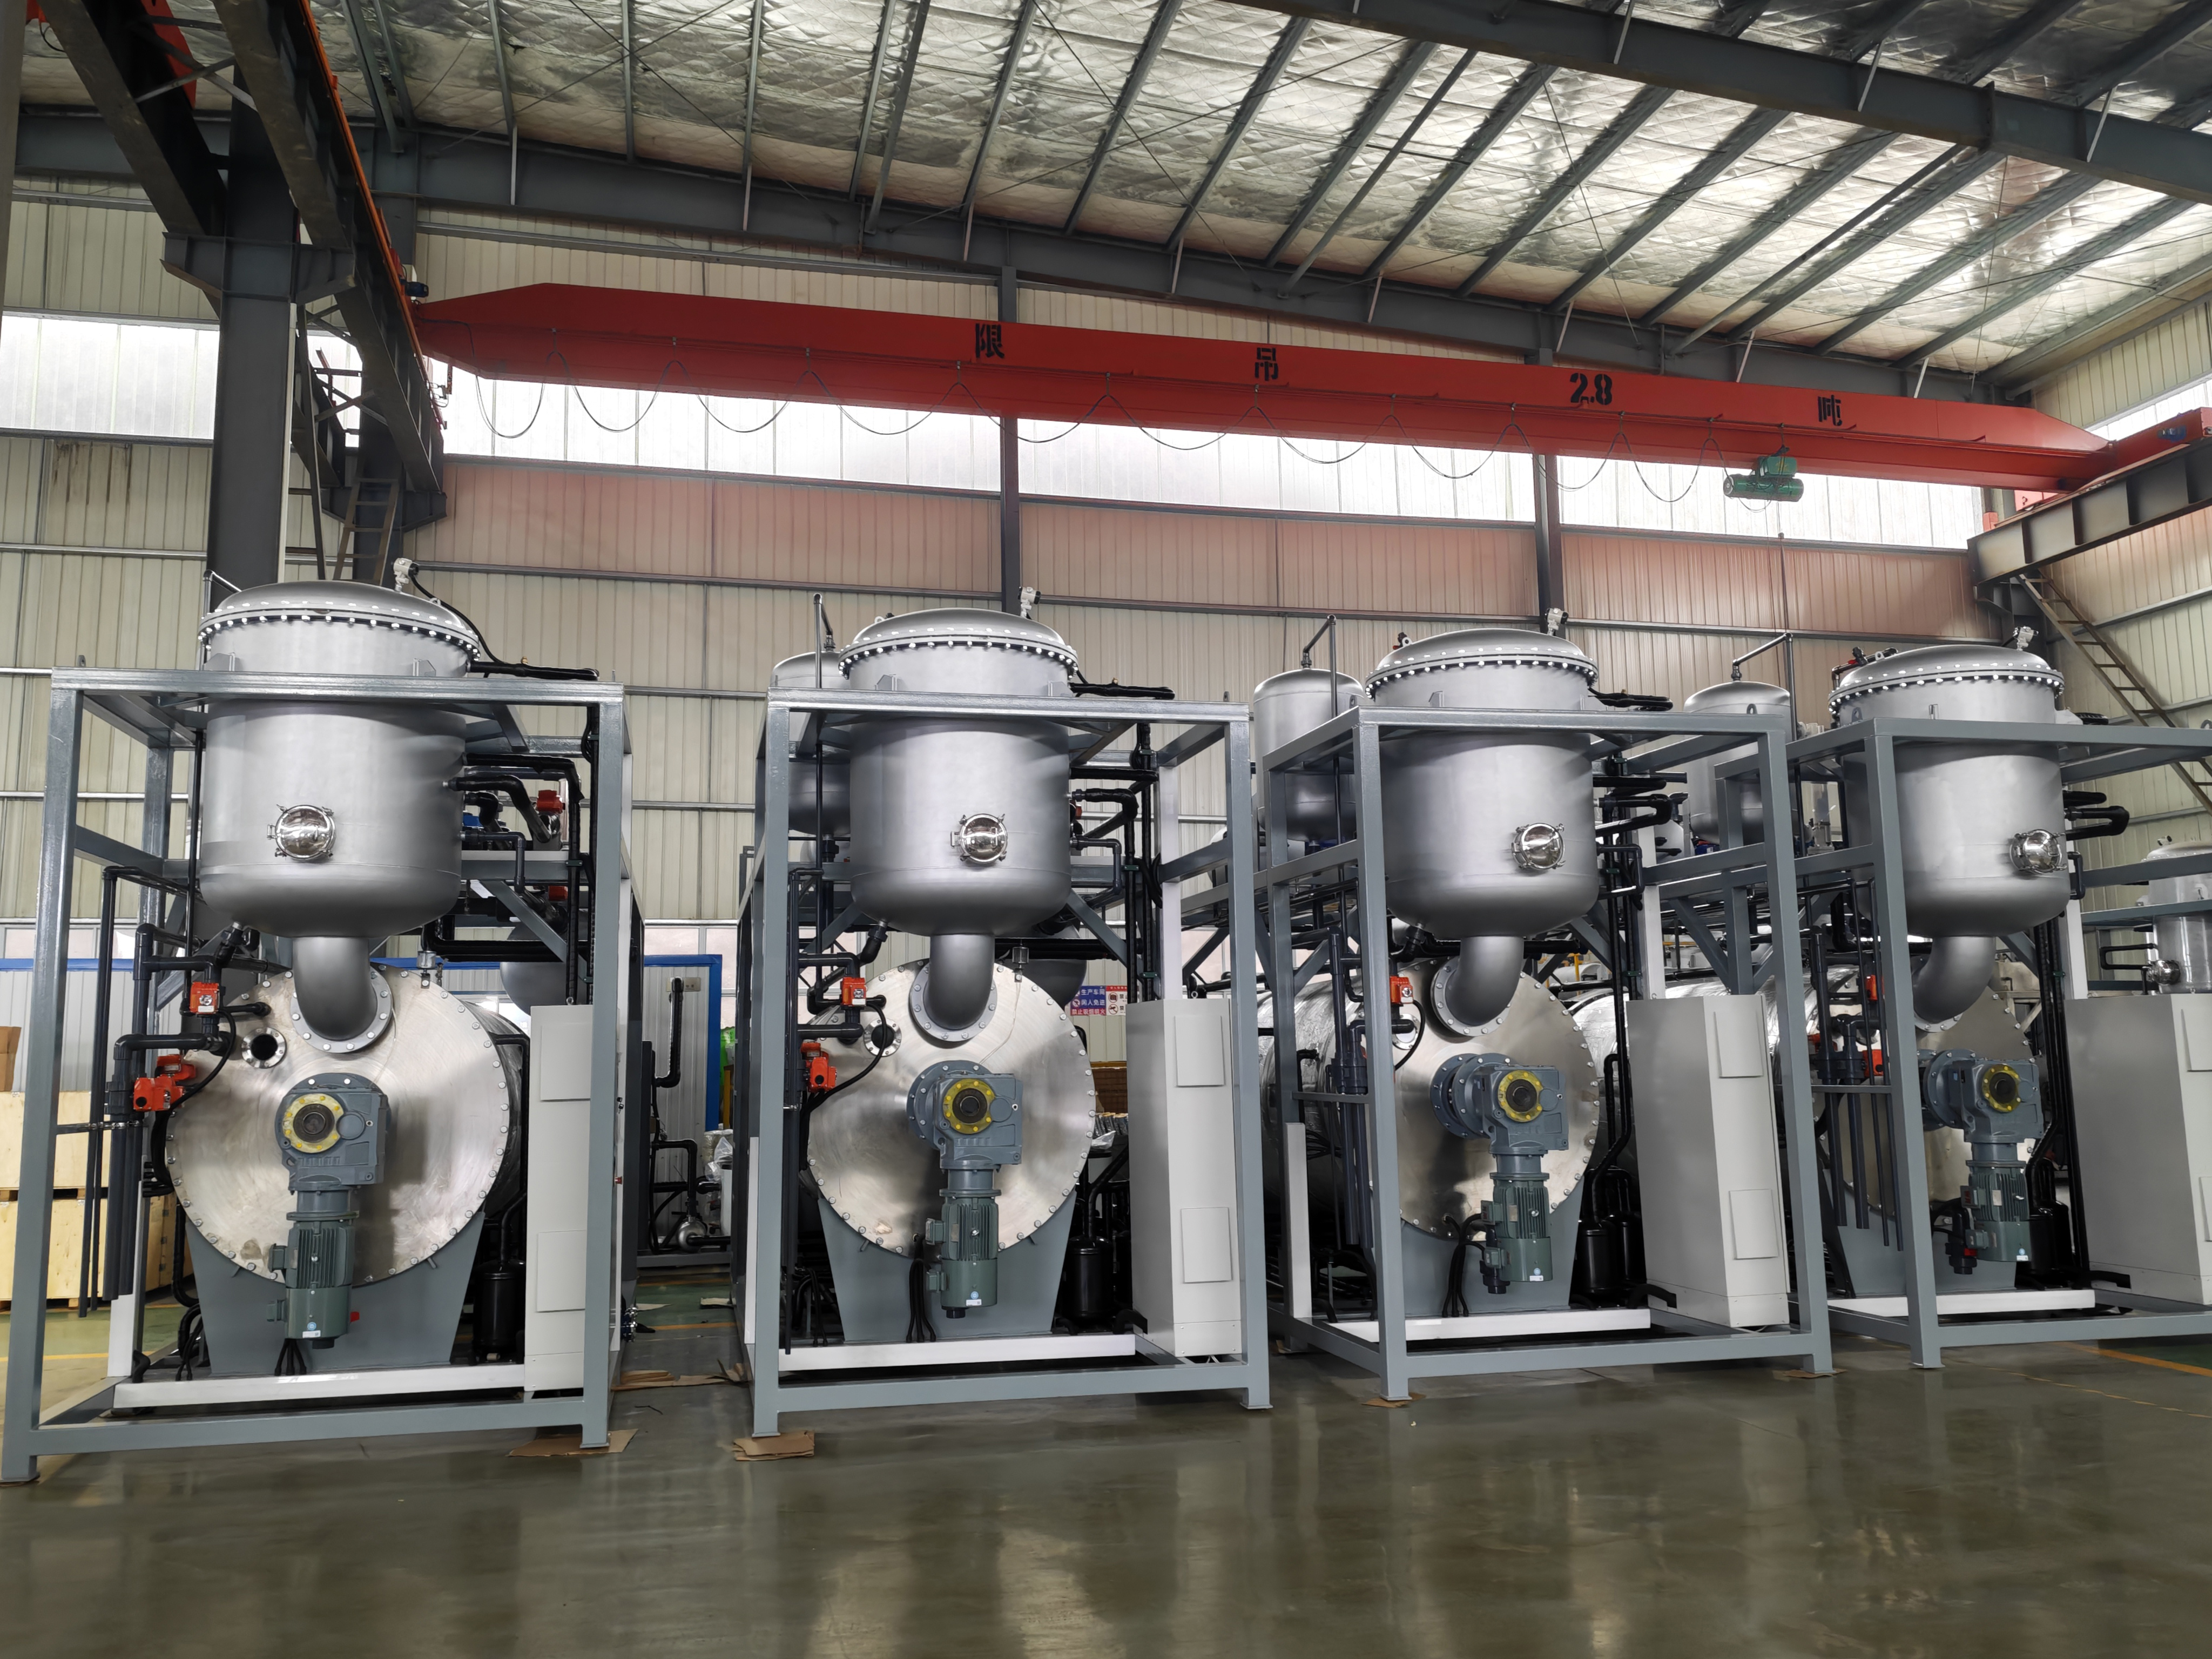
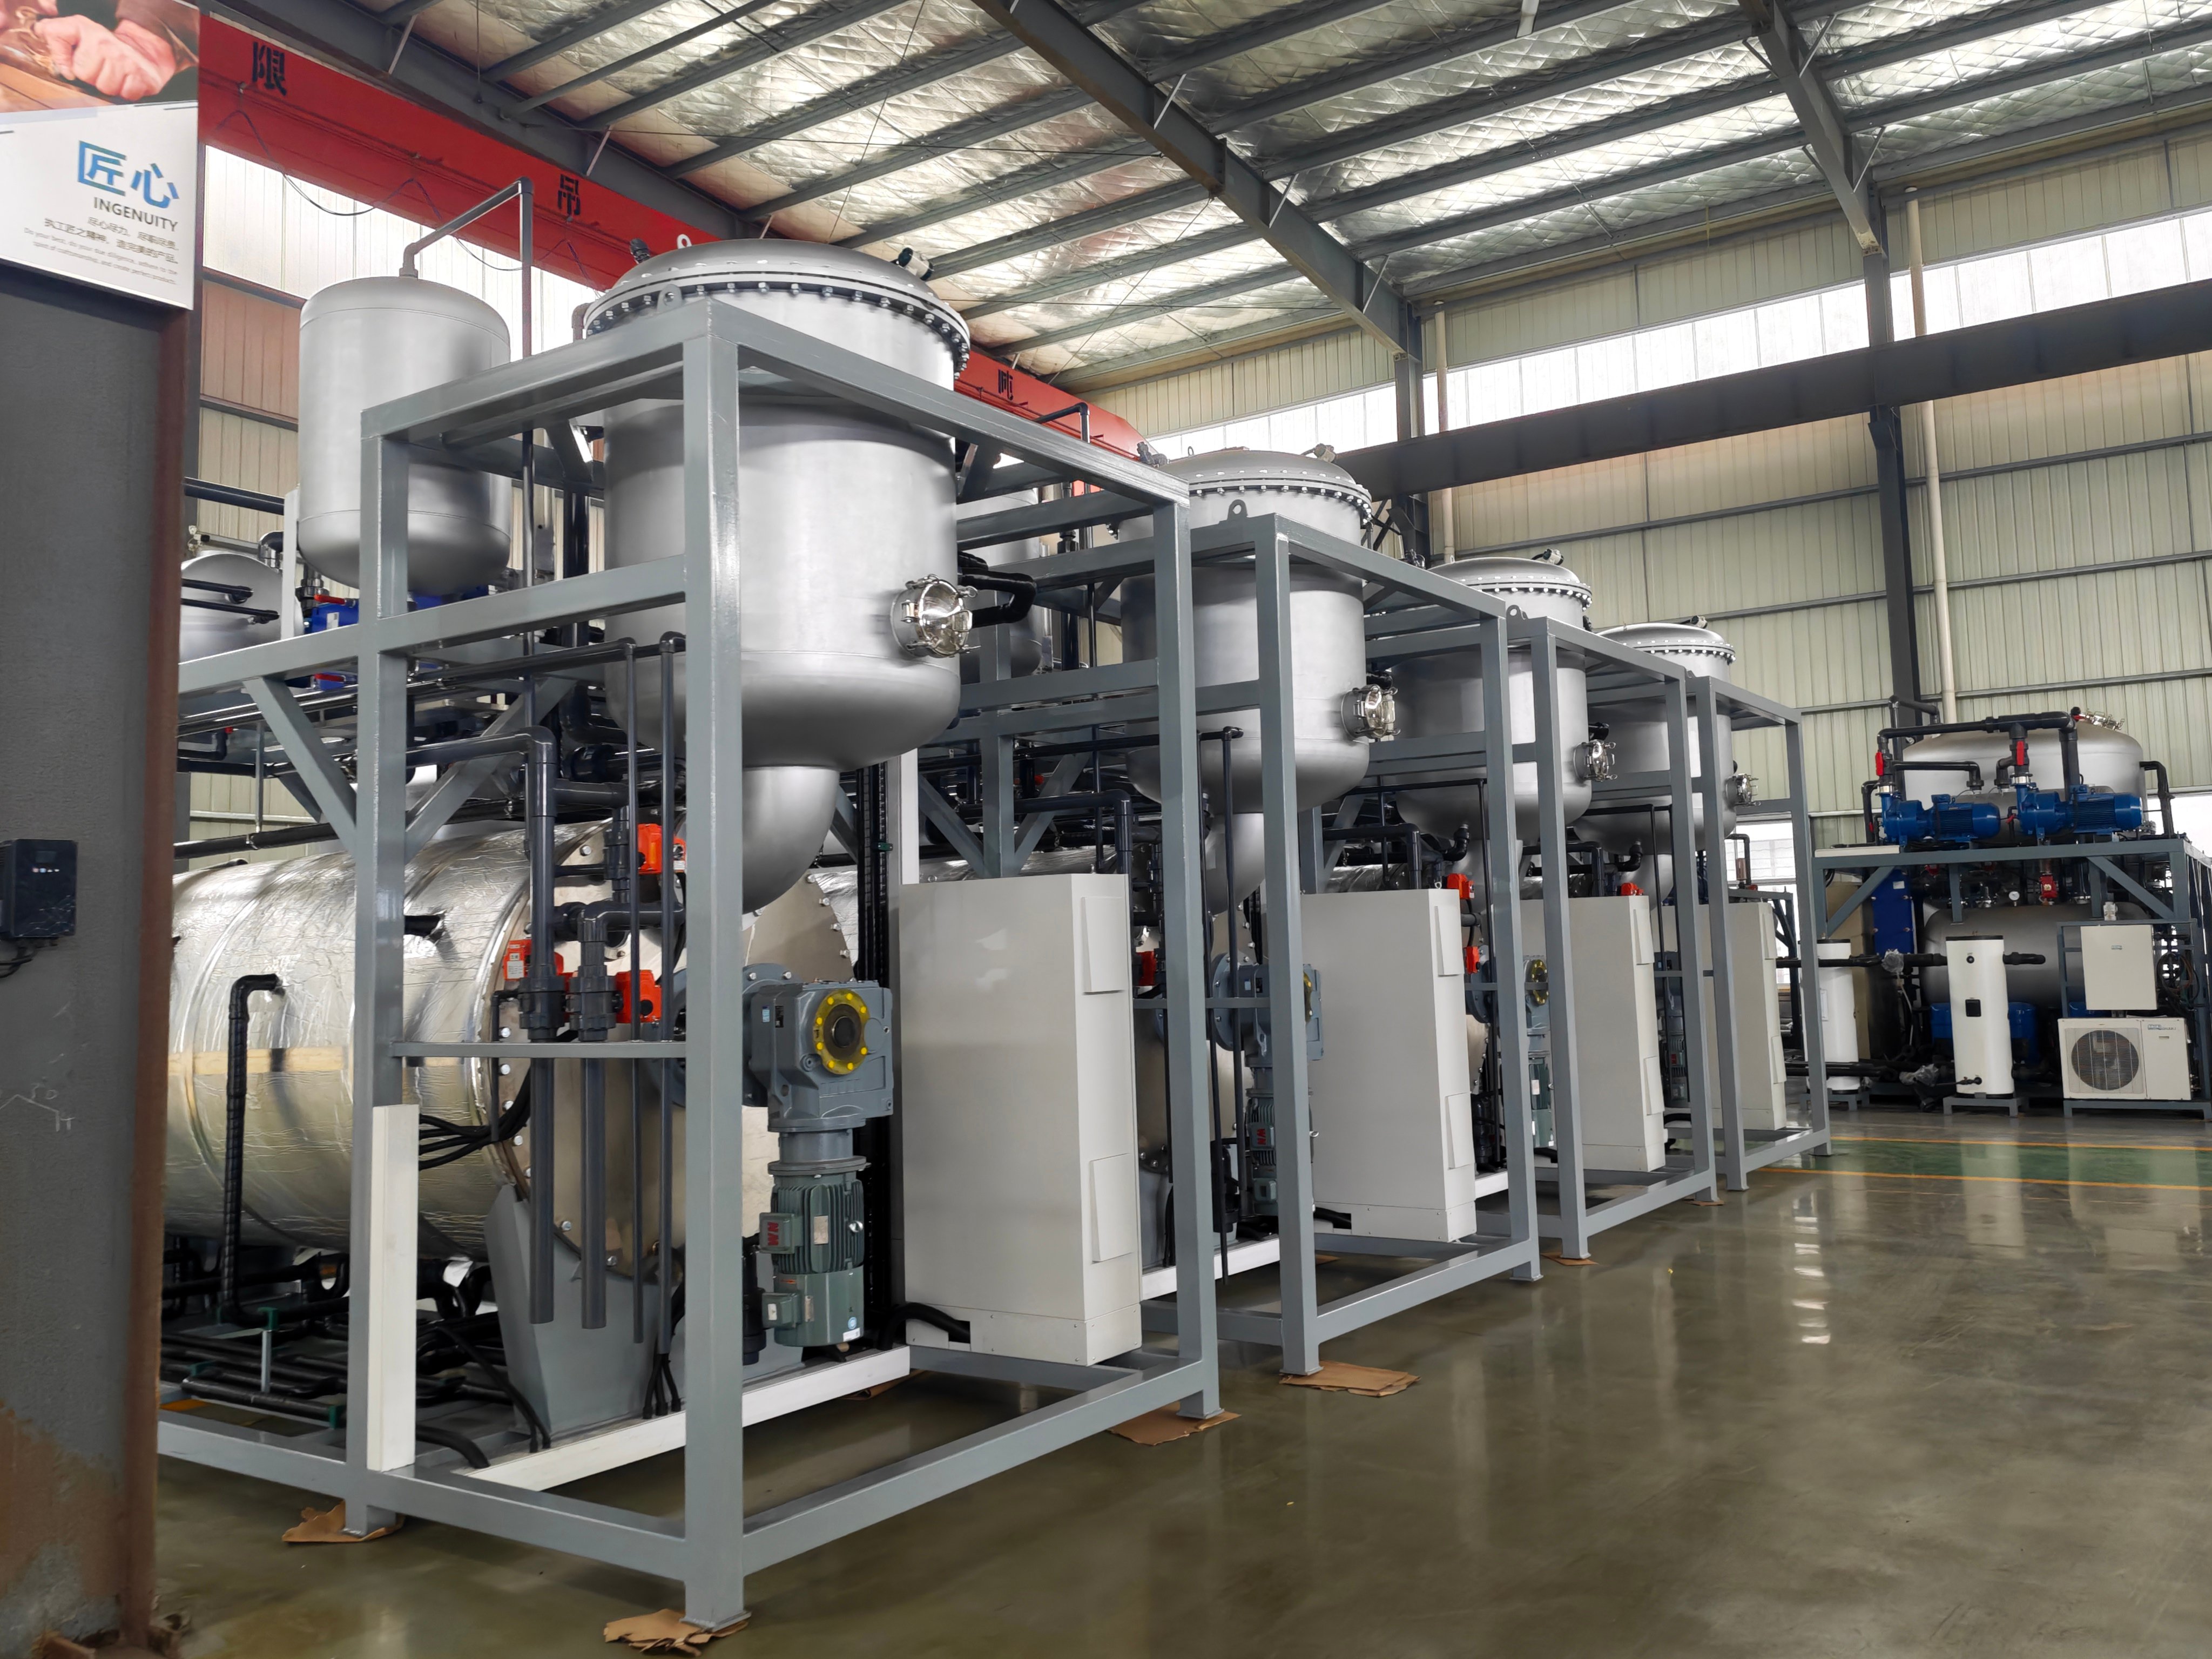
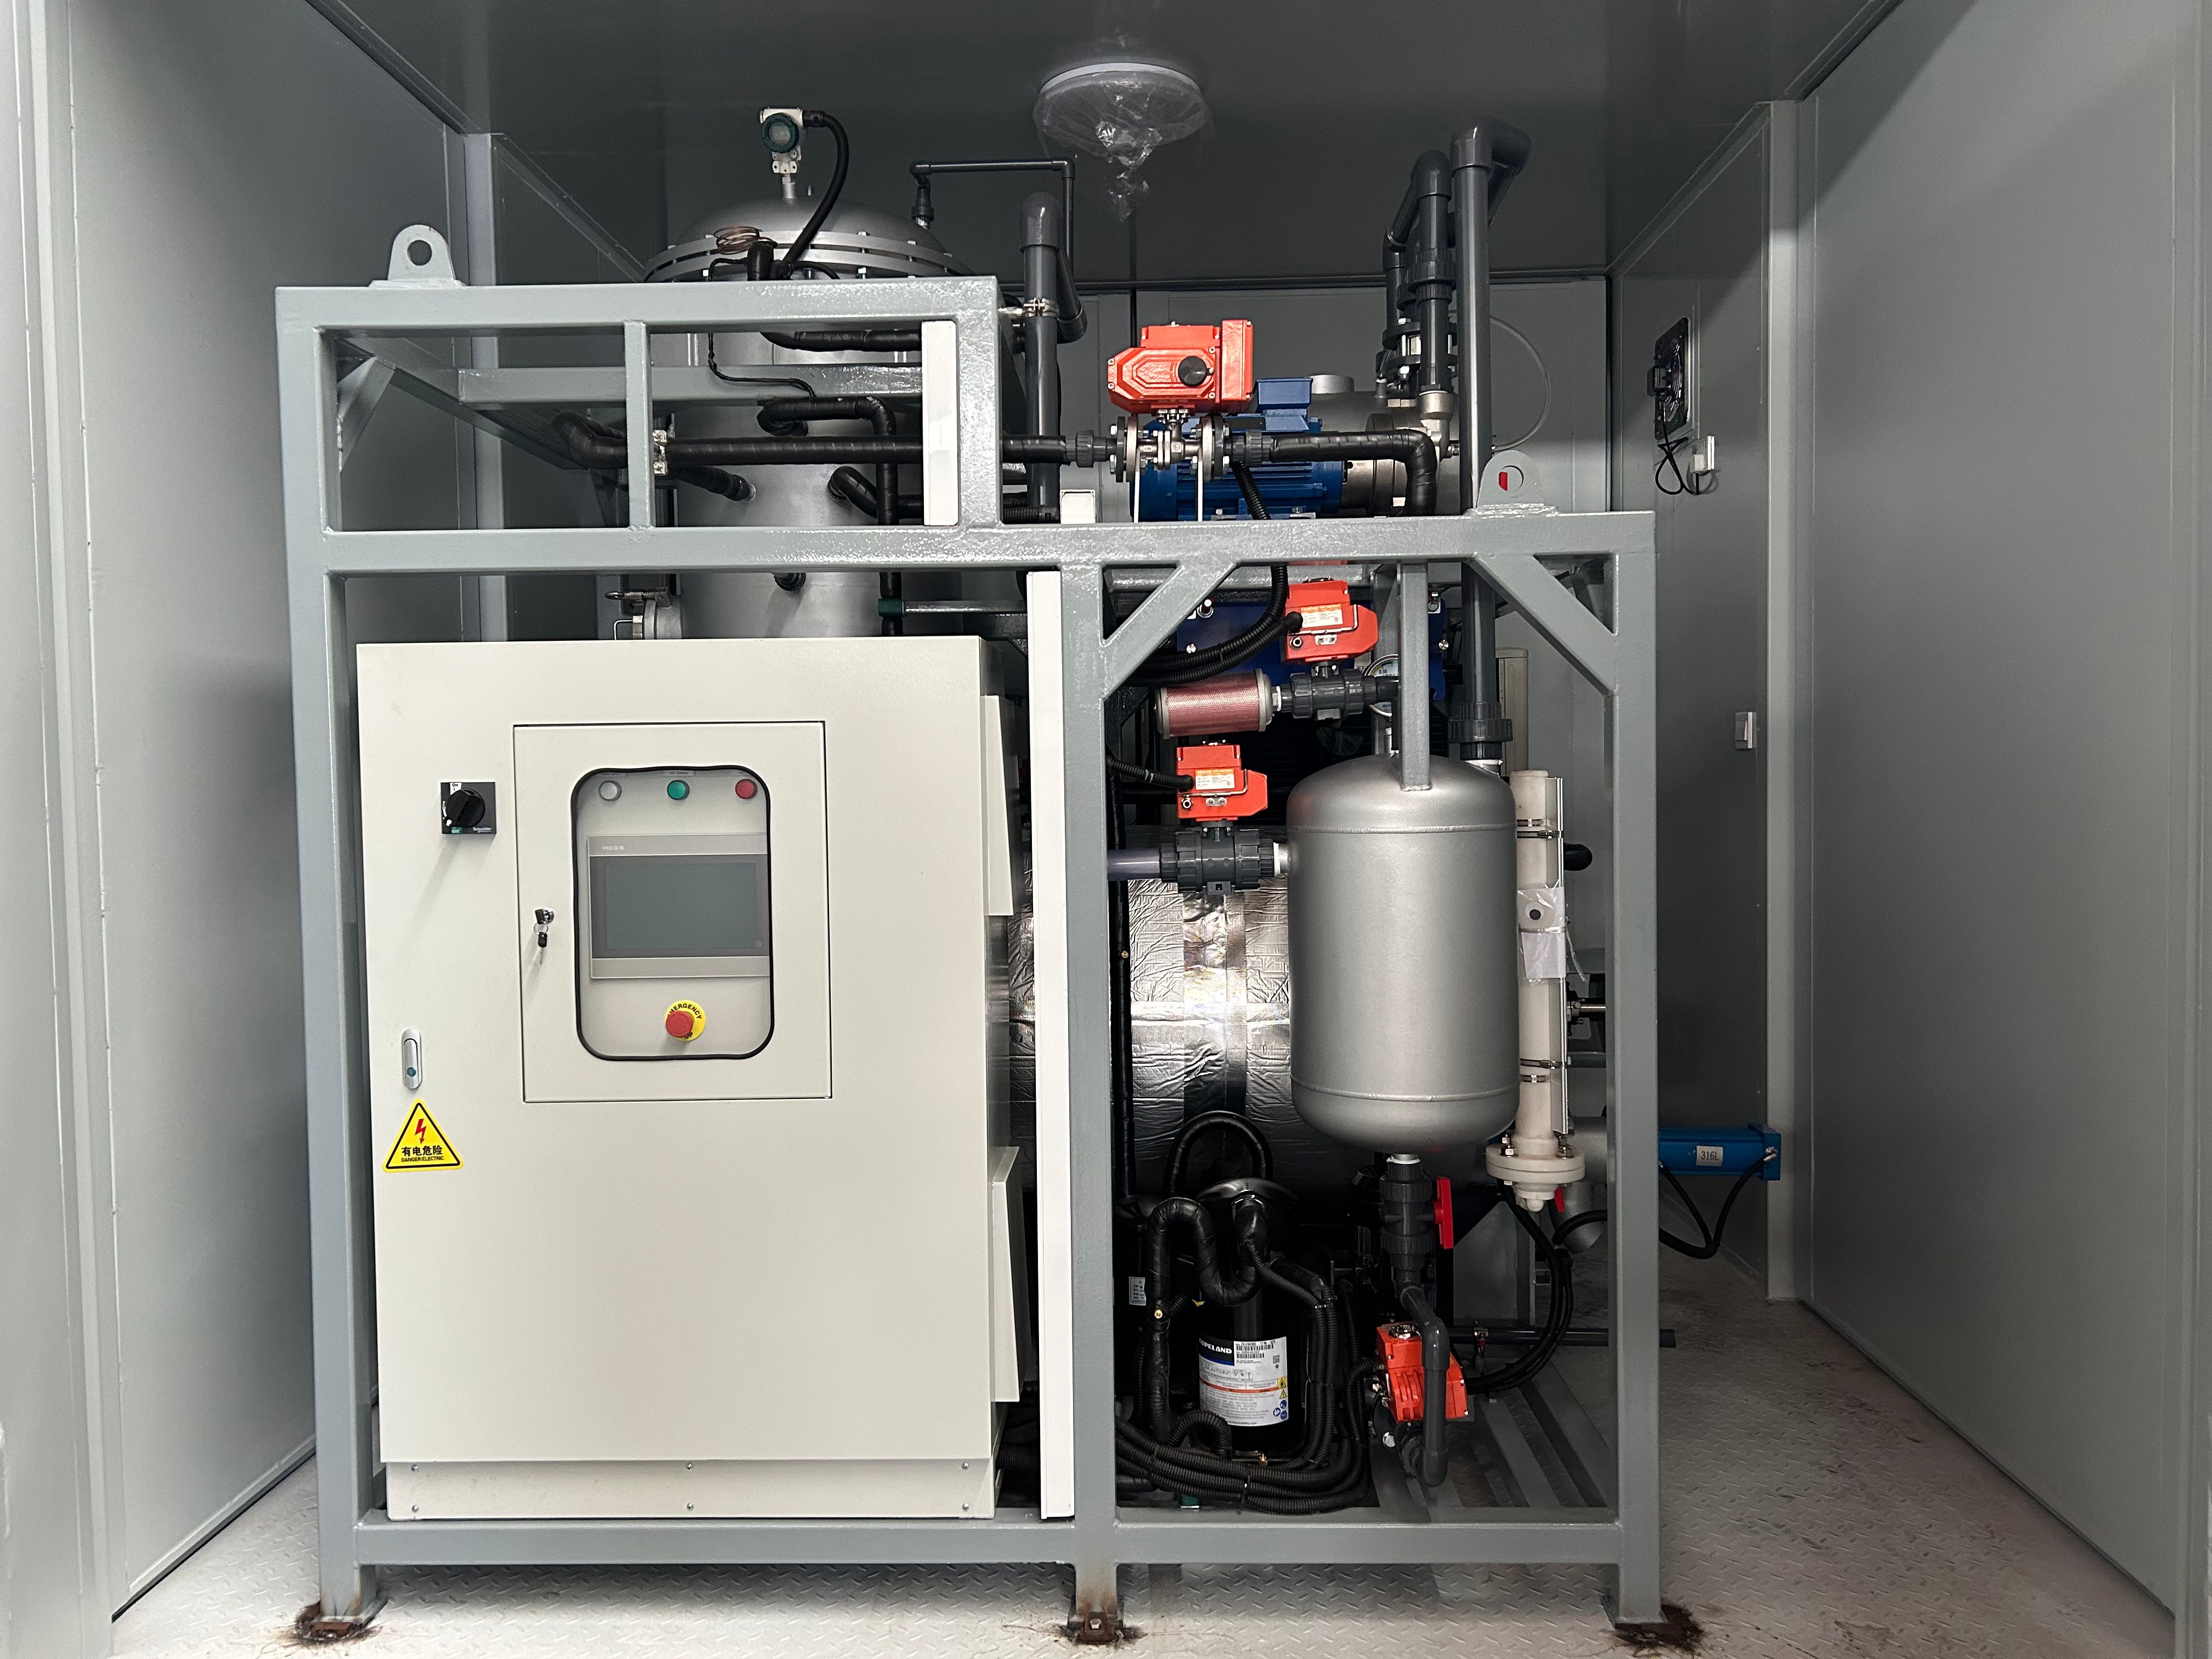
A heat pump crystallizer represents an innovative industrial solution that combines advanced thermal management with crystallization technology. This equipment operates by utilizing heat pump principles to control temperature precisely during the crystallization process, enabling efficient separation and purification of chemical compounds. The heat pump crystallizer functions by extracting heat from a solution and redeploying it strategically to manage crystallization conditions. This dual-function approach makes the heat pump crystallizer particularly effective for temperature-sensitive materials that require strict thermal control. The system removes solvent through evaporation while simultaneously cooling the mother liquor, promoting crystal formation. Key technological features of a heat pump crystallizer include advanced refrigeration cycles, integrated temperature sensors, and automated control systems. These components work together to maintain optimal crystallization environments. The heat pump crystallizer operates at reduced energy consumption compared to conventional methods because it recycles thermal energy rather than dissipating it. Applications for the heat pump crystallizer span multiple industries, including pharmaceuticals, chemicals, food processing, and specialty materials manufacturing. Industries benefit from using a heat pump crystallizer when they need to produce high-purity crystals, reduce operational costs, or minimize environmental impact. The heat pump crystallizer proves especially valuable in producing temperature-dependent compounds where precision matters significantly. Its versatility makes it suitable for both laboratory-scale and industrial-scale operations, addressing diverse crystallization challenges across sectors.

New Product Releases

The heat pump crystallizer delivers substantial practical benefits that transform industrial crystallization operations. First, this technology significantly reduces energy consumption compared to traditional crystallization methods. By recycling waste heat through the heat pump crystallizer system, companies achieve lower utility bills and reduced carbon footprints simultaneously. Operational efficiency represents another critical advantage of employing a heat pump crystallizer. The equipment maintains precise temperature control automatically, eliminating manual adjustments and reducing human error. Operators benefit from consistent crystal quality because the heat pump crystallizer delivers uniform thermal conditions throughout the process cycle. Cost savings extend beyond energy reduction when using a heat pump crystallizer. Improved product yields mean less material waste, translating directly to higher profitability. The heat pump crystallizer also requires less frequent maintenance than conventional systems, reducing downtime and service expenses. For pharmaceutical and chemical manufacturers, the heat pump crystallizer offers unmatched application suitability. Products requiring strict temperature control benefit tremendously because the heat pump crystallizer maintains precise conditions automatically. Complex compounds that previously required expensive cooling systems now become economically viable to produce. Scalability represents a decision-useful advantage of investing in a heat pump crystallizer. Whether processing small research batches or large commercial quantities, the heat pump crystallizer adapts to meet production demands. Environmental compliance improves substantially because this technology minimizes emissions and reduces water consumption. From a buyer perspective, the heat pump crystallizer justifies its initial investment through rapid payback periods. Companies typically recover costs within two to three years through energy savings alone. The heat pump crystallizer ultimately enables businesses to compete more effectively while meeting sustainability objectives and regulatory requirements.

Tips And Tricks

Vacuum Distillation vs Traditional Distillation Methods

24

Jul

Vacuum Distillation vs Traditional Distillation Methods

Vacuum distillation and traditional distillation methods represent two distinct approaches to separating liquid mixtures through controlled evaporation and condensation. Understanding the differences between vacuum distillation and traditional distil...
View More
Top 5 Evaporator System Design Features for Industry

24

Jul

Top 5 Evaporator System Design Features for Industry

Selecting the right evaporator system design is critical for industrial operations managing wastewater treatment, chemical processing, and liquid concentration challenges. An effective evaporator system design determines not only operational efficien...
View More
Evaporator System Maintenance: Tips for Longevity

24

Jul

Evaporator System Maintenance: Tips for Longevity

Evaporator system maintenance is critical to ensuring your industrial cooling and waste-water treatment equipment operates reliably and efficiently over the long term. Whether your facility relies on evaporator systems for refrigeration, heat exchang...
View More
Choosing the Right Evaporator System for Your Plant

24

Jul

Choosing the Right Evaporator System for Your Plant

Selecting an evaporator system for your industrial plant is one of the most critical decisions you will make in your facility's operational strategy. An evaporator system directly impacts energy consumption, product quality, waste management efficien...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

heat pump crystallizer

Energy-Efficient Heat Recovery Technology

Energy-Efficient Heat Recovery Technology

The heat pump crystallizer incorporates sophisticated heat recovery systems that capture thermal energy typically wasted in conventional crystallization processes. This innovative approach makes the heat pump crystallizer remarkably efficient, reducing overall energy consumption by up to sixty percent compared to traditional methods. Rather than simply discarding cooling or heating waste, the heat pump crystallizer redirects this energy back into the process cycle. This closed-loop thermal management means your operation consumes significantly less electricity while maintaining perfect crystallization conditions. For manufacturers processing large volumes, this efficiency translates into substantial annual savings. The heat pump crystallizer pays dividends immediately through reduced utility expenses. Companies implementing this technology consistently report impressive return-on-investment figures. The environmental benefits prove equally compelling, as decreased energy demand directly reduces your facility's carbon footprint and supports corporate sustainability initiatives.
Precise Temperature Control and Consistency

Precise Temperature Control and Consistency

The heat pump crystallizer delivers unparalleled precision in temperature management, a critical factor determining crystal quality and product purity. Advanced sensors integrated throughout the heat pump crystallizer system monitor conditions continuously, making real-time adjustments automatically. This sophisticated control means operators never experience temperature fluctuations that compromise product quality. The heat pump crystallizer maintains setpoint accuracy within fractions of a degree, enabling consistent batch-to-batch results. For pharmaceutical companies requiring stringent quality standards, this precision proves invaluable. The heat pump crystallizer eliminates variability that often occurs with manual temperature management. Your production team can focus on other critical tasks while the heat pump crystallizer handles thermal regulation independently. This consistent performance reduces rejected batches, waste material, and production delays significantly.
Versatile Applications Across Multiple Industries

Versatile Applications Across Multiple Industries

The heat pump crystallizer demonstrates remarkable adaptability, making it suitable for diverse industrial applications and processing challenges. Pharmaceutical manufacturers use the heat pump crystallizer to produce active pharmaceutical ingredients with consistent purity levels. Chemical processors employ the heat pump crystallizer for specialty compound manufacturing where temperature sensitivity demands precision. Food industry applications showcase how the heat pump crystallizer handles delicate products requiring careful thermal handling. Specialty materials manufacturers benefit from the heat pump crystallizer's ability to process complex compounds previously considered economically unfeasible. The heat pump crystallizer works equally effectively whether scaling from laboratory research to full commercial production. This versatility eliminates the need for multiple specialized equipment purchases. Investment in a single heat pump crystallizer system addresses varied processing needs across your facility. Companies gain significant competitive advantages through this flexible technology platform that evolves with their changing production requirements.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000