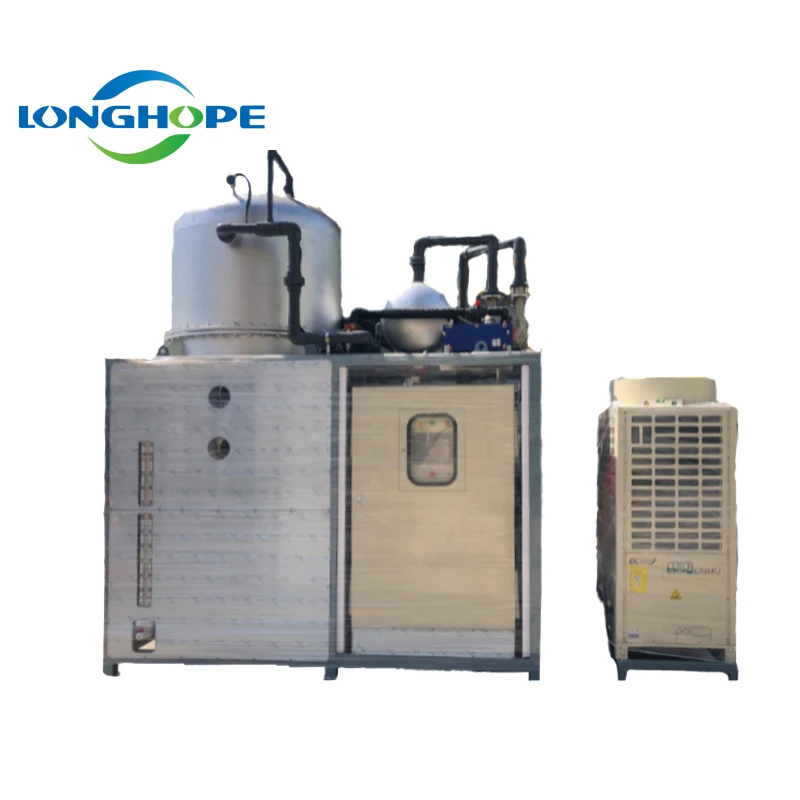
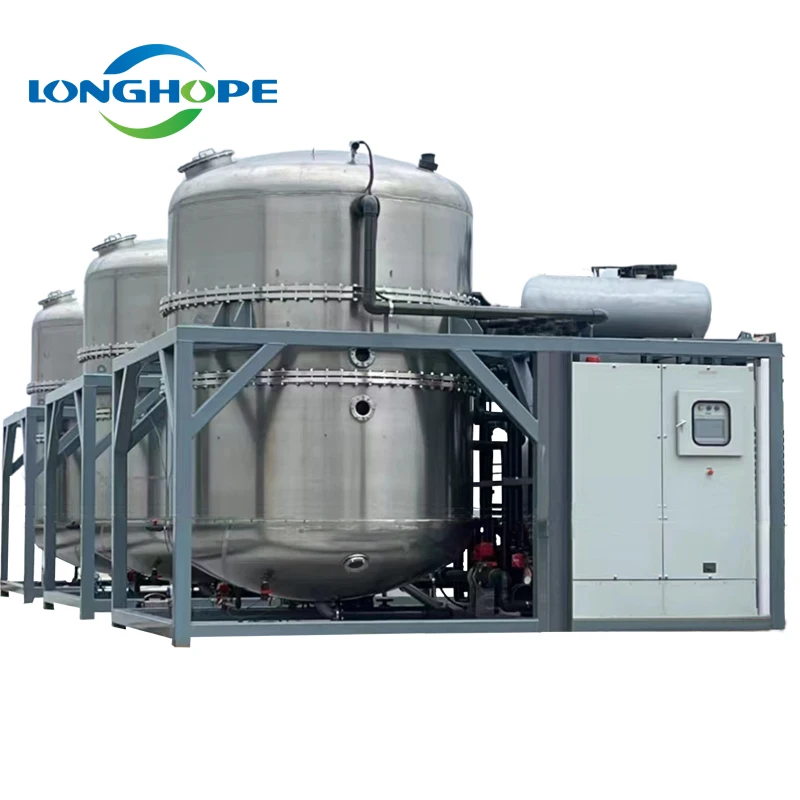
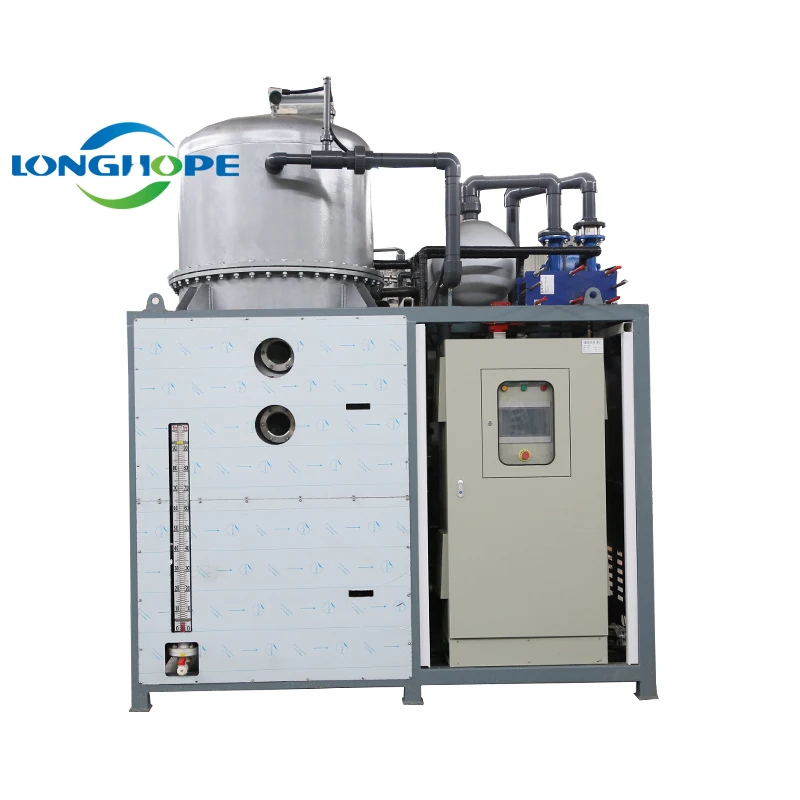
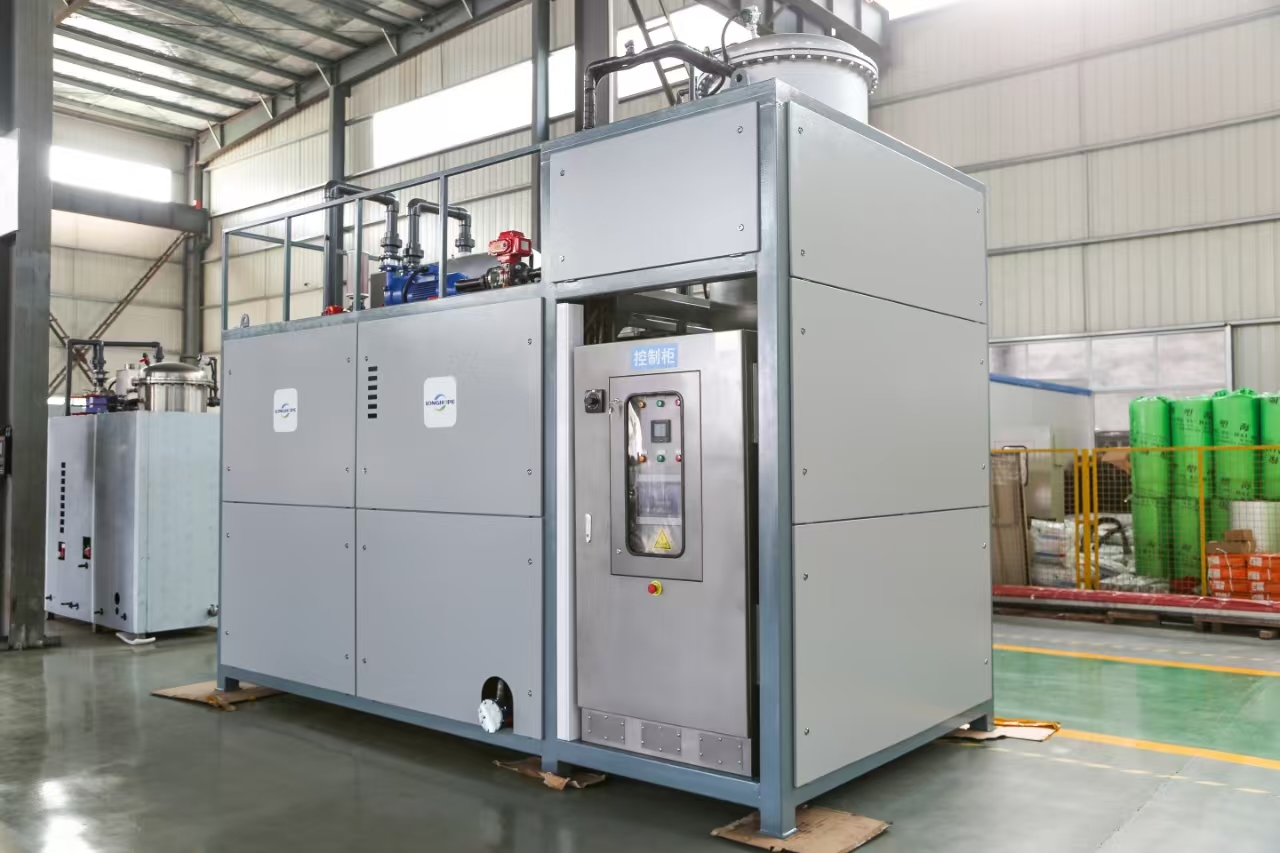
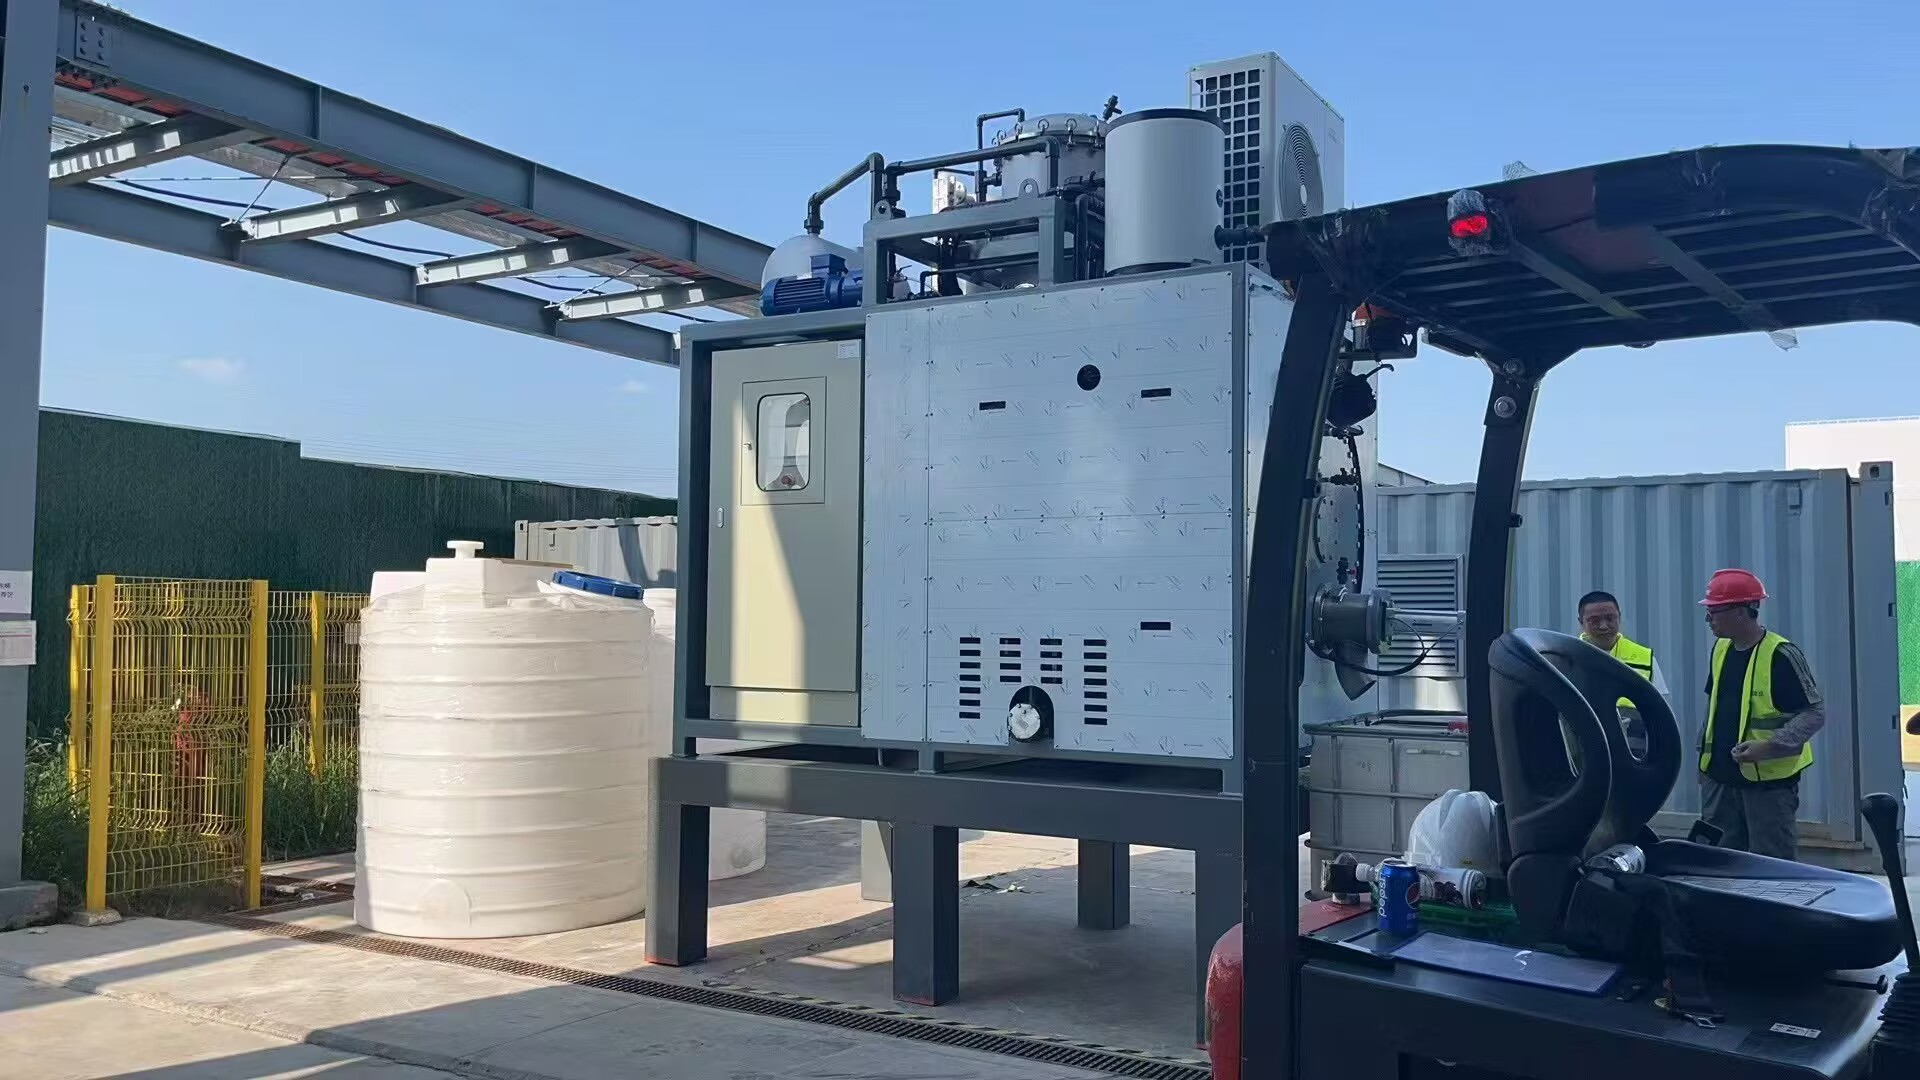
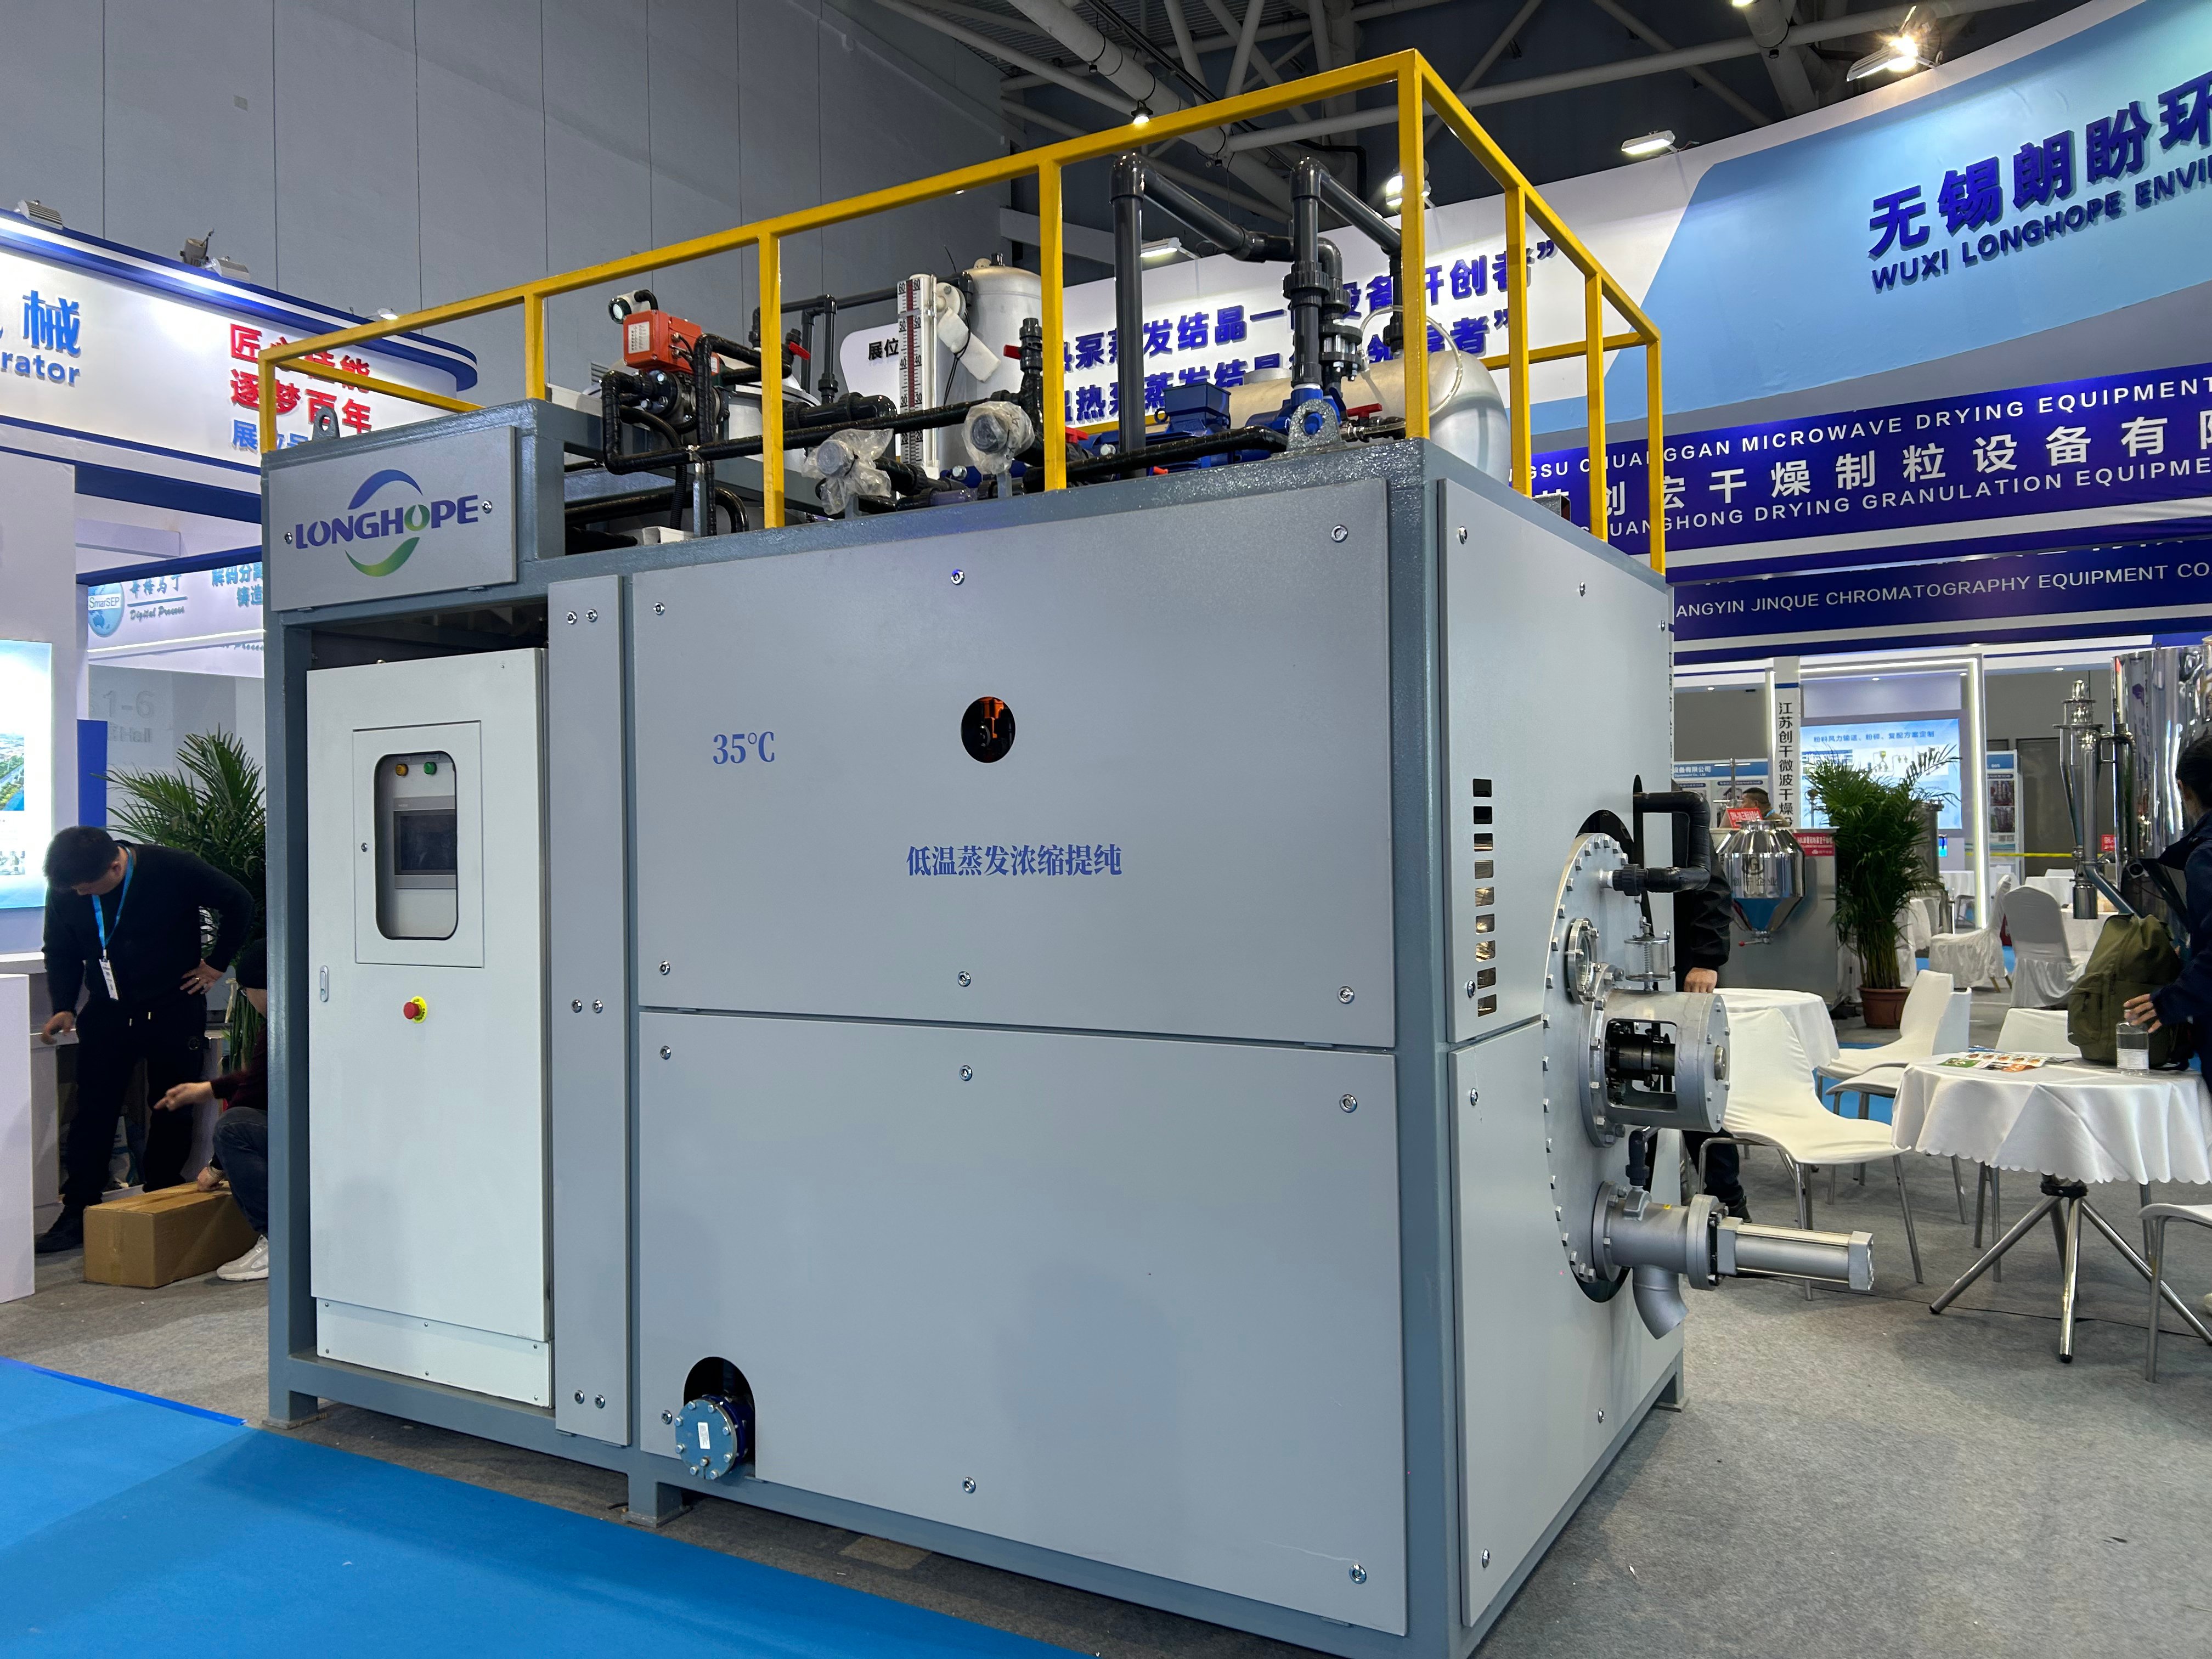
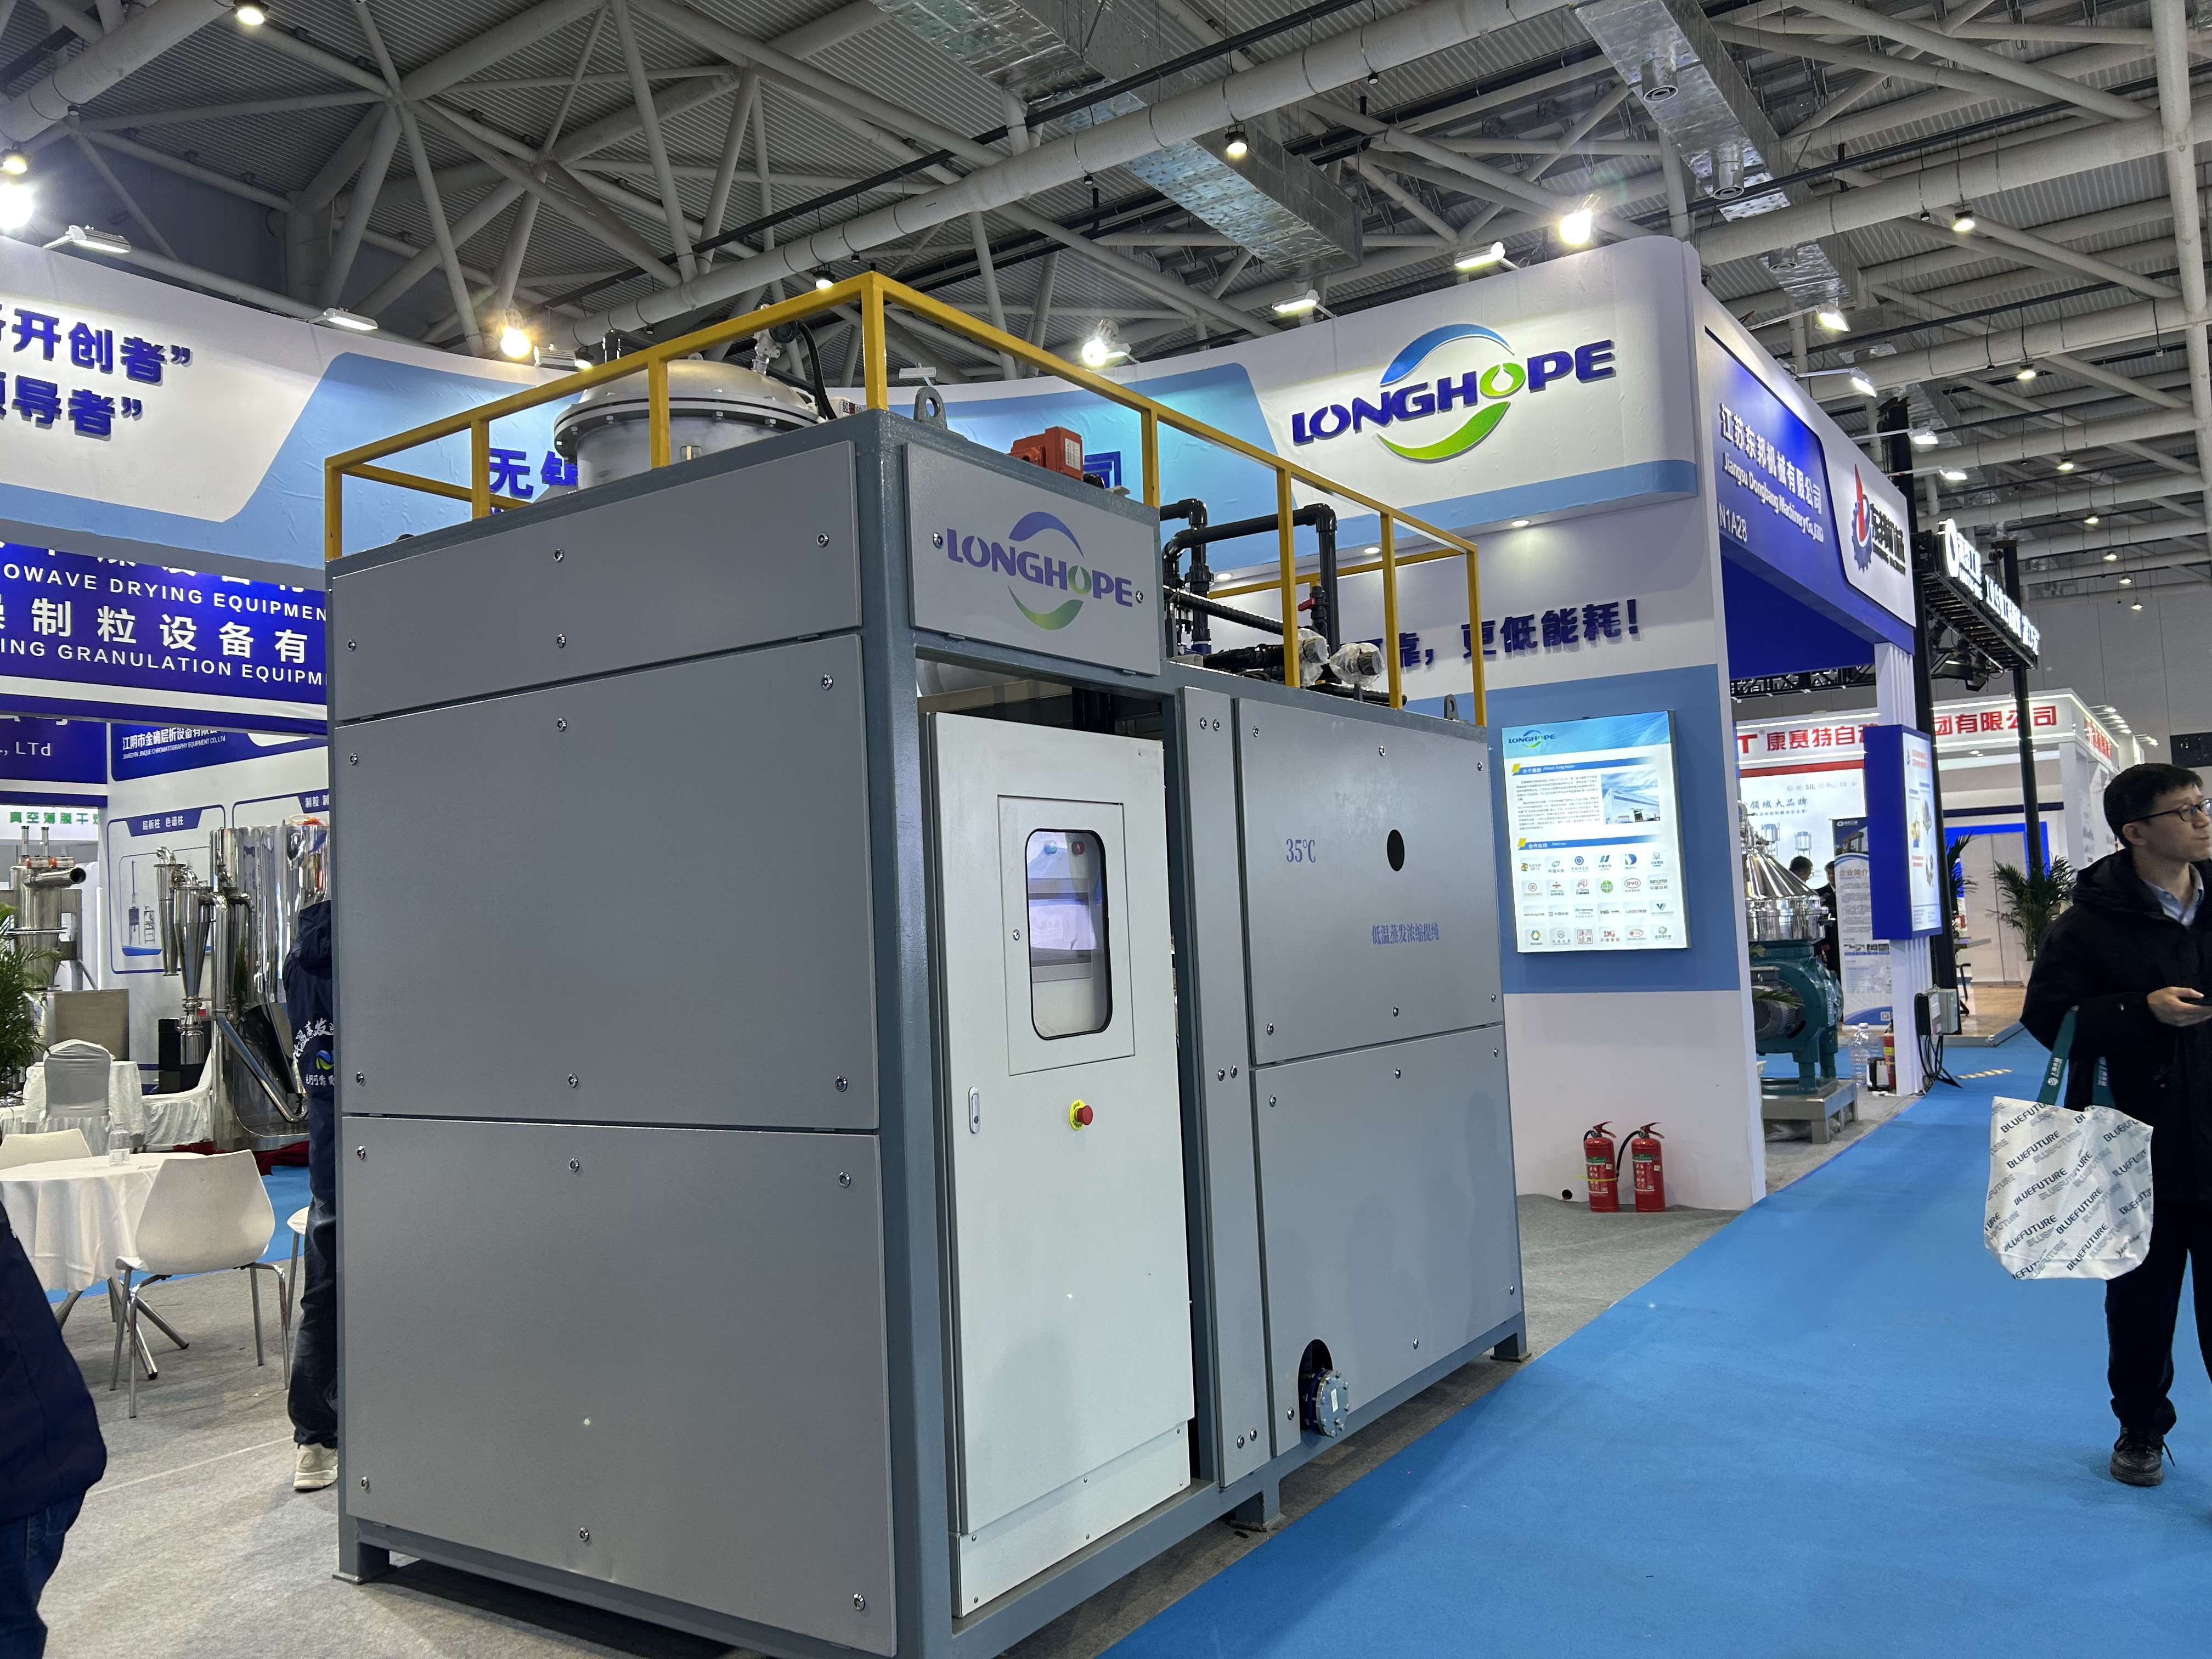
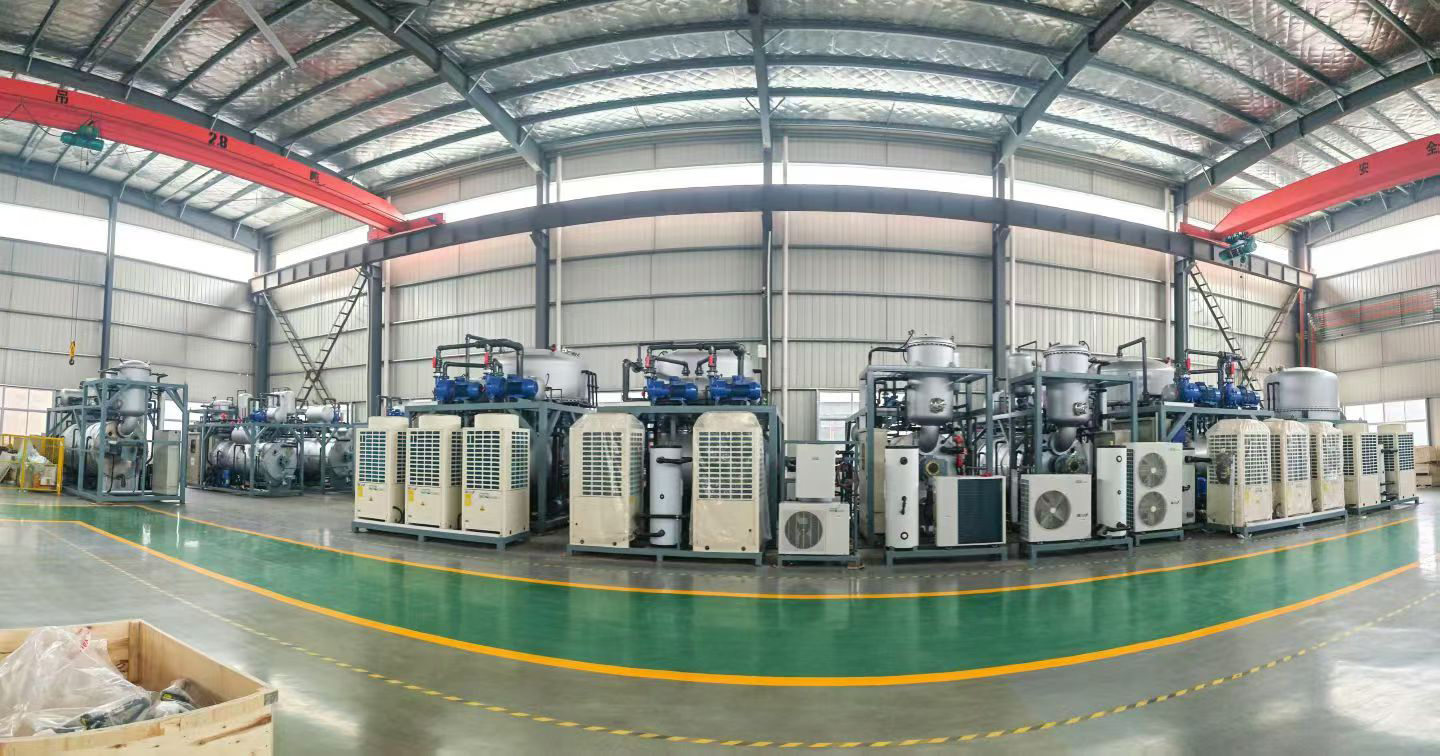
industrial crystallization equipment
Industrial crystallization equipment represents a cornerstone technology in modern manufacturing processes, designed to separate dissolved solids from liquid solutions through controlled crystal formation. This specialized machinery plays a vital role across pharmaceutical, chemical, food, and agricultural industries, enabling precise control over crystal size, purity, and yield.
The primary function of industrial crystallization equipment is to facilitate the transition of dissolved substances into solid crystal form under carefully managed conditions. Industrial crystallization equipment achieves this through regulated temperature changes, evaporation, cooling, or precipitation mechanisms. The technology allows manufacturers to recover valuable compounds, purify products, and reduce waste in production cycles.
Key technological features of modern industrial crystallization equipment include advanced temperature control systems, automated monitoring sensors, variable cooling rates, and scalable vessel designs. These systems maintain optimal conditions for crystal growth while preventing unwanted crystal agglomeration. Industrial crystallization equipment utilizes sophisticated mixing mechanisms to ensure uniform distribution and consistent product quality.
Applications of industrial crystallization equipment span numerous sectors. In pharmaceuticals, it produces high-purity active ingredients and excipients. Chemical manufacturers use industrial crystallization equipment to isolate compounds and recover solvents economically. The food industry applies this equipment for sugar refinement, salt production, and specialty ingredient processing. Agricultural sectors benefit from fertilizer crystallization and nutrient recovery.
The versatility and reliability of industrial crystallization equipment make it indispensable for companies seeking efficient separation and purification solutions that meet stringent quality standards and regulatory requirements.

 EN