Vacuum Crystallizer: Industrial Crystallization Equipment

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

vacuum crystallizer

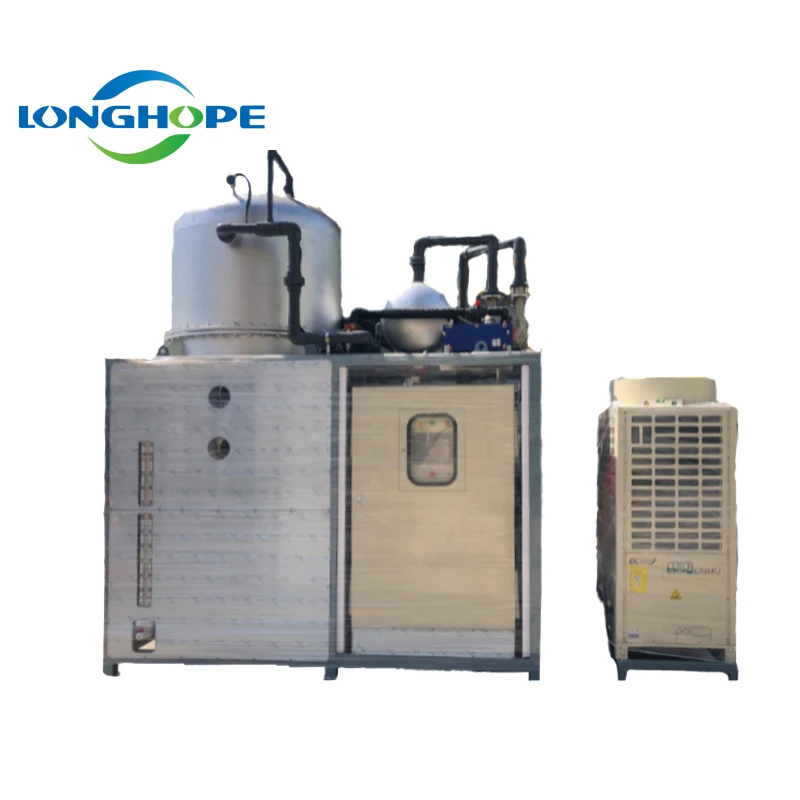
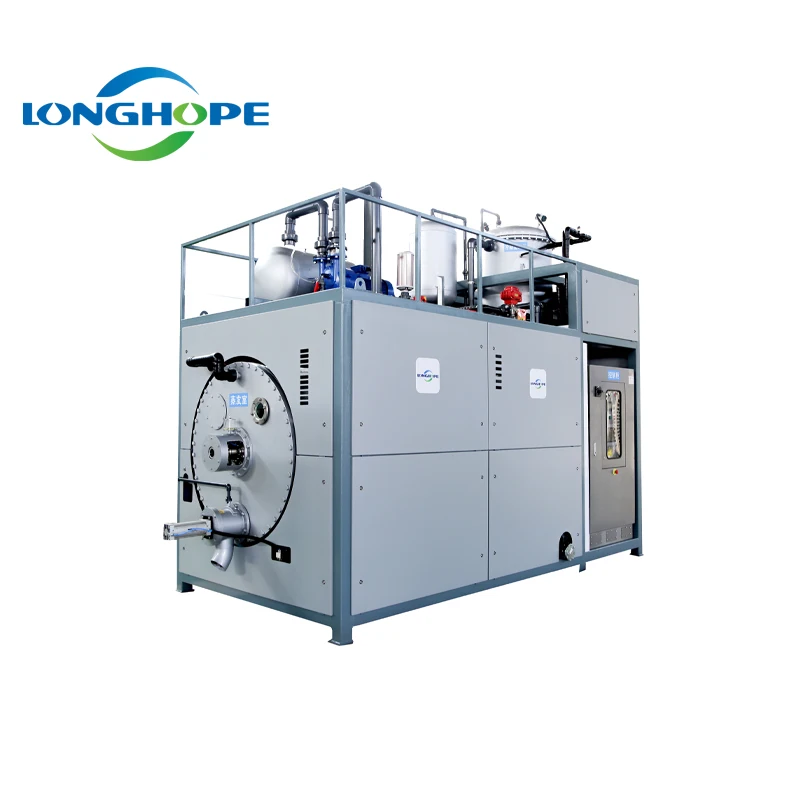
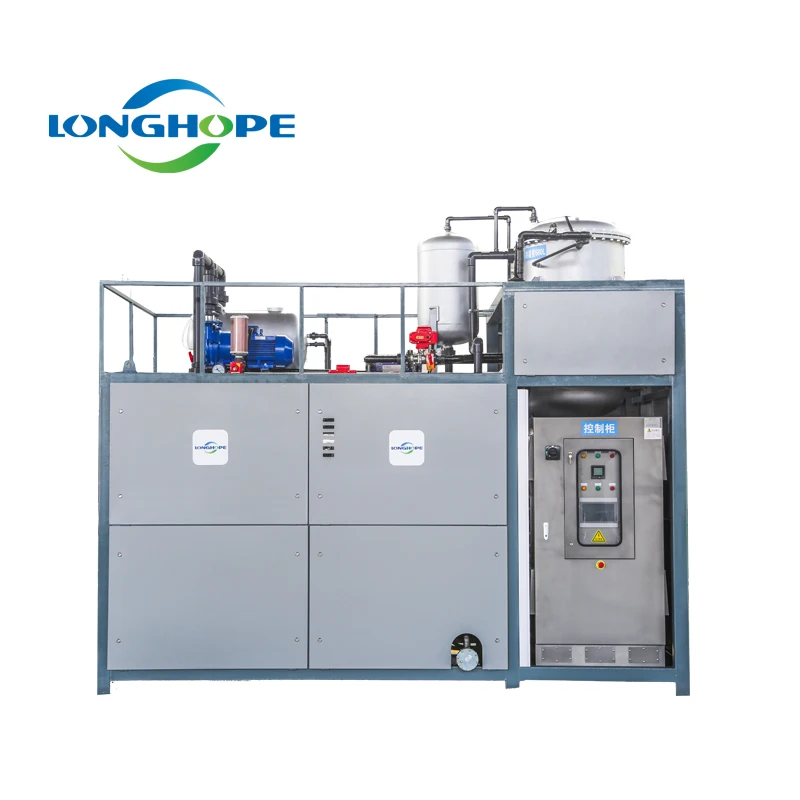
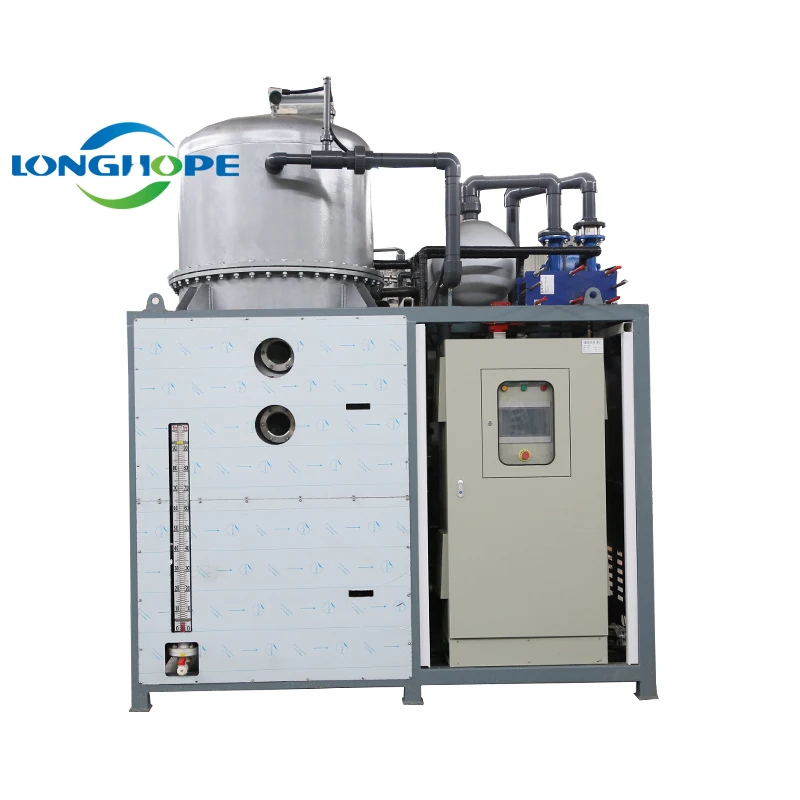
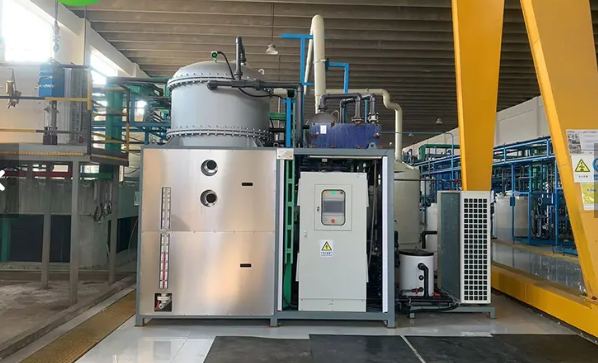
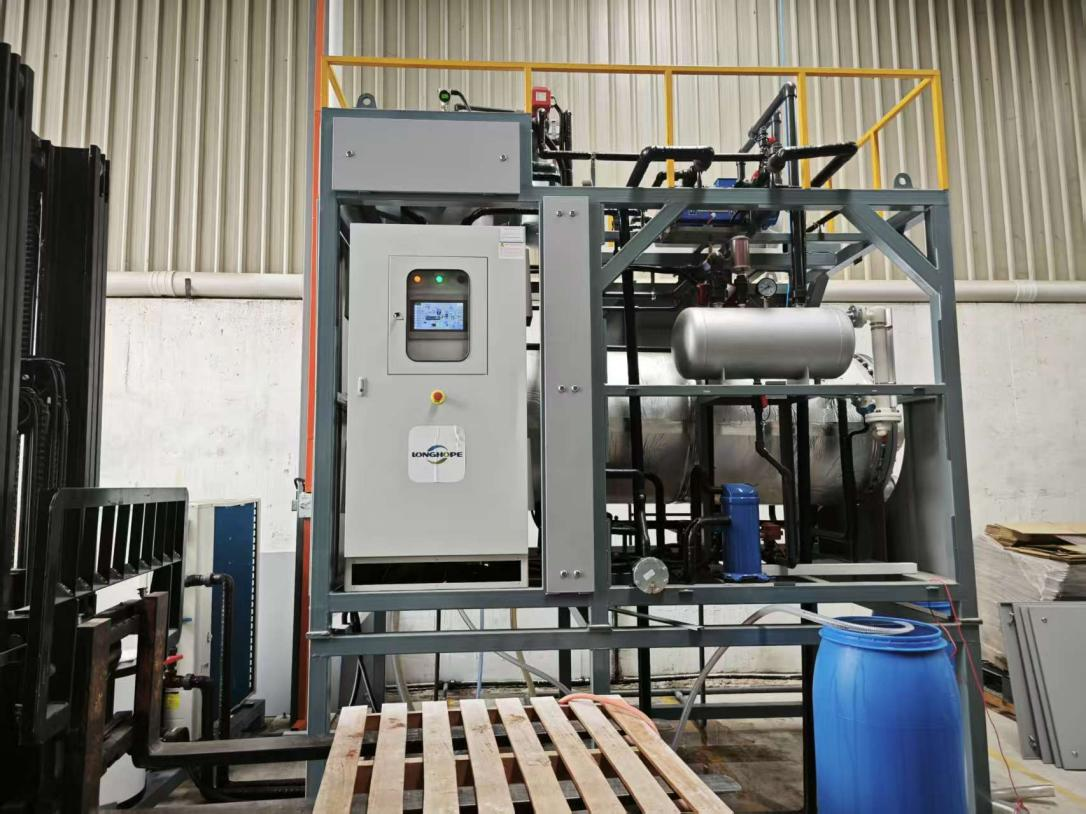
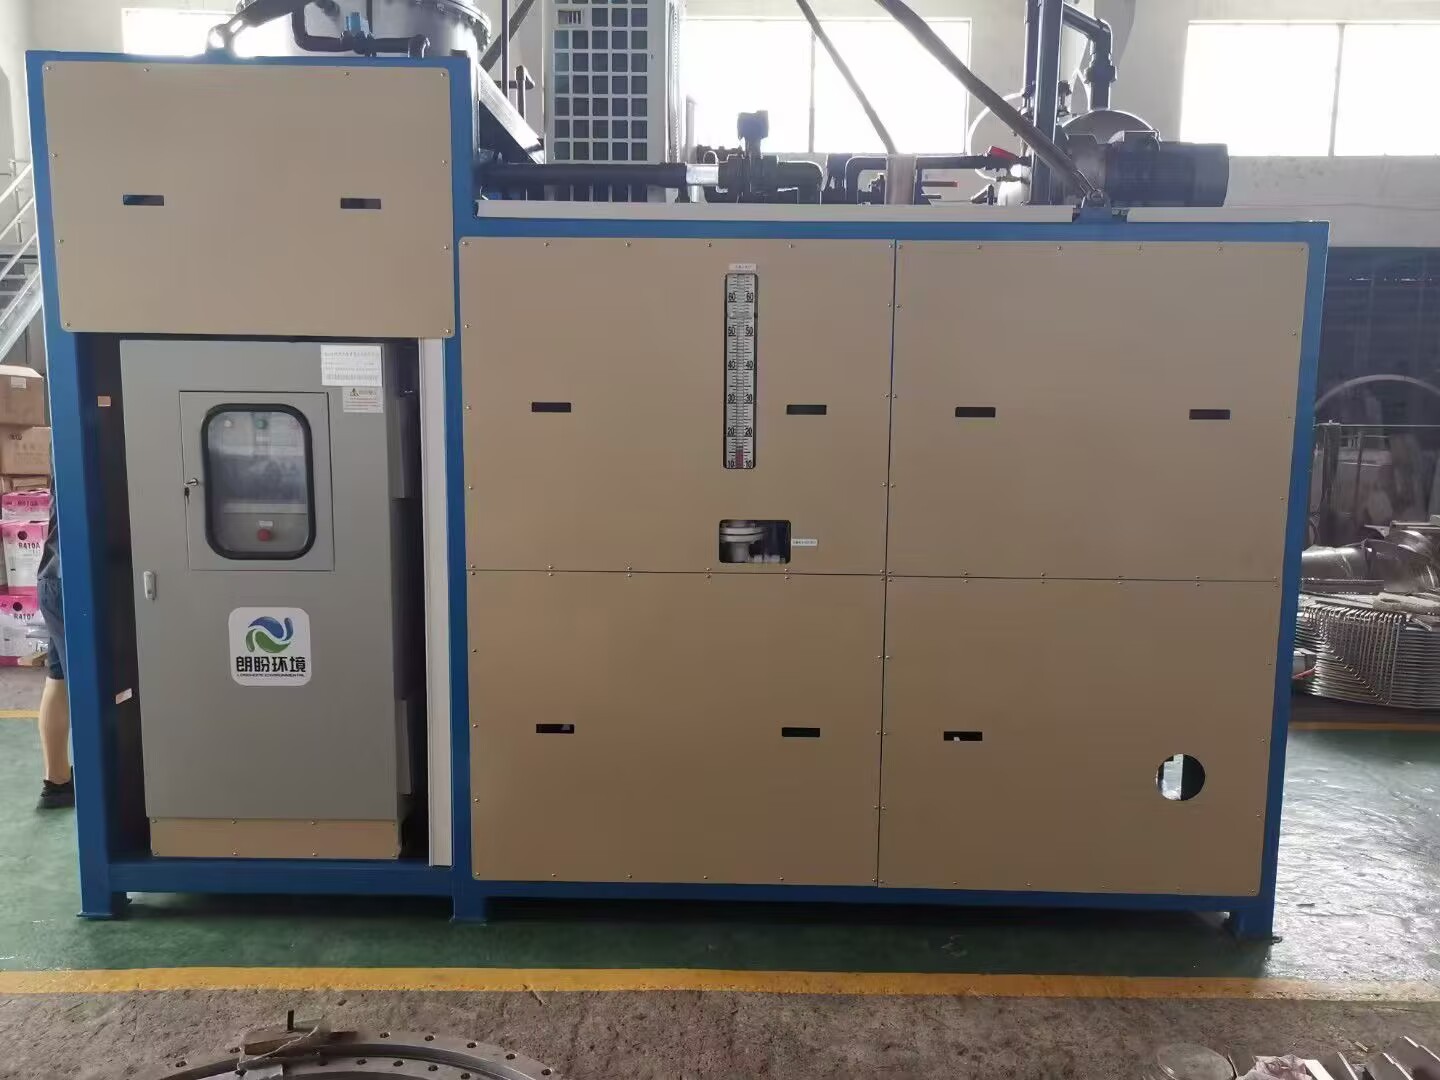
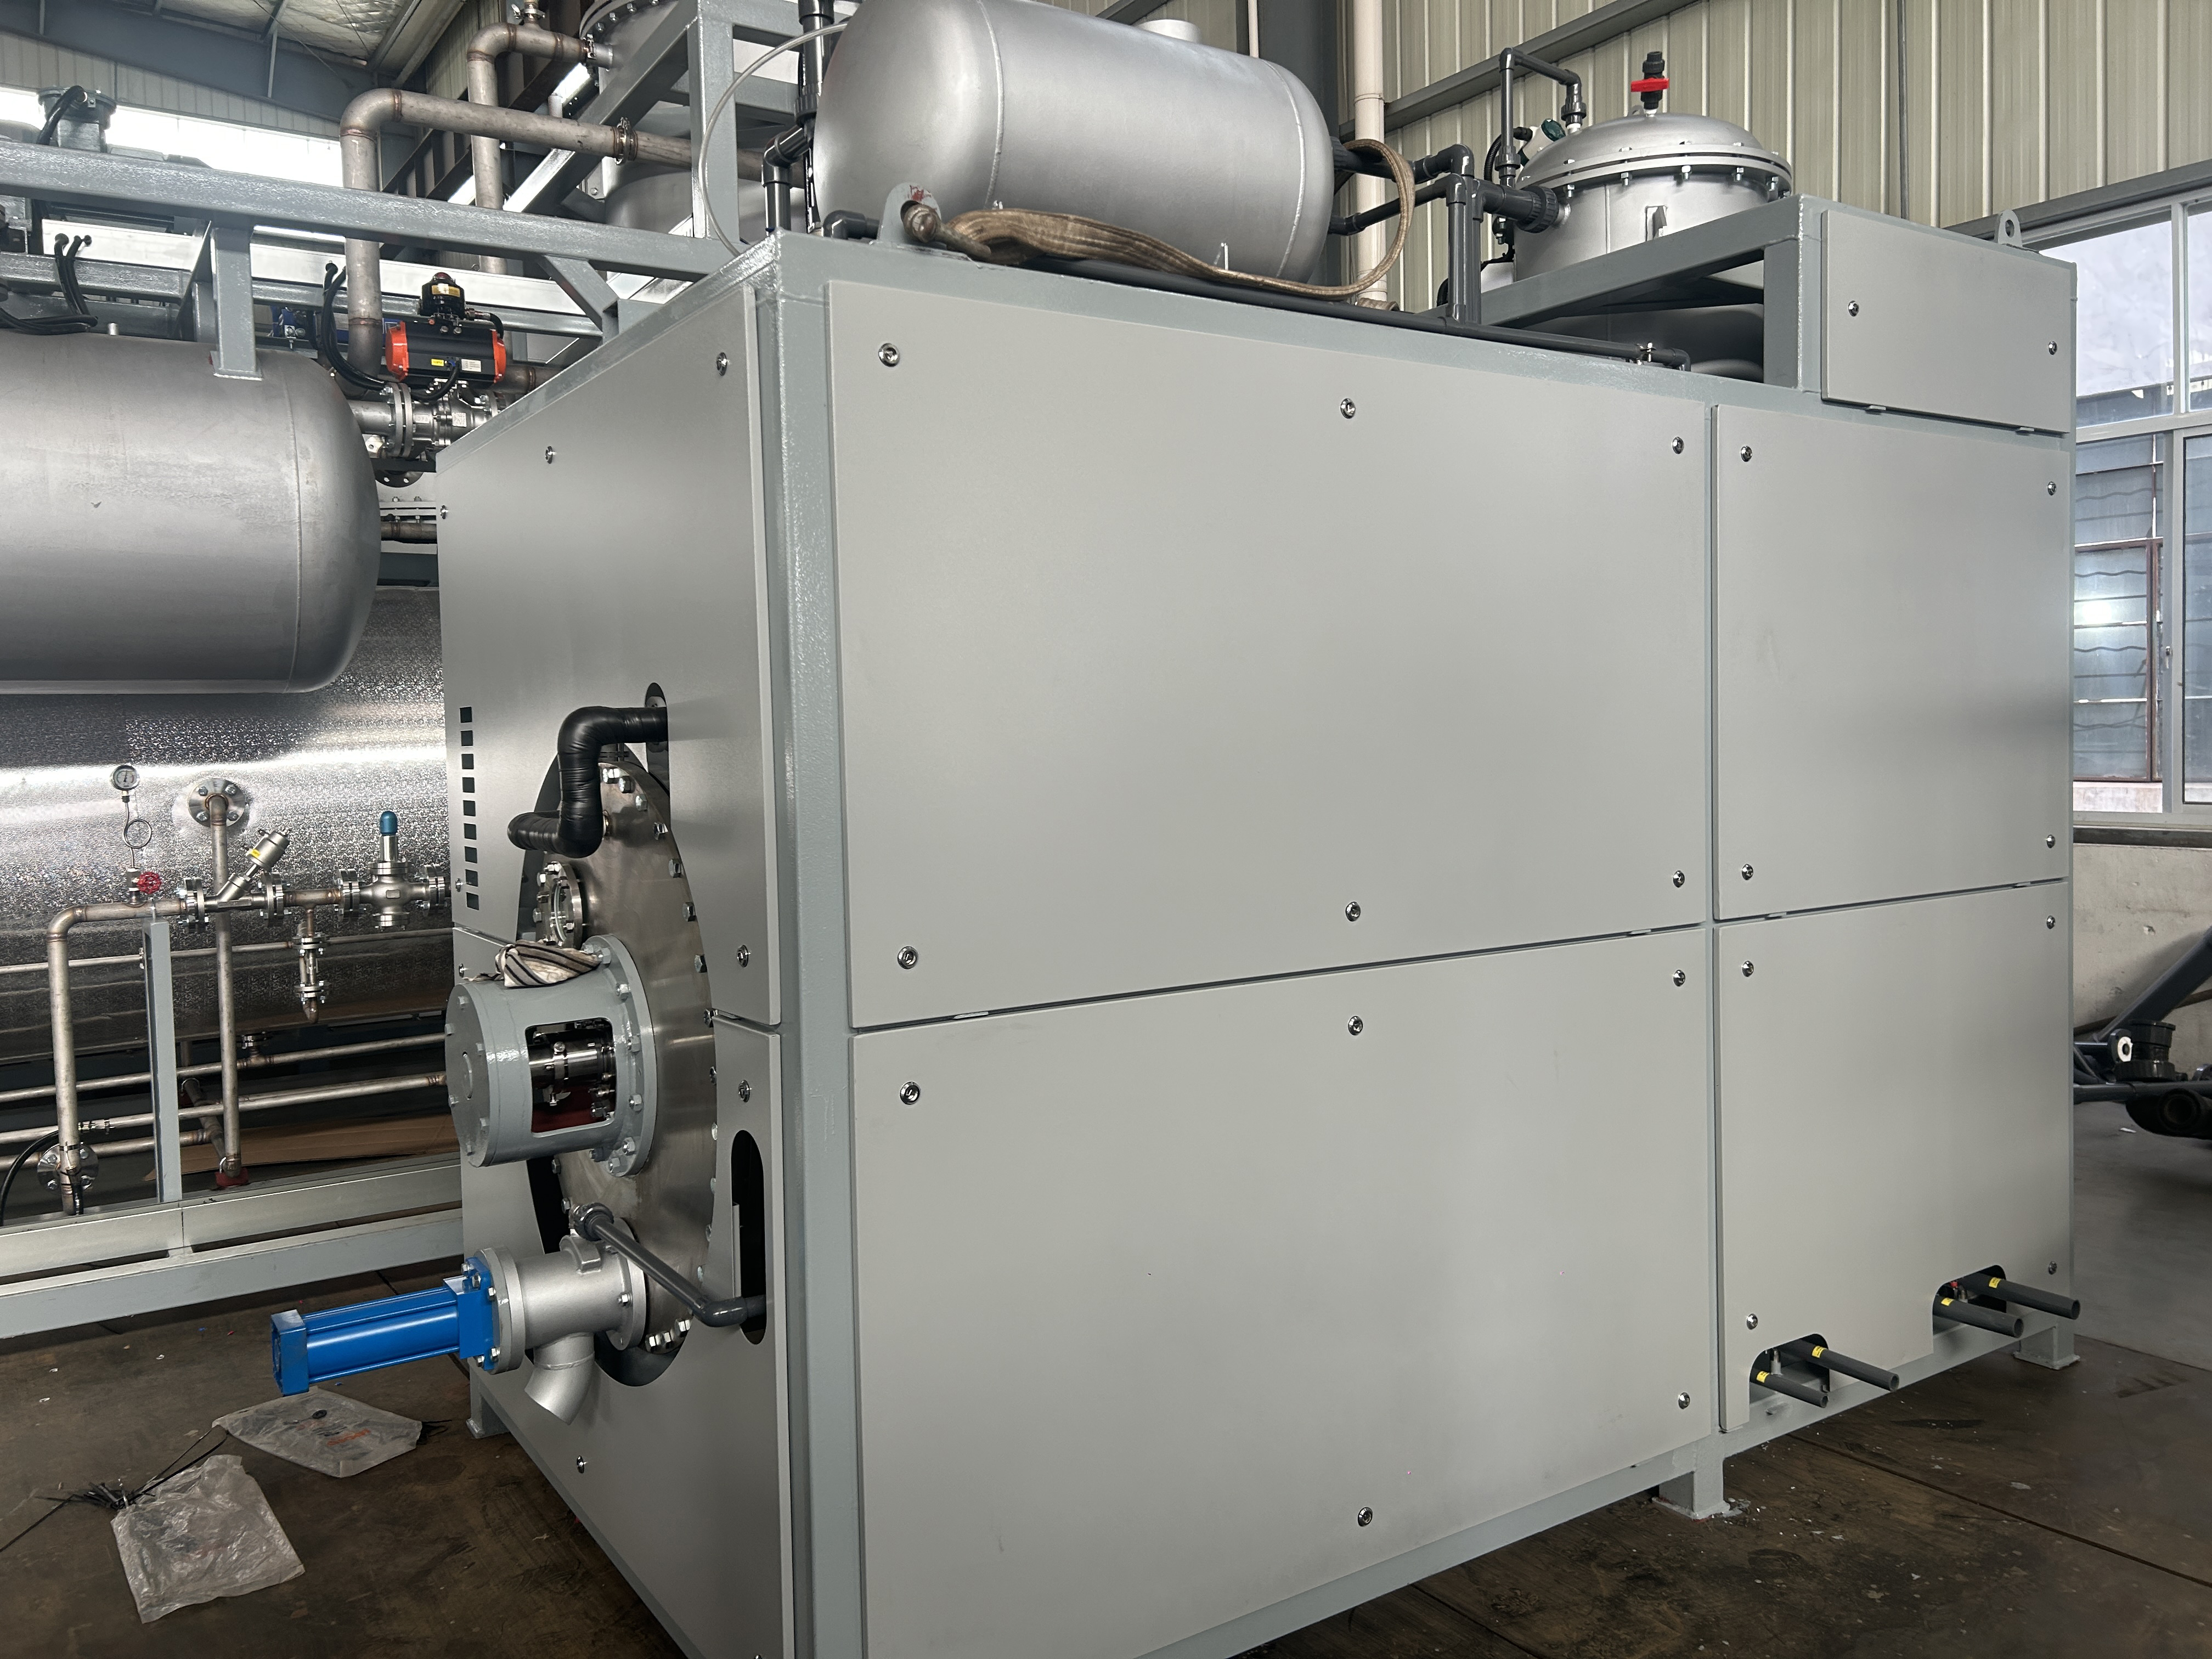
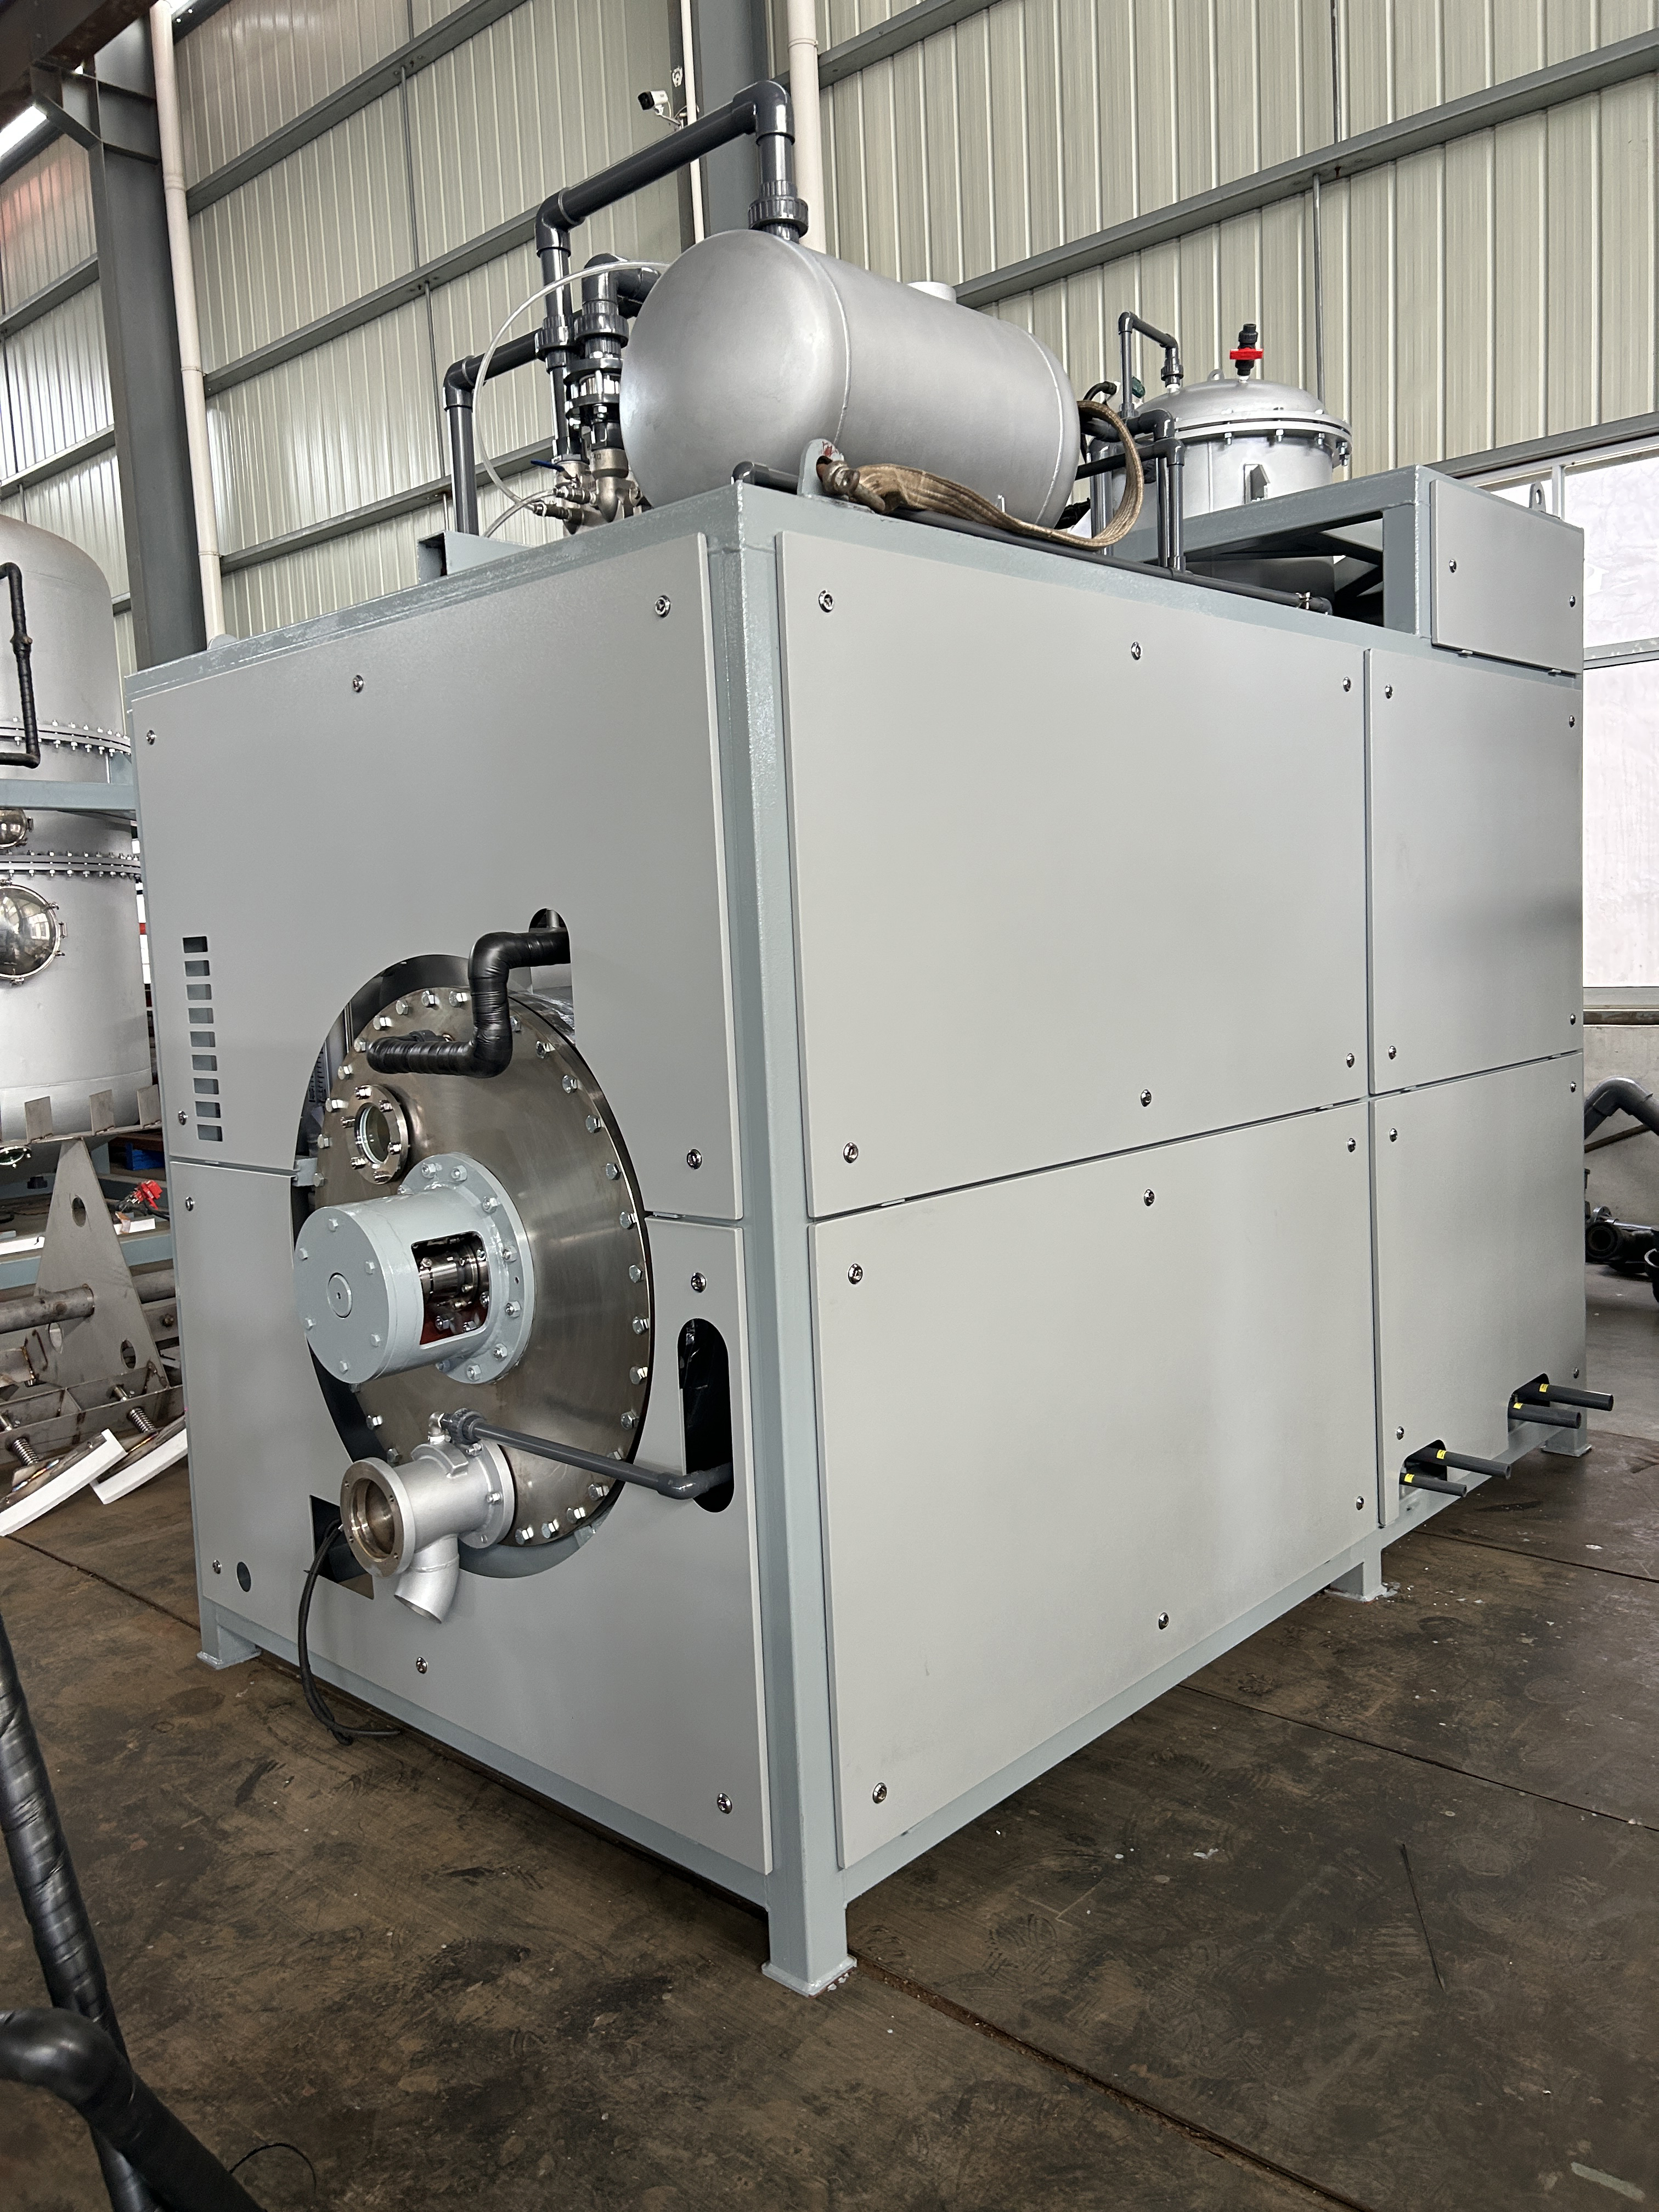
A vacuum crystallizer is an advanced industrial equipment designed to separate crystalline solids from liquid solutions through controlled evaporation and cooling under reduced pressure conditions. This sophisticated apparatus functions by removing moisture from saturated solutions while maintaining precise temperature control, enabling the formation of high-quality crystals with minimal impurities. The vacuum crystallizer operates by heating a solution within a sealed chamber where pressure is reduced, lowering the boiling point of liquids and promoting efficient evaporation. As the solution concentrates, crystals begin to form through nucleation and growth stages. The vacuum environment prevents thermal degradation of heat-sensitive materials, making the vacuum crystallizer ideal for pharmaceutical, chemical, and food processing applications. Technologically, the vacuum crystallizer features a robust vacuum system with condensers, separation chambers, and automated controls that monitor temperature, pressure, and crystal formation rates. Modern designs incorporate energy-efficient heat exchangers and recycling systems that reduce operational costs significantly. Key applications for the vacuum crystallizer include pharmaceutical manufacturing, salt production, sugar processing, and specialty chemical production. Industries rely on vacuum crystallizer technology to produce pure, uniform crystals meeting strict quality specifications. The equipment's versatility allows processing of various materials, from inorganic salts to organic compounds, making the vacuum crystallizer an essential investment for facilities requiring consistent crystallization processes with superior product quality and minimal waste generation.

Popular Products

The vacuum crystallizer delivers exceptional practical benefits that make it an intelligent choice for manufacturers seeking reliable crystallization solutions. Operating under reduced pressure conditions, this equipment produces superior crystal quality with enhanced purity levels compared to conventional crystallization methods. The vacuum crystallizer achieves this by preventing thermal decomposition of sensitive materials during processing, ensuring final products maintain their chemical integrity and market value. Operationally, the vacuum crystallizer significantly reduces energy consumption through its efficient heat recovery systems and optimized vacuum management. Businesses experience lower utility costs and improved production efficiency, directly impacting profitability. The automated control systems integrated into modern vacuum crystallizer units minimize manual intervention, reducing labor requirements and human error while ensuring consistent batch quality. The vacuum crystallizer excels in handling heat-sensitive compounds where traditional crystallization fails, opening opportunities in pharmaceutical and specialty chemical sectors. Its controlled environment prevents unwanted side reactions and product degradation. This capability directly translates to higher yields and reduced material waste, maximizing return on investment. From a decision-making perspective, investing in a vacuum crystallizer strengthens competitive positioning by enabling production of premium-grade crystals commanding higher market prices. The equipment's reliability minimizes downtime and maintenance disruptions, supporting continuous production schedules. Additionally, the vacuum crystallizer meets stringent regulatory requirements in pharmaceutical and food industries, facilitating market compliance and customer confidence. For facilities processing multiple material types, the vacuum crystallizer's flexibility represents substantial operational value, accommodating diverse crystallization requirements without equipment changes.

Tips And Tricks

Top 5 Low Temperature Heat Pump Evaporator Applications

24

Jul

Top 5 Low Temperature Heat Pump Evaporator Applications

The low temperature heat pump evaporator represents a critical advancement in industrial thermal management and energy efficiency. This innovative component enables heat pump systems to operate effectively at reduced temperatures, making it indispens...
View More
Top 5 Vacuum Distillation Applications in Industry

24

Jul

Top 5 Vacuum Distillation Applications in Industry

Vacuum distillation applications have become essential across multiple industrial sectors, transforming how manufacturers separate, purify, and concentrate valuable materials. By operating below atmospheric pressure, vacuum distillation applications ...
View More
Industrial Water Treatment Technologies for 2026

02

Sep

Industrial Water Treatment Technologies for 2026

Industrial water treatment remains one of the most critical operational priorities across manufacturing, chemical processing, food production, and energy sectors. As facilities face increasingly stringent environmental regulations, rising operational...
View More
Evaporator System Maintenance: Tips for Longevity

24

Jul

Evaporator System Maintenance: Tips for Longevity

Evaporator system maintenance is critical to ensuring your industrial cooling and waste-water treatment equipment operates reliably and efficiently over the long term. Whether your facility relies on evaporator systems for refrigeration, heat exchang...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

vacuum crystallizer

Superior Crystal Purity and Quality Control

Superior Crystal Purity and Quality Control

The vacuum crystallizer produces exceptionally pure crystals by eliminating contaminants through controlled evaporation under reduced pressure. This advanced purification mechanism ensures crystal products meet pharmaceutical and industrial grade specifications consistently. The vacuum crystallizer's precise environmental control—including temperature, pressure, and humidity management—enables reproducible results across production batches. Manufacturers benefit from reduced sorting and reprocessing requirements, directly improving productivity metrics. The crystal uniformity achieved through the vacuum crystallizer surpasses conventional methods, creating premium products that command higher market values. Quality assurance becomes streamlined when using the vacuum crystallizer, as its automated monitoring systems track critical parameters continuously, documenting compliance data for regulatory requirements. This superior quality control capability makes the vacuum crystallizer invaluable for industries where product consistency determines market success and customer retention.
Energy Efficiency and Cost Reduction

Energy Efficiency and Cost Reduction

Modern vacuum crystallizer systems incorporate advanced heat recovery technology that captures and recycles thermal energy throughout the crystallization process. This innovative approach significantly reduces overall energy consumption compared to traditional crystallization equipment, lowering operational expenses substantially. The vacuum crystallizer's efficient vapor management system minimizes steam requirements and condensation losses, translating to measurable utility cost savings. Businesses operating the vacuum crystallizer experience rapid returns on equipment investment through reduced energy bills and lower water consumption for cooling. The automated control systems within the vacuum crystallizer optimize operating conditions continuously, preventing energy waste from inefficient processing cycles. Long-term operational cost benefits accumulate as the vacuum crystallizer maintains peak performance with minimal maintenance requirements. Industries utilizing the vacuum crystallizer gain competitive advantages through reduced production costs, enabling more attractive pricing strategies or improved profit margins while maintaining quality standards.
Versatility Across Multiple Industrial Applications

Versatility Across Multiple Industrial Applications

The vacuum crystallizer adapts to diverse crystallization requirements across pharmaceutical, chemical, food, and specialty industries, eliminating the need for multiple specialized equipment systems. This remarkable versatility allows manufacturers to process various compounds—from inorganic salts to complex organic molecules—using a single platform. The vacuum crystallizer handles heat-sensitive materials that decompose under conventional crystallization methods, expanding product development possibilities significantly. Process flexibility within the vacuum crystallizer enables businesses to respond quickly to market demands and develop new product formulations without substantial capital reinvestment. The equipment's scalability from laboratory to industrial production scales supports companies at various growth stages using the same core technology. Industries leverage the vacuum crystallizer's adaptability to optimize production sequences, integrating multiple crystallization batches efficiently within existing manufacturing timelines. This operational flexibility positions the vacuum crystallizer as a strategic asset for manufacturers seeking equipment solutions supporting long-term business growth and market diversification.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000