Vacuum Distillation Equipment Manufacturer

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

vacuum distillation equipment manufacturer

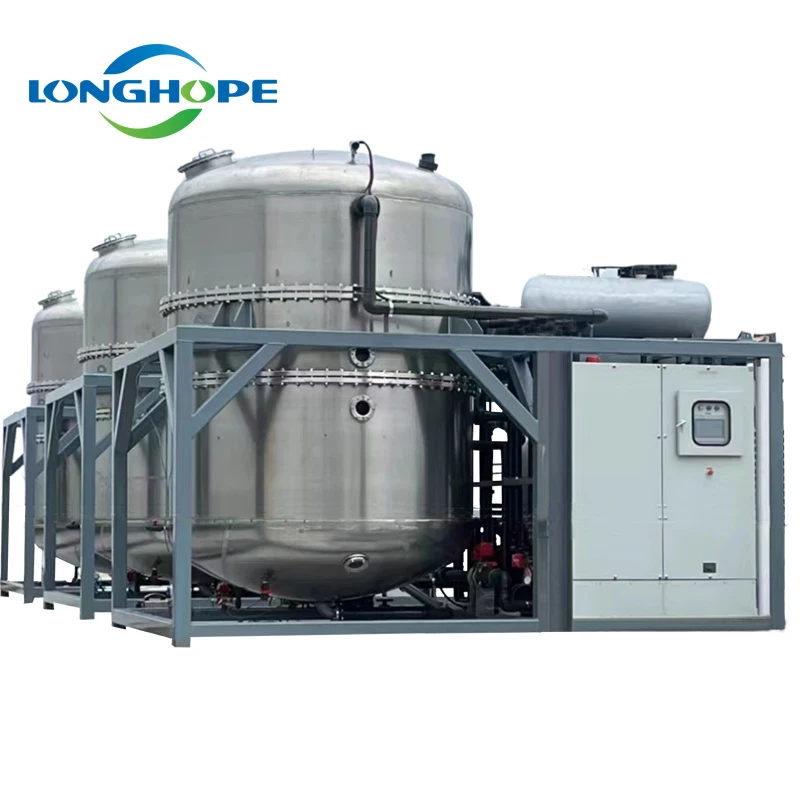
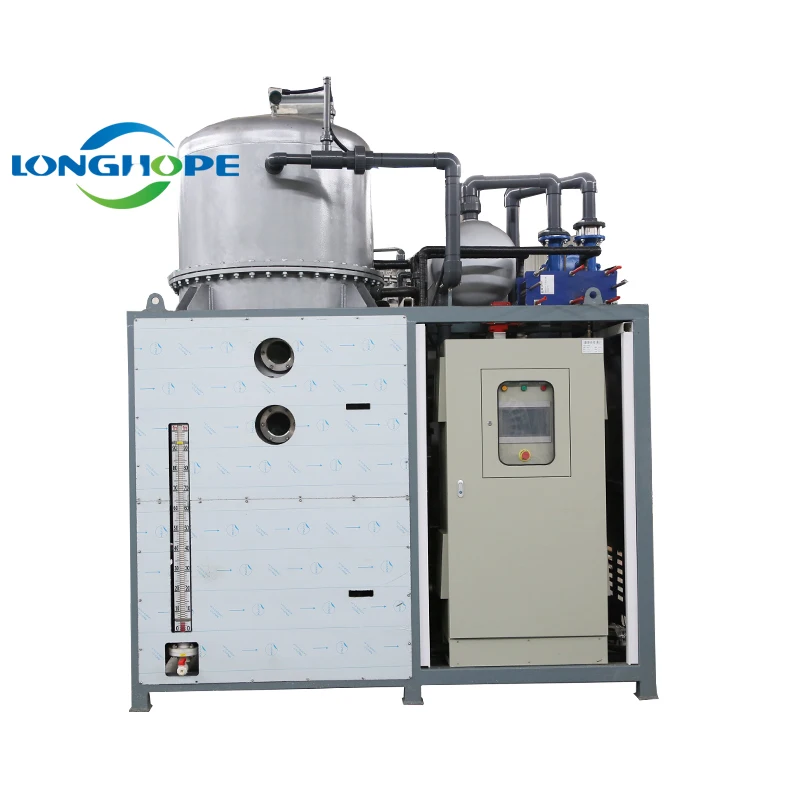
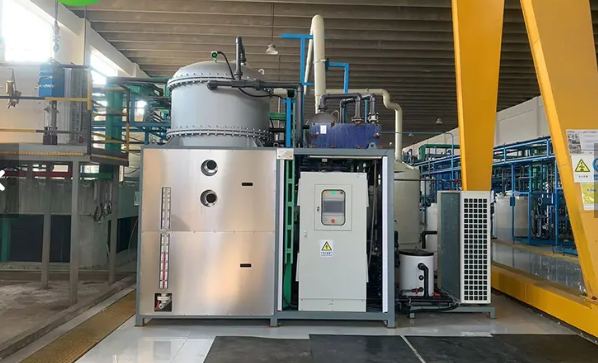
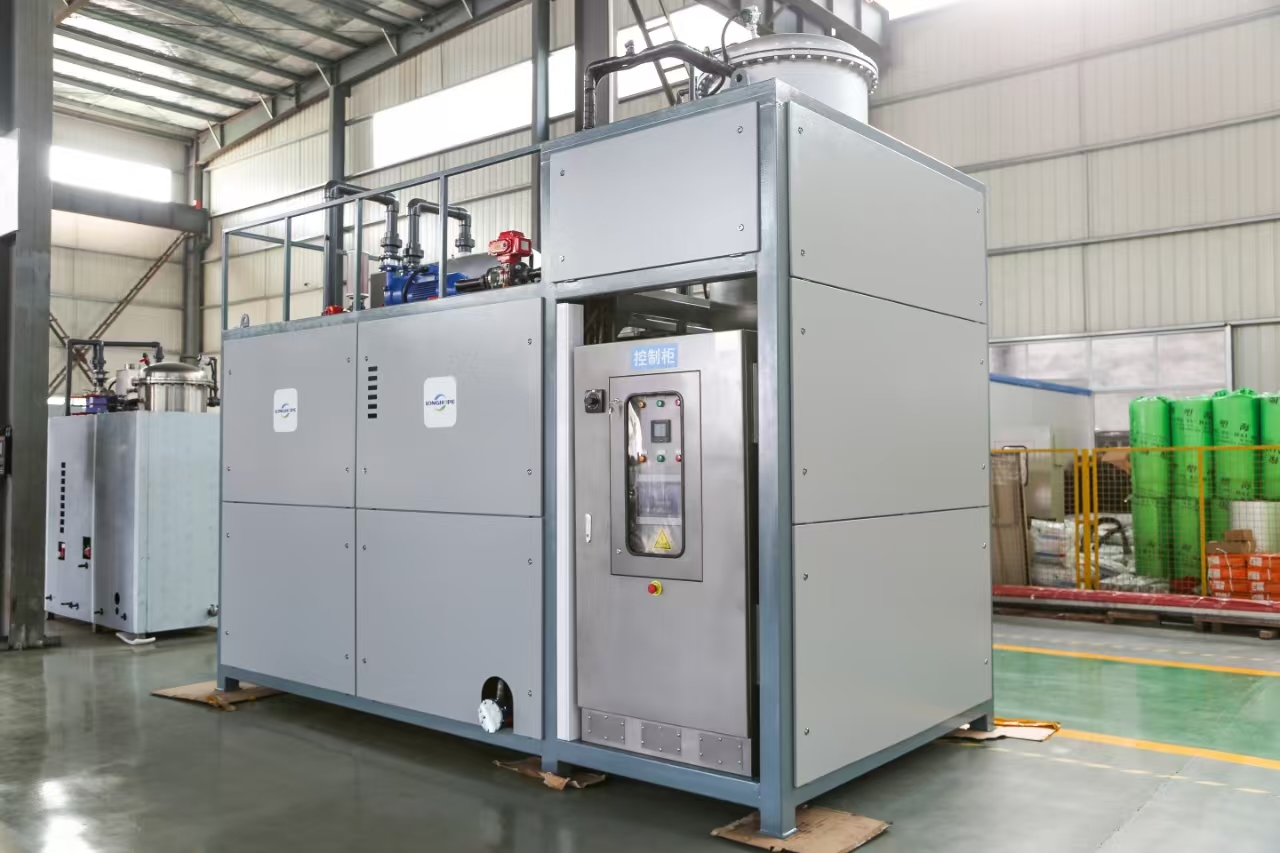
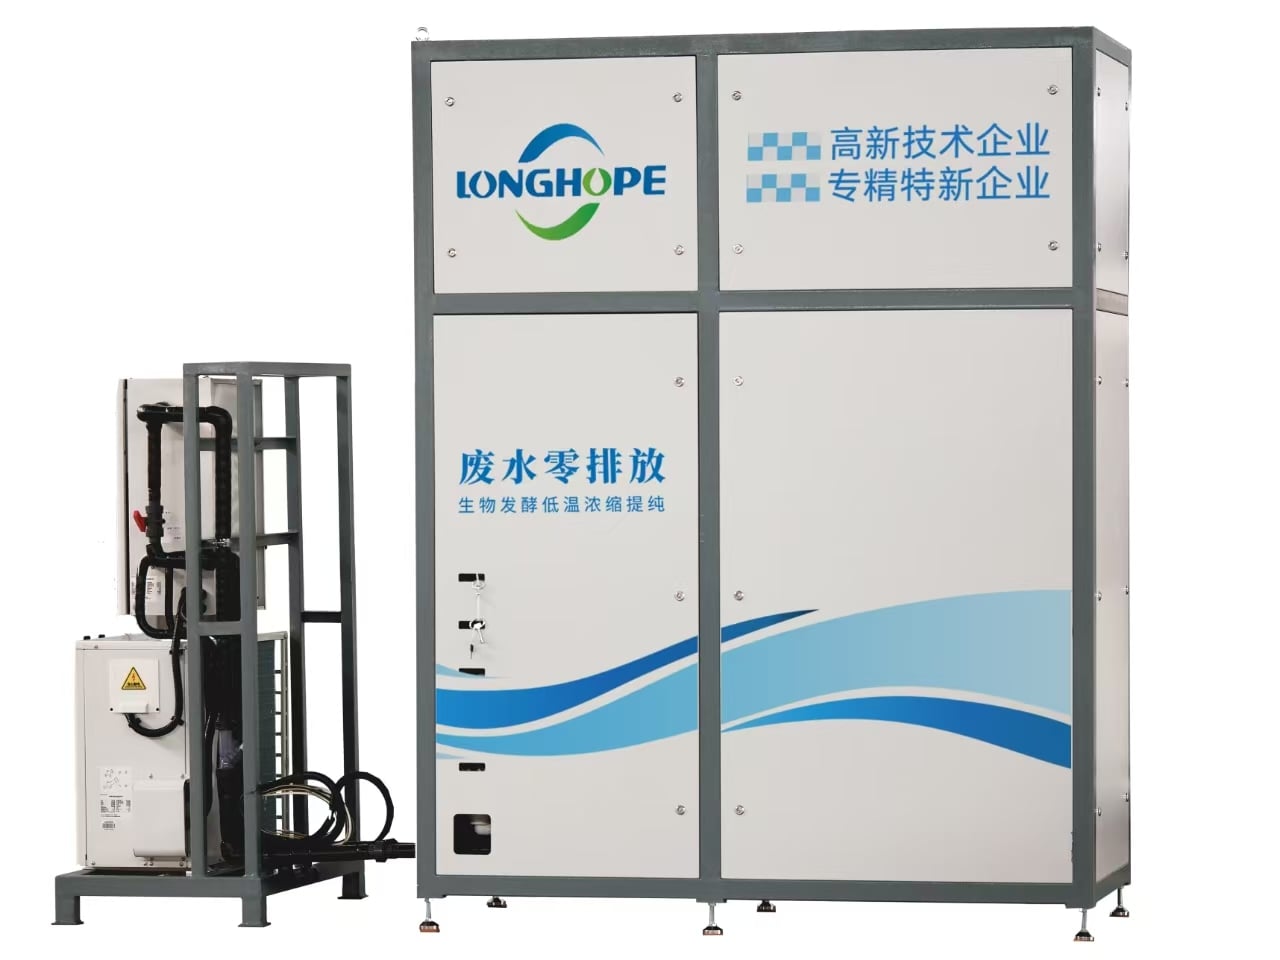
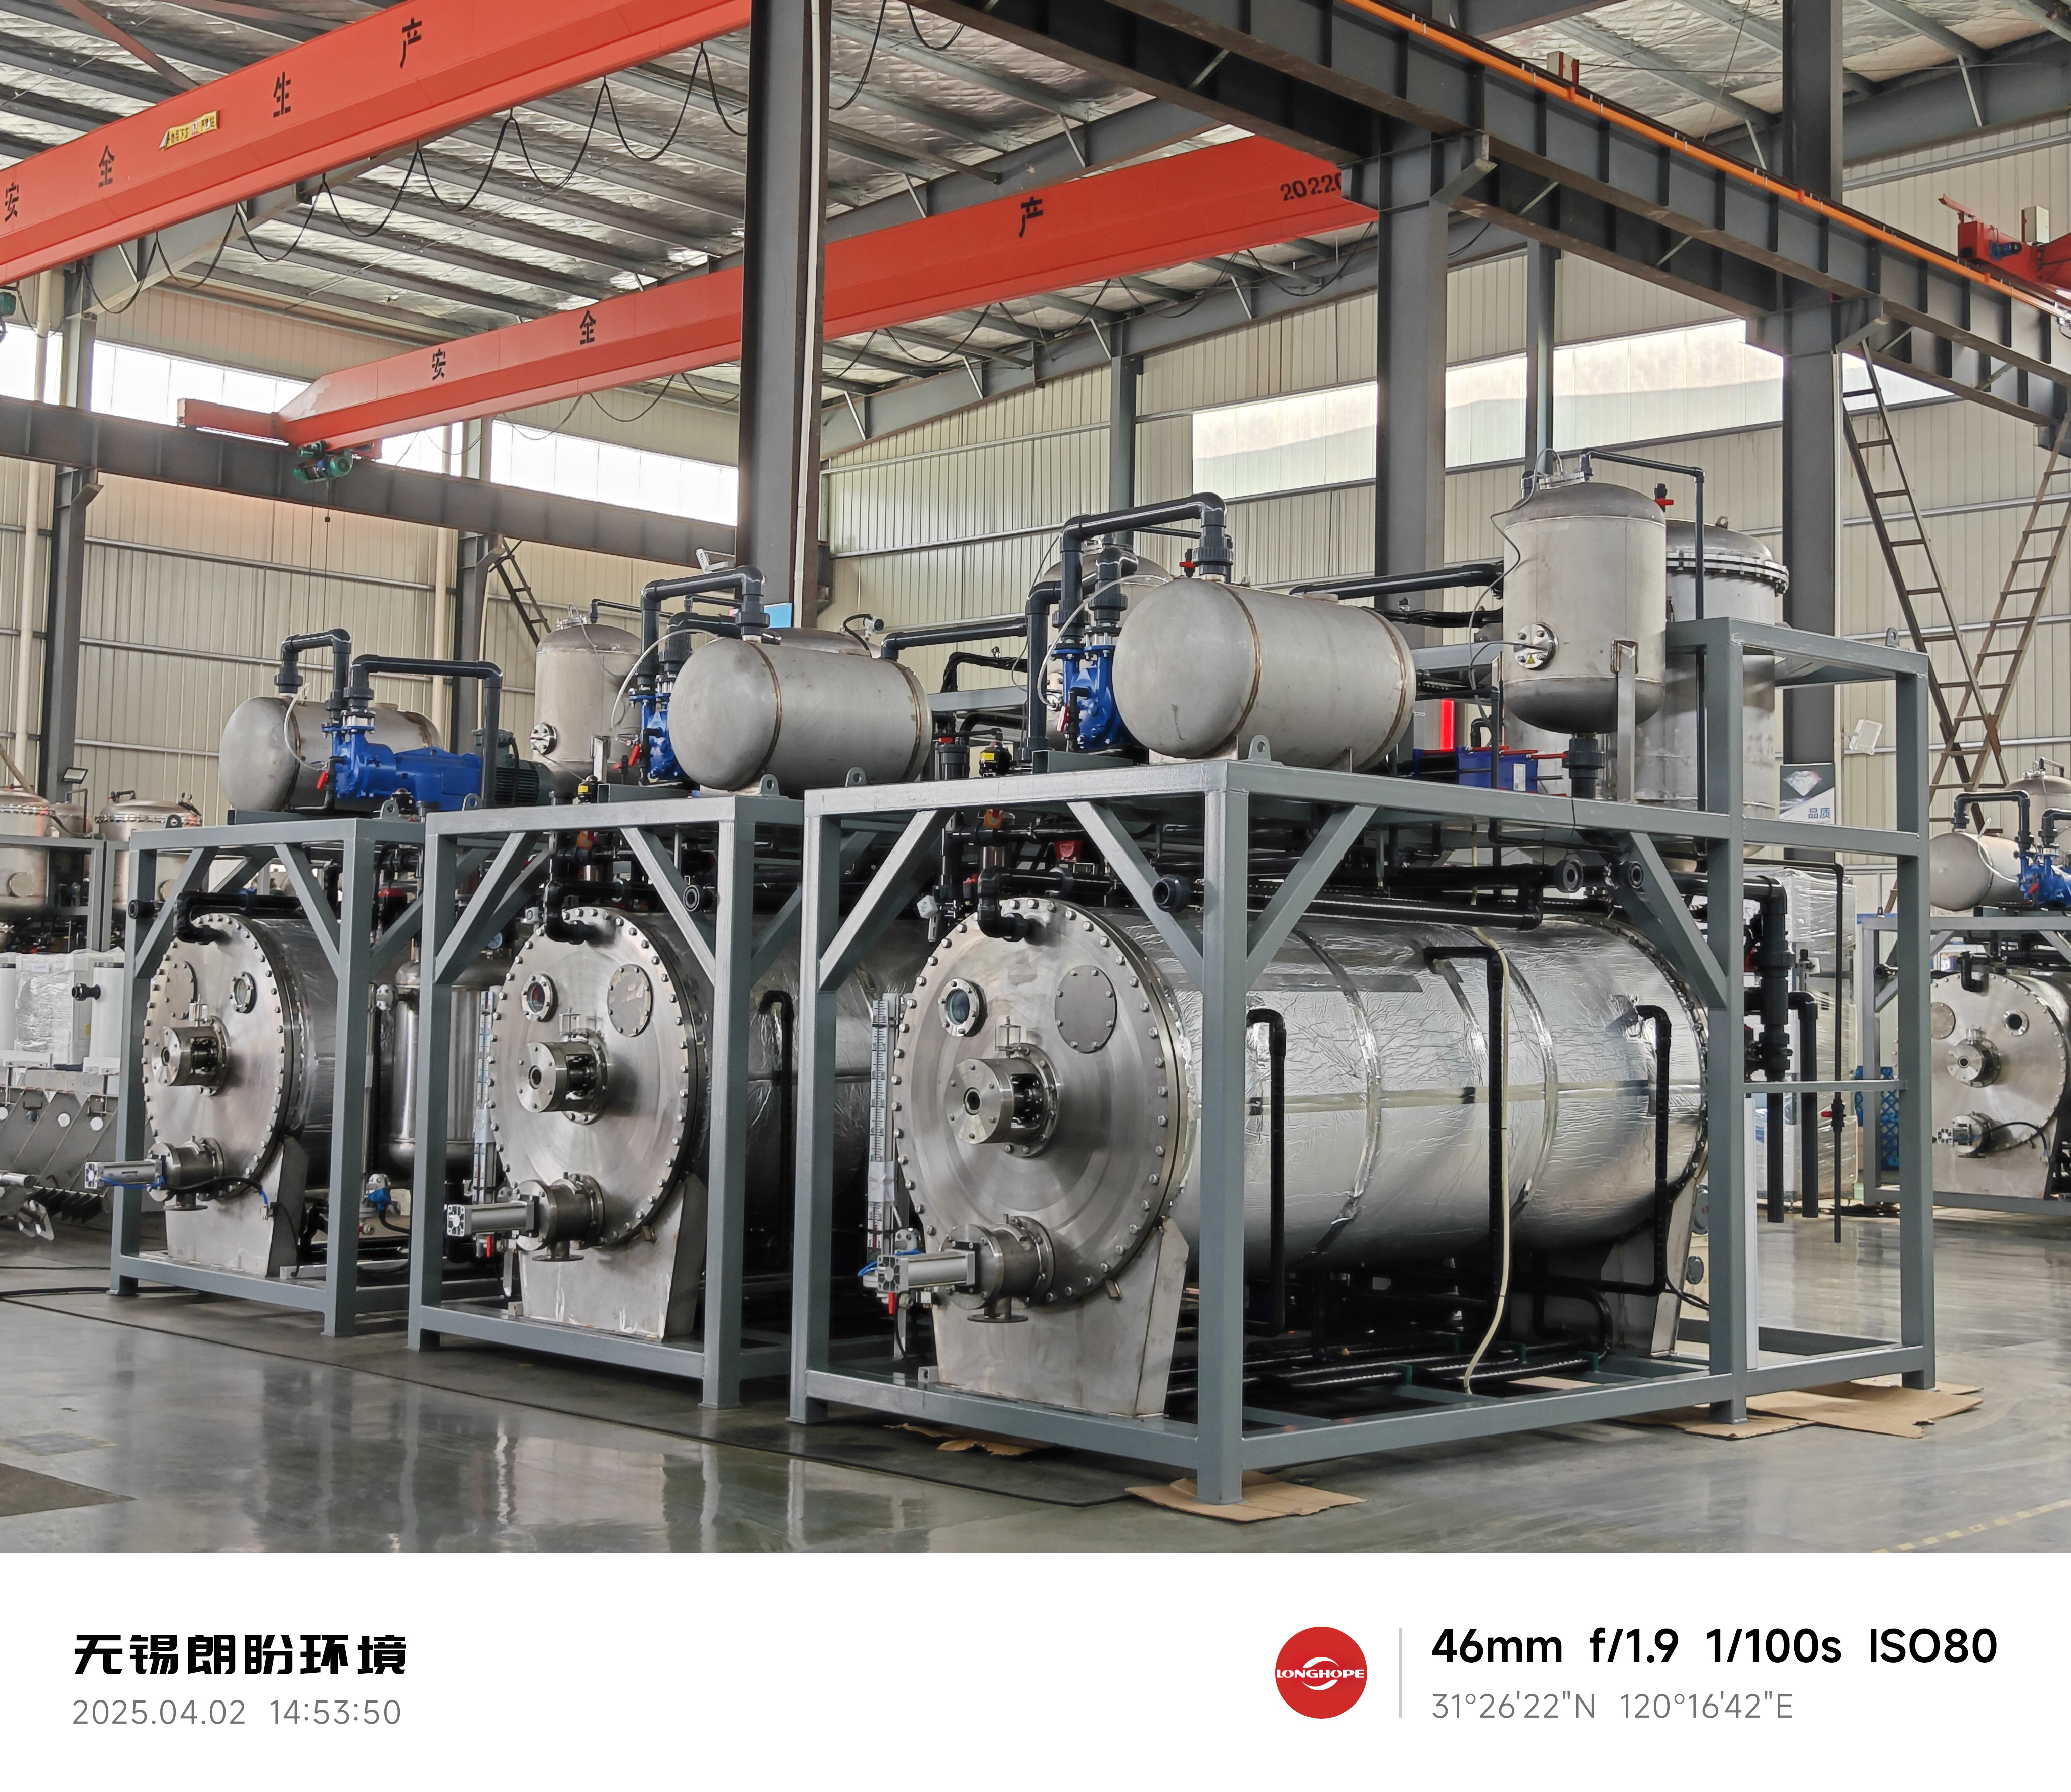
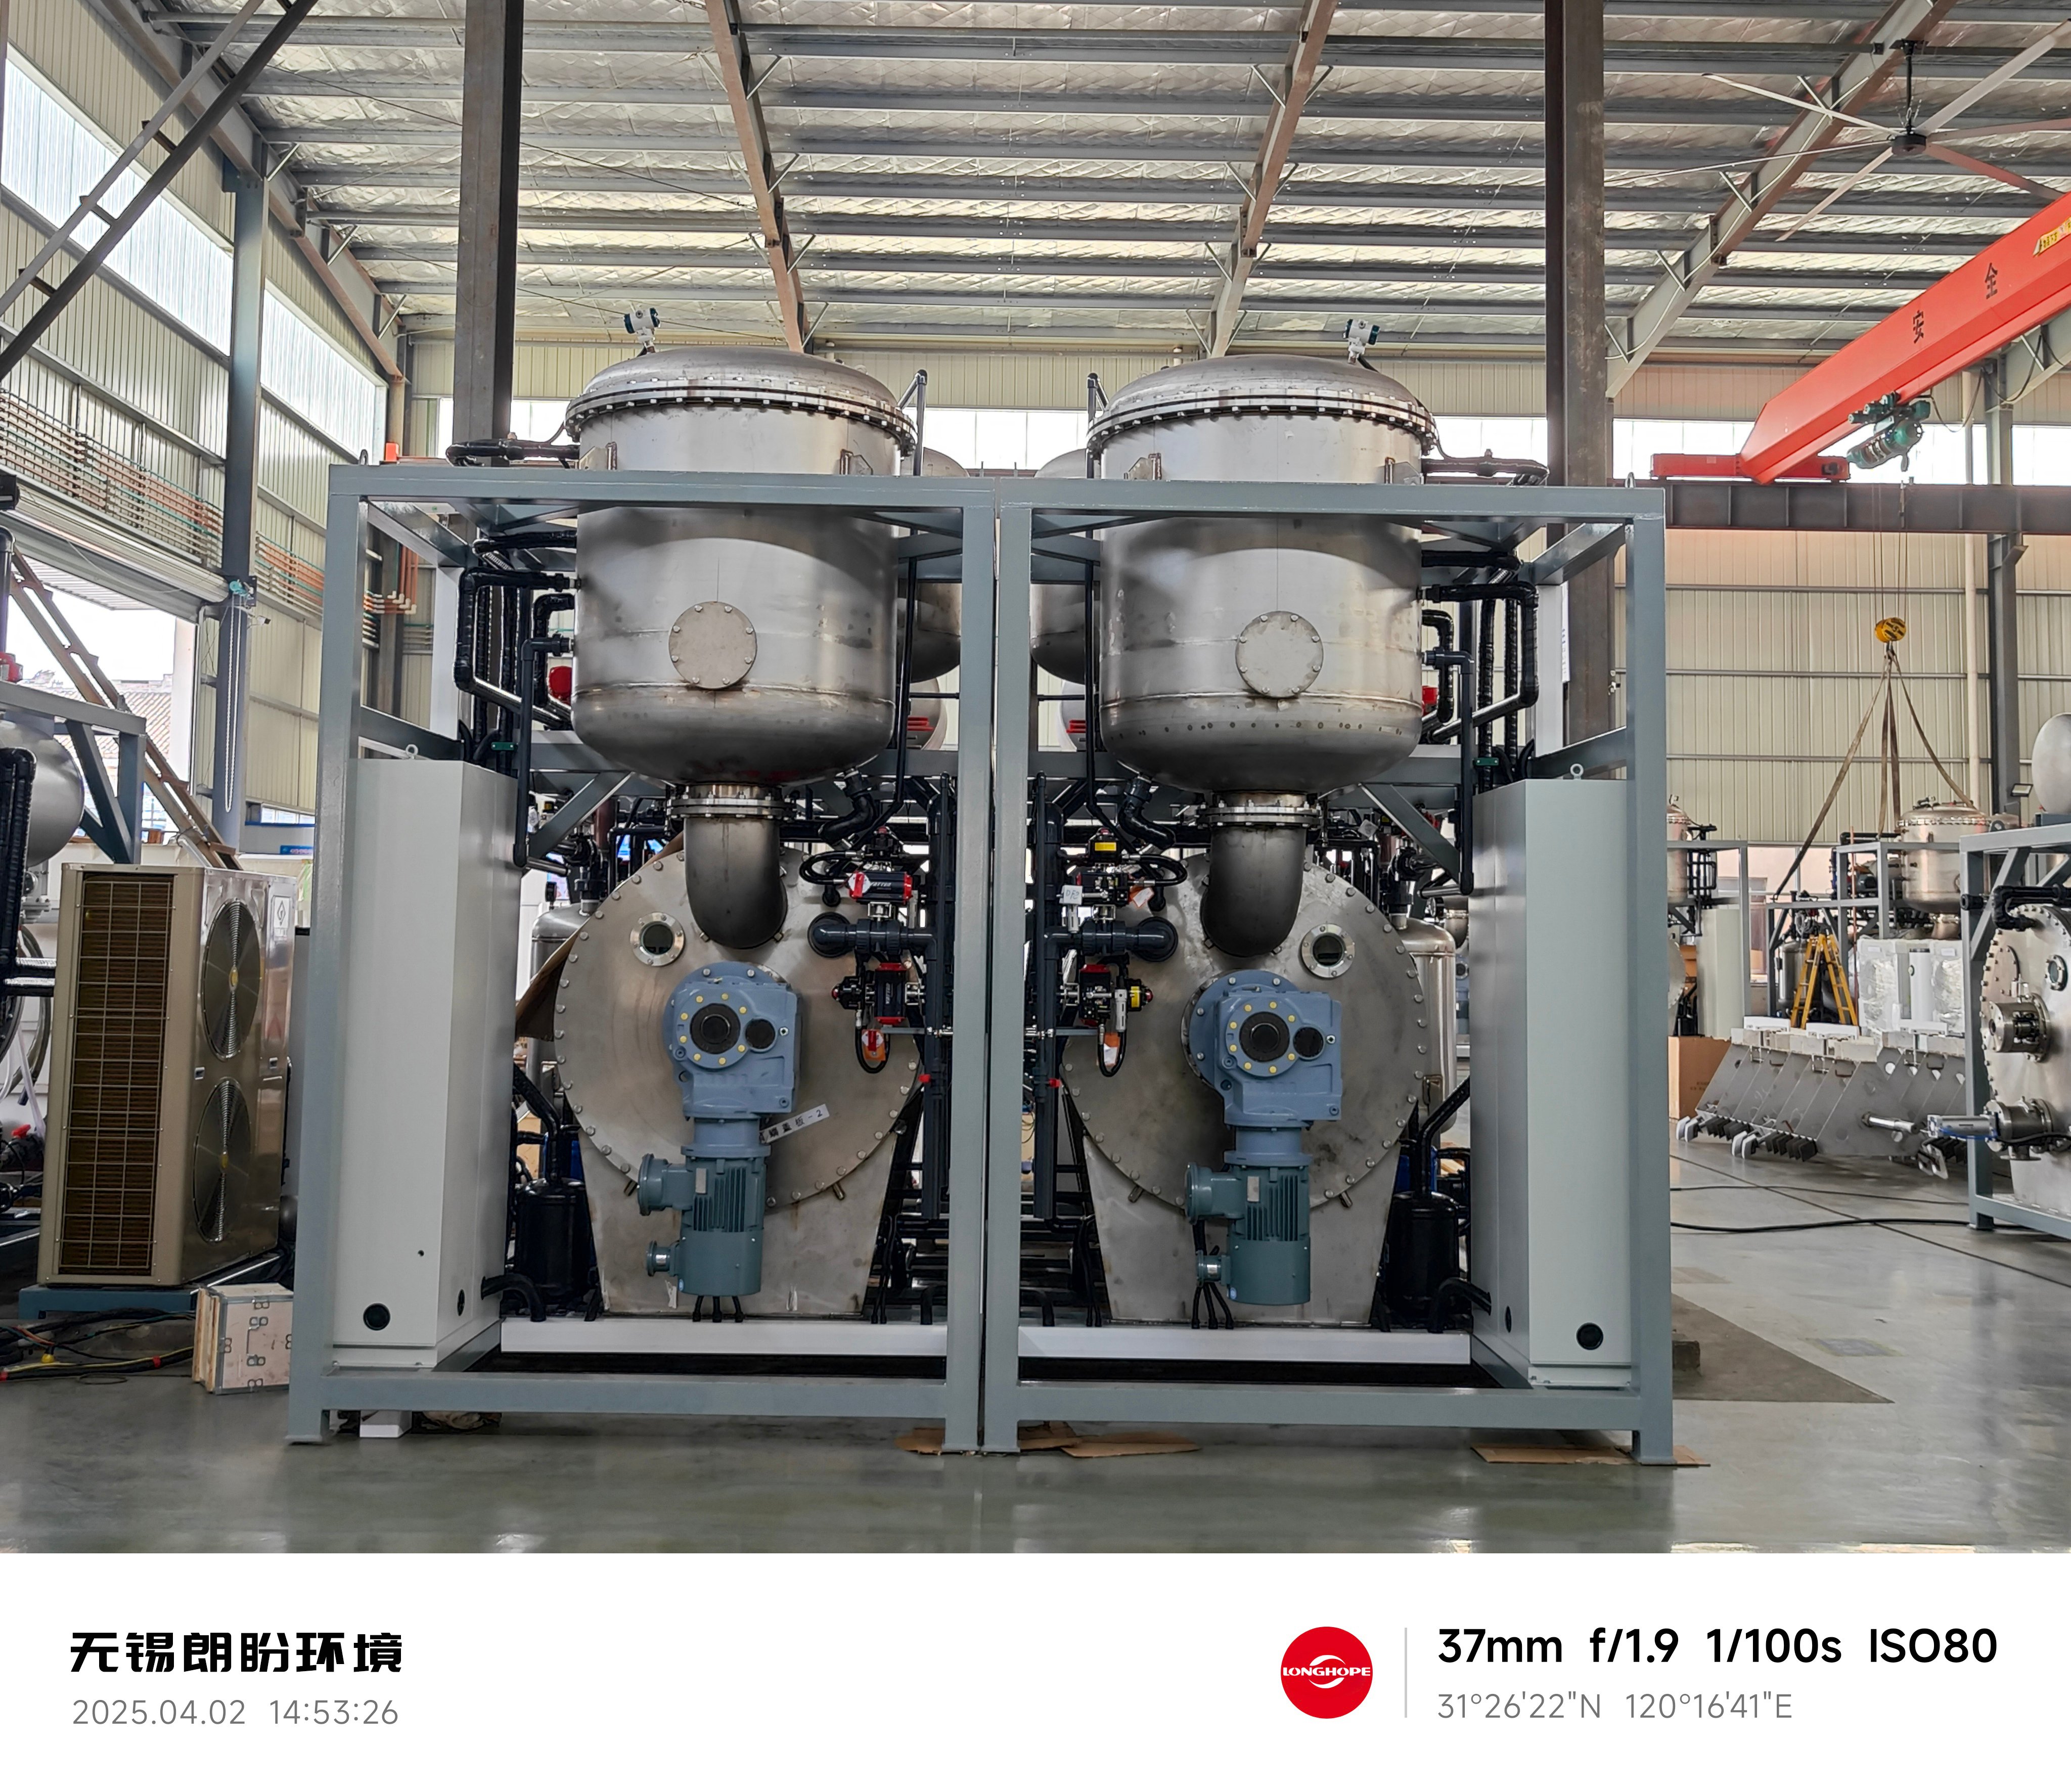
A vacuum distillation equipment manufacturer specializes in designing and producing advanced separation systems that operate under reduced pressure conditions. These innovative machines enable the distillation of heat-sensitive materials without thermal degradation, making them essential in pharmaceutical, chemical, and food processing industries. The vacuum distillation equipment manufacturer creates solutions that separate liquid mixtures based on boiling point differences while maintaining product integrity. The primary function of vacuum distillation equipment involves lowering atmospheric pressure to reduce boiling temperatures, allowing heat-sensitive compounds to separate without decomposition. This vacuum distillation equipment manufacturer integrates precision engineering with sophisticated control systems to achieve optimal separation efficiency. Key technological features include vacuum pumps, condensers, collection vessels, and automated temperature monitoring systems that work in harmony. Applications span diverse sectors where thermal sensitivity poses significant challenges. Pharmaceutical manufacturers rely on vacuum distillation equipment manufacturer solutions to purify active pharmaceutical ingredients and extract essential oils. Chemical processors use this technology for solvent recovery and product refinement. Food industry professionals employ these systems for flavoring extraction and concentrate production. A reputable vacuum distillation equipment manufacturer offers customizable configurations to match specific production requirements. Whether processing small research batches or large-scale industrial volumes, modern equipment delivers consistent results. The technology addresses the critical need for maintaining product quality while achieving efficient separation, making it indispensable for quality-conscious manufacturers worldwide.

New Product Recommendations

Choosing a trusted vacuum distillation equipment manufacturer delivers substantial operational and financial benefits that directly impact your bottom line. These systems protect your valuable materials from thermal damage by operating at significantly lower temperatures than conventional distillation methods. Your heat-sensitive compounds remain intact, preserving their chemical properties and market value throughout the separation process. Operational efficiency gains are immediate and measurable. A quality vacuum distillation equipment manufacturer provides equipment that reduces processing time while increasing yield rates substantially. You recover more usable product from each batch, directly improving profitability without requiring additional raw materials. The automated control systems minimize human intervention, reducing labor costs and operator errors that compromise product quality. The vacuum distillation equipment manufacturer designs systems that adapt to your specific production needs. Whether you handle volatile solvents, delicate botanical extracts, or pharmaceutical compounds, flexible configurations ensure optimal performance. This versatility means your single investment supports multiple product lines, maximizing equipment utilization throughout your facility. Maintenance requirements remain minimal when you partner with an experienced vacuum distillation equipment manufacturer. Robust construction and intelligent design reduce breakdowns and extend equipment lifespan significantly. Preventive maintenance schedules keep systems running smoothly, ensuring consistent production capacity. Environmental compliance becomes straightforward with modern vacuum distillation equipment manufacturer solutions. Sealed systems prevent vapor emissions, meeting strict regulatory requirements while protecting worker safety. Your facility operates cleaner and more responsibly. Investment in quality vacuum distillation equipment manufacturer technology positions your company as industry leader, attracting quality-conscious customers who value sustainability and excellence.

Practical Tips

Top 5 Low Temperature Heat Pump Evaporator Applications

24

Jul

Top 5 Low Temperature Heat Pump Evaporator Applications

The low temperature heat pump evaporator represents a critical advancement in industrial thermal management and energy efficiency. This innovative component enables heat pump systems to operate effectively at reduced temperatures, making it indispens...
View More
Vacuum Distillation System Maintenance Best Practices

24

Jul

Vacuum Distillation System Maintenance Best Practices

Proper vacuum distillation system maintenance is critical for industries relying on separation, purification, and concentration processes. A well-maintained vacuum distillation system ensures consistent product quality, minimizes operational downtime...
View More
How Low Temperature Heat Pump Evaporator Cuts Energy Costs

24

Jul

How Low Temperature Heat Pump Evaporator Cuts Energy Costs

Industrial operations consume significant energy, and equipment efficiency directly impacts profitability. A low temperature heat pump evaporator represents a transformative approach to reducing energy expenditure while maintaining operational perfor...
View More
Choosing the Right Evaporator System for Your Plant

24

Jul

Choosing the Right Evaporator System for Your Plant

Selecting an evaporator system for your industrial plant is one of the most critical decisions you will make in your facility's operational strategy. An evaporator system directly impacts energy consumption, product quality, waste management efficien...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

vacuum distillation equipment manufacturer

Advanced Temperature Control for Superior Product Protection

Advanced Temperature Control for Superior Product Protection

The vacuum distillation equipment manufacturer integrates sophisticated temperature regulation systems that maintain precise conditions throughout your distillation process. Advanced sensors continuously monitor thermal fluctuations, automatically adjusting heating elements to prevent product degradation. This intelligent control mechanism ensures your heat-sensitive materials experience minimal thermal stress, preserving valuable compounds that conventional methods would destroy. The vacuum distillation equipment manufacturer's temperature management technology allows you to process premium ingredients while maintaining their therapeutic potency or commercial grade standards. Real-time feedback systems provide operators with detailed process data, enabling informed decisions and quality assurance validation. By maintaining exact temperature parameters, you achieve consistent batch-to-batch results that satisfy rigorous industry specifications. This technological advantage directly translates to higher product yields and reduced waste, significantly improving your return on investment throughout the equipment's operational lifespan.
Efficient Solvent Recovery and Environmental Sustainability

Efficient Solvent Recovery and Environmental Sustainability

Leading vacuum distillation equipment manufacturer solutions feature integrated recovery systems that capture and recycle valuable solvents during processing. These closed-loop designs minimize solvent loss while reducing environmental impact substantially. Your facility operates with minimal vapor emissions, ensuring compliance with increasingly stringent environmental regulations. The vacuum distillation equipment manufacturer's recovery technology transforms waste into recoverable resources, creating additional revenue streams from materials typically discarded. Advanced condensing systems capture over ninety-five percent of solvent vapors, dramatically reducing disposal costs and environmental liability. By choosing a vacuum distillation equipment manufacturer committed to sustainability, you demonstrate corporate responsibility while improving operational efficiency. The economic benefits accumulate monthly as solvent recovery reduces consumable expenses. Enhanced environmental performance also strengthens relationships with regulatory agencies and environmentally conscious customers seeking responsible business partners.
Scalable Design for Growing Production Demands

Scalable Design for Growing Production Demands

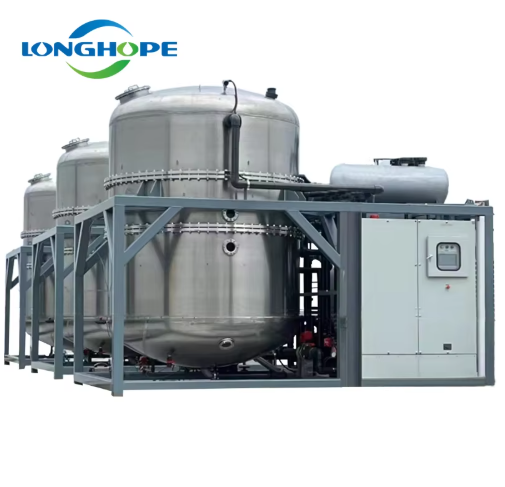
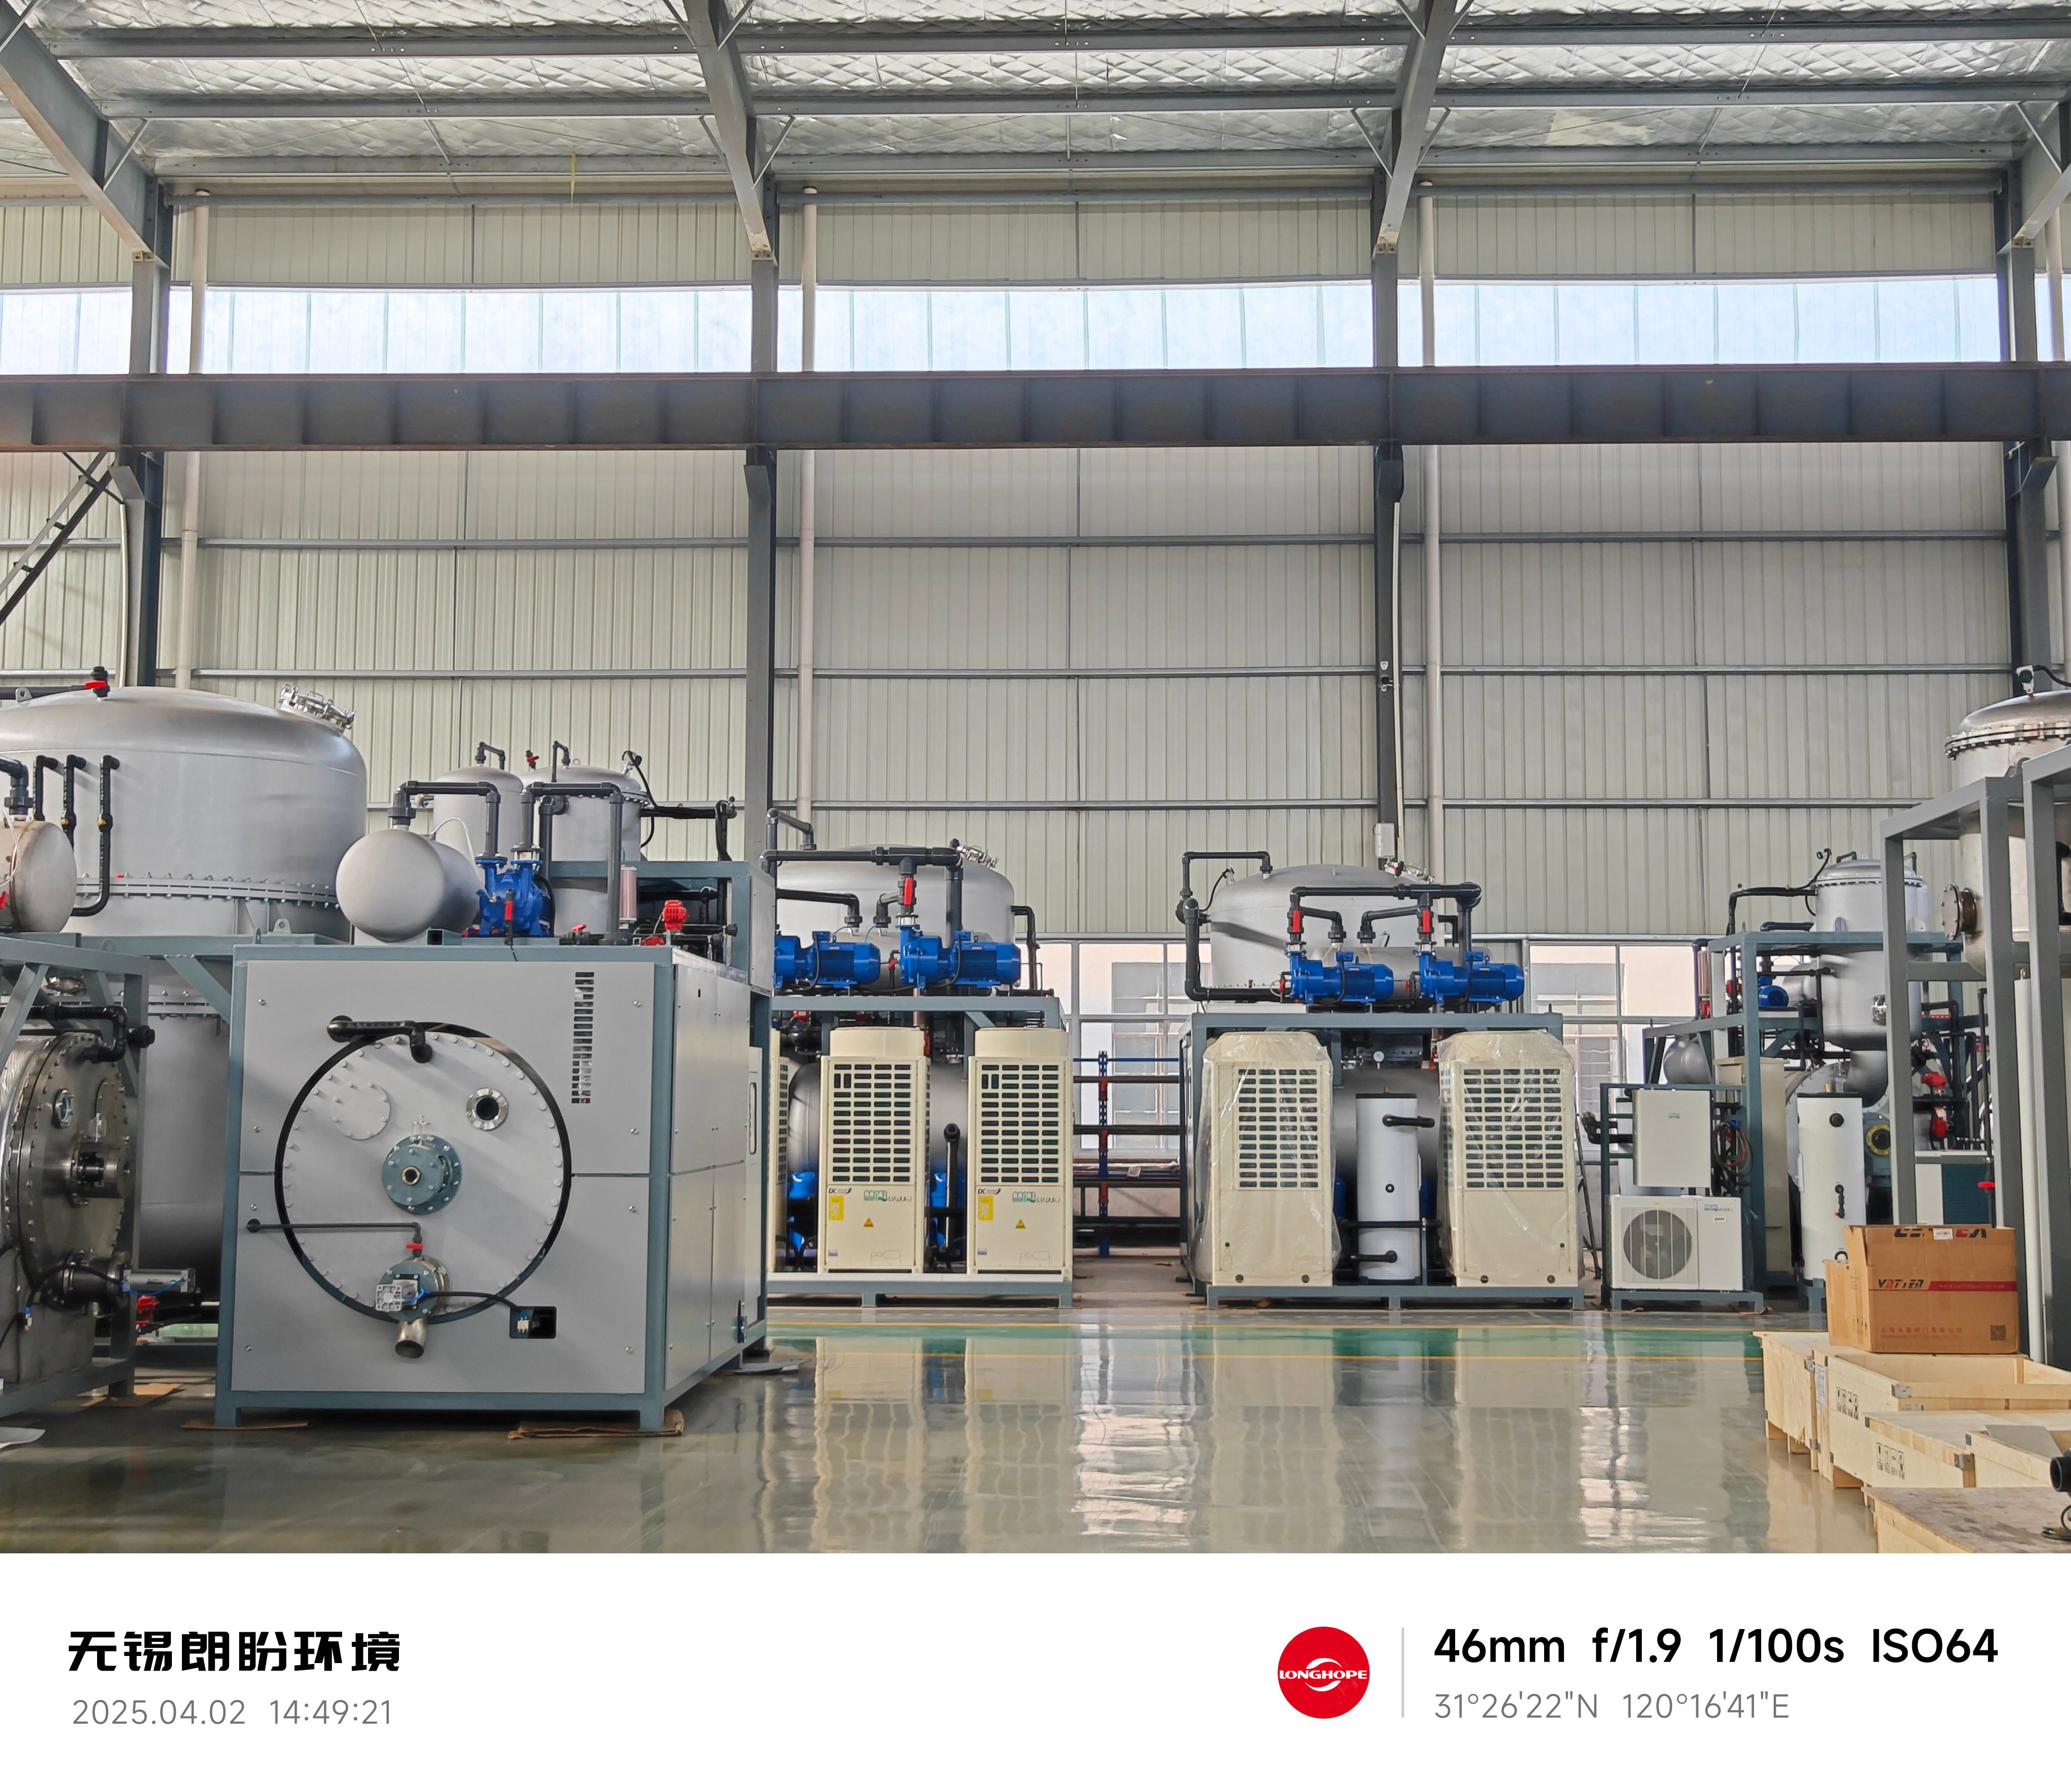
The vacuum distillation equipment manufacturer delivers scalable solutions that grow alongside your business. Modular configurations allow capacity upgrades without replacing entire systems, protecting your initial investment while accommodating expansion. Whether processing laboratory quantities or industrial-scale volumes, the vacuum distillation equipment manufacturer provides standardized platforms that maintain consistent quality parameters across all production scales. This flexibility ensures your equipment remains relevant despite changing market demands and production targets. Advanced vacuum distillation equipment manufacturer systems accommodate multiple processing modules operating simultaneously, multiplying throughput without proportional space requirements. Your facility maximizes square footage efficiency while maintaining consistent separation quality. The scalable approach reduces capital expenditure during growth phases, enabling strategic reinvestment in other business areas. Standardized operation across different system sizes simplifies staff training and ensures production continuity during transitions between capacity levels.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000