vacuum distillation system supplier
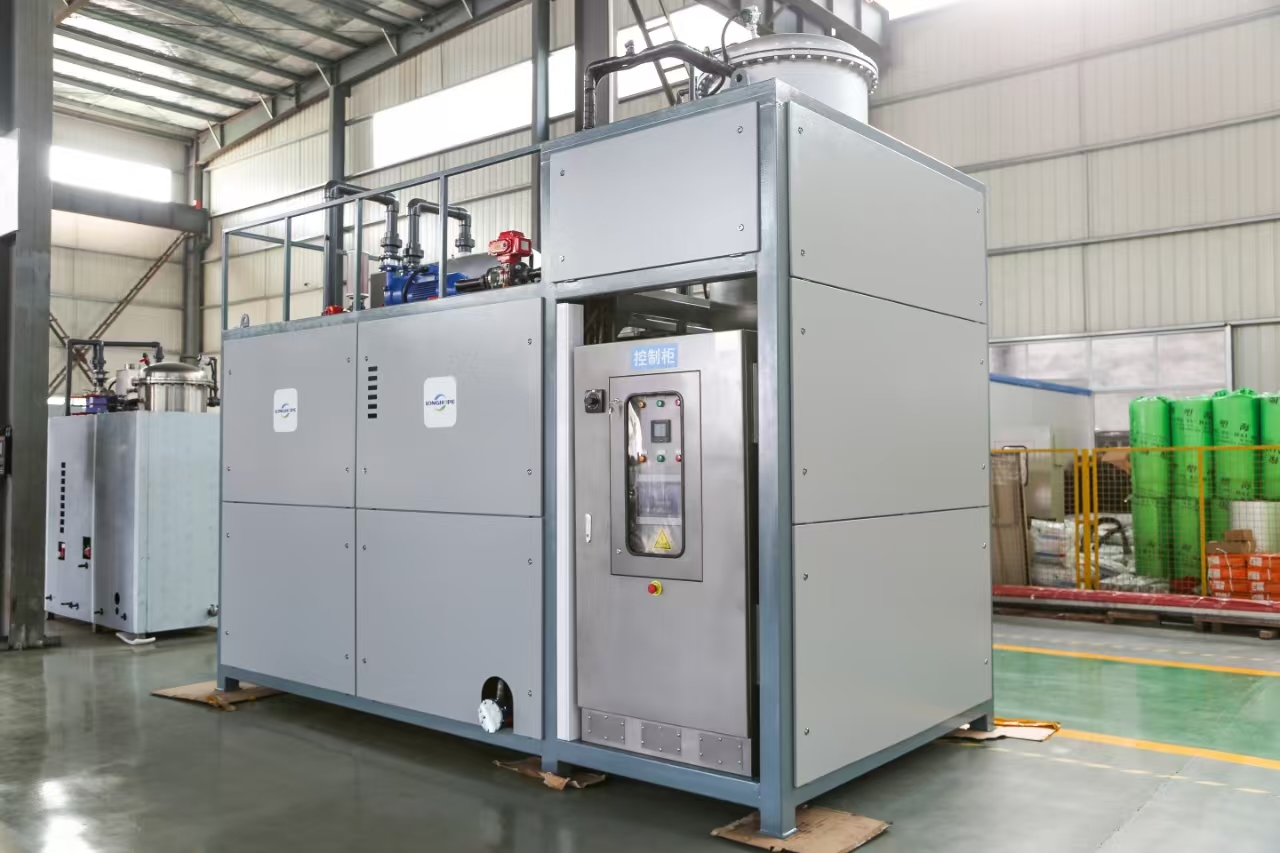
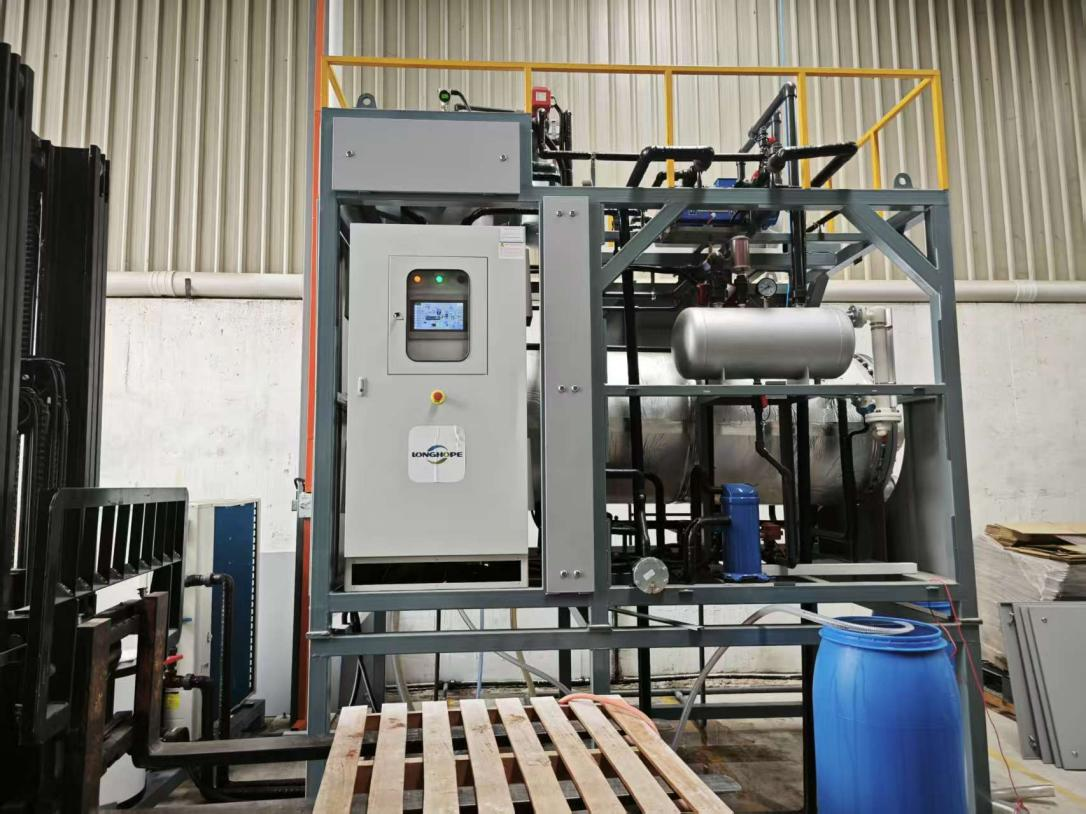
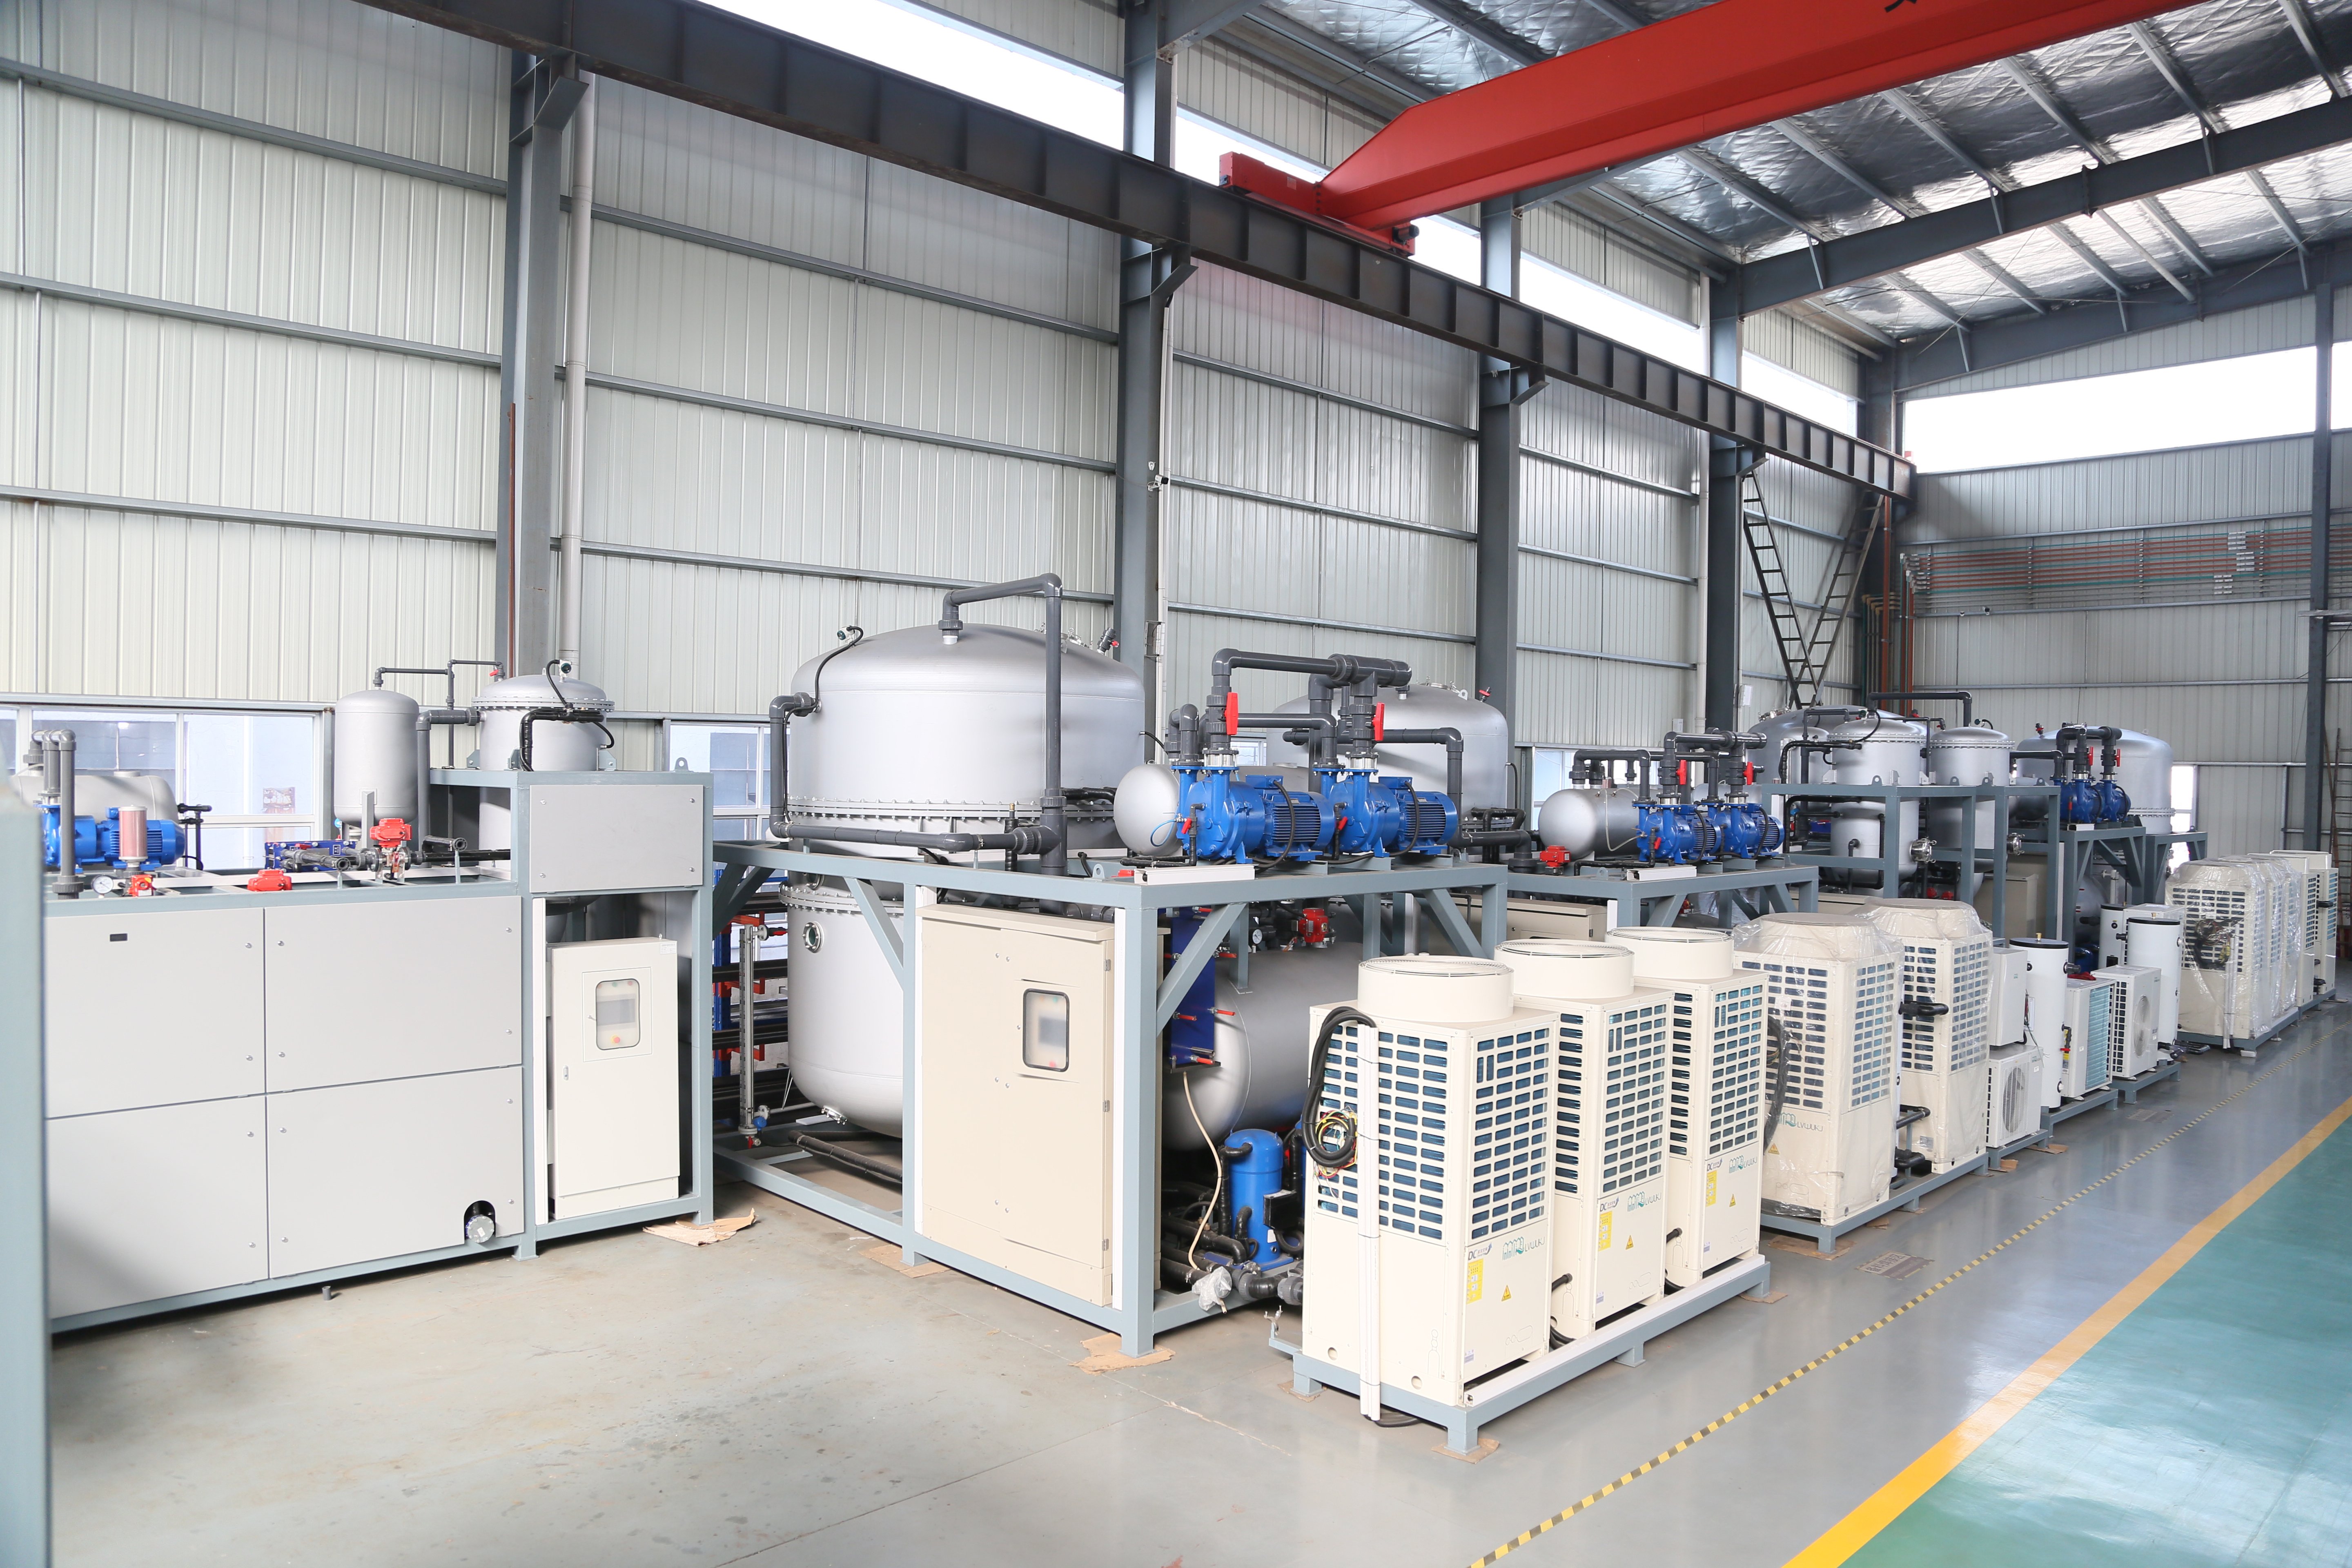
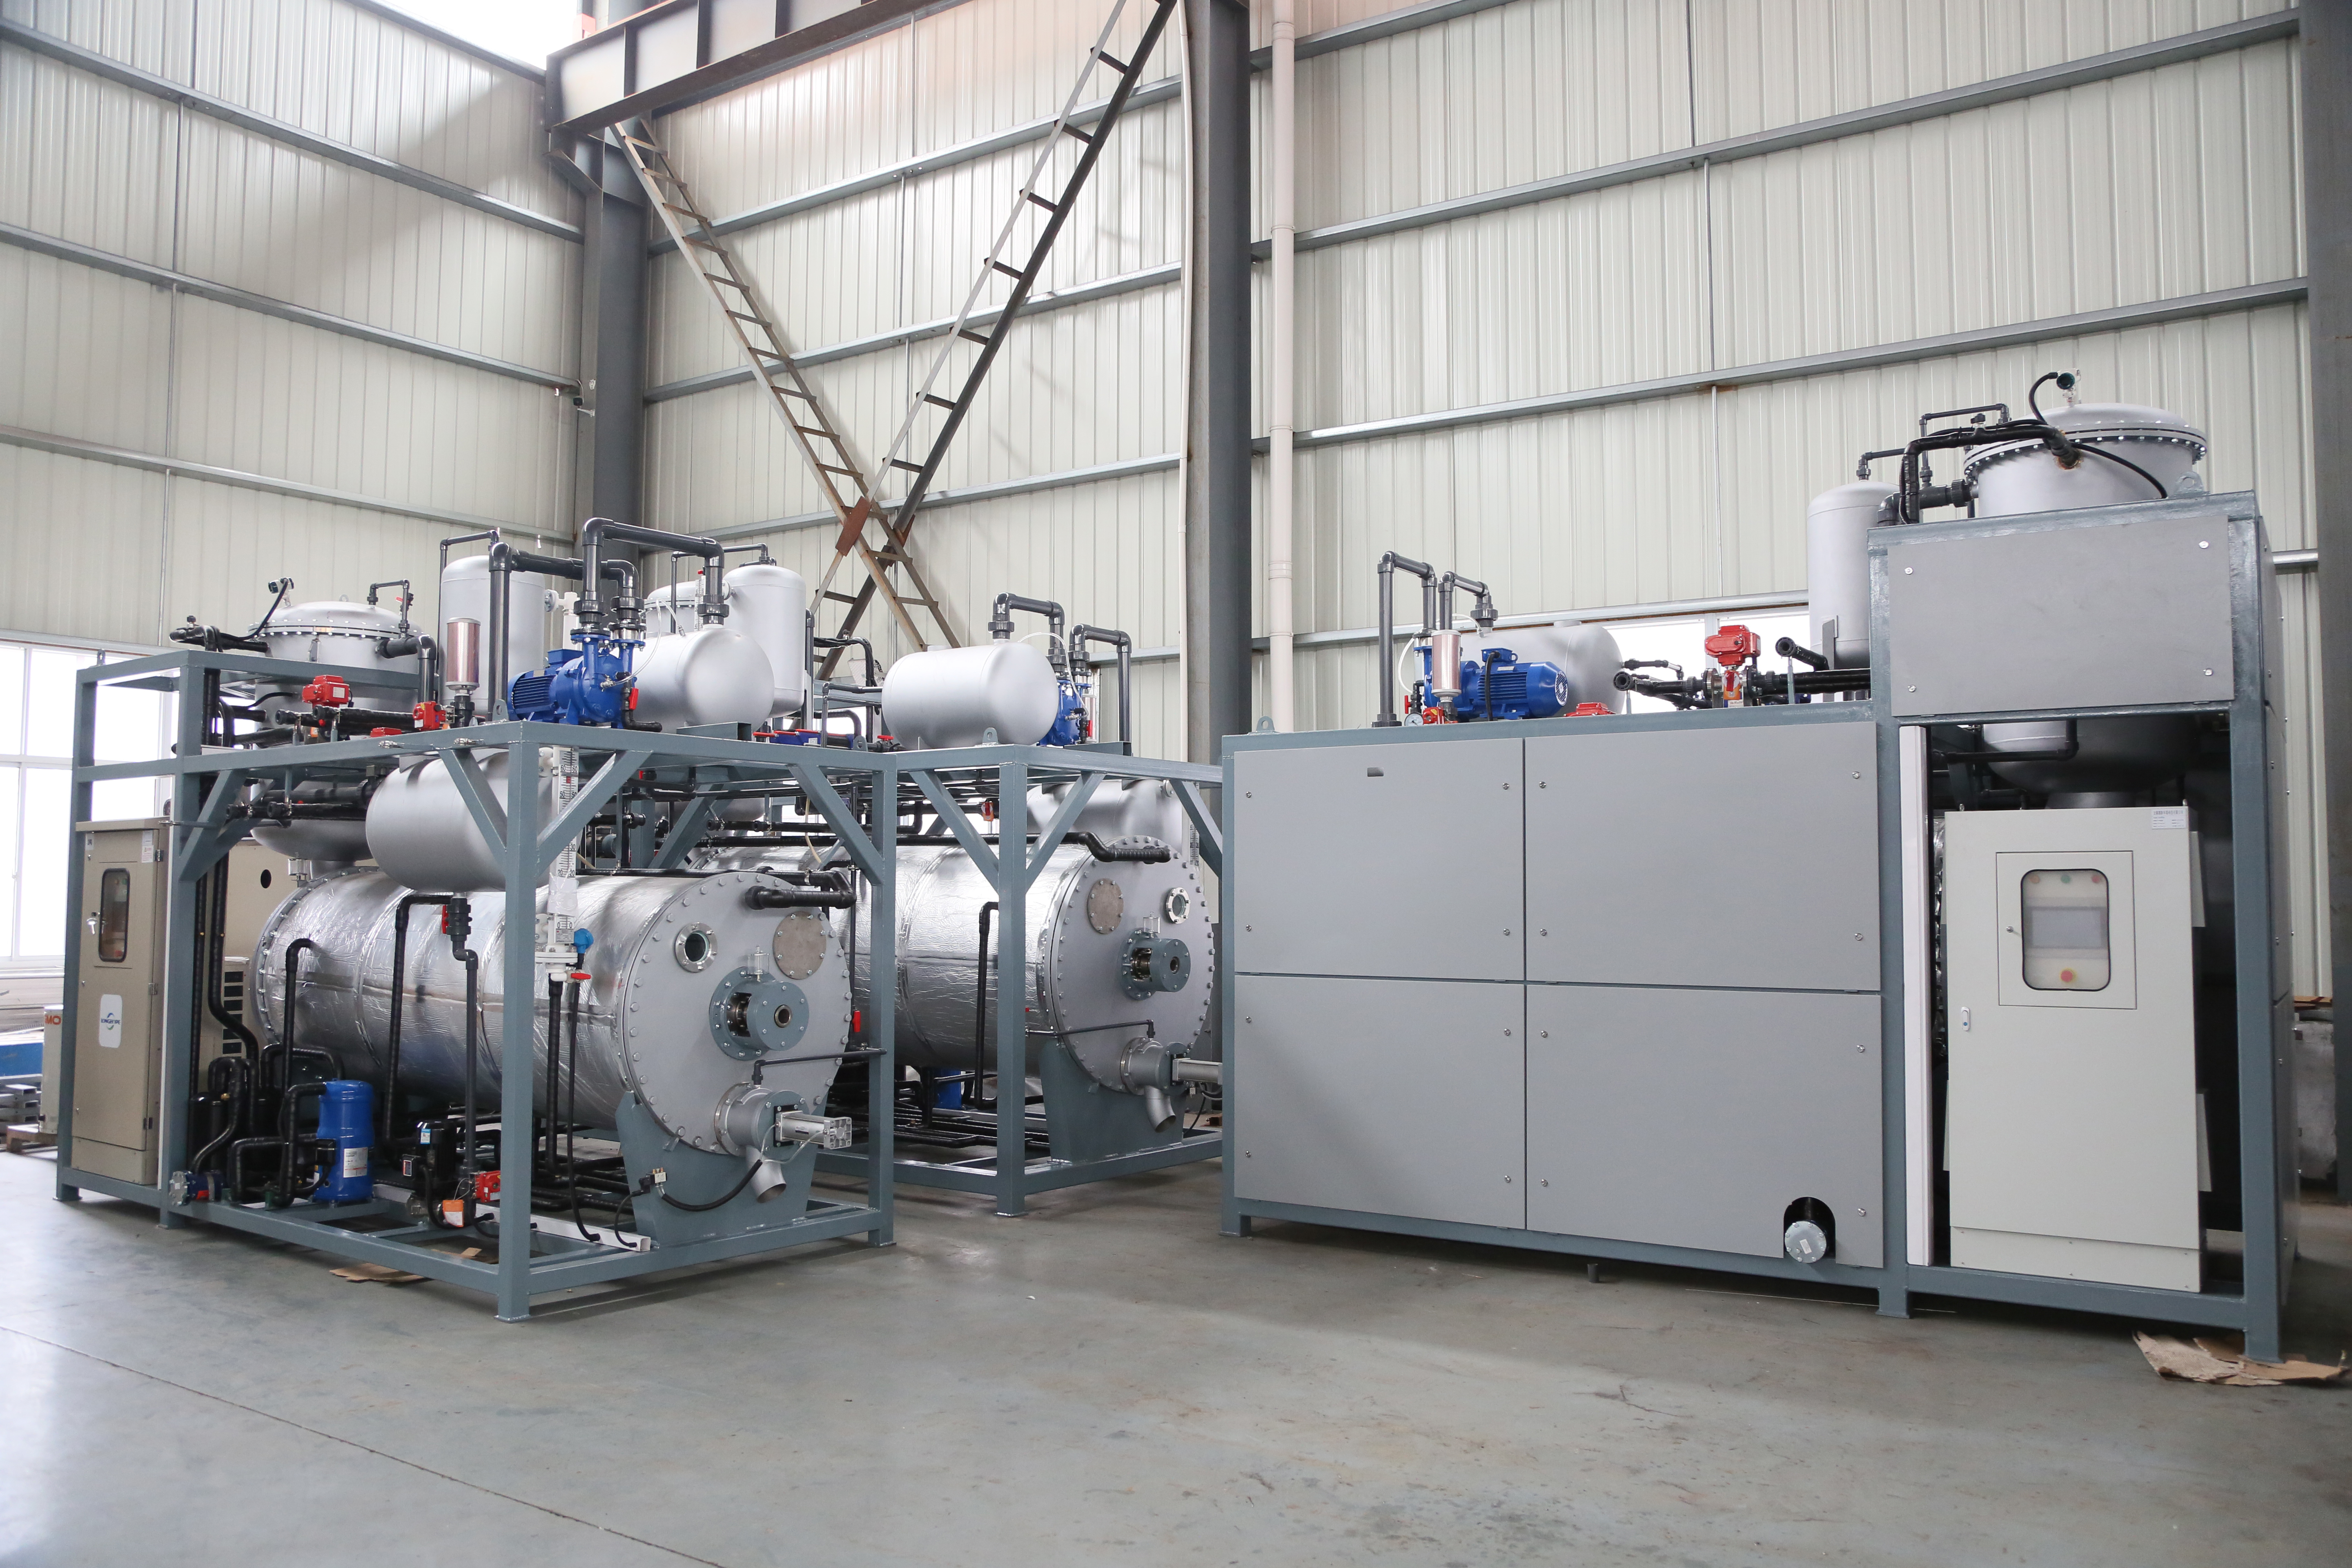
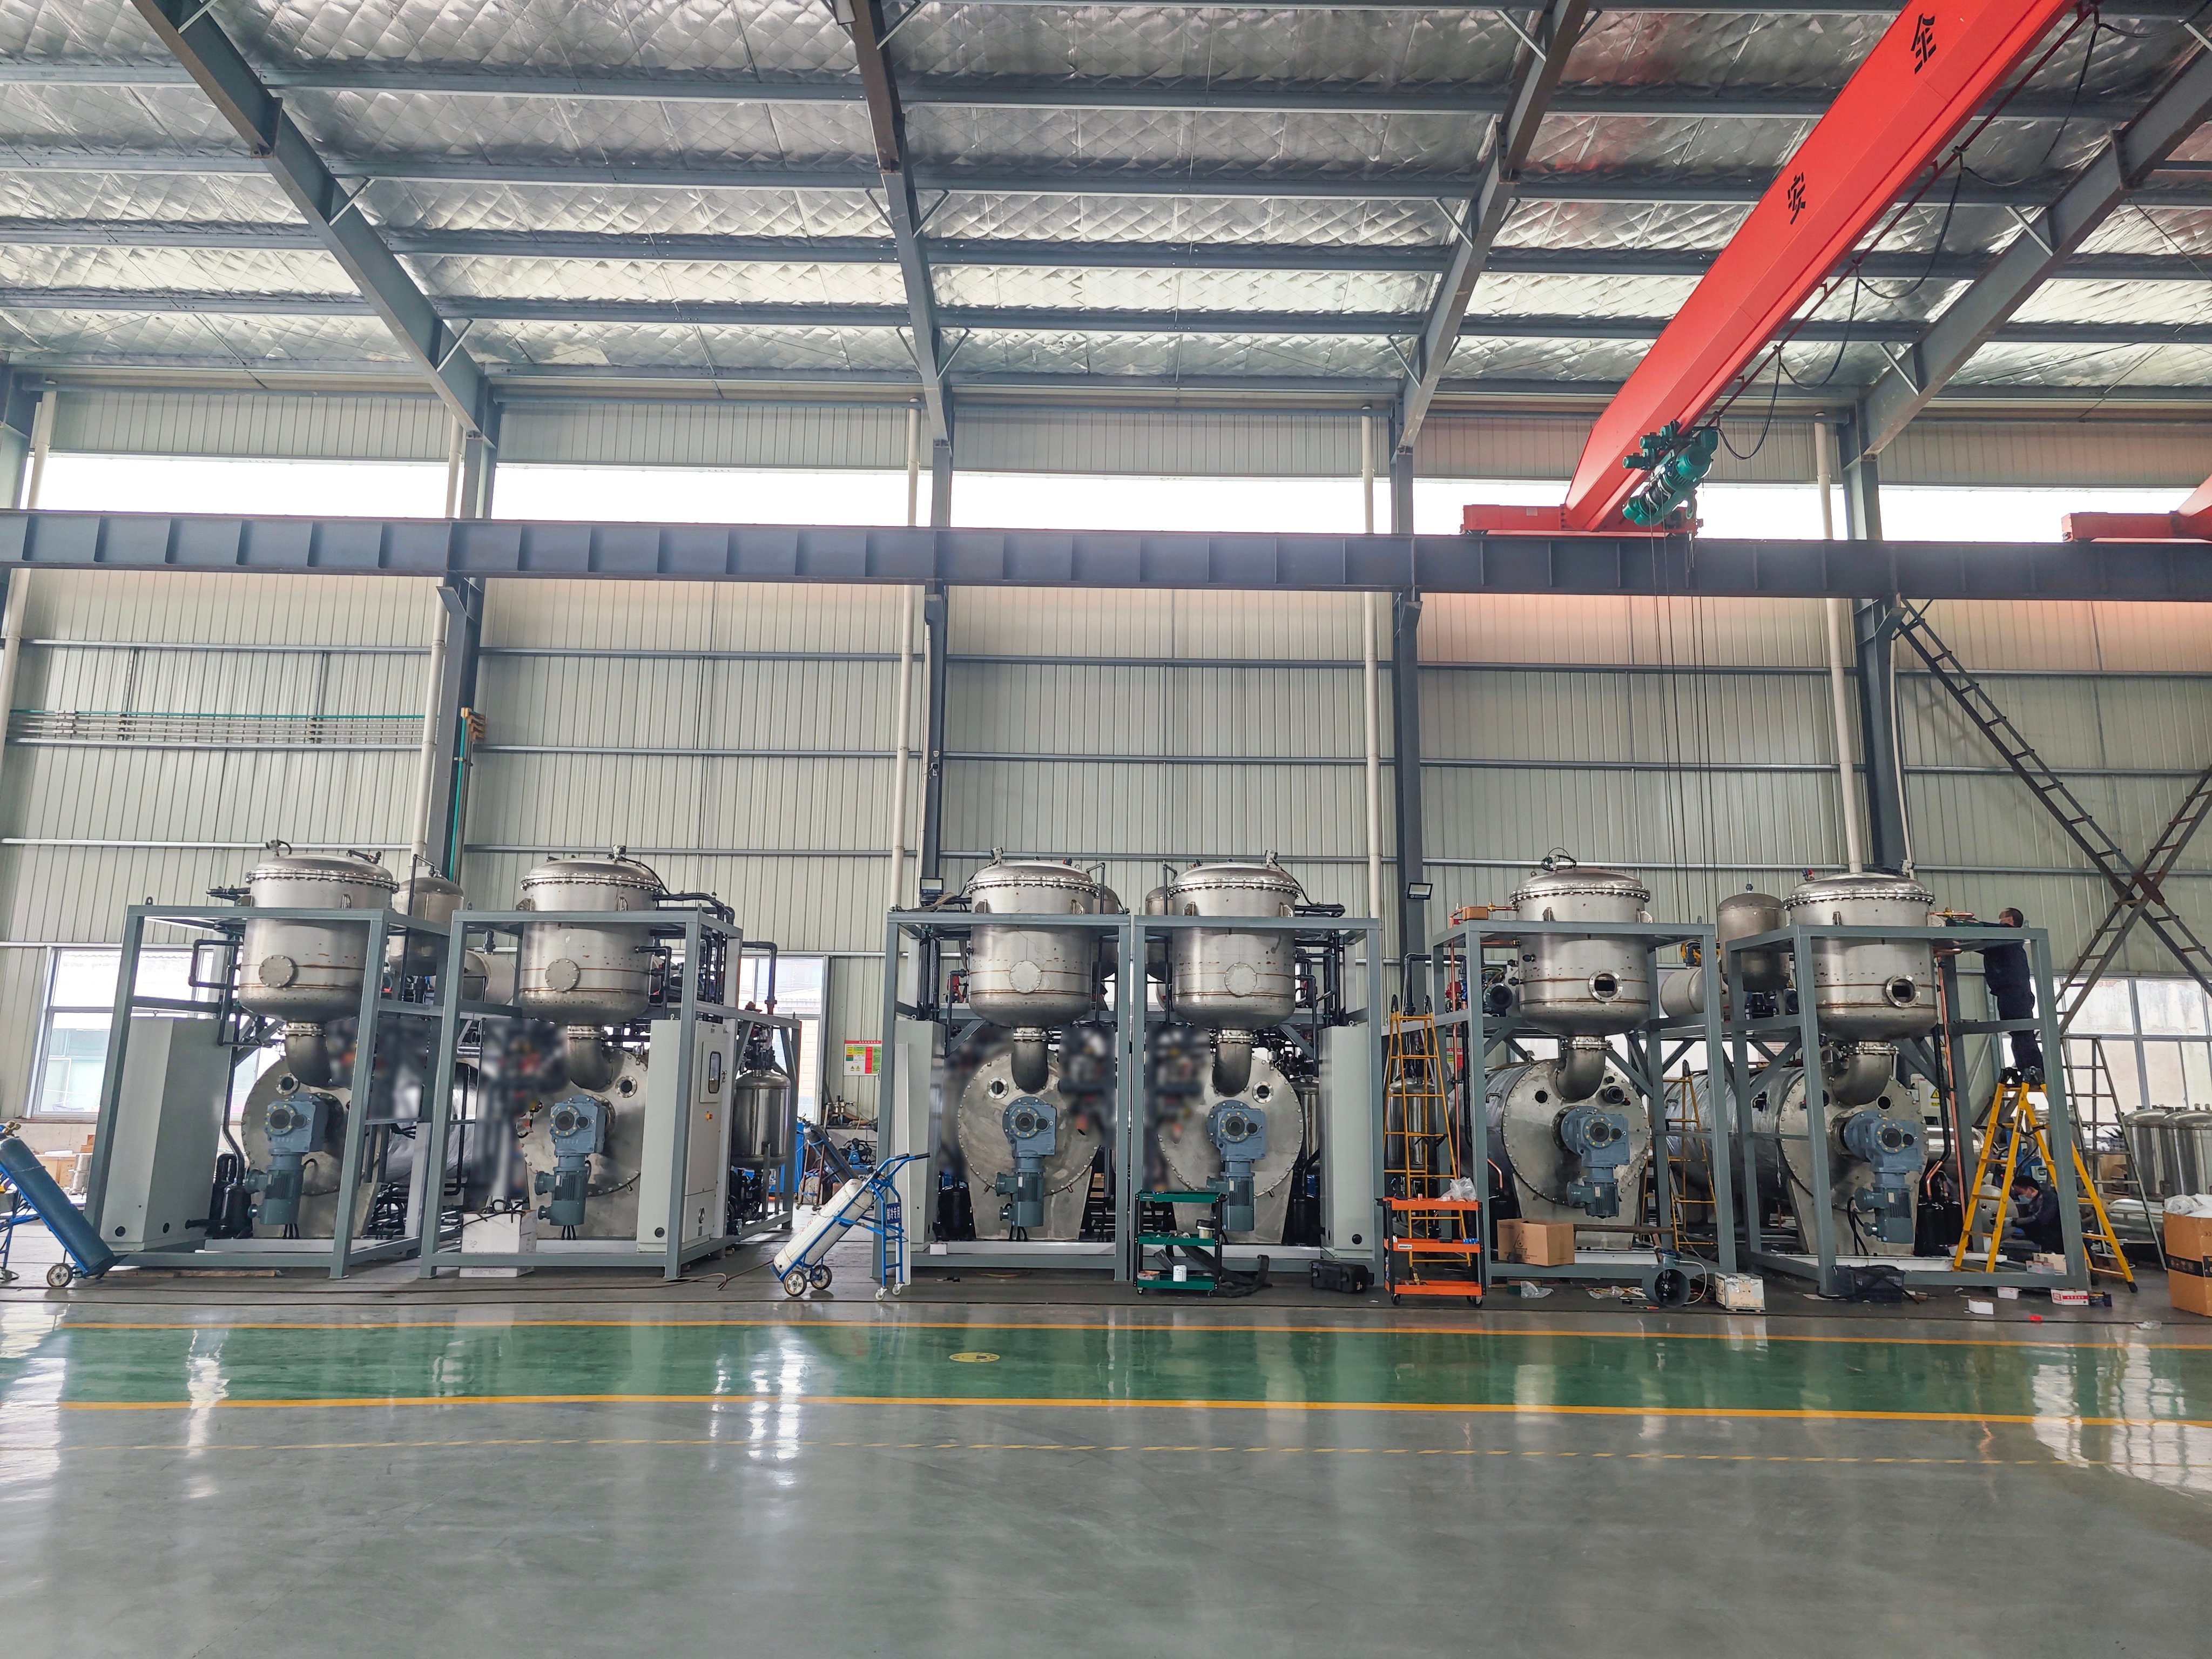
A vacuum distillation system supplier provides specialized equipment designed to separate liquid mixtures through distillation under reduced pressure conditions. This technology represents a critical solution for industries requiring precise separation of temperature-sensitive compounds that would degrade under normal atmospheric pressure and heat. A professional vacuum distillation system supplier offers systems that maintain lower boiling points, enabling efficient separation without compromising product quality or integrity.
The core function of equipment from a vacuum distillation system supplier involves creating a controlled low-pressure environment where volatile components vaporize at significantly reduced temperatures. This fundamental capability makes vacuum distillation systems essential for pharmaceutical, chemical, petrochemical, and food processing applications. Modern vacuum distillation system supplier technology incorporates advanced condensing systems, vacuum pumps, and precise temperature controls to achieve optimal separation efficiency.
Key technological features include stainless steel construction for corrosion resistance, adjustable vacuum levels ranging from moderate to high vacuum conditions, and integrated heating systems with precise temperature regulation. A reliable vacuum distillation system supplier ensures their equipment includes safety mechanisms, pressure relief valves, and monitoring systems for operational security.
Applications serviced by a leading vacuum distillation system supplier span numerous industries. Essential uses include essential oil extraction, pharmaceutical compound purification, biodiesel production, waste oil recycling, and specialty chemical manufacturing. The versatility of systems from a quality vacuum distillation system supplier makes them indispensable for processing heat-sensitive materials that require gentle, controlled separation methods.

 EN