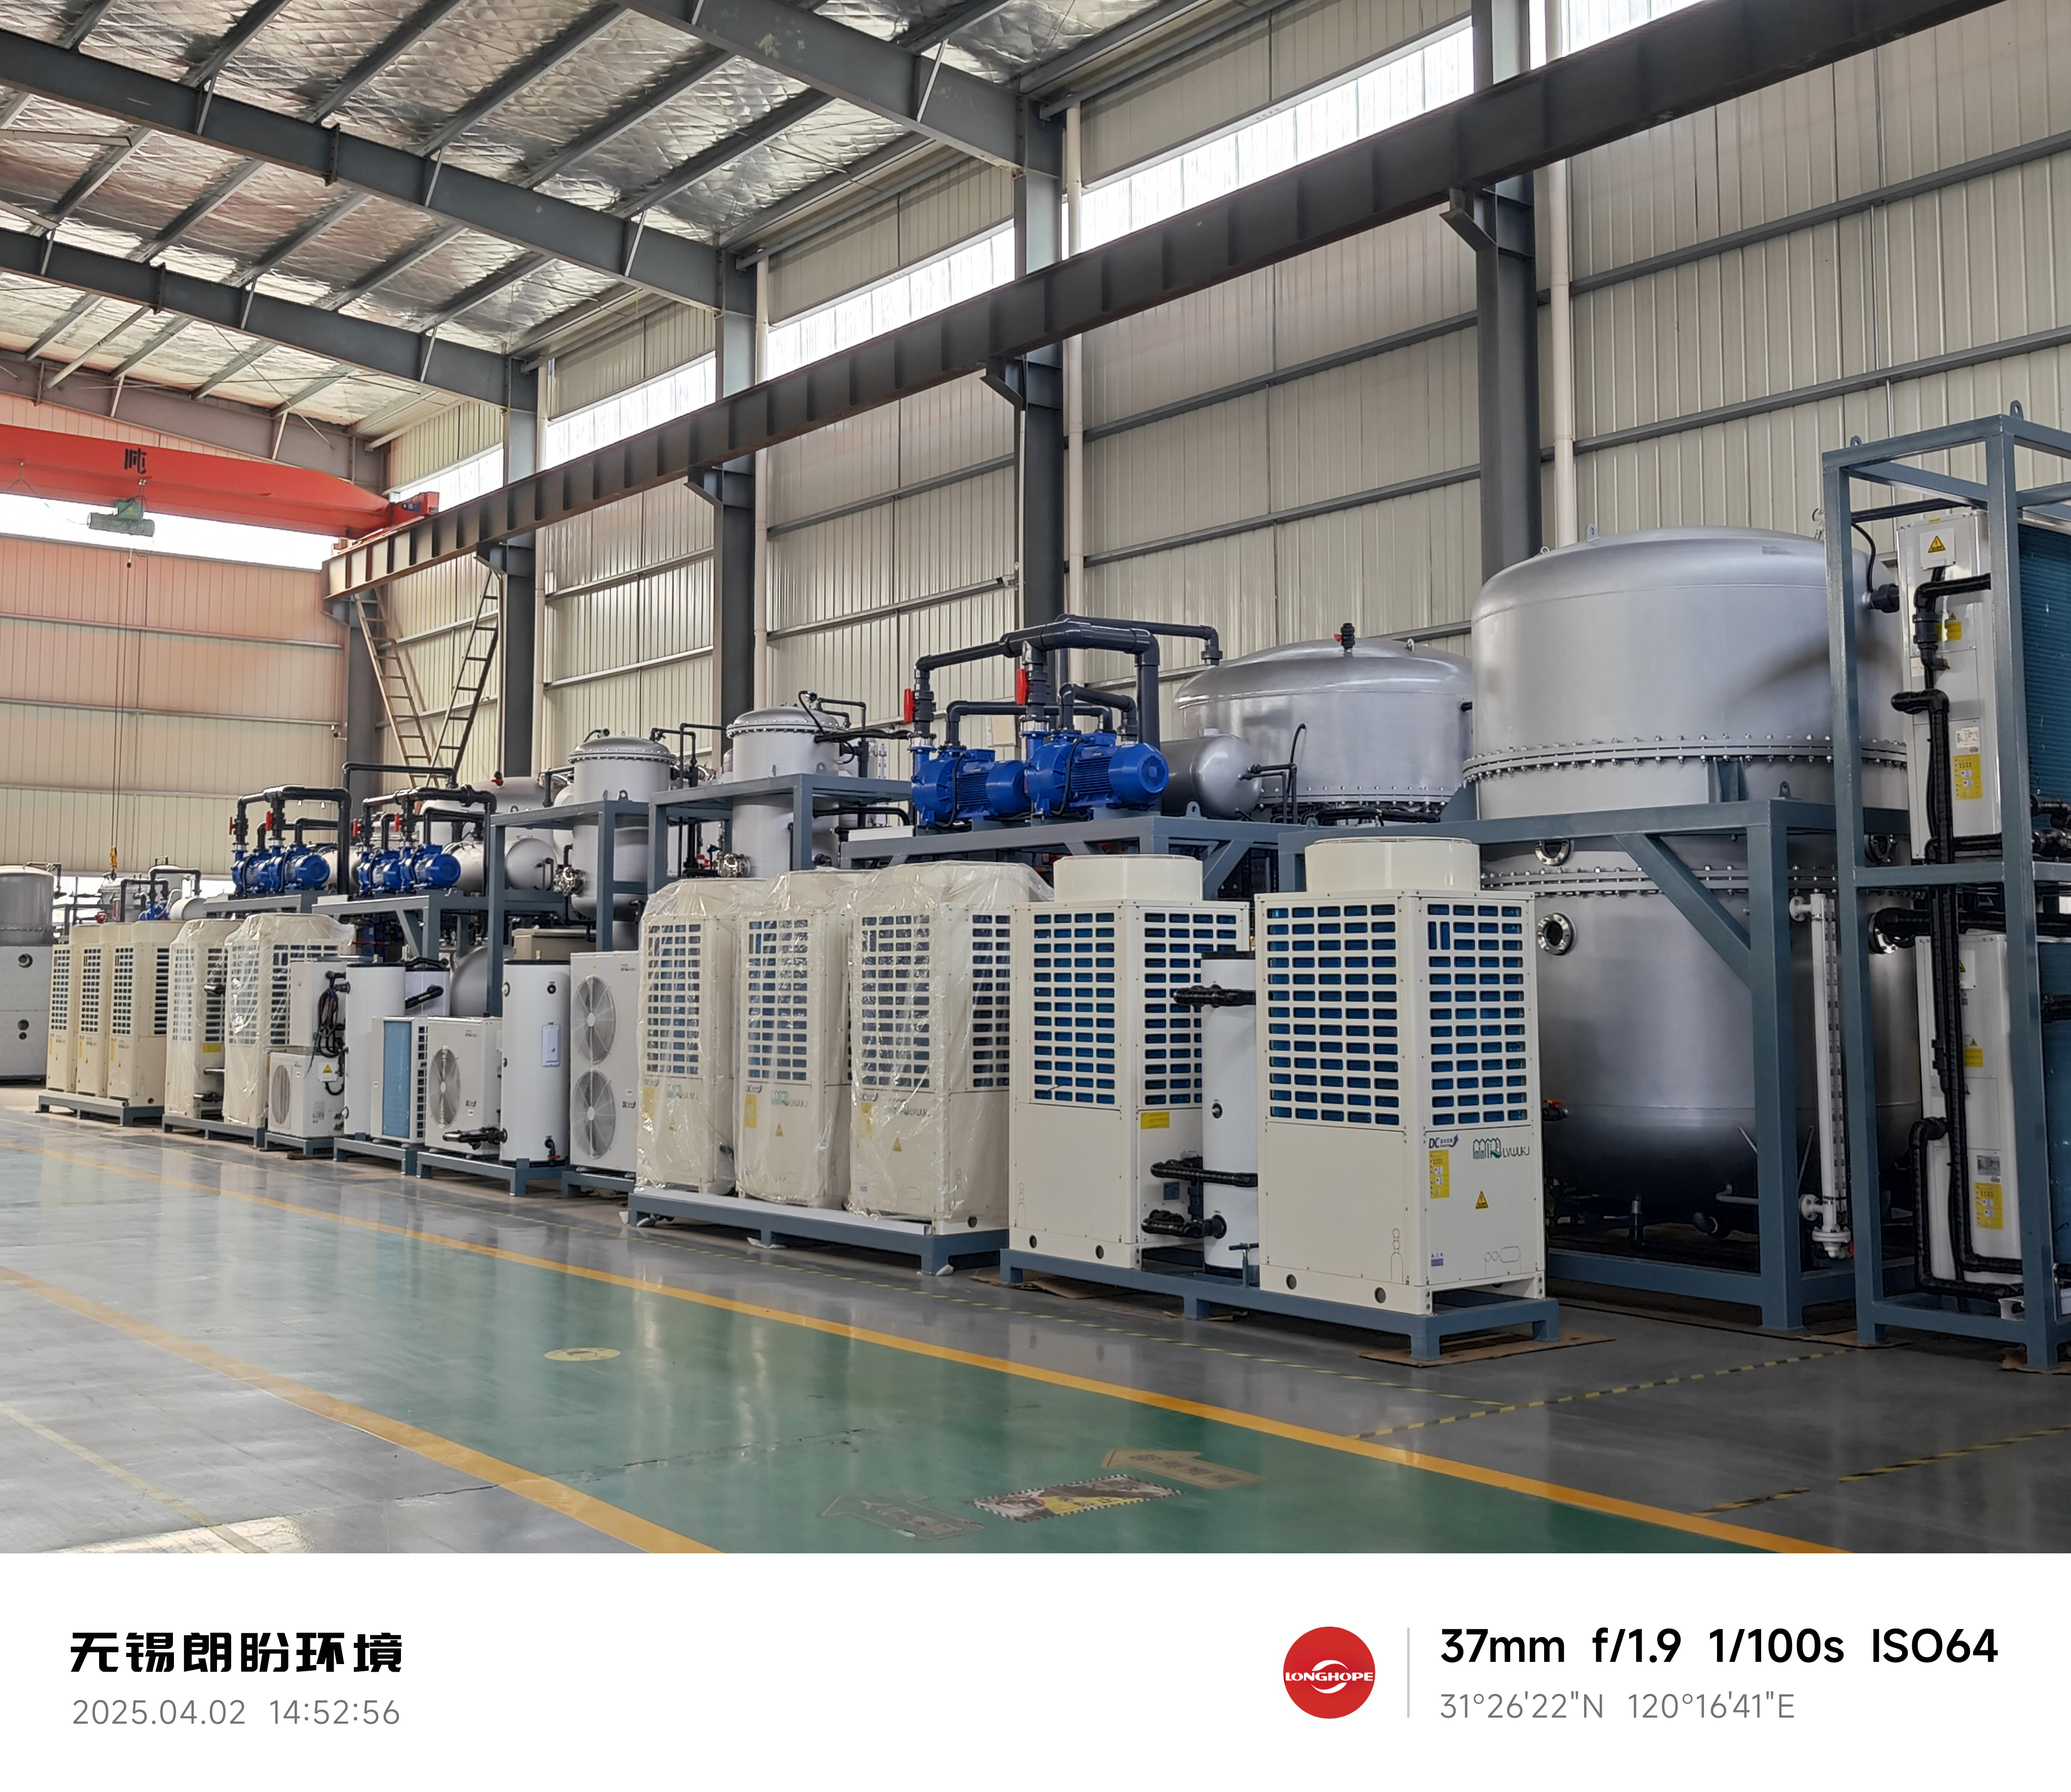
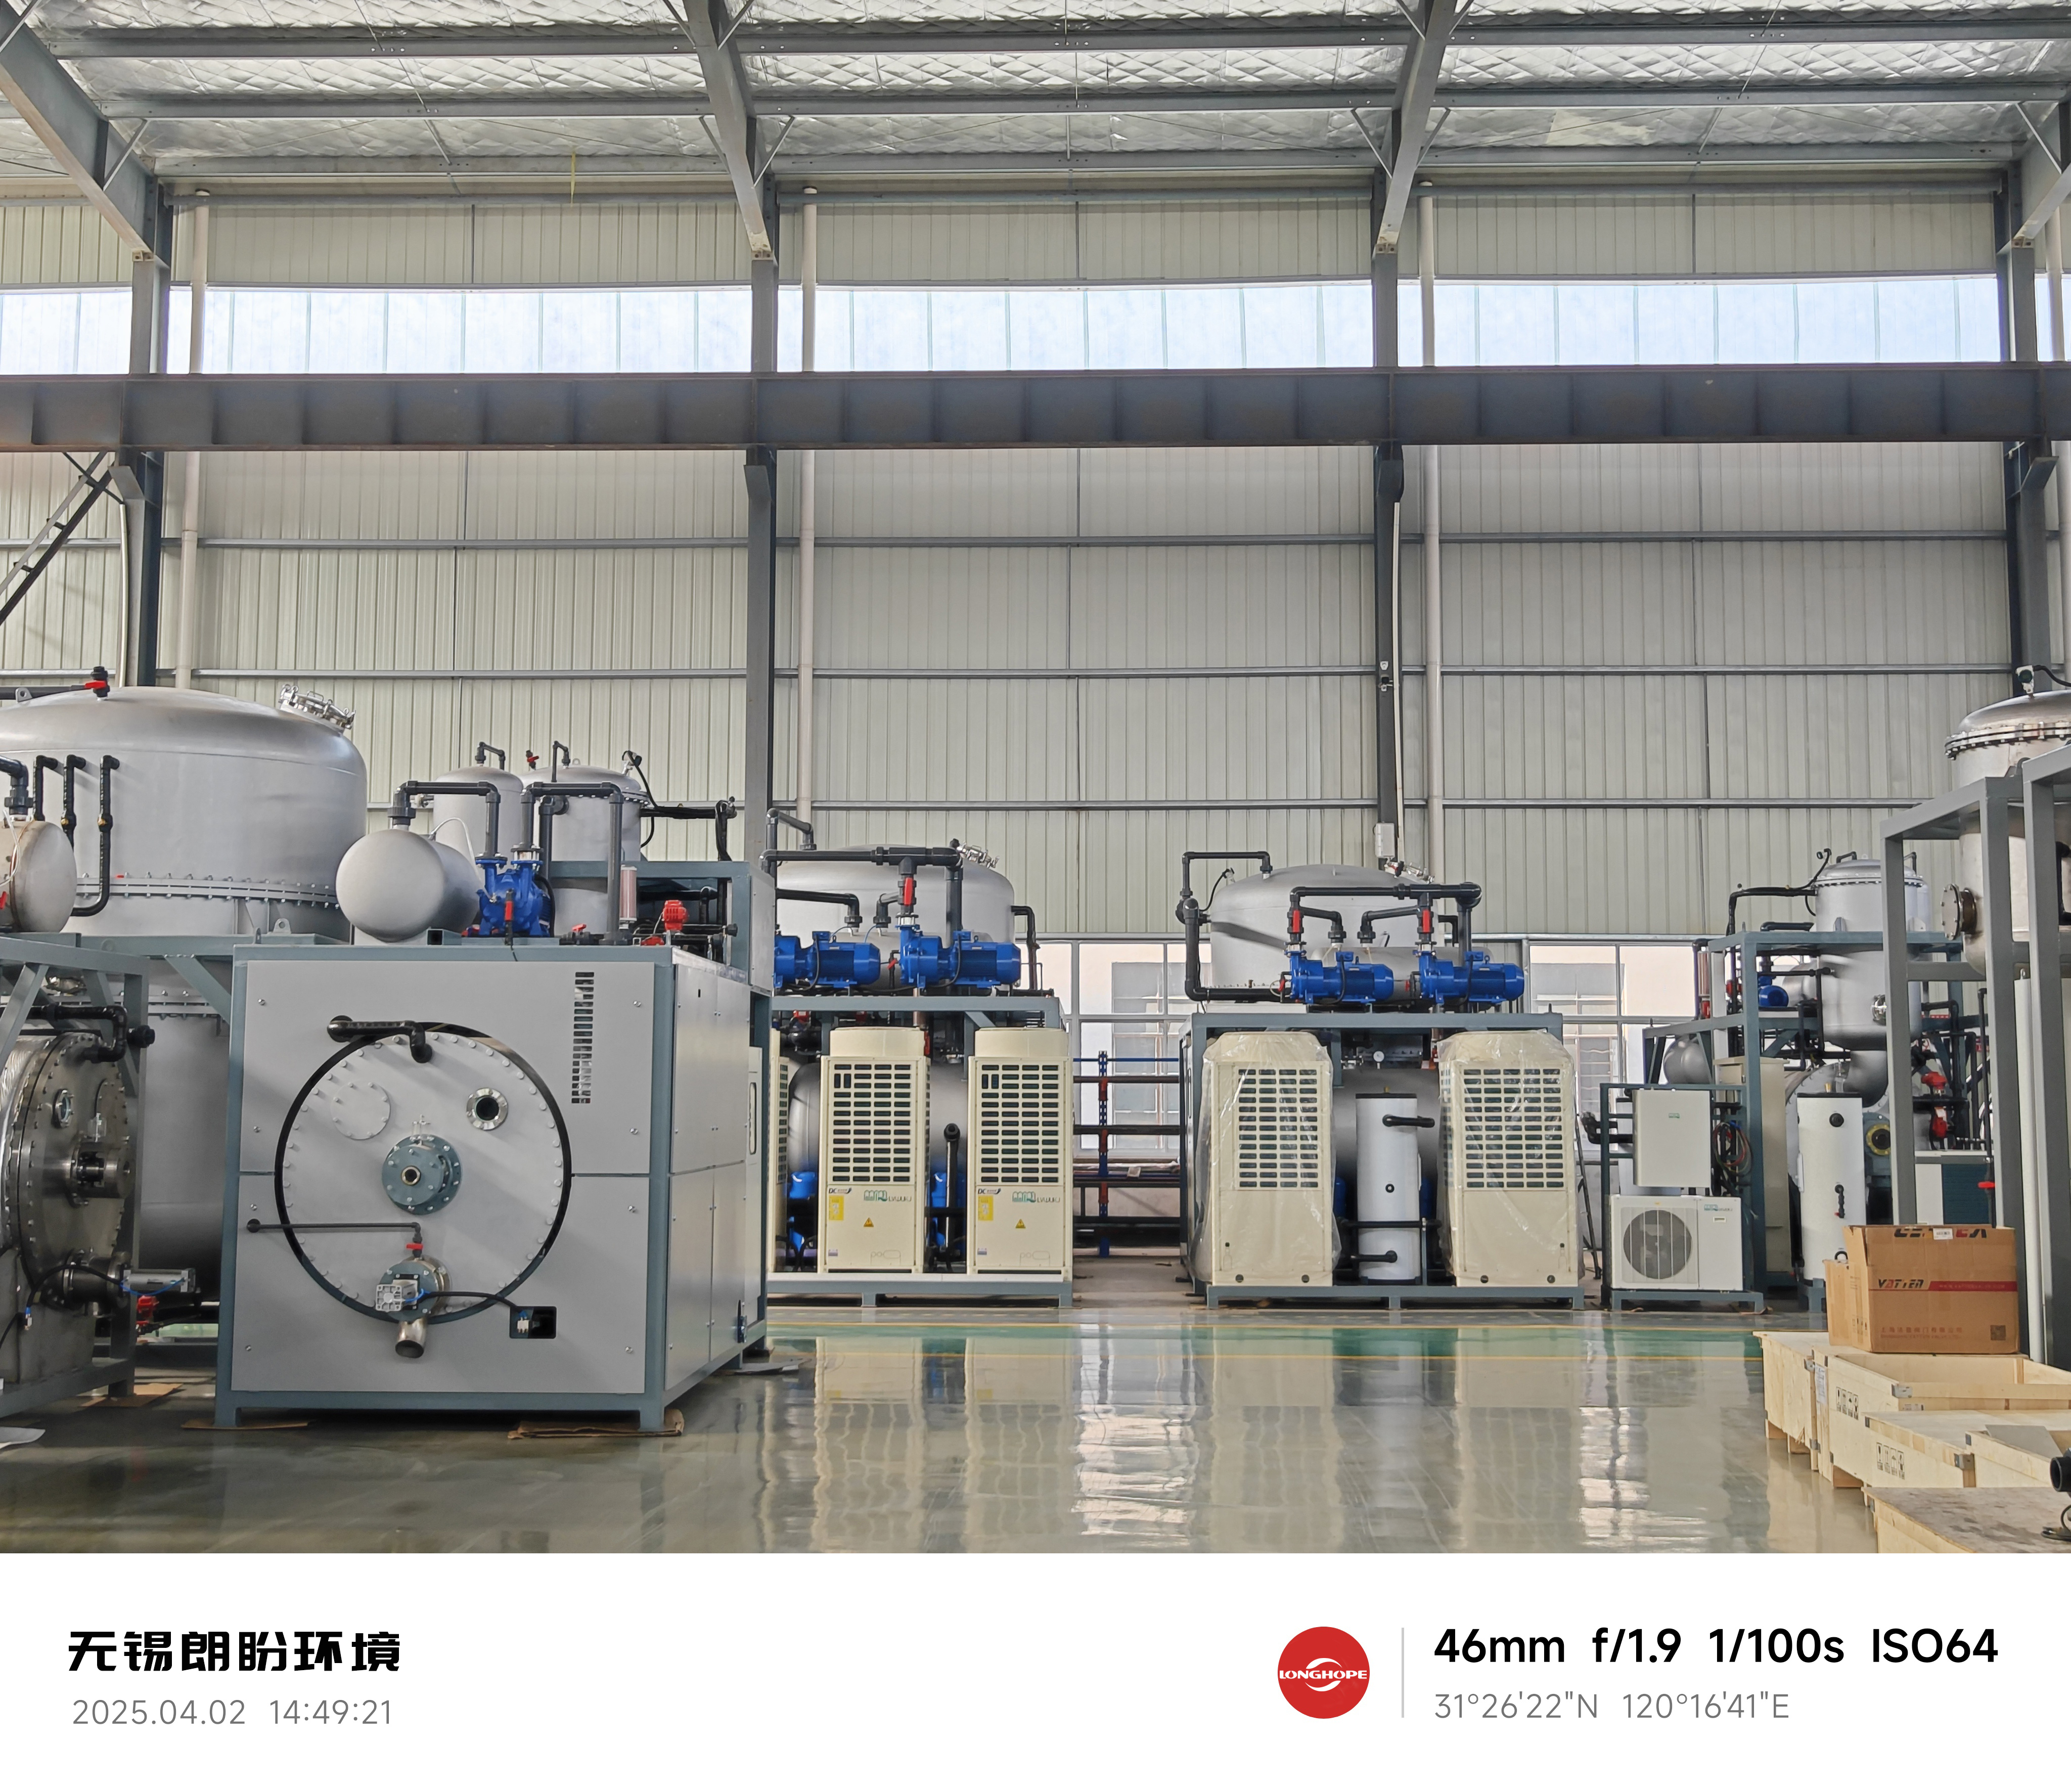
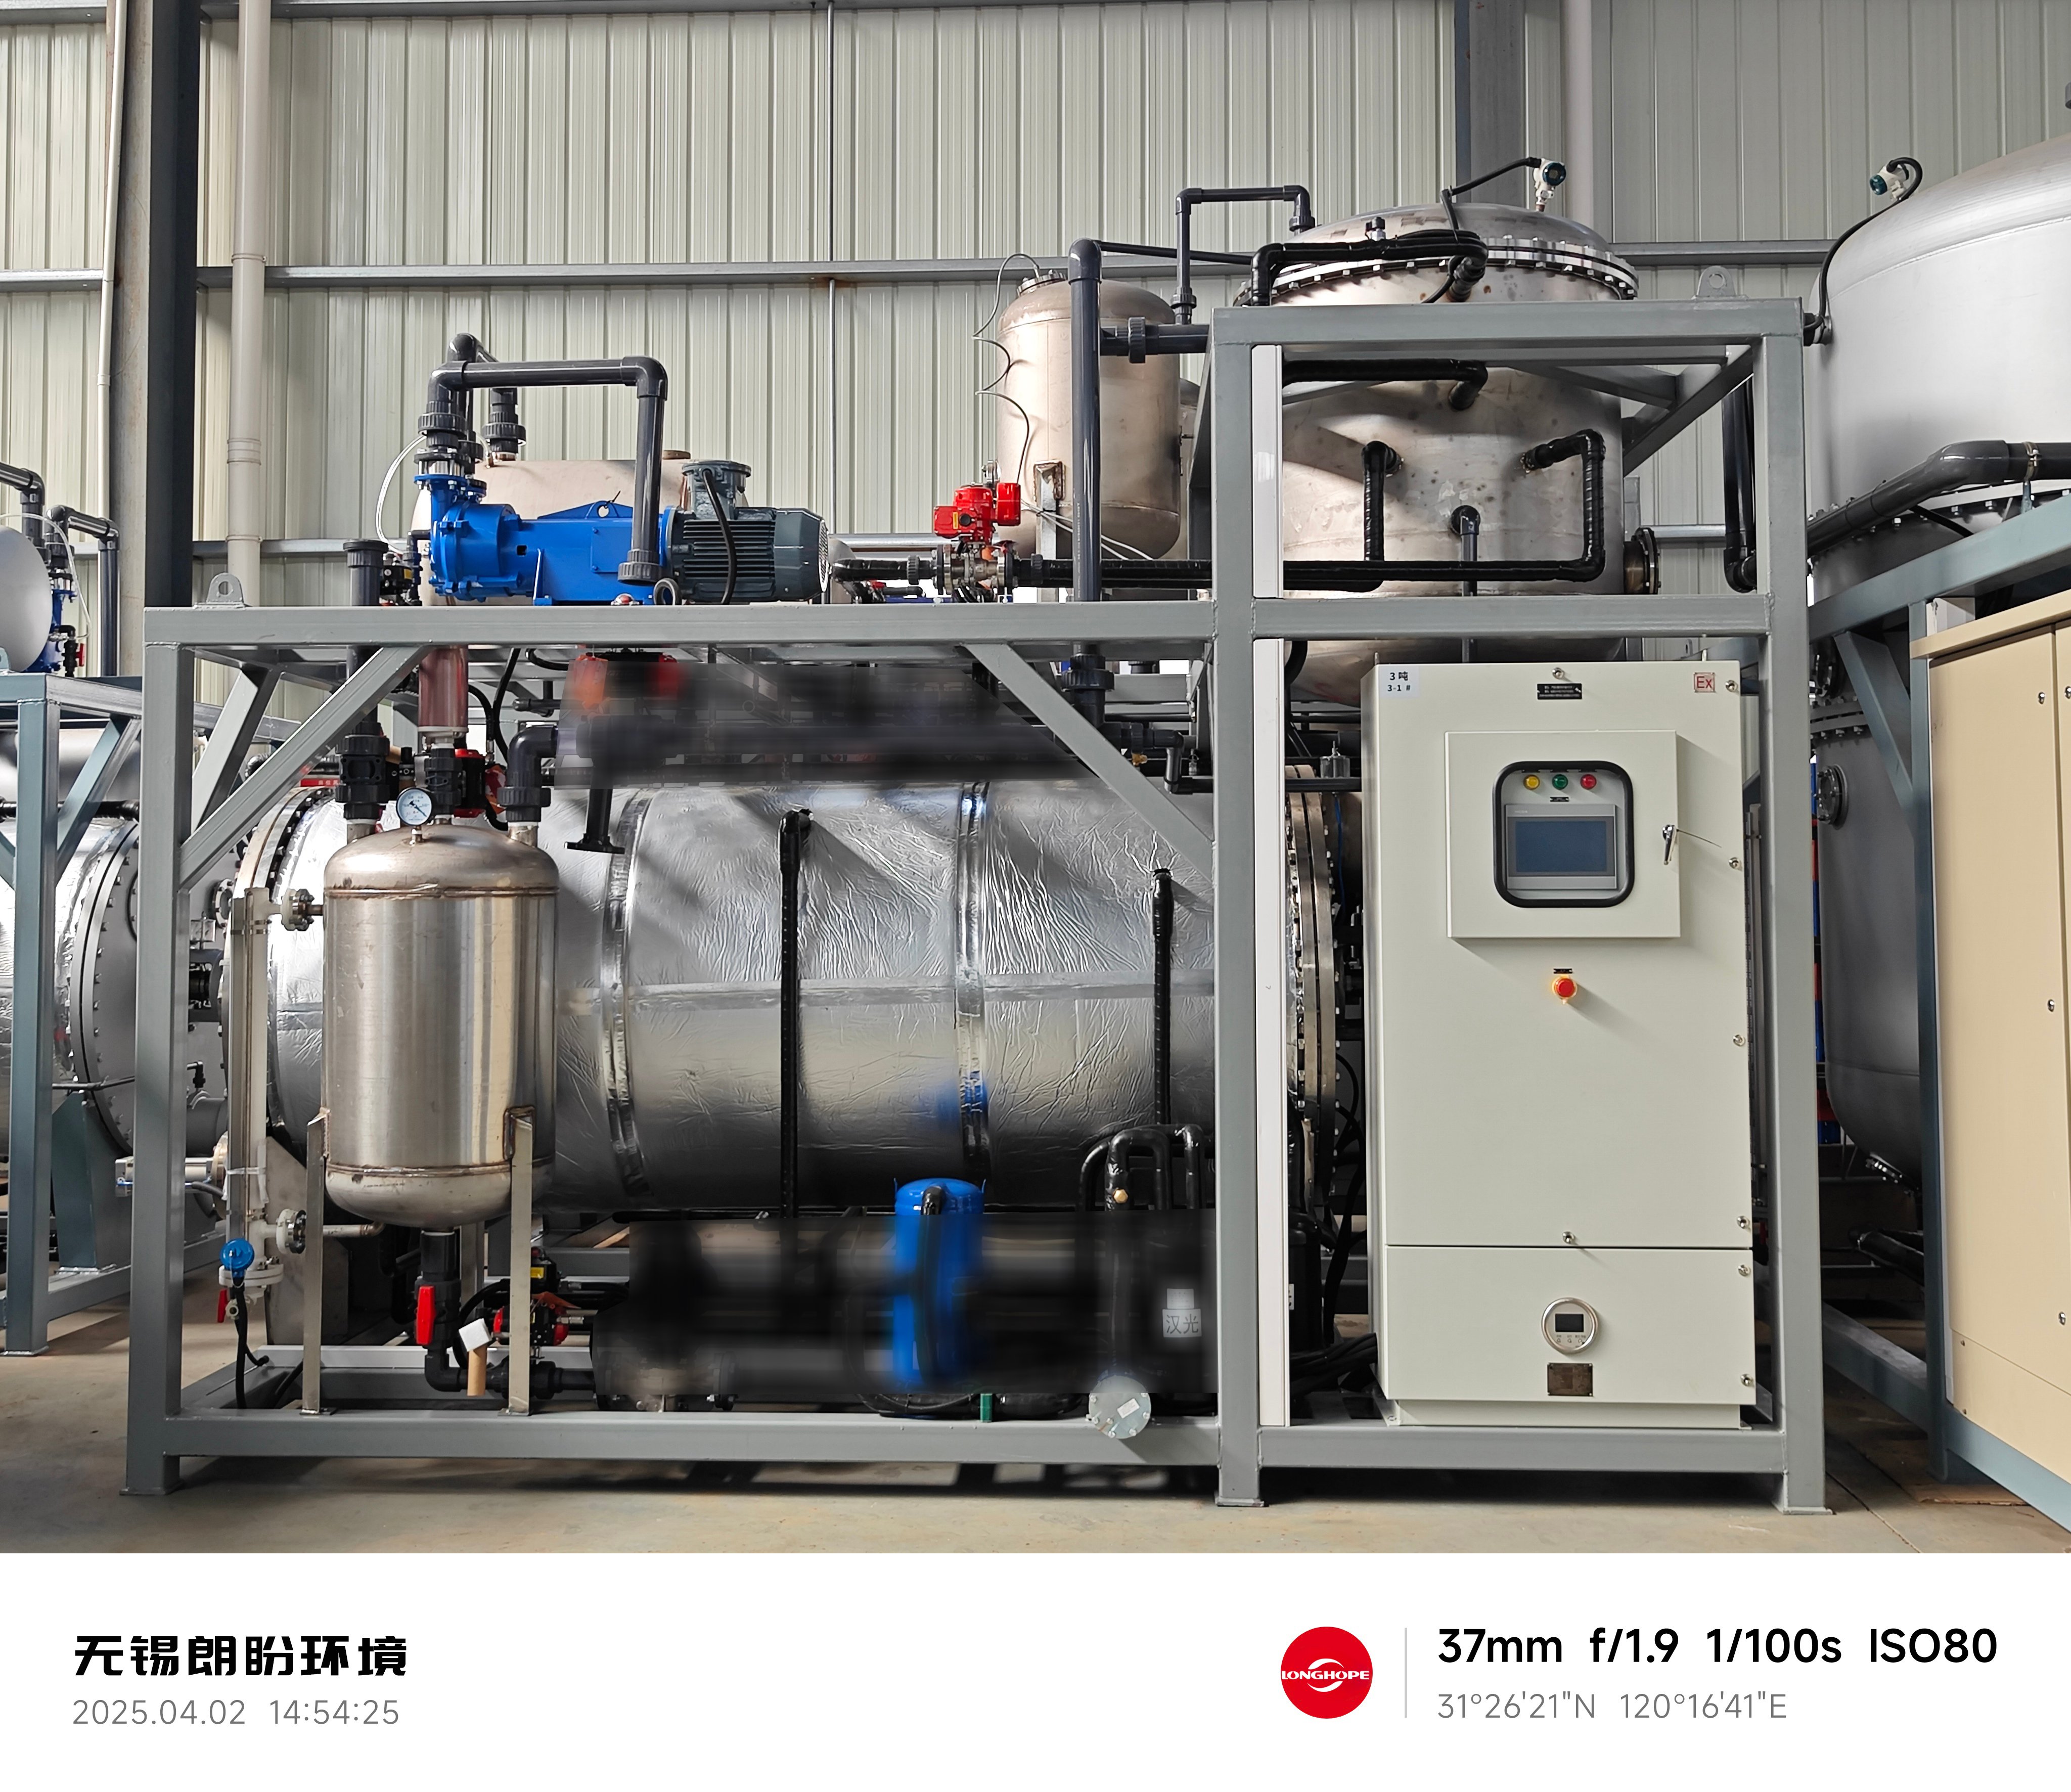
industrial vacuum distillation manufacturer
An industrial vacuum distillation manufacturer specializes in producing advanced equipment designed to separate and purify liquid mixtures through controlled evaporation under reduced pressure conditions. These sophisticated systems operate by lowering atmospheric pressure within a sealed chamber, enabling liquids to evaporate at temperatures significantly lower than their normal boiling points. This capability makes an industrial vacuum distillation manufacturer essential for processing heat-sensitive materials that would degrade at conventional temperatures.
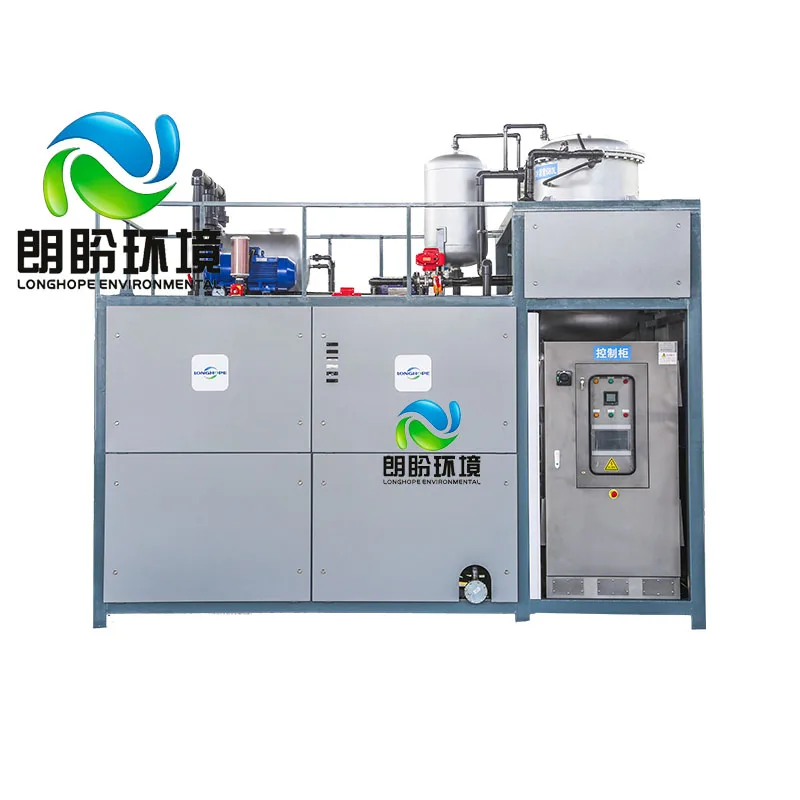
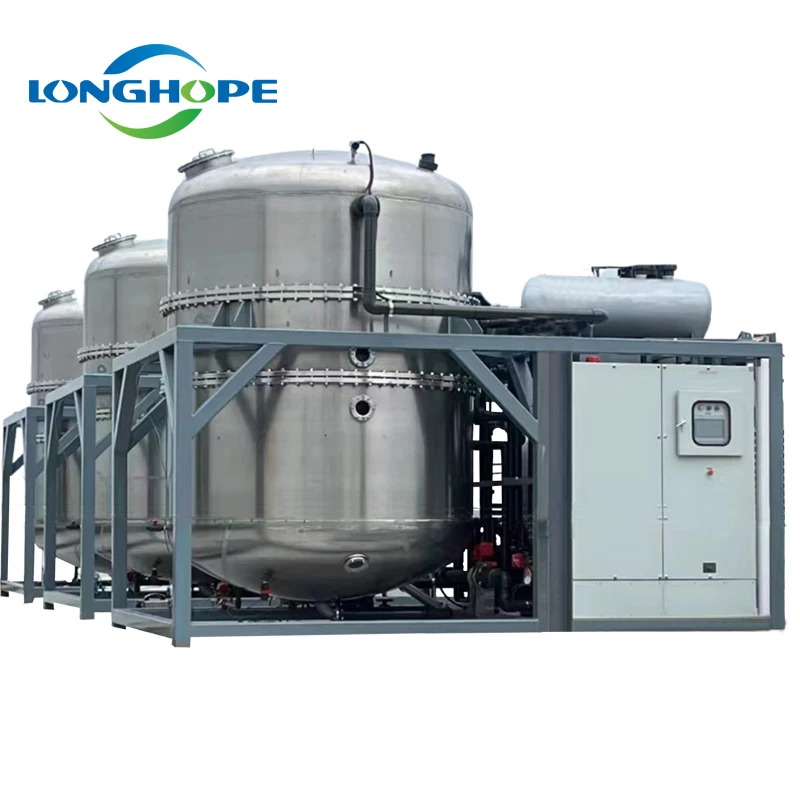
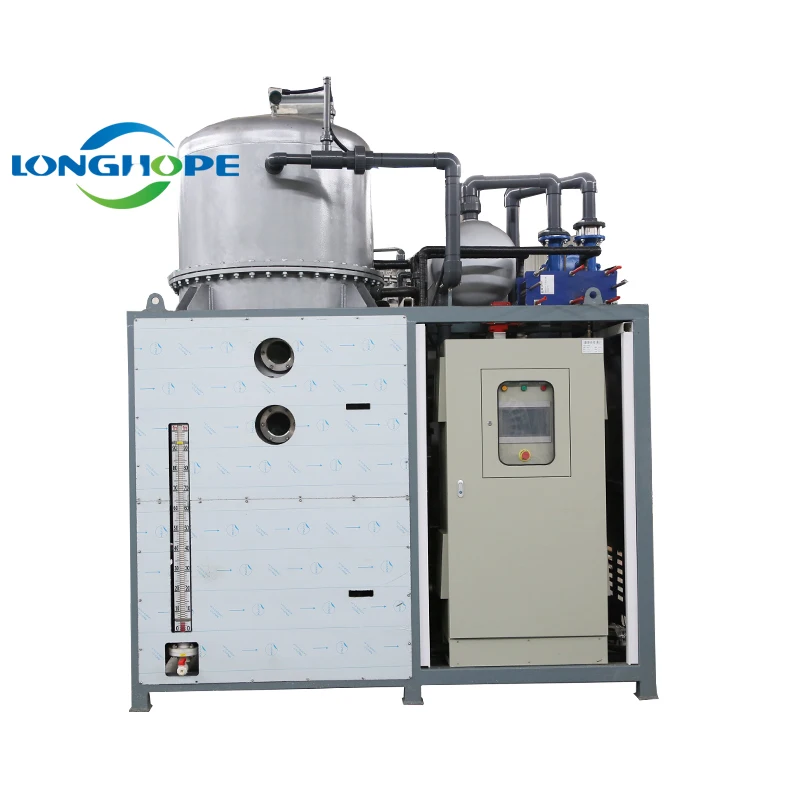
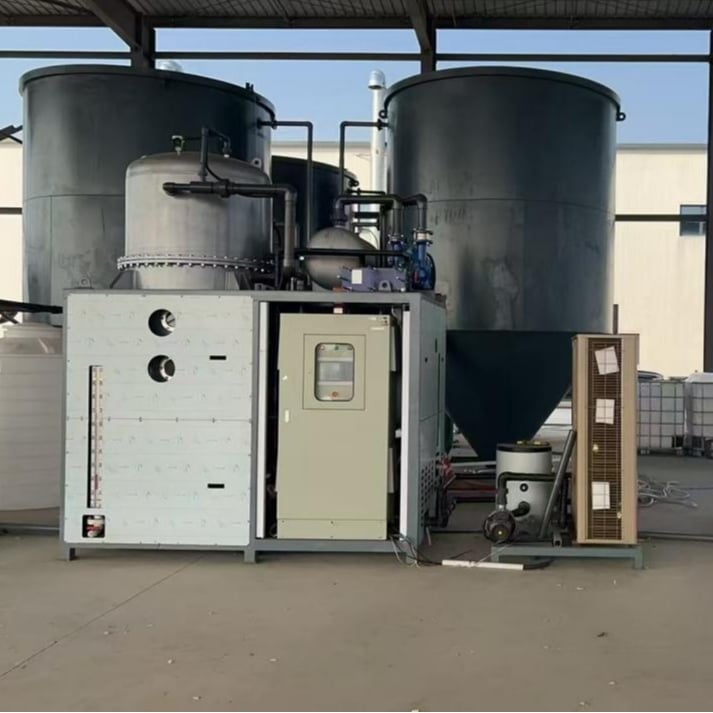
The primary functions of an industrial vacuum distillation manufacturer include designing, engineering, and constructing distillation units that handle complex separation challenges across multiple industries. These systems feature precise temperature control, vacuum regulation systems, and condensation technology that ensures efficient separation of components with varying volatility levels. An industrial vacuum distillation manufacturer incorporates advanced materials and engineering solutions to maximize throughput while maintaining product quality and safety standards.
Technological features include stainless steel construction, multi-stage condensers, automated vacuum monitoring systems, and integrated safety mechanisms. The equipment operates on principles of molecular weight and boiling point differences, allowing manufacturers to achieve superior purity levels. Applications span pharmaceutical production, chemical refinement, essential oil extraction, food processing, and waste recovery operations. An industrial vacuum distillation manufacturer delivers customized solutions addressing specific industry requirements, offering both batch and continuous processing capabilities. These manufacturers provide complete systems with comprehensive support, training, and maintenance services to ensure optimal performance and reliability throughout the equipment's operational lifespan.

 EN