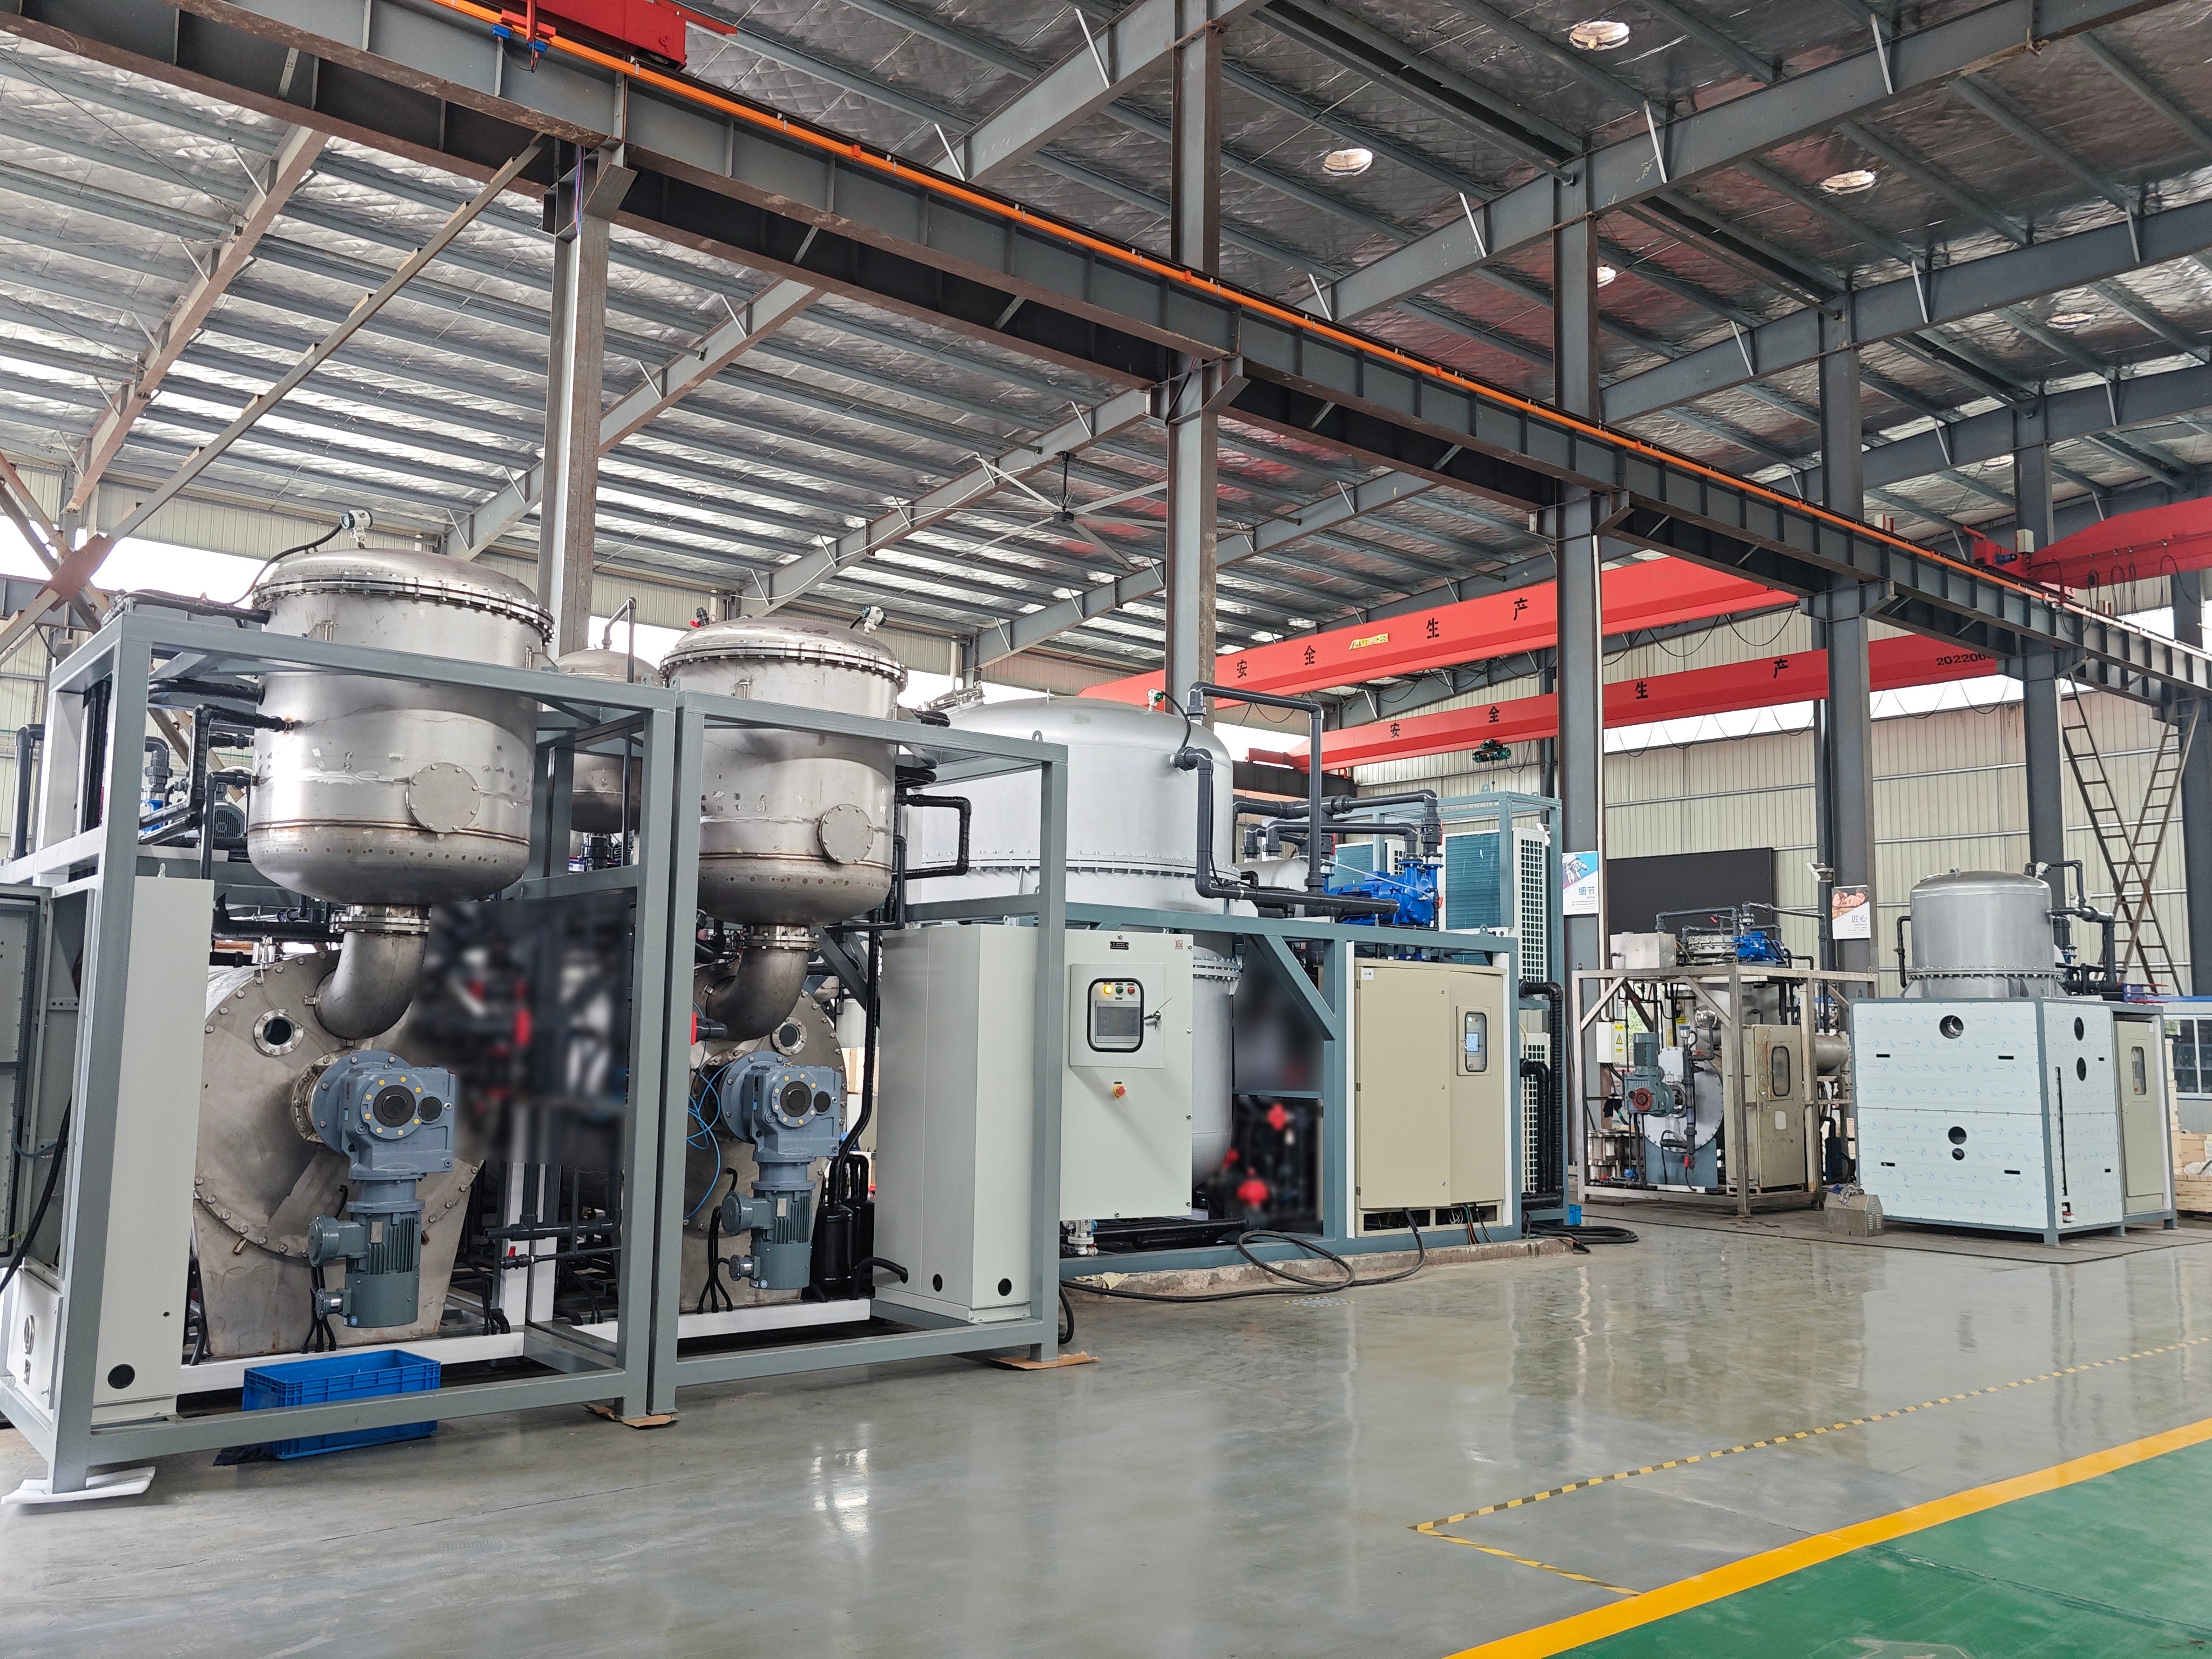
Custom Vacuum Distillation System

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

custom vacuum distillation system

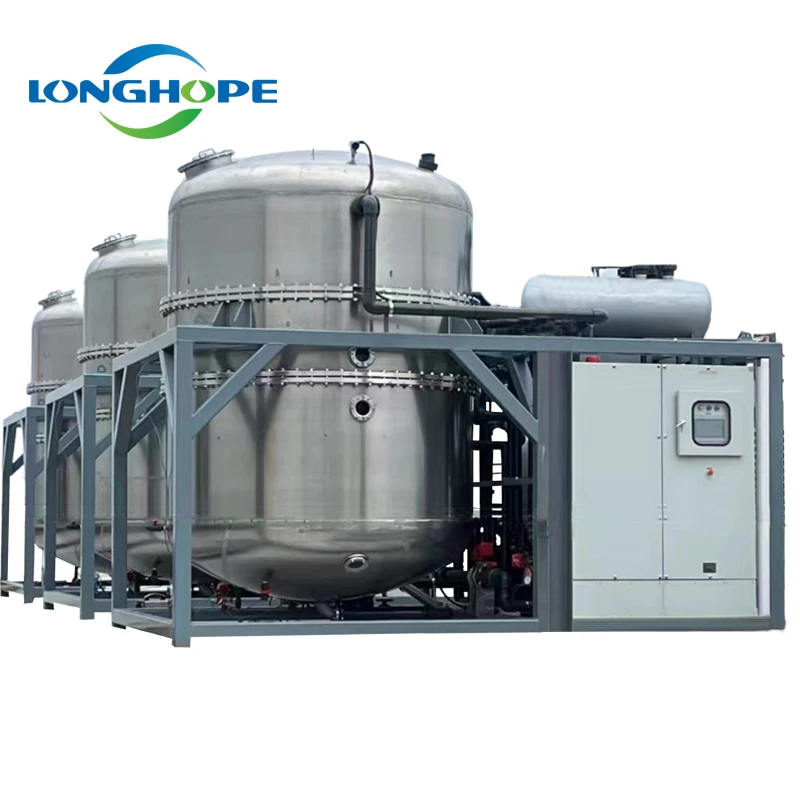
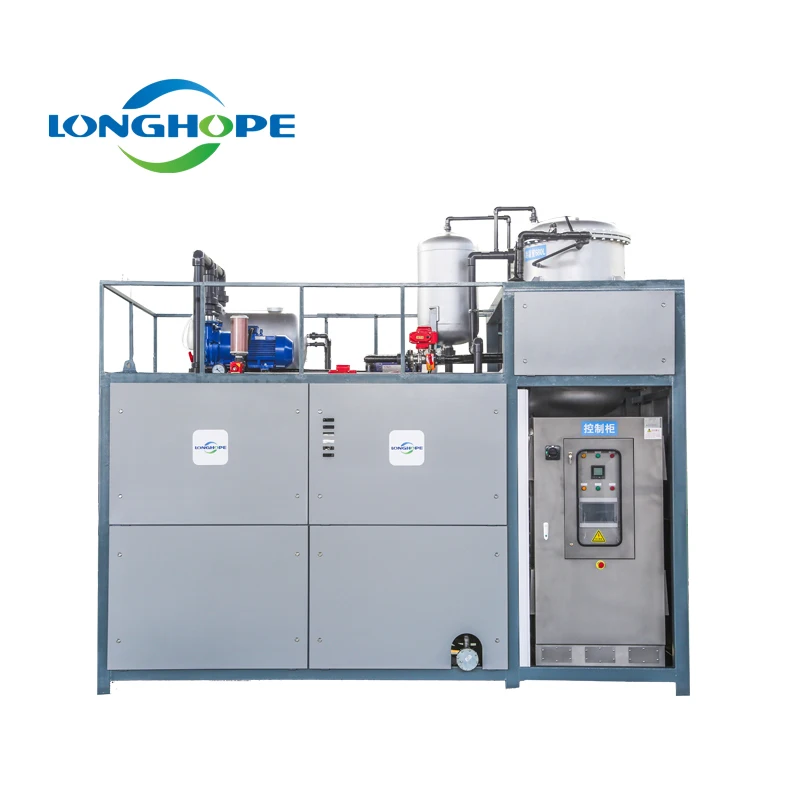
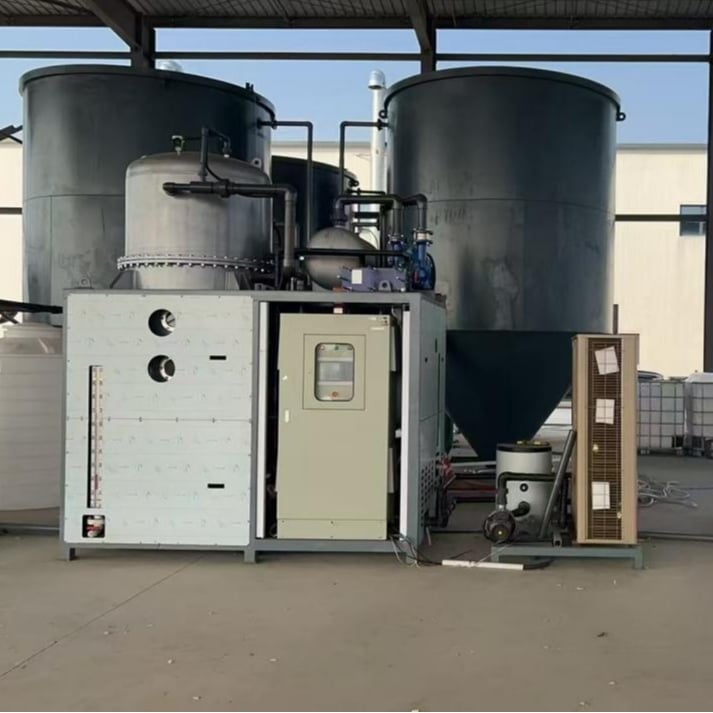
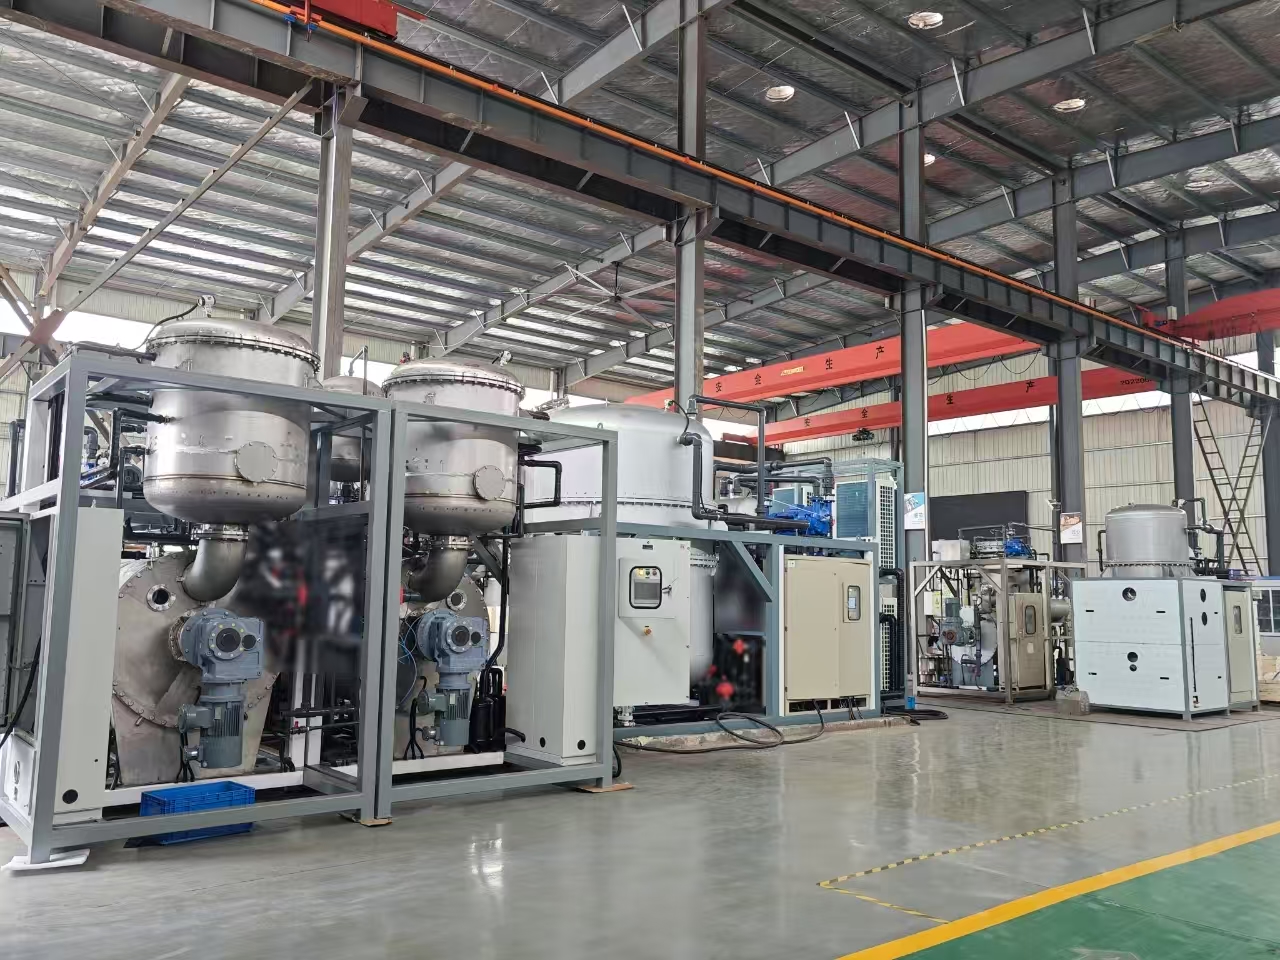
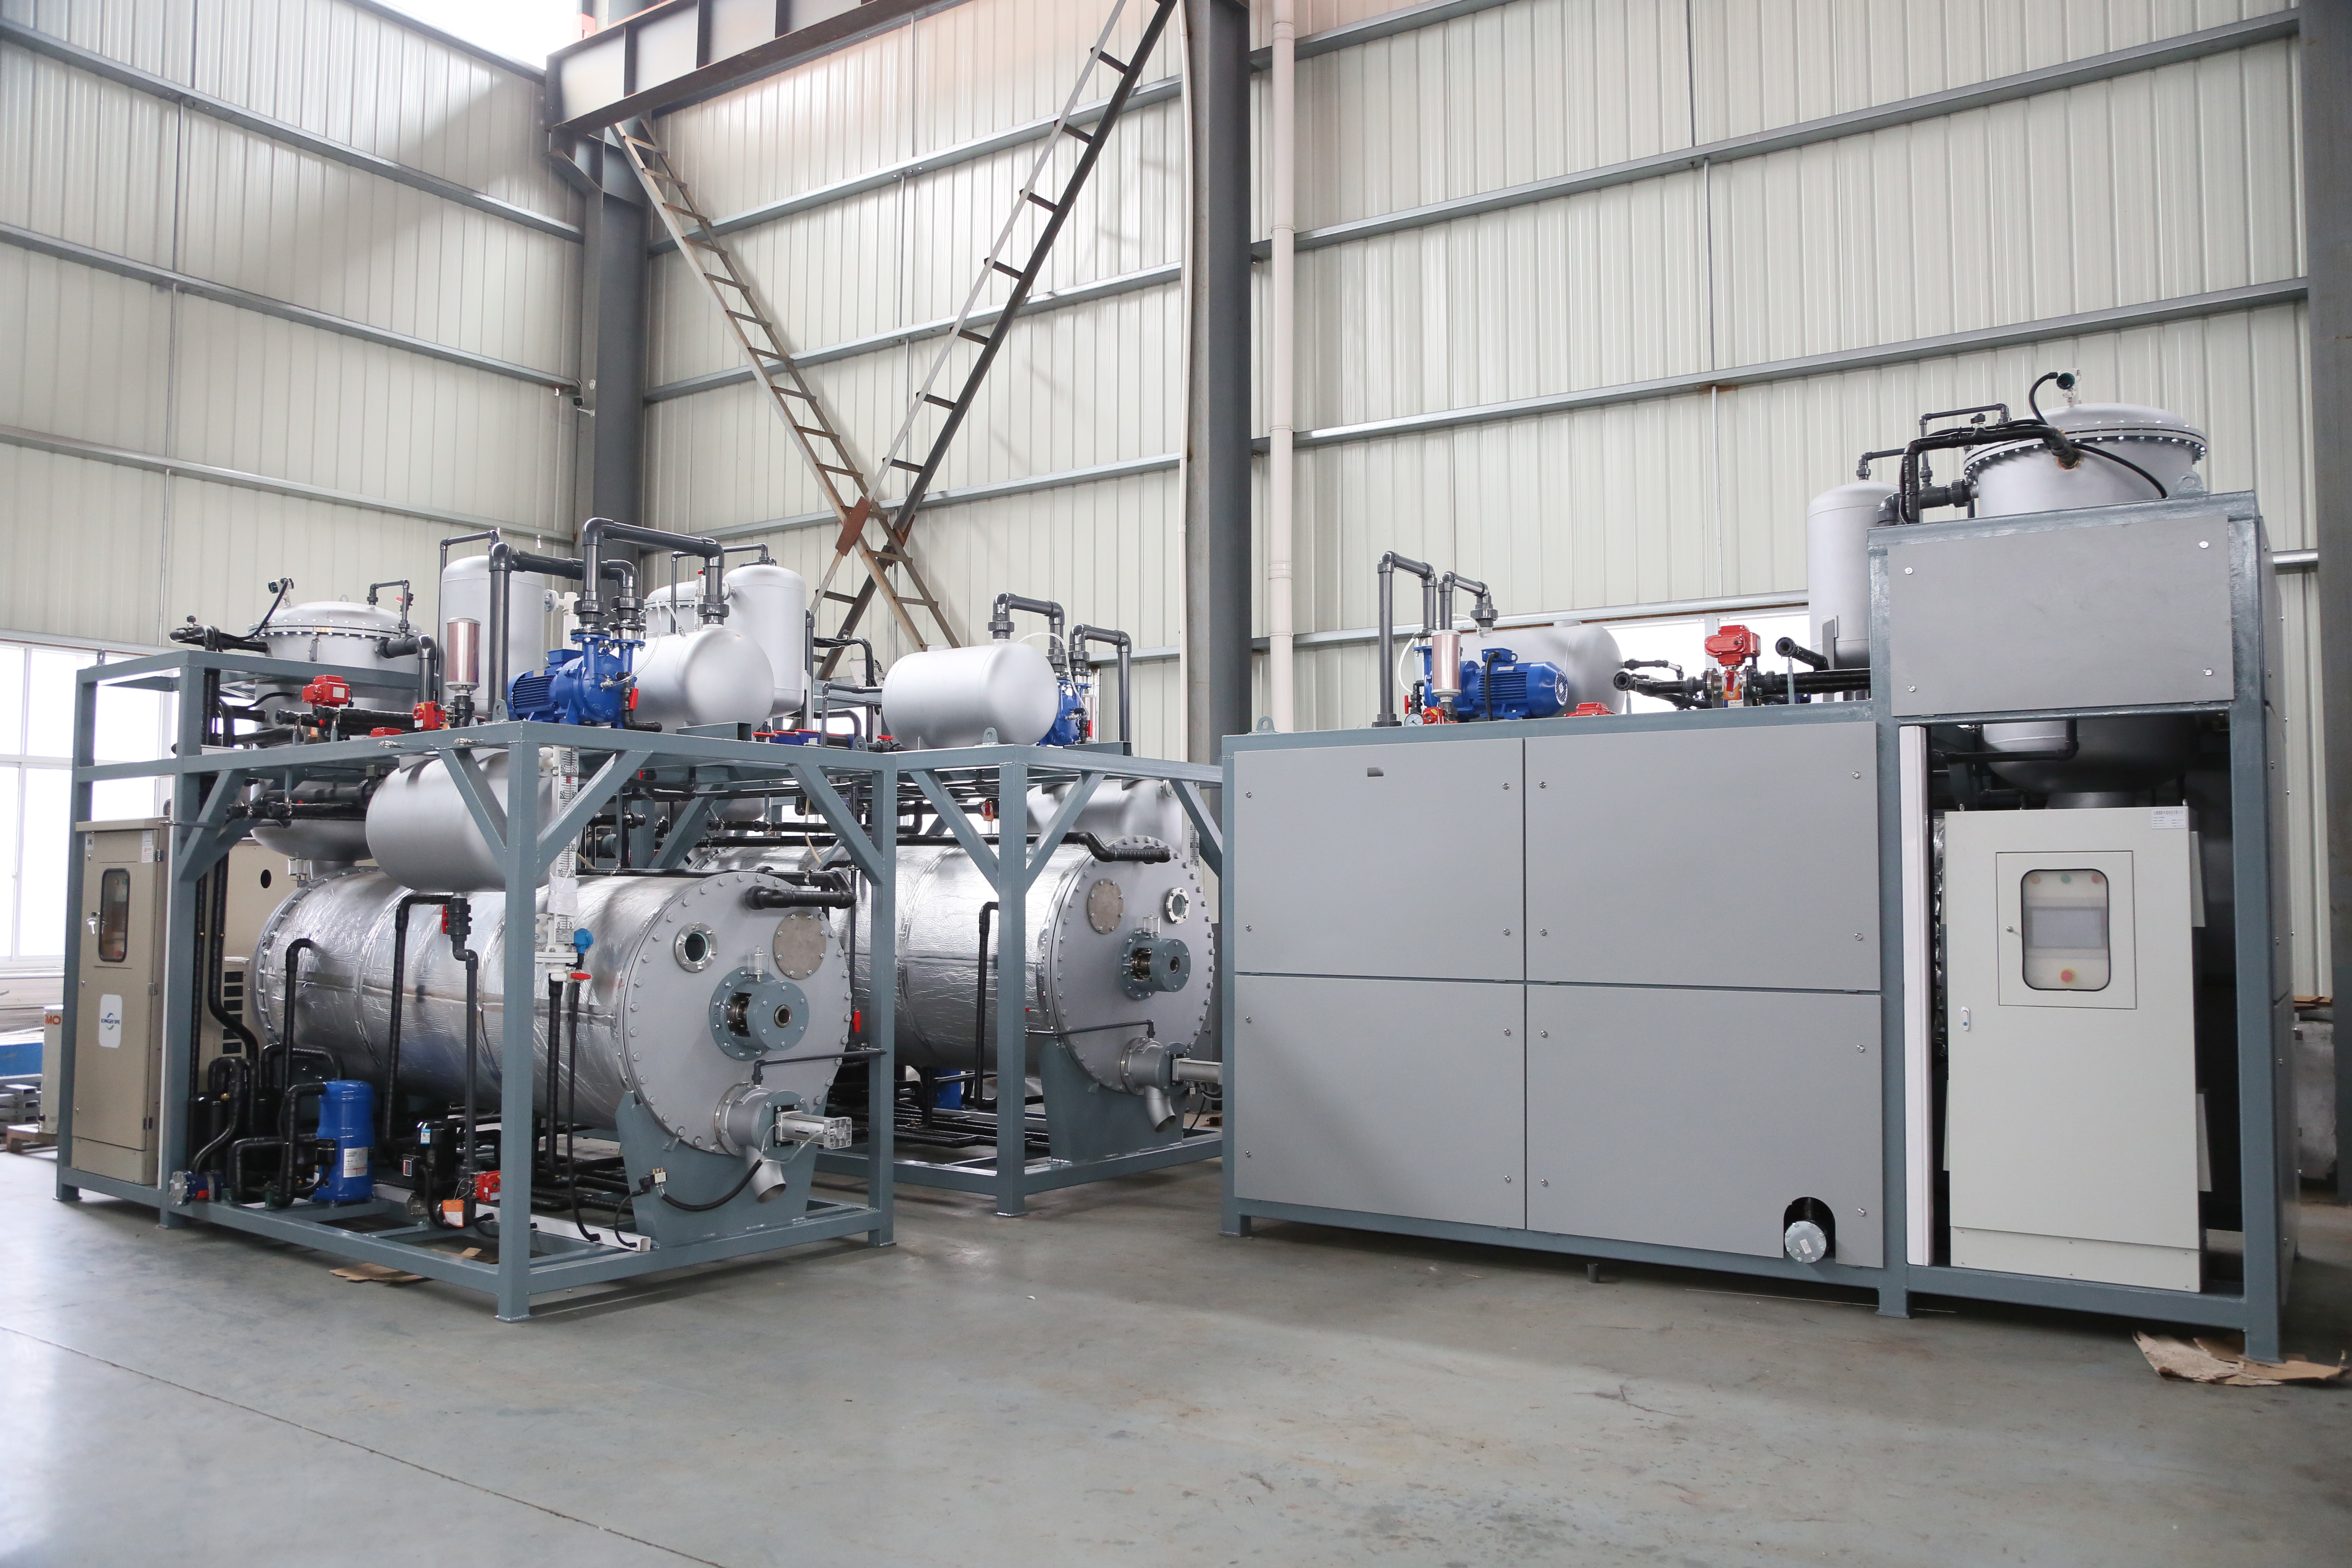
A custom vacuum distillation system represents an advanced separation technology designed to purify liquids and recover valuable compounds under reduced pressure conditions. This specialized equipment operates by lowering atmospheric pressure within the distillation chamber, enabling liquids to vaporize at significantly lower temperatures than conventional distillation methods would require. The custom vacuum distillation system serves multiple industries by efficiently separating components based on their boiling points while minimizing thermal degradation of heat-sensitive materials. The primary function of a custom vacuum distillation system involves separating liquid mixtures into pure fractions through controlled evaporation and condensation processes. By maintaining reduced pressure environments, this equipment protects temperature-sensitive compounds from decomposition, making it ideal for processing pharmaceuticals, essential oils, natural extracts, and specialty chemicals. The custom vacuum distillation system incorporates precision temperature controls, automated pressure regulation, and efficient condensing systems that work together to achieve superior separation results. Key technological features include variable vacuum pumps, stainless steel construction for corrosion resistance, integrated heating systems with precise temperature monitoring, and condensing coils optimized for heat transfer efficiency. The custom vacuum distillation system configuration allows operators to adjust pressure levels and temperatures according to specific material requirements, ensuring optimal distillation performance. Modern installations feature digital controls, safety interlocks, and real-time monitoring capabilities that enhance operational reliability and product quality while reducing processing time and material waste throughout the distillation cycle.

Popular Products

A custom vacuum distillation system delivers substantial operational and economic benefits that make it an excellent investment for processing operations requiring precise separation capabilities. The most immediate advantage involves protecting temperature-sensitive materials from degradation. By operating at reduced pressures, your custom vacuum distillation system enables distillation at lower temperatures, preserving the integrity of delicate compounds that would otherwise decompose under conventional heating methods. Operational efficiency represents another significant benefit. Your custom vacuum distillation system reduces processing time by accelerating evaporation rates while maintaining precise control over separation parameters. This translates to increased production capacity without requiring additional equipment investments or facility expansions. The enhanced efficiency directly improves your bottom line through higher throughput and better resource utilization. Cost savings accumulate through multiple channels when you implement a custom vacuum distillation system. Reduced energy consumption during extended processing cycles lowers utility bills substantially. Improved product recovery rates mean less material waste and higher profit margins on each batch processed. The custom vacuum distillation system minimizes contamination risks through enclosed processing environments, reducing product rejections and rework requirements. Product quality improvements distinguish operations using a custom vacuum distillation system from competitors. Superior purity levels, consistent batch characteristics, and enhanced component recovery enable you to command premium pricing for finished products. The equipment's scalability accommodates business growth without workflow disruptions, while customizable configurations adapt to evolving production requirements. Industries ranging from pharmaceuticals to food processing rely on custom vacuum distillation system technology to meet stringent quality standards and regulatory compliance requirements. Your competitive advantage strengthens significantly through investment in this proven separation technology.

Latest News

Low Temperature Heat Pump Evaporator Maintenance Best Practices

24

Jul

Low Temperature Heat Pump Evaporator Maintenance Best Practices

Effective low temperature heat pump evaporator maintenance is essential for preserving system efficiency, extending equipment lifespan, and preventing costly downtime in industrial refrigeration applications. The evaporator represents a critical heat...
View More
Industrial Water Treatment Technologies for 2026

02

Sep

Industrial Water Treatment Technologies for 2026

Industrial water treatment remains one of the most critical operational priorities across manufacturing, chemical processing, food production, and energy sectors. As facilities face increasingly stringent environmental regulations, rising operational...
View More
Benefits of a Modern Evaporator System for Wastewater

24

Jul

Benefits of a Modern Evaporator System for Wastewater

Modern industrial facilities face mounting pressure to reduce wastewater disposal costs while meeting strict environmental regulations. An evaporator systems for wastewater represents a transformative solution that addresses both operational expenses...
View More
How to Design an Efficient Vacuum Distillation Setup

02

Sep

How to Design an Efficient Vacuum Distillation Setup

Designing an efficient vacuum distillation setup requires careful attention to equipment selection, operational parameters, and system layout. A properly engineered vacuum distillation setup maximizes separation efficiency while minimizing energy con...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

custom vacuum distillation system

Precise Temperature Control for Heat-Sensitive Compounds

Precise Temperature Control for Heat-Sensitive Compounds

Temperature management stands as a critical advantage of your custom vacuum distillation system, particularly when processing materials prone to thermal degradation. The system's advanced heating mechanisms maintain exact temperature parameters within narrow ranges, protecting valuable compounds from decomposition. By reducing operational pressure, your custom vacuum distillation system allows boiling point reduction, enabling separation processes to occur at substantially lower temperatures than conventional distillation requires. This capability proves invaluable for pharmaceutical manufacturers, botanical extractors, and specialty chemical producers handling temperature-sensitive formulations. The precision temperature control incorporated into every custom vacuum distillation system configuration ensures consistent results across multiple production batches, eliminating quality variations that plague competitors. Real-time temperature monitoring with automated adjustment features maintains optimal processing conditions throughout entire distillation cycles. Your custom vacuum distillation system delivers reliability and repeatability that laboratory-scale operations require while scaling efficiently to commercial production volumes without compromising material integrity or separation effectiveness.
Enhanced Separation Efficiency and Recovery Rates

Enhanced Separation Efficiency and Recovery Rates

Maximum component recovery represents a fundamental benefit delivered by modern custom vacuum distillation system technology. The equipment's optimized condensing systems and precise pressure control work synergistically to capture valuable compounds that traditional distillation methods often lose to decomposition or incomplete separation. Your custom vacuum distillation system achieves superior separation effectiveness by creating ideal conditions where different compounds vaporize at predictable rates based on molecular weight and boiling point characteristics. This translates directly to higher product yields and improved profitability for every processing batch. The enhanced efficiency of your custom vacuum distillation system reduces processing time significantly compared to conventional alternatives, increasing facility throughput without additional capital investments. Industries dependent on maximum material recovery—including pharmaceutical extraction, essential oil production, and waste stream processing—recognize that implementing a custom vacuum distillation system provides competitive advantages through superior recovery performance. The system's enclosed design minimizes environmental exposure and contamination risks, further protecting valuable compounds during separation. Operators report consistent improvements in production metrics after upgrading to dedicated custom vacuum distillation system equipment.
Scalable Design Supporting Business Growth

Scalable Design Supporting Business Growth

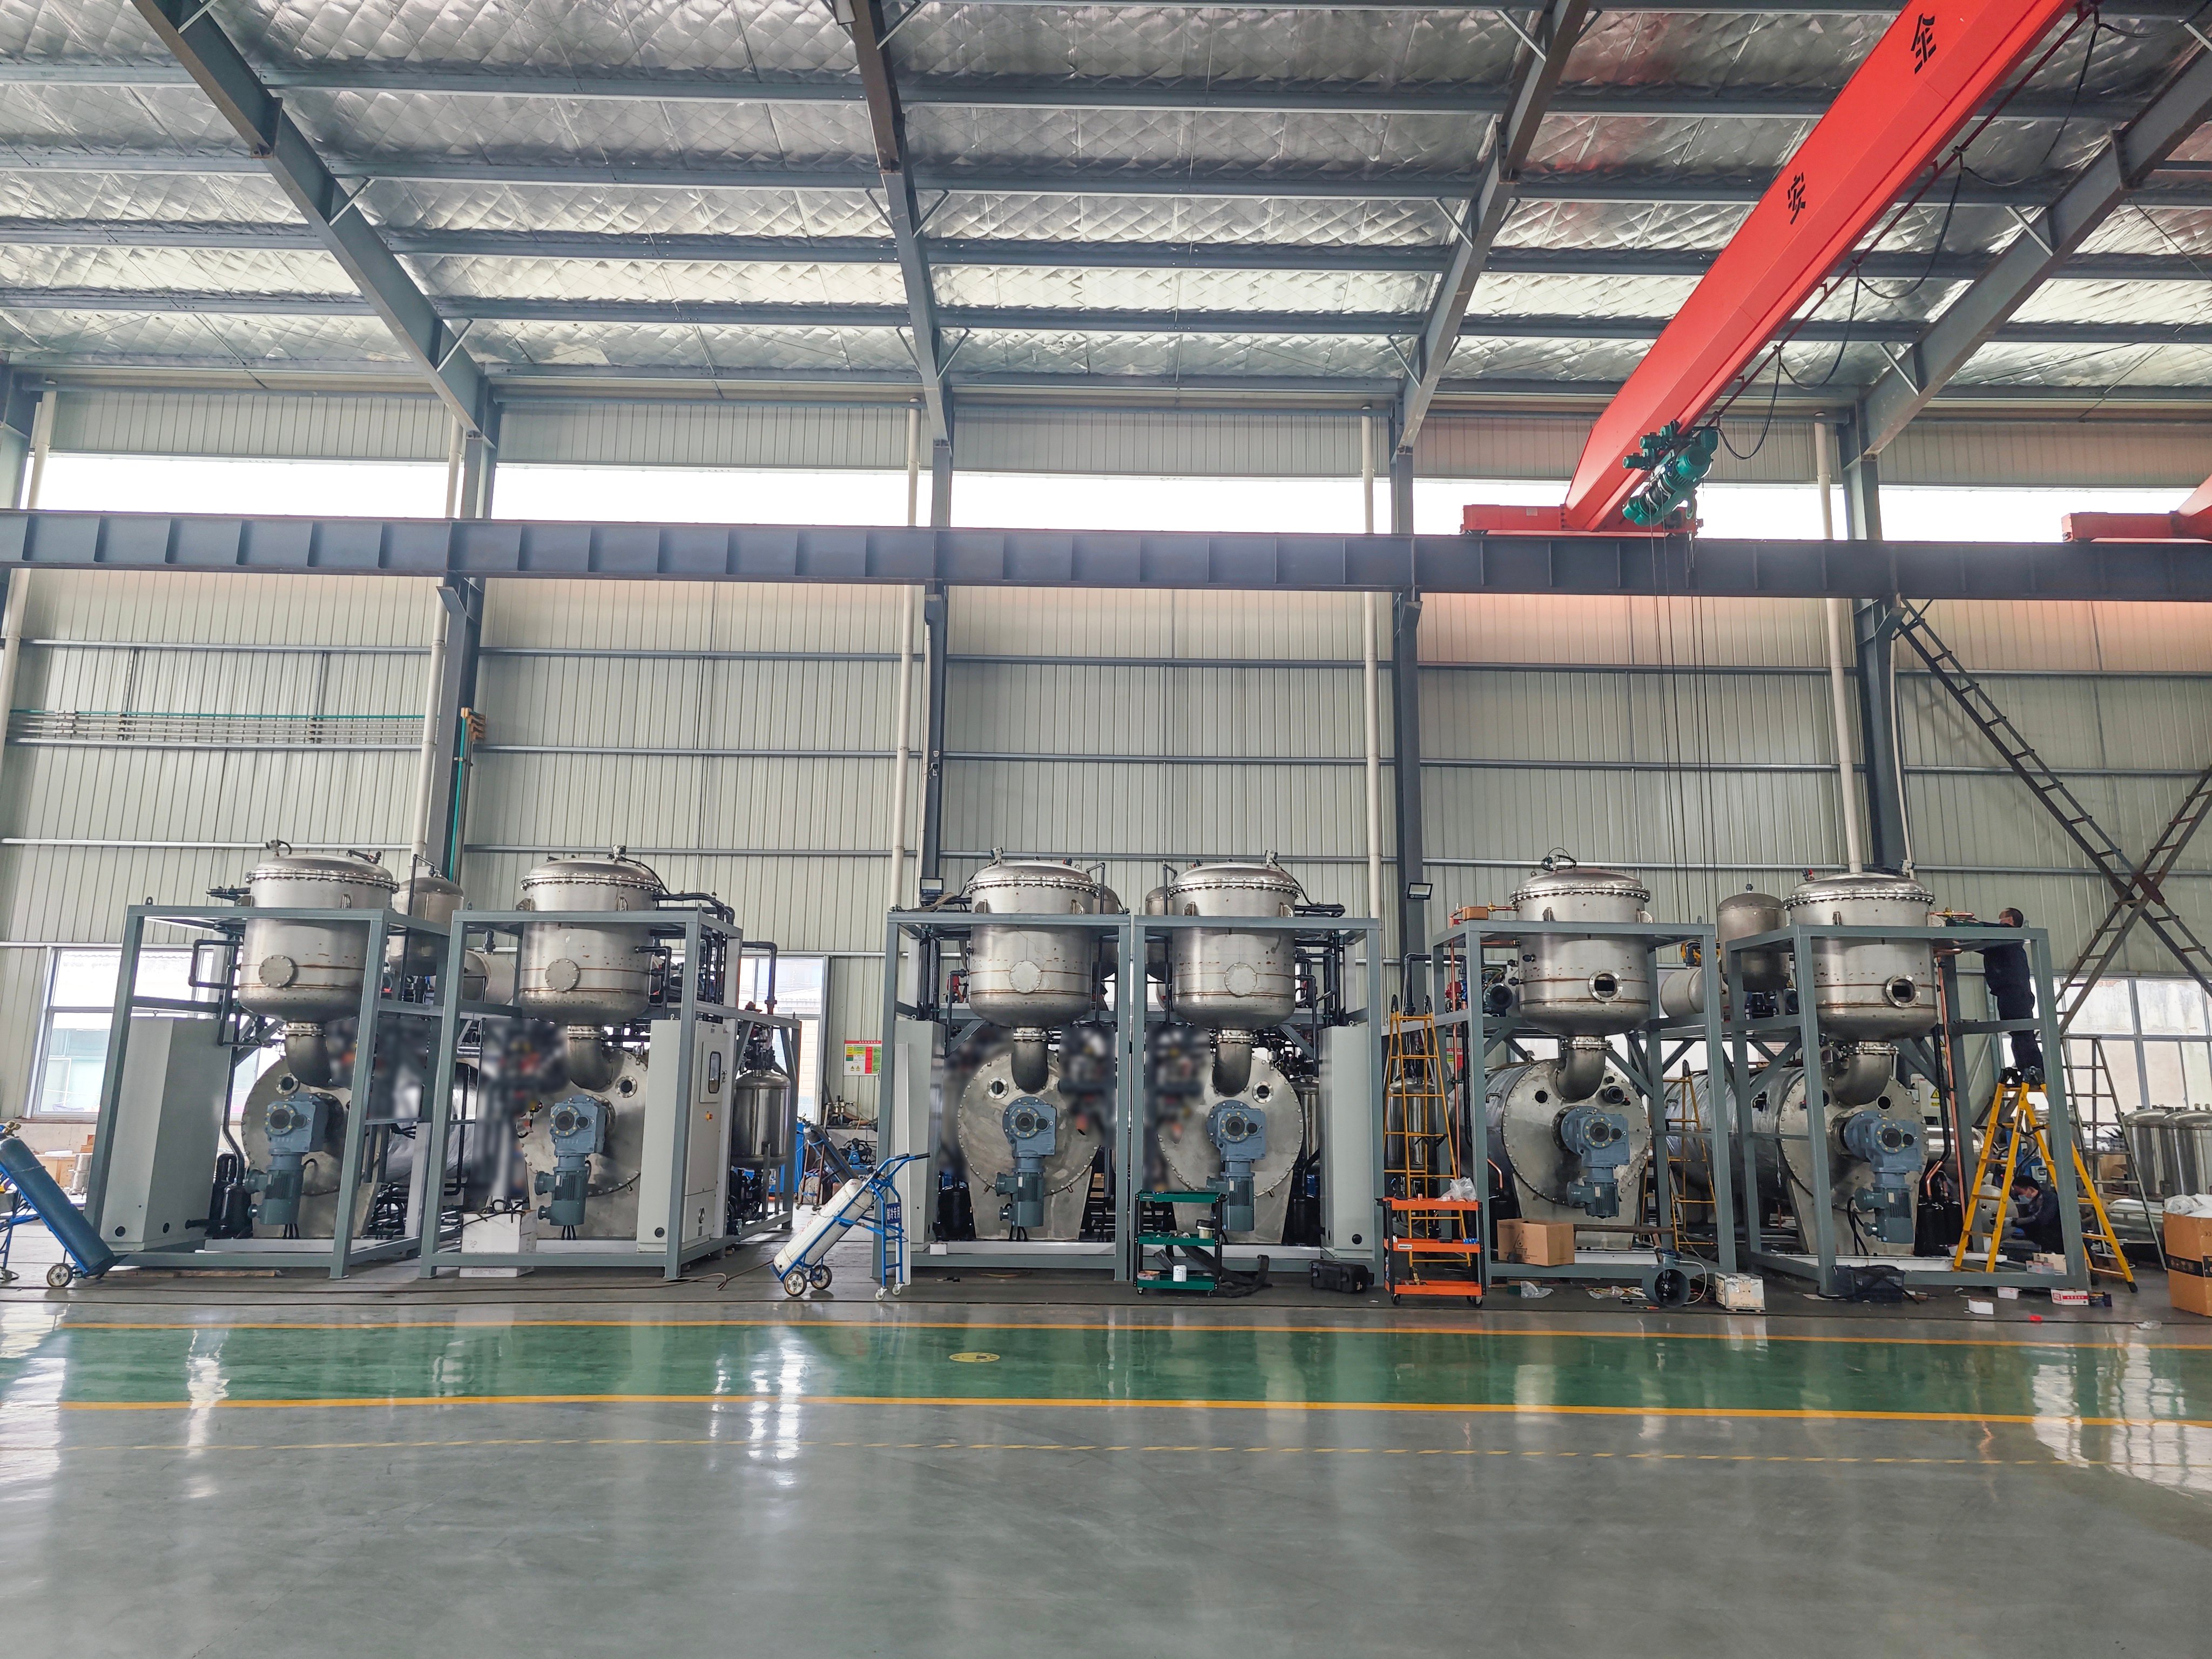
Flexibility and scalability distinguish premium custom vacuum distillation system solutions from basic alternatives. Whether your operation requires benchtop equipment for research applications or large-scale industrial systems for continuous production, a custom vacuum distillation system adapts to your specific requirements. The modular design approach allows capacity expansion by adding components without replacing existing infrastructure, protecting previous investments while accommodating increased production demands. Your custom vacuum distillation system configuration options address diverse industry applications, from pharmaceutical manufacturing to food ingredient processing and specialty chemical production. The equipment's versatility handles various material types and processing specifications, reducing the need for multiple distillation systems to address different applications. Customizable features including chamber volume, heating capacity, condensing efficiency, and vacuum pump specifications ensure your custom vacuum distillation system perfectly matches operational requirements. Future upgrades integrate seamlessly with existing equipment, extending system lifespan while maintaining technological currency. Manufacturers appreciate how a custom vacuum distillation system investment protects long-term competitiveness by enabling rapid product line extensions and market diversification without facility constraints limiting business growth opportunities.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000