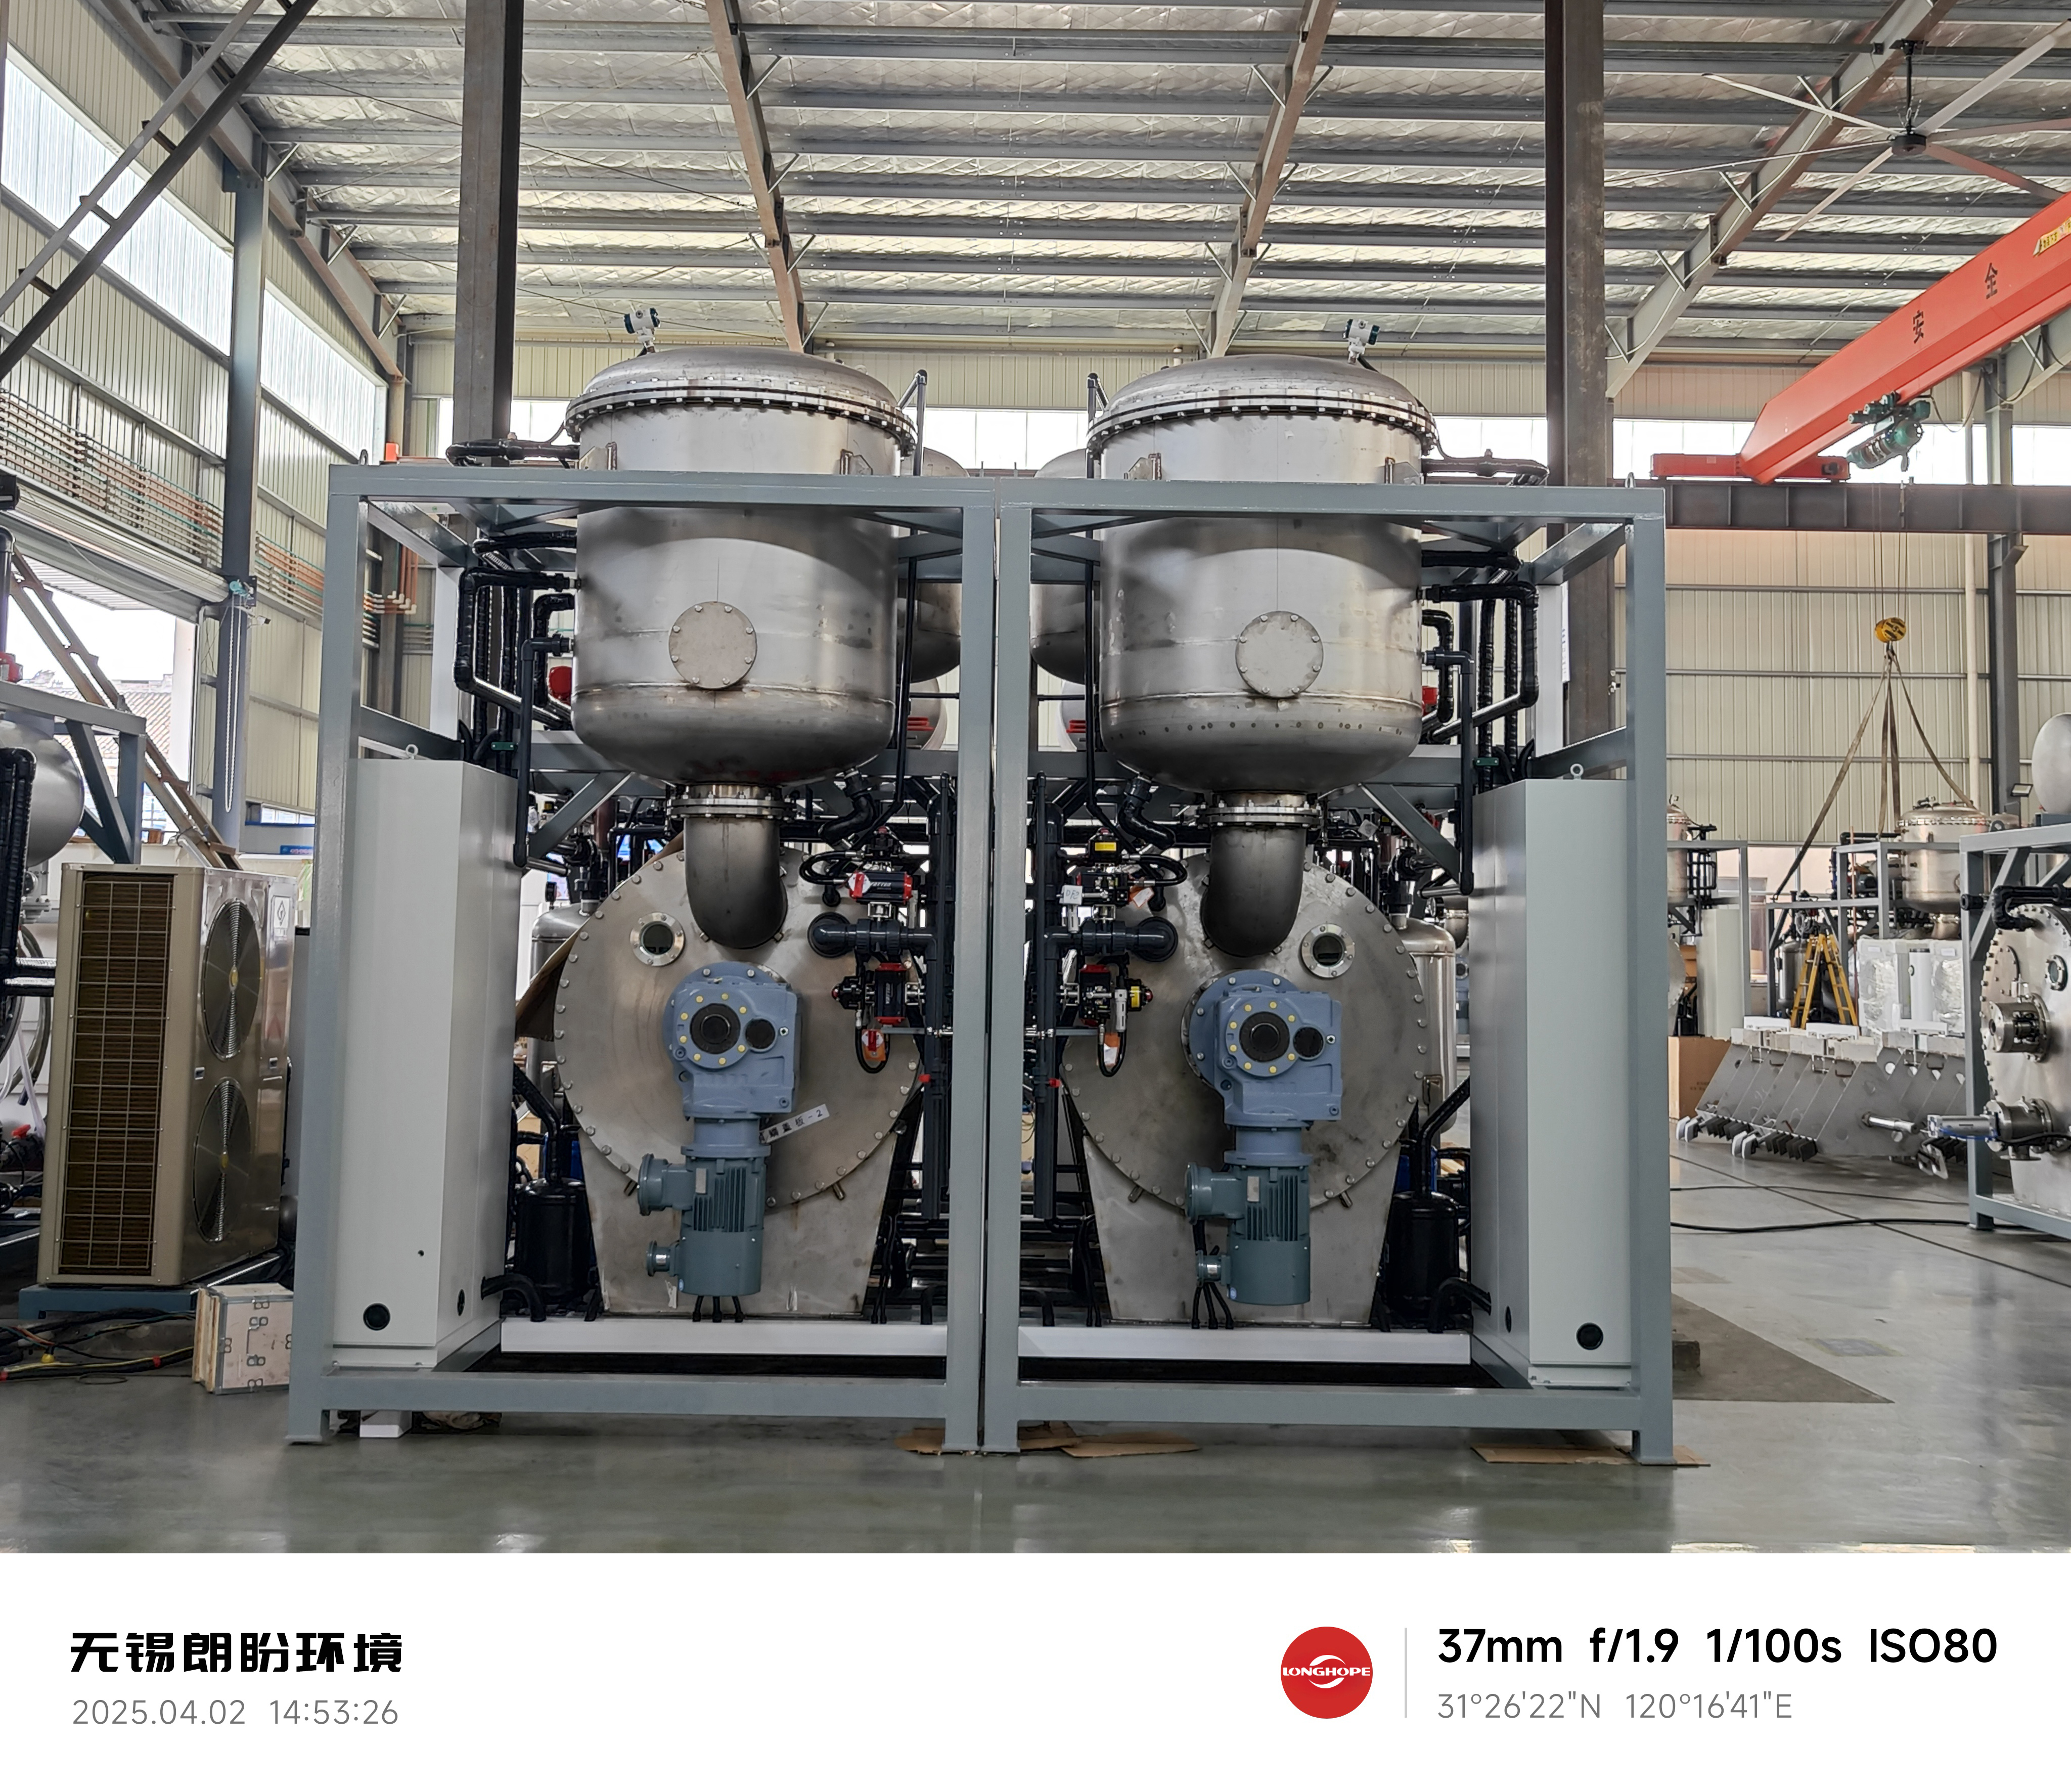
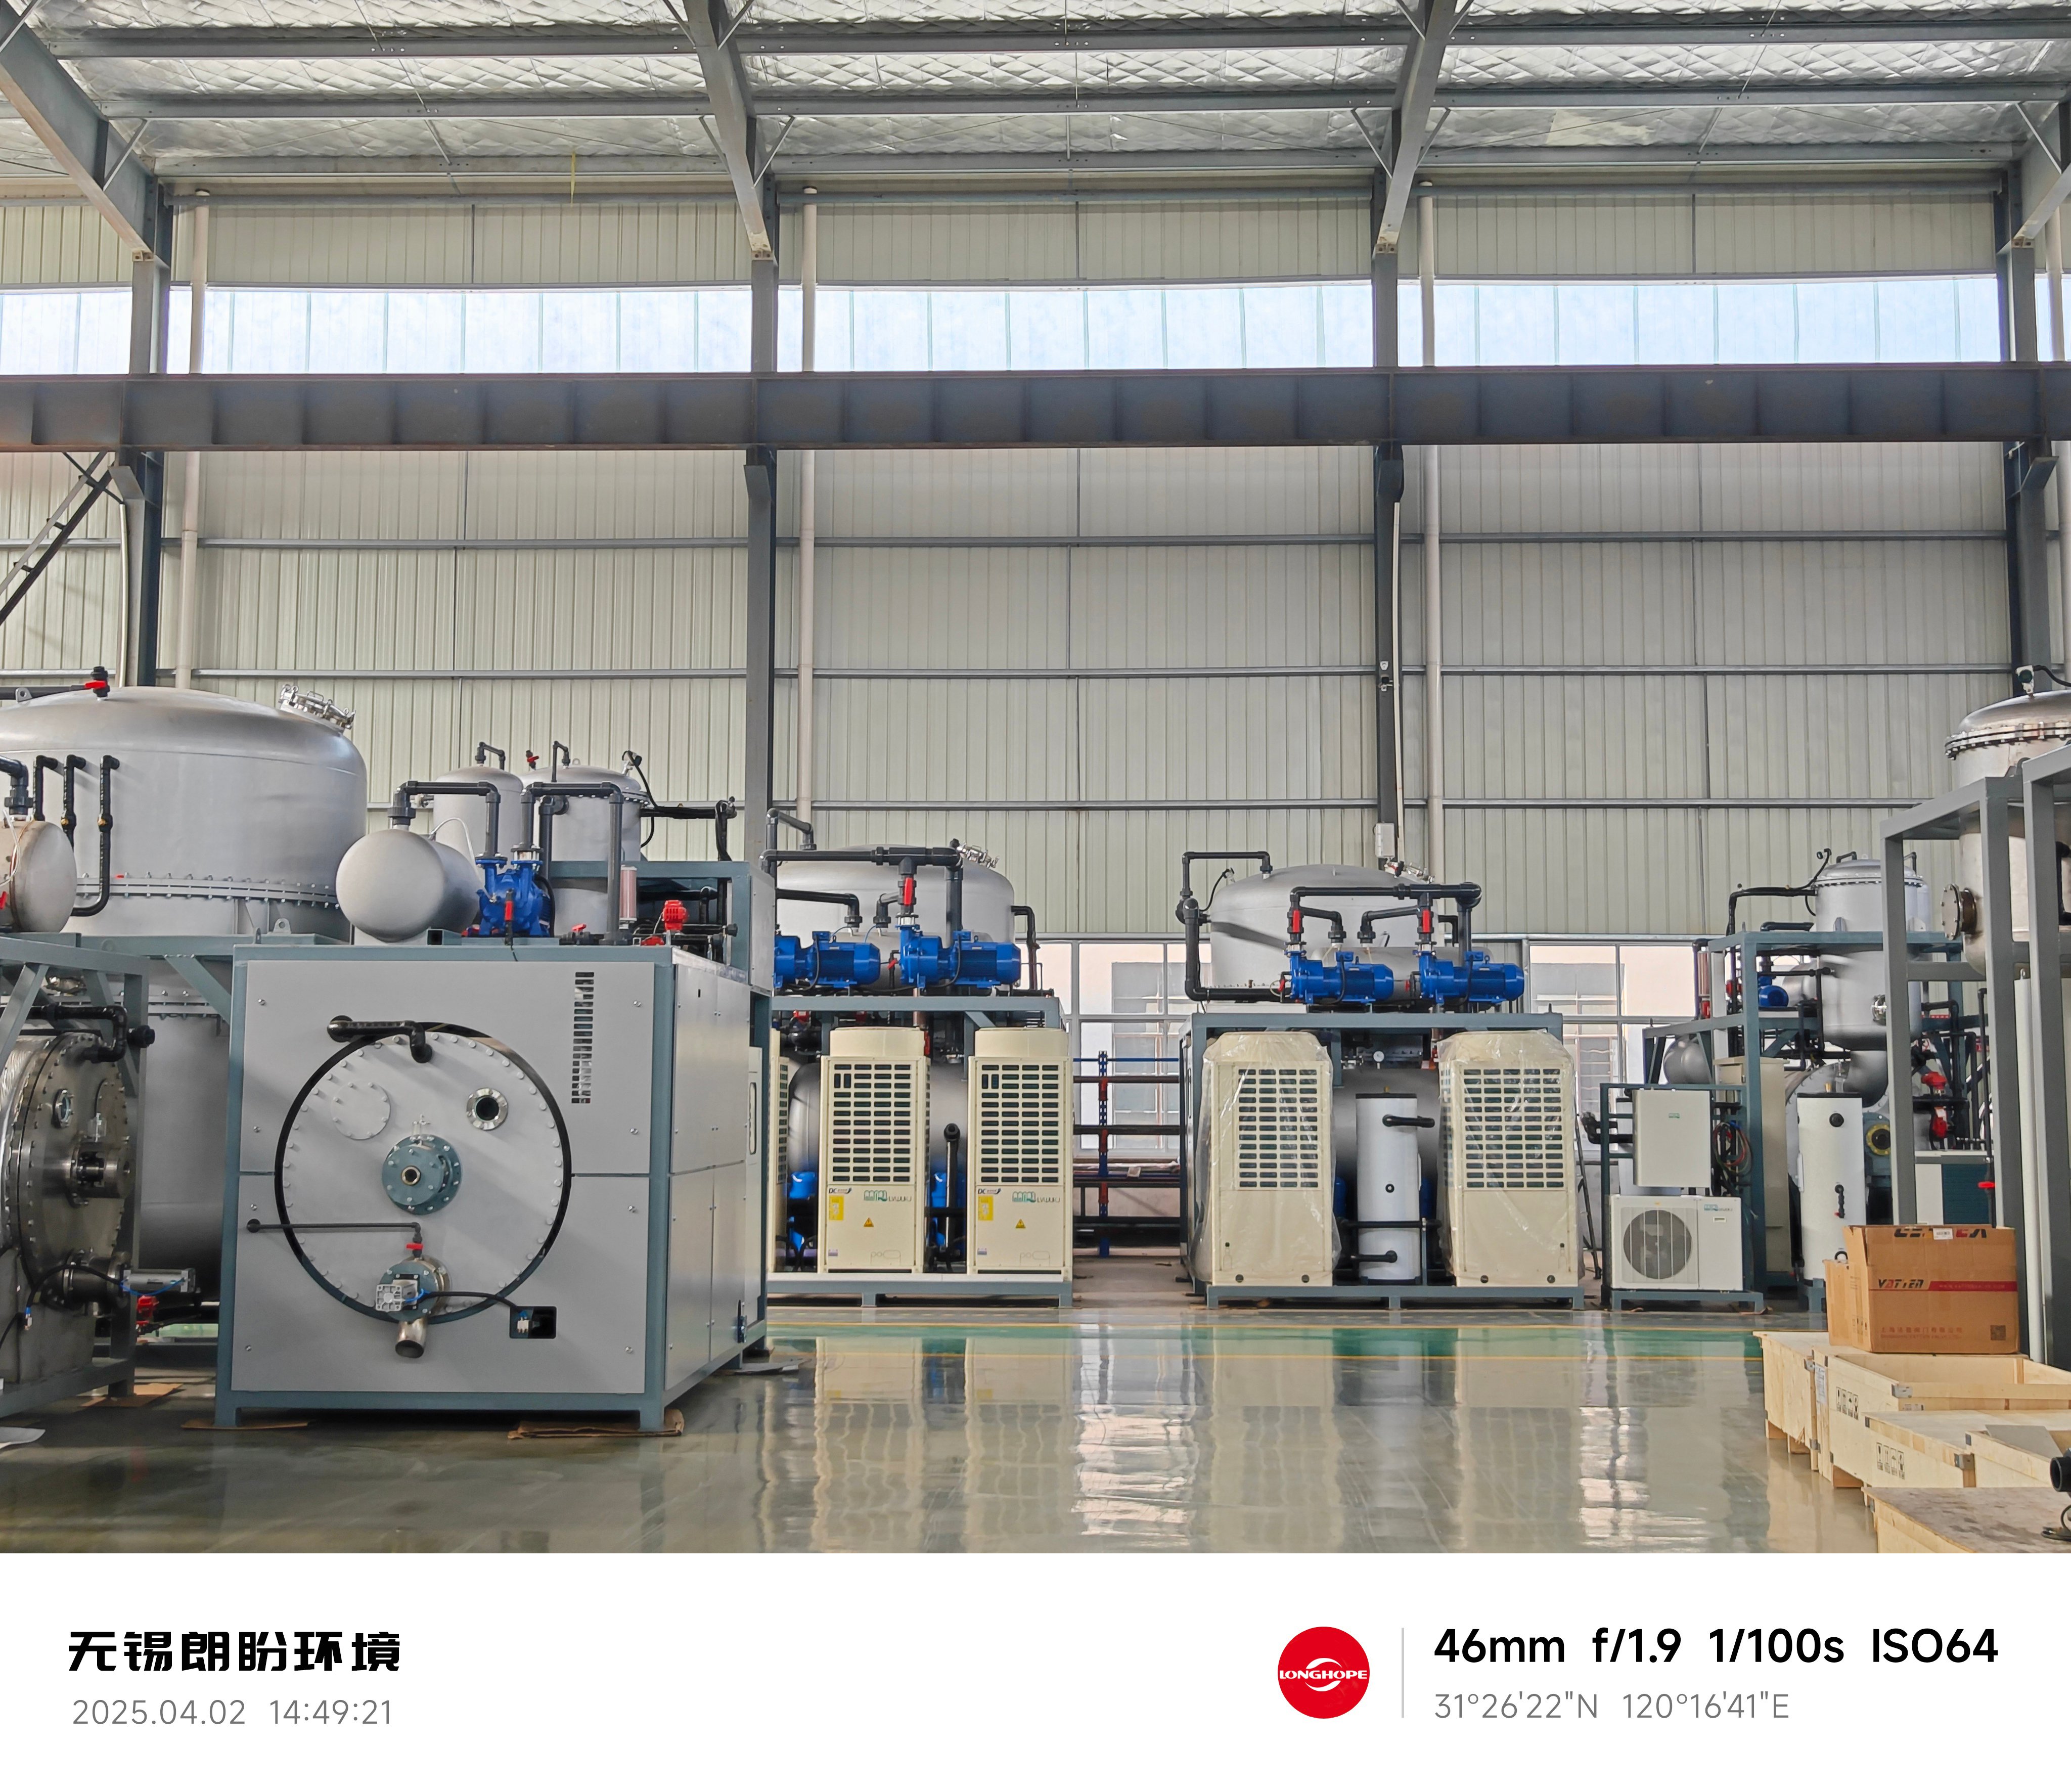
Continuous Vacuum Distillation Technology

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

continuous vacuum distillation

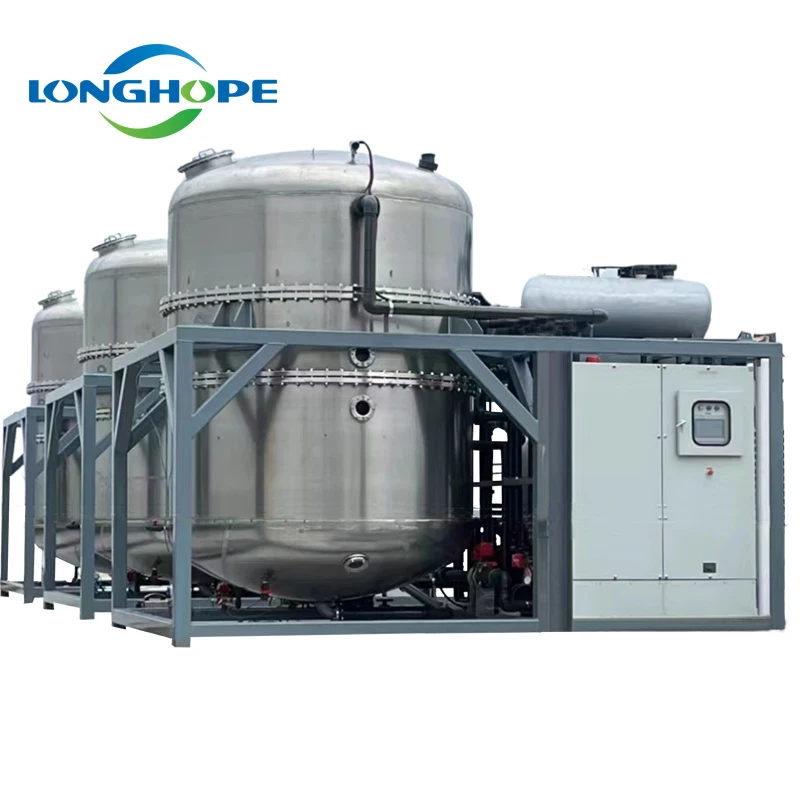
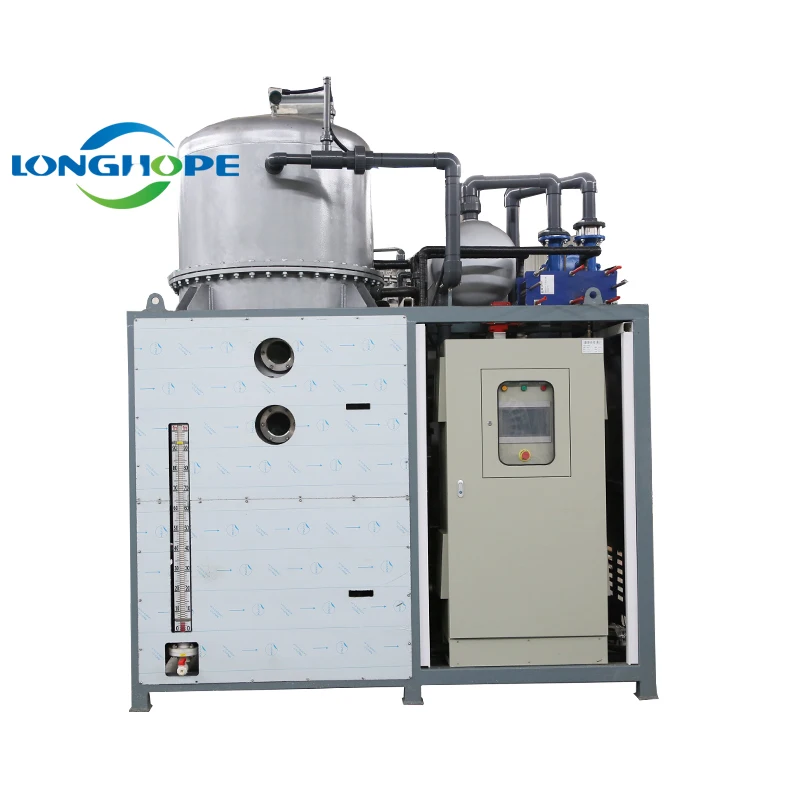
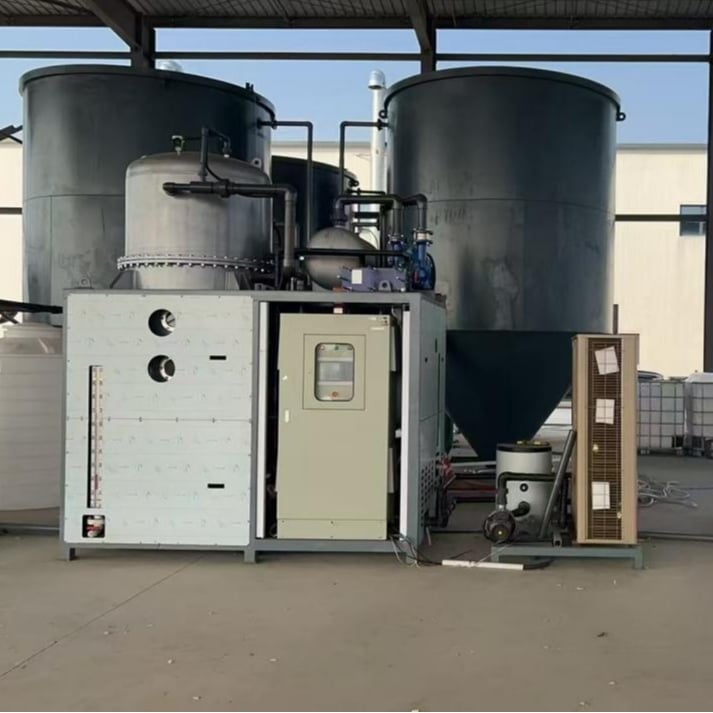
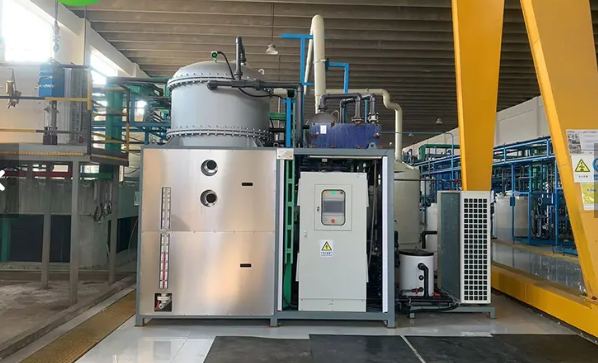
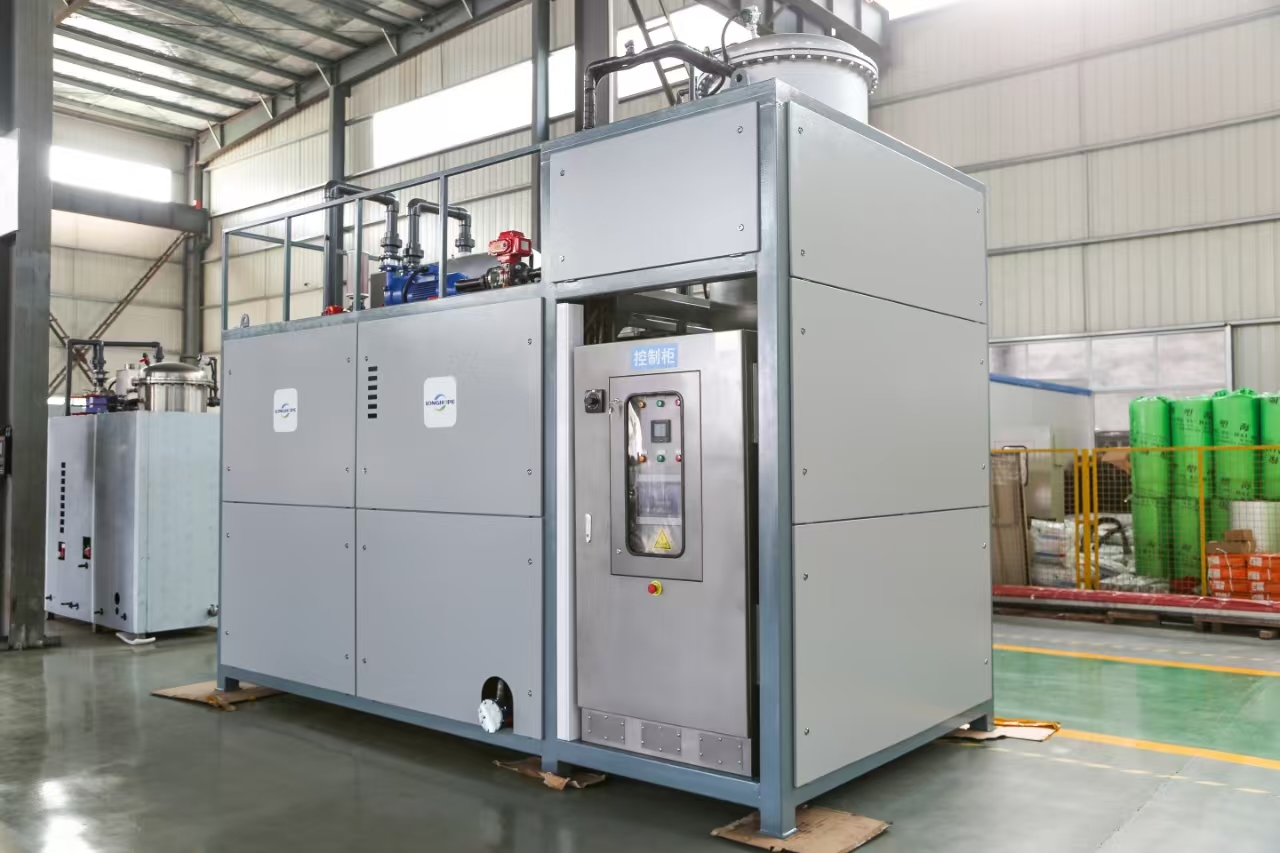
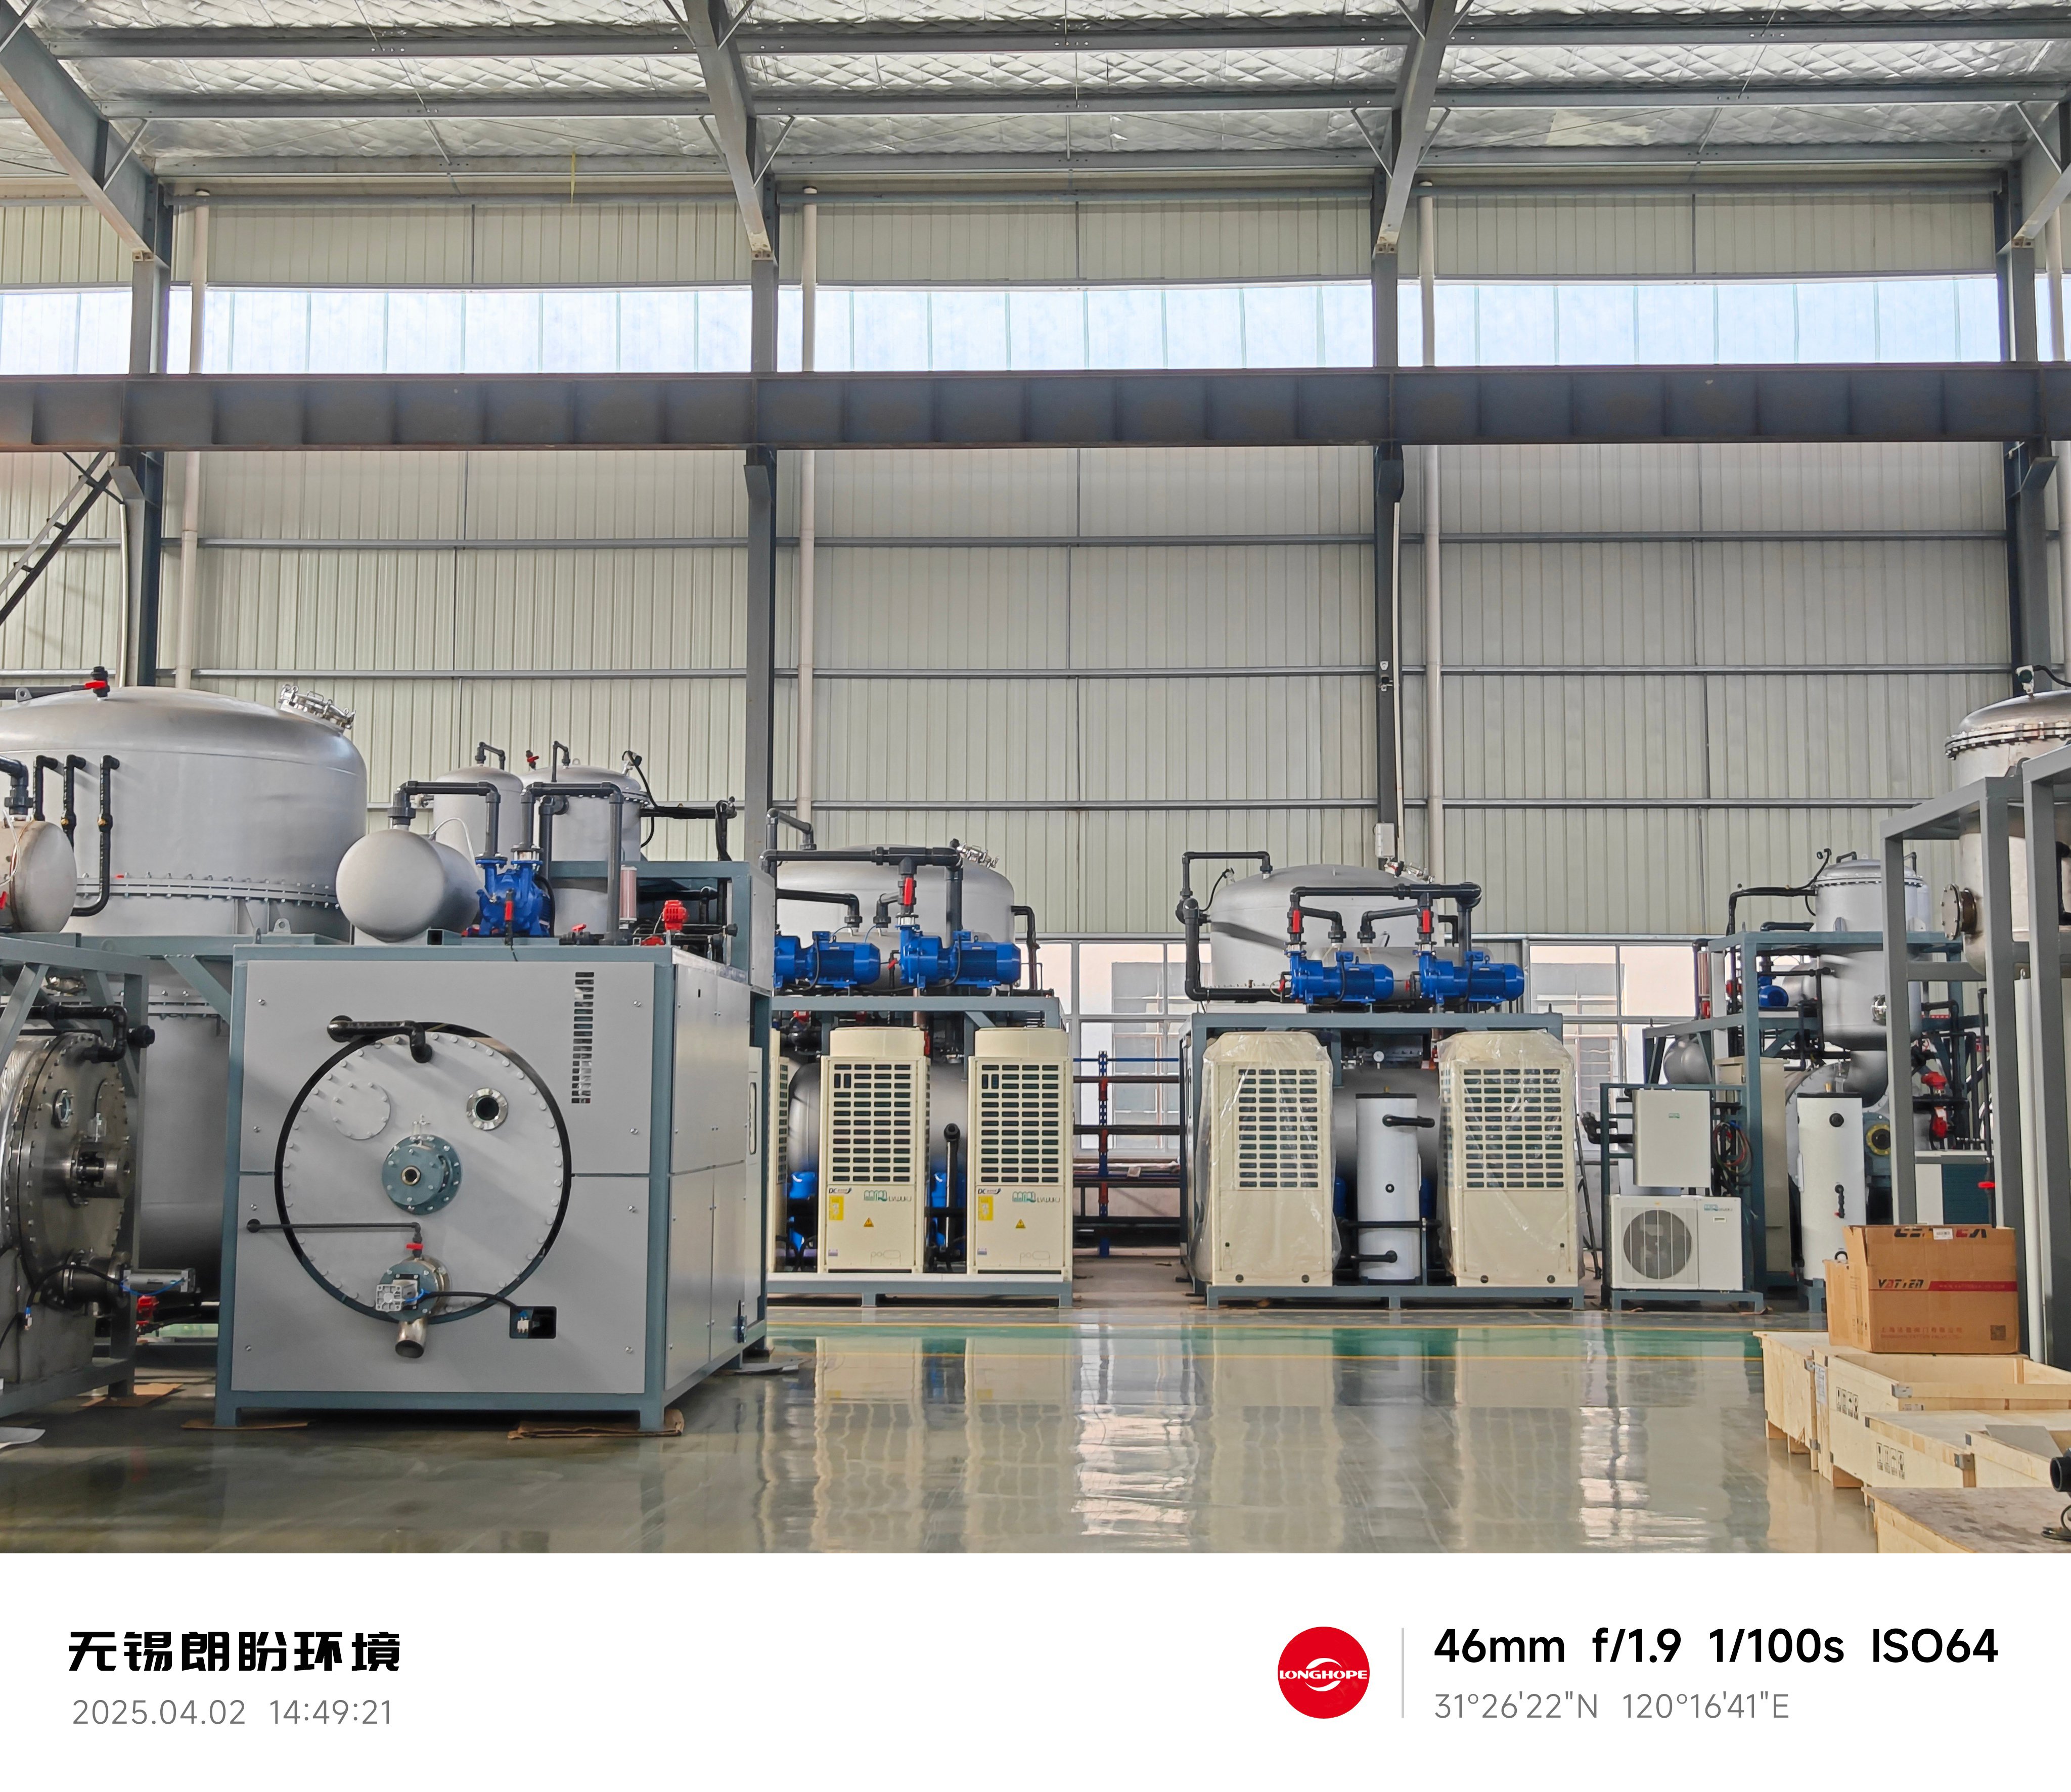
Continuous vacuum distillation represents a sophisticated separation technology designed to process heat-sensitive materials with exceptional precision and efficiency. This advanced distillation method operates under reduced pressure conditions, allowing volatile compounds to evaporate at lower temperatures than conventional atmospheric distillation. The continuous vacuum distillation process maintains steady-state operations, enabling consistent product quality and high throughput rates. Unlike batch systems, continuous vacuum distillation delivers uninterrupted production flows, making it ideal for large-scale industrial applications. The technology features specialized equipment including vacuum chambers, condenser units, and collection vessels that work synergistically to achieve optimal separation. Continuous vacuum distillation excels at processing crude oil, vegetable oils, pharmaceutical compounds, and specialty chemicals where thermal degradation poses significant risks. The system incorporates advanced monitoring controls that maintain precise pressure and temperature parameters throughout the distillation cycle. By utilizing continuous vacuum distillation, manufacturers dramatically reduce processing times while enhancing product purity and recovery rates. The technology's innovative design minimizes product loss and energy consumption, delivering superior environmental performance compared to traditional methods. Industries ranging from petroleum refining to cosmetics production rely on continuous vacuum distillation to meet stringent quality standards and regulatory requirements. This distillation approach represents the industry standard for applications demanding reliability, efficiency, and consistent results in sensitive material processing.

New Product Releases

Continuous vacuum distillation delivers exceptional operational value by eliminating the inefficiencies associated with batch processing systems. Your facility benefits immediately from uninterrupted production cycles, meaning higher output volumes without requiring additional equipment or floor space. The continuous nature of this distillation method ensures that product quality remains uniform across every batch, eliminating quality variations that frustrate customers and damage reputation. Processing at reduced pressures through continuous vacuum distillation protects heat-sensitive materials from degradation, preserving the integrity and efficacy of valuable compounds. Decision-makers choose continuous vacuum distillation because it substantially reduces energy consumption compared to conventional distillation techniques, directly improving your bottom line. This approach minimizes product loss during separation, maximizing yield rates and ensuring that expensive raw materials convert efficiently into marketable products. Maintenance requirements for continuous vacuum distillation systems remain remarkably low, reducing unexpected downtime and associated costs. The technology adapts seamlessly to various feedstock types, making your investment flexible for future market demands and product diversification. Safety improvements accompany continuous vacuum distillation implementation, as closed-loop systems eliminate hazardous vapor exposure for your workforce. Scaling production becomes straightforward with continuous vacuum distillation, allowing businesses to expand operations without comprehensive facility overhauls. Environmental compliance improves significantly since continuous vacuum distillation generates minimal emissions and waste. The straightforward operation of modern continuous vacuum distillation equipment requires minimal specialized training, reducing long-term staffing challenges. These practical benefits collectively position continuous vacuum distillation as the premier choice for serious manufacturers prioritizing efficiency, profitability, and sustainable operations.

Practical Tips

Low Temperature Heat Pump Evaporator Maintenance Best Practices

24

Jul

Low Temperature Heat Pump Evaporator Maintenance Best Practices

Effective low temperature heat pump evaporator maintenance is essential for preserving system efficiency, extending equipment lifespan, and preventing costly downtime in industrial refrigeration applications. The evaporator represents a critical heat...
View More
Top 5 Low Temperature Heat Pump Evaporator Applications

24

Jul

Top 5 Low Temperature Heat Pump Evaporator Applications

The low temperature heat pump evaporator represents a critical advancement in industrial thermal management and energy efficiency. This innovative component enables heat pump systems to operate effectively at reduced temperatures, making it indispens...
View More
Vacuum Distillation System Maintenance Best Practices

24

Jul

Vacuum Distillation System Maintenance Best Practices

Proper vacuum distillation system maintenance is critical for industries relying on separation, purification, and concentration processes. A well-maintained vacuum distillation system ensures consistent product quality, minimizes operational downtime...
View More
Common Challenges in Industrial Water Treatment Solved

02

Sep

Common Challenges in Industrial Water Treatment Solved

Manufacturing facilities, chemical plants, and processing operations face mounting pressure to manage wastewater efficiently while meeting regulatory standards. Industrial water treatment remains one of the most critical operational functions across ...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

continuous vacuum distillation

Precision Temperature Control at Lower Operating Pressures

Precision Temperature Control at Lower Operating Pressures

Continuous vacuum distillation operates at dramatically reduced pressures, enabling precise separation of valuable compounds without subjecting them to excessive heat exposure. This technological advantage proves critical for processing pharmaceuticals, natural extracts, and refined oils where thermal sensitivity creates quality challenges. Your products maintain superior quality characteristics when continuous vacuum distillation prevents degradation reactions triggered by high temperatures. The system automatically adjusts operating parameters, ensuring consistent results regardless of feedstock variations or seasonal changes. Modern continuous vacuum distillation equipment incorporates real-time monitoring sensors that detect pressure fluctuations instantly, triggering immediate compensatory adjustments. This precision engineering capability delivers product consistency that justifies premium pricing in competitive markets. Pharmaceutical manufacturers particularly value continuous vacuum distillation because it preserves delicate molecular structures that determine therapeutic effectiveness. The technology enables processing of compounds impossible to handle through conventional methods, opening entirely new product opportunities for your business. Investment in continuous vacuum distillation positions your company as a quality leader capable of meeting international standards and customer expectations for product purity and performance.
Maximized Yield Efficiency and Reduced Material Waste

Maximized Yield Efficiency and Reduced Material Waste

Continuous vacuum distillation dramatically improves recovery rates compared to batch distillation alternatives, meaning substantially more sellable product emerges from each production run. This efficiency advantage directly translates to improved profit margins and reduced per-unit production costs across your entire operation. When you implement continuous vacuum distillation, material losses typical in traditional processes simply disappear, protecting your investment in expensive raw materials. The continuous flow design of this distillation method ensures complete processing of feedstock, with minimal residue or byproducts requiring disposal. Advanced separation capabilities inherent in continuous vacuum distillation capture trace components that batch systems consistently miss, further enhancing total yield. Your waste disposal costs plummet substantially because continuous vacuum distillation generates minimal solid or liquid waste streams. Environmental regulators increasingly favor continuous vacuum distillation because the technology demonstrates superior resource conservation and sustainability performance. Market advantages emerge when your manufacturing efficiency supports competitive pricing without compromising quality standards. Customers recognize that continuous vacuum distillation quality justifies premium positioning in market segments where purity and performance define purchasing decisions. The economic benefits of implementing continuous vacuum distillation extend beyond immediate production improvements to encompass long-term competitive positioning and business resilience.
Uninterrupted Production Flow and Scalable Capacity

Uninterrupted Production Flow and Scalable Capacity

Unlike batch processes requiring frequent shutdown cycles for product removal and system cleaning, continuous vacuum distillation maintains steady production flows that maximize facility utilization rates. Your manufacturing facility operates at peak efficiency without the productivity losses inherent in traditional distillation approaches requiring batch cycle management. Continuous vacuum distillation scales effortlessly to meet growing demand, allowing capacity expansion through simple parameter adjustments rather than equipment replacement. This scalability advantage provides remarkable flexibility for responding to market opportunities and customer requirements without major capital investments. Production planning becomes significantly simpler with continuous vacuum distillation because output remains predictable and stable throughout operating periods. The technology adapts to varied feedstock characteristics automatically, maintaining consistent separation performance regardless of minor material variations. Equipment downtime for continuous vacuum distillation maintenance occurs during scheduled intervals only, never impacting production continuity. Your workforce manages continuous vacuum distillation operations through straightforward protocols, reducing training expenses and operational complexity. Growth-focused manufacturers select continuous vacuum distillation because capacity expansion becomes seamless and cost-effective as business scales. The reliability of continuous vacuum distillation operations creates dependable supply chains that strengthen customer relationships and competitive positioning in demanding markets.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000