Vacuum Membrane Distillation Technology

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

vacuum membrane distillation

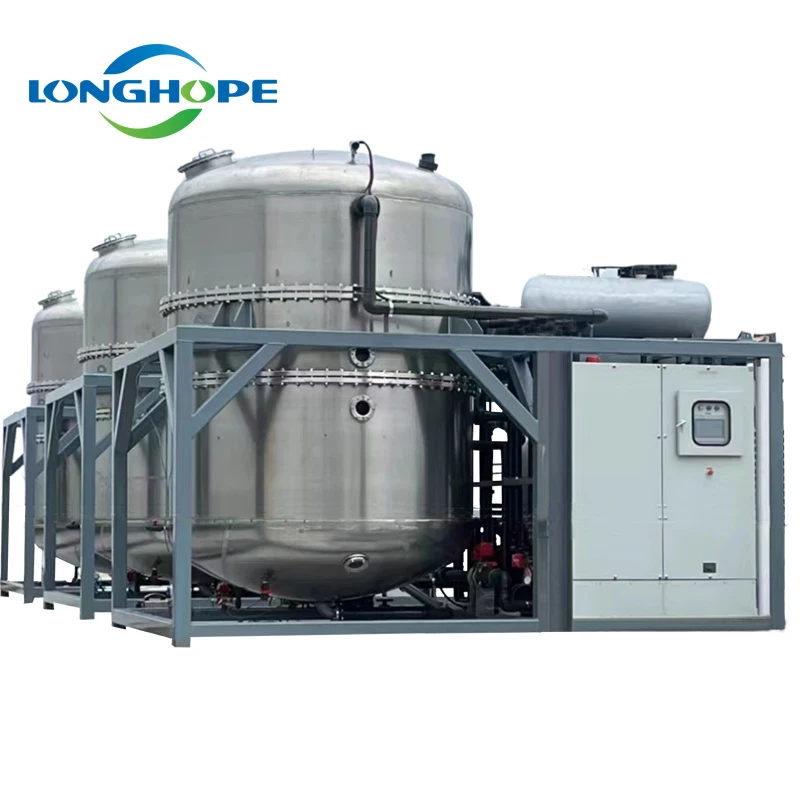
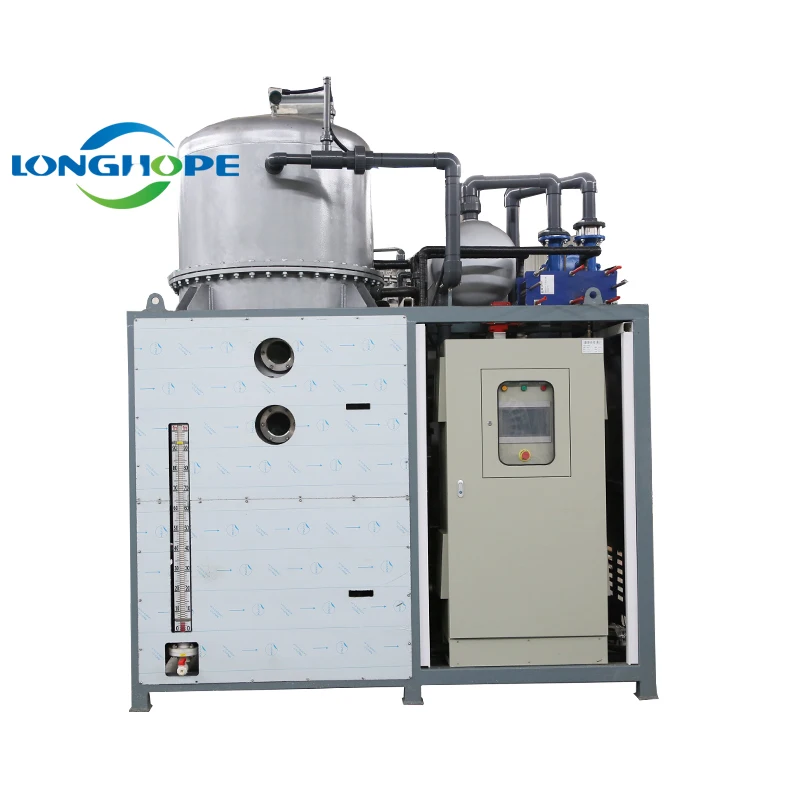
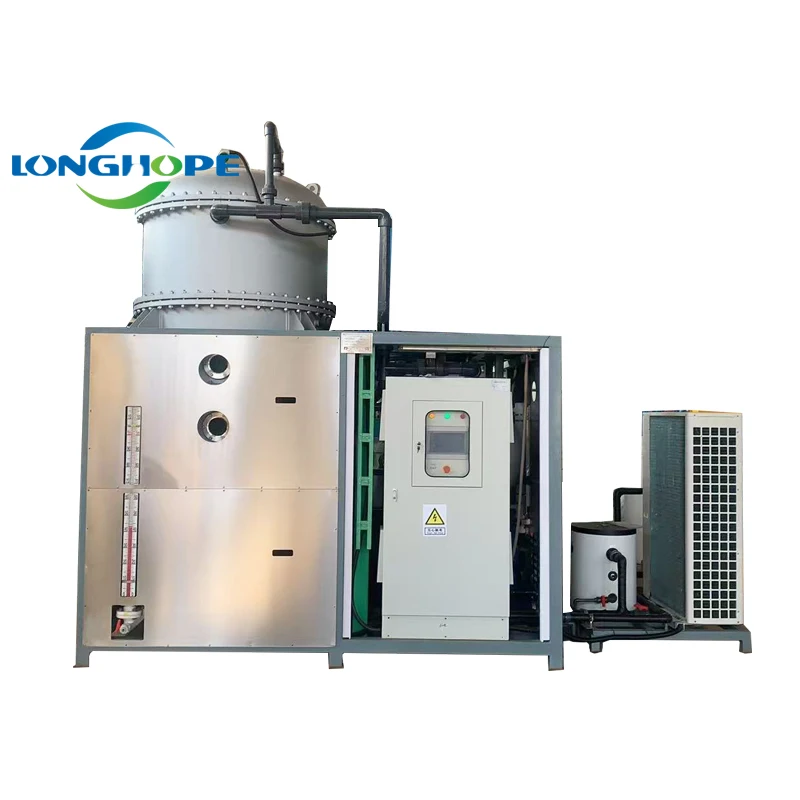
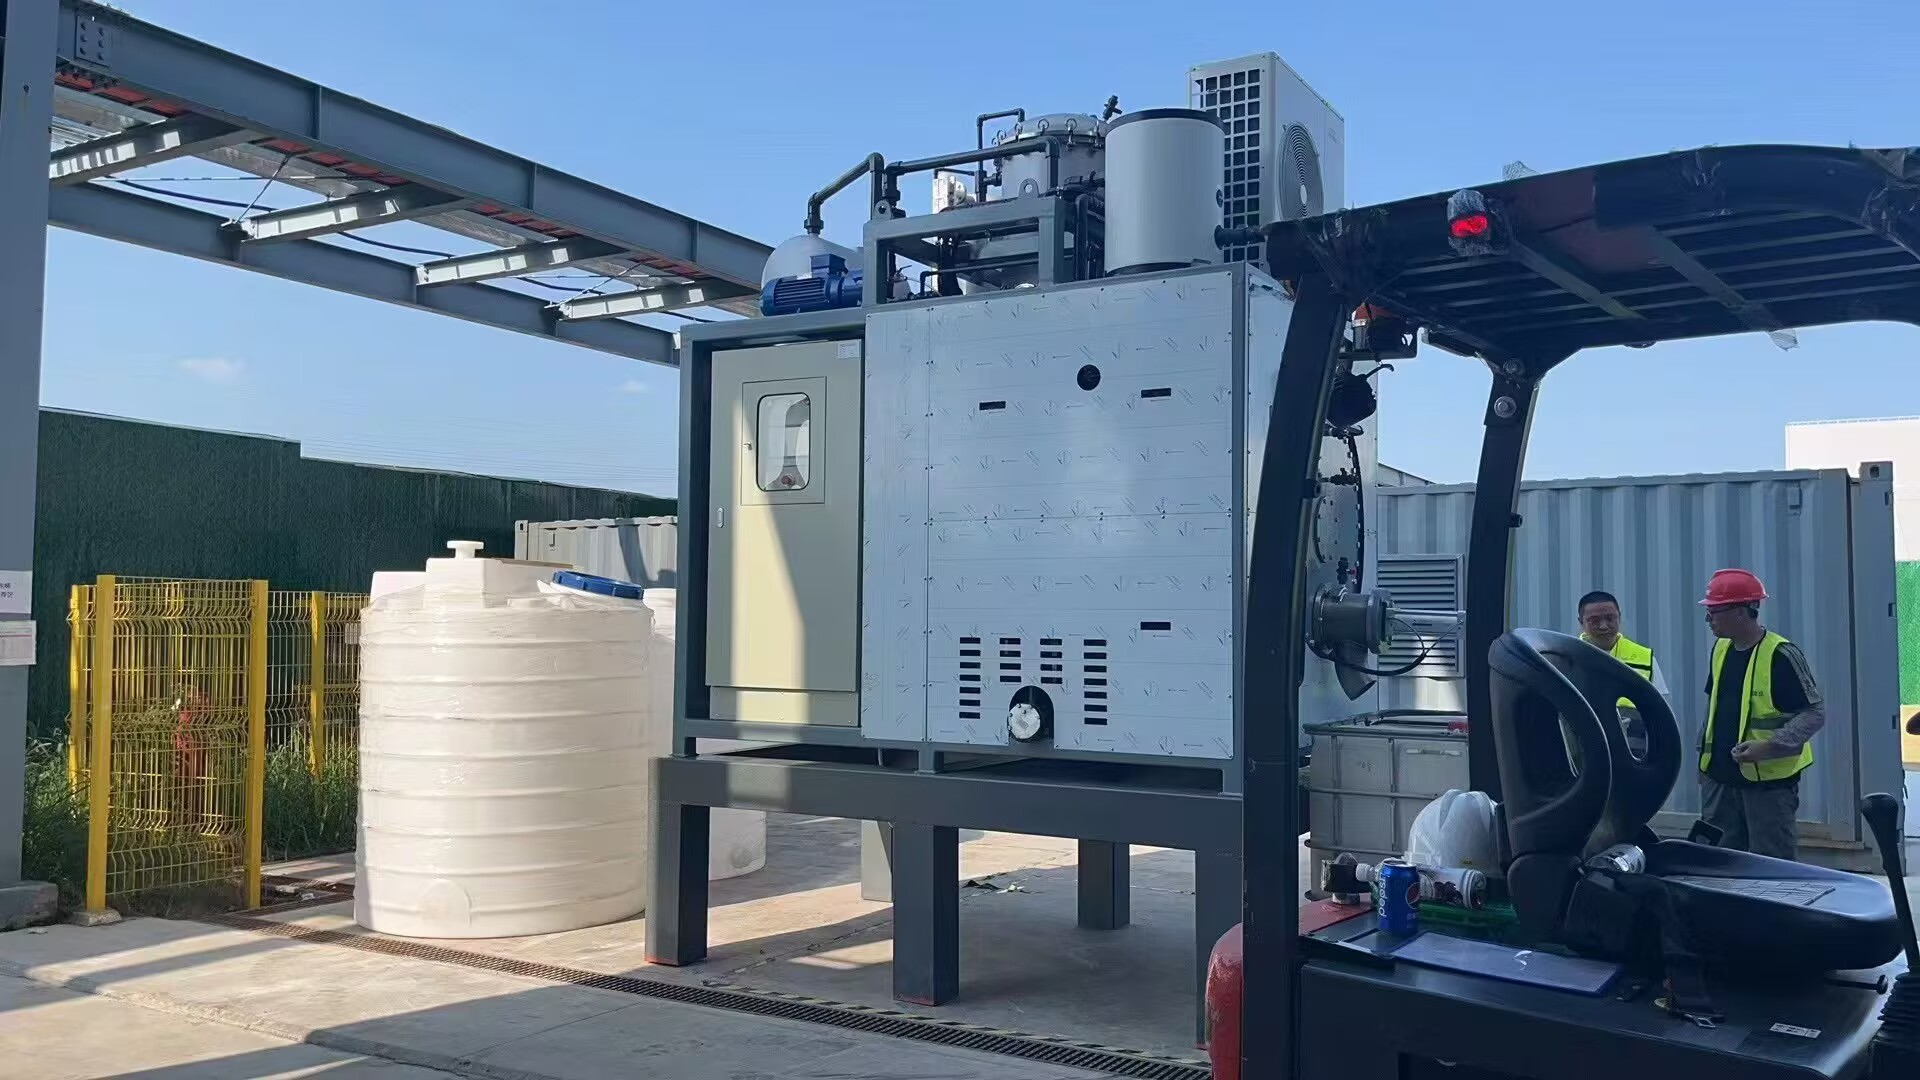
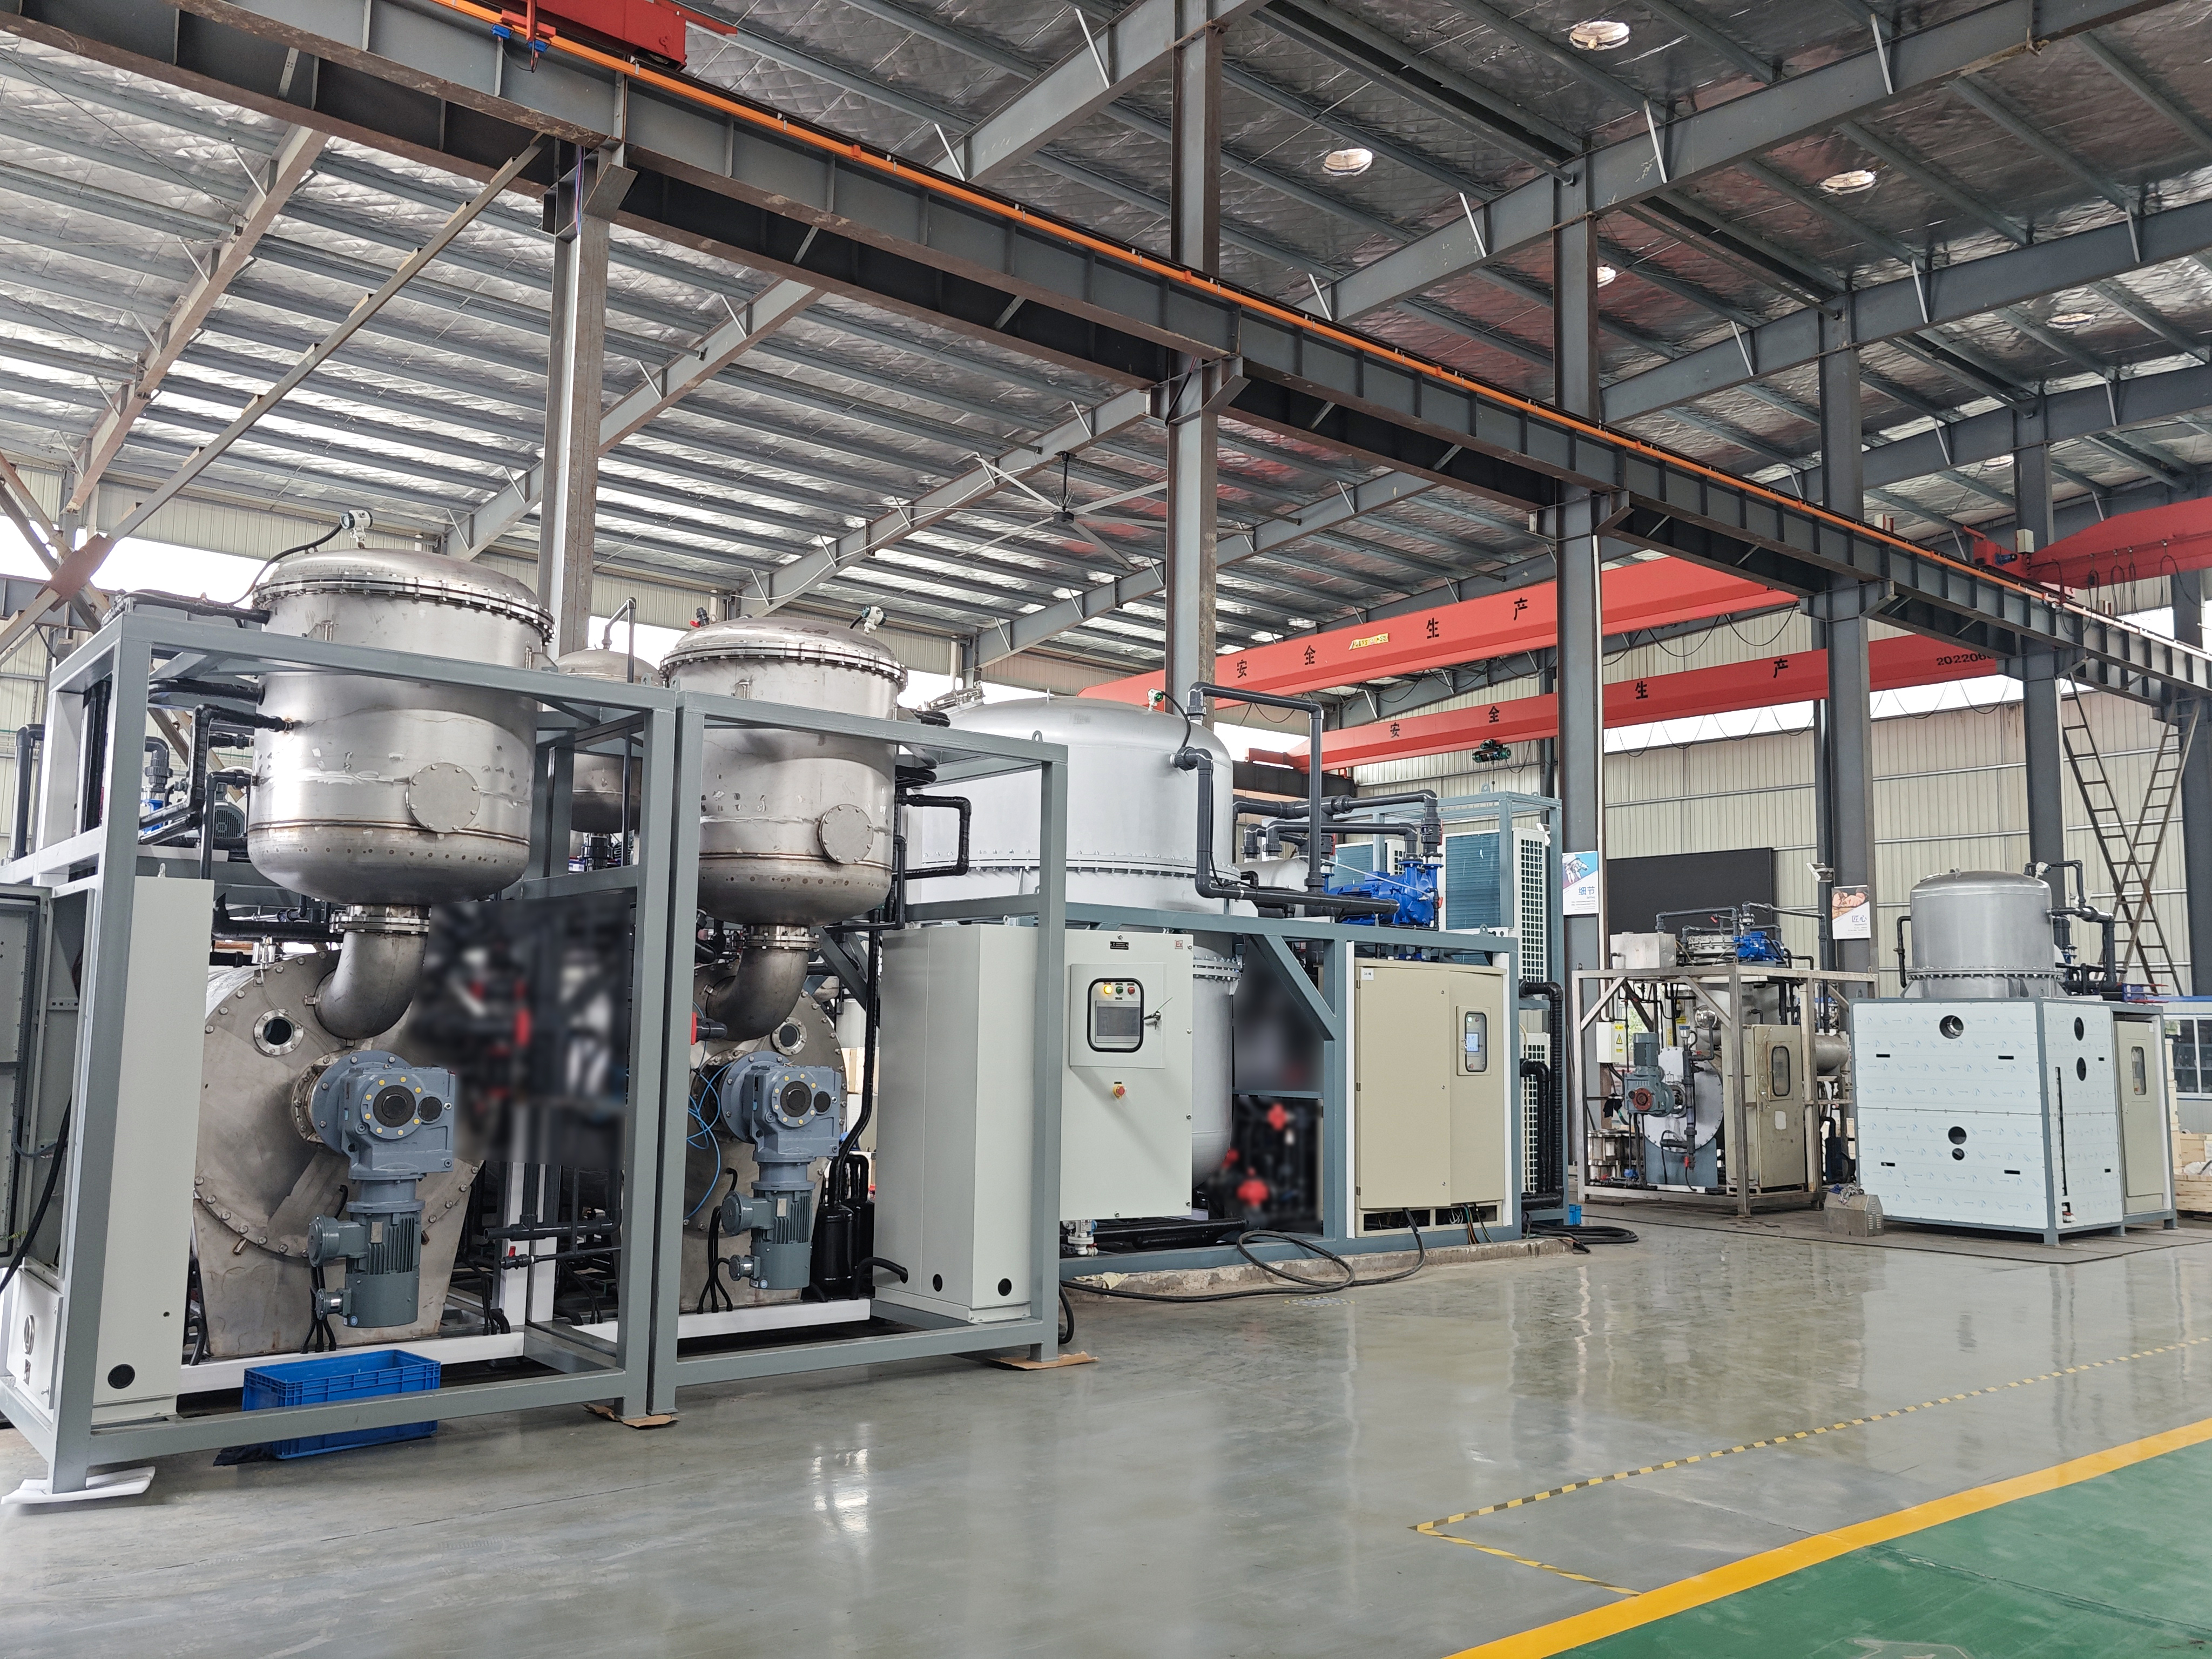
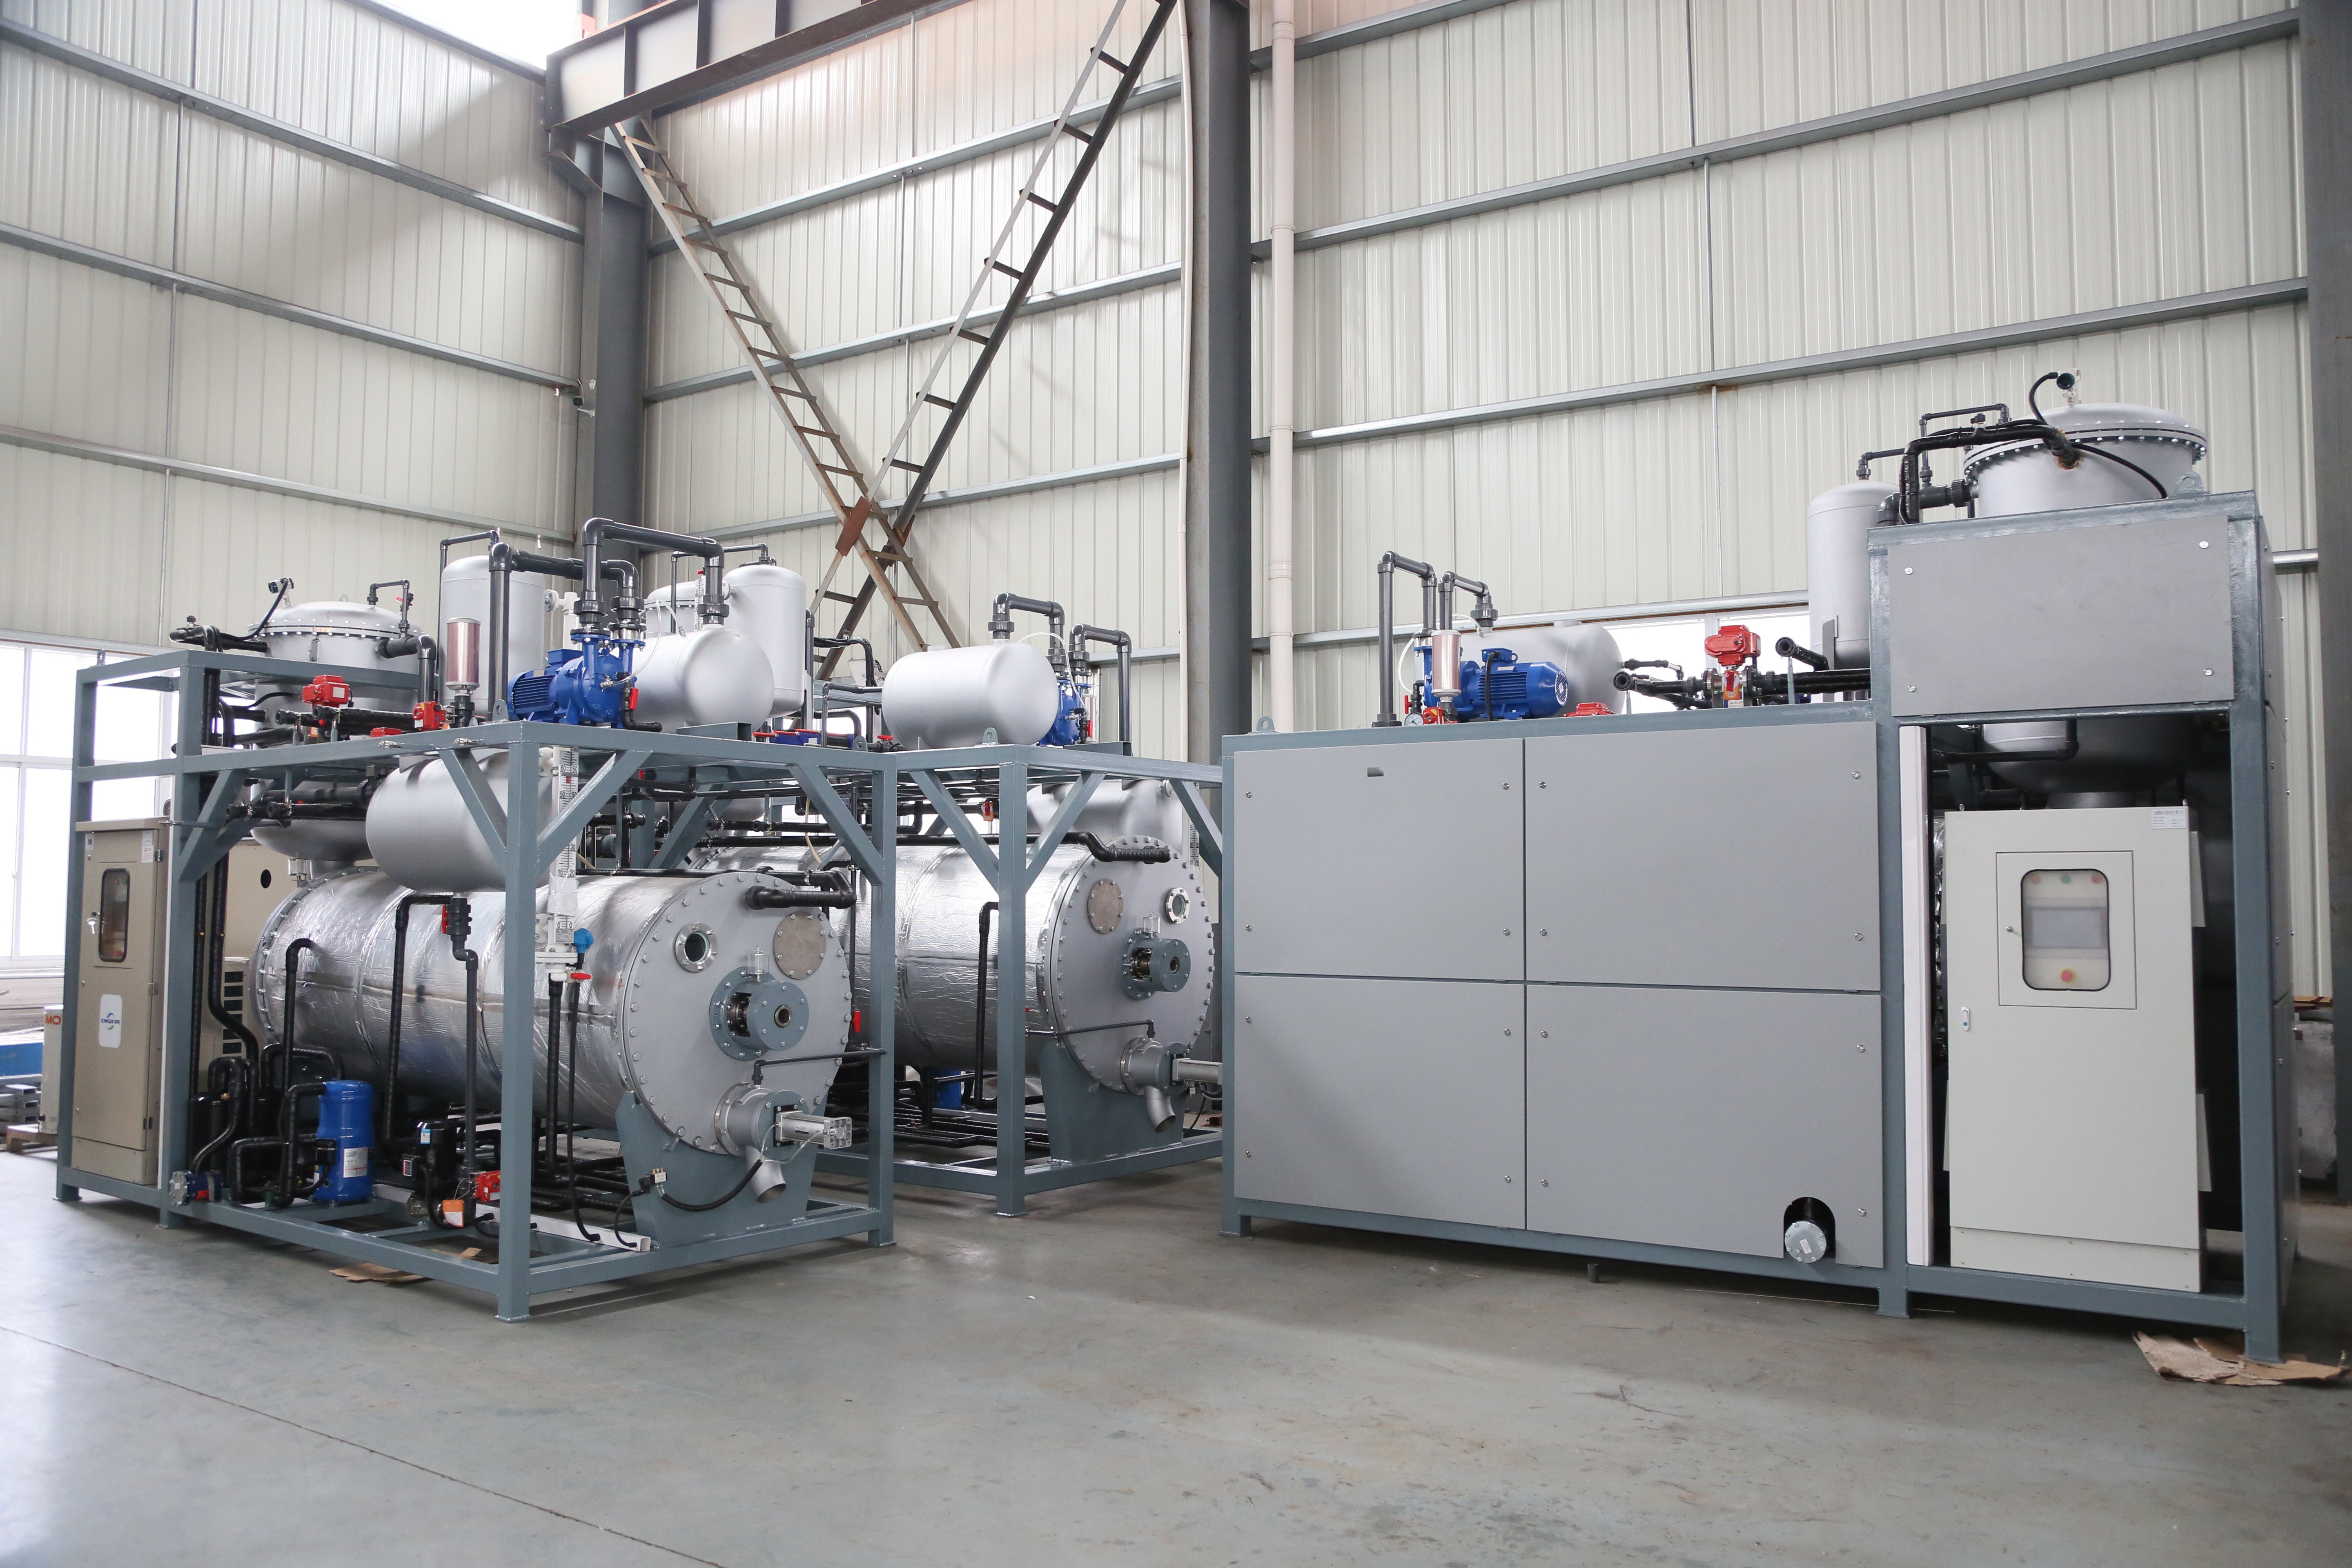
Vacuum membrane distillation represents a cutting-edge separation technology that combines membrane filtering with vacuum pressure to purify liquids effectively. This advanced process works by creating a pressure differential across a microporous membrane, allowing volatile components to evaporate while non-volatile substances remain behind. The vacuum membrane distillation technique operates at lower temperatures compared to conventional distillation methods, making it ideal for heat-sensitive materials. The primary function of vacuum membrane distillation is to separate and concentrate liquids by removing water, salts, and impurities while preserving the integrity of valuable compounds. The technology features a hydrophobic membrane that prevents liquid passage while permitting vapor transport. This selective permeability makes vacuum membrane distillation particularly effective for desalination, wastewater treatment, and pharmaceutical applications. Vacuum membrane distillation technology operates through several key mechanisms. The process maintains consistent pressure levels while regulating temperature to optimize separation efficiency. Applications span across industries including food processing, chemical manufacturing, environmental remediation, and medical sectors. The system's compact design and modular construction allow flexible deployment in various operational environments. Vacuum membrane distillation continues gaining adoption due to its environmental benefits and superior purification capabilities. The technology produces minimal waste while delivering high-quality purified water suitable for demanding industrial requirements and sensitive applications.

New Product Releases

Vacuum membrane distillation delivers exceptional value to customers seeking reliable purification solutions without compromising product quality. The most significant advantage is energy efficiency—this technology operates at substantially lower temperatures than traditional distillation methods, reducing operational costs and extending equipment lifespan. Your facility experiences immediate savings on heating requirements and maintenance expenses. Operational benefits are substantial and measurable. Vacuum membrane distillation operates continuously with minimal downtime, ensuring consistent output and predictable production schedules. The equipment requires simple maintenance routines, and replacement membrane modules are straightforward to install without complex procedures. This simplicity translates to reduced labor costs and faster troubleshooting when needed. Application suitability sets vacuum membrane distillation apart from competing technologies. The process handles heat-sensitive compounds effectively, making it invaluable for pharmaceutical companies, beverage producers, and specialty chemical manufacturers. Unlike traditional methods that degrade temperature-sensitive ingredients, vacuum membrane distillation preserves nutritional and chemical properties while achieving superior purity levels. The environmental advantages prove compelling for sustainability-focused organizations. Vacuum membrane distillation generates significantly less chemical waste and requires no harsh treatment chemicals, aligning with modern environmental regulations and corporate responsibility initiatives. Water recovery rates exceed conventional technologies, reducing freshwater consumption and wastewater disposal costs. Decision-useful context demonstrates why vacuum membrane distillation represents a smart investment. The scalability accommodates growth from pilot operations to full-scale production without process modifications. Implementation timelines are shorter than alternative purification systems, enabling faster market entry. The technology's proven track record across diverse industries provides confidence in reliability and performance outcomes that meet stringent quality standards consistently.

Latest News

How to Optimize Your Evaporator System for Efficiency

24

Jul

How to Optimize Your Evaporator System for Efficiency

An evaporator system efficiency directly impacts your operational costs, production capacity, and environmental footprint in industrial processing. Whether you operate in chemical manufacturing, food processing, pharmaceutical production, or waste ma...
View More
Industrial Water Treatment Technologies for 2026

02

Sep

Industrial Water Treatment Technologies for 2026

Industrial water treatment remains one of the most critical operational priorities across manufacturing, chemical processing, food production, and energy sectors. As facilities face increasingly stringent environmental regulations, rising operational...
View More
Common Challenges in Industrial Water Treatment Solved

02

Sep

Common Challenges in Industrial Water Treatment Solved

Manufacturing facilities, chemical plants, and processing operations face mounting pressure to manage wastewater efficiently while meeting regulatory standards. Industrial water treatment remains one of the most critical operational functions across ...
View More
Top 5 Evaporator System Design Features for Industry

24

Jul

Top 5 Evaporator System Design Features for Industry

Selecting the right evaporator system design is critical for industrial operations managing wastewater treatment, chemical processing, and liquid concentration challenges. An effective evaporator system design determines not only operational efficien...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

vacuum membrane distillation

Superior Energy Efficiency and Cost Reduction

Superior Energy Efficiency and Cost Reduction

Vacuum membrane distillation operates at significantly lower temperatures—typically between 30-60°C—compared to conventional distillation requiring 100°C or higher. This temperature advantage translates directly into reduced energy consumption, lowering utility bills substantially. Your operational costs decrease as heating requirements diminish, and equipment experiences less thermal stress, extending service life considerably. Vacuum membrane distillation achieves remarkable thermal efficiency while maintaining exceptional separation performance. The lower operating temperatures also reduce carbon emissions associated with energy production, supporting sustainability objectives. For facilities processing large liquid volumes continuously, the accumulated energy savings over months and years become substantial financial benefits. Companies implementing vacuum membrane distillation typically report 40-60% reductions in thermal energy requirements compared to traditional methods. The technology's economic advantage extends beyond direct energy costs, as reduced heat generation decreases cooling system demands. Investment in vacuum membrane distillation equipment pays dividends through consistent operational savings throughout the system's lifetime.
Gentle Processing for Heat-Sensitive Materials

Gentle Processing for Heat-Sensitive Materials

Vacuum membrane distillation excels at treating temperature-sensitive compounds that conventional distillation would damage or degrade. The low-temperature operation preserves delicate pharmaceutical compounds, essential oils, vitamins, and specialty chemicals that demand gentle handling. This capability makes vacuum membrane distillation indispensable for industries where product integrity directly affects market value and regulatory compliance. Heat-sensitive applications benefit tremendously from vacuum membrane distillation's protective processing conditions. Volatile aromatic compounds remain intact, nutritional components suffer no degradation, and molecular structures stay undamaged throughout purification. The technology handles complex mixtures containing multiple sensitive components without compromising any single ingredient. Pharmaceutical manufacturers particularly value vacuum membrane distillation for processing biotech products requiring absolute preservation of efficacy. Beverage companies utilize this technology for juice concentration while maintaining fresh flavor profiles. Food processors apply vacuum membrane distillation to extract valuable components without altering taste or nutritional content. The technique represents the optimal solution when material sensitivity supersedes speed considerations in processing decisions.
Compact Design with Modular Scalability

Compact Design with Modular Scalability

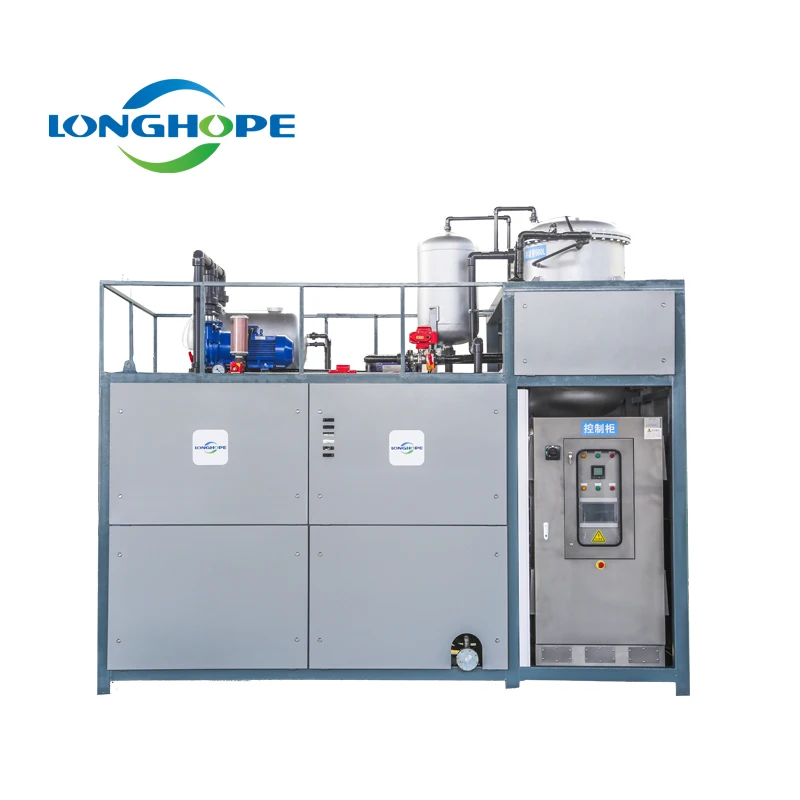
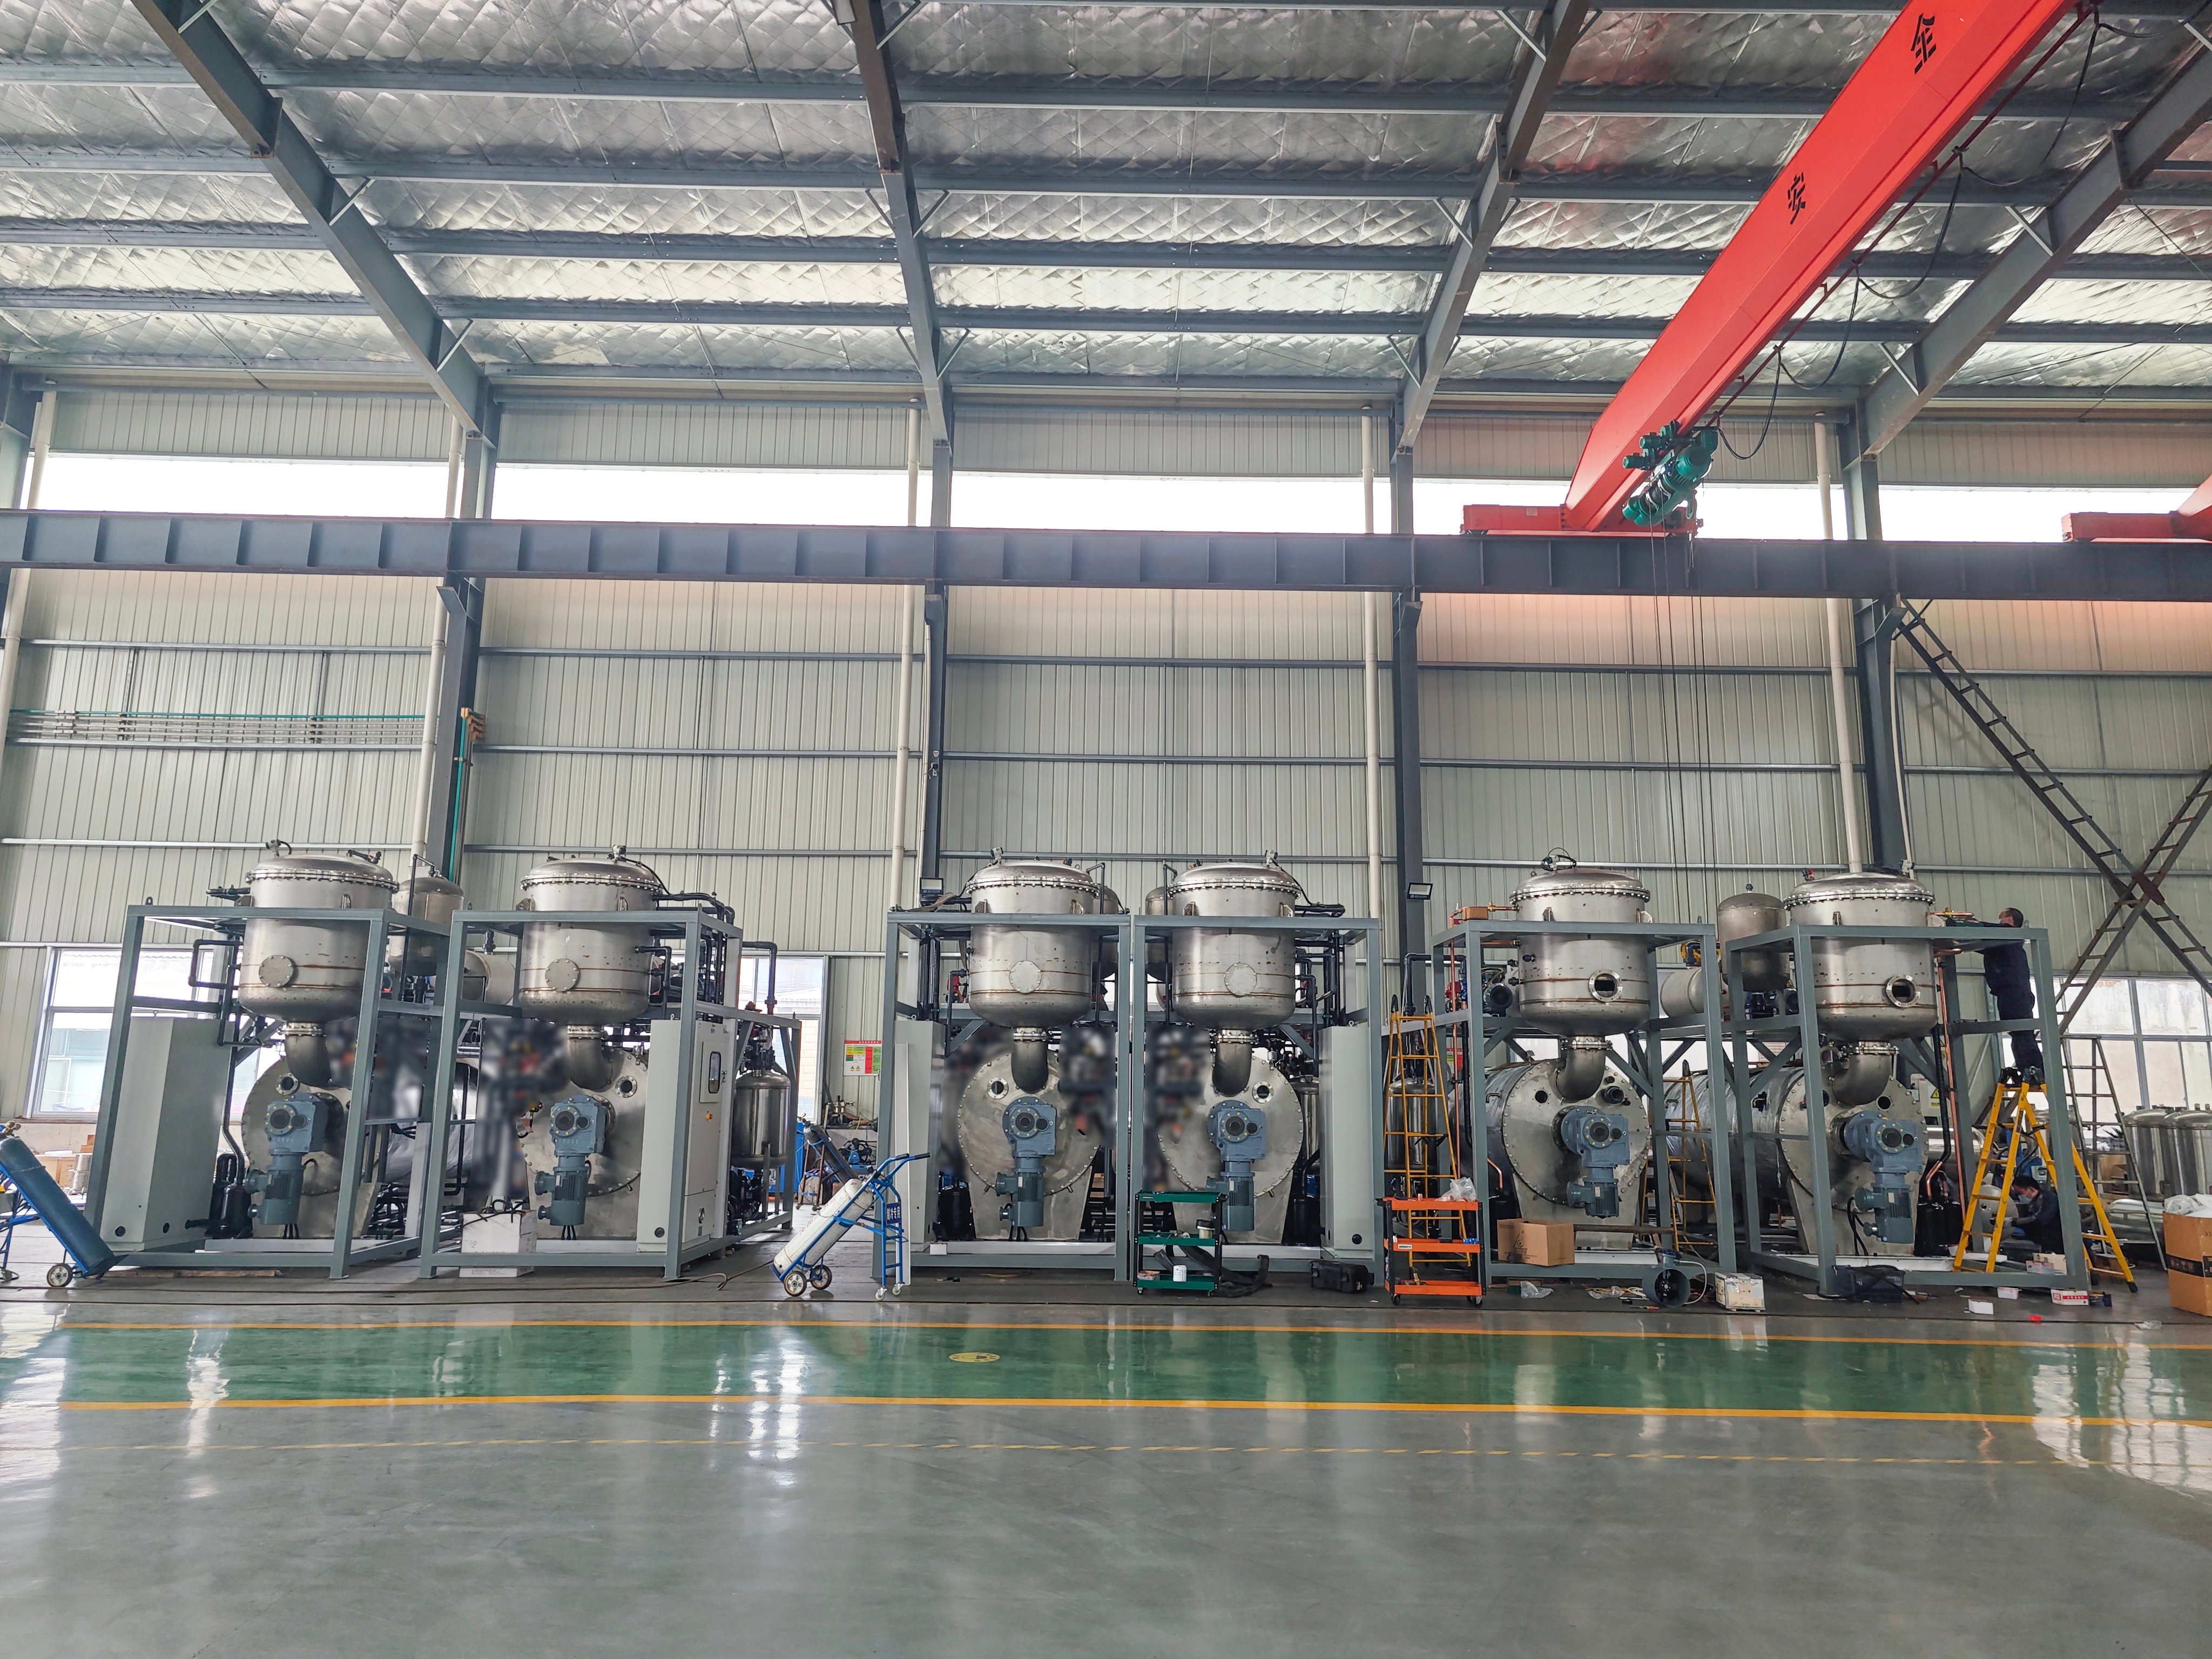
Vacuum membrane distillation systems feature remarkably compact footprints, occupying minimal facility space compared to traditional distillation towers requiring extensive floor areas. The modular design allows businesses to start with single-unit installations and expand capacity seamlessly by adding additional modules without complete system overhauls. This scalability provides extraordinary flexibility for growing operations or variable production demands. The modular architecture of vacuum membrane distillation enables customization for specific application requirements. Additional modules integrate effortlessly into existing systems, scaling production capacity proportionally without introducing operational complexity. This approach proves particularly valuable for contract manufacturers and seasonal processors requiring flexible capacity management. Installation simplicity accelerates deployment timelines significantly—vacuum membrane distillation systems integrate into existing facilities within weeks rather than months. Retrofitting established production lines becomes feasible due to compact dimensions and straightforward integration requirements. The space-saving advantages allow facilities to maintain multiple separation processes simultaneously within existing buildings. Modular vacuum membrane distillation systems provide future-proofing advantages, accommodating technological upgrades and capacity expansions without costly facility modifications or production interruptions.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000