Industrial Water Treatment Plants | Efficient Solutions

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

water treatment plant for industrial use

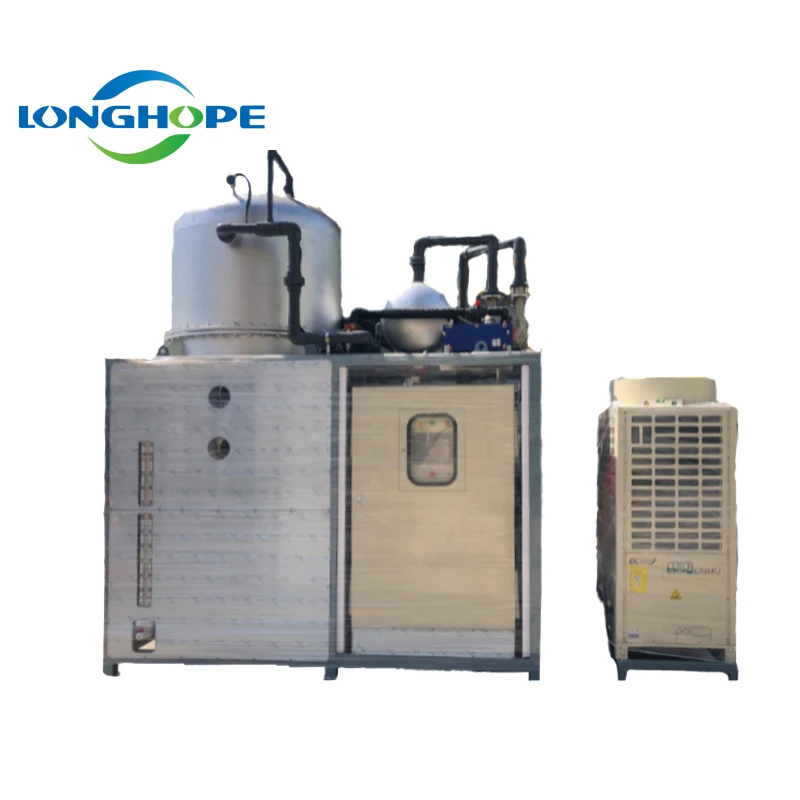
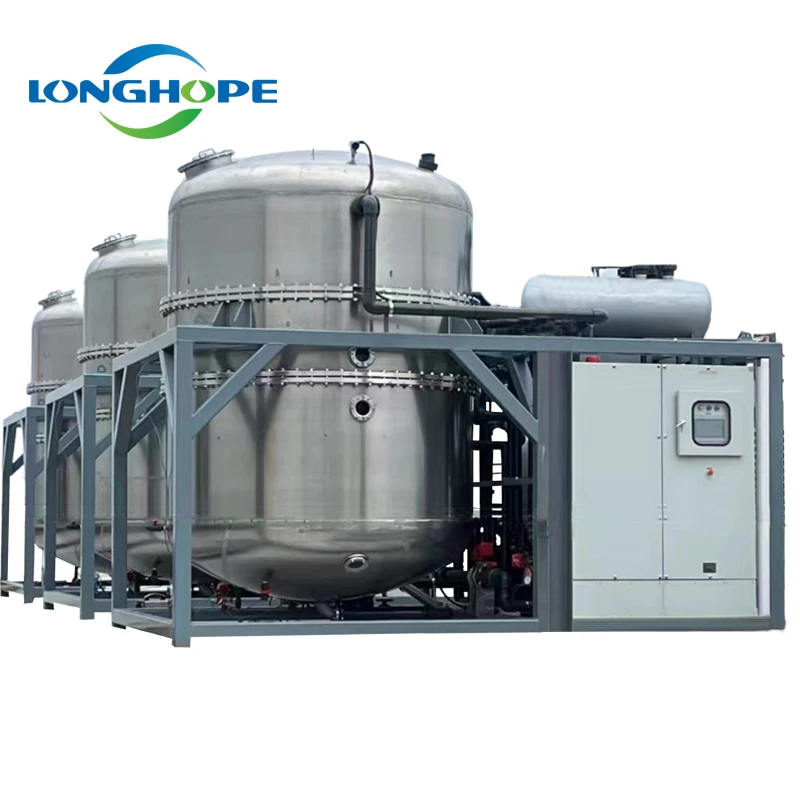
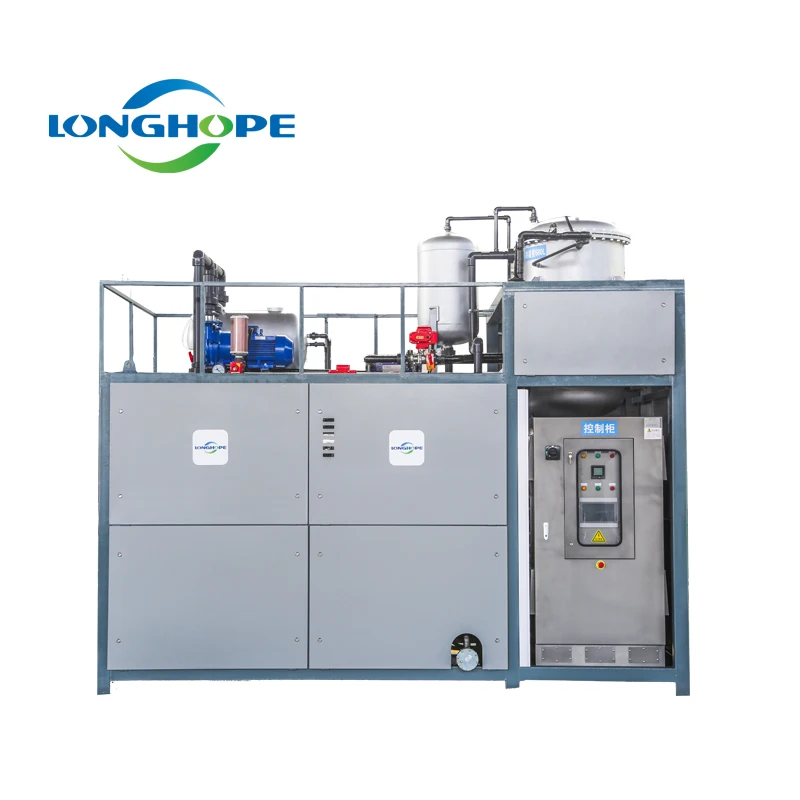
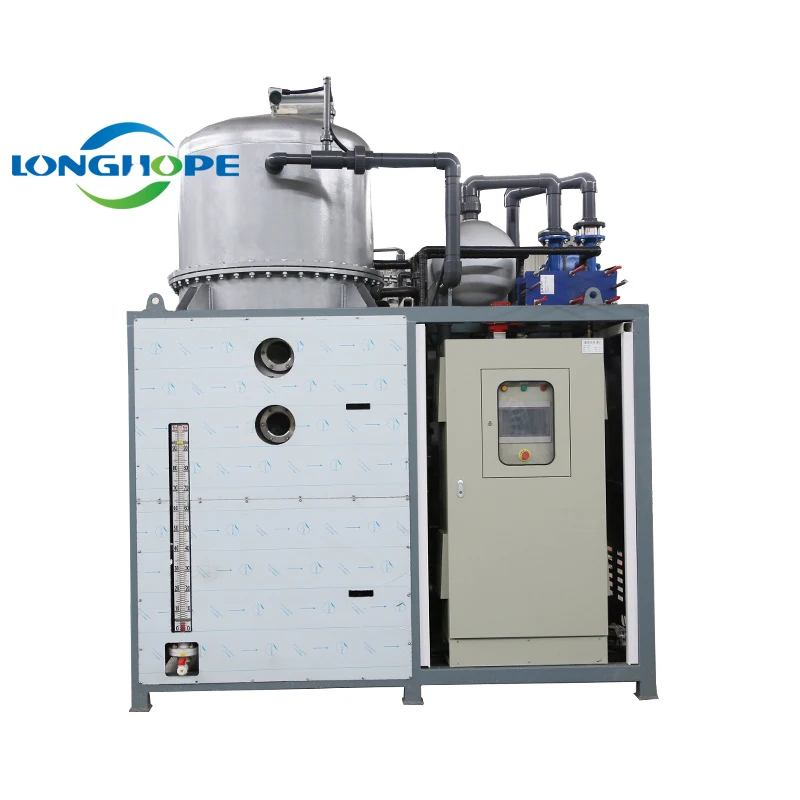
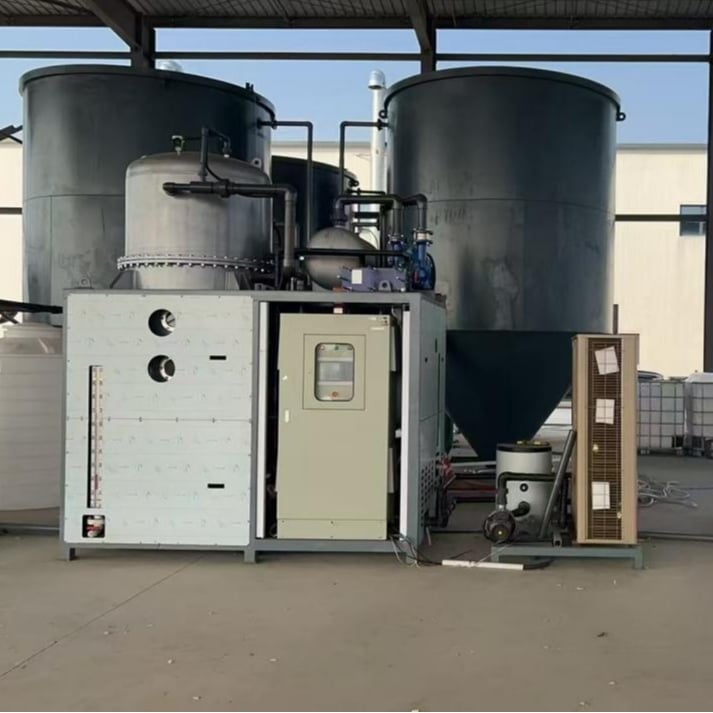
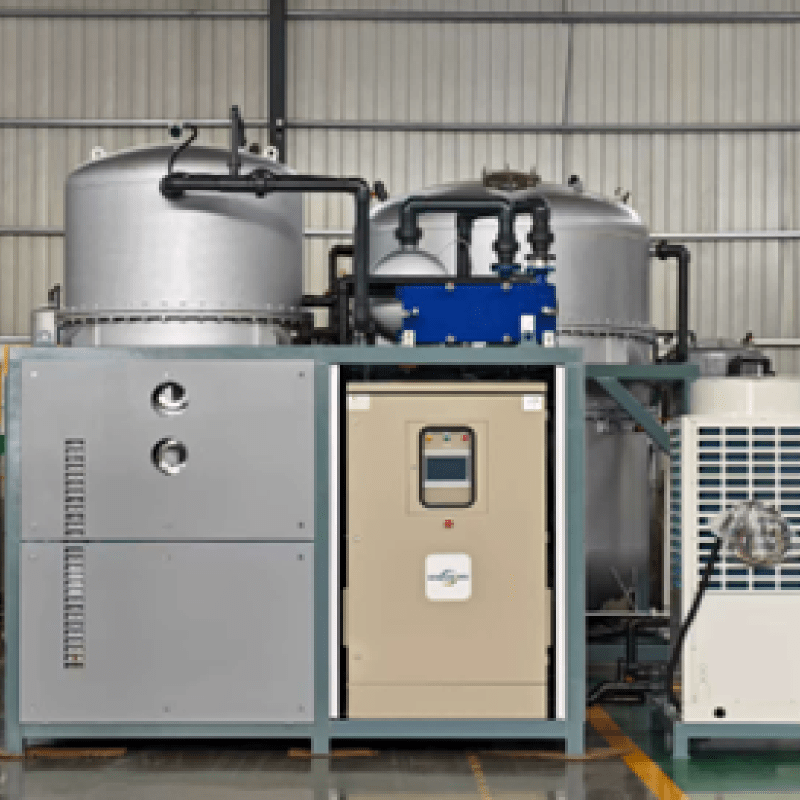
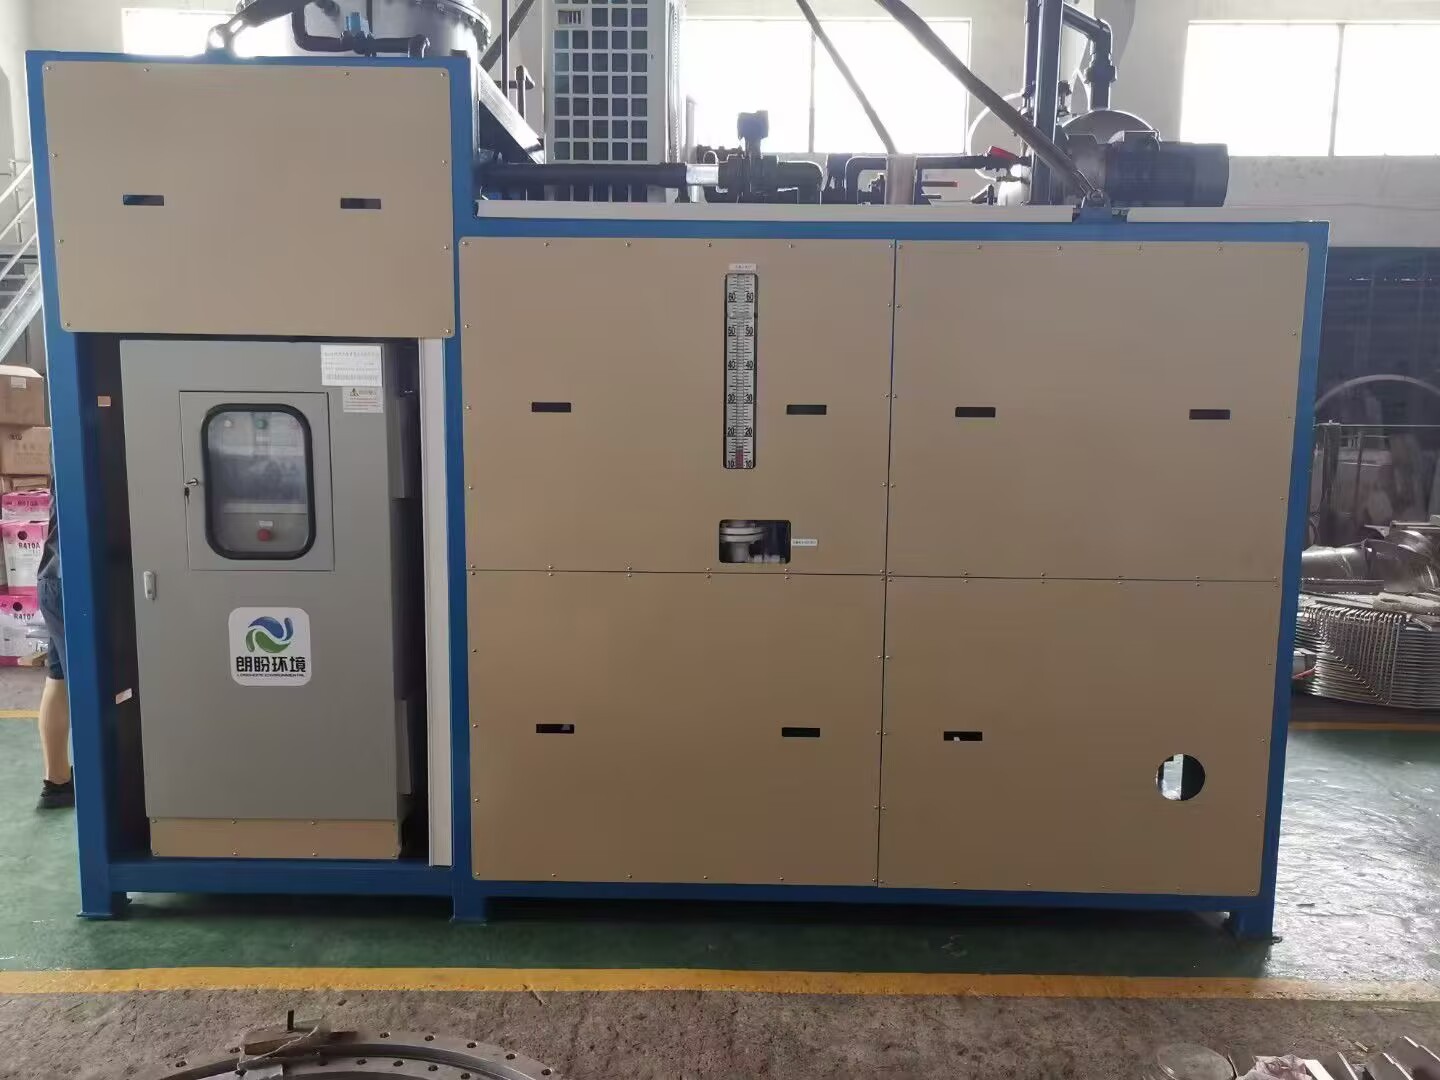
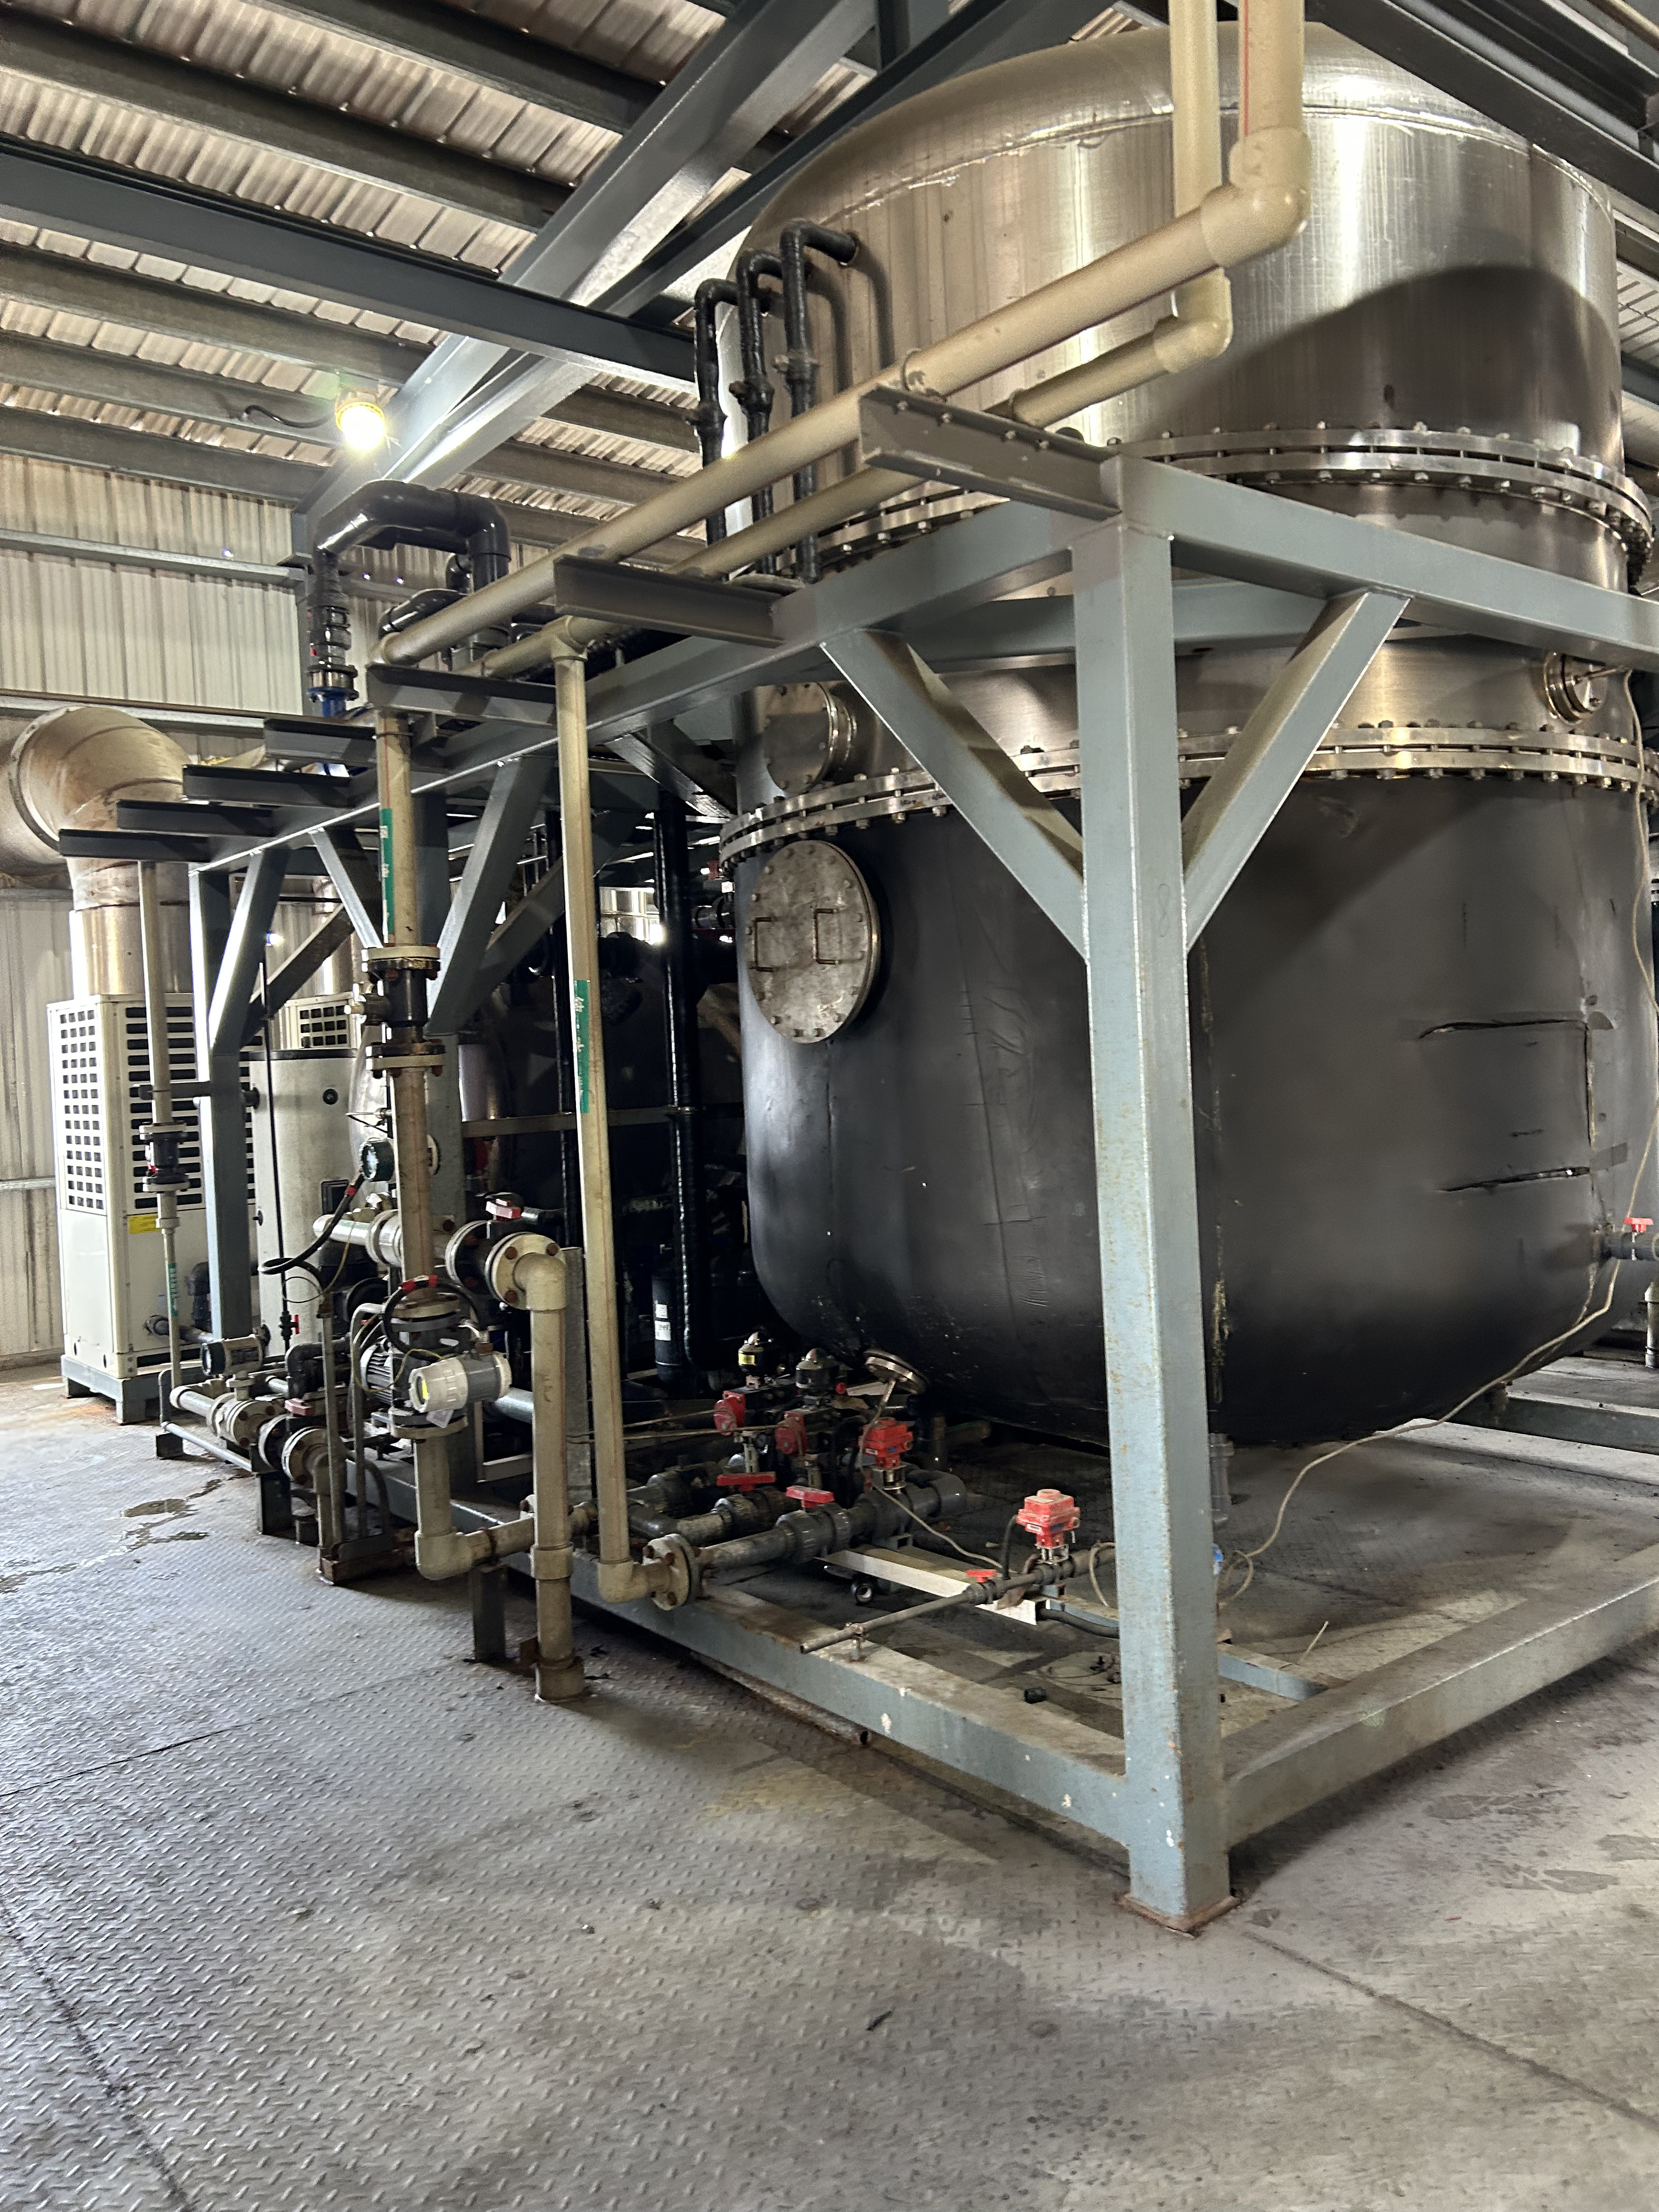
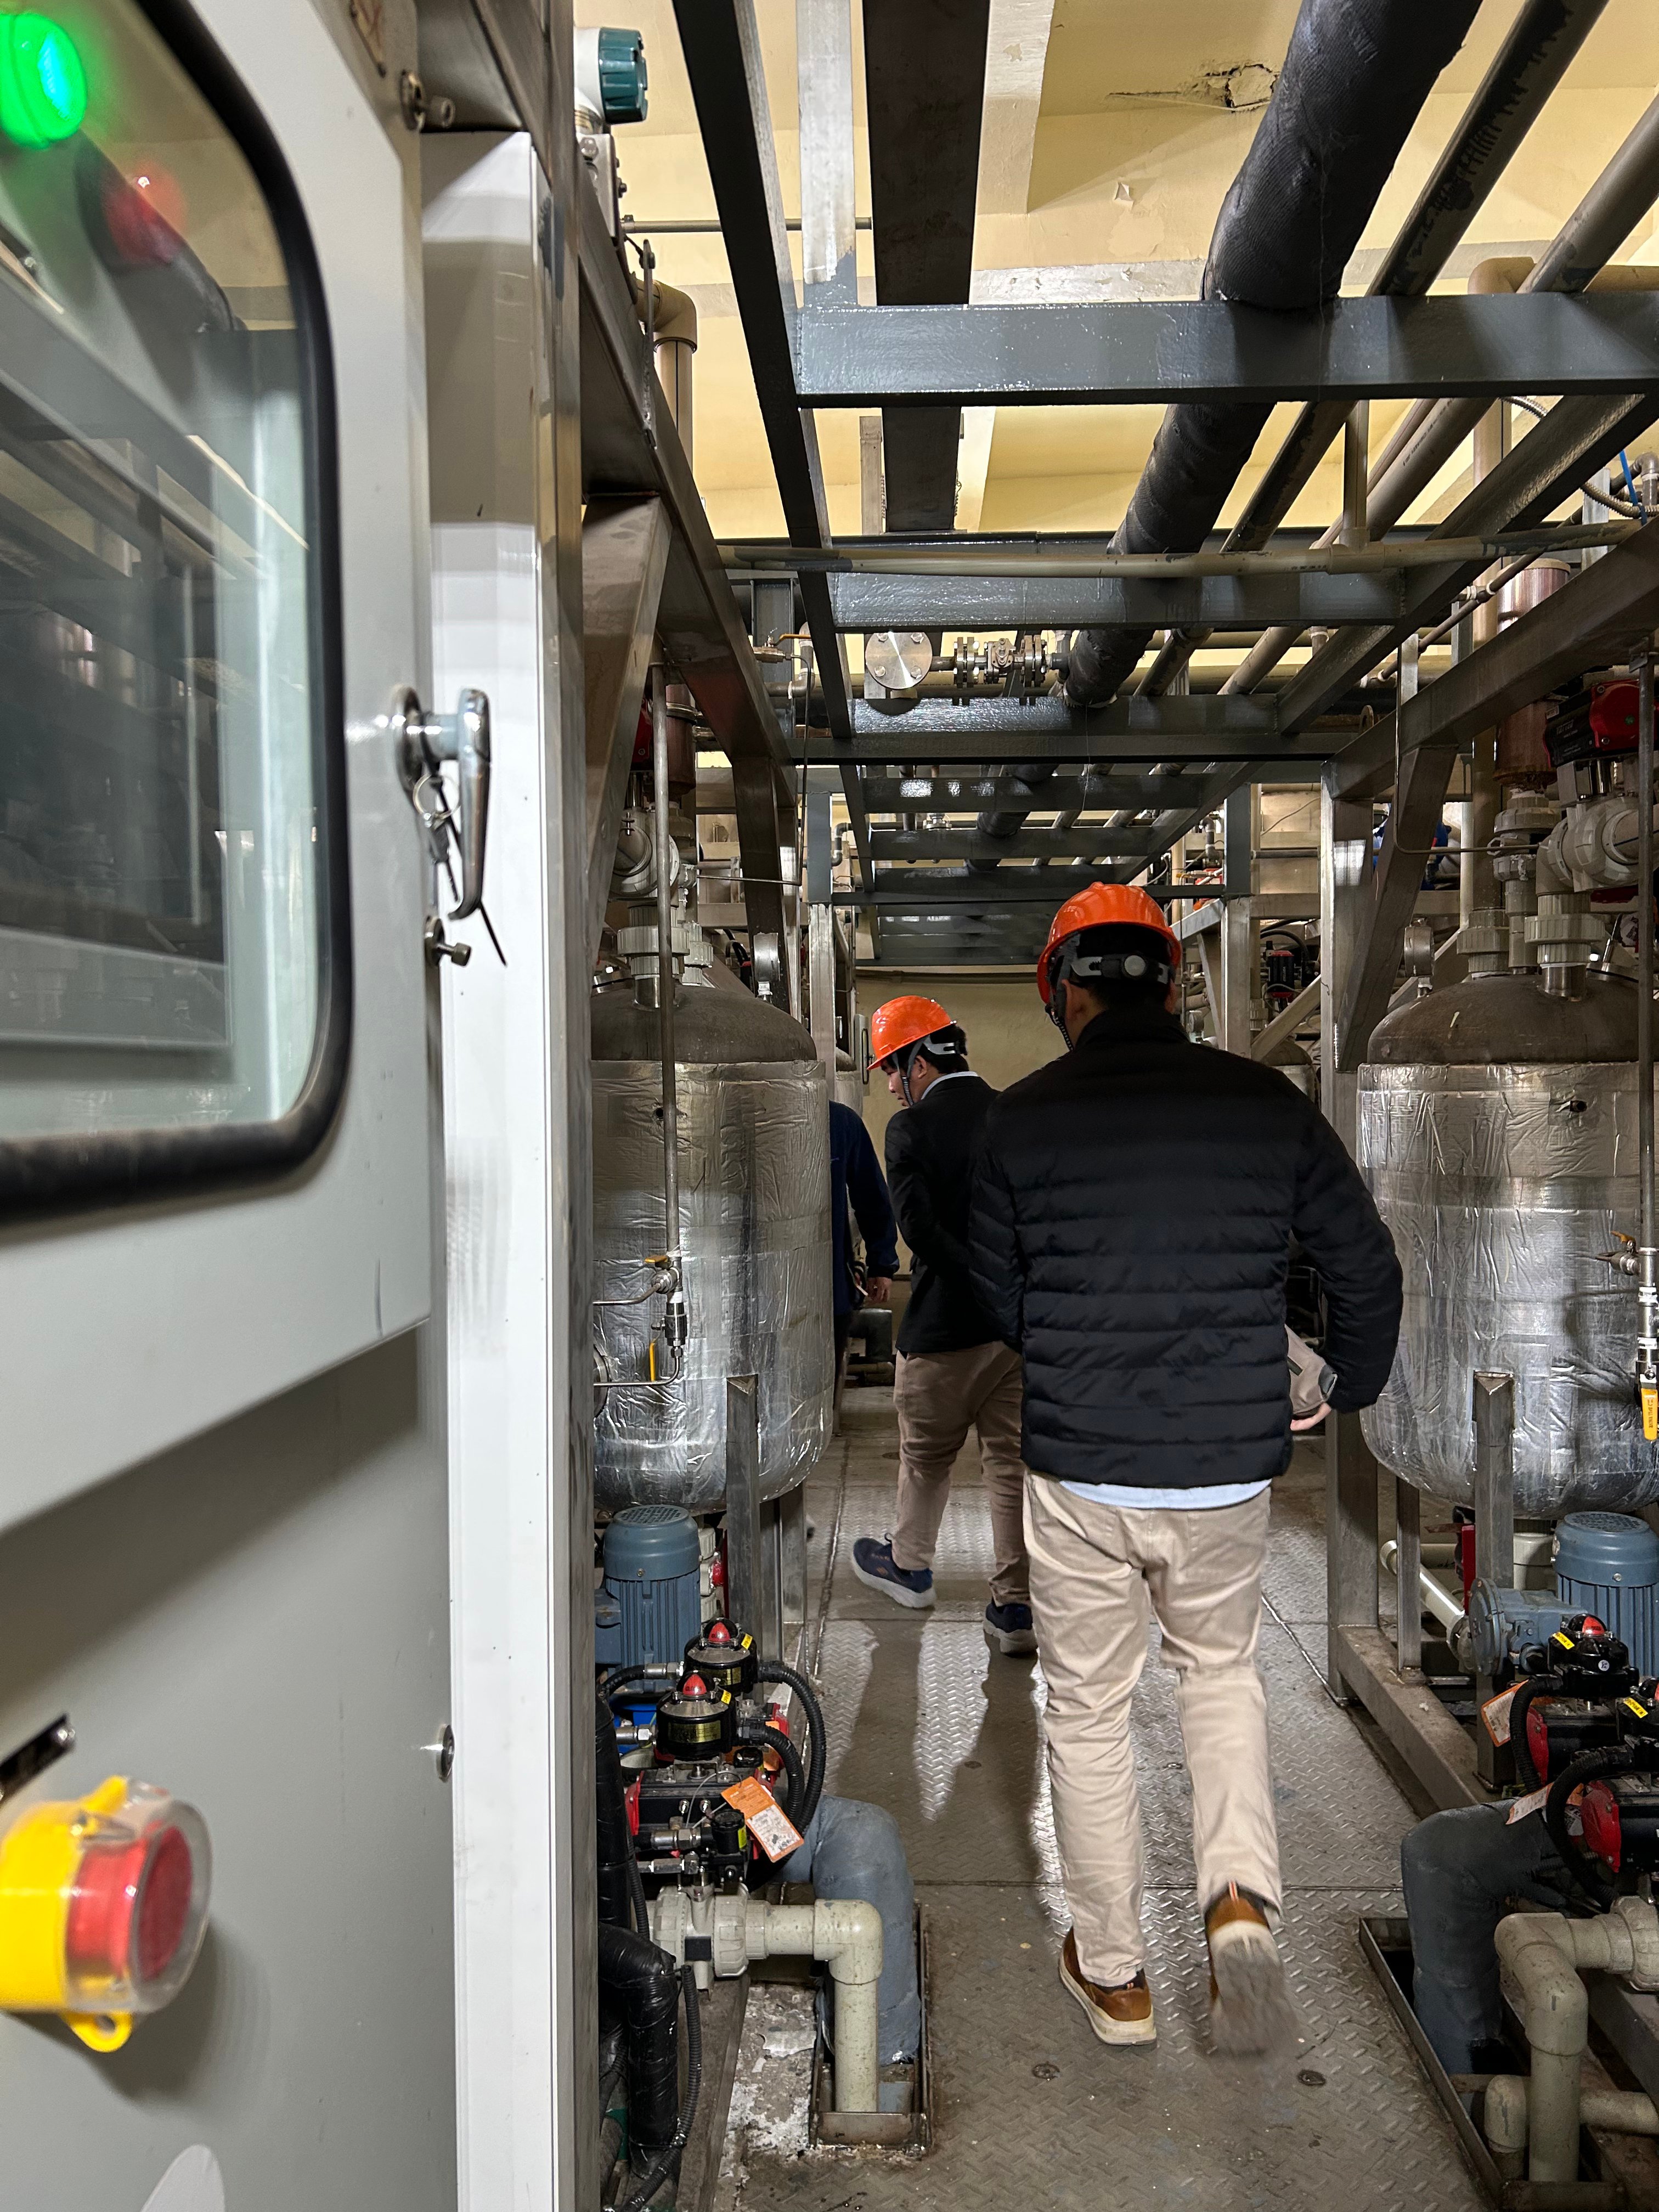
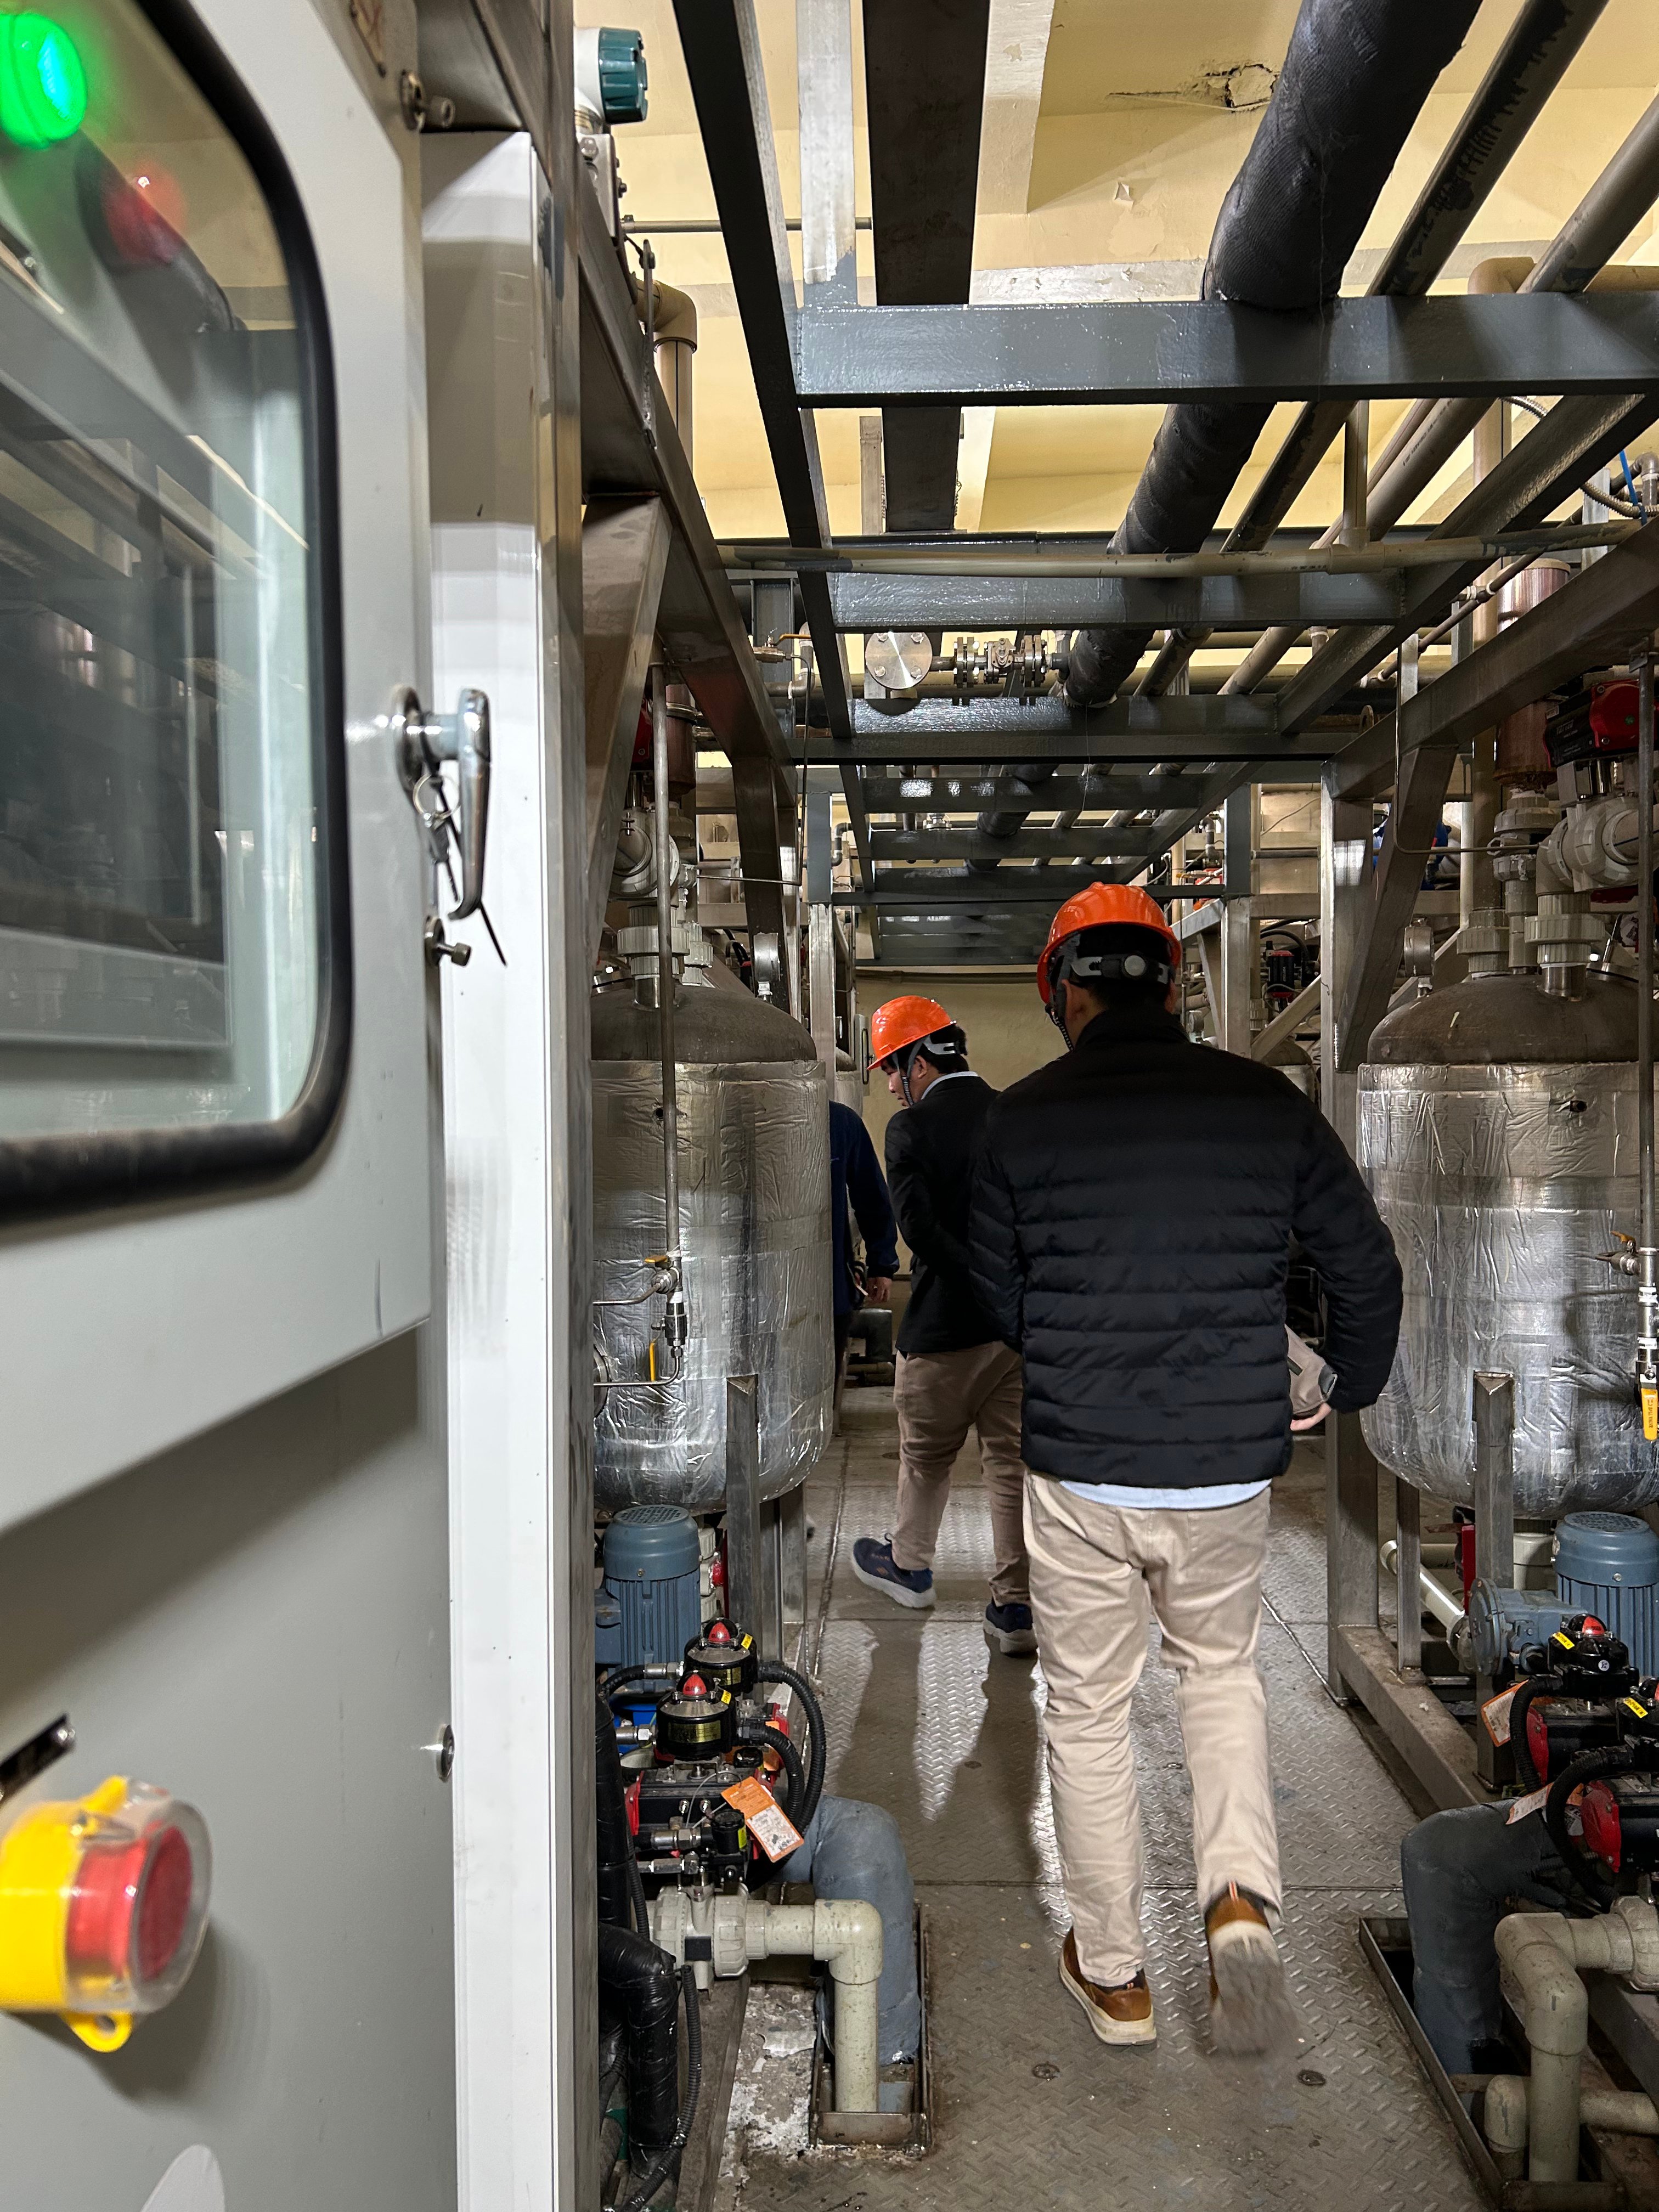
A water treatment plant for industrial use represents a comprehensive solution designed to purify and manage water resources for manufacturing, processing, and operational needs. This specialized system addresses the critical demand for clean, safe water in industrial facilities while ensuring compliance with environmental regulations and operational efficiency. The primary function of a water treatment plant for industrial use is to remove contaminants, suspended solids, chemicals, and biological matter from raw water sources. Industrial facilities require treated water for cooling systems, steam generation, product manufacturing, and equipment operation. The water treatment plant for industrial use employs advanced filtration technologies, including activated carbon filters, reverse osmosis membranes, and ultraviolet sterilization systems. Technologically, modern water treatment plants feature automated monitoring systems that track water quality in real-time. These plants incorporate multi-stage treatment processes that address specific industrial requirements. The water treatment plant for industrial use integrates chemical treatment, physical separation, and biological remediation methods to achieve optimal water purity levels. Applications span diverse industries including pharmaceuticals, food and beverage production, textile manufacturing, power generation, and chemical processing. Each sector depends on the water treatment plant for industrial use to meet stringent quality standards and regulatory compliance. The system's scalability allows adaptation to various facility sizes and production volumes, making it essential infrastructure for modern industrial operations.

New Product Recommendations

A water treatment plant for industrial use delivers substantial operational and financial benefits that directly impact your manufacturing efficiency and bottom line. By investing in a dedicated water treatment plant for industrial use, your facility gains access to consistent, high-quality water that meets stringent industry standards and regulatory requirements. Operational efficiency represents the primary advantage. The water treatment plant for industrial use reduces equipment downtime by preventing scale buildup, corrosion, and contamination within your systems. This translates to longer machinery lifespan and reduced maintenance costs. Your production processes experience fewer interruptions, enabling higher output and improved profitability. Cost reduction is another critical benefit. Rather than purchasing expensive bottled or pre-treated water, the water treatment plant for industrial use treats existing water sources on-site, dramatically lowering per-unit water expenses. Lower chemical consumption and reduced waste disposal fees further enhance your financial performance. Environmental compliance becomes straightforward with a water treatment plant for industrial use. The system ensures your facility meets local and national water quality standards, eliminating regulatory penalties and legal complications. Your company demonstrates environmental responsibility while maintaining operational flexibility. Product quality improvement is essential for competitive advantage. The water treatment plant for industrial use provides consistently pure water that enhances manufacturing quality and product consistency. This reliability strengthens customer relationships and market reputation. Scalability represents a practical advantage. Whether your facility expands or contracts, the water treatment plant for industrial use adapts to changing water demands without requiring complete system replacement. This flexibility protects your capital investment long-term.

Tips And Tricks

Low Temperature Heat Pump Evaporator Maintenance Best Practices

24

Jul

Low Temperature Heat Pump Evaporator Maintenance Best Practices

Effective low temperature heat pump evaporator maintenance is essential for preserving system efficiency, extending equipment lifespan, and preventing costly downtime in industrial refrigeration applications. The evaporator represents a critical heat...
View More
Benefits of Low Temperature Heat Pump Evaporator in Industry

24

Jul

Benefits of Low Temperature Heat Pump Evaporator in Industry

Industrial facilities worldwide face mounting pressure to reduce operating costs while maintaining production quality and environmental compliance. The low temperature heat pump evaporator has emerged as a transformative solution that addresses these...
View More
Low Temperature Heat Pump Evaporator: Energy Saving Guide

24

Jul

Low Temperature Heat Pump Evaporator: Energy Saving Guide

Industrial facilities continuously seek ways to reduce operational costs while maintaining peak performance. A low temperature heat pump evaporator represents one of the most effective technologies for achieving significant energy savings in thermal ...
View More
Evaporator System Maintenance: Tips for Longevity

24

Jul

Evaporator System Maintenance: Tips for Longevity

Evaporator system maintenance is critical to ensuring your industrial cooling and waste-water treatment equipment operates reliably and efficiently over the long term. Whether your facility relies on evaporator systems for refrigeration, heat exchang...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000

water treatment plant for industrial use

Advanced Filtration Technology for Superior Water Purity

Advanced Filtration Technology for Superior Water Purity

The water treatment plant for industrial use incorporates multi-stage filtration systems that deliver exceptional water purity levels. This advanced technology combines mechanical filtration, chemical treatment, and membrane separation to remove contaminants at microscopic levels. The system efficiently eliminates suspended solids, dissolved minerals, organic compounds, and biological pollutants that could compromise your industrial processes. Advanced filtration ensures your equipment operates optimally without corrosion or scale accumulation. Industries relying on ultra-pure water, such as semiconductor manufacturing and pharmaceuticals, depend on this technological capability. The water treatment plant for industrial use maintains consistent performance across varying source water conditions, adapting automatically to seasonal changes and contamination fluctuations. Real-time monitoring sensors alert operators to any quality deviations, enabling immediate corrective action. This proactive approach prevents production disruptions and maintains product quality standards consistently.
Automated Monitoring and Control Systems for Operational Reliability

Automated Monitoring and Control Systems for Operational Reliability

Modern water treatment plants feature sophisticated automated systems that continuously monitor water quality parameters without manual intervention. The water treatment plant for industrial use incorporates sensors measuring pH, turbidity, total dissolved solids, conductivity, and chlorine residuals. Automated controls adjust treatment processes in real-time, ensuring optimal performance under all operational conditions. Operators receive instant alerts when parameters deviate from preset ranges, enabling quick response and preventing compliance violations. The water treatment plant for industrial use reduces labor requirements and human error, enhancing operational consistency and safety. Integration with facility management systems enables remote monitoring from multiple locations, improving operational oversight. Predictive maintenance capabilities identify equipment degradation before failures occur, minimizing downtime. Historical data logging provides valuable insights for process optimization and regulatory documentation, simplifying compliance reporting and auditing procedures.
Cost-Effective Sustainability for Long-Term Industrial Operations

Cost-Effective Sustainability for Long-Term Industrial Operations

Investing in a water treatment plant for industrial use creates substantial long-term financial and environmental benefits for your facility. This system eliminates expensive reliance on external water suppliers and reduces per-unit treatment costs significantly. The water treatment plant for industrial use decreases chemical consumption compared to traditional treatment methods, lowering operational expenses and environmental impact simultaneously. Energy-efficient designs minimize electricity requirements, further reducing operating costs. Waste reduction capabilities mean less sludge disposal and fewer environmental compliance fees. The water treatment plant for industrial use demonstrates corporate commitment to sustainability, enhancing brand reputation with environmentally conscious stakeholders. Lower water consumption reduces municipal fees and promotes responsible resource management. Depreciation benefits and potential tax incentives for environmental infrastructure investments improve financial performance. Over a typical ten-year operational period, most facilities recover their initial investment through cumulative savings, making the water treatment plant for industrial use a financially prudent decision for industrial operators.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile
Name
Company Name
Message
0/1000