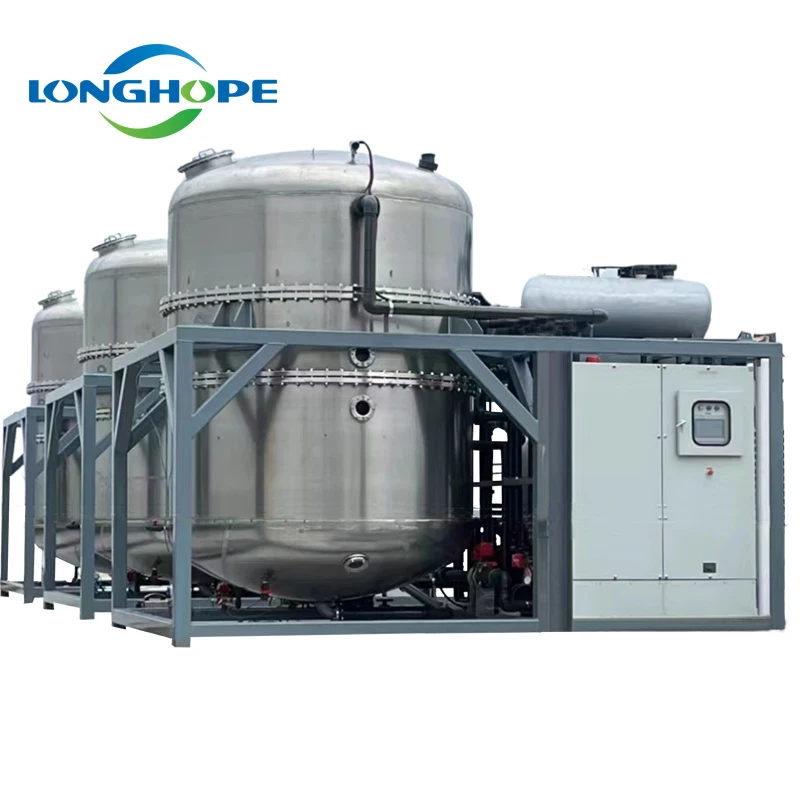
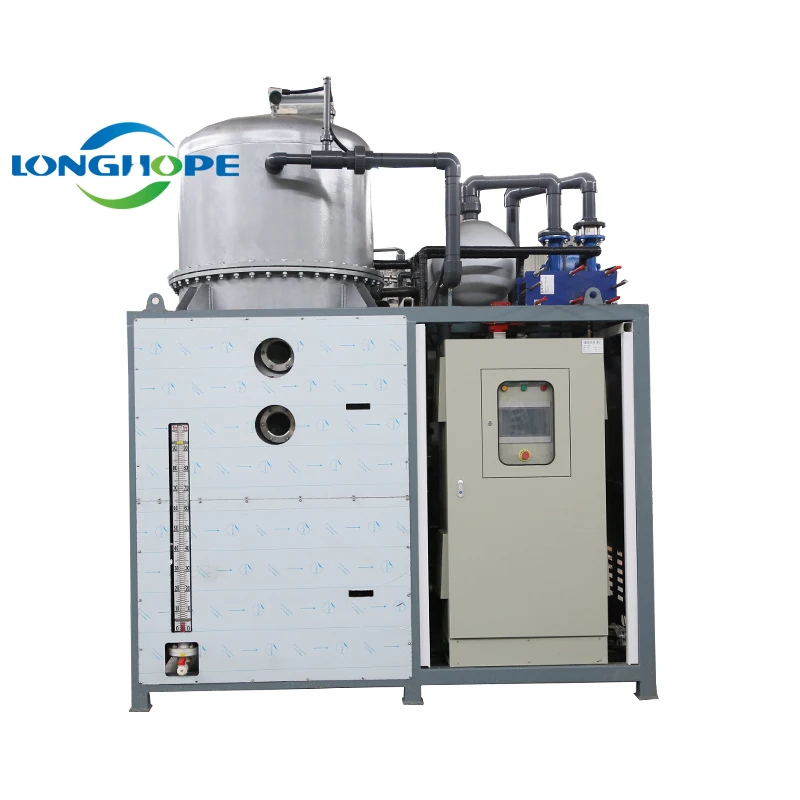
industrial concentration system
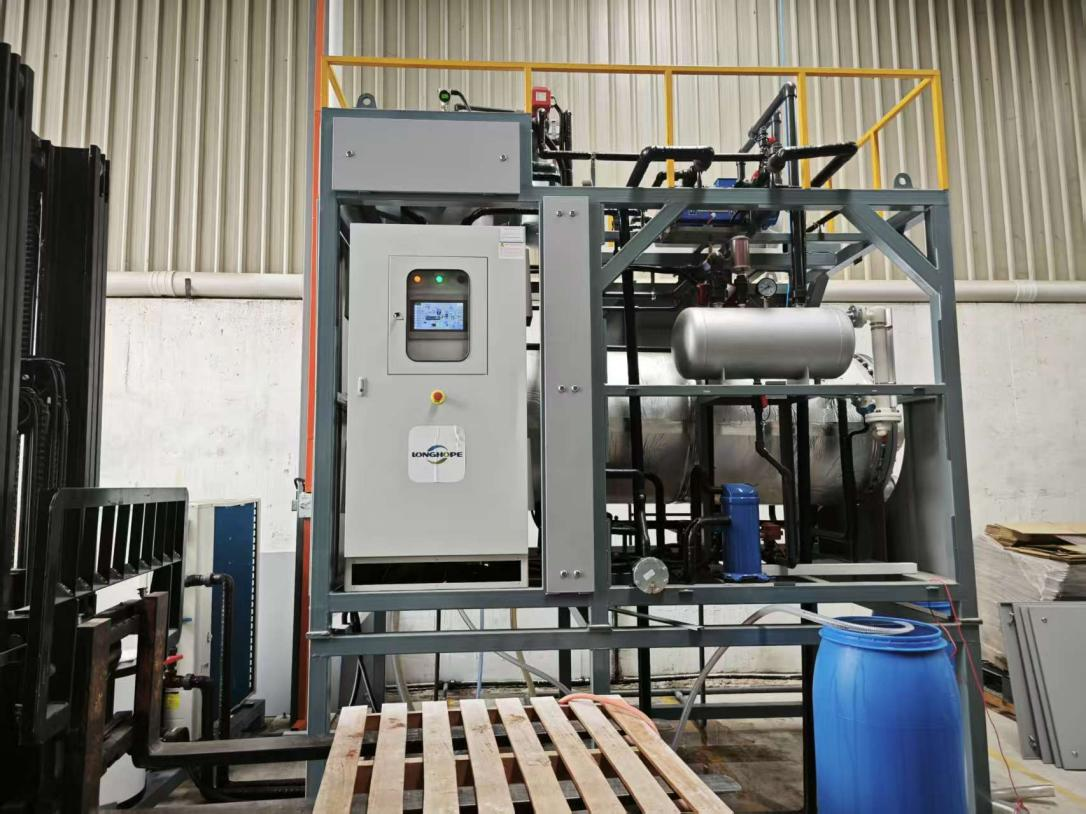
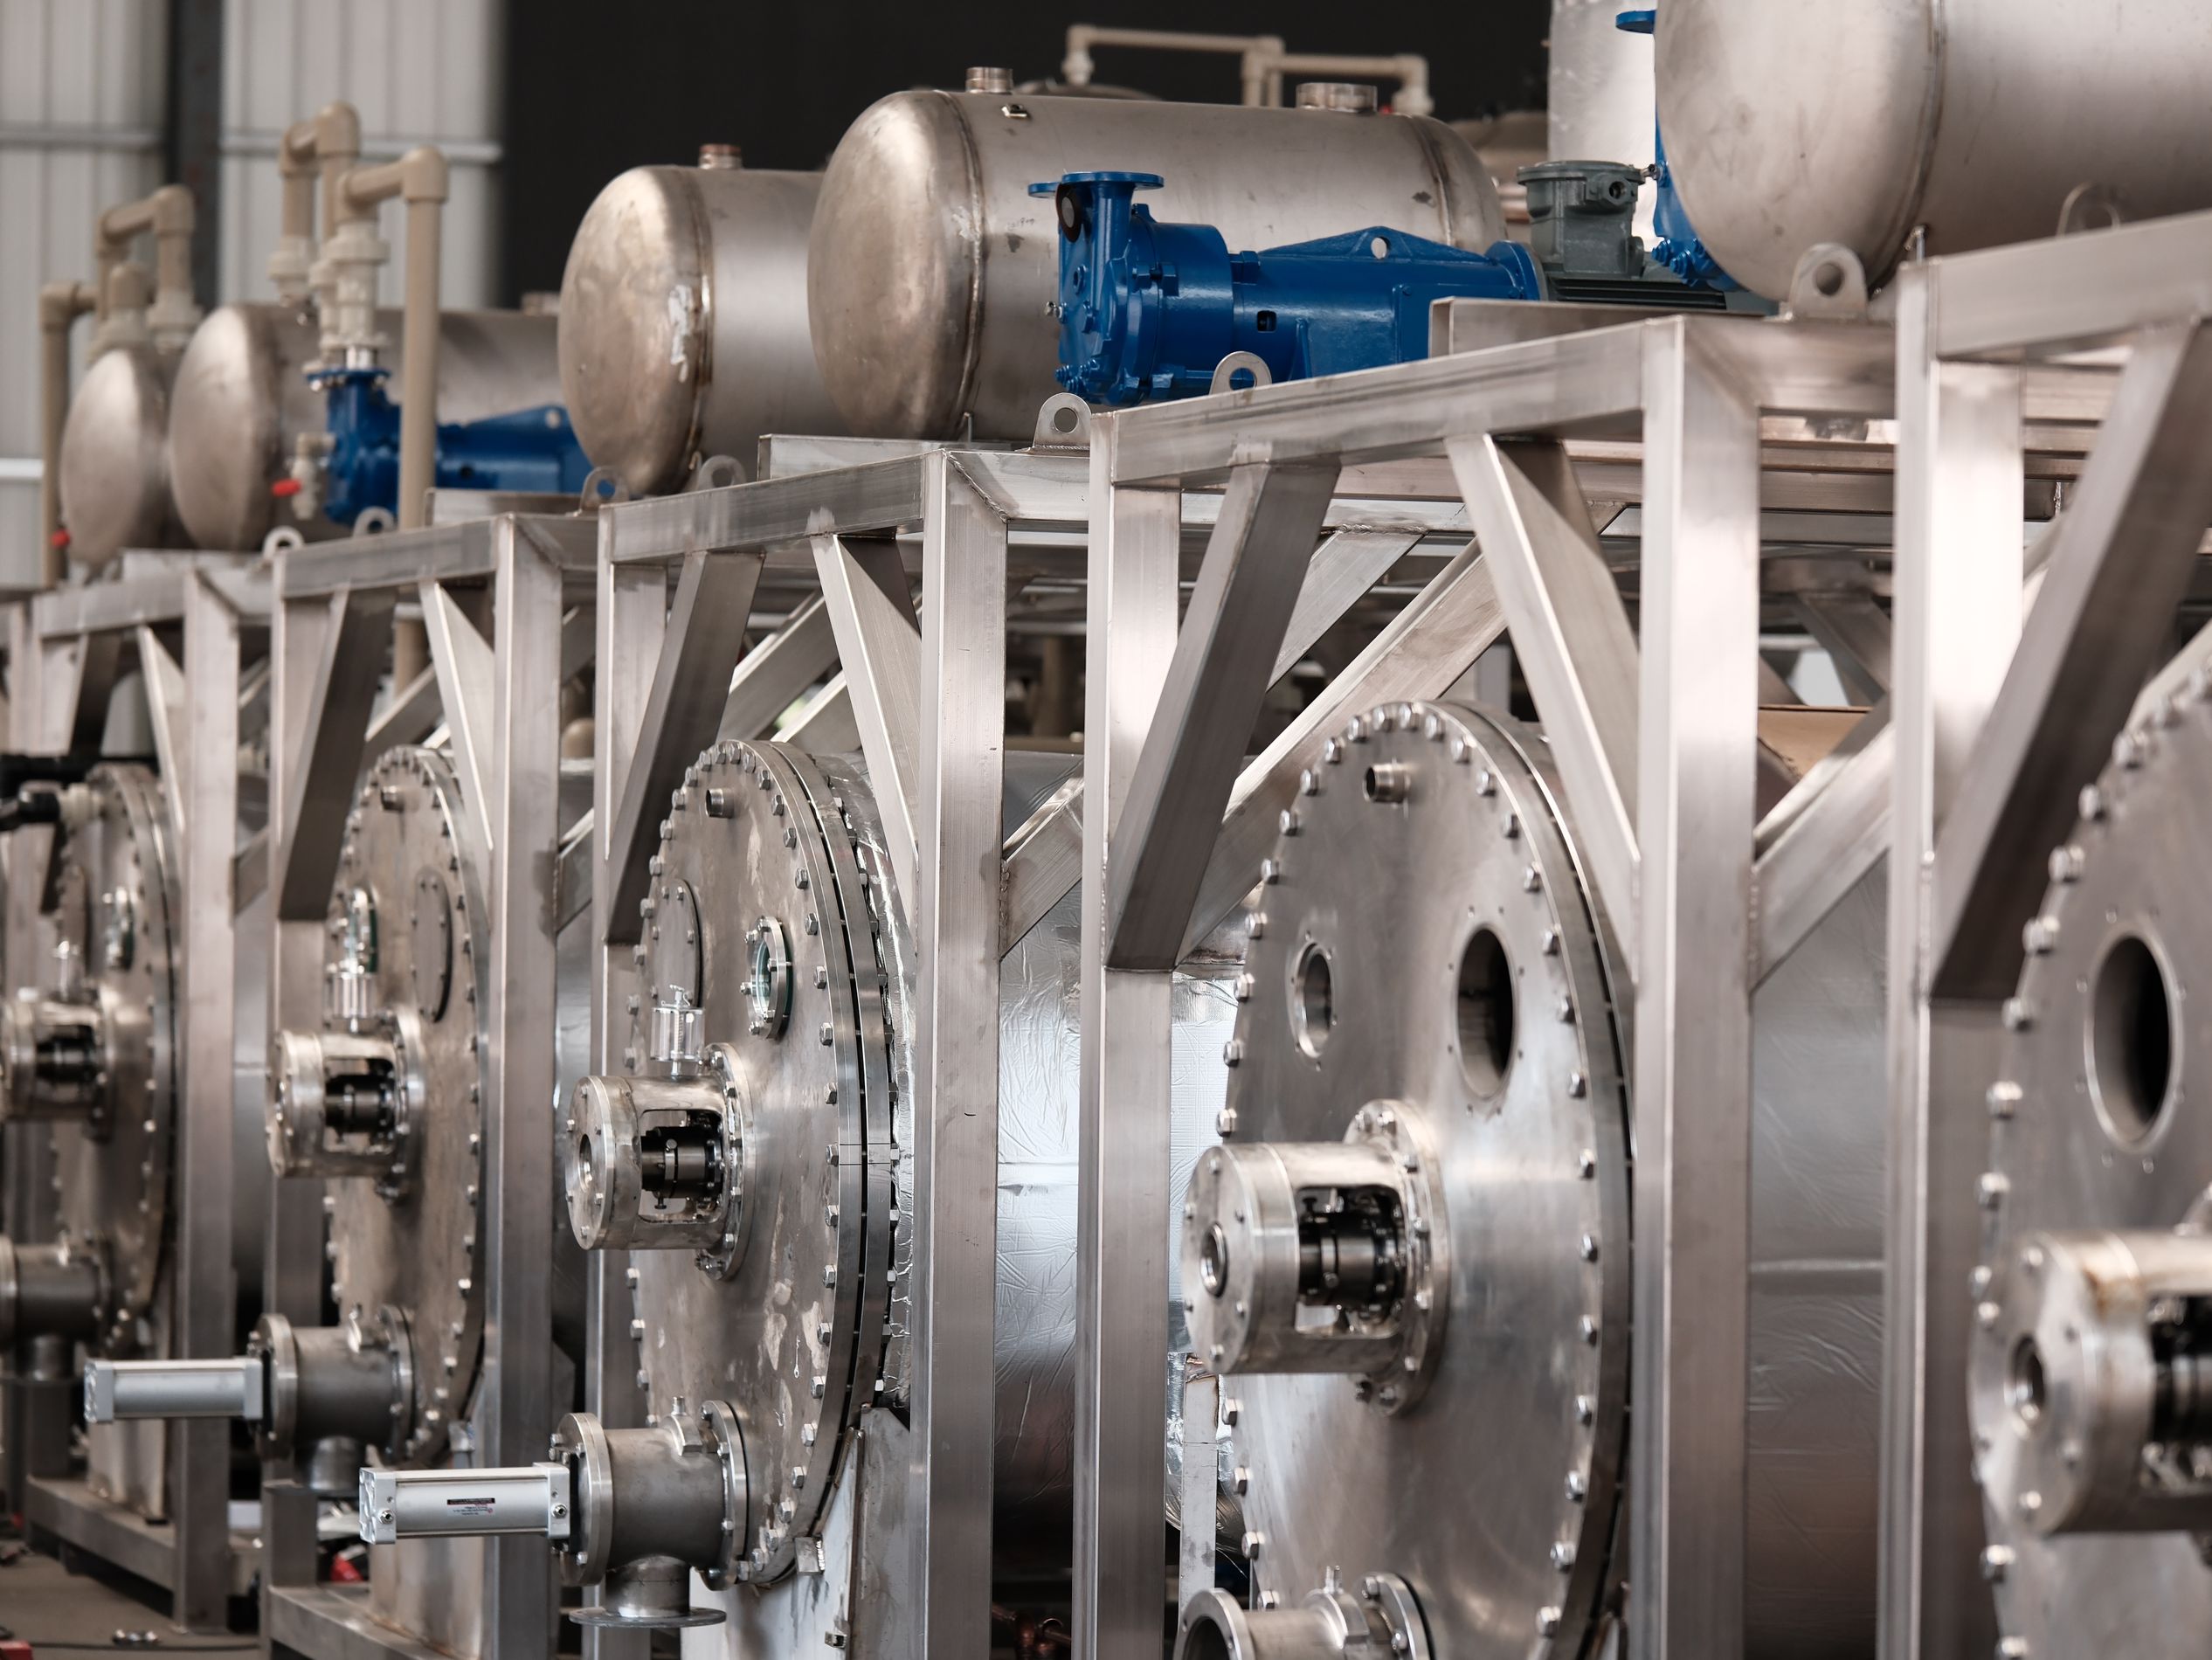
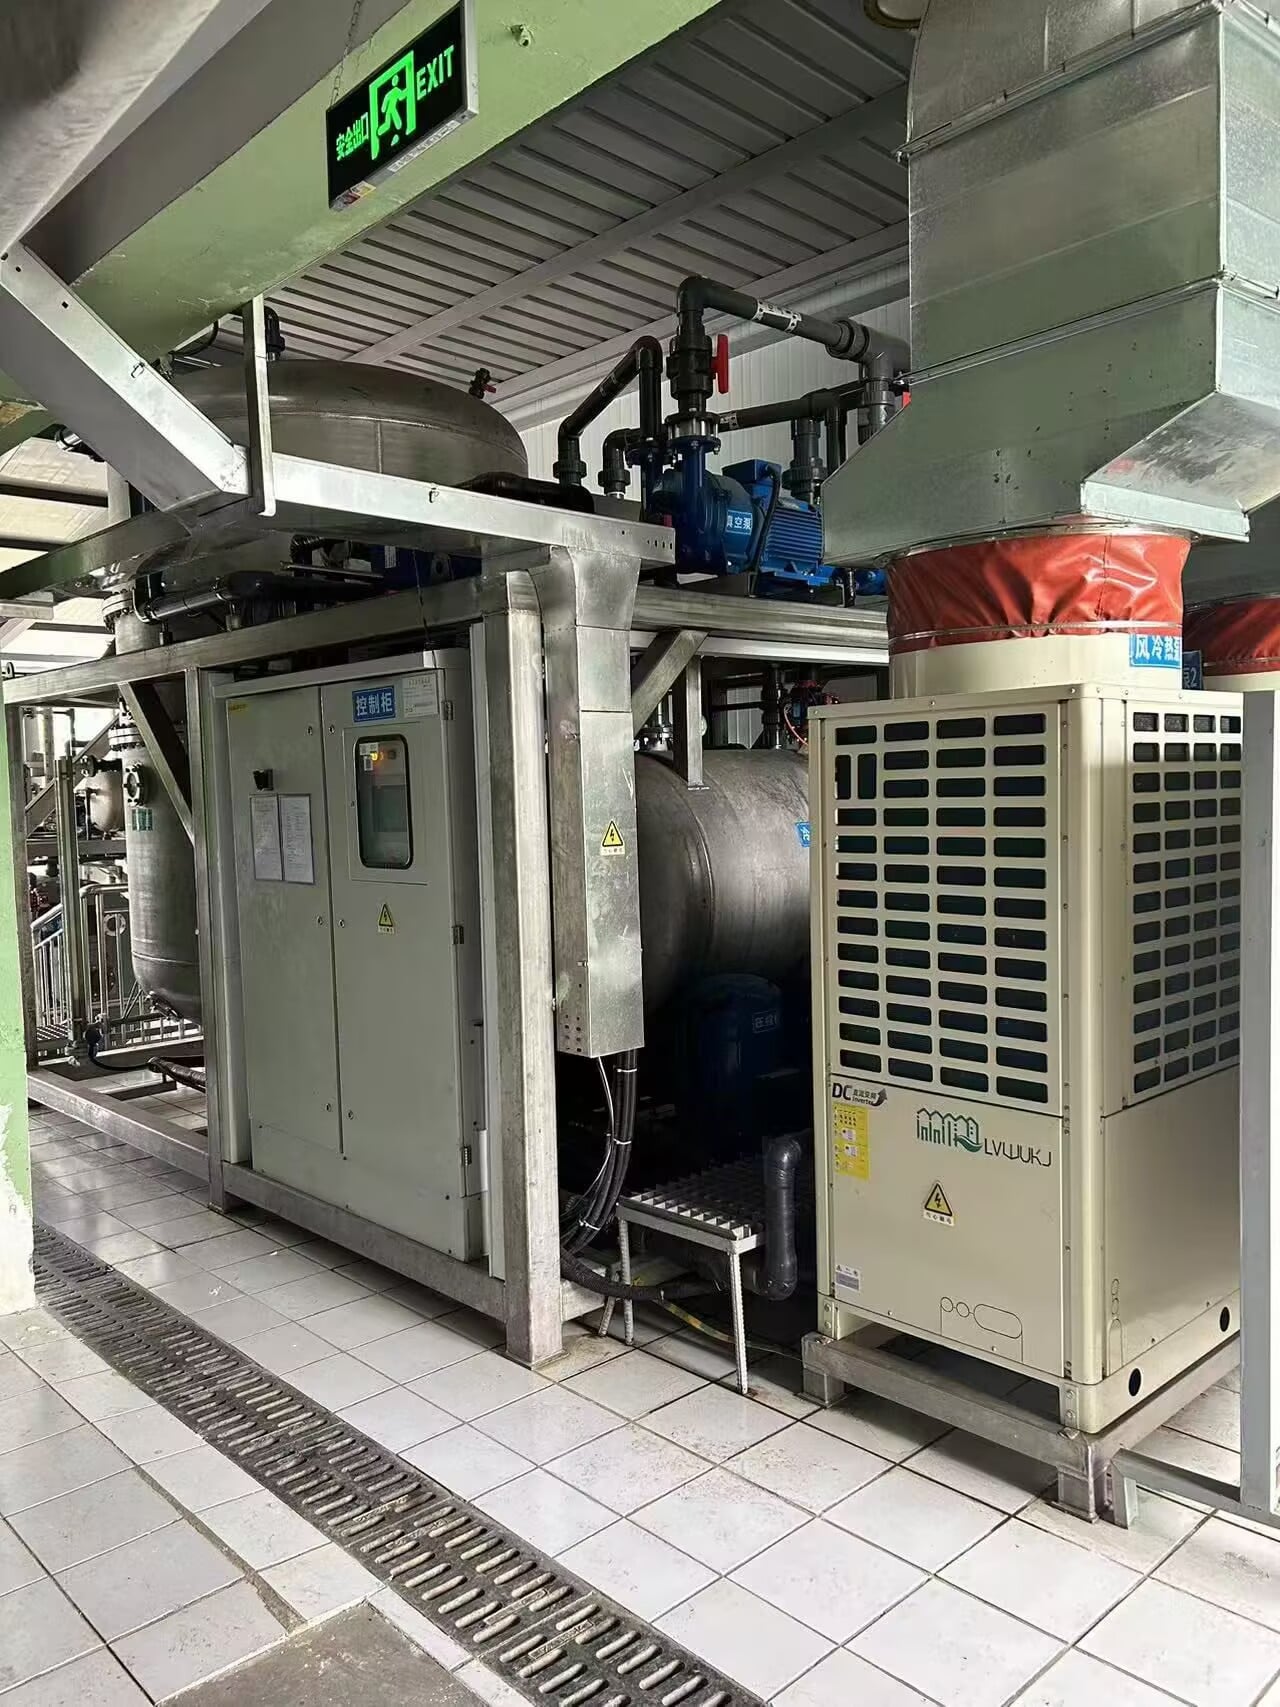
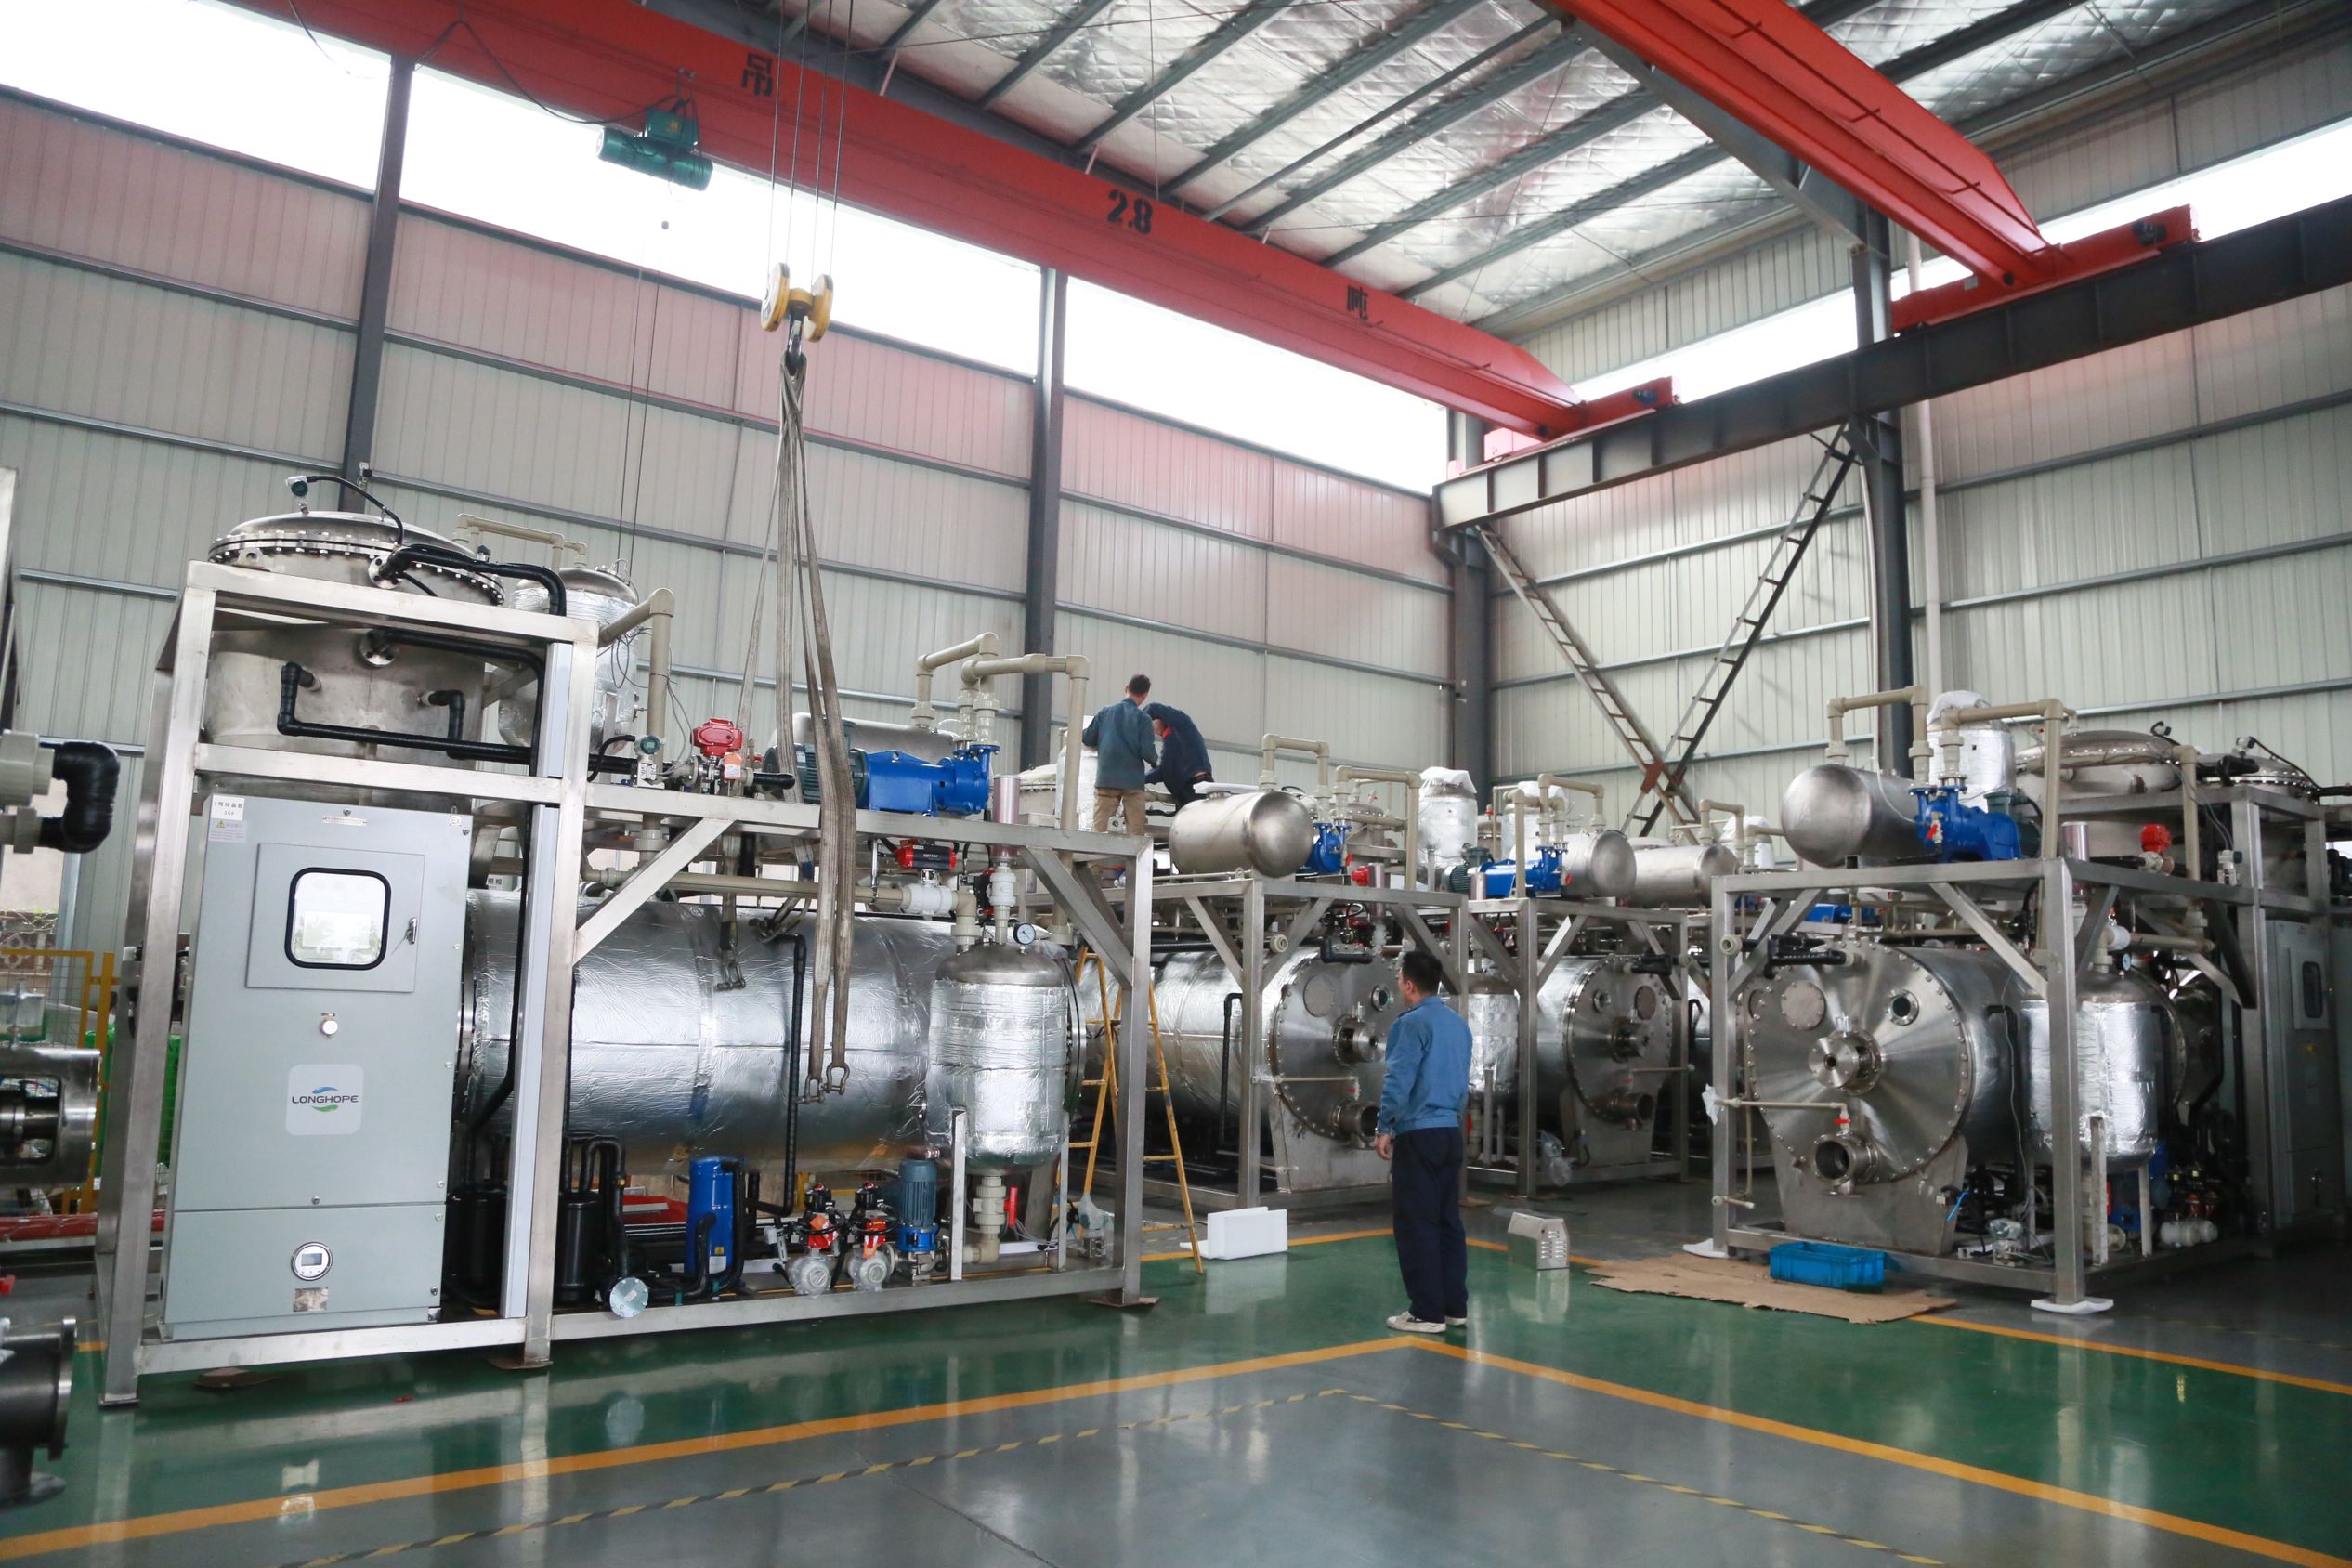
An industrial concentration system represents a sophisticated technological solution designed to separate, concentrate, and process materials efficiently within manufacturing environments. This industrial concentration system operates by utilizing advanced filtration, centrifugal, or evaporative technologies to extract valuable components from raw materials or waste streams. The primary functions of an industrial concentration system include material separation, waste reduction, product purification, and resource optimization across diverse industrial applications.
The technological features of an industrial concentration system incorporate automated monitoring systems, precision control mechanisms, and high-capacity processing capabilities. Modern industrial concentration system designs integrate real-time data analytics, allowing operators to optimize performance and maintain consistent output quality. These systems typically feature robust construction materials that withstand corrosive environments and continuous operation demands.
Applications for an industrial concentration system span multiple sectors, including chemical manufacturing, pharmaceutical production, food and beverage processing, wastewater treatment, and mining operations. The industrial concentration system proves particularly valuable in industries requiring precise material handling and regulatory compliance. Whether processing industrial liquids, separating solids from liquids, or concentrating valuable minerals, an industrial concentration system delivers reliable performance and measurable results, making it an indispensable component of modern industrial infrastructure and operational efficiency strategies.

 EN